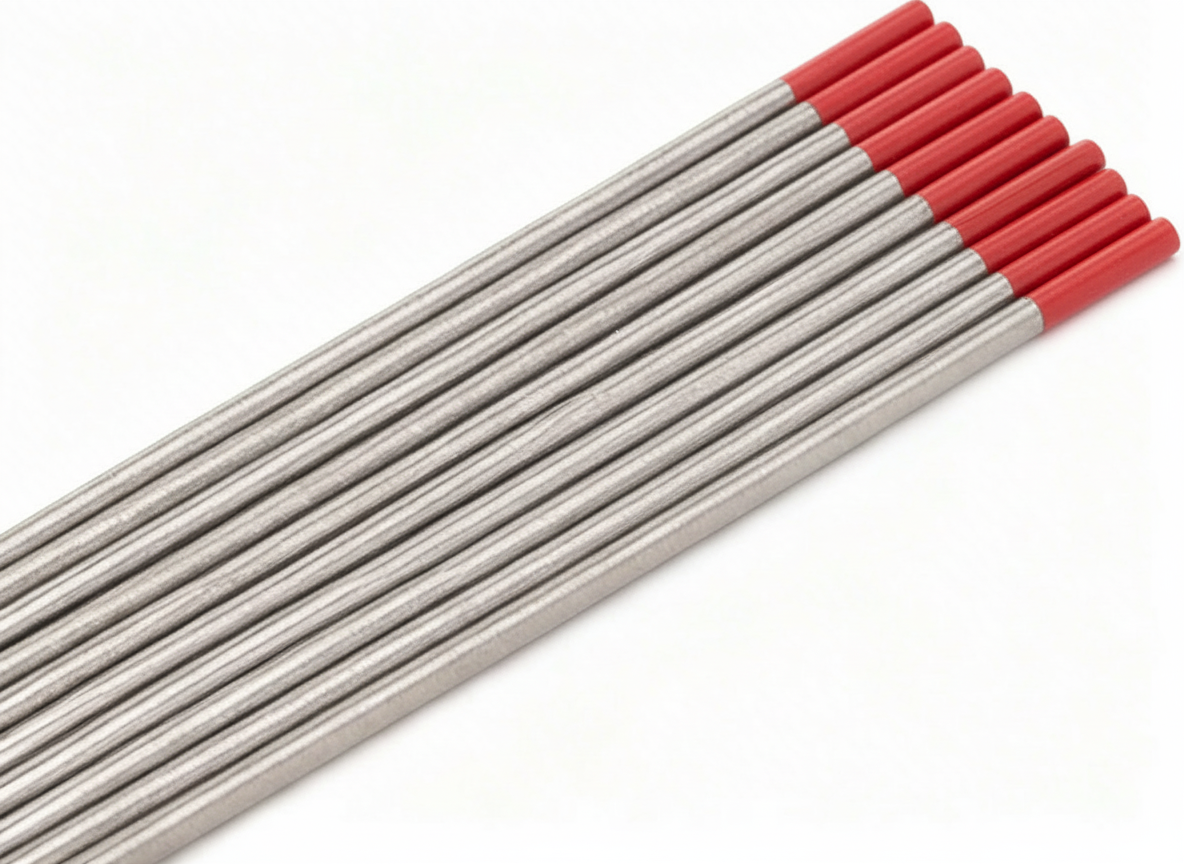

The CK T1167GT2 2% Thoriated Tungsten Electrode 1/16" X 7", 10 pack is a TIG support item that gets attention for arc starting and high-current use. Before buying it for a job, verify the actual process, polarity, amperage range, and any site rules for thoriated tungsten handling. Do not assume a tungsten electrode choice is correct just because it is common in the field.
Key Takeaways
- 2% thoriated tungsten is commonly selected when stable arc starting matters, but the correct choice depends on the job, power source, and operating practice.
- Use this electrode only after you verify the application, electrode prep method, and any shop or site restrictions on thoriated material.
- For unknown fit or procedure approval, use Unknown (Verify) rather than assuming compatibility.
- Buying by the 10-pack makes sense only if the diameter, length, and tungsten type match your standard setup.
What this electrode is used for
Based on the provided product summary, this is a 2% thoriated tungsten electrode in 1/16 in. by 7 in. format, supplied in a 10-pack. The source summary lists carbon steel, stainless steel, nickel alloy, titanium, and copper as materials welded. Treat that list as a source reference, not a site-wide approval. Actual suitability depends on the procedure, shielding gas, current type, torch setup, and work authorization.
For TIG operators, the main buying question is not only whether the tungsten will run, but whether it matches the exact welding condition in front of you. Check the following before you order or issue it from stores:
- Electrode diameter requirement: 1/16 in.
- Electrode length requirement: 7 in.
- Tungsten type permitted by the welding procedure or internal standard: Unknown (Verify) if not documented
- Current type in use: DC, AC, or mixed process conditions Unknown (Verify)
- Any restrictions on thorium-bearing consumables at the jobsite
Check, inspect, verify before purchase
- Check the job requirement. Confirm the procedure sheet, welder preference, or supervisor instruction for tungsten type and size.
- Inspect the torch setup. Verify collet, back cap, and torch body accept 1/16 in. electrodes. If the torch is configured for a different size, do not force the fit.
- Verify the amperage demand. The product summary says this electrode suits high current requirements. If the current is low or the arc is especially delicate, confirm whether another tungsten type is preferred.
- Check the tip prep practice. The summary also notes low-amperage AC use with a modified point. If your shop grinds or shapes tungsten differently, use the approved method for your procedure.
- Verify handling rules. Thoriated tungsten has handling and grinding considerations. Confirm local safety practice before using or dressing the electrode.
Troubleshooting support: when the tungsten choice is wrong
If the arc is unstable, starts poorly, or the tip deteriorates faster than expected, do not assume the tungsten is defective. Start with a process check.
- Check the polarity and current mode. Unknown (Verify) if the setup matches the electrode choice.
- Inspect the tip geometry. A point that is too blunt, too sharp, or unevenly ground can cause erratic starting.
- Verify gas coverage. Poor shielding can mimic tungsten problems.
- Check contamination. Contact with filler metal, base metal, or dirty work can ruin arc stability.
- Inspect the electrode size. A 1/16 in. tungsten may be too small for the current demand in some applications. Confirm against the procedure rather than guessing.
If the electrode is being selected for a new procedure, use a trial only after reviewing the welding procedure and any safety limits on thorium-bearing products. If your team does not have written guidance, stop at verification instead of proceeding on assumption.
Buying checks for maintenance and welding support teams
For stores and maintenance buyers, the main risk is issuing the right tungsten type in the wrong size. A 10-pack is only useful if your team actually runs 1/16 in. electrodes often enough to justify inventory. Before stocking, verify these points:
- Whether 1/16 in. is a standard shop size or an occasional use item
- Whether 7 in. length matches the torch hardware in service
- Whether operators are trained to handle thoriated tungsten safely
- Whether your facility allows thoriated tungsten in all work areas
- Whether an alternate tungsten type is preferred on some procedures
WSP lookup section
Use the Weld Support Parts tungsten lookup page as a starting point when confirming tungsten selection, but treat it as a reference tool rather than a procedure approval. If your team needs a broader tungsten cross-check, review the related guide here: TIG Welding Tungsten Electrodes 3/32" (WT20 Red Tip) – Specs, Safety & Buying Guide.
Filler metal finder section
This product is a tungsten electrode, not filler metal, so a filler metal finder does not approve or reject it directly. Still, if you are matching tungsten choice to a broader TIG setup, use the filler metal finder as a selection starting point only. Do not treat it as a guaranteed procedure approval. If your weld is low-amp or precision focused, another related reference may help: LaYZr Tungsten Electrode – Safer Precision for Low-Amp TIG Welding.
Safety notes
- Follow your site rules for thoriated tungsten handling and disposal.
- Avoid unnecessary dust exposure when grinding tungsten. Use the approved grinding method and local ventilation controls.
- Do not use a tungsten type just because it is familiar. Verify it against the procedure and application.
- If your operation has restrictions on thorium-bearing consumables, stop and confirm an approved alternative.
FAQ
Is the CK T1167GT2 suitable for every TIG job?
No. The source summary indicates it is useful for arc starting and higher current needs, but suitability still depends on the procedure, current mode, and shop rules. Unknown (Verify) where not documented.
Can I use this electrode for AC aluminum work?
Do not assume that from the product name alone. The summary mentions low-amperage AC applications with a modified point, but actual approval depends on your machine setup and procedure. Verify before use.
What should I check before stocking the 10-pack?
Confirm the 1/16 in. diameter, 7 in. length, operator training, and whether thoriated tungsten is allowed in your facility. Also verify that this size is actually used often enough to justify a 10-pack.
What if I need a different tungsten size?
Do not substitute without checking the torch hardware and welding procedure. If the size is not documented, mark it Unknown (Verify) and confirm with the welding lead or manufacturer guidance.
Sources Checked
- Provided ArcWeld product summary for CK T1167GT2 2% Thoriated Tungsten Electrode 1/16" X 7", 10 pack
- TIG Welding Tungsten Electrodes 3/32" (WT20 Red Tip) – Specs, Safety & Buying Guide
- LaYZr Tungsten Electrode – Safer Precision for Low-Amp TIG Welding
Related Arc Weld Part
CK T1167GT2 2% Thoriated Tungsten Electrode 1/16" X 7", 10 pack
2% Throriated Tungsten offers good arc starting and is ideal for high current requirements. It is also good for low-amperage AC applications using a modified point. It is composed of 97.3% Tungsten, 1.7%-2.2% Thorium, and .5% other. Materials Welded- Carbon Steel, Stainless Steel, Nickel Alloy, Titanium, and Copper. Package of 10
View at Arc Weld Store
Leave a Reply