
Tag: consumables

  • Hobart Handler 125 MIG Welder Support: Parts Lookup and Buying Checks

    Hobart Handler 125 MIG Welder Support: Parts Lookup and Buying Checks

    Hobart Handler 125 MIG Welder Support

    If you are supporting a Hobart Handler 125 in the shop, the goal is simple: confirm the machine configuration, match the wear items to the existing setup, and verify the part details before ordering. The Handler 125 is commonly serviced through a small set of support items: MIG gun, gas hose, regulator, drive roll, liners, tips, and related consumables. This guide is built as a buying and inspection checklist for maintenance teams and welders who need to keep the machine running without guessing.

    Key Takeaways

    • Start with the machine support page and verify the exact model before ordering parts.
    • Do not assume the gun, liner, or drive roll is correct based on appearance alone.
    • Check hose routing, gas delivery, tip size, and wire feed condition before replacing major parts.
    • Use filler metal pages as selection starting points only; they do not replace procedure approval.
    • When a detail is unclear, mark it as Unknown (Verify) and confirm against the machine, manual, or supplier support.

    Initial Support Check: What to Inspect First

    Before buying anything, inspect the welder as it sits in service. The most common mistake is replacing parts based on symptoms without checking the source of the fault.

    • Inspect the gun cable: look for kinks, damaged strain relief, or heat damage.
    • Inspect the contact tip: check for burnback, egged-out openings, or inconsistent wire stickout.
    • Inspect the drive roll: look for slippage, wire shaving, or incorrect groove profile.
    • Inspect the gas hose: check for cracks, loose fittings, or poor flow at the gun end.
    • Inspect the regulator and flow path: verify the gauge response and look for leaks.

    If the machine feeds erratically, separate the problem into three buckets: wire feed, gas delivery, and gun condition. That keeps you from replacing consumables when the drive system is actually at fault.

    Buying Checks for the Hobart Handler 125

    Use the Hobart Handler 125 support page as the first reference point for parts lookup and machine-specific checks:

    Hobart Handler 125 MIG Welder Support page

    That page references machine support items including the H-9D MIG gun, gas hose, regulator, drive roll, and consumable part links. Before you order, verify each item against the machine and any existing replacement parts already installed.

    • Check the gun model: verify whether the installed gun is the H-9D or another setup. Do not assume based on the handle or connector style.
    • Check the wire size used in service: confirm the wire diameter from the spool label or production record.
    • Check the drive roll groove: match the drive roll to the wire type and diameter. Exact groove details are Unknown (Verify) unless confirmed from the machine or parts listing.
    • Check regulator needs: confirm the gas type in use and verify whether the existing regulator is stable and leak-free.
    • Check gas hose length and fittings: confirm the installed hose routing and connection points before ordering a replacement.

    Troubleshooting Support by Symptom

    Wire feeds inconsistently

    • Check: drive roll tension, spool drag, and liner condition.
    • Inspect: the contact tip for wear and the gun cable for sharp bends.
    • Verify: the wire diameter and drive roll match the current setup.

    Arc starts poorly or tip burns back

    • Check: contact tip size and condition.
    • Inspect: the gun neck and internal wire path for debris or damage.
    • Verify: the wire feed speed and polarity settings for the application; settings are application-specific and may be Unknown (Verify) without the procedure sheet.

    Shielding gas coverage is unstable

    • Check: cylinder valve, regulator adjustment, and hose fittings.
    • Inspect: the hose for cuts, loose clamps, or leaks.
    • Verify: gas flow at the torch end using shop procedure and leak-check practice.

    Parts Lookup Workflow

    For maintenance buyers, the best workflow is to document the machine condition before the order is placed.

    1. Record the welder model and serial information from the machine plate.
    2. Identify the installed gun, hose, and regulator by visual inspection and any existing labels.
    3. Measure or confirm wire diameter from the active spool or production spec.
    4. Check the drive roll and tip for wear patterns that indicate the failure mode.
    5. Use the support page to compare the needed items with the machine-specific listing.
    6. Flag anything uncertain as Unknown (Verify) before purchase approval.

    This process reduces return orders and avoids downtime caused by ordering the wrong gun parts or consumables.

    Filler Metal Selection Starting Point

    When the job requires a new wire choice, use filler metal pages only as a starting point for selection, not as a guaranteed procedure approval. If you are matching stainless or aluminum wire to a job, confirm the base metal, shielding gas, and procedure requirements first.

    These pages help with wire selection logic, but they do not confirm weld procedure compliance, code acceptance, or application approval.

    Safety Notes

    • Lock out power before opening the machine or changing internal parts.
    • Bleed pressure safely before disconnecting any gas hose or regulator connection.
    • Use proper PPE when inspecting worn tips, wire ends, or damaged cable insulation.
    • Do not run a damaged gun cable or leaking gas system in production.
    • If a part fit is uncertain, stop and verify the part number or configuration first.

    FAQ

    How do I confirm the right replacement gun for a Hobart Handler 125?

    Check the machine support page, then compare the installed gun, cable connection, and visible labels. If the existing gun is not clearly identified, mark it Unknown (Verify) and confirm against the machine record or supplier support before ordering.

    What should I inspect before replacing the drive roll?

    Inspect the wire path, spool drag, liner condition, and contact tip. A worn tip or damaged liner can cause feed problems that look like a drive roll issue.

    Can I use the filler metal pages as procedure approval?

    No. Use them as selection starting points only. Final approval depends on the job requirements, base metal, shielding gas, and any applicable procedure or code requirements.

    What if I cannot confirm the hose or regulator details?

    Do not guess. Record the existing component information, take photos, and verify the exact configuration before purchase. Unknown (Verify) is the correct status until confirmed.

    Sources Checked

    Use the machine support page as the primary lookup reference, then verify the installed parts against the actual welder before placing an order.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

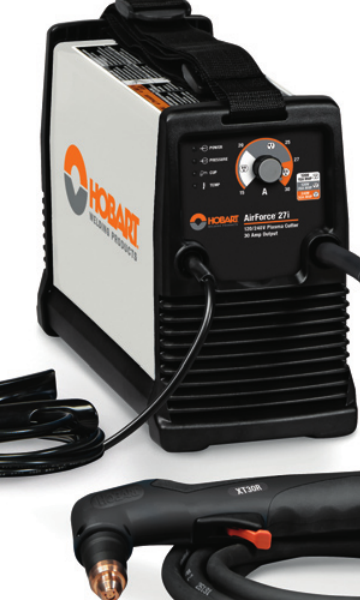
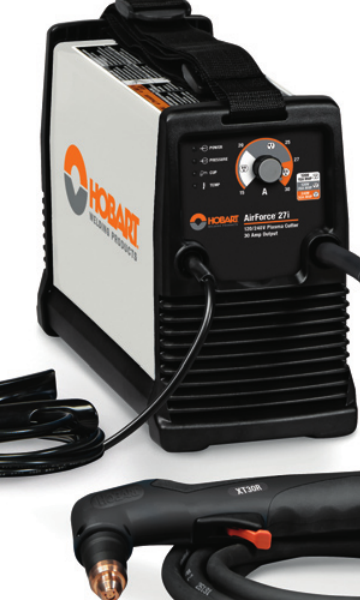
  • Hobart AirForce 27i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 27i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 27i Plasma Cutter Support

    If you maintain a Hobart AirForce 27i, the fastest way to avoid wrong-parts orders is to verify the machine identifier, torch family, power input, and air-side support items before you buy. The AirForce 27i support page from Weld Support Parts is set up as a lookup starting point for those checks. It lists the unit support page, the stock reference 500575, 120/240 V information, an XT30R replacement torch reference, consumables, MVP adapters, an air filter kit, cutting guides, and plasma support links.

    Key Takeaways

    • Use the support page to confirm the AirForce 27i parts path before ordering.
    • Verify torch model, consumable style, and power input at the machine nameplate and on the existing torch.
    • Air quality matters. Inspect the air filter path before troubleshooting arc problems.
    • Do not assume adapter or torch compatibility from appearance alone.
    • When details are unclear, mark them as Unknown (Verify) and confirm against the machine and torch labels.

    What the Support Page Is Useful For

    The Weld Support Parts AirForce 27i page is a parts lookup and support reference, not a substitute for the machine manual. It is useful when you need to match the cutter to support items such as the replacement torch, consumables, and air-side accessories. For this model, the page references stock 500575 and indicates 120/240 V support information. Treat those details as lookup cues and verify them on the machine before purchasing or installing parts.

    Open the Hobart AirForce 27i support page

    Buying Checks Before You Order Parts

    Before a maintenance buyer releases an order, do these checks in order:

    1. Check the machine data plate. Verify the exact model is Hobart AirForce 27i and confirm input power requirements. If the plate is unclear, record Unknown (Verify).
    2. Inspect the torch neck and handle label. Confirm whether the installed torch matches the XT30R family reference shown on the support page. Do not assume the torch is original.
    3. Pull the consumable set and compare wear patterns. Look at the nozzle, electrode, swirl ring, shield, and retaining parts. Replace only with the correct style for the torch in use.
    4. Check the air delivery path. Inspect filters, fittings, hoses, and water or oil contamination. A plasma cutter with poor air quality will often show unstable arc behavior.
    5. Confirm adapter needs. If the shop uses an alternate power plug or input arrangement, check whether the MVP adapter reference is relevant to your setup. Compatibility details not shown on the support page should stay Unknown (Verify).

    Troubleshooting and Support Checks

    Use these checks when the cutter starts to misbehave or when you are deciding which support part to buy.

    1) Torch and Consumable Check

    • Inspect: Look for heat damage, cracked cups, eroded electrodes, and loose retaining parts.
    • Verify: Match the torch consumables to the actual torch family on the machine. If the torch label is unreadable, mark the torch type Unknown (Verify) until confirmed.
    • Replace: Only the parts that are visibly worn or listed for the identified torch family.

    2) Air Supply Check

    • Inspect: Air filter kit condition, bowl contamination, hose leaks, and regulator settings.
    • Verify: The shop air is dry and clean enough for plasma use. If you see oil, water, or heavy debris, correct that before blaming the torch.
    • Check: Flow remains stable during trigger pull. A pressure drop can mimic a bad torch or bad consumable.

    3) Power and Input Check

    • Inspect: Input cord, plugs, adapters, and receptacle condition.
    • Verify: The machine is connected to the correct input class shown for the AirForce 27i support reference. If the exact electrical setup is not confirmed, note it Unknown (Verify).
    • Check: Any adapter or extension is rated and approved for the actual jobsite setup. Do not use an adapter just because the plug shape fits.

    4) Cut Quality Check

    • Inspect: Edge squareness, dross, and arc consistency.
    • Verify: The torch is held at a consistent standoff and travel speed.
    • Check: The cut guide or drag shield is appropriate for the work method you are using.

    WSP Lookup Page Notes

    The AirForce 27i support page is the correct first stop when you need a parts and support overview for this machine. It identifies the machine support page, stock 500575, the XT30R replacement torch reference, consumables, MVP adapters, air filter kit, cutting guides, and other plasma support links. Use those references to narrow the search, then confirm exact fitment against the machine and torch markings.

    Important: This page is a selection aid, not a blanket approval for every installed torch or accessory. If the part family is not confirmed from labels or existing component markings, the correct status is Unknown (Verify).

    Go to the Hobart AirForce 27i support page

    Practical Inspection Routine for Shops

    For routine maintenance, use a short inspection routine before each parts order or service ticket:

    • Record the machine model and serial tag information.
    • Compare torch markings to the support page reference.
    • Pull the last installed consumables and note wear pattern.
    • Inspect air filters and moisture traps.
    • Check the power plug, adapters, and cord strain relief.
    • Confirm any cutting guides or accessories are intended for the actual torch setup.

    Safety Notes

    • De-energize the machine before inspecting internal or electrical components.
    • Bleed pressure from the air system before opening filters or fittings.
    • Do not touch hot consumables immediately after cutting.
    • Use eye, hand, and body protection suitable for plasma cutting and grinding cleanup.
    • Do not bypass safety devices or use unverified adapters in an attempt to make a part fit.

    FAQ

    Is the XT30R replacement torch definitely the correct torch for every AirForce 27i?

    No. The support page references XT30R as a replacement torch reference, but you should still verify the torch family on the machine and existing torch. If the installed torch is not confirmed, mark it Unknown (Verify).

    Can I order consumables just by machine model?

    Not safely. Consumables must match the actual torch family and installed setup. Start with the AirForce 27i support page, then verify the torch label and worn parts before ordering.

    What should I check first if the cutter will not make a stable arc?

    Start with the consumables and the air supply. Inspect electrode and nozzle wear, then verify that air is clean, dry, and steady. If those checks are inconclusive, move to power input and torch condition.

    Are the MVP adapters universal?

    Do not assume that. The support page lists MVP adapters as a support reference, but any actual compatibility must be confirmed against the machine and power setup. If it is not confirmed, use Unknown (Verify).

    Sources Checked

    For maintenance teams, the key is simple: verify the machine, verify the torch, verify the air, then buy the parts that match what is actually installed. That is the cleanest way to support a Hobart AirForce 27i without creating avoidable returns or downtime.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • 000-069 Miller Style M-Series Contact Tip .045 – Arc Weld by Masterweld Pack of (25): Replacement Part Breakdown

    Choosing the right contact tip is basic maintenance, but it affects wire feed stability, arc consistency, and how often you have to stop and correct a problem. This guide covers the 000-069 Miller Style M-Series Contact Tip .045 – Arc Weld by Masterweld Pack of (25) as a replacement part item for MIG welding support workflows. The key point is simple: treat this as a consumable fitment decision, not a guess. If the gun, neck, diffuser, or thread pattern is not verified, do not assume interchangeability.

    Key Takeaways

    • A .045 contact tip must match the wire size you are actually running.
    • “Miller Style M-Series” is a fitment description, not a guarantee for every Miller gun or every third-party gun labeled similar.
    • Contact tips wear from heat, spatter, and wire friction. A worn tip can look minor and still cause feed issues.
    • If fit, thread, or gun series is uncertain, mark it Unknown (Verify) and inspect before installation.

    What this part is used for

    A contact tip transfers welding current to the wire and helps guide that wire into the puddle. In practical terms, it is a wear part that sits at the front of the gun and takes abuse from heat and spatter. When it is correct and clean, wire feed is smoother. When it is damaged or the bore is oversized, undersized, or contaminated, you may see erratic feed, burnback, or a wandering arc.

    The product name indicates .045 diameter and a Miller style M-Series fitment. That is the starting point for selection only. Verify the gun model, tip threading, diffuser style, and wire diameter before using it in production.

    Check, inspect, verify before installation

    1. Check the wire size. Confirm the wire being used is .045. Do not install a .045 tip on a different wire size without a documented procedure.
    2. Inspect the thread and shoulder. Compare the new tip to the removed tip. Verify thread pattern, length, and seat profile. If anything does not match, stop and label it Unknown (Verify).
    3. Verify gun compatibility. Confirm the gun and front-end parts are truly Miller M-Series style. “Style” language can be broad. Do not assume cross-compatibility.
    4. Check for spatter damage. If the old tip has heavy spatter buildup, inspect the diffuser and nozzle as well. A bad tip is often only one part of a larger front-end issue.
    5. Clean the mounting surface. Wipe the diffuser threads and seating area before installing the replacement tip.

    Troubleshooting and support

    If the wire feed becomes inconsistent after a tip change, work through the front-end items in order.

    • Check: Is the wire size actually .045? Mixed wire and tip sizes create drag or chatter.
    • Inspect: Is the tip bore worn, burned, or partially blocked with spatter?
    • Verify: Is the tip fully seated and tightened correctly without over-torquing?
    • Check: Is the liner condition acceptable, or is the problem upstream in the gun cable?
    • Inspect: Are the drive rolls set correctly for the wire type and diameter?
    • Verify: Is the nozzle clear enough that spatter is not overheating the tip?

    Common symptoms tied to a contact tip problem include burnback, intermittent arc starts, birdnesting caused by feed resistance, and a rough or unstable arc. Do not replace one front-end part and assume the rest of the system is good. Support teams should inspect the tip, diffuser, nozzle, liner, drive rolls, and gun cable as a set.

    Product and parts notes

    This item is listed as an Arc Weld by Masterweld replacement part pack of 25 under ASIN B07Y41NL57. That tells you the part is being marketed as a consumable replacement item, but it does not replace verification of fit. Use the product listing only as the source of the provided item name. Do not assume the part is approved for every Miller or Miller-style setup.

    For purchasing workflows, the important questions are practical:

    • Does the gun front end take a Miller-style M-Series tip?
    • Is the current wire diameter .045?
    • Is the replacement tip shape and thread the same as the removed tip?
    • Has the surrounding front-end hardware been inspected for wear?

    If any answer is uncertain, classify the fit as Unknown (Verify) and confirm against the actual gun and front-end parts in the shop.

    How maintenance buyers should evaluate the part

    Maintenance buyers usually need consistency, not just a part number. This means confirming the existing gun fleet, wire sizes in use, and whether a single front-end standard is being held across multiple machines. If the shop runs mixed guns or mixed consumables, keep replacement tips separated by verified fitment, not by appearance alone.

    When a tip pack is received, log the following before issuing it:

    • Gun model verified against shop equipment
    • Wire diameter verified as .045
    • Thread/seat style matched to the removed part
    • Front-end wear condition recorded

    This reduces false troubleshooting. Many feed complaints are not caused by the tip alone. They are caused by a worn liner, wrong drive roll groove, poor cable routing, or a dirty gun neck.

    Safety notes

    • Lock out the welding power source before handling front-end consumables during maintenance.
    • Allow the gun and tip to cool before removal. Contact tips can retain heat long after welding stops.
    • Wear gloves when removing spatter-damaged parts. Sharp slag and hot metal can cut or burn.
    • Do not force a tip onto a mismatched diffuser or thread pattern.
    • Use only verified consumables in production work. If fitment is uncertain, stop and inspect.

    FAQ

    Q1: Is this contact tip automatically correct for every Miller MIG gun?
    No. The listing says Miller style M-Series, but that is not a blanket compatibility claim. Verify the actual gun model and front-end parts.

    Q2: Why does a worn contact tip cause wire feed trouble?
    Wear enlarges the bore and changes wire guidance. That can produce unstable current transfer, burnback, or erratic feed.

    Q3: Can I use this tip if my wire is not .045?
    No. The listed size is .045. Using another wire size without verification can create feed problems and poor arc performance.

    Q4: What should I check if a new tip does not seat correctly?
    Check the thread pattern, diffuser fit, seating surface, and the removed tip as a reference. If the match is uncertain, mark it Unknown (Verify).

    Sources Checked

    Note: No WSP lookup page or filler metal finder page was provided for this draft, so no selection-link section was included.

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

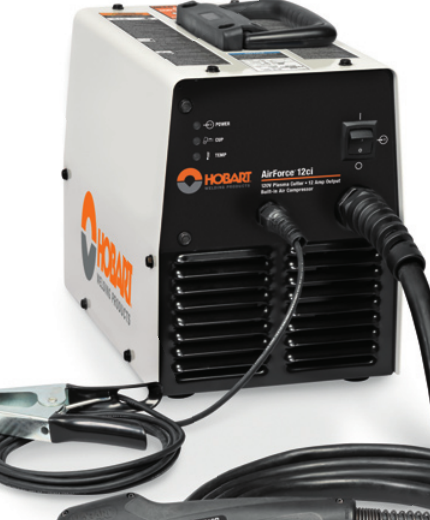
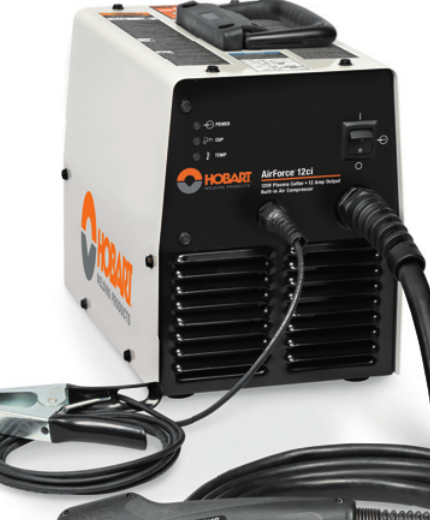
  • Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 12ci Plasma Cutter Support

    The Hobart AirForce 12ci is a compact plasma cutter support case where the buying risk is usually not the cutter itself, but the parts that keep it running: torch fitment, consumables, protective gear, and whether the replacement item matches the machine’s input and torch family. This guide is built to help welders, fabricators, and maintenance buyers verify the basics before ordering.

    Key Takeaways

    • Use the Hobart AirForce 12ci support page as the first parts reference before you buy.
    • Verify torch model, consumable type, and input power before ordering any replacement item.
    • Do not assume a plasma torch, consumable kit, or cover fits because it looks similar.
    • Check wear items first: nozzle, electrode, shield, swirl ring, retaining parts, air supply, and cable condition.
    • Safety glasses and a protective cover are support items, not optional extras.

    Start with the WSP lookup page

    The primary support page for this unit is here: Hobart AirForce 12ci Plasma Cutter Support. The page indicates stock 500564 and lists 120 V specs, XT12R replacement torch, consumable kits, safety glasses, and a protective cover. Treat those listings as the starting point for verification, not as a substitute for checking your exact machine and torch tag.

    Check before you order

    • Inspect the machine label: confirm the model is Hobart AirForce 12ci, not a similar unit.
    • Verify input power: the support page shows 120 V specs. Confirm your unit nameplate and outlet setup match.
    • Inspect the torch tag: confirm whether the unit uses the XT12R replacement torch listed on the support page.
    • Check consumable wear: look for recessed electrode, enlarged nozzle orifice, heat damage, cracks, or unstable arc start.
    • Verify cable and lead condition: cuts, melted sections, or loose strain reliefs can mimic consumable failure.

    Troubleshooting and support checks

    If the cutter is not performing well, the fastest path is a basic inspection sequence. Start simple and document what you find.

    1) No start or weak start

    • Check: power source status, plug condition, and supply voltage at the receptacle.
    • Inspect: trigger switch, torch lead, and any visible torch damage.
    • Verify: the consumables are installed correctly and are not worn beyond serviceable condition.

    2) Arc starts but cut quality is poor

    • Check: air pressure and air quality at the cutter.
    • Inspect: nozzle, electrode, shield, and retaining parts for spatter buildup or heat distortion.
    • Verify: the work clamp is clean and attached to bare metal.

    3) Arc drops out during cutting

    • Check: thermal condition of the machine and duty cycle usage pattern.
    • Inspect: torch lead for intermittent breaks or damaged insulation.
    • Verify: the air supply is steady and dry. Moisture can cause unstable operation and consumable damage.

    4) Consumables wear too quickly

    • Check: cutting technique, standoff distance, and travel speed.
    • Inspect: whether the nozzle is being run beyond normal wear indicators.
    • Verify: you are using the correct consumable kit for the torch family. If uncertain, use Unknown (Verify) until the exact kit is matched.

    Parts lookup buying checks for this model

    For the Hobart AirForce 12ci, the most useful parts categories are torch replacement, consumable kits, and protective items. The support page points to an XT12R replacement torch, but buyers should verify the torch family, connector style, and lead length against the existing machine before ordering. Unknown (Verify) should be used for any detail that is not confirmed by the machine label or the support page.

    Replacement torch check

    • Inspect: the old torch for model markings, connector type, and damage location.
    • Verify: the new torch is listed for the same support page and matches the original torch family.
    • Confirm: no modification is required for fitment unless the manufacturer states otherwise.

    Consumable kit check

    • Inspect: all wear components removed from the torch.
    • Compare: thread shape, size, and seating surfaces.
    • Verify: the kit is intended for the same torch model, not just a similar plasma system.

    Protective gear and cover

    • Check: whether the shop already stocks plasma-rated eye protection.
    • Inspect: the machine’s storage location for dust, slag, and moisture exposure.
    • Verify: a protective cover will not trap heat when the machine is warm after use.

    Use the internal guides as support references

    If the cutter is giving you symptoms beyond basic wear, these related articles can help narrow the fault before you order parts:

    Safety notes

    • Disconnect power before inspecting torch leads, consumables, or internal connections.
    • Use eye protection and hand protection when checking the torch or removing worn parts.
    • Do not use damaged leads, cracked torch bodies, or loose consumable assemblies.
    • Verify ventilation and keep flammables clear of the cutting area.
    • If a part fitment is uncertain, mark it Unknown (Verify) and confirm through the machine label, torch tag, or support listing before use.

    FAQ

    What should I verify first for Hobart AirForce 12ci parts?

    Verify the machine model, input power, and torch family first. Then check consumables, cable condition, and air supply quality.

    Is the XT12R replacement torch listed on the support page the correct part for every unit?

    Unknown (Verify). The support page lists XT12R, but you should confirm the torch tag and connector style on your specific machine before ordering.

    How do I know if the problem is consumables or the torch?

    Inspect the nozzle, electrode, and shield first. If wear is visible or the arc is unstable, consumables are often the first suspect. If the lead, trigger, or torch body is damaged, the torch may need replacement.

    Can I buy based on similar-looking plasma parts?

    No. Similar appearance does not confirm fitment. Match the part to the support page and the machine tag, then verify before purchasing.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • Hypertherm 851462 Powermax30 AIR Essential Consumable Kit: Replacement Part Breakdown

    The Hypertherm 851462 Powermax30 AIR Essential Consumable Kit is a replacement-part purchase, not a process-change item. Buyers usually need it to keep a handheld plasma system ready for service, reduce downtime, and restore cut quality after normal wear. For support teams and maintenance buyers, the practical question is simple: what is included, what wears first, and what should be checked before the kit is installed?

    This guide focuses on part-level verification and field-use checks. It does not assume any unlisted compatibility beyond the product name provided. If you are matching a machine, torch, or cartridge configuration, verify every identifier against your system documentation before ordering or installation.

    Key Takeaways

    • This is an essential consumable kit for a Powermax30 AIR setup; treat it as wear-part support.
    • Consumables are normal replacement items. Poor cut quality is often a wear issue, not a machine failure.
    • Before use, verify torch model, retaining hardware, and electrode/nozzle condition against your current parts.
    • If the kit contents are not fully confirmed from your source listing, mark the unclear items as Unknown (Verify).
    • Do not force-fit plasma consumables. If the stack-up does not match, stop and confirm the part numbers.

    What to Check Before You Order

    For a consumable kit, the safest buying method is to confirm three points first:

    • Machine identity: confirm the exact plasma unit and torch family in service.
    • Consumable style: confirm whether your torch uses the same electrode, nozzle, shield, and retaining arrangement as the kit you are sourcing.
    • Wear pattern: inspect your current parts and compare the wear to the symptoms on the floor.

    Check: Look for arc instability, rough edge quality, excessive dross, or difficulty transferring arc. These are common reasons crews replace consumables early.

    Inspect: Remove the current tip stack and inspect for pitting, distortion, heat damage, or gas-flow contamination. Examine the torch body for damage that would shorten consumable life.

    Verify: Match the replacement parts to the exact service documents or parts diagram for your setup. If a component cannot be confirmed from the source listing, list it as Unknown (Verify).

    Replacement-Part Breakdown

    The product is identified as an essential consumable kit. That means the useful breakdown is functional, not speculative. In plasma service, the common wear components are typically the electrode, nozzle, shield or deflector, and retaining components. However, the exact contents of this kit should be confirmed from the source listing or packaging.

    • Electrode: Carries the arc load and is a primary wear item.
    • Nozzle: Shapes the arc and affects cut quality and kerf consistency.
    • Shield/deflector: Helps protect the torch and can influence cut standoff behavior.
    • Retaining hardware: Holds the consumable stack in position. Any damage or thread wear can affect retention.

    If the kit contents are not explicitly confirmed by your purchase source, do not assume the stack includes every item above. Mark unknown contents as Unknown (Verify) and cross-check the carton or listing before dispatching it to the field.

    Troubleshooting and Support Checks

    When a plasma cutter starts cutting poorly, do not jump straight to machine repair. Consumables are the first inspection point.

    Check: Inspect the nozzle orifice for enlargement, oval wear, or spatter contamination.

    Inspect: Examine the electrode face for a deep pit or uneven erosion.

    Verify: Confirm that the shield and retaining parts are not cracked, cross-threaded, or seated incorrectly.

    Check: If the arc starts but cuts are inconsistent, verify air quality, line pressure at the machine, and the condition of the consumable stack.

    Inspect: Look for moisture, oil, or debris in the air line and filter path. Contaminated air shortens consumable life.

    Verify: Make sure the torch is assembled in the correct order. A mis-stacked consumable set can create the same symptoms as a worn part.

    Check: If you see repeated consumable burn-back, inspect duty cycle and operating technique.

    Inspect: Review cut travel speed, pierce height, and standoff consistency.

    Verify: Confirm that the operator is using the correct technique for the workpiece thickness and edge condition.

    Product and Parts Section

    Product referenced: Hypertherm 851462 Powermax30 AIR Essential Consumable Kit

    ASIN: B01CSBV3FE

    Amazon affiliate product reference:

    No products found.

    Use this product as a replacement consumable source only. Do not assume it changes the procedure, the duty cycle, or the machine configuration. If your maintenance program requires serialized parts control, record the kit identification and the installation date when the parts are issued.

    Part verification step:

    1. Confirm the machine and torch model in service.
    2. Open the existing consumable stack and compare wear against the replacement parts.
    3. Verify that each part matches the required stack order.
    4. Install only after fit and seating are confirmed.
    5. Test cut on approved scrap material before returning the unit to production.

    Safety Notes

    • De-energize the system before service.
    • Allow hot parts to cool before handling.
    • Wear eye protection and gloves during inspection and replacement.
    • Do not touch electrode or nozzle surfaces with bare hands if contamination control is required by your shop practice.
    • Use approved torch and machine procedures only. Unknown (Verify) settings should not be guessed in the field.

    FAQ

    Q: Is this kit for routine maintenance or repair?
    A: Routine maintenance. Consumables are wear parts and are replaced as performance declines.

    Q: Can I assume the kit fits every Powermax30 system?
    A: No. Verify the exact machine and torch configuration before ordering. Compatibility details not confirmed in the source should be treated as Unknown (Verify).

    Q: What causes consumables to wear out early?
    A: Common causes include poor air quality, incorrect cut technique, excessive pierce abuse, and contaminated or damaged torch components.

    Q: What should I do if the replacement parts do not match my existing stack?
    A: Stop and verify the part numbers against the machine manual, torch diagram, or current packaging before installation.

    Sources Checked

    Note: No raw Amazon URL was used. Any unconfirmed content details remain Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

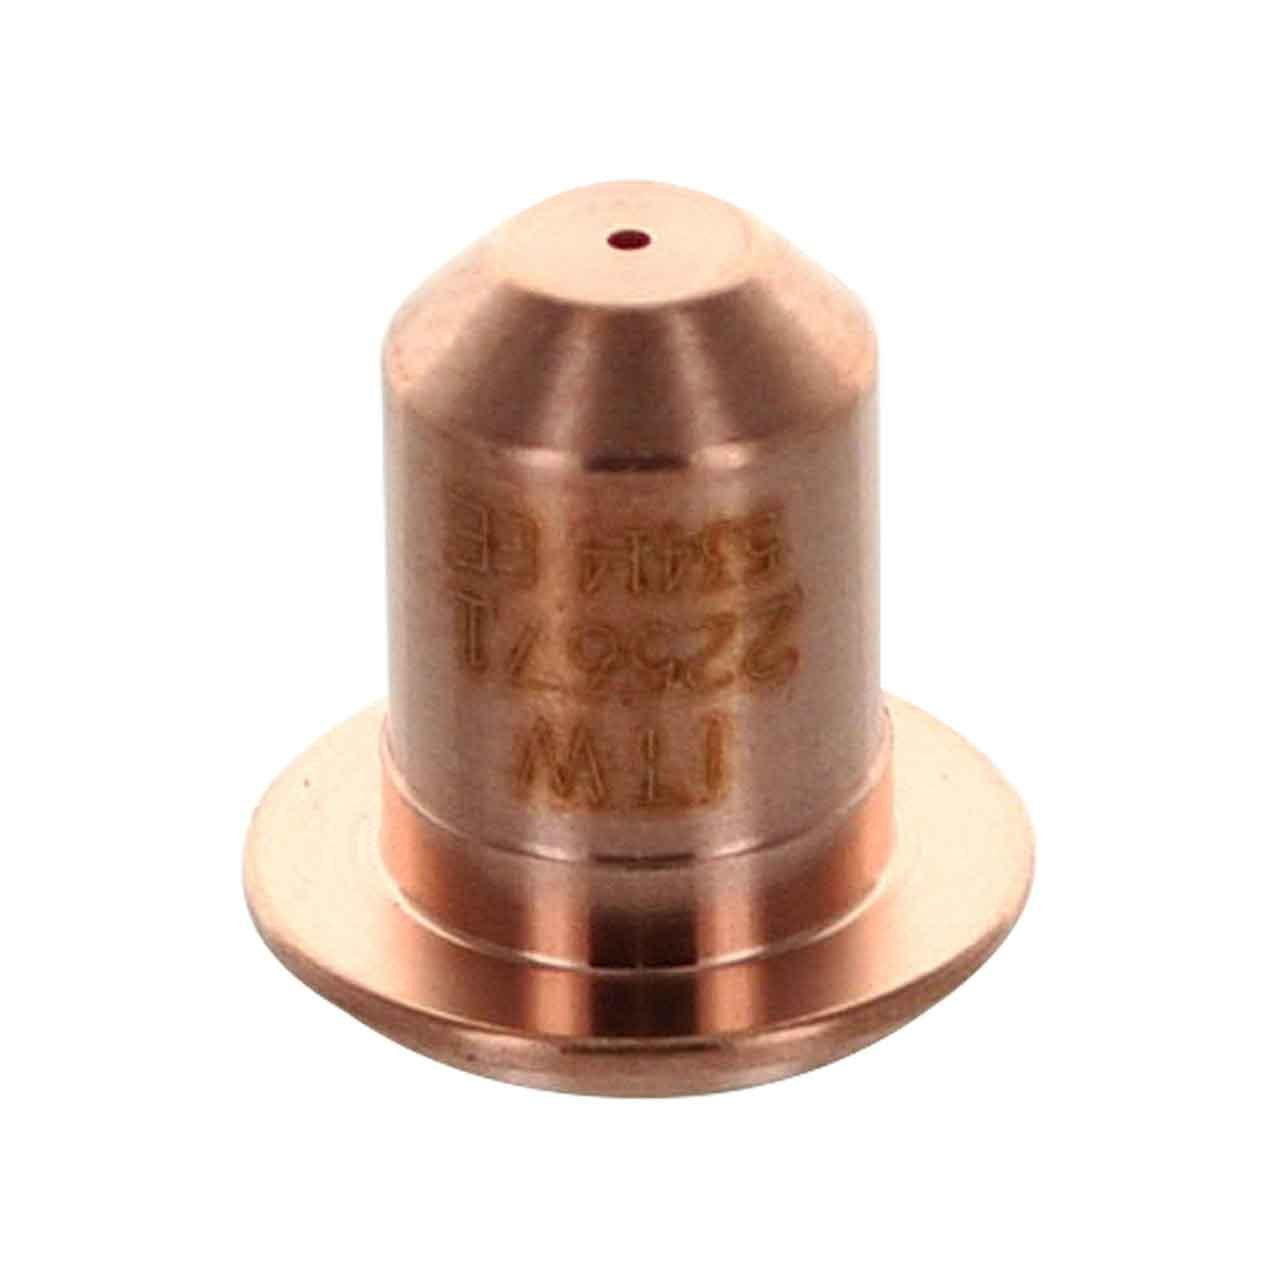
  • Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack: Product Breakdown

    Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack: Product Breakdown

    Product not found.
    “>Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack

    The Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack is a torch consumable package for plasma cutting support work. For buyers and maintenance teams, the key question is not just whether the tip is on the shelf, but whether it matches the torch system, amperage range, and wear pattern your crew is actually running. This part is listed as an extended tip for the ICE-27C plasma cutter torch and is associated with Miller Spectrum 375 and 3765 X-tremes plasma cutters based on the product source provided. Confirm the torch model on the equipment before ordering or installing.

    Key takeaways

    • This is a 5-pack of consumable tips.
    • It is identified as an extended tip for the ICE-27C torch.
    • Source material ties it to Miller Spectrum 375 and 3765 X-tremes plasma cutters.
    • Do not assume fit from the machine name alone. Verify torch model and consumable designation at the unit.
    • Use wear checks, not guesswork, to decide when to replace the tip.

    What this part does

    Plasma tips focus the cutting arc and help control cut quality. As the tip wears, cut performance can shift in ways that are easy to spot in the field: rougher edges, more dross, unstable arc starts, or visible damage at the orifice. The right replacement restores the torch’s intended arc shape, but only if the whole consumable stack and torch are in proper condition.

    Because this is a consumable, the buying decision is usually about consistency and uptime. Maintenance teams should stock tips based on actual torch usage, not only on machine count. If a torch is heavily used on production cuts, tips should be treated as planned replacement items, not emergency parts.

    Check, inspect, verify before install

    Use this sequence before installing a new tip:

    1. Check the torch model. Confirm the torch is ICE-27C or ICE-27T as applicable to your setup. If the torch designation is unclear, mark it as Unknown (Verify) and stop until the model is confirmed.
    2. Inspect the consumable stack. Look at the electrode, shield, swirl ring, retaining hardware, and tip seat. A new tip will not correct damage elsewhere in the stack.
    3. Verify amperage use. The product title identifies 25Amp. Verify your operating setup against the torch and machine manual before use.
    4. Check for heat and contamination. Carbon, spatter, moisture, and torch body damage can shorten tip life. Clean the torch components only according to the machine manual.
    5. Verify correct seating. Install the tip fully and evenly. If seating feels inconsistent, stop and inspect the torch body and mating parts.

    Troubleshooting support for poor cut quality

    If cut quality drops after a tip change, do not assume the new tip is defective. Work through the torch system first.

    Problem: rough edge or heavy dross

    • Check whether the tip is worn, damaged, or installed incorrectly.
    • Inspect the work speed, standoff, and material condition.
    • Verify the torch components are the correct series for the machine.

    Problem: unstable arc or hard starts

    • Check the electrode and tip together. A new tip with a worn electrode can still misbehave.
    • Inspect for contamination in the torch or air delivery path.
    • Verify air quality, machine settings, and torch compatibility against the manual. Unknown (Verify) if documentation is not available at the work area.

    Problem: repeated short tip life

    • Check for contact with the workpiece or excessive drag.
    • Inspect the torch body for heat damage, cracked components, or loose parts.
    • Verify operator technique and consumable handling. Tips should not be forced into place.

    Parts and application notes

    This product listing identifies the part as a Miller consumable for the ICE-27C torch, with application to Miller Spectrum 375 and 3765 X-tremes plasma cutters per the source data provided. That is the safest level of identification available here. Any further compatibility detail is Unknown (Verify) until checked against the machine manual, torch label, or internal maintenance record.

    For buyers, the main control points are straightforward:

    • Match the torch designation first.
    • Match the amperage and consumable family second.
    • Confirm the replacement count in the package before issuing stock.
    • Record the tip as a tracked wear item so ordering is based on usage, not panic replacement.

    How maintenance teams should stock it

    Consumables like this tip are best managed with a simple issue-and-replace process. Keep the package sealed until needed, label inventory by torch family, and separate plasma consumables by system if your shop uses more than one torch platform. Mixing tips by appearance alone is a common cause of downtime. Use the part number and torch designation for stock control.

    If your site uses a formal parts approval process, tie the tip to the machine asset record and the torch serial or family record where possible. If that record is missing, the compatibility status is Unknown (Verify) and should be confirmed before release to production.

    Safety notes

    • De-energize the equipment before servicing consumables.
    • Allow hot components to cool before handling.
    • Follow the machine and torch manual for installation, cleaning, and replacement steps.
    • Do not force consumables into a torch body.
    • Wear suitable hand and eye protection for plasma service work.

    FAQ

    Is this tip only for the ICE-27C torch?

    The source listing identifies it as an extended tip for the ICE-27C plasma cutter torch. Any use beyond that is Unknown (Verify) and should be checked against the torch and machine documentation.

    Can I use this with a Spectrum 375 or 3765 X-tremes unit?

    The provided source says the torch is on Miller Spectrum 375 and 3765 X-tremes plasma cutters. Verify your exact machine and torch configuration before ordering or installing.

    What should I inspect if the new tip does not improve cut quality?

    Inspect the electrode, shield, swirl ring, torch body, air quality, and operator technique. A new tip alone will not fix wear or contamination elsewhere in the system.

    How should I decide when to replace the tip?

    Replace it when wear is visible, cut quality declines, or the arc becomes unstable. If the condition is uncertain, mark it Unknown (Verify) and inspect the full consumable set.

    Sources checked

    • ArcWeld product source: Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack
    • Provided product short description and source URL

    Related Arc Weld Part

    Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack

    Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack

    Miller 225671 Extended Tips. This is for the ICE-27C plasma cutter torch. Which is on the Miller Spectrum 375 and 3765 X-tremes plasma cutters. Package of 5

    View at Arc Weld Store
  • ESAB PT-39 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-39 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-39 Torch Parts Breakdown

    The ESAB PT-39 Torch Parts Breakdown is a practical reference for maintenance buyers, welders, and support teams who need to identify replacement consumables before ordering. Plasma torches fail for simple reasons: worn electrodes, damaged nozzles, loose retaining parts, air leaks, or a torch assembly that does not match the machine setup. The right buying step is to verify the torch family and item number first, then inspect the worn parts against the parts breakdown before you place an order.

    This guide is not a substitute for the machine manual or the torch documentation. Use it as a buying and inspection aid. If a detail is not confirmed, treat it as Unknown (Verify).

    Key Takeaways

    • Confirm the exact torch model before ordering any PT-39 replacement part.
    • Match the item number on the parts breakdown to the worn component, not just the visual shape.
    • Inspect electrodes, nozzles, shields, and retaining hardware as a set.
    • Check lead condition, torch body damage, and air delivery before replacing consumables again.
    • Use the WSP lookup page as the primary source for part identification.

    How to Use the PT-39 Parts Breakdown

    Start with the parts lookup page and identify the component by item number, not by assumption. On plasma torches, two parts can look similar but differ in thread style, length, seat profile, or torch-family match. If you only compare pictures, the risk of ordering the wrong part is high.

    Check: the torch label, machine documentation, and worn part geometry.
    Inspect: the nozzle orifice, electrode pit depth, shield face, and retaining cap threads.
    Verify: the replacement item number against the WSP lookup page before purchase.

    Troubleshooting and Support Checks

    When a PT-39 torch starts cutting poorly, do not assume the consumables are the only issue. Plasma cut quality problems often come from a combination of wear and setup errors.

    1) No start or weak start

    • Check the torch lead connection and power source setup.
    • Inspect the electrode and nozzle for heavy wear, burn marks, or contamination.
    • Verify the consumables are seated correctly and tightened to the proper hand-tight condition per the equipment manual.

    If the torch parts are new and the problem remains, the issue may be in air supply, trigger circuit, or internal torch damage. Unknown (Verify) if the source is torch-related until the upstream system is checked.

    2) Arc dropout during cutting

    • Check for loose retaining parts or poor contact between consumables.
    • Inspect the nozzle opening for distortion and the electrode tip for uneven erosion.
    • Verify that the air supply is stable and clean.

    Arc dropout is often caused by consumable wear, but supply instability can produce the same symptom. Replace only the parts that are actually worn or damaged.

    3) Poor cut edge or excessive dross

    • Check cut speed, torch standoff, and work lead condition.
    • Inspect nozzle wear and shield damage.
    • Verify that the torch setup matches the intended cut mode and amperage range. Unknown (Verify).

    Do not buy consumables only by amperage label or general appearance. Match the parts breakdown first, then compare the physical wear pattern.

    Buying Checks Before Ordering Parts

    For buyers and storeroom teams, the important step is reducing return risk. Use these checks before placing an order:

    • Check the torch family: Confirm it is PT-39 and not another ESAB torch model.
    • Check item numbers: Use the parts breakdown item number for the replacement part.
    • Check wear history: If the torch repeatedly burns the same part, the upstream issue may be air quality or handling.
    • Check the machine record: Match the torch to the cutter or power source documentation.
    • Check packaging notes: If the listing does not clearly match the item number, do not guess.

    If a part description is unclear, keep it as Unknown (Verify) until the item number and torch family are confirmed.

    WSP Lookup Section

    Use the official Weld Support Parts page for the ESAB PT-39 torch to review the parts breakdown and item-number lookup:

    ESAB PT-39 Torch Parts Breakdown on Weld Support Parts

    This page is the starting point for identifying replacement consumables and related torch parts. Use it to compare the worn component to the listed item number before you buy.

    Practical Inspection Steps at the Torch

    Before replacing consumables, do a short field inspection:

    1. Lock out the system and make sure the torch cannot fire.
    2. Remove the consumables and lay them out in order.
    3. Inspect the electrode for crater wear, pitting, and heat damage.
    4. Inspect the nozzle for ovality, enlarged orifice, or spatter damage.
    5. Inspect the shield/retaining parts for cracks, thread wear, and burn marks.
    6. Inspect the torch body for heat damage, cracks, and contamination.
    7. Verify that the part numbers on the replacement order match the lookup page.

    This sequence helps prevent unnecessary parts swaps. If the consumables fail early, verify the air supply quality and torch handling before assuming the replacement parts are wrong.

    Safety Notes

    • De-energize the cutter before removing torch consumables or opening covers.
    • Let hot parts cool before inspection. Plasma tips and electrodes can retain heat.
    • Use eye protection and gloves when handling used consumables with sharp or hot edges.
    • Do not fire a torch with missing or loose parts.
    • If a torch shows burn-through, cracked insulation, or exposed conductors, remove it from service until repaired by qualified personnel.

    FAQ

    How do I confirm the correct PT-39 replacement part?

    Use the WSP PT-39 parts breakdown, then match the item number to the worn component. Do not order by appearance alone.

    What if the torch looks like another ESAB model?

    Treat it as Unknown (Verify) until the torch label, machine manual, and parts breakdown all match. Similar torch parts are not interchangeable by default.

    Should I replace only the electrode?

    Only if inspection shows the electrode is the only worn part. If the nozzle or retaining hardware is damaged, replace the matching consumables as needed after verification.

    Why do new consumables sometimes fail early?

    Early failure can come from air contamination, improper torch setup, loose parts, or handling damage. Inspect the whole torch system before ordering the same parts again.

    Sources Checked

    • Weld Support Parts: ESAB PT-39 Torch Parts Breakdown — https://www.weldsupportparts.com/esab-pt-39-torch.html
    • Internal link: Plasma Consumable Compatibility: How to Verify Torch Parts Before Ordering
    • Internal link: Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
    • Internal link: Plasma Drag Shield Compatibility Guide: Torch Family, Amperage, Nozzle, Retaining Cap, and Cut Mode Checks

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • ESAB PT-38 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-38 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-38 Torch Parts Breakdown

    If you are maintaining an ESAB PT-38 torch, the main job is not just finding a part number. The job is matching the torch body, head, consumables, shields, and accessory rows to the exact setup on the machine before you order. A wrong consumable can look close enough to install and still fail in cut quality, arc stability, or wear life.

    This guide is a practical parts-lookup and buying-check article for the ESAB PT-38 Torch Parts Breakdown. Use it to verify what you have, compare the layout to the Weld Support Parts lookup page, and avoid ordering by appearance alone.

    Key Takeaways

    • Start with the torch family and item-number lookup, not the part photo.
    • Verify the torch model, amperage class, and cut process before ordering consumables.
    • Check the nozzle, electrode, shield, retaining cap, swirl ring, and handle-side accessories as a set.
    • If any fitment detail is unclear, treat it as Unknown (Verify) until you confirm it against the lookup page or the torch itself.
    • Use the parts breakdown for replacement planning, not as proof that two similar-looking parts are interchangeable.

    What the PT-38 parts breakdown is good for

    The Weld Support Parts page for the ESAB PT-38 is a lookup reference for replacement parts, consumables, kits, and accessory rows with item-number lookup. That makes it useful for maintenance buyers and shop support teams who need to match what is installed on the torch to what should be ordered next.

    Use the page to identify:

    • Consumable rows tied to the PT-38 torch family
    • Replacement items for wear parts
    • Kit rows or grouped accessory rows, if listed
    • Item numbers that help cross-check your internal stock labels

    Important: the lookup page is a starting point for identification. It is not a substitute for confirming the torch variant in the field.

    Practical check steps before you order

    Use these checks at the bench, not from memory.

    1. Check the torch nameplate or body marking. Verify that the torch is actually PT-38. If the marking is missing or worn, note it as Unknown (Verify).
    2. Inspect the consumable stack. Remove the nozzle, electrode, shield, and retaining components as needed and lay them out in order. Compare that stack to the parts breakdown.
    3. Verify wear pattern. Look for rounded nozzle orifice, heat distortion, pit marks, or thread damage. If the wear pattern is abnormal, do not assume the next size up or down is correct.
    4. Match item numbers. Use the Weld Support Parts lookup rows to confirm the item numbers before purchase.
    5. Check for accessory dependence. Some torch setups rely on specific shields, caps, or adapters. Verify each row individually.
    6. Confirm the machine-side connection. The torch body can only be matched correctly if the lead, connector, and machine interface are also verified. If you do not have that information, record it as Unknown (Verify).

    Troubleshooting and support checks

    If the torch is cutting poorly, do not start with the most expensive part. Start with the consumable stack and the torch condition.

    No start or unstable start

    • Inspect electrode condition and seating.
    • Verify the nozzle is not damaged, clogged, or oversized from wear.
    • Check shield and retaining parts for heat damage or loose fit.
    • Verify the torch cable, trigger circuit, and machine connection. If the machine-side details are not known, mark them Unknown (Verify).

    Weak arc or arc dropout

    • Inspect the consumable stack for improper assembly.
    • Verify that the parts match the PT-38 breakdown and not a similar torch family.
    • Look for excessive nozzle erosion or electrode wear.
    • Confirm gas or air delivery conditions only if your setup uses them and the machine instructions support that check.

    Rough cut edge or rapid consumable wear

    • Inspect nozzle alignment and seating.
    • Verify the shield and retaining components are correct for the torch head.
    • Check for contamination, heat damage, or mechanical impact.
    • Compare the installed parts against the lookup page before ordering a full consumable kit.

    How to use the WSP lookup page

    Use the Weld Support Parts PT-38 lookup page here: ESAB PT-38 Torch Parts Breakdown.

    Use that page as your first pass for part identification. Review each row carefully and compare the item number to the physical part in your hand. If a row is unclear, do not guess. Mark the detail Unknown (Verify) and confirm it against the torch body, existing packaging, or your maintenance records.

    For shops managing multiple plasma torches, this page is useful for reducing mix-ups between similar torch families. The main check is still the same: torch model first, consumable stack second, order third.

    Buying checks for maintenance teams

    Before you release a purchase order, verify the following:

    • Model match: PT-38 confirmed, or Unknown (Verify) if not confirmed.
    • Part-level match: nozzle, electrode, shield, cap, and any adapter or spacer verified by row.
    • Usage history: record whether the failed part was damaged by heat, impact, poor seating, or normal wear.
    • Stock control: confirm the warehouse label matches the item number on the lookup page.
    • Machine-side details: verify cable length, connector style, or system interface only from documented records. If not documented, use Unknown (Verify).

    Do not approve a replacement just because the part looks close. Plasma torch consumables are often similar by appearance and still not interchangeable.

    Safety notes

    • Disconnect power and follow plant lockout procedures before opening torch assemblies.
    • Allow hot parts to cool before handling.
    • Wear eye protection and gloves when removing worn consumables.
    • Do not reuse parts with cracked threads, heavy heat distortion, or visible structural damage.
    • If the torch condition is uncertain, stop and verify rather than forcing a fit.

    FAQ

    How do I know which PT-38 part I need?

    Start with the torch marking, then compare the installed consumables to the parts breakdown. Match the item numbers on the lookup page to the parts in your hand.

    Can I order by appearance alone?

    No. Similar plasma consumables can look alike and still differ in fitment or function. Verify the row, item number, and torch model first.

    What if my torch label is missing?

    Treat the model as Unknown (Verify) until you confirm it from records, machine documentation, or a direct parts comparison.

    Is the parts breakdown enough to approve a replacement?

    It is a good starting point, but not enough by itself if the torch or machine interface is unclear. Confirm all uncertain details before ordering.

    Sources Checked

    For the ESAB PT-38, the safe buying process is simple: verify the torch, verify the consumable stack, verify the item number, then order. If any detail is not confirmed, keep it as Unknown (Verify) until you have the right match.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • ESAB MT-200 Gun Parts Breakdown: Parts Lookup and Buying Checks

    ESAB MT-200 Gun Parts Breakdown: Parts Lookup and Buying Checks

    ESAB MT-200 Gun Parts Breakdown

    The ESAB MT-200 gun is a serviceable welding and cutting support item, but the part names, item numbers, and wear points need to be matched carefully before ordering. A breakdown article is useful only if it helps you identify what is on the gun, what is worn, and what must be verified before a purchase. This guide focuses on parts lookup discipline, inspection steps, and buying checks using the Weld Support Parts lookup page for the ESAB MT-200 gun assembly.

    Key Takeaways

    • Use the item-number lookup first. Do not guess from appearance alone.
    • Separate assembly-level needs from service-part needs before you order.
    • Inspect wear, thread condition, sealing surfaces, and electrical continuity where applicable.
    • Match the exact MT-200 gun variant and connection style before buying.
    • When a detail is not confirmed, mark it as Unknown (Verify) instead of assuming compatibility.

    What the ESAB MT-200 Gun Parts Breakdown Is For

    A parts breakdown is a reference for identifying subassemblies and replacement items by position or item number. For the MT-200 gun, that usually means separating the gun body, handle components, triggers or switches, leads, liners or internal paths where applicable, tips or end components, and any external hardware used to secure the assembly. The exact structure of the assembly should be verified against the lookup page rather than assumed from other ESAB guns.

    If you are troubleshooting intermittent performance, the common failure is not the whole gun. It is often one worn item, one loose connector, or one damaged consumable. The breakdown helps you identify the minimum part set needed to restore function.

    How to Use the WSP Lookup Page

    Start with the Weld Support Parts reference for this gun: ESAB MT-200 Gun Parts Breakdown. Use it as the item-number source of record. If your maintenance team keeps a log, record the item number exactly as shown on the page before checking stock or placing an order.

    Check:

    • Gun model marking on the assembly.
    • Item number or callout on the breakdown page.
    • Any variation in handle, lead, or connector style.
    • Whether the needed item is a full assembly, a subassembly, or a wear part.

    Inspect:

    • Cracks in the handle or outer shell.
    • Heat damage near the front end or cable entry.
    • Loose fasteners, stripped threads, or missing retainers.
    • Signs of arcing, discoloration, or contamination.

    Verify:

    • That the item number on the WSP page matches the failed part position.
    • That the replacement is not a similar-looking part from a different gun series.
    • That any connection or interface detail is known, or marked Unknown (Verify).

    Troubleshooting by Symptom

    1) Poor output or unstable performance

    If the gun is not performing consistently, start with the simplest checks.

    Check: the front-end wear items, visible damage, and the condition of the cable or lead.

    Inspect: for loose connections, bent hardware, or contamination at contact points.

    Verify: whether the issue follows the gun or stays with the machine. If the issue stays with the gun, the fault is likely in the gun assembly or a wear component.

    2) Mechanical damage

    Handle damage, broken retainers, and damaged front-end components can create intermittent issues and make the gun unsafe to handle.

    Check: for cracks, missing fasteners, and exposed internal parts.

    Inspect: the trigger area, strain relief, and front-end section for impact marks.

    Verify: whether the damaged item is sold as a separate part or only as part of a larger assembly.

    3) Fit-up or replacement mismatch

    Wrong-order purchases happen when the buyer uses only the model name and ignores the item number. The MT-200 name alone is not enough for a safe purchase decision.

    Check: the part callout and the physical mounting or connection points.

    Inspect: the old part for labels, molded numbers, or unique geometry.

    Verify: any uncertain compatibility detail as Unknown (Verify) before issuing the purchase request.

    Buying Checks for Maintenance Teams

    Before you buy, confirm the part role and the scope of replacement. A shop can waste time and budget by replacing a complete assembly when only a small service part is needed. The opposite also causes downtime if a worn lead or front-end component is left in service.

    Use this checklist:

    • Identify the failed item by position on the breakdown.
    • Confirm whether you need an assembly, subassembly, or consumable/service item.
    • Match the item number from the WSP page.
    • Confirm the gun variant and any connection detail.
    • Record Unknown (Verify) for any data you cannot prove from the source.
    • Save the old part until the replacement is installed and tested.

    If your purchasing process requires a second check, have the welder or technician mark the worn item on the physical gun and compare it with the lookup page before release.

    What to Record in the Maintenance Log

    Good records reduce repeat mistakes. Log the model name, item number, failure symptom, date removed, and whether the gun was returned to service or sent for further inspection. If the part description is unclear, add Unknown (Verify) rather than guessing. That helps the next buyer avoid a mismatch.

    Safety Notes

    • De-energize and isolate equipment before inspection or disassembly.
    • Do not test a damaged gun with exposed conductors or broken insulation.
    • Replace damaged parts before returning the gun to service.
    • If there is heat damage, arcing evidence, or melted insulation, stop and inspect the full assembly.

    FAQ

    How do I know which MT-200 part to order?

    Use the item-number lookup on the Weld Support Parts page, then match the failed component to the callout position. Do not order by appearance alone.

    Can I replace only the worn section instead of the whole gun?

    Often yes, but only if the breakdown shows that part as a separate service item. If that detail is not confirmed on the lookup page, mark it Unknown (Verify).

    What if the old part has no readable label?

    Use the physical location on the gun, the shape, and the breakdown item position. If you still cannot confirm it, hold the order until the item is verified.

    Why does the same MT-200 name still require verification?

    Because variant details, connection interfaces, and subassembly layouts can differ. The model name is not enough to confirm compatibility.

    Sources Checked

    For procurement, the rule is simple: inspect the failed gun, verify the item number, and only then buy the replacement. If any detail cannot be confirmed from the source, treat it as Unknown (Verify) until it is checked.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • Hypertherm 120979 Deflector: Replacement Part Breakdown

    No products found.

    The Hypertherm 120979 deflector is a replacement part used in plasma cutting support workflows. If you are sourcing this part for maintenance, repair, or inventory control, the main task is to confirm that the part matches the torch, shield, and consumable set in use before install. Do not assume fitment from the name alone. Verify the torch system, cut process, and related consumable stack against the machine documentation and the part marking on the removed component.

    Key Takeaways

    • Confirm the deflector part number before ordering or installing.
    • Inspect the torch consumable stack for wear, heat damage, and misalignment.
    • Replace damaged support parts as a set when wear patterns indicate system issues.
    • Use the WSP lookup page to confirm internal part reference data before purchase.
    • Keep safety practices in place during removal, inspection, and test cutting.

    What the Deflector Does

    A deflector in a plasma cutting setup helps manage the interaction between the torch nozzle area and the work environment. In practical terms, it is part of the consumable or support stack that can affect arc behavior, cut consistency, and the condition of nearby components. If the deflector is worn, heat affected, cracked, or physically deformed, the system may show poor cut quality or accelerated wear in other consumables. The exact function and placement depend on the torch family and cutting setup. Unknown (Verify).

    Before You Replace It: Check, Inspect, Verify

    Check the part number on the removed deflector and compare it to the replacement part listing. For this product, the ASIN-linked product reference is Hypertherm 120979 Deflector B008BJFT3K.

    Inspect the mating components in the consumable stack. Look for burn marks, slag buildup, melted edges, thread damage, or out-of-round features. If a companion part is damaged, replacing only the deflector may not correct the root issue.

    Verify that the torch is de-energized, air or gas pressure is isolated as required by your shop procedure, and the work area is clean before removal. Confirm that the replacement part matches the torch model and assembly configuration. Compatibility not otherwise documented is Unknown (Verify).

    Troubleshooting When a Deflector Is Failing Early

    If the deflector shows short service life, do not stop at part replacement. Look for process issues that can drive premature wear.

    • Check torch height control: Verify the torch is not running too low and striking spatter or the plate surface.
    • Inspect air quality: Moisture, oil, and contamination can shorten consumable life. Confirm your air prep system is operating correctly.
    • Verify cut settings: Excess current, improper pierce timing, or incorrect cut speed can overheat the support parts.
    • Check for physical damage: A bent torch retaining area or damaged head can misalign the consumable stack.
    • Inspect installation torque or seating: A loose or poorly seated part may arc unpredictably. Torque values are Unknown (Verify).

    If repeated failure happens after replacement, document the failure pattern, machine settings, and consumable condition. That record helps separate part defects from operating problems.

    Support Parts and Replacement Logic

    For maintenance buyers and welding support teams, the correct purchasing approach is to evaluate the full wear stack, not the individual part in isolation. When a deflector is replaced, also review the nozzle, shield, swirl ring, electrode, retaining hardware, and any torch-specific components in the same area. The exact set depends on the torch family. Unknown (Verify).

    If the shop uses a planned replacement schedule, track install date, cutting hours, material type, and observed wear. That data helps determine whether the replacement interval is normal or whether the system needs troubleshooting. A deflector that keeps failing early is often a symptom, not the root cause.

    Product Reference

    The referenced product for this draft is the Hypertherm 120979 Deflector, associated with ASIN B008BJFT3K. Use the provided product shortcode below for the Amazon affiliate listing in the WordPress editor:

    No products found.

    Do not infer fitment from the product name alone. Confirm the intended torch platform and consumable family against your service records or the machine manual. If your internal part lookup or service notes are incomplete, mark compatibility as Unknown (Verify) until confirmed.

    Installation and Return-to-Service Checks

    After installing the deflector, run these checks before returning the torch to production:

    1. Visual check: Confirm the part is seated correctly and that no foreign material is trapped in the assembly.
    2. Alignment check: Verify the consumable stack is centered and installed in the proper order.
    3. Leak or air-path check: Confirm the torch gas path is unobstructed and connections are secure.
    4. Dry function check: If your procedure allows, cycle the system without cutting to confirm normal operation.
    5. Test cut: Make a short cut on known material and inspect edge quality, dross, and arc stability.

    If the test cut is unstable, stop and inspect the entire consumable stack before continuing. Replacing the deflector alone may not resolve the fault.

    Safety Notes

    • Lock out and isolate the plasma system before service.
    • Allow hot components to cool before handling.
    • Wear gloves and eye protection when removing spent consumables.
    • Do not touch torch components with bare hands if contamination control matters to your process.
    • Follow the equipment manual and site procedure for maintenance and return-to-service steps.

    FAQ

    Q: Is the Hypertherm 120979 deflector a universal part?
    A: No. Do not treat it as universal. Confirm the torch model and consumable family before ordering. Compatibility not otherwise documented is Unknown (Verify).

    Q: What are the signs that the deflector needs replacement?
    A: Common signs include heat distortion, cracking, burn-through, slag buildup, or fit issues during assembly. Also inspect for abnormal wear in nearby consumables.

    Q: Can I replace only the deflector if cutting performance drops?
    A: Sometimes, but not always. If the nozzle, electrode, or shield is also worn, the root cause may remain after replacement. Inspect the full consumable stack.

    Q: What should I verify before putting the torch back in service?
    A: Verify correct seating, clean assembly surfaces, secure connections, and a stable test cut. If the cut is poor, stop and recheck the setup.

    Sources Checked

    • Provided Amazon affiliate product reference: ASIN B008BJFT3K
    • Provided product name: Hypertherm 120979 Deflector
    • Internal prompt constraints for the Weld Support Parts draft

    Technical details not explicitly provided above are marked Unknown (Verify) to avoid unsupported assumptions.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • Try Amazon Prime Free