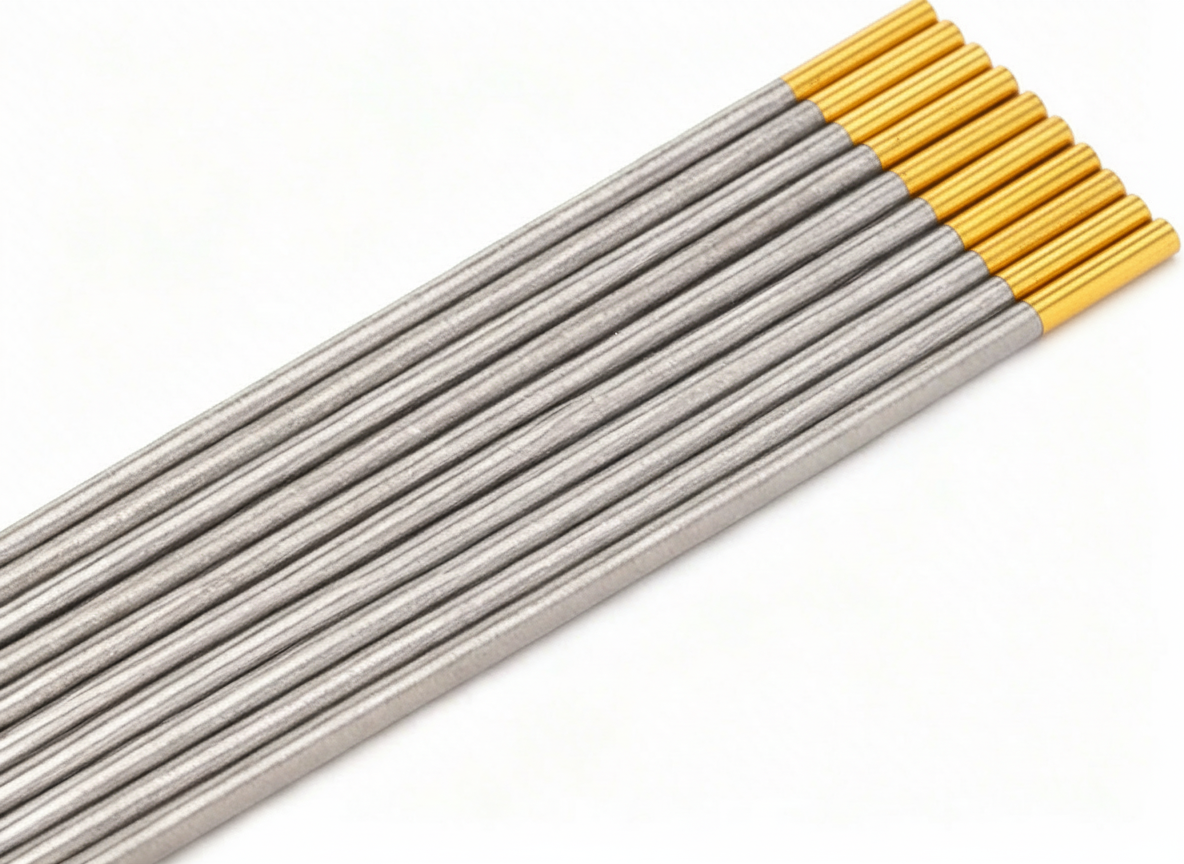

CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack is a standard TIG support item for shops that need a larger-diameter tungsten for stable arc starts and controlled current delivery. The practical value of this size is simple: 1/8 in. tungsten is commonly considered when the job calls for more current capacity than smaller electrodes can handle cleanly. That said, tungsten selection is always a setup check, not a guess. Verify torch size, collet compatibility, amperage range, joint access, and the current process before you buy or install.
Key Takeaways
- 1/8 in. x 7 in. lanthanated tungsten is typically used in TIG setups that need a larger electrode size.
- Lanthanated tungsten is a common general-purpose option, but final suitability depends on the welding procedure and base material.
- Do not assume a larger tungsten is automatically better. Check amperage, torch hardware, and access around the joint.
- If your torch or collet body is not set up for 1/8 in. tungsten, verify the hardware before ordering.
- Use the linked reference pages as starting points for selection, not as a substitute for your procedure or WPS.
What this electrode size is used for
A 1/8 in. tungsten electrode is chosen when the job requires a more robust tungsten than 3/32 in. or smaller options. In many fabrication and repair settings, this size supports steadier operation at higher amperage. The 7 in. length is a common torch length format, but torch setup must still be verified against your collet, gas lens, cup, and stickout practice. Unknown (Verify) if your shop uses a nonstandard torch body or specialty holder.
Buying checks before you order
Use the steps below before approving the purchase:
- Check tungsten diameter. Confirm the torch hardware accepts 1/8 in. (3.2 mm) electrodes. Do not rely on visual fit.
- Check electrode length. Confirm 7 in. length works with your storage, grinding station, and torch setup. Some setups can handle multiple lengths, others cannot.
- Check current demand. Compare the electrode size to the amperage range in your procedure. If the weld is low current, this size may be unnecessary.
- Check the torch consumables. Verify collet, collet body, back cap, and cup arrangement. Unknown (Verify) if your torch uses a special series or adapter.
- Check alloy choice. Lanthanated tungsten is often selected for general TIG work, but material and procedure requirements still control the final choice.
Troubleshooting and support checks
If your tungsten performance is poor after installation, use a methodical inspection instead of changing multiple variables at once.
Check
- Check that the electrode is straight and free of chipped ends.
- Check that the grind is consistent and aligned with your intended arc start method.
- Check that the tungsten is seated fully in the collet.
- Check for contamination from touching filler metal, joint edges, or a dirty grind surface.
Inspect
- Inspect the cup, collet body, and gas coverage for obstruction.
- Inspect the electrode end after a short test start. Look for wandering arc, rapid balling, or excessive discoloration.
- Inspect torch stickout. Excessive stickout may reduce shielding and arc stability.
Verify
- Verify the base material, filler choice, shielding gas, and current settings against your procedure.
- Verify that the torch setup matches the electrode diameter. If it does not, correct the hardware before continuing.
- Verify whether your weld schedule calls for a different tungsten type, diameter, or tip preparation.
WSP lookup section
For related support content and search functions, use the Weld Support Parts site resources as a starting point:
Use this site to confirm related support items and internal references. It does not replace your welding procedure or manufacturer guidance.
Filler metal finder section
If you are matching tungsten selection to a filler strategy, start with the filler metal reference page here:
This page should be treated as a selection starting point. It is not a guaranteed approval for any specific base material, joint type, or code job. Verify final compatibility against the procedure, job requirements, and supervision rules for the work.
Safety notes
- Use gloves and eye protection when handling ground tungsten and sharpened ends.
- Do not grind tungsten on contaminated wheels or surfaces used for other metals.
- Control dust from grinding and keep the area clean.
- Keep the electrode away from oils, dirt, and shop debris before use.
- If the tungsten shows unusual behavior during welding, stop and inspect the torch and procedure before continuing.
FAQ
Is 1/8 in. tungsten too large for light TIG work?
Often yes, but not always. For low-amperage work, a smaller electrode may be better. Verify the procedure and amperage before choosing this size.
Does lanthanated tungsten work for every TIG job?
No. Lanthanated tungsten is widely used, but final selection depends on material, polarity, current type, and shop procedure. Unknown (Verify) for any job-specific approval without a WPS or manufacturer reference.
What should I confirm before putting this in stock?
Confirm electrode diameter, length, torch consumable compatibility, and expected amperage range. Also confirm whether your team already standardizes on a different tungsten type for certain materials.
Why does the grind matter?
Tip preparation affects arc start and arc direction. Poor grinding can cause unstable starts and wandering arc. Keep the grind clean and consistent.
Sources Checked
- ArcWeld product summary for CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack
- TIG Welding 2% Lanthanated Tungsten Guide for Best Results
- TIG Welding Tungsten Electrodes 3/32″ (WT20 Red Tip) – Specs, Safety & Buying Guide
All uncertain fit and procedure details should be verified against the job specification, WPS, and manufacturer guidance.
Related Arc Weld Part
CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack
CK T187GL 1.5% Lanthanated Tungsten Electrodes are built for TIG welders who need dependable arc starts and stable arc control, especially at higher amperage where a larger diameter electrode makes sense. This 10-pack includes 1/8 in. (3.2 mm) electrodes in a 7 in. length for common torch setups in fabrication and repair work. Lanthanated tungsten is widely used as a versatile, general-purpose option for many TIG…
View at Arc Weld Store
Leave a Reply