Tag: maintenance
-
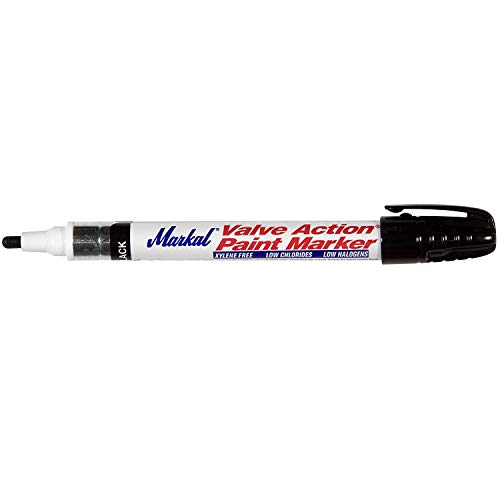
Markal 96823, Valve Action Black Paint Marker, Pack of (1): Product Breakdown
“>
The Markal 96823, Valve Action Black Paint Marker, Pack of (1) is a shop marking tool for layout, identification, and field marking where a standard ink marker is not enough. The product information provided identifies it as a real paint marker with valve action, a replaceable fiber nib, and a stated dry time of about 3 minutes. For welders, fabricators, and maintenance teams, the main value is simple: a marker that lays down visible paint on work surfaces and is built for repeated use.
Key Takeaways
- Valve action releases paint as needed for continuous marking.
- The marker uses real paint, not standard pen ink.
- Stated dry time is 3 minutes.
- Lead-free and low halogens are listed features.
- The fiber nib is replaceable, which supports full use of the marker body.
- Overall product weight is listed as 0.1 pounds.
Where this marker fits in a welding and fabrication shop
A black paint marker is generally used for part identification, cut lines, fit-up notes, and general shop marking on surfaces where visibility matters. The valve-action design helps control paint flow, which is useful when marking long runs or repeated notes. If you need a mark that stays visible through handling, the real-paint format is usually more practical than a standard felt-tip marker.
This is not a process-control device. It does not approve materials, procedures, or weld parameters. Use it as a shop marking tool only.
Check, inspect, verify before use
- Check the surface: Verify the material is suitable for paint marking. Clean, dry surfaces usually give better visibility. Unknown (Verify) on adhesion to coated, oily, or heavily oxidized surfaces.
- Inspect the nib: Make sure the fiber nib is present, seated, and not damaged before first use.
- Verify flow: Test on scrap or a non-critical area to confirm paint release before marking production parts.
- Check drying time: The stated dry time is 3 minutes, but actual dry time can vary with surface condition, film thickness, temperature, and airflow. Verify on your actual work surface.
- Inspect for contamination: If the marker has been stored open or in a dirty area, verify the nib is not clogged before relying on it for layout.
Troubleshooting and support
If the marker does not perform as expected, use a simple inspection sequence before replacing it.
- No paint transfer: Check that the nib is fully engaged. Then verify the tip is primed per normal paint-marker practice. If flow does not start, inspect for clogging or drying at the nib.
- Weak or uneven line: Verify the surface is not dusty, oily, or excessively rough. Inspect the nib for wear. The replaceable fiber nib is intended to support continued use once the tip wears.
- Excessive paint release: Check whether the marker is being pressed too hard. Valve-action markers are meant to release paint as needed; too much pressure can flood the line.
- Poor visibility: Verify the base material color and finish. Black paint may be difficult to read on dark or contaminated surfaces.
Handling and use notes
The listed features suggest a marker designed for straightforward manual use in the shop or field. Because it is a paint marker, treat it as a consumable that can dry out if left uncapped or handled incorrectly. Keep the cap secured when not in use. If the nib becomes worn, the replaceable tip supports continued use without discarding the entire body immediately.
Use the marker for identification and layout only. Do not assume the mark remains permanent under grinding, blasting, heat, solvent exposure, or weather. Unknown (Verify) on resistance to these conditions because no additional performance data was provided.
Product and parts notes
Provided product information for the Markal 96823 identifies these details:
- Product type: Marker
- Category: Paint
- Marker style: Valve action
- Nib: Fiber nib, replaceable
- Paint type: Real paint
- Lead status: Lead-free
- Halogens: Low halogens
- Dry time: 3 minutes
- Overall product weight: 0.1 pounds
Any use beyond those statements should be treated as Unknown (Verify). Do not assume surface chemistry, temperature limits, or chemical resistance without a current manufacturer data sheet or direct product confirmation.
Safety notes
- Use the marker in a ventilated area if you are sensitive to paint odors.
- Avoid skin and eye contact with wet paint.
- Keep away from ignition sources unless the manufacturer documentation states otherwise. Unknown (Verify) on flammability details.
- Do not mark parts where paint contamination is prohibited without verifying downstream process requirements.
- Follow local shop rules for solvent, paint, and waste handling.
FAQ
Is the Markal 96823 a standard ink marker?
No. The provided product information identifies it as a real paint marker with valve action.Can it be used on any metal surface?
Unknown (Verify). Surface condition matters, and no full compatibility list was provided. Test on scrap or a non-critical area first.Does the marker dry fast enough for shop use?
The stated dry time is 3 minutes. Actual dry time can change based on surface, film thickness, and environment, so verify on the part being marked.Can the nib be replaced?
Yes. The provided information states that the fiber nib is replaceable.Sources Checked
- ArcWeld product page: Markal 96823, Valve Action Black Paint Marker, Pack of (1)
- Provided product summary fields for features and dimensions
Related Arc Weld Part
Markal 96823, Valve Action Black Paint Marker, Pack of (1)
434-96823 Features: -Marks with real paint, dries in 3 minutes. -Nib releases paint as needed for continuous marking. -Lead-free, low halogens. -The fiber nib is replaceable to assure complete use of each marker. Product Type: -Markers. Category: -Paint. Dimensions: Overall Product Weight: -0.1 Pounds.
View at Arc Weld Store
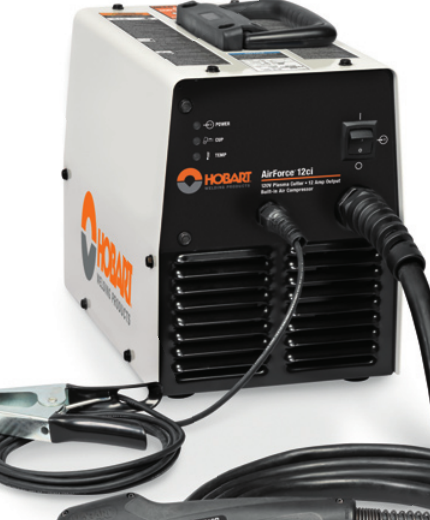
Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks
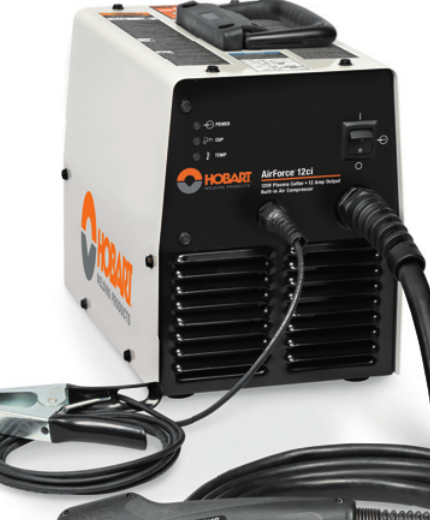
The Hobart AirForce 12ci is a compact plasma cutter support case where the buying risk is usually not the cutter itself, but the parts that keep it running: torch fitment, consumables, protective gear, and whether the replacement item matches the machine’s input and torch family. This guide is built to help welders, fabricators, and maintenance buyers verify the basics before ordering.
Key Takeaways
- Use the Hobart AirForce 12ci support page as the first parts reference before you buy.
- Verify torch model, consumable type, and input power before ordering any replacement item.
- Do not assume a plasma torch, consumable kit, or cover fits because it looks similar.
- Check wear items first: nozzle, electrode, shield, swirl ring, retaining parts, air supply, and cable condition.
- Safety glasses and a protective cover are support items, not optional extras.
Start with the WSP lookup page
The primary support page for this unit is here: Hobart AirForce 12ci Plasma Cutter Support. The page indicates stock 500564 and lists 120 V specs, XT12R replacement torch, consumable kits, safety glasses, and a protective cover. Treat those listings as the starting point for verification, not as a substitute for checking your exact machine and torch tag.
Check before you order
- Inspect the machine label: confirm the model is Hobart AirForce 12ci, not a similar unit.
- Verify input power: the support page shows 120 V specs. Confirm your unit nameplate and outlet setup match.
- Inspect the torch tag: confirm whether the unit uses the XT12R replacement torch listed on the support page.
- Check consumable wear: look for recessed electrode, enlarged nozzle orifice, heat damage, cracks, or unstable arc start.
- Verify cable and lead condition: cuts, melted sections, or loose strain reliefs can mimic consumable failure.
Troubleshooting and support checks
If the cutter is not performing well, the fastest path is a basic inspection sequence. Start simple and document what you find.
1) No start or weak start
- Check: power source status, plug condition, and supply voltage at the receptacle.
- Inspect: trigger switch, torch lead, and any visible torch damage.
- Verify: the consumables are installed correctly and are not worn beyond serviceable condition.
2) Arc starts but cut quality is poor
- Check: air pressure and air quality at the cutter.
- Inspect: nozzle, electrode, shield, and retaining parts for spatter buildup or heat distortion.
- Verify: the work clamp is clean and attached to bare metal.
3) Arc drops out during cutting
- Check: thermal condition of the machine and duty cycle usage pattern.
- Inspect: torch lead for intermittent breaks or damaged insulation.
- Verify: the air supply is steady and dry. Moisture can cause unstable operation and consumable damage.
4) Consumables wear too quickly
- Check: cutting technique, standoff distance, and travel speed.
- Inspect: whether the nozzle is being run beyond normal wear indicators.
- Verify: you are using the correct consumable kit for the torch family. If uncertain, use Unknown (Verify) until the exact kit is matched.
Parts lookup buying checks for this model
For the Hobart AirForce 12ci, the most useful parts categories are torch replacement, consumable kits, and protective items. The support page points to an XT12R replacement torch, but buyers should verify the torch family, connector style, and lead length against the existing machine before ordering. Unknown (Verify) should be used for any detail that is not confirmed by the machine label or the support page.
Replacement torch check
- Inspect: the old torch for model markings, connector type, and damage location.
- Verify: the new torch is listed for the same support page and matches the original torch family.
- Confirm: no modification is required for fitment unless the manufacturer states otherwise.
Consumable kit check
- Inspect: all wear components removed from the torch.
- Compare: thread shape, size, and seating surfaces.
- Verify: the kit is intended for the same torch model, not just a similar plasma system.
Protective gear and cover
- Check: whether the shop already stocks plasma-rated eye protection.
- Inspect: the machine’s storage location for dust, slag, and moisture exposure.
- Verify: a protective cover will not trap heat when the machine is warm after use.
Use the internal guides as support references
If the cutter is giving you symptoms beyond basic wear, these related articles can help narrow the fault before you order parts:
- Plasma Cutter Not Cutting Through: Causes and Fixes
- Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
- Plasma Cutter Buying Guide 2025 | Duty Cycle, Cut Capacity & Air Requirements
Safety notes
- Disconnect power before inspecting torch leads, consumables, or internal connections.
- Use eye protection and hand protection when checking the torch or removing worn parts.
- Do not use damaged leads, cracked torch bodies, or loose consumable assemblies.
- Verify ventilation and keep flammables clear of the cutting area.
- If a part fitment is uncertain, mark it Unknown (Verify) and confirm through the machine label, torch tag, or support listing before use.
FAQ
What should I verify first for Hobart AirForce 12ci parts?
Verify the machine model, input power, and torch family first. Then check consumables, cable condition, and air supply quality.
Is the XT12R replacement torch listed on the support page the correct part for every unit?
Unknown (Verify). The support page lists XT12R, but you should confirm the torch tag and connector style on your specific machine before ordering.
How do I know if the problem is consumables or the torch?
Inspect the nozzle, electrode, and shield first. If wear is visible or the arc is unstable, consumables are often the first suspect. If the lead, trigger, or torch body is damaged, the torch may need replacement.
Can I buy based on similar-looking plasma parts?
No. Similar appearance does not confirm fitment. Match the part to the support page and the machine tag, then verify before purchasing.
Sources Checked
- Hobart AirForce 12ci Plasma Cutter Support
- Powermax30 XP Plasma Cutter Review: Precision Cutting Power in a Compact Package
- Plasma Cutter Buying Guide 2025 | Duty Cycle, Cut Capacity & Air Requirements
- Plasma Cutter Not Cutting Through: Causes and Fixes
- Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
Related Weld Support Guides
- Powermax30 XP Plasma Cutter Review: Precision Cutting Power in a Compact Package
- Plasma Cutter Buying Guide 2025 | Duty Cycle, Cut Capacity & Air Requirements
- Plasma Cutter Not Cutting Through: Causes and Fixes
- Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
Markal 96270, Silver Steak Markal PRO Holder, Pack of (1): Replacement Part Breakdown
The Markal 96270, Silver Steak Markal PRO Holder, Pack of (1) is best treated as a consumable support item in a marking system, not as a standalone process-critical welding component. For maintenance buyers, shop leads, and support teams, the main question is simple: when a holder starts to fail, what should you inspect before you replace it, and what should you verify after it arrives?
This guide breaks the part down from a service and support angle. It does not assume undocumented compatibility, dimensions, or internal construction details. Where technical details are not confirmed here, they are listed as Unknown (Verify).
Key Takeaways
- The Markal 96270 listing identifies a replacement holder item, but exact internal build details are Unknown (Verify).
- Before ordering a replacement, inspect the current holder for wear, binding, cracked body parts, or poor lead/marking retention.
- After receipt, verify fit, actuation, retention, and general condition before putting it into service.
- Do not assume compatibility with other Markal holders or marking formats unless confirmed by the seller or your internal part records.
- Use the Amazon product listing only as a product reference point; do not rely on it for undocumented repair guidance.
What This Part Is Used For
The product name indicates a Markal PRO holder associated with Silver Steak marking use. In practice, holders in this category are used to secure and present a marking stick or similar consumable in a controlled way. The exact operating method for this specific unit is Unknown (Verify), so support teams should confirm the current tool design before attempting repair, disassembly, or substitution.
If the holder is being used in a fabrication or maintenance environment, common failure symptoms include poor retention, inconsistent feed, damaged locking features, or a body that no longer holds alignment. Those symptoms do not prove the holder is the only problem. The marking stick, operator handling, storage conditions, or contamination can also be involved.
Inspection Checklist Before Replacement
Use this sequence before writing off the holder:
- Inspect the body. Look for cracks, bent sections, gouges, or heat damage.
- Check retention surfaces. Verify the part still grips the marking material consistently.
- Check movement. If the holder has a sliding or advancing function, verify it moves without sticking.
- Inspect for debris. Clean out dust, metal fines, and marker residue.
- Verify operator handling. Check whether the tool is being dropped, over-tightened, or stored in a way that causes premature wear.
If any of these checks fail, document the condition with photos and note whether the problem is intermittent or continuous. That record helps avoid repeating the same failure after replacement.
Troubleshooting Support Steps
1) Holder will not retain the marking stick
Check: Confirm the stick type matches the holder’s intended size and format. Exact fit data is Unknown (Verify).
Inspect: Look for worn jaws, damaged guides, or missing internal parts.
Verify: Test with a known good marking stick from the same inventory lot if available.
2) Advancement feels stiff or inconsistent
Check: Make sure the unit is not loaded with broken fragments or compacted dust.
Inspect: Examine sliding interfaces for contamination, bending, or corrosion.
Verify: Clean the holder and repeat the movement test before replacing the unit.
3) Marking quality has declined
Check: Confirm the issue is not in the marking material itself.
Inspect: Review the tip presentation and whether the holder is keeping the stick aligned.
Verify: Compare output against a known good holder under the same operator and surface conditions.
Product and Parts Notes
The only confirmed product detail provided here is the Amazon ASIN reference for the Markal 96270, Silver Steak Markal PRO Holder, Pack of (1): B074WGYF21. No additional specifications, dimensions, or repair kits are verified in the source data available for this draft.
If you are building a replacement-part record, capture the following internally:
- Original part name and ASIN reference
- Observed failure mode
- Date removed from service
- Any matching model or lot data from packaging
- Operator notes on fit, feel, and performance
Do not assume a “similar” holder will work as a direct substitute unless the vendor or your own verified records confirm it.
Support and Ordering Considerations
For buyers, the main risk is ordering on description alone. The product title suggests a specific Markal PRO holder variant, but the available source data does not confirm cross-compatibility with other holder bodies, refill formats, or accessories. Keep that uncertainty in the purchase record and verify against your own approved-use list before standardizing the part.
If the existing holder is failing repeatedly, review the root cause before replacement. Storage, contamination, impact damage, and incorrect loading are common contributors in marking tool service problems. A replacement part will not fix a handling issue.
Safety Notes
- Wear appropriate hand protection when inspecting used marking tools with sharp or worn edges.
- Do not force a jammed mechanism apart unless the tool design and service method are confirmed.
- Keep solvents, compressed air, and cleaning methods compatible with your site procedures.
- Remove the holder from service if cracks, breakage, or loose internal parts are found.
- Use lockout, housekeeping, and tool-control practices where required by site policy.
FAQ
Is this a complete tool or a replacement support part?
The product name indicates a holder product. Exact internal configuration is Unknown (Verify), so confirm whether your application treats it as a complete tool, a replacement component, or a consumable support item.
Can I use it with other Markal products?
Not enough verified data is available here to confirm compatibility. Treat compatibility as Unknown (Verify) unless your internal part records or the seller confirm it.
What should I check before buying a replacement?
Inspect the existing holder for wear, binding, damage, and contamination. Verify the marking material type, the loading method, and any model identifiers from the old unit before placing an order.
What if the new holder still does not work properly?
Verify the marking stick or consumable, the loading method, and the operator technique. If the failure repeats, document the issue and compare the new part against the removed part for fit and function.
Sources Checked
- Amazon product reference provided in the task: Markal 96270, Silver Steak Markal PRO Holder, Pack of (1), ASIN B074WGYF21
- No WSP lookup page provided
- No filler metal finder page provided
- No internal links provided
Note: This draft intentionally avoids unverified specifications, pricing, certifications, and compatibility claims. Use internal records or supplier confirmation to complete any unresolved technical details.
Matched Replacement Option
No products found.
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
Hypertherm 851462 Powermax30 AIR Essential Consumable Kit: Replacement Part Breakdown
The Hypertherm 851462 Powermax30 AIR Essential Consumable Kit is a replacement-part purchase, not a process-change item. Buyers usually need it to keep a handheld plasma system ready for service, reduce downtime, and restore cut quality after normal wear. For support teams and maintenance buyers, the practical question is simple: what is included, what wears first, and what should be checked before the kit is installed?
This guide focuses on part-level verification and field-use checks. It does not assume any unlisted compatibility beyond the product name provided. If you are matching a machine, torch, or cartridge configuration, verify every identifier against your system documentation before ordering or installation.
Key Takeaways
- This is an essential consumable kit for a Powermax30 AIR setup; treat it as wear-part support.
- Consumables are normal replacement items. Poor cut quality is often a wear issue, not a machine failure.
- Before use, verify torch model, retaining hardware, and electrode/nozzle condition against your current parts.
- If the kit contents are not fully confirmed from your source listing, mark the unclear items as Unknown (Verify).
- Do not force-fit plasma consumables. If the stack-up does not match, stop and confirm the part numbers.
What to Check Before You Order
For a consumable kit, the safest buying method is to confirm three points first:
- Machine identity: confirm the exact plasma unit and torch family in service.
- Consumable style: confirm whether your torch uses the same electrode, nozzle, shield, and retaining arrangement as the kit you are sourcing.
- Wear pattern: inspect your current parts and compare the wear to the symptoms on the floor.
Check: Look for arc instability, rough edge quality, excessive dross, or difficulty transferring arc. These are common reasons crews replace consumables early.
Inspect: Remove the current tip stack and inspect for pitting, distortion, heat damage, or gas-flow contamination. Examine the torch body for damage that would shorten consumable life.
Verify: Match the replacement parts to the exact service documents or parts diagram for your setup. If a component cannot be confirmed from the source listing, list it as Unknown (Verify).
Replacement-Part Breakdown
The product is identified as an essential consumable kit. That means the useful breakdown is functional, not speculative. In plasma service, the common wear components are typically the electrode, nozzle, shield or deflector, and retaining components. However, the exact contents of this kit should be confirmed from the source listing or packaging.
- Electrode: Carries the arc load and is a primary wear item.
- Nozzle: Shapes the arc and affects cut quality and kerf consistency.
- Shield/deflector: Helps protect the torch and can influence cut standoff behavior.
- Retaining hardware: Holds the consumable stack in position. Any damage or thread wear can affect retention.
If the kit contents are not explicitly confirmed by your purchase source, do not assume the stack includes every item above. Mark unknown contents as Unknown (Verify) and cross-check the carton or listing before dispatching it to the field.
Troubleshooting and Support Checks
When a plasma cutter starts cutting poorly, do not jump straight to machine repair. Consumables are the first inspection point.
Check: Inspect the nozzle orifice for enlargement, oval wear, or spatter contamination.
Inspect: Examine the electrode face for a deep pit or uneven erosion.
Verify: Confirm that the shield and retaining parts are not cracked, cross-threaded, or seated incorrectly.
Check: If the arc starts but cuts are inconsistent, verify air quality, line pressure at the machine, and the condition of the consumable stack.
Inspect: Look for moisture, oil, or debris in the air line and filter path. Contaminated air shortens consumable life.
Verify: Make sure the torch is assembled in the correct order. A mis-stacked consumable set can create the same symptoms as a worn part.
Check: If you see repeated consumable burn-back, inspect duty cycle and operating technique.
Inspect: Review cut travel speed, pierce height, and standoff consistency.
Verify: Confirm that the operator is using the correct technique for the workpiece thickness and edge condition.
Product and Parts Section
Product referenced: Hypertherm 851462 Powermax30 AIR Essential Consumable Kit
ASIN: B01CSBV3FE
Amazon affiliate product reference:
No products found.
Use this product as a replacement consumable source only. Do not assume it changes the procedure, the duty cycle, or the machine configuration. If your maintenance program requires serialized parts control, record the kit identification and the installation date when the parts are issued.
Part verification step:
- Confirm the machine and torch model in service.
- Open the existing consumable stack and compare wear against the replacement parts.
- Verify that each part matches the required stack order.
- Install only after fit and seating are confirmed.
- Test cut on approved scrap material before returning the unit to production.
Safety Notes
- De-energize the system before service.
- Allow hot parts to cool before handling.
- Wear eye protection and gloves during inspection and replacement.
- Do not touch electrode or nozzle surfaces with bare hands if contamination control is required by your shop practice.
- Use approved torch and machine procedures only. Unknown (Verify) settings should not be guessed in the field.
FAQ
Q: Is this kit for routine maintenance or repair?
A: Routine maintenance. Consumables are wear parts and are replaced as performance declines.
Q: Can I assume the kit fits every Powermax30 system?
A: No. Verify the exact machine and torch configuration before ordering. Compatibility details not confirmed in the source should be treated as Unknown (Verify).
Q: What causes consumables to wear out early?
A: Common causes include poor air quality, incorrect cut technique, excessive pierce abuse, and contaminated or damaged torch components.
Q: What should I do if the replacement parts do not match my existing stack?
A: Stop and verify the part numbers against the machine manual, torch diagram, or current packaging before installation.
Sources Checked
- Provided Amazon product reference: ASIN B01CSBV3FE
- Provided product name: Hypertherm 851462 Powermax30 AIR Essential Consumable Kit
- Allowed internal links: none provided for lookup or filler-metal support on this task
- Internal link supplied by user: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog
Note: No raw Amazon URL was used. Any unconfirmed content details remain Unknown (Verify).
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
Related Weld Support Guides
Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack: Product Breakdown
“>
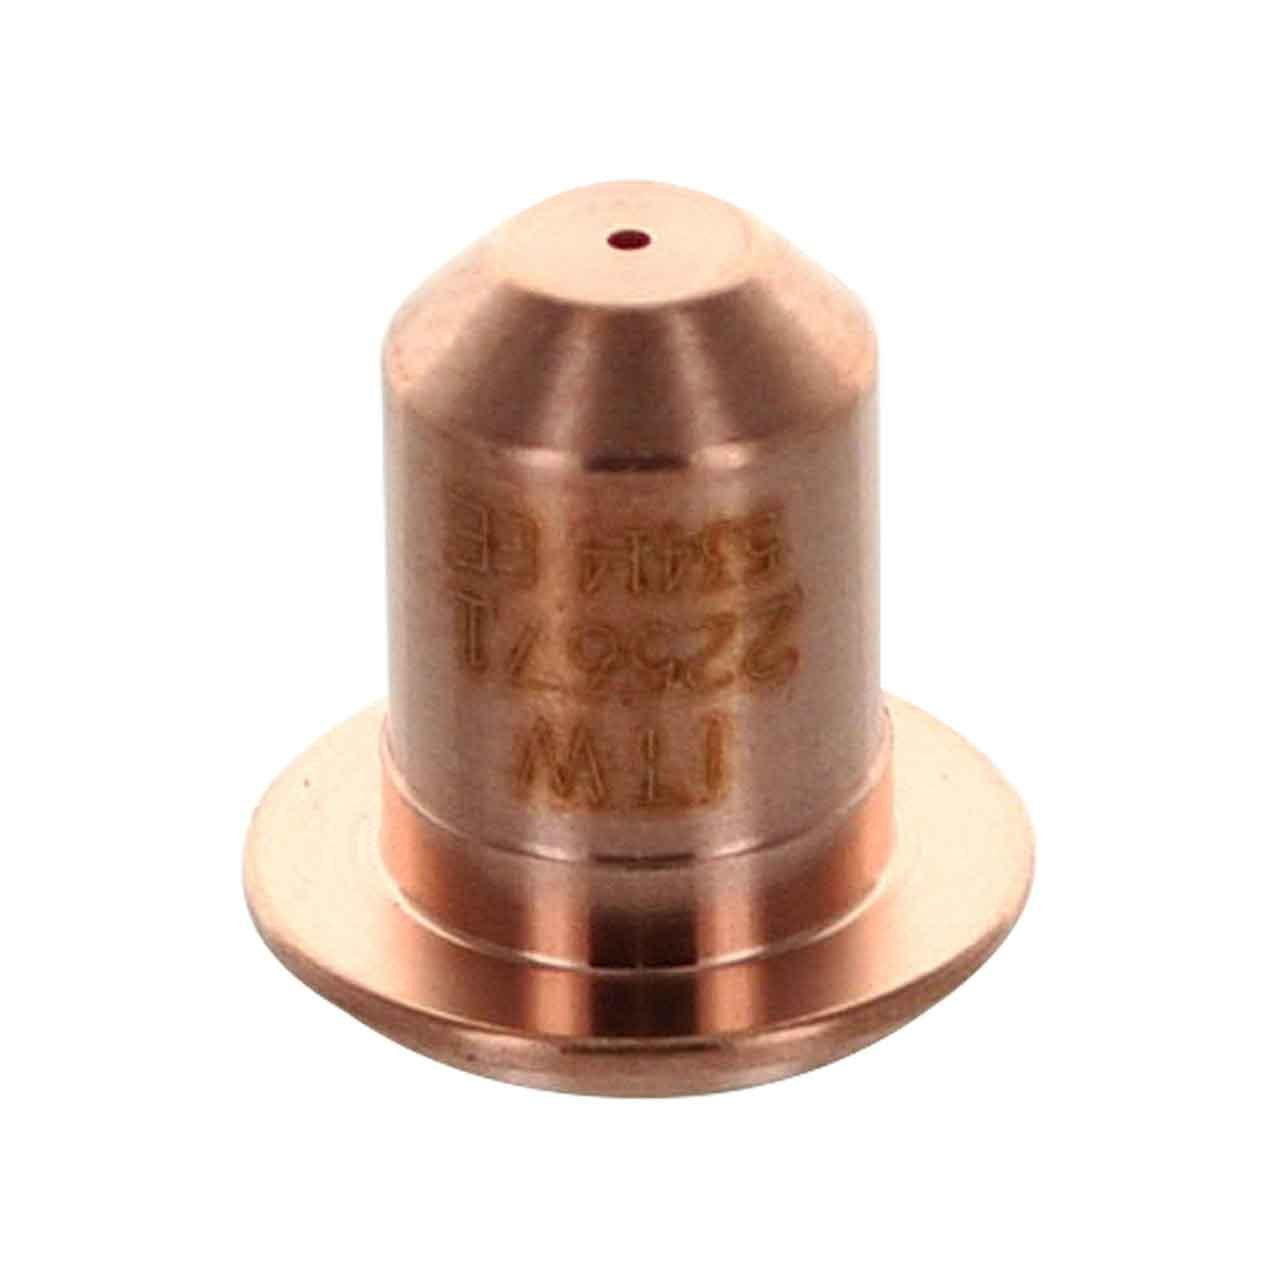
The Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack is a torch consumable package for plasma cutting support work. For buyers and maintenance teams, the key question is not just whether the tip is on the shelf, but whether it matches the torch system, amperage range, and wear pattern your crew is actually running. This part is listed as an extended tip for the ICE-27C plasma cutter torch and is associated with Miller Spectrum 375 and 3765 X-tremes plasma cutters based on the product source provided. Confirm the torch model on the equipment before ordering or installing.
Key takeaways
- This is a 5-pack of consumable tips.
- It is identified as an extended tip for the ICE-27C torch.
- Source material ties it to Miller Spectrum 375 and 3765 X-tremes plasma cutters.
- Do not assume fit from the machine name alone. Verify torch model and consumable designation at the unit.
- Use wear checks, not guesswork, to decide when to replace the tip.
What this part does
Plasma tips focus the cutting arc and help control cut quality. As the tip wears, cut performance can shift in ways that are easy to spot in the field: rougher edges, more dross, unstable arc starts, or visible damage at the orifice. The right replacement restores the torch’s intended arc shape, but only if the whole consumable stack and torch are in proper condition.
Because this is a consumable, the buying decision is usually about consistency and uptime. Maintenance teams should stock tips based on actual torch usage, not only on machine count. If a torch is heavily used on production cuts, tips should be treated as planned replacement items, not emergency parts.
Check, inspect, verify before install
Use this sequence before installing a new tip:
- Check the torch model. Confirm the torch is ICE-27C or ICE-27T as applicable to your setup. If the torch designation is unclear, mark it as Unknown (Verify) and stop until the model is confirmed.
- Inspect the consumable stack. Look at the electrode, shield, swirl ring, retaining hardware, and tip seat. A new tip will not correct damage elsewhere in the stack.
- Verify amperage use. The product title identifies 25Amp. Verify your operating setup against the torch and machine manual before use.
- Check for heat and contamination. Carbon, spatter, moisture, and torch body damage can shorten tip life. Clean the torch components only according to the machine manual.
- Verify correct seating. Install the tip fully and evenly. If seating feels inconsistent, stop and inspect the torch body and mating parts.
Troubleshooting support for poor cut quality
If cut quality drops after a tip change, do not assume the new tip is defective. Work through the torch system first.
Problem: rough edge or heavy dross
- Check whether the tip is worn, damaged, or installed incorrectly.
- Inspect the work speed, standoff, and material condition.
- Verify the torch components are the correct series for the machine.
Problem: unstable arc or hard starts
- Check the electrode and tip together. A new tip with a worn electrode can still misbehave.
- Inspect for contamination in the torch or air delivery path.
- Verify air quality, machine settings, and torch compatibility against the manual. Unknown (Verify) if documentation is not available at the work area.
Problem: repeated short tip life
- Check for contact with the workpiece or excessive drag.
- Inspect the torch body for heat damage, cracked components, or loose parts.
- Verify operator technique and consumable handling. Tips should not be forced into place.
Parts and application notes
This product listing identifies the part as a Miller consumable for the ICE-27C torch, with application to Miller Spectrum 375 and 3765 X-tremes plasma cutters per the source data provided. That is the safest level of identification available here. Any further compatibility detail is Unknown (Verify) until checked against the machine manual, torch label, or internal maintenance record.
For buyers, the main control points are straightforward:
- Match the torch designation first.
- Match the amperage and consumable family second.
- Confirm the replacement count in the package before issuing stock.
- Record the tip as a tracked wear item so ordering is based on usage, not panic replacement.
How maintenance teams should stock it
Consumables like this tip are best managed with a simple issue-and-replace process. Keep the package sealed until needed, label inventory by torch family, and separate plasma consumables by system if your shop uses more than one torch platform. Mixing tips by appearance alone is a common cause of downtime. Use the part number and torch designation for stock control.
If your site uses a formal parts approval process, tie the tip to the machine asset record and the torch serial or family record where possible. If that record is missing, the compatibility status is Unknown (Verify) and should be confirmed before release to production.
Safety notes
- De-energize the equipment before servicing consumables.
- Allow hot components to cool before handling.
- Follow the machine and torch manual for installation, cleaning, and replacement steps.
- Do not force consumables into a torch body.
- Wear suitable hand and eye protection for plasma service work.
FAQ
Is this tip only for the ICE-27C torch?
The source listing identifies it as an extended tip for the ICE-27C plasma cutter torch. Any use beyond that is Unknown (Verify) and should be checked against the torch and machine documentation.
Can I use this with a Spectrum 375 or 3765 X-tremes unit?
The provided source says the torch is on Miller Spectrum 375 and 3765 X-tremes plasma cutters. Verify your exact machine and torch configuration before ordering or installing.
What should I inspect if the new tip does not improve cut quality?
Inspect the electrode, shield, swirl ring, torch body, air quality, and operator technique. A new tip alone will not fix wear or contamination elsewhere in the system.
How should I decide when to replace the tip?
Replace it when wear is visible, cut quality declines, or the arc becomes unstable. If the condition is uncertain, mark it Unknown (Verify) and inspect the full consumable set.
Sources checked
- ArcWeld product source: Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack
- Provided product short description and source URL
Related Arc Weld Part
Miller 225671 Tip, ICE- 27C/27T 25Amp, 5 pack
Miller 225671 Extended Tips. This is for the ICE-27C plasma cutter torch. Which is on the Miller Spectrum 375 and 3765 X-tremes plasma cutters. Package of 5
View at Arc Weld Store