Tag: maintenance

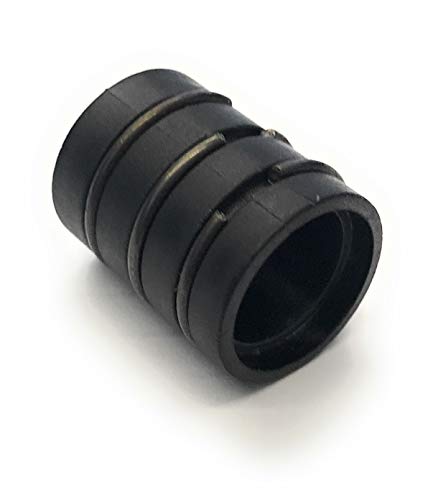
  • AN RG-300-12 36″ ROD GUARD, Pack of (1): Replacement Part Breakdown

    Rod storage looks simple until consumables get damaged, contaminated, or misplaced on the job. The AN RG-300-12 36″ Rod Guard, Pack of (1) is listed here as a replacement part reference for buyers and maintenance teams that need a basic storage or protection component for stick electrodes. The key question is not just whether it exists, but whether it matches the way your crew stores rods, handles boxes, and moves material between the bench, the truck, and the jobsite.

    This guide focuses on replacement-part breakdown, what to inspect before ordering or installing, and how to verify that the part belongs in your support setup. Any unconfirmed technical detail should be treated as Unknown (Verify).

    Key Takeaways

    • The product is identified as AN RG-300-12 36″ ROD GUARD, Pack of (1), ASIN B00VJ3A0CK.
    • Use this as a replacement part verification step, not as a substitute for confirming fit.
    • Do not assume rod diameter, closure style, mounting method, or material construction. If not documented in your source data, mark it Unknown (Verify).
    • Inspect the surrounding storage system, not just the guard itself. Damage often comes from impact, heat, or poor handling.
    • For purchasing teams, confirm the guard against the current asset list, carton labeling, and any internal maintenance record before release.

    What This Part Is Used For

    A rod guard is generally used to protect welding electrodes or related consumables during storage and handling. In a stick welding environment, that matters because rod condition affects usability. Moisture, contamination, bent packages, and crushed containers can create waste and slow the work.

    For this specific listing, treat the function as a storage-protection component and verify all details that affect fit or use. If your operation relies on a particular holder, tube, bracket, or carry method, compare the guard to the existing unit before purchase.

    Replacement Part Breakdown: What to Check

    Before you approve this item as a replacement, work through a short breakdown process.

    1) Identify the Existing Part

    • Check the current rod guard or storage tube for visible part markings.
    • Inspect the overall length and physical configuration of the installed item.
    • Verify whether the old part was damaged by impact, heat, wear, or missing hardware.

    2) Confirm the Storage Requirement

    • Check whether the crew needs a guard for daily transport, bench storage, or long-term electrode protection.
    • Inspect the environment for moisture, dust, and physical handling risk.
    • Verify whether your process requires a sealed tube, open guard, or another form of protection. Unknown (Verify) if not documented.

    3) Match the Replacement to the Application

    • Check the current mounting or carry method.
    • Inspect the replacement part dimensions against the removed part.
    • Verify that the replacement does not interfere with adjacent tools, holders, or storage racks.

    Troubleshooting Before You Buy

    When a rod guard is being replaced, the failure may not be the guard alone. Use this support checklist.

    If Rods Are Getting Dirty or Damaged

    • Check the guard for cracks, open seams, or missing caps.
    • Inspect the storage area for contact with grinding dust, oil, or moisture.
    • Verify whether rods are being returned to a dry storage location after use.

    If the Guard Was Lost or Mixed Up

    • Check jobsite labeling and inventory records.
    • Inspect the purchase history and part number references.
    • Verify the actual replacement before installation or issue to the crew.

    If the Part Does Not Fit

    • Check whether the original part was modified.
    • Inspect the replacement against the original part side by side.
    • Verify dimensions, mounting points, and closure method directly from the source listing or receiving paperwork. Unknown (Verify) if not stated.

    Product and Parts Reference

    The available product reference for this article is the Amazon-registered item below. Use it as a procurement reference only after fit and application checks are complete.

    AN RG-300-12 36″ ROD GUARD, Pack of (1)
    ASIN: B00VJ3A0CK
    Amazon shortcode:

    No products found.

    Do not assume compatibility with every rod storage setup. The identifying information confirms the listing, not your specific application. If you manage multiple stick welding stations, compare the old part, the equipment record, and the receiving label before ordering extras.

    How Maintenance Buyers Should Verify the Part

    For purchasing and maintenance teams, the best process is simple and repeatable:

    1. Check the ASIN or item reference against the approved part list.
    2. Inspect the old component, including length, shape, and attachment points.
    3. Verify the replacement against the same physical sample or drawing.
    4. Confirm the issue date of the order and the job location.
    5. Document any unknown details as Unknown (Verify) instead of guessing.

    That process prevents false matches and reduces returns. It also helps when a part number is referenced informally by the crew but not tied to a controlled asset record.

    Safety Notes

    • Keep electrode storage dry and away from contaminants.
    • Do not use a damaged guard if it cannot protect the rods from dirt, impact, or moisture.
    • Handle welding consumables according to site procedure and the manufacturer’s instructions for the rod type in use.
    • If any feature of the guard is not clearly documented, treat it as Unknown (Verify) before field use.

    FAQ

    Is this a consumable or a replacement support part?

    It is treated here as a replacement support part for rod storage and handling. Verify the exact role in your setup before purchase.

    Can I assume the rod size or mounting method from the product name?

    No. The product name includes “36″,” but any more detailed fit, mounting, or compatibility information is Unknown (Verify) unless it is confirmed in the source listing or your internal records.

    What should I compare before ordering?

    Compare the old part, any part number on the asset, the physical length, the attachment method, and the storage application. If any item is unclear, mark it Unknown (Verify).

    Can this guide confirm procedure approval for specific electrodes?

    No. It is a buyer and replacement-part guide only. Procedure approval, electrode handling, and storage requirements must come from your welding procedure, site rules, or manufacturer documentation.

    Sources Checked

    • Allowed Amazon product reference: AN RG-300-12 36″ ROD GUARD, Pack of (1), ASIN B00VJ3A0CK
    • Provided internal link review for stick welding support context
    • No WSP lookup page was provided in the allowed sources for this task
    • No filler metal finder page was provided in the allowed sources for this task

    Related reading: Welding Electrode Holder: Stinger Guide & Stick Welding Tips

    Related reading: Welding Electrode Holder: Choose the Best for Stick Welding

    Related reading: Stick Welding Arc Blow Causes and Fixes: Magnetic Arc Deflection, Ground Clamp Placement, AC/DC Settings, and Weld Sequence
    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

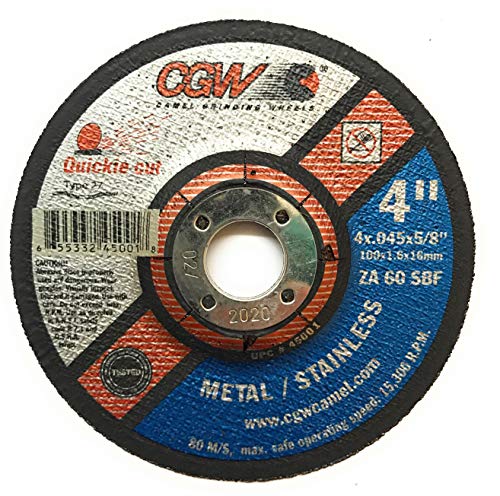
  • CGW 45001, Cut-Off Wheel 4″ x 5/8″, Type 27, Pack of (25): Product Breakdown

    CGW 45001, Cut-Off Wheel 4″ x 5/8″, Type 27, Pack of (25): Product Breakdown

    Product not found.
    “>CGW 45001, Cut-Off Wheel 4" x 5/8", Type 27, Pack of (25)

    The CGW 45001 cut-off wheel is a small-diameter abrasive wheel intended for cutting tasks in metal fabrication and maintenance work. The listed product data identifies it as a 4-inch wheel with a 5/8-inch center hole, Type 27 form, and pack quantity of 25. The available source data also identifies zirconia aluminum oxide abrasive, 60 grit, medium grade, and a maximum speed of 19,000 RPM. Use those details as the starting point for selection, setup, and inspection. Do not assume more than the source confirms.

    Key Takeaways

    • Confirm grinder arbor size before buying or mounting. This wheel is listed with a 5/8-inch center hole.
    • Confirm wheel type and application. Type 27 is commonly used for angle grinder work, but actual use depends on the tool, guard, and job.
    • Do not exceed the listed maximum speed of 19,000 RPM.
    • Inspect every wheel before use. Do not install cracked, chipped, or dropped wheels.
    • Use the wheel only for the material and cutting method supported by the source data. The listing states carbon and stainless steels. Other applications are Unknown (Verify).

    Product Breakdown

    The source product listing for CGW 45001, Cut-Off Wheel 4″ x 5/8″, Type 27, Pack of (25) identifies it as a CGW Abrasives wheel built with zirconia aluminum oxide abrasive. The wheel size is 4 inches in diameter with a 5/8-inch center hole. The wheel type is Type 27. Grit is listed as 60 and grade as medium. Maximum speed is listed as 19,000 RPM.

    That combination points to a wheel intended for general cutting support in shop and field maintenance work. The source specifically mentions cutting carbon and stainless steels. Anything beyond that is Unknown (Verify).

    How to Check Fit Before Use

    Before mounting this wheel, verify the grinder and accessory interface. Cutting wheel failures often start with the wrong size, wrong flange setup, or a damaged tool.

    • Check arbor size: Confirm the grinder arbor matches the 5/8-inch center hole.
    • Inspect the guard: Verify the guard is installed, secure, and positioned for cutting work.
    • Inspect flanges: Verify the flanges are clean, flat, and free of nicks or debris.
    • Check the speed rating: Verify the grinder’s no-load speed does not exceed 19,000 RPM.
    • Check the wheel face: Verify there are no cracks, chips, moisture damage, or edge damage before mounting.

    Installation and Setup Checks

    Use a simple pre-use routine. This helps reduce runout, wobble, and early wheel damage.

    1. Disconnect power before changing the wheel.
    2. Remove the old wheel and clean both flanges.
    3. Inspect the spindle, nut, and guard for damage.
    4. Install the new wheel without forcing it onto the arbor.
    5. Seat the wheel evenly between the flanges.
    6. Snug the retaining nut to the tool maker’s instructions. Do not overtighten.
    7. Spin the wheel by hand and verify it clears the guard and does not contact the work support.
    8. Run the tool briefly at no load and verify no abnormal vibration, noise, or wobble.

    Troubleshooting Cutting Problems

    If the wheel is not cutting cleanly, do not assume the wheel is defective. Check the setup and the work process first.

    Problem: Wheel vibrates or wobbles

    • Inspect: Look for a bent flange, dirty mounting surfaces, or a damaged wheel.
    • Verify: Confirm the center hole and arbor are the correct match.
    • Check: Make sure the wheel is seated flat and the nut is not cocked.
    • Action: Replace the wheel if it has been dropped or shows any damage.

    For more detail on vibration causes, see Cut-Off Wheel Vibration Troubleshooting: Grinder Wobble, Wheel Runout, Flange Problems, and Unsafe Cutting Symptoms.

    Problem: Slow cut or excessive pressure needed

    • Inspect: Check whether the wheel is loaded, glazed, or worn down.
    • Verify: Confirm the material is actually carbon steel or stainless steel if following the source guidance.
    • Check: Reduce side loading and keep the cut straight.
    • Action: Replace the wheel if cutting performance drops below acceptable shop standards.

    Problem: Wheel wears faster than expected

    • Inspect: Verify grinder speed and pressure technique.
    • Check: Avoid twisting, binding, or forcing the cut.
    • Verify: Confirm the wheel is appropriate for the workpiece thickness and cut method. If not, this is Unknown (Verify).

    How to Evaluate Whether This Wheel Fits the Job

    Maintenance buyers and supervisors should compare the task to the source data rather than rely on general assumptions. Use this wheel as a candidate when you need a 4-inch Type 27 wheel with a 5/8-inch bore and a 19,000 RPM limit. The source says it is for carbon and stainless steels. If the job involves another alloy, a different grinder class, or a special cutting method, verify compatibility before issue.

    If you need help understanding Type 1 versus Type 27 cut-off wheel selection, review Type 1 and Type 27 Cut-Off Wheels: Pros, Cons, and Applications.

    Safety Notes

    • Wear eye protection, face protection, hearing protection, gloves, long sleeves, and suitable clothing.
    • Keep the guard installed. Do not run abrasive wheels unguarded.
    • Do not use a damaged wheel.
    • Do not exceed the listed maximum RPM.
    • Keep hands out of the cut line and avoid side loading unless the wheel and tool setup support it. If uncertain, verify with the tool maker’s instructions.
    • Stop immediately if the wheel develops cracking, vibration, or unusual sound.

    FAQ

    Is the CGW 45001 wheel for stainless steel?
    The source listing states it is for cutting carbon and stainless steels. Verify the exact stainless grade and job conditions before use.

    What grinder does it fit?
    The source provides a 5/8-inch center hole and a 4-inch diameter. Exact tool compatibility is Unknown (Verify). Match the arbor, guard, and speed rating to the grinder manufacturer’s instructions.

    Can this wheel be used above 19,000 RPM?
    No. The source lists a maximum of 19,000 RPM. Do not exceed that value.

    What does Type 27 mean here?
    Type 27 is the wheel form listed by the source. Use it only when the grinder, guard, and application are suitable. For a broader breakdown of Type 27 use, verify against the tool and wheel manufacturer data.

    Sources Checked

    Note: All uncertain compatibility and application details are marked as Unknown (Verify). Do not infer approvals or certifications not stated in the source data.

    Related Arc Weld Part

    CGW 45001, Cut-Off Wheel 4" x 5/8", Type 27, Pack of (25)

    CGW 45001, Cut-Off Wheel 4" x 5/8", Type 27, Pack of (25)

    CGW Abrasives 45001 Cut-Off Wheel 4" x 5/8" 60 Grit Type 27 Zirconia Aluminium Oxide General purpose cutting wheel. Zirconia grain for faster cutting and longer life. For cutting carbon and stainless steels. Specification: BRAND: CGW Abrasives ABRASIVE MATERIAL: Zirconia Aluminum Oxide GRIT: 60 GRADE: Medium DIAMETER INCHES: 4 CENTER HOLE DIAMETER INCHES: 5/8 MAX RPM: 19000 WHEEL TYPE: Type 27 TOOL COMPATIBILITY:…

    View at Arc Weld Store

    Related Weld Support Guides

  • Hypertherm Air T30 Torch Parts Breakdown: Parts Lookup and Buying Checks

    Hypertherm Air T30 Torch Parts Breakdown: Parts Lookup and Buying Checks

    Hypertherm Air T30 Torch Parts Breakdown

    The Hypertherm Air T30 torch support path is a parts-lookup problem before it is a buying problem. For maintenance buyers and weld shop support teams, the main risk is ordering a consumable or service part by name instead of confirming the torch family, cut mode, and part interface. The result is wasted time, mismatched hardware, or a torch that will not assemble correctly.

    This guide is a practical breakdown for the Hypertherm Air T30 Torch Parts Breakdown process. It focuses on what to inspect, what to verify before ordering, and how to use the Weld Support Parts lookup page as a starting point for parts identification.

    Key Takeaways

    • Start with torch family identification, not the cut tip alone.
    • Verify retaining hardware, shield style, nozzle style, and electrode condition before ordering.
    • Do not assume compatibility from a similar Hypertherm torch name.
    • Use the WSP lookup page as the source page for parts identification, then confirm against the torch in hand.
    • When a detail is uncertain, mark it as Unknown (Verify) and confirm from the machine, torch label, or service documentation.

    What the Air T30 Parts Breakdown Should Cover

    For a torch service check, the useful breakdown is the set of wear parts and torch-side service items that affect arc start, cut quality, and torch assembly. That usually includes the electrode, nozzle, shield or drag shield style if used, retaining cap or retaining hardware, swirl ring or gas distribution component if used, and any torch body or lead-side service items that are specific to the torch family.

    For this support path, the source page is the place to begin the lookup:

    Hypertherm Air T30 hand torch support on Weld Support Parts

    Use that page to identify the support path, then verify the exact torch and consumable set before placing an order.

    Check the Torch Before You Buy

    Do not order from memory. A fast visual inspection often prevents the wrong part from being purchased.

    • Check the torch label. Confirm the torch family and any visible model marking. If unreadable, note it as Unknown (Verify).
    • Inspect the retaining hardware. Verify whether the cap, shield, or front-end hardware matches the torch you have in service.
    • Inspect the nozzle and electrode wear. Look for pit wear, heat discoloration, erosion, and arc damage.
    • Verify the front-end stack-up. Count the parts in the assembly as removed, and compare that stack to the lookup page or service parts breakdown.
    • Check for cut-quality symptoms. Heavy dross, arc wandering, or repeated pilot-arc issues may indicate worn consumables rather than a power supply fault.

    Troubleshooting Support: Where Parts Checks Matter

    Many torch problems look electrical at first but are actually consumable-related. Before replacing components upstream, inspect the torch front end.

    1) No-start or weak start

    • Inspect the electrode and nozzle for obvious wear or burn damage.
    • Verify the torch stack is assembled correctly and tightened to the correct feel for the design, not over-torqued.
    • Check for contamination, moisture, or debris in the torch front end.

    2) Pilot arc dropout

    • Inspect the retaining hardware and front-end fit.
    • Verify the consumables are the correct family for the Air T30 support path.
    • Check lead condition, damage at the torch neck, and any visible burn-through.

    3) Poor cut quality

    • Inspect nozzle orifice wear and edge damage.
    • Verify the shield or drag shield style against the torch setup in use.
    • Check the work clamp, air quality, and cut technique before replacing parts again.

    For a deeper fault tree, the internal support article on pilot arc issues is a useful follow-up:

    Plasma Cutter Pilot Arc Failure Troubleshooting

    Buying Checks for Service Parts

    When you move from inspection to purchasing, treat every line item as a verification step.

    • Check part family first. The torch family must match the support path.
    • Inspect the old part. Compare shape, thread style, contact surfaces, and overall length. If the old part is damaged beyond comparison, mark the detail Unknown (Verify).
    • Verify the assembly count. Some torch fronts use multiple small parts that are easy to miss.
    • Confirm the use case. Drag cutting, standoff cutting, or shielded use may require different front-end hardware. If not confirmed, the requirement is Unknown (Verify).
    • Do not substitute by brand alone. Similar plasma parts are not interchangeable without verification.

    If you need a methodical way to compare drag-shield and front-end configurations, use this internal reference:

    Plasma Drag Shield Compatibility Guide

    WSP Lookup Section

    Use the Weld Support Parts lookup page as the starting point for the Air T30 support path:

    View the Hypertherm Air T30 hand torch support page

    Practical workflow:

    1. Open the lookup page.
    2. Match the torch family to the machine and torch in service.
    3. Remove and inspect the worn parts.
    4. Compare the old parts to the page listing and any internal support notes.
    5. Only then place the order.

    Any item that cannot be confirmed from the torch, the page, or service paperwork should remain Unknown (Verify) until checked.

    Safety Notes

    • De-energize the plasma system before removing torch parts.
    • Allow the torch to cool before handling front-end consumables.
    • Do not inspect burned parts by touch immediately after use.
    • Use eye protection when cleaning the torch front end.
    • Do not mix unknown parts into a live torch assembly.

    FAQ

    How do I know if the Air T30 part I need is a consumable or a service part?

    Check the wear pattern and location. Front-end items such as electrodes, nozzles, shields, and retaining hardware are consumable-facing. Torch-body, lead-side, or connector items are service parts. If the category is unclear, label it Unknown (Verify) and compare against the lookup page.

    Can I order by torch name only?

    No. Torch name alone is not enough. Verify the exact torch family, front-end stack, and cut mode before ordering.

    What should I do if the old part is too damaged to identify?

    Use the torch label, machine model, and the support page as reference points. If a detail still cannot be confirmed, keep it as Unknown (Verify) until checked against service documentation or a known-good assembly.

    Why does a torch sometimes fail even when the power supply is fine?

    Worn or mismatched consumables can cause no-start, weak arc, dropout, and poor cut quality. Start with the torch front end before replacing larger components.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • S19417 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2): Product Breakdown

    S19417 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2): Product Breakdown

    Product not found.
    “>S19417 Lincoln Style Nozzle Insulator - Arc Weld by Masterweld Pack of (2)

    The S19417 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2) is a MIG support part meant for a specific torch-component stack. According to the product source, it is a Lincoln style nozzle insulator, it is used with the S19418 gas diffuser, and it does not work with PRO series equipment. That is the core buying point: this is a fitment-sensitive part, not a universal consumable.

    For welders and maintenance buyers, the practical question is not only “what is it?” but “will it match the torch setup already in service?” This article keeps the focus on verification steps, fit checks, and support-side troubleshooting before the part is installed into production use.

    Key Takeaways

    • This part is identified as a Lincoln style nozzle insulator.
    • It is intended to be used with the S19418 gas diffuser.
    • It does not work with PRO series equipment, per the product source.
    • Fitment should be verified before ordering replacement parts for the bench, cart, or job trailer.
    • Unknown (Verify) for any torch-family details not stated in the source listing.

    What This Part Does

    A nozzle insulator sits in the consumable stack and helps isolate and position the nozzle assembly relative to the diffuser and contact area. In practical shop use, that means the part needs to match the torch design closely. If the geometry is wrong, the nozzle may not seat correctly, or the assembly may not maintain the intended spacing.

    Because the source data only confirms the Lincoln style designation, the S19418 diffuser pairing, and the PRO series exclusion, any deeper compatibility claims are Unknown (Verify). Do not assume it will interchange with all Lincoln-pattern MIG guns or all aftermarket diffuser designs.

    Buyer Check: Before You Order

    • Check the torch family. Confirm the gun on the machine is not a PRO series setup.
    • Inspect the diffuser part number. Verify whether the torch uses the S19418 gas diffuser named in the source.
    • Compare the worn part. Pull the old insulator and compare profile, seating shape, and thread or snap features as applicable. Unknown (Verify) on retention style if the old part is missing.
    • Check the nozzle stack. Confirm the nozzle, diffuser, and insulator all belong to the same consumable system.
    • Verify the purchase quantity. This listing is a pack of (2), so confirm the maintenance need matches the pack size.

    Installation and Support Checks

    Use the following checks during replacement and return-to-service:

    • Inspect: Look for heat damage, cracking, distortion, or carbon buildup on the removed insulator.
    • Verify: The replacement insulator seats fully on the intended diffuser without forcing the fit.
    • Check: The nozzle installs straight and does not wobble after the insulator is in place.
    • Inspect: Contact tips and diffusers for wear that could make a good insulator appear defective.
    • Verify: The assembled consumable stack clears the workpiece and maintains the expected nozzle position.

    If the nozzle will not seat, do not grind the insulator to make it fit. That usually indicates a mismatch in the torch system, a worn diffuser, or the wrong consumable family. Unknown (Verify) for any workaround not stated in the source.

    Troubleshooting Support

    Problem: Nozzle will not seat correctly

    • Inspect the diffuser model and confirm it is the S19418 gas diffuser called out by the source.
    • Verify the torch is not a PRO series unit.
    • Check for spatter, deformation, or thread damage in the mating parts.

    Problem: Consumable life is short

    • Inspect the welding process for excessive spatter that may be loading the nozzle area.
    • Verify shielding gas coverage and stickout practices at the torch setup level.
    • Check whether the insulator is being used in the correct torch family. Mismatch can create abnormal wear.

    Problem: Replacements do not match the old part

    • Compare the removed part against the supplier image and part description.
    • Verify the torch manufacturer and model before reordering.
    • Confirm whether the old part was already an aftermarket substitute. Unknown (Verify).

    Product and Parts Notes

    This article only uses the product information supplied for the Arc Weld by Masterweld listing. The available facts are limited to the Lincoln style nozzle insulator designation, the S19418 diffuser pairing, and the PRO series limitation. No additional specs, dimensions, materials, or certifications are provided here because they were not supplied in the source data.

    If you are building a stocking plan, treat this part as a torch-specific support item. Stocking the wrong consumable family creates avoidable downtime. The quickest support check is to pull one unit from the tool crib and compare it to the torch in service before ordering multiples.

    Product reference:

    S19417 Lincoln Style Nozzle Insulator - Arc Weld by Masterweld Pack of (2)

    S19417 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2)

    Lincoln Style Nozzle Insulator – Use with S19418 gas diffuser – Does not work with PRO series

    View at Arc Weld Store

    Related Reading

    For another consumable example and a different material category, see this internal Weld Support Parts post: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog. Use it as a reference for how filler metal content is organized, not as a compatibility guide for this nozzle insulator.

    Safety Notes

    • Shut down and lock out welding equipment before changing consumables where your site rules require it.
    • Allow hot parts to cool before handling.
    • Do not force mismatched parts together to keep a job moving.
    • After installation, verify the nozzle stack is secure before striking an arc.
    • If the torch shows heat damage, inspect the full consumable set before returning it to service.

    FAQ

    Is this insulator universal across Lincoln-style MIG guns?

    No. The source only confirms Lincoln style and the S19418 diffuser pairing. Universal use is Unknown (Verify).

    Can it be used with PRO series equipment?

    No according to the product source. It states that it does not work with PRO series.

    What should I verify before ordering a replacement?

    Check the torch family, confirm the diffuser part number, compare the old part to the new part, and verify that the setup is not a PRO series unit.

    Does the listing provide material, dimensions, or certifications?

    No. Those details are not provided in the source data and should be treated as Unknown (Verify).

    Sources Checked

    • Arc Weld product listing: S19417 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2)
    • Provided source note: use with S19418 gas diffuser; does not work with PRO series
    • Provided internal link: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog

    Related Weld Support Guides

  • Lincoln KP2743-1-62R Nozzle, Thread-on, 1/8R, 5/8 ID, Pack of (1): Replacement Part Breakdown

    This page breaks down the Lincoln KP2743-1-62R Nozzle, Thread-on, 1/8R, 5/8 ID, Pack of (1) as a replacement part listing for maintenance and purchasing review. Use it to confirm the part number, inspect the current nozzle condition, and verify fit before ordering. Do not assume compatibility from the product name alone. Verify the gun model, consumable family, and thread-on interface against your equipment records.

    Key Takeaways

    • This is a replacement nozzle listing tied to part number KP2743-1-62R.
    • The product title indicates a thread-on nozzle with 1/8R and 5/8 ID; exact machine and gun compatibility is Unknown (Verify).
    • Use the part number first, then verify physical dimensions and thread style against the installed nozzle.
    • Check for spatter buildup, arc instability, and contact-tip-to-nozzle alignment before replacing parts.
    • This article is a buyer and support guide, not a substitute for the gun manual or Lincoln parts list.

    What this part is used for

    A MIG nozzle directs shielding gas and helps protect the weld zone from contamination. In daily use, the nozzle is also exposed to spatter, heat, and handling damage. A worn nozzle may still install on the gun, but it can cause poor gas coverage, excessive cleanup, or inconsistent performance.

    For this listing, the only confirmed product identifier available here is the Amazon ASIN reference B008BJD92S and the product name provided above. Any deeper fitment details, gun series compatibility, or Lincoln cross-reference should be treated as Unknown (Verify) unless confirmed in the manufacturer documentation or your parts database.

    Inspect before you replace

    Before ordering a replacement, inspect the current nozzle and the rest of the front-end consumables. A nozzle problem is sometimes caused by another worn part.

    • Check the nozzle bore: Look for heavy spatter, oval wear, or internal distortion.
    • Inspect the threads: Verify the thread-on connection is clean and not galled, stripped, or cross-threaded.
    • Verify tip centering: Check whether the contact tip sits centered in the nozzle opening.
    • Inspect the diffuser/retainer area: Damage there can make a new nozzle fit poorly.
    • Check for heat discoloration: Excessive heat signs can indicate duty cycle, technique, or fitment issues.

    Troubleshooting support: common signs and checks

    If you are seeing performance problems, use a simple inspection path before authorizing replacement:

    • Gas shielding looks weak: Check for nozzle blockage, loose threads, damaged seals, or incorrect nozzle size. Verify gas flow at the torch separately.
    • Spatter buildup increases quickly: Inspect wire stickout, technique, process settings, and anti-spatter practices. A worn nozzle may be a symptom, not the root cause.
    • Arc starts become inconsistent: Verify contact tip condition, liner condition, and nozzle alignment.
    • Nozzle will not thread on smoothly: Stop and inspect the gun neck threads. Do not force installation.
    • Visible burnback or overheating: Verify consumable fit and process parameters. Unknown (Verify) on exact operational limits for this part without the gun manual.

    Check / Inspect / Verify steps

    1. Check the current nozzle part number if it is still legible.
    2. Inspect the thread-on interface for damage, contamination, or spatter lock.
    3. Verify the gun model and consumable series from the parts diagram or maintenance record.
    4. Check the contact tip size and seating position.
    5. Verify whether the nozzle dimensions on the listing match the nozzle removed from service.

    Product / parts section

    Product: Lincoln KP2743-1-62R Nozzle, Thread-on, 1/8R, 5/8 ID, Pack of (1)

    ASIN reference: B008BJD92S

    Availability, certification, and price: Unknown (Verify)

    Compatibility: Unknown (Verify). Confirm against the exact gun and parts list before purchase.

    View the referenced product listing

    Use the product listing as a procurement reference only. Do not use the title alone to approve fitment for production use. If you are supporting a fleet of welders, compare the installed nozzle against this part number, then confirm the neck thread pattern and the gun family in the service manual.

    Replacement decision: when to replace

    Replace the nozzle when cleaning no longer restores a stable bore, when threads are damaged, or when the part no longer seats correctly. If the nozzle can be cleaned and reinstalled without loss of fit, the support team may choose to keep it in service. Verify the shop standard before returning a worn part to production.

    If a replacement is ordered, record the old part number, the machine ID, and the reason for replacement. That log helps maintenance buyers avoid repeated mismatches.

    Safety notes

    • Allow the torch to cool before handling the nozzle.
    • Wear gloves and eye protection when removing spatter or checking threads.
    • Do not force a threaded consumable into damaged threads.
    • Verify the welding power source is de-energized or in a safe state before service.
    • Use only approved shop procedures for consumable cleaning and replacement.

    FAQ

    Is this nozzle guaranteed to fit my Lincoln gun?

    No. Compatibility is Unknown (Verify) from the information provided here. Confirm the exact gun model and parts diagram before ordering.

    What does thread-on mean?

    It indicates a nozzle that installs by threading onto the torch neck or related front-end assembly. Verify the exact thread form and seating method on your equipment.

    What should I check if the nozzle keeps filling with spatter?

    Check technique, gas coverage, contact tip condition, and any damage to the nozzle bore. A replacement may help, but the root cause may be elsewhere.

    Can I use this listing as an approval for procedure settings?

    No. A parts listing is not a procedure approval. Use the welding procedure, gun manual, and shop standards for operating settings.

    Sources Checked

    • Provided product data for Lincoln KP2743-1-62R Nozzle, Thread-on, 1/8R, 5/8 ID, Pack of (1)
    • Provided ASIN reference: B008BJD92S
    • Provided internal link rules: no WSP lookup link provided, no filler metal link provided

    Note: No WSP lookup page or filler metal finder page was provided in the allowed links for this draft, so none is included here.

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1): Product Breakdown

    Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1): Product Breakdown

    Product not found.
    “>Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1)

    If a MIG gun starts feeding erratically, the liner is one of the first wear parts to inspect. The Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1) is listed as a 1/16″ x 25′ zinc plated MB spring wire liner intended for certain Tweco MIG gun families. For maintenance buyers and welding support teams, the key question is not just what the part is called, but whether it matches the gun, wire, and feed path you are servicing.

    This breakdown stays focused on practical use: what to verify before ordering, what to inspect during install, and how to troubleshoot feeding problems after replacement. Where technical details are not confirmed by the provided source, they are marked Unknown (Verify).

    Key Takeaways

    What This Part Does

    A MIG gun liner guides wire from the feeder through the cable to the contact tip. In service, the liner must stay smooth internally and properly matched to the wire being run. A spring-style liner can support feeding in heavier-duty applications, but the correct selection still depends on the specific gun and application. The source listing identifies the liner as zinc plated MB spring wire liner, but any additional material details beyond that are Unknown (Verify).

    Check Before You Order

    Use these checks before replacing a liner:

    Verify: If the existing liner was changed to solve a problem once before, confirm whether the root cause was actually the liner or another part of the feed system. Drive rolls, inlet guides, gun neck angle, and cable routing can create similar symptoms.

    Troubleshooting Support

    When wire feed is unstable, go through the system in order.

    1) Feed from the feeder first

    2) Move to the cable

    3) Check the liner itself

    4) Confirm the contact tip and neck components

    If feeding improves after the liner change but problems return quickly, do not assume the liner was the only issue. Verify wire quality, spool condition, and whether the process is pushing the gun beyond its normal duty conditions. Any exact compatibility outside the product listing remains Unknown (Verify).

    Installing a Replacement Liner: Practical Steps

    1. Power down the machine and isolate the welding circuit.
    2. Remove the consumables and release wire tension.
    3. Withdraw the old liner carefully to avoid leaving fragments in the cable.
    4. Inspect the cable path for debris, wear, or internal obstruction.
    5. Insert the new liner slowly and keep it from kinking.
    6. Trim only as required by the gun setup after confirming length and seating.
    7. Reassemble the gun and reinstall consumables.
    8. Test feed at low speed first, then verify under normal operating settings.

    Verify: The source listing does not provide installation tolerances, trim allowances, or torque values. Those details are Unknown (Verify) and should be taken from the gun manufacturer’s service documentation.

    When to Replace Instead of Clean

    Cleaning can help when the liner is only contaminated. Replacement is usually the better choice when the liner is scored, rusted, crushed, or repeatedly causing drag after the rest of the feed path has been checked. If a gun is used in a high-production environment, a liner may become a scheduled wear item rather than an emergency repair part.

    Product and Parts Notes

    The provided ArcWeld product listing identifies this item as the Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1). The short description states it is a 1/16″ x 25′ zinc plated MB spring wire liner for use with 300 – 500 amp Tweco Eliminator, Tweco Spray Master, Tweco No. 3, Tweco No. 4, and Tweco No. 5 X-Gun MIG guns. No additional compatibility should be assumed beyond that listing. If your gun variant differs from the named families, verify before ordering.

    Product reference:

    Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1)

    Tweco 44-116-25, Replacement Liner/Conduit, Pack of (1)

    Tweco Model 44-116-25 1/16" X 25' Zinc Plated MB Spring Wire Liner For Use With 300 – 500 Amp Tweco® Eliminator®, Tweco® Spray Master®, Tweco® No. 3, Tweco® No. 4, Tweco® No. 5 X-Gun MIG Guns

    View at Arc Weld Store

    For related feed-wire context, see this internal article: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog. That page is not a liner guide, but it can help support teams think through wire handling and feed consistency when reviewing the whole system.

    Safety Notes

    FAQ

    Is the Tweco 44-116-25 a complete gun?

    No. It is a replacement liner/conduit only, based on the provided product listing.

    Can I use this liner on any Tweco gun?

    No. The listing names specific Tweco gun families, but final fit still needs to be verified against your exact model and cable setup. Unknown (Verify) for any unlisted variants.

    What usually causes feeding issues if the liner is new?

    Drive roll tension, damaged cable routing, incorrect tip size, dirty wire, or a mismatched liner can still cause feed problems. Verify the full feed path, not just the liner.

    Should I clean the old liner or replace it?

    Clean only if contamination is the likely issue and the liner is still in serviceable condition. Replace it if there is scoring, rust, deformation, or recurring drag.

    Sources Checked

    Related Weld Support Guides

  • Hypertherm 220990, 105 Amp Nozzles for Powermax 105, Pack of (5): Replacement Part Breakdown

    Hypertherm 220990 is a consumable replacement nozzle pack listed for Powermax 105 use. For buyers and maintenance teams, the main job is not just ordering the part; it is confirming that the nozzle match is correct for the torch, amperage setting, and current wear condition. Consumables fail in ways that affect cut quality fast, so replacement decisions should be based on inspection, not guesswork.

    This guide breaks down what to check before you buy, how to inspect the nozzle stack after shutdown, and how to troubleshoot the symptoms that usually point to nozzle wear or mismatch. Product details beyond the listing itself are marked Unknown (Verify) when not confirmed.

    Key Takeaways

    • Hypertherm 220990 is listed as a 105 amp nozzle pack for Powermax 105 use.
    • Consumable replacement should follow visual inspection and cut-quality symptoms, not only runtime.
    • Check the full torch consumable stack, not just the nozzle, before ordering parts.
    • If fitment, torch family, or amperage is not confirmed, use Unknown (Verify) until verified by the equipment manual or parts list.
    • Use the Amazon product box below as a buying reference only; do not assume compatibility beyond the listing title.

    What this part is for

    The listing identifies this item as a nozzle replacement pack for a Hypertherm Powermax 105 system. In plasma cutting, the nozzle controls the constricted arc as it exits the torch. When the nozzle wears, the arc can lose focus and the cut can become wider, rougher, or less stable. That is why nozzle replacement is part of routine torch maintenance.

    Do not assume this nozzle is interchangeable with other amperage ratings or other Powermax models unless you verify the torch manual, the OEM parts list, or the markings on the existing consumables. If the exact torch or cartridge arrangement is not confirmed, mark it Unknown (Verify).

    Check before you order

    1. Inspect the torch model. Verify the machine and torch are actually Powermax 105 compatible.
    2. Check the nozzle rating. Confirm the current nozzle is a 105 amp nozzle, not a different amp class.
    3. Inspect the consumable stack. Look at the nozzle, electrode, swirl ring, shield, retaining cap, and any retaining hardware.
    4. Verify the wear pattern. Excessive pit formation, ovality, meltback, or arc instability suggests replacement is due.
    5. Confirm count and pack size. The product title shows a pack of five; verify that is what you need for stock or service planning.

    Troubleshooting: when to suspect nozzle wear

    If cut quality changes, the nozzle may be the cause, but it is not the only cause. Use a simple inspection sequence.

    Check

    • Check for a wider-than-normal kerf.
    • Check for heavy dross that appears suddenly after a period of normal cutting.
    • Check for an unstable arc or frequent arc transfer problems.
    • Check for visible heat damage on the nozzle or adjacent consumables.

    Inspect

    • Inspect the nozzle orifice for distortion, enlargement, or meltback.
    • Inspect the electrode for wear; a new nozzle with a worn electrode can still cut poorly.
    • Inspect the shield and swirl ring for contamination, cracking, or heat damage.
    • Inspect the torch body and retaining parts for debris, looseness, or damaged threads.

    Verify

    • Verify the amperage setting matches the consumable rating.
    • Verify the air supply is clean and dry.
    • Verify the torch assembly is seated correctly.
    • Verify the part number against the OEM parts list before stocking replacements.

    If the cut problem remains after replacing the nozzle, the issue may be elsewhere in the stack or in system setup. In that case, the nozzle is not the sole corrective action.

    Replacement support notes for maintenance buyers

    For shops that keep consumables on hand, part control matters. Separate nozzles by torch model and amperage class. Do not mix open stock between similar-looking plasma parts. A correct-looking nozzle with the wrong internal geometry can create false confidence and waste labor time.

    When you receive replacement parts, compare them against the old part before installation. Match the outside dimensions, contact surfaces, and visible openings as far as the OEM design allows. If any feature is unclear, treat it as Unknown (Verify) and stop before installation.

    Product / parts reference

    Hypertherm 220990, 105 Amp Nozzles for Powermax 105, Pack of (5)

    Amazon product reference:

    No products found.

    Use this as the identified replacement listing only. Do not infer additional specifications, certifications, or machine compatibility beyond the product title unless you verify them from the OEM documentation.

    Safety notes

    • De-energize the plasma system before any consumable inspection or replacement.
    • Allow the torch and consumables to cool before handling.
    • Use eye protection and gloves when inspecting used plasma consumables.
    • Do not install damaged parts just to finish a job; damaged consumables can worsen cut quality and increase torch wear.
    • Keep compressed air and debris away from the work area during maintenance.

    FAQ

    Is this nozzle pack confirmed for every Powermax 105 torch?

    No. The listing title says it is for Powermax 105 use, but exact torch and configuration compatibility should still be verified against the OEM parts list. If unconfirmed, mark it Unknown (Verify).

    Can I replace only the nozzle if cut quality drops?

    Sometimes, but not always. Inspect the electrode, swirl ring, shield, and retaining parts as a set. A fresh nozzle will not fix damage or contamination in the rest of the consumable stack.

    What is the fastest way to tell if the nozzle is worn out?

    Look for visible orifice distortion, heat damage, or a cut that suddenly becomes wider and less stable. Then verify the amperage setting and air quality before ordering parts.

    Should I stock this part without testing the torch first?

    Only if your equipment records already confirm the torch model and consumable class. If not, verify the machine and torch details before putting the part into stock.

    Sources Checked

    • Provided Amazon product reference for ASIN B00KCPSYGA via allowed product shortcode
    • Internal project brief and topic metadata

    Note: No WSP lookup page or filler metal finder page was provided for this task, so no such internal links were added.

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Hobart Handler 140EZ MIG Welder Support: Parts Lookup and Buying Checks

    Hobart Handler 140EZ MIG Welder Support: Parts Lookup and Buying Checks

    Hobart Handler 140EZ MIG Welder Support

    The Hobart Handler 140EZ is a compact MIG setup, but support work still comes down to the same basics: confirm the machine variant, identify the gun and feeder parts you actually have, and verify consumable fit before placing an order. This guide is built for buyers, maintenance techs, and welders who need to replace worn items without guessing.

    Key Takeaways

    • Start with the machine support page before you buy parts or consumables.
    • Verify gun type, drive roll style, wire size, and contact tip fit before ordering.
    • Do not assume the package contents match a unit that has been modified in service.
    • Use filler metal pages as a selection starting point, not as a guarantee of procedure approval.
    • If a compatibility point is not confirmed on the support page, mark it as Unknown (Verify).

    What to Check on a Hobart Handler 140EZ Before Ordering Parts

    Before you order anything, inspect the machine as it sits in the shop. A unit that has been in service may have a different gun, cable length, liner, drive roll, or wire path than the original package. That affects what will fit.

    Check

    • Confirm the exact machine model on the nameplate.
    • Inspect the gun and cable for wear, cuts, heat damage, or a loose neck connection.
    • Look at the drive rolls and note the wire size marking if present.
    • Verify the installed contact tip size and thread style before buying replacements.
    • Check the wire spool size and wire type currently in use.

    Inspect

    • Feed path: look for dust, liner wear, or birdnesting signs.
    • Contact tip: check for arc instability, oval wear, or spatter buildup.
    • Nozzle: inspect for spatter closure, heat distortion, or missing insulator parts.
    • Drive system: verify whether the roll surface matches the wire you run.

    Verify

    • Confirm whether the installed gun is the HM-100 MIG gun referenced on the support page.
    • Verify whether the unit uses a SpoolRunner 150 arrangement or a standard feeder setup, if applicable to your machine. Unknown (Verify) if not confirmed by the support page or machine inspection.
    • Verify the wire diameter you intend to run before ordering tips, liners, or rolls.

    WSP Lookup: Hobart Handler 140EZ Support Page

    The primary starting point for this model is the Weld Support Parts support page here: Hobart Handler 140EZ MIG Welder Support.

    Use that page to review the model-specific support notes, listed package contents, and the consumable and accessory references tied to the Hobart Handler 140EZ. The page also references the HM-100 MIG gun, the SpoolRunner 150, drive rolls, and consumable part links. If a part or configuration is not explicitly confirmed there, treat it as Unknown (Verify).

    Practical buying check: compare the support page against your machine in the shop. If the machine has been repaired, upgraded, or altered, do not rely on memory or a prior invoice. Check the machine first, then match the part family.

    Troubleshooting Support: Common Ordering Mistakes to Avoid

    Most support problems happen before the order is placed. The wrong consumable or gun component may still look close enough to fit, but a close visual match is not enough.

    Check for these issues

    • Wrong wire diameter selected for tips and drive rolls.
    • Wrong gun family selected after a previous service swap.
    • Mixed consumable parts from different setups.
    • Assuming package contents are still original after ownership changes.
    • Replacing the liner or tip without checking the feeder condition.

    Inspect, then verify

    • Inspect the tip seat: confirm whether the existing tip threads or seats match the replacement part you plan to order.
    • Inspect the roll grooves: look for wear or polishing that suggests the roll has been used with a different wire size.
    • Verify the liner length and routing: if the gun cable has been replaced or shortened, liner fit may not match the original configuration. Unknown (Verify) if not documented.
    • Verify the consumable family: use the support page references, not guesswork from a similar Hobart machine.

    Drive Rolls, Tips, and Gun Parts: What to Match

    For a MIG feeder, the most common replacement items are drive rolls, contact tips, nozzles, liners, and the gun itself. Matching starts with the wire and ends with the feeder hardware.

    • Drive rolls: match roll type to wire type and wire size as confirmed on the machine.
    • Contact tips: match the tip to wire diameter and the correct gun family.
    • Nozzles and insulators: match the gun assembly shown on the support page or on the installed gun.
    • Liners: verify liner style and length before purchase. Unknown (Verify) if the machine has been modified.
    • Gun assembly: confirm whether you need the HM-100 MIG gun or another setup before ordering.

    Filler Metal Finder: Use It as a Starting Point

    If you are also selecting wire, use the Weld Support Parts filler metal content and wire selection resources as a starting point, not as a final approval document. A useful reference is this internal guide: Best MIG Wire for Stainless Steel (ER308L vs ER309L).

    That page helps frame selection decisions, but it does not replace procedure approval, WPS requirements, or base-metal review. For any production job, verify the required wire classification, shielding gas, and procedure requirements against your shop documentation. Unknown (Verify) if not documented.

    Buying Checks for Maintenance and Purchasing

    • Match the support page to the machine serial/model label.
    • Confirm whether the current gun and feeder parts are original or field-replaced.
    • Order by verified wire size and gun family, not by appearance.
    • Keep a record of the installed consumable part numbers after replacement.
    • When in doubt, stop and verify before opening the package for install.

    Safety Notes

    • Disconnect input power before inspection or part replacement.
    • Let the gun and nozzle cool before handling after welding.
    • Wear eye protection when checking the wire path, drive rolls, or contact tip area.
    • Do not run damaged gun cables, cracked nozzles, or worn liners in service.
    • Use the correct PPE and follow your shop lockout practices.

    FAQ

    How do I know which parts fit the Hobart Handler 140EZ?

    Start with the dedicated WSP support page for the model, then inspect the machine in the shop. Match the gun, consumables, and drive components to what is installed. If the part family is not confirmed, treat it as Unknown (Verify).

    Can I buy consumables based only on the model name?

    No. The model name is a starting point, not enough by itself. Confirm wire size, gun type, and the actual feeder setup before ordering tips, rolls, or liners.

    Is the SpoolRunner 150 definitely part of every Hobart Handler 140EZ package?

    No. The support page references the SpoolRunner 150, but package contents can vary by listing, revision, or prior modification. Verify the installed configuration before purchase.

    Can I use filler metal pages to approve a production weld procedure?

    No. Use filler metal pages to narrow down likely wire options only. Final approval must come from your WPS, procedure documents, or engineering requirements.

    Sources Checked

    All uncertain technical details should be verified against the machine in service and the referenced support page before ordering.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Metabo W11-125 Quick 9.6-Amp 5-Inch Angle Grinder: Replacement Part Breakdown

    The Metabo W11-125 Quick 9.6-Amp 5-Inch Angle Grinder is a common shop tool, but any grinder that sees regular cutting, grinding, and cleanup work will eventually need service. Bearings wear, brushes shorten, switches fail, cords get damaged, and guards or flanges get misplaced. For maintenance buyers and shop support teams, the useful question is not just what the grinder is called, but what can be checked, what can be replaced, and what must be verified before returning it to service.

    This guide is a practical replacement part breakdown for the Metabo W11-125 Quick B001CS9U5A. It does not assume a specific parts diagram or service kit unless verified by the manufacturer or seller documentation. Where technical details are not confirmed, they are listed as Unknown (Verify).

    Key Takeaways

    • Start with inspection, not part ordering. Many grinder failures look electrical but begin with mechanical wear.
    • Verify the exact model and serial information before ordering replacement parts.
    • Do not assume cross-compatibility with other 5-inch grinders.
    • Use original documentation or a verified parts breakdown when possible.
    • When a part detail is unclear, mark it Unknown (Verify) instead of guessing.

    What to Check First

    Before removing covers or ordering parts, confirm the symptom. This saves time and reduces the chance of replacing the wrong component.

    Check

    • Does the grinder start intermittently, not at all, or only under load?
    • Is there unusual vibration, noise, sparking, or heat?
    • Does the spindle turn freely by hand with the tool unplugged?
    • Are the guard, flange, wheel, and spindle lock operating correctly?

    Inspect

    • Power cord: cuts, crushed sections, exposed conductors, loose strain relief.
    • Switch: stiffness, arcing smell, intermittent contact.
    • Brushes and brush caps: wear length, spring pressure, carbon dust buildup. Exact brush dimensions: Unknown (Verify).
    • Bearings and gears: rough rotation, noise, side play, grease leakage.
    • Spindle and flange threads: damage, galling, or contamination.

    Verify

    • Tool model designation matches the service part source.
    • Voltage, amperage, and electrical configuration are verified from the nameplate or documentation before any electrical repair.
    • Any replacement guard, switch, brushes, bearings, or cord set is confirmed for this exact model or confirmed by the manufacturer as compatible.

    Replacement Part Breakdown: Typical Service Areas

    A grinder of this class usually has several serviceable areas. The exact part list for the Metabo W11-125 Quick should be taken from a verified parts diagram or service manual. The categories below are the parts most often inspected during maintenance.

    1. Power cord and strain relief

    The cord is one of the first wear points. Repeated bending near the entry point can break conductors inside the jacket before damage is visible outside.

    • Check for soft spots, cuts, flattened sections, or warm spots after brief operation.
    • Inspect the strain relief where the cord enters the housing.
    • Verify continuity and conductor integrity before reuse.

    2. On/off switch

    A failed switch often shows up as intermittent operation, delayed start, or no start. Dust and heat can shorten switch life in abrasive work.

    • Check for positive actuation and full return.
    • Inspect for discoloration, melted plastic, or loose terminals.
    • Verify switch replacement by exact model reference, not only by physical appearance.

    3. Carbon brushes

    Brush wear is routine on brushed motors. Short brushes can cause loss of power, excessive sparking, or stop-start behavior.

    • Inspect brush length and spring pressure.
    • Check the commutator area for heavy scoring or carbon dust.
    • Verify brush part number and dimensions from the correct parts source. Brush size for this model: Unknown (Verify).

    4. Bearings

    Worn bearings usually present as noise, rough rotation, or shaft play. If a bearing failure is ignored, the motor and gear train can be damaged further.

    • Rotate the shaft by hand with the tool unplugged.
    • Listen for grinding, rumbling, or scraping.
    • Verify bearing numbers from the service diagram or after teardown. Bearing numbers: Unknown (Verify).

    5. Gear set and spindle assembly

    Grinding work loads the gear train heavily. Impact loading, wheel pinch, and poor lubrication can damage gears or the spindle.

    • Inspect for chipped teeth, abnormal backlash, or metal debris in the housing.
    • Check spindle lock engagement and release.
    • Verify whether the spindle, flange, and lock components are sold separately or only as assemblies through the verified parts source.

    6. Guard, flange, and wheel hardware

    These are not wear items in the same way as brushes or bearings, but they are critical to safe operation.

    • Inspect the guard for cracks, deformation, and secure clamping.
    • Check backing flange and locking nut for damage or thread wear.
    • Verify wheel size and speed rating from the wheel label before installation. Wheel compatibility for this tool: Unknown (Verify) unless confirmed by the manufacturer documentation.

    Troubleshooting Support Flow

    Use this sequence when the grinder is out of service.

    1. Unplug the tool. Confirm zero power before any inspection.
    2. Check the cord and plug first. Many no-start complaints come from cord damage rather than internal failure.
    3. Inspect the switch. If the cord checks out, move to the switch and terminal connections.
    4. Spin the shaft by hand. Rough rotation points toward bearings or gear damage.
    5. Inspect brushes. If the motor runs but performs poorly, brush wear is a common cause.
    6. Verify the parts source. Do not order based on photos alone.

    If the problem is heat, smell, or sparking, stop use and inspect before applying power again. If the problem is mechanical binding, do not force the spindle lock or wheel hardware.

    How to Order the Right Replacement Part

    For a buyer guide, the most important control is identification. Do not rely on a generic “fits 5-inch grinder” claim.

    • Check the nameplate and record the exact model designation.
    • Use the verified parts breakdown or manufacturer service information if available.
    • Match the electrical and mechanical details before purchase.
    • If a part number cannot be confirmed, hold the order and verify with the seller or manufacturer.

    Product reference for this article:

    No products found.

    Safety Notes

    • Disconnect power before inspection, service, or part removal.
    • Do not defeat the guard, spindle lock, or switch mechanisms.
    • Use only wheels and accessories rated for the operating speed and application.
    • After replacement, perform a no-load test in a controlled area before returning the tool to production use.
    • If there is evidence of insulation damage, burned wiring, or internal arcing, remove the tool from service until repaired by a qualified technician.

    FAQ

    What parts wear out first on a grinder like this?

    Common wear items are the cord, switch, carbon brushes, bearings, and spindle hardware. Actual wear depends on duty cycle and the type of abrasive work.

    Can I order parts by appearance only?

    No. Appearance is not enough for safe ordering. Verify the exact model, part number, and source documentation before purchase.

    Is every 5-inch grinder part interchangeable?

    No. Size alone does not confirm compatibility. Switches, brushes, bearings, guards, and spindle parts may differ even between similar tools.

    What should I do if the tool runs but sounds rough?

    Unplug it and inspect the bearings, gears, wheel hardware, and spindle for wear or debris. Do not continue running a grinder that sounds rough under no-load conditions.

    Sources Checked

    • Provided Amazon product reference for Metabo W11-125 Quick B001CS9U5A
    • Task instructions and allowed-source constraints

    Note: No WSP lookup page, filler metal finder page, internal links, or additional verified product links were provided for this draft. No compatibility claims were made beyond what could be verified from the supplied source data.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

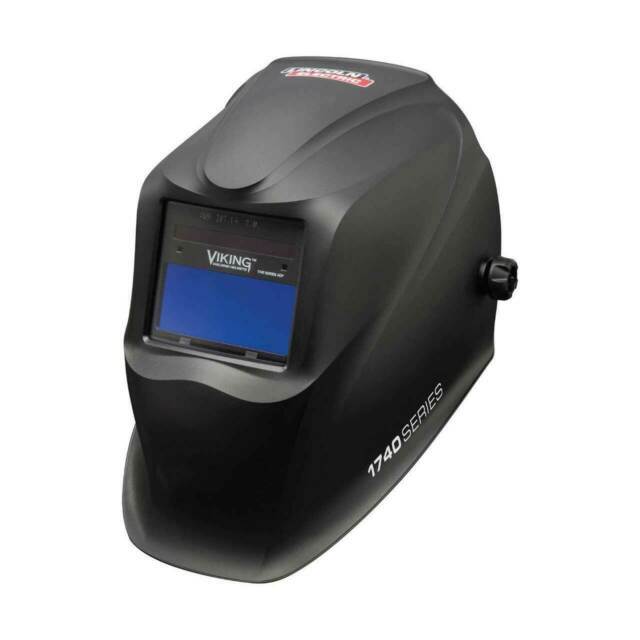
  • Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3: Product Breakdown

    Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3: Product Breakdown

    Product not found.
    “>Lincoln Viking 1740 Auto-Darkening Welding Helmet - K3282-3

    The Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3 is a welding PPE item intended for day-to-day fabrication and repair work where a stable view of the weld zone matters. For buyers and support teams, the main question is not whether the helmet is “advanced,” but whether it fits the job, the user, and the maintenance routine. On a shop floor, consistent lens response, proper fit, and basic inspection discipline matter more than marketing terms.

    Key Takeaways

    What this helmet is for

    Based on the product description provided, this helmet is aimed at general fabrication and repair, shop work, field welding, and common arc processes such as MIG, TIG, and stick. The practical value of an auto-darkening helmet is simple: it lets the welder see the work area clearly before the arc starts, then darkens when the arc is struck. That reduces the need to repeatedly nod the hood up and down and can help reduce eye strain during repetitive work.

    For maintenance buyers, the priority is not just the helmet model name. It is whether the unit supports the welders’ actual tasks, how often consumable parts are checked, and whether the team has a repeatable inspection routine. If the application includes grinding, overhead welds, tight access work, or frequent start-stop cycles, the helmet must stay comfortable and reliable enough to avoid operator workarounds.

    Product / parts notes

    This article is limited to the product listing provided. Specific technical specs, lens sizes, shade ranges, sensor counts, and certification details were not supplied here, so they are Unknown (Verify). Do not assume compatibility with aftermarket headgear, cover lenses, or cartridge-style replacements unless the manufacturer documentation confirms it.

    For shop support, verify the following before issue or deployment:

    Troubleshooting and support checks

    1) Lens does not darken consistently

    2) Helmet feels loose or shifts during work

    3) Visibility is poor even when the hood is up

    How to inspect before use

    1. Visual check: look over the shell for cracks, heat damage, and spatter.
    2. Lens check: inspect both cover surfaces for scratches, haze, or debris.
    3. Fit check: put the helmet on and verify secure headgear contact without pressure points that force the user to loosen the hood.
    4. Function check: perform a controlled arc-response test if shop procedure allows it.
    5. Record check: note any recurring issue, especially if the same helmet is being reassigned between shifts.

    Related support references

    If you are comparing this model to adjacent Lincoln helmet support content, these internal pages may help with broader helmet selection and setup context:

    Safety notes

    FAQ

    Is the Lincoln Viking 1740 K3282-3 suitable for MIG, TIG, and stick welding?

    The provided product description says it is intended for daily MIG, TIG, and stick work. Specific duty limits, settings, and procedure approvals are Unknown (Verify).

    Can I use this helmet as a direct replacement for other Lincoln Viking models?

    Not without verification. Compatibility with other models, covers, headgear parts, or accessories is Unknown (Verify) unless the manufacturer documentation confirms it.

    What should I inspect first if the helmet starts acting up?

    Start with the basics: lens cleanliness, cover condition, sensor obstruction, headgear fit, and shell damage. In many cases, the issue is a contaminated cover lens or a loosened adjustment point.

    How often should the helmet be checked?

    At minimum, check it before each use. For shared helmets or high-volume shops, add shift-start and post-incident checks after drops, spatter strikes, or heavy grinding exposure.

    Sources Checked

    For procurement or support decisions, keep the focus on fit, function, and inspection discipline. If a technical detail is not documented in the available source material, treat it as Unknown (Verify) before buying or issuing the helmet to the floor.

    Related Arc Weld Part

    Lincoln Viking 1740 Auto-Darkening Welding Helmet - K3282-3

    Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3

    Lincoln Viking 1740 Auto-Darkening Welding Helmet (K3282-3) is a professional-grade auto-darkening hood built for daily MIG, TIG, and stick work where clear visibility and consistent shade response matter. It’s designed to reduce eye strain by giving you a bright, high-clarity view of the puddle and joint before and during the arc. What it’s for General fabrication and repair Shop and field welding Processes with…

    View at Arc Weld Store

    Related Weld Support Guides

  • Watch with Prime Video