• Weldmark TIG Collet Body #9, 20, 25 Torch Pk = 5 (13N27-1/16″) Replacement Part Breakdown

    The Weldmark TIG Collet Body #9, 20, 25 Torch Pk = 5 (13N27-1/16″) is a replacement torch component used in the collet stack. In practical terms, this part helps locate and support the tungsten and collet assembly inside the torch head. If the tungsten slips, the arc becomes inconsistent, or the consumable stack will not assemble correctly, the collet body is one of the first parts to inspect.

    This article is a buyer and troubleshooting guide for maintenance teams, welders, and parts buyers who need to verify whether the part is the right replacement before ordering. Use the checks below to confirm condition, fit, and application. Do not assume compatibility from the torch size alone. Verify the torch model, internal thread pattern, and consumable family before installation.

    Key Takeaways

    • This is a replacement collet body for TIG torch consumable stacks, not a universal part.
    • Fit depends on torch series and consumable system. Verify the torch before ordering.
    • Wear, heat damage, and cross-threading can cause tungsten slippage and poor arc stability.
    • If the tungsten will not clamp securely, inspect the full stack: collet, collet body, back cap, and cup.
    • Use the product listing as a reference point only. Confirm dimensions and compatibility in your own setup.

    What the part does

    The collet body sits inside the TIG torch head and works with the collet to hold the tungsten in position. When the internal bore or external thread area is worn, the tungsten may not stay fixed. That can show up as a wandering arc, inconsistent stickout, or visible damage to the consumable stack.

    For support teams, the most useful question is not simply “is the part available?” It is “does the torch need this part, and does the replacement match the torch body and consumable family?” In many cases, the failure is not the collet body alone. A worn collet, cracked cup, damaged insulator, or heat-distorted back cap can create the same complaint.

    Troubleshooting: when to suspect the collet body

    • Tungsten slips even when the collet is tightened correctly.
    • Arc starts are inconsistent after repeated tungsten regrinds and resets.
    • Threads feel rough, gritty, or no longer engage smoothly.
    • Consumables overheat, discolor, or show localized galling near the torch head.
    • The torch requires more tightening than usual to hold the electrode.

    Check

    Remove the cup, back cap, collet, and tungsten. Check the collet body for heat tint, spatter, nicks, deformation, or thread damage. Look for signs that the bore is no longer round or that the electrode seat is worn.

    Inspect

    Inspect the mating parts as a set. A damaged collet can mimic a bad collet body. A bent tungsten can also make the assembly feel loose or unstable. If the torch head has been dropped, inspect for cracked insulators and distorted internal hardware.

    Verify

    Verify the torch model and consumable series before ordering a replacement. If the torch identification is unreadable, compare the current parts to a known sample from the same torch family. When compatibility is uncertain, record it as Unknown (Verify) and do not release the order until confirmed.

    Replacement decision points

    Replace the collet body when the wear is mechanical and repeatable. That includes damaged threads, obvious heat distortion, or a bore that no longer supports the tungsten properly. If the only issue is poor arc quality, do not stop at the collet body. Check gas coverage, tungsten condition, power settings, and work lead connection as well.

    If the torch has repeated overheating, address the cause before installing new parts. A replacement consumable will not solve a cooling issue, an oversize tungsten for the application, or abuse from excessive duty cycle.

    Product / parts section

    The referenced product is the Weldmark TIG Collet Body #9, 20, 25 Torch Pk = 5 (13N27-1/16″). The available ASIN in the Forge OS registry is B071SHY115. Use the product box below as the checkout reference point.

    No products found.

    Before purchase, verify the following:

    • Torches supported by this part in your shop.
    • Whether the torch uses this exact collet body style or a different consumable family.
    • Required tungsten diameter and matching collet size. Unknown (Verify) if not documented.
    • Whether the part count in the package matches your maintenance requirement.

    Install and support checks

    1. Power down the welding machine and isolate the torch.
    2. Disassemble the cup, back cap, collet, and tungsten.
    3. Clean the torch head threads and consumable seats.
    4. Compare the old and new collet body side by side.
    5. Hand-start threads only. Do not force engagement.
    6. Install the tungsten and confirm it clamps securely without excessive force.
    7. Test the torch on a controlled setup before returning it to production.

    If the torch still slips after replacement, verify the collet size, tungsten diameter, and mating consumables. Also check for heat damage in the torch head. Do not keep tightening hardware past normal hand torque just to make the tungsten stay put.

    Related support articles

    Safety notes

    • Shut down and isolate the power source before disassembly.
    • Allow hot torch parts to cool before handling.
    • Do not use damaged consumables that will not thread or seat correctly.
    • If the torch shows heat damage beyond the consumable stack, remove it from service until inspected.
    • Use PPE when handling worn tungsten, sharp collet edges, or contaminated parts.

    FAQ

    How do I know if the collet body is the problem?

    Start with the symptom. If the tungsten slips, the threads feel damaged, or the torch head shows repeatable wear at the same point, inspect the collet body. If the issue is only arc instability, verify the entire torch setup before replacing parts.

    Can I confirm compatibility from the product title alone?

    No. The title is a starting point, not proof of fit. Verify the torch series, consumable family, and tungsten size before ordering. If documentation is incomplete, mark the match as Unknown (Verify).

    What else should be replaced with a worn collet body?

    Inspect the collet, tungsten, cup, back cap, and insulator. Replace any part that is cracked, heat damaged, or no longer threads and seats correctly. A worn collet body often appears alongside other consumable wear.

    Does a new collet body fix poor arc performance by itself?

    Not always. It may fix tungsten clamping issues, but arc quality also depends on gas flow, tungsten prep, work clamp condition, and machine settings. Verify the full system.

    Sources Checked

    • Provided Amazon product registry reference for ASIN B071SHY115
    • Allowed internal link: Weldmark 13N26 TIG Collet Body Review
    • Allowed internal link: TIG Torch Slipping Tungsten? Your Collet Body Is Worn (Here’s the Fix)

    For maintenance buyers, the main decision is simple: verify the torch family, inspect the full consumable stack, and replace the collet body only when the wear pattern supports it. That keeps the order accurate and reduces repeat failures in the field.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Western 603, 1/4″ NPT X 1 3/4″ Long Male Brass Regulator Nipple CGA 660: Product Breakdown

    Product not found.
    “>Western 603, 1/4" NPT X 1 3/4" Long Male Brass Regulator Nipple CGA 660

    The Western 603, 1/4" NPT x 1 3/4" long male brass regulator nipple CGA 660 is a gas apparatus support part used in compressed gas connections. For buyers and maintenance teams, the main job is not just to identify the fitting by name. The job is to verify thread form, connection standard, service conditions, and sealing method before installation. In compressed gas work, a part that looks close enough is not acceptable.

    This breakdown stays within the available product information. The source listing identifies the part as a Western brass regulator nipple with a 1/4" NPT connection, 1 3/4" length, and CGA 660 designation. Other technical details such as pressure rating, finish, exact end geometry, and approved gas service are Unknown (Verify).

    Key Takeaways

    • Verify the regulator side and cylinder side connection before ordering or installing.
    • 1/4" NPT indicates a threaded pipe connection, but the mating component still has to be confirmed on the actual assembly.
    • CGA 660 is a connection standard, not a substitute for visual inspection or system verification.
    • Brass is listed as the material. If your gas service has material restrictions, verify compatibility before use.
    • Unknown (Verify) details should be confirmed from the regulator documentation, gas supplier guidance, and site procedure.

    What This Part Is

    The Western 603 is a regulator nipple used as a connection component in gas apparatus. In practical terms, it is part of the interface between a regulator and the rest of the gas delivery system. The available listing identifies it as a male brass nipple with 1/4" NPT and CGA 660 designation. That is enough to start a purchasing review, but not enough to approve installation by itself.

    For maintenance buyers, this means the part should be treated as a configuration item. Match the connection standard, confirm the thread, and compare the installed component to the drawing, regulator data plate, or service record. Do not assume that every CGA-marked part is interchangeable.

    Inspection and Verification Before Use

    Use the following checks before releasing the part to service:

    • Check the thread designation: confirm the assembly requires 1/4" NPT. If the mating port is not NPT, stop and verify.
    • Inspect the body material: the listing indicates brass. Verify that brass is acceptable for the gas service and environmental conditions at your site.
    • Inspect the connection ends: look for nicks, deformation, burrs, or cross-threading damage.
    • Verify the CGA number: confirm the system specification calls for CGA 660. Do not rely on visual similarity alone.
    • Check for contamination: remove oil, debris, sealant residue, and shipping debris before installation if your procedure allows cleaning.

    If any item does not match the job requirement, set the part aside and verify against the gas equipment record or supplier documentation. Unknown (Verify) is the correct status until the system is confirmed.

    Troubleshooting and Support Checks

    If a new or replacement nipple does not fit correctly, work through the problem in a controlled way.

    • Check: Does the male end start cleanly by hand? If not, verify thread size and thread type before forcing the fit.
    • Inspect: Are the threads damaged, galled, or contaminated? A poor thread start usually means the part or the mating port needs repair or replacement.
    • Verify: Is the mating component actually CGA 660? Recheck the regulator, adapter, or cylinder connection callout.
    • Check: Is the installation procedure requiring a sealant, or does the system call for a dry thread approach? Follow the procedure for the specific gas system. Unknown (Verify) if not documented.
    • Inspect: After assembly, look for alignment issues or mechanical stress in the connected hardware.
    • Verify: Perform whatever leak test your site procedure requires before returning the system to service.

    If the connection repeatedly fails to assemble cleanly, stop and compare the installed part to the parts list. Do not correct thread mismatch by over-tightening or by mixing incompatible adapters.

    Purchasing and Parts Control Notes

    For buyers, the most useful purchasing control is document matching. Order the part only when the following are confirmed:

    • the required thread size is 1/4" NPT;
    • the required CGA designation is 660;
    • the expected body material is brass;
    • the application matches the regulator and gas service record.

    If any of those items are missing from the purchase request, return it for clarification. A regulator nipple is a small part, but it can stop an entire gas system when it is wrong.

    Product / Parts Notes

    The source product is the Western 603, 1/4" NPT x 1 3/4" long male brass regulator nipple CGA 660. The listing also states that Western offers complete lines of CGA connections, fittings, valves, manifold components, pigtails, and safety and convenience products in brass and stainless steel. That statement describes the brand range, not a guarantee that every related part is interchangeable with this nipple.

    Use the product page as the primary reference for identification only. Final acceptance should still depend on the specific regulator, cylinder connection, and site procedure. If a required specification is not present in the source information, mark it Unknown (Verify) and confirm it before use.

    Safety Notes

    • Compressed gas systems require strict handling. Follow all site and supplier safety rules.
    • Do not force threaded gas connections.
    • Do not mix fittings based on appearance only.
    • Keep oil, grease, and other contaminants away from gas connection surfaces unless your written procedure states otherwise.
    • If a leak, thread mismatch, or damaged connection is found, remove the part from service until verified.

    Western’s source note emphasizes that compressed gas users should adhere to all safety guidelines and practices. That warning should be treated as a baseline requirement, not a general reminder.

    FAQ

    Is the Western 603 ready for any CGA 660 system?
    No. The part is identified as CGA 660, but final suitability depends on the full gas assembly, thread match, and site procedure. Verify before use.

    Can I assume 1/4" NPT will fit any regulator port?
    No. NPT is specific, and the mating port must also be confirmed as 1/4" NPT. If the mating thread is unknown, inspect and verify.

    Is brass always acceptable for compressed gas service?
    No. The listing says brass, but gas compatibility requirements vary by service. Confirm against the gas specification and equipment manual. Unknown (Verify) if not documented.

    What should I do if the part threads in poorly?
    Stop installation, inspect both threads, and verify the part number and CGA designation. Do not force the connection or use it as a workaround.

    Sources Checked

    • ArcWeld product listing: Western 603, 1/4" NPT X 1 3/4" Long Male Brass Regulator Nipple CGA 660
    • Provided source idea and product short description

    Related Arc Weld Part

    Western 603, 1/4" NPT X 1 3/4" Long Male Brass Regulator Nipple CGA 660

    Western 603, 1/4" NPT X 1 3/4" Long Male Brass Regulator Nipple CGA 660

    WES603 Features: -Western has complete lines of CGA connections, fitting, valves, manifold components, pigtail, safety and convenience products. Brass and stainless steel.. -WESTERN. -Safety First Western strongly encourages users of compressed gases to adhere to all safety guidelines and practices. Only an absolute and constant respect for compressed gases is acceptable for safe operations. Refer to the Western s…

    View at Arc Weld Store
  • Nobody Starts With a Perfect Bead: What the First Weeks of Welding School Really Build

    The first practice plate has a way of telling the truth. The bead wanders. The starts are heavy. The stops leave craters. You lift the hood, look at the coupon, and wonder whether everyone else in the lab understands something you missed.

    They probably do not. They are learning, too.

    The opening weeks of welding school are not a highlight reel. They are an introduction to repetition, observation, safety, and the strange experience of training your hands to follow what your eyes are only beginning to see. Nobody walks into that booth with years of hood time already earned.

    The First Lesson Is Not About Looking Talented

    New welders often arrive carrying an invisible pressure to prove they belong. Maybe a parent welded. Maybe friends already work in the trades. Maybe this is a career change, and starting over feels heavier than expected.

    But the booth does not care about anybody’s backstory. It responds to preparation, position, consistency, and time. That can be humbling, but it is also fair. The work gives immediate feedback. A rough bead is not a verdict on your future; it is information about the next attempt.

    You Begin by Learning to See

    Before a student develops smooth travel, there is a more basic skill taking shape: noticing. You start seeing the difference between clean and contaminated material. You notice how body position changes control. You begin to recognize when the puddle is doing what you intended and when you are simply chasing it.

    This is why an instructor may spend more time asking what you see than telling you exactly what to do. Good feedback teaches a student to diagnose the work instead of waiting for somebody else to rescue every pass. The goal is not to memorize one magic motion. It is to build judgment that travels with you to the next joint, process, and job.

    Safety Becomes Part of the Craft

    Early training can make safety feel like a long list that stands between the student and the arc. Experienced welders understand it differently. PPE, ventilation, fire prevention, cylinder handling, housekeeping, and awareness of the people around the booth are part of doing the work correctly.

    The Occupational Safety and Health Administration’s welding overview organizes welding, cutting, and brazing requirements around recognized hazards and protective measures. A student does not need to memorize every standard in the first week, but the habits start immediately: protect your eyes and skin, understand the space, respect hot material, and ask when something is unclear.

    Feedback Is Where Confidence Actually Starts

    Real confidence is not announcing that you have it figured out. It is being willing to hear why a pass failed, make one deliberate change, and try again. That process can be frustrating because improvement rarely arrives in a straight line. One plate looks better. The next one falls apart. Then something clicks that you could not force the day before.

    The students who keep progressing are not always the loudest or fastest. They are often the ones who stay curious. They compare attempts. They keep notes. They watch a demonstration closely. They ask a specific question instead of hiding a mistake. Humility is not weakness in a welding lab; it is a practical tool.

    There Is More Than One Door Into the Trade

    Welding careers do not begin through one universal route. The U.S. Bureau of Labor Statistics describes a mix of technical education and on-the-job training, with opportunities through vocational programs, community colleges, private schools, military training, employers, and apprenticeships. The American Welding Society’s student resources also include education, certification information, and a school directory.

    That variety matters. A seventeen-year-old in a career center and a forty-year-old changing industries may stand at neighboring booths with different goals and the same assignment. Neither path makes the first plate easier. Both deserve room to learn.

    The Culture Is Being Built Around You

    The first weeks also reveal what kind of shop culture a class will create. Does somebody explain a setup without making the new person feel foolish? Do students clean the booth for whoever comes next? Does the class treat safety as shared responsibility? Can people laugh at a rough practice plate without laughing at the person who made it?

    Those small choices matter because welding is rarely a completely solitary trade. Even when one person holds the torch, the work depends on fitters, inspectors, operators, supervisors, helpers, instructors, and customers. Skill earns respect, but so does being the person others can trust around the work.

    Keep the First Plate

    If the program allows it, keep an early practice coupon. Months later, it becomes evidence—not of where you failed, but of how far repetition carried you. The wandering bead, the ugly restart, and the uneven rhythm are part of the record.

    That is the part of Arc Life worth remembering: pride in the trade does not begin when the work looks perfect. It begins when you decide the work is worth learning. Read more about the community behind Arc Life Co., built around people who keep showing up for the craft.

    Shop question: What did your first practice weld teach you that you still remember?

    Sources and further reading

  • What Arc Life Means: The Culture Welders Carry Beyond the Booth

    A clean bead is easy to admire. What most people never see is everything behind it: the early starts, the hood time, the rework, the burnt sleeves, and the quiet satisfaction of leaving a joint better than you found it.

    That is the heart of Arc Life. It is bigger than a welding process and more lasting than a good day in the booth. It is the culture welders carry with them—into the shop, onto the jobsite, and home at the end of a shift.

    The Work Has a Way of Shaping You

    Welding teaches patience in a hurry. You learn that rushing fit-up usually creates more work, that preparation matters, and that a small mistake can announce itself all the way down the joint. You also learn to keep going when the position is awkward, the weather is ugly, or the first attempt does not land the way you wanted.

    Those lessons do not stay under the hood. They show up in how welders solve problems, how they judge their own work, and how quickly they notice when something was built with care—or without it. Pride in the trade is not about pretending every weld is perfect. It is about caring enough to improve the next one.

    Every Process Has Its People

    Ask a group of welders about their favorite process and the conversation rarely stays technical for long. MIG has its production rhythm. TIG rewards control and focus. Stick carries a reputation for going where the work is rough and access is limited. Flux-cored welding has its own loyal crowd, too.

    The differences create plenty of shop talk, but the common ground matters more. Everyone remembers learning to read a puddle. Everyone has lifted a hood and known immediately that a pass was right—or that it was time to grind. Process pride can be fun without turning into a contest. The arc is the shared language.

    Shop Culture Is Built in the Small Moments

    The welding community is not held together by slogans. It is built through small acts: somebody lending a marker, explaining a machine setting without making a new welder feel small, calling out a hazard before it becomes an injury, or staying a few minutes to help finish a difficult fit-up.

    Good crews make room for high standards and good humor at the same time. They know when to give someone a hard time and when to step in. They respect the person doing the work, not just the job title on the badge. That sense of belonging is one reason welding becomes more than a paycheck for so many people.

    Arc Life is the pride of knowing what the work demands—and choosing to do it well anyway.

    Why Welders Wear the Trade

    A welding shirt, hat, sticker, or hoodie can look simple from the outside. To another welder, it can say a lot. It can recognize the process you prefer, the hours you have put in, or the kind of people you want to represent. It can start a conversation in a parking lot or earn a knowing nod across a counter.

    That is the idea behind Arc Life Co.: apparel and gear shaped by shop-floor experience and pride in the craft. The best welding culture does not need to shout. It simply feels familiar to the people who have lived it.

    Beyond the Booth

    When the helmet comes off, the identity does not disappear. Welders bring the trade into garages, side projects, family conversations, and the way they look at anything made from metal. They notice brackets, handrails, trailer repairs, and structural connections that everyone else walks past.

    Arc Life belongs in those off-the-clock moments, too. It is the story behind a toolbox sticker, the reason a process-specific shirt makes a good gift, and the shared pride that connects apprentices, instructors, fabricators, pipe welders, artists, repair technicians, and weekend builders.

    A Standard Worth Passing On

    Trade culture stays healthy when experience is passed forward. A veteran welder who explains the reason behind a habit gives a new hand more than a shortcut. An instructor who demands clean preparation teaches that quality begins before the arc starts. A coworker who treats safety as part of craftsmanship helps set the standard for the whole crew.

    That does not mean everyone has to work the same way or follow the same career path. Welding is broad enough for production, construction, repair, inspection, education, art, and entrepreneurship. The connection is a respect for the skill—and a willingness to leave the trade stronger for the people coming next.

    Keep the Arc Alive

    The strongest version of welding culture is welcoming, skilled, safety-minded, and proud without being closed off. It remembers where it came from while making room for the next person learning to strike an arc. It respects the old hands, encourages the new ones, and never forgets that every expert once had an unsteady first bead.

    If that sounds like your kind of community, explore the current Arc Life collection and find the piece that fits how you live the trade.

  • MIG Wire Feeds but No Arc? Check the Work Clamp and Return Path

    Your wire is feeding, the fan is running, and the gun trigger sounds normal—but the arc will not start, or it starts only after you drag the wire across the joint. Before replacing the gun, control board, or drive motor, inspect the welding current return path. A loose, dirty, undersized, or damaged work-clamp connection can interrupt the circuit even when the wire-feed system is working perfectly.

    This checklist focuses on the work clamp, cable, and connection points. It applies broadly to MIG and flux-cored machines, but the owner’s manual for your exact welder remains the final authority for cable size, polarity, connector type, and service procedures.

    Quick answer: what should you check first?

    1. Turn the welder off and disconnect input power before inspecting cables or hardware.
    2. Move the work clamp onto clean, bare steel close to the weld.
    3. Remove paint, rust, mill scale, oil, and weld spatter from the contact area.
    4. Inspect both clamp jaws and the cable-to-clamp connection for looseness, heat damage, oxidation, or broken strands.
    5. Confirm the work cable and gun polarity match the wire and shielding setup in the machine manual.
    6. Reconnect power and test on clean scrap steel using the manufacturer’s recommended settings.
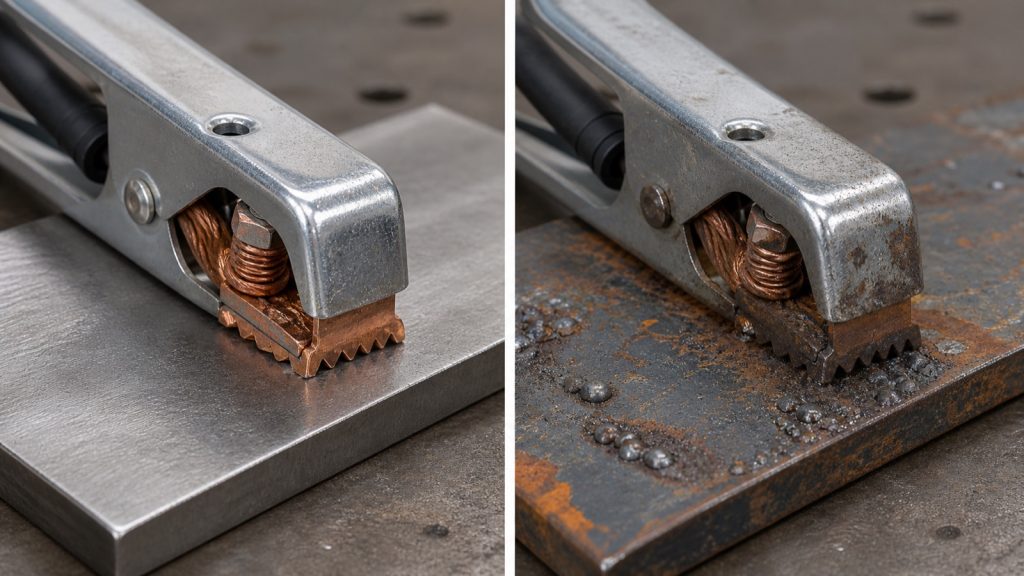
    Comparison of a MIG work clamp on clean bare steel and on a rusty spattered surface
    Broad contact on clean bare steel gives welding current a lower-resistance return path than a clamp placed over rust, coating, scale, or spatter.

    Why the clamp matters when the wire still feeds

    The wire-feed motor and the welding output circuit are related, but they are not the same path. The trigger can energize the feeder while a bad work connection prevents useful welding current from returning to the power source. That is why “wire feeds but no arc” can point to the clamp even though the machine appears alive.

    OSHA requires work leads to be firmly attached and says welding connections should be mechanically strong and electrically adequate. It also specifically calls for removing adhering metal particles from magnetic clamp contact surfaces. Miller’s Millermatic 142 manual warns that loose work-clamp hardware can cause poor weld performance and excessive heating.

    A five-minute work-clamp inspection

    1. Make the inspection safe

    Switch the welder off and disconnect its input power before opening a case, tightening internal terminals, or handling damaged insulation. Let recently used cables and connectors cool. Stop using the machine if insulation is cut through, copper is exposed, a connector is badly burned, or the clamp becomes hot enough to discolor or soften nearby insulation.

    2. Improve the contact point

    Attach the clamp directly to the workpiece or to a properly bonded fixture. Choose a flat area of clean bare metal, as close to the weld as practical. Paint, powder coat, rust, heavy mill scale, adhesive, oil, and spatter can reduce the area that actually carries current. A clamp hanging on an edge by one tooth may feel secure while making poor electrical contact.

    3. Inspect the jaws and spring pressure

    Open the clamp and inspect both contact faces. Clean away spatter and oxidation with an appropriate hand tool while the machine is de-energized. Look for pitted copper contacts, twisted jaws, a weak or broken spring, and a hinge that prevents the jaws from closing squarely. Replace the clamp if it cannot maintain firm, broad contact.

    4. Check the cable-to-clamp hardware

    Follow the work cable into the clamp handle. The lug, braid, fastener, washers, and nut should be intact and tight according to the manufacturer’s design. Darkened copper, melted insulation, green corrosion, loosened hardware, or broken cable strands indicate resistance and heat. Do not improvise undersized fasteners or bypass strain relief.

    5. Inspect the rest of the return path

    Run your hand along the disconnected cable and look for hard spots, crushed sections, cuts, repaired areas, or a loose machine connector. Confirm plug-style connectors are fully seated and locked. If you are using a table or fixture as part of the return path, verify that joints between the clamp and workpiece are electrically bonded; paint and loosely bolted sections can break the path.

    Symptoms and likely clamp-side checks

    SymptomLikely return-path issueFirst check
    Wire feeds but no arcOpen or very poor work connectionMove the clamp to clean bare steel and reseat the machine connector
    Arc starts only when wire scratches the workMarginal contact or contaminated surfaceClean the contact area and inspect jaw pressure
    Arc is erratic or sounds harshLoose connection, damaged cable, or wrong polarityTighten approved connections and verify polarity in the manual
    Clamp or cable lug gets hotHigh resistance at the jaw, lug, or broken strandsStop, cool, inspect, and replace damaged parts

    Work clamp versus equipment ground

    Welders often say “ground clamp,” but the clamp on the welding lead is normally the work clamp: it completes the welding current circuit back to the power source. The safety grounding conductor for the machine frame serves a different protective purpose. Do not treat building conduit, chains, wire rope, hoists, or random grounded structures as substitutes for the correct work lead. OSHA prohibits several of those paths from carrying welding current.

    When cleaning is not enough

    Replace or have qualified personnel repair the work lead assembly when the clamp cannot hold firmly, contact faces are badly eroded, the cable is undersized for the machine, strands are broken, insulation is damaged, or connectors show repeated overheating. Match the replacement cable, clamp, lug, and connector to the welder’s rated output and duty cycle. If a clean, tight return path does not restore the arc, continue with the gun connection, contact tip, polarity block, output terminals, and machine-specific diagnostics.

    For related checks, see our guides to poor MIG arc stability and MIG contact-tip overheating.

    Frequently asked questions

    Can a bad work clamp let the wire feed normally?

    Yes. The feeder can operate even when the welding-current return path is open or highly resistive. That makes the clamp and work cable an early check for a machine that feeds wire but will not establish an arc.

    Should the clamp be close to the weld?

    Usually, yes. Place it on clean metal as close to the weld as practical while following the equipment manual and job-specific requirements. This reduces unnecessary current paths through hinges, bearings, electronics, or poorly bonded joints.

    Is a hot work clamp normal?

    Noticeable heating can indicate excessive resistance, loose hardware, inadequate contact area, damaged conductors, an undersized assembly, or use beyond the component’s rating. Stop and correct the cause rather than continuing until the clamp or insulation fails.

    Primary references

  • What Welders Should Wear in Hot Weather: Cotton, FR Gear, and the T-Shirt Problem

    Balancing Heat Stress and Arc Protection

    Summer heat introduces a dangerous balancing act for welders, fabricators, and shop personnel. As temperatures inside the shop climb, the temptation to strip off heavy protective gear becomes overwhelming. However, sacrificing personal protective equipment (PPE) to stay cool directly exposes you to ultraviolet (UV) radiation, severe burns, and spatter injuries.

    Understanding what welders should wear in hot weather requires knowing the critical difference between ordinary cotton, flame-resistant (FR) gear, and synthetics. A lifestyle T-shirt is not a protective garment. True welding safety in high temperatures relies on strategic layering, breathable FR fabrics, and rigorous heat-stress management.

    The T-Shirt Problem: Why Ordinary Cotton is Not PPE

    Walk into many fabrication shops in July, and you may see someone welding in a standard graphic T-shirt. That garment should not be treated as protective welding apparel. Everyday lifestyle T-shirts are generally not designed, tested, or labeled for the hazards created by an active arc.

    Safety note: Welding arcs produce intense ultraviolet and infrared radiation. Any exposed skin can burn, so the garment system should provide complete coverage appropriate to the process and position.

    Untreated cotton is generally preferable to common meltable synthetic blends when selecting an underlayer, but an ordinary cotton T-shirt is not automatically welding PPE. Fabric weight, condition, coverage, garment construction, and the amount of sparks or spatter all matter. Polyester, nylon, spandex, and similar fibers can soften or melt when exposed to heat and spatter, increasing the severity of a burn. Follow the employer’s hazard assessment and the garment manufacturer’s instructions.

    What Welders Should Wear in Hot Weather: Cotton, FR Gear, and the T-Shirt ProblemChoosing the right FR gear ensures you are protected from sparks and UV rays without adding unnecessary bulk.

    Understanding Your Fabric Options

    When selecting hot-weather gear, welders must choose materials that naturally resist ignition or are chemically treated to self-extinguish.

    Flame-Resistant Workwear

    FR garments are designed to resist ignition or limit continued burning when used and maintained as directed. Lightweight FR shirts and jackets may reduce bulk in summer, but suitability depends on the welding process, position, spatter level, and the garment’s verified rating and instructions.

    Leather Protection

    Leather provides durable protection where heavy sparks and spatter are expected, including many stick-welding and overhead applications. It also adds weight and reduces heat loss, so the coverage should be matched to the hazard rather than treated as a one-size-fits-all solution.

    Common Synthetic Blends

    Many polyester, nylon, and stretch fabrics can melt or shrink when exposed to heat. Do not assume moisture-wicking or athletic clothing is suitable for welding; use garments selected through the workplace hazard assessment and verified for the intended exposure.

    Strategies for Managing Heat Stress

    Instead of stripping down to unsafe clothing, welders should adapt their PPE strategy to the climate. Heat stress can lead to heat cramps, heat exhaustion, and potentially fatal heat stroke. Managing your core temperature involves smart layering and strategic coverage.

    Do not solve heat stress by removing required protection. Instead, use the lightest protective system that still matches the hazard assessment—for example, verified FR workwear with localized leather coverage where heavy spatter is expected. Employers should also use ventilation, work/rest cycles, hydration, acclimatization, and cool recovery areas. Any head covering worn under a helmet must fit without interfering with the helmet, headgear, or protective seal.

    Summer Welding Clothing Checklist

    Before stepping into the shop during a heatwave, ensure your gear meets fundamental safety requirements. True protective workwear minimizes catching points and covers all exposed skin.

    • Full Sleeve Coverage: Sleeves must extend to the welding glove cuff. Exposed wrists will suffer severe UV arc burns.
    • High Collars: Keep collars buttoned up to protect the neck from stray spatter and intense light bouncing off the table.
    • No Cuffs or Open Pockets: Pants should fall smoothly over the top of leather work boots without cuffs. Shirts should lack open chest pockets, which act as catch-basins for hot slag.
    • Approved Undergarments: Ensure whatever touches your skin directly is 100% natural fiber, like standard heavy cotton, even if covered by an FR jacket.
    What Welders Should Wear in Hot Weather: Cotton, FR Gear, and the T-Shirt ProblemBreathable, flame-resistant workwear is essential for maintaining safety and preventing heat stress during summer shifts.

    Changing and Caring for Work Clothes

    Hot-weather gear becomes wet, dirty, and easier to damage. Inspect garments for holes, thin spots, open seams, oil, grease, and other contamination that could reduce protection. Follow the garment manufacturer’s laundering and retirement instructions, especially for treated FR clothing.

    A clean change of clothes can also help keep shop dust and residue out of personal vehicles and living areas. Where the work involves metals or coatings that create hazardous contamination, follow the employer’s hygiene and decontamination program rather than relying on a general home-laundry routine.

    Sources and Safety Guidance

    Protective clothing should be selected through a workplace hazard assessment and matched to the size, nature, and location of the welding work.

    The Practical Rule

    Do not trade away required protection to get cooler. Match the clothing system to the actual welding hazard, then control heat with ventilation, hydration, acclimatization, appropriate rest breaks, and cool recovery areas.

    Arc Life Media Note: A welder’s lifestyle clothing belongs off the arc. Never wear athletic wear, synthetic blends, or untreated thin cotton while welding, cutting, or grinding unless the garment is specifically labeled and verified as protective workwear.

  • ER5556 MIG / GMAW Filler Metal: Filler Metal Finder Notes

    ER5556 MIG / GMAW Filler Metal

    ER5556 MIG / GMAW filler metal is a high-magnesium aluminum wire used where a stronger deposit is needed on compatible 5xxx aluminum joints. Treat the selection page as a starting point only. Before ordering wire or welding parts, verify the WPS, code requirements, base metal grade, service conditions, and the manufacturer data sheet. If those items do not line up, do not assume ER5556 is acceptable.

    Key Takeaways

    • ER5556 is a filler metal selection point for MIG / GMAW work on 5xxx aluminum applications that need higher deposit strength.
    • Do not use a product page as procedure approval. Verify against the WPS and applicable code or customer specification.
    • Confirm the base alloy, joint design, required mechanical properties, and service environment before choosing wire.
    • Check wire diameter, feeding setup, and storage conditions before production use.

    What ER5556 is used for

    ER5556 is commonly considered when the weld deposit must support stronger 5xxx aluminum joints than a lower-strength general-purpose wire might provide. That does not mean it is the correct choice for every aluminum job. Base metal chemistry, post-weld service, corrosion exposure, and cracking sensitivity all matter. For marine service, pressure-retaining work, or regulated fabrication, verify the filler metal against the governing document before use.

    Common support questions arise when a shop is comparing ER5556 to other aluminum filler metals such as ER5183 or ER5356. Do not substitute based on memory alone. Compare the WPS, the actual alloy designation on the base material, and the required mechanical or corrosion performance. If any of that is unclear, stop and verify.

    Filler metal finder section

    Use the filler metal page as a selection starting point, not as a guaranteed procedure approval. Review the product page here: ER5556 MIG / GMAW Filler Metal. If you are not sure whether ER5556 fits the job, cross-check it with the Filler Metal Finder and then confirm the final choice against the WPS and the manufacturer data sheet.

    Check / inspect / verify

    • Check the base metal alloy designation from drawings, mill certs, or part markings.
    • Inspect the WPS for filler classification, wire diameter, shielding gas, polarity, and transfer mode requirements.
    • Verify whether the service conditions introduce corrosion or cracking concerns that affect filler selection.
    • Check spool condition, packaging integrity, and storage history before opening wire.
    • Inspect the feeder setup, drive rolls, liner, and contact tip size for aluminum wire handling.
    • Verify the final purchase against the manufacturer data sheet before the wire is issued to production.

    Troubleshooting and support notes

    If the wire feeds poorly, do not assume the filler metal is defective. Aluminum MIG issues often start with setup. Check the liner, drive roll tension, gun length, contact tip fit, and spool handling. Inspect for contamination or damage to the wire surface. Verify that the feeder is set up for soft aluminum wire and that the contact tip size is appropriate for the selected diameter.

    If the weld deposit is not meeting expected performance, review the full welding system and the job requirements. Check the WPS first. Inspect whether the correct base metal was identified. Verify that the shielding gas, technique, and heat input match the procedure. If the job involves code work, testing, or customer qualification, do not continue on the assumption that ER5556 will satisfy the requirement without documentation.

    Common support checks

    • Check if the aluminum alloy being welded is truly a 5xxx grade.
    • Inspect for contamination from oil, oxide, or moisture.
    • Verify spool diameter and wire size against feeder capability.
    • Check if the selected filler metal is listed on the WPS.
    • Inspect the work order for any corrosion, fatigue, or seawater exposure notes.

    How to use the product page correctly

    The ER5556 page should be treated as a starting point for selection, not as a final approval document. That means the buyer, welder, or supervisor still needs to verify the governing standard, the base alloy, and the service condition before release. If the procedure package is missing, Unknown (Verify) is the correct answer until the paperwork is found.

    For maintenance buyers, the most useful question is not only “Is this ER5556?” but also “Does the current job package require ER5556, or another aluminum filler?” If the answer is not documented, route it back for verification.

    Safety notes

    • Use local exhaust and the required PPE for aluminum GMAW work.
    • Do not weld on unknown alloys without confirming the base metal and procedure.
    • Handle wire and spools with clean gloves to reduce contamination.
    • Keep aluminum filler metal dry, clean, and protected from shop debris.
    • Follow the site welding procedure and hot-work controls before starting.

    FAQ

    Is ER5556 always the right choice for 5xxx aluminum?

    No. It is a possible selection for some higher-strength 5xxx aluminum applications, but you still need to verify the WPS, base metal grade, and service conditions. If those are not confirmed, Unknown (Verify).

    Can I substitute ER5556 for ER5356?

    Do not substitute without procedure approval. Compare the WPS and the job requirements first. A filler metal page is not a substitute for code or engineering review.

    What should I check before ordering ER5556 wire?

    Check the base alloy, the required wire diameter, the WPS, and the manufacturer data sheet. Inspect whether the feeder and gun setup are suitable for aluminum wire. Verify all of it before issuing the order.

    What if the job documentation is missing?

    Stop and verify. Do not guess at filler metal selection for regulated or critical work. Unknown (Verify) is the correct status until the documentation is found.

    Sources Checked

    Reviewed page details were limited to the provided Weld Support Parts filler metal information. Final filler selection still requires verification against the WPS, code requirements, base metal grade, service conditions, and manufacturer data sheet.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
  • KOHLER 47 883 03-S1 Engine Air Filter With Pre-Cleaner Kit: Replacement Part Breakdown

    The KOHLER 47 883 03-S1 Engine Air Filter With Pre-Cleaner Kit is a replacement air intake service item, not a repair for deeper engine problems. For maintenance buyers and shop support teams, the main job is simple: keep dirt out of the engine, match the correct service part, and verify the filter is installed in a way that does not bypass sealing surfaces.

    This guide breaks down the part at a practical level. It is written for inspection, replacement planning, and troubleshooting. It does not assume compatibility beyond the product listing itself. If fitment is uncertain, verify against the engine model, current parts manual, and the equipment serial number before ordering or installing.

    Key Takeaways

    • This is an air filter plus pre-cleaner kit. It is meant for routine intake service.
    • Do not assume universal fit. Verify the engine model and OEM parts listing first.
    • Inspect the air box, sealing surfaces, and intake tract when changing the filter.
    • A dirty pre-cleaner can shorten service intervals, even if the main filter still looks usable.
    • If dirt ingestion is suspected, replace the filter and inspect downstream components before returning the engine to service.

    What This Part Does

    An engine air filter removes airborne dust and debris before it reaches the intake system. The pre-cleaner is a first-stage element that can help trap larger debris before it reaches the main filter. In dusty maintenance environments, both parts matter. A damaged seal, loose housing, or incorrect installation can allow unfiltered air into the engine even if the filter media itself looks acceptable.

    Buyer and Support Checkpoints

    Before ordering or installing the KOHLER 47 883 03-S1 kit, use this check list:

    • Check the engine model number. Do not rely on visual similarity alone.
    • Inspect the current filter dimensions and housing shape. Match against the parts listing and manual.
    • Verify the sealing edge. A distorted seal can be more harmful than a dirty element.
    • Confirm whether the pre-cleaner is included in the service kit. This listing is a kit, but always verify the exact contents at purchase.
    • Check for dust tracking. Powdery dirt downstream of the filter points to bypass or a poor seal.

    Troubleshooting: When to Replace or Inspect Further

    If an engine starts to lose power, runs rich, or shows unusual dust buildup in the intake path, the air filter is one of the first items to inspect. Use the following sequence:

    Check

    • Check the filter media for heavy dust loading, tears, or collapse.
    • Check the pre-cleaner for excessive dirt, oil saturation, or damage.
    • Check the housing for cracks, missing clips, warped covers, or loose fasteners.

    Inspect

    • Inspect the sealing rim and mating surface for sand, debris, or compression set.
    • Inspect the intake tube and clamps for leaks or loose fit.
    • Inspect the old filter for evidence of dirt passing around the element rather than through it.

    Verify

    • Verify the replacement part number against the engine’s official parts record.
    • Verify the filter seats fully and the housing closes without forcing.
    • Verify engine response after service. If performance problems remain, the issue may be fuel, ignition, governor, or mechanical, not the air filter.

    Replacement Part Breakdown

    For maintenance planning, think of this item as three service functions in one package:

    • Main air filter element: Primary barrier for fine particulate.
    • Pre-cleaner: Secondary stage for larger dust and debris.
    • Service fitment: The physical shape and seal interface that must match the engine air box.

    Unknown (Verify): exact media type, dimensions, and engine compatibility. Do not fill those gaps from guesswork. Confirm from the OEM listing or the equipment manual.

    Install and Service Notes

    Use clean hands and a clean work area. Do not tap a damaged filter back into service if the media is torn or the frame is distorted. If the pre-cleaner is reusable on the specific engine setup, inspect it first and follow the OEM service instructions. If service instructions are not available, treat the pre-cleaner as Unknown (Verify) and confirm with the manual.

    Practical install steps:

    1. Shut the engine down and let it cool.
    2. Open the air cleaner housing carefully so debris does not fall into the intake.
    3. Remove the old filter and pre-cleaner.
    4. Clean the housing and sealing surfaces with a dry, lint-free method.
    5. Install the new filter so it seats evenly.
    6. Install the pre-cleaner as specified by the equipment manual, if applicable.
    7. Close the cover and confirm all retainers are secure.
    8. Start the engine and check for abnormal intake noise or leaks.

    Product and Parts Section

    The verified Amazon product associated with this draft is the KOHLER 47 883 03-S1 Engine Air Filter With Pre-Cleaner Kit, ASIN B000H5ZWEC. Use the provided product box for the current listing:

    No products found.

    Do not assume this kit fits every KOHLER-powered machine. Buyer teams should confirm the engine model, serial range, and parts manual before purchase.

    Safety Notes

    • Stop the engine before servicing the air filter.
    • Keep loose dirt out of the intake opening during removal.
    • Do not use compressed air on a filter unless the OEM procedure explicitly allows it.
    • Do not run an engine with a missing filter or open air box.
    • If dust ingestion is suspected, inspect the engine for follow-on wear before placing it back in service.

    FAQ

    How do I know if this is the correct replacement?

    Verify the engine model, the parts manual, and the OEM part number. Do not rely on appearance alone. If any detail does not match, treat fitment as Unknown (Verify).

    Should I replace the pre-cleaner at the same time as the filter?

    For maintenance planning, yes, inspect both together. Replace whichever component is dirty, damaged, or no longer sealing correctly. If the OEM service method is unclear, verify the replacement interval in the manual.

    What if the engine still runs poorly after filter replacement?

    Then the air filter is probably not the only issue. Check fuel delivery, ignition, governor response, intake leaks, and engine condition. Do not keep replacing filters as a substitute for diagnosis.

    Can I use this kit on a different KOHLER engine?

    Unknown (Verify). Use only documented fitment from the OEM parts listing or manual. Similar housings can have different seals and dimensions.

    Sources Checked

    • Provided Amazon product reference: B000H5ZWEC
    • Provided product name: KOHLER 47 883 03-S1 Engine Air Filter With Pre-Cleaner Kit
    • Task instructions and allowed product data only

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
  • Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1): Product Breakdown

    Product not found.
    “>Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1)

    The Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1) is a plasma cutting consumable intended for use in supported torch systems. For buyers and maintenance teams, the main question is not just whether the part is available, but whether it matches the torch, current range, and operating system already in service. This breakdown focuses on practical verification steps so you can avoid fit-up issues and premature consumable wear.

    Per the provided product information, this 80-amp tip is best used on SL60 and SL100 torches. It is also described as usable on a plasma cutting torch that performs with virtually all plasma cutting power supplies. The 1Torch is listed as working with high frequency start systems, CD start systems, touch start systems, and moving parts (blow back) start systems. Verify your exact torch model and power source before ordering or installing.

    Key Takeaways

    • Product: Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1).
    • Reported fit/use: SL60 and SL100 torches.
    • Listed system compatibility for the 1Torch: high frequency start, CD start, touch start, and blow back start systems.
    • Consumable fit and life depend on torch body condition, electrode condition, air quality, and operating technique.
    • Unknown (Verify): exact material composition, dimensional tolerances, and any extended compatibility claims beyond the provided product description.

    Product and Parts Review

    This part is a plasma tip, so it should be treated as a wear item rather than a permanent component. In maintenance planning, tips are normally purchased with other consumables such as electrodes, shields, and retaining parts when applicable. The supplied product description does not list those companion parts, so do not assume a kit configuration. Confirm what your torch head actually uses.

    Before installation, inspect the new tip for obvious defects. Look for damaged threads, distortion, nicks, oval openings, or contamination from storage. If the tip appears damaged, do not install it. Keep consumables clean and dry, and store them in original packaging until needed.

    Check

    • Check the torch model against the tip’s stated fit: SL60 or SL100.
    • Check that the amperage setting aligns with the 80-amp designation.
    • Check the torch head, electrode, and shield components for wear or heat damage.
    • Check air supply quality. Moisture, oil, and dirt can shorten consumable life.

    Inspect

    • Inspect the seating surfaces inside the torch for carbon buildup or arc damage.
    • Inspect the old tip for erosion patterns that may indicate standoff issues, misalignment, or poor air quality.
    • Inspect cable and torch lead condition for cuts, crushed sections, or loose connections.

    Verify

    • Verify polarity and machine setup according to the torch and power source manual.
    • Verify that the start system on the machine matches the torch system type in use.
    • Verify the cut quality after installation using a short test cut before returning the machine to production.

    Troubleshooting and Support Notes

    If the tip installs but the cut is unstable, start with the basics. Consumable issues are often caused by setup, not the part alone. Use the following checks in sequence.

    Arc starts but cut quality is poor

    • Check whether the tip is the correct size and type for the torch.
    • Inspect the electrode. A worn electrode can mimic a bad tip.
    • Verify air pressure and dryness. Unknown (Verify): the exact pressure range for your system.
    • Confirm the work clamp connection and workpiece contact area.

    Tip wear is faster than expected

    • Check for excessive amperage or prolonged pierce time.
    • Inspect technique. Excessive standoff or dragging the tip can shorten life.
    • Verify that the torch is not being operated outside the machine’s rated procedure.
    • Inspect for unfiltered moisture or oil in the air line.

    Tip will not seat correctly

    • Inspect the threads and retaining surfaces for damage.
    • Verify that the torch model is actually SL60 or SL100, not a similar-looking variant.
    • Remove debris from the torch head and recheck fit by hand. Do not force installation.

    WSP Lookup Section

    No WSP lookup page was provided for this draft, so no source-based lookup link is included here. If you need a cross-reference check, use the approved WSP lookup tool available in your internal workflow before procurement.

    Buyer and Maintenance Guidance

    For buyers, the main control point is fit confirmation. An 80-amp plasma tip is only useful if it matches the torch body, consumable stack, and current setting. For maintenance teams, the better approach is to standardize by machine family and keep a small approved consumable list by torch type. That reduces installation errors and keeps replacements predictable.

    When ordering this part, confirm the exact torch model from the machine label, torch tag, or service record. Do not rely on appearance alone. Similar torches can use different consumable designs. If documentation is missing, compare the removed tip with the replacement and verify against the torch manual before use.

    Safety Notes

    • Disable power before servicing the torch or replacing consumables.
    • Allow hot parts to cool before handling.
    • Use eye protection and gloves when inspecting used consumables.
    • Never force a part into the torch head.
    • Follow the machine and torch manufacturer procedures for startup, piercing, and cut distance.
    • Unknown (Verify): any torch-specific insulation or handling precautions not stated in the provided product information.

    FAQ

    Is the Victor Thermal Dynamics 9-8211 Tip 80-Amp compatible with SL60 and SL100 torches?

    Based on the provided product description, yes. It is listed as best used on SL60 and SL100 torches. Verify against your exact torch revision before installation.

    Can this tip be used on all plasma cutting power supplies?

    The provided description says it can be used on a plasma cutting torch that performs with virtually all plasma cutting power supplies. Do not treat that as a blanket approval. Verify your machine, torch, and start system before use.

    Does the 1Torch work with different start systems?

    The supplied information states that the 1Torch works with high frequency start systems, CD start systems, touch start systems, and moving parts (blow back) start systems. Confirm this against the exact torch model in your shop.

    What should I inspect first if cut quality drops after replacing the tip?

    Inspect the electrode, air quality, torch seating surfaces, and amperage setting first. A new tip will not correct a worn electrode, bad air, or an incorrect machine setup.

    Sources Checked

    • Provided ArcWeld product source: Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1)
    • Provided product description text in the task payload

    Final note: treat this tip as a consumable matched to a specific torch family. Verify the torch model, start system, and operating setup before ordering or installing.

    Related Arc Weld Part

    Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1)

    Victor Thermal Dynamics 9-8211 Tip 80-Amp, Pack of (1)

    Victor Thermal Dynamics 9-8211 Tip 80 Amp best to be used on SL60 and SL100 torches. This tip can be used on the plasma cutting torch that performs with virtually all plasma cutting power supplies. The 1Torch works with high frequency start systems, CD start systems, touch start systems and moving parts (blow back) start systems. Pack of 1 each

    View at Arc Weld Store
  • ER5554 MIG / GMAW Filler Metal: Filler Metal Finder Notes

    ER5554 MIG / GMAW Filler Metal

    ER5554 MIG / GMAW filler metal is an aluminum wire used when the job calls for matching 5454-type aluminum service requirements. Treat it as a starting point for filler selection, not as a final approval to weld. Before ordering wire or writing it into production, confirm the WPS, code requirements, base metal grade, service conditions, and the manufacturer data sheet.

    Key Takeaways

    • ER5554 is listed here as a filler metal support option for MIG / GMAW aluminum work.
    • Use it as a selection starting point only.
    • Verify the base metal is actually 5454 aluminum or otherwise approved by the WPS.
    • Confirm the service environment before use, especially if the part sees elevated temperature, cyclic loading, or corrosion exposure.
    • Do not assume a filler metal page equals procedure approval.

    What ER5554 is used for

    The source material identifies ER5554 as aluminum MIG wire used when matching 5454-type aluminum service requirements. That is the correct level of detail for a support page: it helps narrow the search, but it does not replace the welding procedure specification. In practice, the welding team still needs to confirm base metal chemistry, thickness, joint design, cleanliness requirements, and any postweld service conditions before wire is released to the floor.

    Check before you select wire

    Check the job documents first. Look for the WPS, drawing notes, customer spec, and any code references. If the paperwork calls out a different filler classification, stop and verify before substituting. If the paperwork is missing, unknown, or contradictory, treat the filler choice as Unknown (Verify).

    Inspect the base metal identification. Confirm the alloy grade and temper from material traceability, stamps, mill certs, or approved test reports. Do not rely on visual appearance. 5454 aluminum can be confused with other aluminum alloys in mixed inventory or rework areas.

    Verify the service condition. Some aluminum weldments live in corrosion service, some carry load, and some are exposed to heat or vibration. Filler selection may change depending on the application. If the service condition is not clearly documented, record it as Unknown (Verify) and route it to welding engineering or the responsible supervisor.

    Filler metal finder notes

    The ER5554 MIG / GMAW filler metal page should be used as a selection starting point only. The page helps the buyer or welder narrow the candidate list, but it does not guarantee WPS acceptance, code compliance, or compatibility with a specific base alloy and service condition.

    For selection work, use the filler metal finder as a support tool and then confirm the following:

    • Base metal grade: 5454 aluminum or Unknown (Verify)
    • Process: MIG / GMAW
    • Classification: ER5554
    • AWS specification: AWS A5.10
    • Wire diameter: Unknown (Verify)
    • Manufacturer: Unknown (Verify)

    The source keywords also mention ER5356 and multiple manufacturers such as Lincoln Electric, Hobart, Washington Alloy, Victory Alloy, Harris, Weldcote, and ESAB. That indicates the search space, not a confirmed interchange list. Do not assume one brand or one alloy replaces another without a WPS review and manufacturer data sheet review.

    Troubleshooting support: when the weld does not match expectations

    If the weld shows cracking, poor fusion, excess cleaning issues, or appearance that does not meet the job standard, do not jump directly to a filler swap. Work through the problem systematically.

    Check whether the wire matches the approved procedure. If the procedure is unclear, stop and verify it with welding engineering or QA.

    Inspect the joint preparation and cleaning. Aluminum contamination from oxide, oil, marker ink, moisture, or storage handling can drive defects that look like filler metal trouble.

    Verify that shielding gas, polarity, wire feed stability, and torch setup are correct for the process being used. If any of these details are missing from the work package, mark them Unknown (Verify) and review before continuing.

    Check the wire condition. If the spool has been exposed to damage, contamination, or poor storage, replace it. Aluminum wire can be sensitive to feed issues and handling damage.

    Inspect the joint after test welds. Compare bead profile, tie-in, and surface condition against the acceptance criteria in the WPS or inspection plan.

    How maintenance buyers should handle this item

    For purchasing, the main control point is not the product name alone. It is the combination of classification, process, base metal requirement, and the approved procedure. If the requisition only says “aluminum wire” or “ER5554,” send it back for clarification. Request the WPS reference, the base metal grade, diameter, and any packaging or storage requirements from the responsible team. If any field is missing, record it as Unknown (Verify).

    Safety notes

    • Follow the site hot work procedure.
    • Use proper PPE for aluminum GMAW work, including eye protection and hand protection suitable for welding operations.
    • Control fumes, smoke, and arc exposure with ventilation and local exhaust as required by the job.
    • Handle wire and spools carefully to avoid contamination and feed issues.
    • Do not weld from assumptions. Verify the procedure first.

    FAQ

    Is ER5554 automatically approved for 5454 aluminum?
    No. The page identifies ER5554 as a starting point for 5454-type service requirements, but the final decision depends on the WPS, code requirements, and service conditions.

    Can I substitute ER5554 for another aluminum filler without review?
    No. Substitution requires procedure approval. If the document trail is missing or unclear, treat the compatibility as Unknown (Verify).

    Does the filler metal finder page guarantee the right wire?
    No. It is a support tool for selection. It does not replace the WPS, manufacturer data sheet, or engineering review.

    What if the base alloy is not clearly identified?
    Stop and verify the material. Do not release filler metal based on appearance alone.

    Sources Checked

    This page is a support note for selection and verification. Use it with the WPS, the actual material identification, and the manufacturer data sheet before any weld is made.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
  • Try Amazon Prime Free