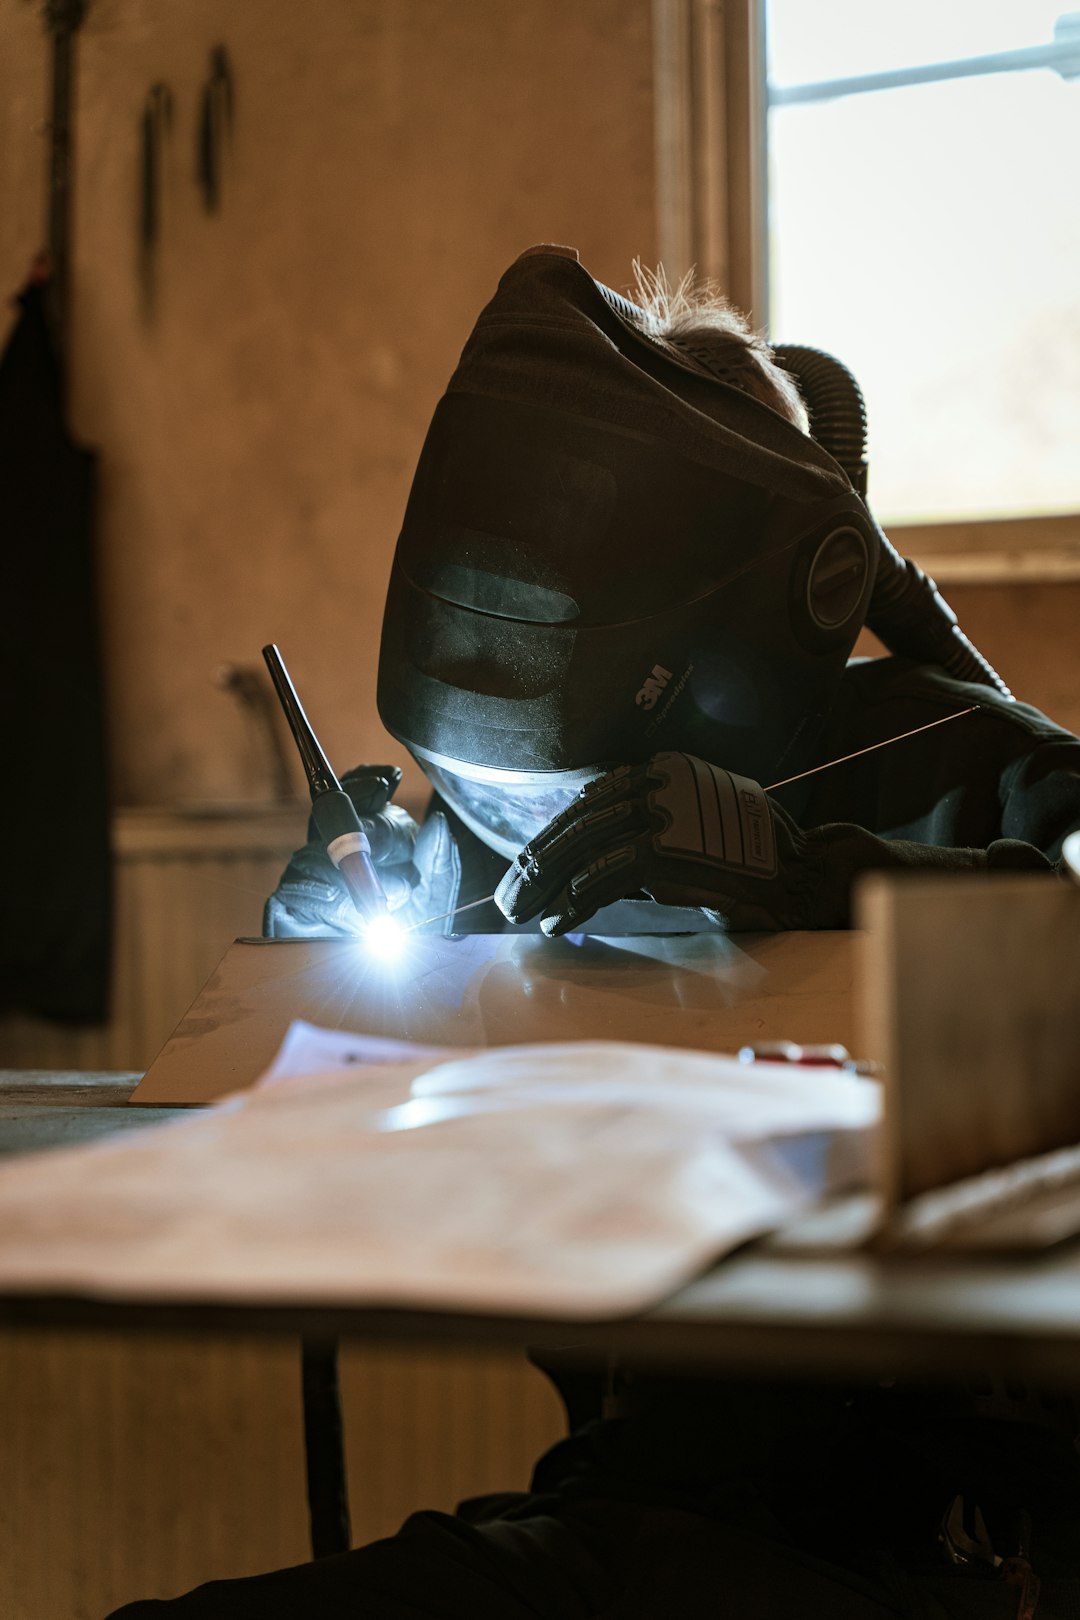
ER310 and ER309L are both stainless TIG filler classifications under AWS A5.9, but they solve different selection problems. ER310 is a high-chromium/high-nickel starting point for 310-family heat-resistant stainless. ER309L is commonly used for 24Cr-13Ni stainless and for selected dissimilar joints or buffer layers. Choosing between them by the word “stainless” alone misses the reason the classifications exist.
Start with the application, not the alloy number
| Question | ER310 starting point | ER309L starting point |
|---|---|---|
| Typical family | 310/310S and 25Cr-20Ni heat-resistant stainless | 309-family stainless, buffer layers and selected stainless-to-carbon-steel joints |
| Manufacturer example | ESAB OK Tigrod 310 | ESAB OK Tigrod 309L |
| AWS classification | ER310 | ER309L |
| Key decision | Heat-resistant alloy match and service conditions | Dissimilar-joint or transition-filler requirements |
| What it does not prove | That ER310 fits every high-temperature joint | That ER309L is approved for every stainless-to-mild-steel weld |
What ESAB says about ER310
ESAB classifies OK Tigrod 310 to SFA/AWS A5.9 ER310 and describes it as a bare corrosion-resistant chromium-nickel rod for heat-resistant austenitic steels of the 25Cr-20Ni type. ESAB specifically points to industrial furnaces, boiler parts and heat exchangers as common applications, and identifies the alloy as fully austenitic. Those are product-family clues, not permission to use ER310 outside the governing WPS or material specification.
What ESAB says about ER309L
ESAB classifies OK Tigrod 309L to SFA/AWS A5.9 ER309L. Its current product guidance describes ER309L for similar 24%Cr-13%Ni steels and also for buffer layers on carbon-manganese steels and dissimilar joints. ESAB notes that dilution control matters when the rod is used for buffer layers and dissimilar joining.
That is the practical distinction: ER309L is commonly considered when the joint transitions between stainless and a lower-alloy steel, while ER310 is aimed at a more highly alloyed heat-resistant stainless family. Neither statement replaces procedure qualification, code rules, corrosion review or service-temperature requirements.
Use the WSP alloy pages as selection starting points
- WSP ER310 TIG filler page — heat-resistant 310-family starting point.
- WSP ER309L TIG filler page — common dissimilar-metal and 309-family starting point.
- WSP Alloy Support / AWS library — browse related classifications.
- WSP Filler Metal Finder — narrow the candidate family when the grade is not already known.
Verification list before welding
- Identify both base metals by documented grade, not appearance.
- Read the active WPS and confirm the filler classification is permitted.
- Verify whether the job is matching, dissimilar joining, buffer layer, overlay or repair.
- Review service temperature, corrosion exposure and dilution concerns.
- Use the exact manufacturer data sheet for the filler product being purchased.
Sources
Manufacturer values and application descriptions are product-specific examples. They are not the complete AWS specification limits and are not a WPS.
Leave a Reply