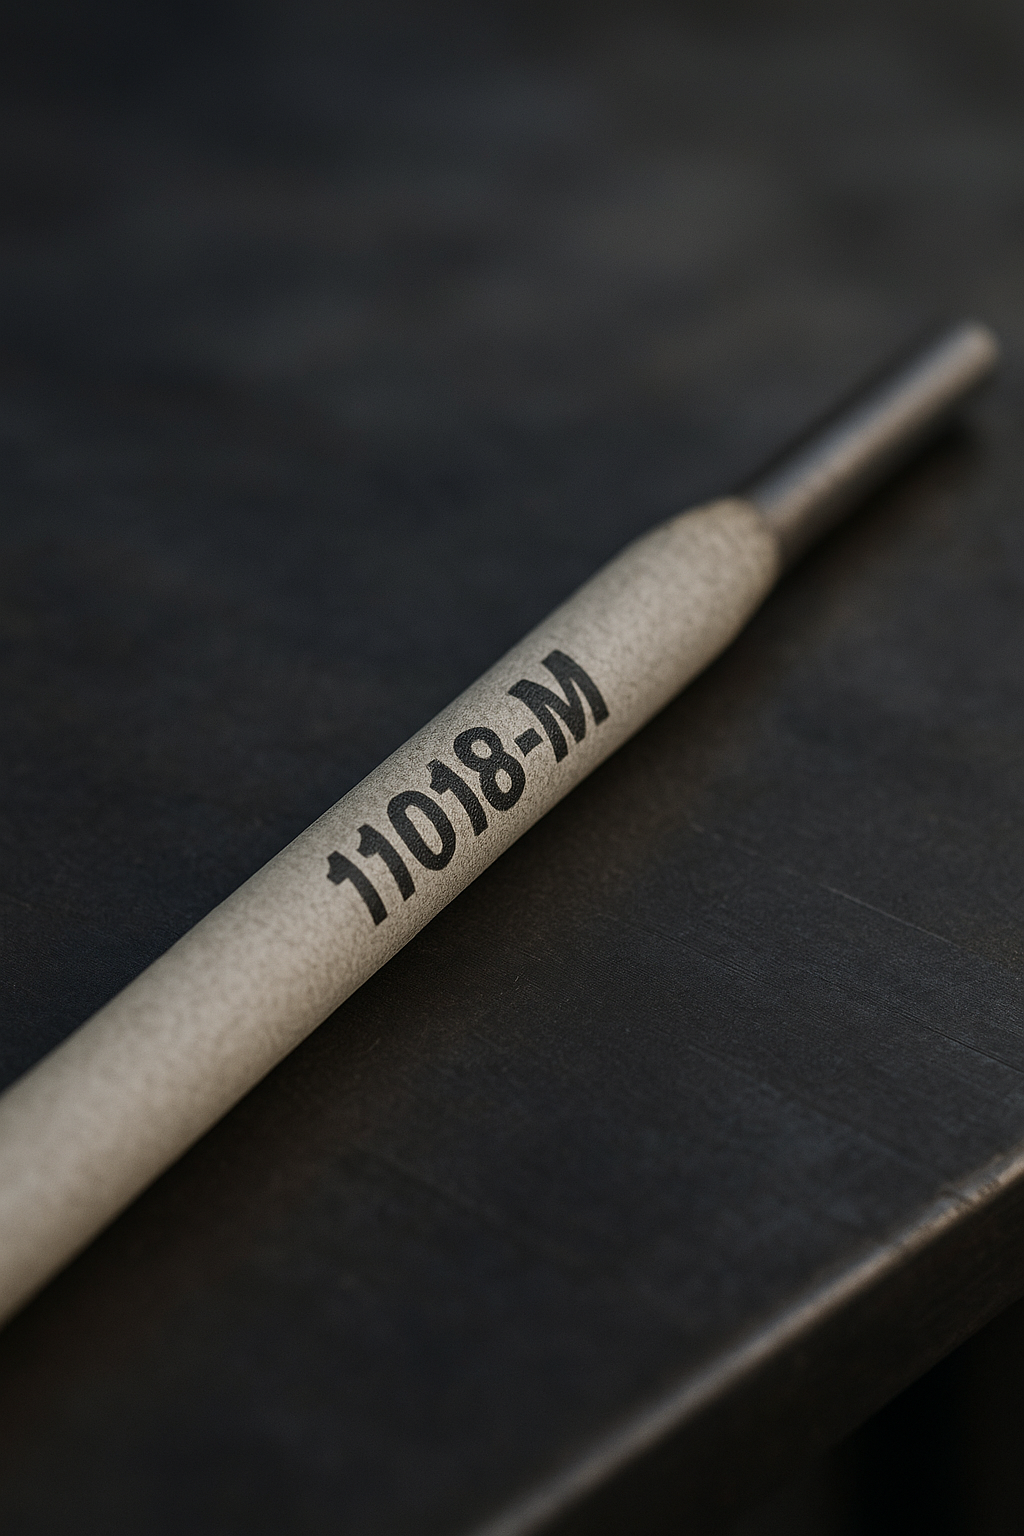
What E11018-M tells you—and what it does not
E11018-M identifies a high-strength low-alloy covered electrode classification. It is not blanket approval for a steel grade, repair, pressure vessel, or code job. Use the electrode manufacturer’s data sheet and the job’s approved welding procedure to establish suitability.
11018-M electrodes are often chosen by professional welders, fabricators, engineers, and QA inspectors working on critical infrastructure, where weld performance and compliance with code standards (such as AWS D1.1 or ASME IX) are non-negotiable.
If you’re welding on quenched and tempered steels or need to meet MIL-spec or code requirements, understanding how to use 11018-M electrodes properly is a must.
Types / Classifications / Variants
While 11018-M is a specific classification under AWS A5.5 for low-alloy steel electrodes, it comes in several variants based on performance and application needs:
- Read the complete classification printed on the package and its supporting data sheet.
- Additional hydrogen and moisture-resistance designators describe specified tests; they do not remove storage and handling requirements.
- Check the exact classification rather than substituting a similarly named electrode.
Key AWS Classification Breakdown (E11018-M):
- E = Electrode
- 110 = Minimum tensile strength (110,000 psi)
- 1 = All-position capable
- 8 = Low-hydrogen, iron powder coating
- M is part of the classification; it is not independent evidence of military approval or job acceptance.
Key Characteristics or Properties
11018-M rods are designed to deliver high mechanical strength and excellent ductility, even in critical joints subjected to stress, vibration, or extreme temperature shifts.
Check the specific electrode data sheet
Lincoln’s regional Excalibur 11018M data sheet lists E11018M H4R and 110 ksi minimum tensile strength. Yield, impact-test conditions, chemistry, usable positions, diameter, polarity, and current must be checked for the exact product and applicable specification. Typical manufacturer test results are not guaranteed properties of your completed joint.
Real-World Example:
A crane-boom repair is a case where the steel name and electrode tensile strength are not enough. Obtain the repair authority and approved procedure before selecting consumables; this article is not approval to repair a lifting component.
Process Considerations
Welding Process: SMAW (Shielded Metal Arc Welding)
11018-M is SMAW-only, making it ideal for field work and hard-to-reach weldments. It’s often used where wire-fed processes are impractical.
Equipment Compatibility:
- Use the power-source type, polarity, current range, and electrode diameter specified for the exact consumable and procedure.
- Follow manufacturer and job requirements for unopened storage, heated holding, exposure limits, and redrying.
- Do not assume a household oven, a generic temperature, or a longer heating time is an acceptable substitute.
Pros:
- High-strength weld metal
- Good impact resistance at low temperatures
- All-position usability
Cons:
- Requires preheat and postheat on some base metals
- Not suitable for thin or low-strength steels
- Rod storage and handling are critical
Application Use Cases
11018-M is designed for critical structural work that requires code compliance and toughness. It’s not for everyday mild steel jobs—this rod shines in specialized applications.
Typical Projects and Industries:
- Bridge and crane fabrication
- Pressure vessels and piping
- Military-grade armor steel
- Offshore platforms
- Power plant infrastructure
- High-strength steel repair welding
Ideal Base Metals:
- ASTM A514 (T1 Steel)
- ASTM A517 (Pressure vessel steels)
- HY-80 and HY-100 naval steels
- MIL-spec structural alloys
What makes this rod unique is that it maintains its strength while resisting cracking under high-stress or low-temperature conditions.
Best Practices & Pro Tips
Proper usage is critical with 11018-M to avoid weld failures. Here are some proven tips:
Rod Handling:
- Keep package identification and handling records with the electrodes.
- Use the manufacturer’s exact holding and redrying instructions and the job’s exposure limits.
- Quarantine questionable or damaged electrodes until their disposition is established.
Welding Technique:
- Use short arc length and maintain steady travel speed.
- Avoid weaving on vertical-up stringer beads are preferred.
- The backstep technique can reduce heat buildup on thinner base metal.
Joint Preparation:
- Preheat, interpass limits, heat input, joint preparation, and any postweld heat treatment come from the approved procedure and base-material requirements.
- Do not use a universal temperature range for high-strength steels.
Safety Tip:
- Due to higher amperage, rods get hotter. Use proper gloves and rod holders to avoid burns when removing stubs.
Conclusion
E11018-M may be specified for particular high-strength-steel work, but classification alone cannot establish code compliance, crack resistance, or joint acceptance. Keep the data sheet and approved procedure together.
Before purchasing, confirm the exact electrode, package size, diameter, classification, and procedure requirements. If those details are unresolved, seek the responsible welding authority’s direction first.
Some of the links on this page may be affiliate links. If you purchase through them, we may earn a small commission at no additional cost to you. This helps support our work in providing welding guides and reviews.

- AWS A5.5 E11018M ASME SFA 5.5 E11018M
- 10 LB Package – 11018-M
- 3/32“ Stick Electrode
- Tensile strength (psi) 120,001
- Yield strength (psi) 104,001
- AWS A5.5 E11018M ASME SFA 5.5 E11018M
- 10 LB Package – 11018-M
- 1/8″ Stick Electrode
- Tensile strength (psi) 120,000
- Yield strength (psi) 104,000
- AWS A5.5 E11018M ASME SFA 5.5 E11018M
- 10 LB Package – 11018-M
- 5/32“ Stick Electrode
- Tensile strength (psi) 120,002
- Yield strength (psi) 104,002
Last update on 2026-10-11 / Affiliate links / Images from Amazon Product Advertising API
Keep the details for your next job
Keep the electrode brand, complete classification, diameter, batch details, quantity, and storage location in one record. Do not mix unmarked loose rods into a traceable stock count.
Download the free consumables count sheet (PDF) — no signup required.
Read next
- Stick-machine input and duty-cycle checks — Read the rating for the actual supply available.
- Welding cable-selection inputs — Do not select leads from headline amperage alone.
Need a replacement? Start with parts identification before ordering. A lookup result is not manufacturer confirmation of compatibility.
Manufacturer references
- Lincoln Excalibur 11018M data sheet (regional product)
- Lincoln low-hydrogen electrode redrying guidance
Updated September 24, 2026: buyer-check information and related resources revised by Weld Support Parts. Manufacturer references are identified above where checked; this is not an independent product test, a welding procedure, or verification of every accessory on the page. Report a correction or suggest a guide.
Leave a Reply