Tag: cut quality
-
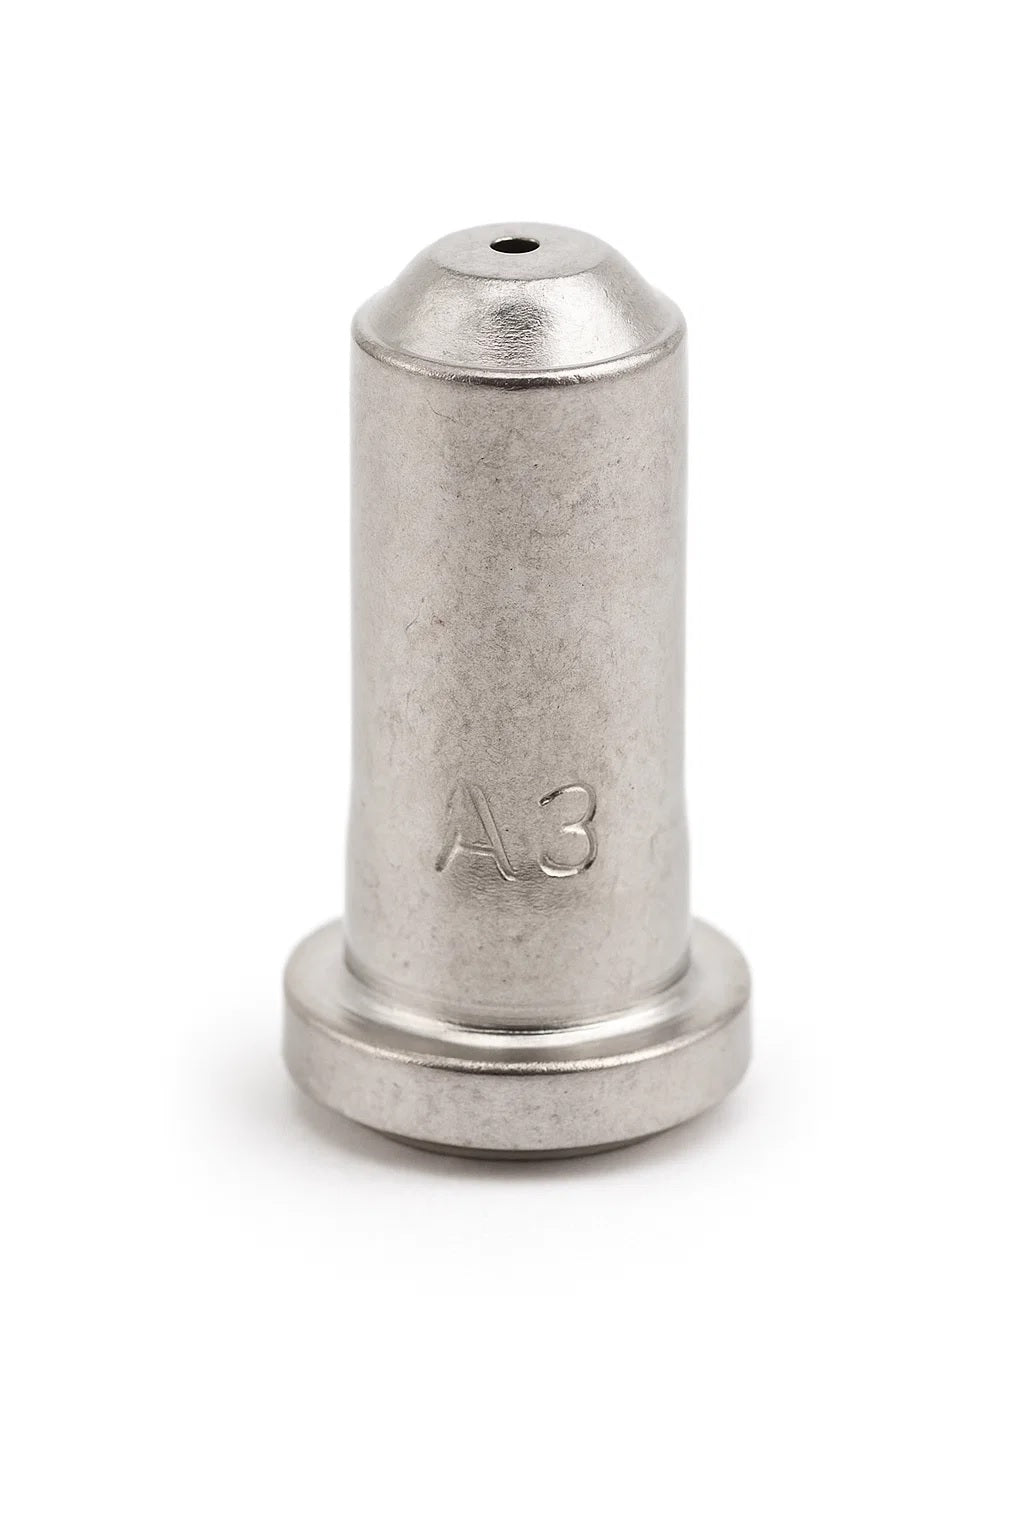
ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5): Product Breakdown
The ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5) is a consumable part used in plasma cutting. For buyers, maintenance teams, and welding support staff, the…
-
When to Replace Plasma Electrodes and Nozzles
Plasma consumables wear out by design. The question is not whether they will need replacement, but when wear starts affecting arc stability, cut quality, or torch protection. For maintenance buyers and weld…
-
Lincoln Electric FlexCut 45 Plasma Cutter Troubleshooting, Consumables, and Air Supply Setup
Troubleshooting guide for the Lincoln Electric FlexCut 45 plasma cutter covering arc transfer issues, consumable wear, air supply problems, cut quality issues, and setup verification.
-
Torch Tip Popping During Cutting
Torch tip popping during cutting is commonly caused by blocked tip passages, gas pressure imbalance, overheating, loose tips, or flashback-related flow problems.
-
Plasma Cutter Air Pressure Too High Symptoms
Excessive plasma cutter air pressure can cause unstable arcs, bevel cuts, double arcing, consumable wear, torch overheating, and poor cut quality.
-
Cutting Tip Slag Blockage Symptoms
Cutting tip slag blockage causes weak oxygen streams, uneven flames, rough cuts, heavy slag buildup, and torch instability during oxy-fuel cutting.
-
Plasma Consumable Wear Indicators: Electrode, Nozzle, Shield, Swirl Ring, and Retaining Cap Checks
If a plasma cutter starts leaving heavy dross, a wider kerf, angled cuts, poor starts, double arcing, arc dropouts, or inconsistent pierces, inspect the consumables before blaming the power source. Plasma consumable…