Tag: gun liner
-
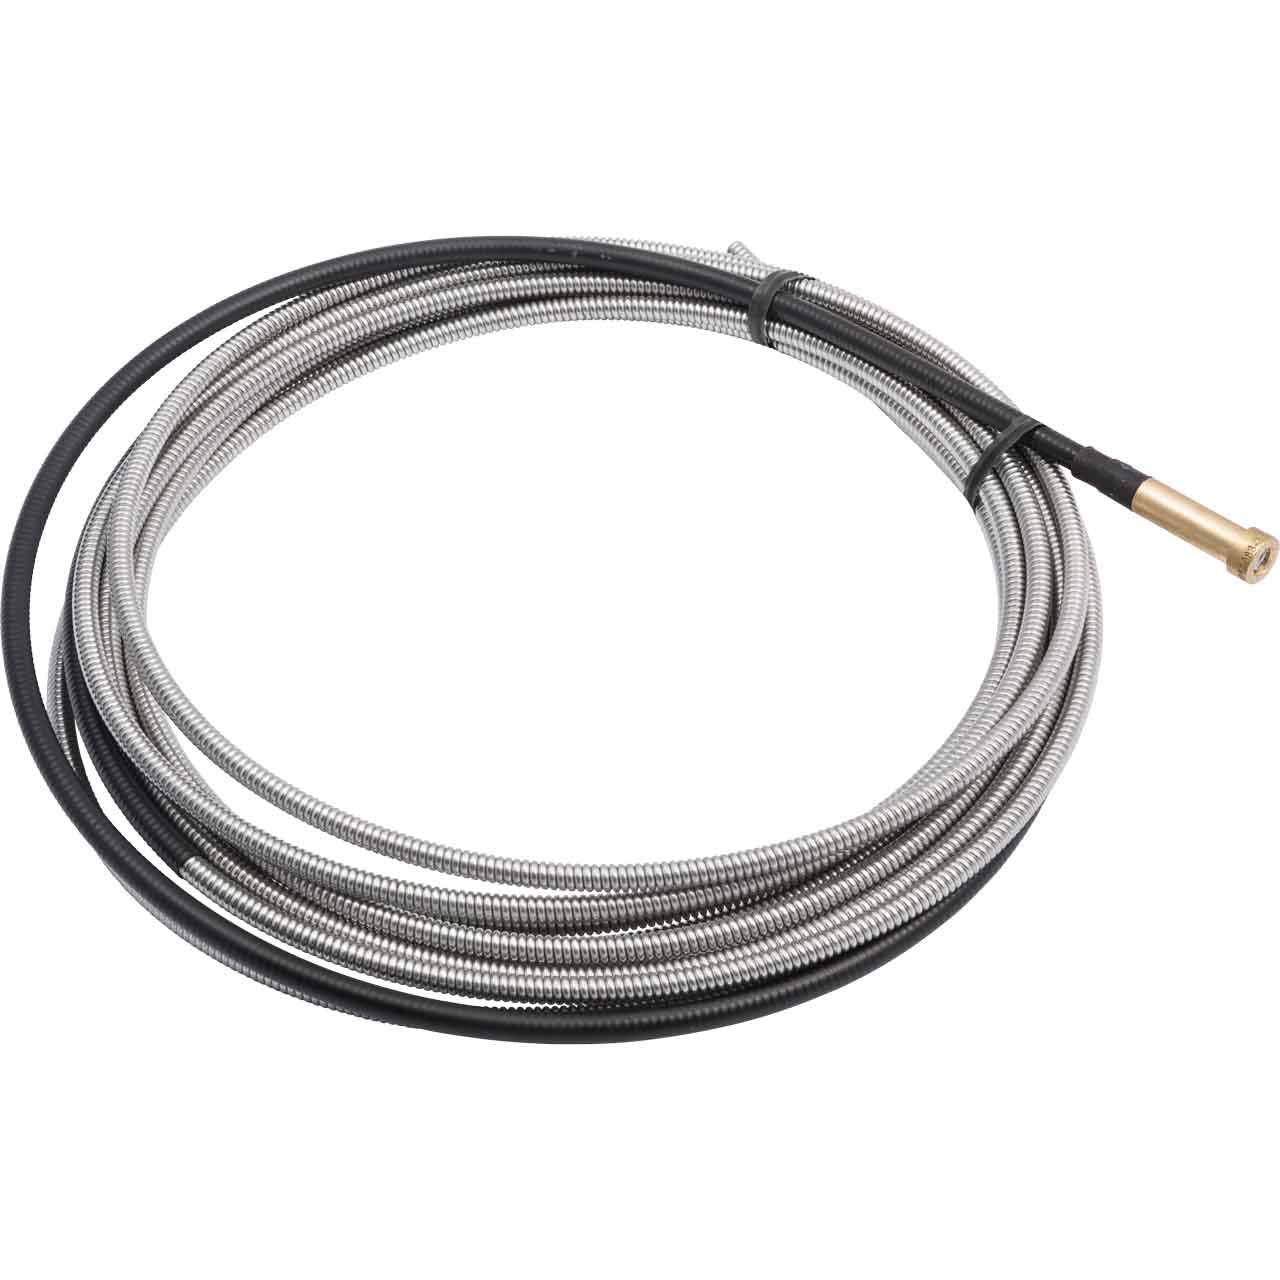
Lincoln Electric KP44-3545-15, .035-.045 Liner, 15′: Product Breakdown
“>
Lincoln Electric KP44-3545-15 is a 15 ft MIG gun liner for 0.035 to 0.045 in wire. In routine service, this type of liner is a wear item. When it becomes contaminated, kinked, or worn, wire feed quality can drop and the operator may see inconsistent feeding, burnbacks, or birdnesting. The practical value of a replacement liner is not complicated: reduce drag inside the cable, restore smoother feed, and remove one variable from the setup.
This article is a buyer guide and maintenance breakdown for shop use. It does not replace the gun manual or procedure qualification. If your gun model, drive rolls, or wire size are uncertain, verify before ordering.
Key Takeaways
- This is a consumable maintenance part, not a performance upgrade by itself.
- Wire feeding problems often trace back to liner condition, but the liner is only one part of the system.
- Match the liner to the gun model and wire diameter range before installation.
- If the feed path is dirty, damaged, or incorrectly assembled, a new liner may not solve the issue.
- Use the liner as part of a complete inspection: drive rolls, inlet guide, contact tip, cable routing, and spool tension all matter.
What This Liner Is Used For
KP44-3545-15 is intended for MIG wire delivery in the stated 0.035 to 0.045 in range. The 15 ft length is a practical detail for service planning, but it does not tell you everything about fit. In MIG guns, liner design must align with the specific gun family and cable assembly. If that information is not confirmed in your maintenance records, mark it as Unknown (Verify) and check the gun manual or parts listing before purchase.
Troubleshooting: When to Suspect the Liner
Use the liner as a suspect when feed problems appear at the gun end rather than at the feeder. Common signs include more drag when pulling wire by hand, erratic feeding that changes as the cable bends, or repeated feed interruptions after other parts have already been checked.
Check: Does the wire feed smoothly with the gun laid out straight?
Inspect: Are there sharp bends, crushed sections, or heat damage along the cable?
Verify: Is the liner size correct for the wire diameter and gun model?
Check: Are there signs of debris, rust, or liner wear at the ends?
Inspect: Remove the contact tip and look for wire shaving, discoloration, or contamination at the exit point.
Verify: Is the inlet and outlet path clean and aligned?
Check: Does feeding improve only when drive roll pressure is increased?
Inspect: Excess roll pressure can mask a liner problem and create more wire deformation.
Verify: Set drive tension only as high as needed to feed consistently.
Support Checks Before You Replace the Part
A liner swap is often justified, but it should not be a blind replacement. Before ordering, walk through the full feed path.
- Drive rolls: Inspect for wear, incorrect groove profile, or contamination.
- Inlet guide: Verify correct alignment and that the wire enters without scraping.
- Contact tip: Check for wear, spatter buildup, and bore size issues.
- Spool condition: Look for rust, birdnesting at the reel, or irregular unwind.
- Cable routing: Verify the gun cable is not twisted, crushed, or bent tighter than normal shop handling allows.
If these items are in acceptable condition and the feed issue remains, liner replacement becomes a logical next step. If several parts are worn at once, replace the worn items together so the diagnosis does not get blurred.
Product and Parts Notes
Product: Lincoln Electric KP44-3545-15, .035-.045 Liner, 15′
Listed application: MIG gun liner for 0.035 to 0.045 in wire
Length: 15 ft
Compatibility: Unknown (Verify). Confirm the exact Lincoln gun and cable series before ordering.
Installation note: Do not force the liner through a bent or obstructed cable. If the liner binds during installation, stop and inspect the cable path. Trimming should follow the gun manual, not guesswork.
Use the product listing as a maintenance reference when the liner part number is already known. If you are cross-checking the full gun assembly, verify the gun model number and compare it against the Lincoln parts documentation used in your shop.
How to Inspect the Liner in Service
Use a simple maintenance routine during downtime.
- Lock out the machine as required by site procedure.
- Remove the contact tip and visually inspect the wire path.
- Feed wire manually and feel for drag or pulsing resistance.
- Check the cable for kinks, crushing, or abrasion.
- Inspect the liner ends for contamination, wear, or misalignment.
- Reassemble and test feed at low speed before returning to production.
If the liner was replaced, record the part number, date, and observed condition of the old liner. That record helps maintenance decide whether the failure was due to normal wear, contamination, or a cable handling issue.
Safety Notes
- Disconnect power and follow site lockout/tagout rules before service.
- Wear gloves and eye protection when handling wire and liner ends.
- Do not assume feed problems are only mechanical; inspect for spatter and hot surfaces after welding.
- Keep fingers clear of drive rolls and pinch points during feed testing.
- Dispose of cut wire and used liner sections to prevent puncture injuries.
FAQ
How do I know if the liner needs replacement?
Look for rising feed resistance, inconsistent wire delivery, birdnesting, or repeated burnbacks after the rest of the feed path has been checked. If the liner is contaminated, kinked, or visibly worn, replace it.Can I use this liner with any Lincoln MIG gun?
No. Compatibility is Unknown (Verify) unless the exact gun and cable model are confirmed. Match the part number to the correct Lincoln gun series before ordering.Does a new liner fix every wire feeding problem?
No. Feed issues can also come from drive rolls, contact tips, spool tension, inlet guides, or cable damage. Treat the liner as one part of the system, not the whole diagnosis.Should I replace the liner on a schedule?
That depends on duty cycle, wire type, contamination, and cable handling. A fixed interval is Unknown (Verify). Replace based on inspection results and feed performance, not only on calendar time.Sources Checked
- ArcWeld product listing: Lincoln Electric KP44-3545-15, .035-.045 Liner, 15′
- Weld Support Parts internal product data provided in the task
- Internal link used for related wire reference: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog
Final note: treat the part number as the primary identifier, then verify gun model, wire diameter range, and cable condition before installation. That approach prevents avoidable feed issues and reduces repeat troubleshooting.
Related Arc Weld Part
Lincoln Electric KP44-3545-15, .035-.045 Liner, 15'
Lincoln Electric KP44-3545-15 is a 15 ft MIG gun liner built for 0.035–0.045 in wire. Replacing a worn or contaminated liner helps restore smooth wire feeding by reducing drag inside the gun cable, which supports a steadier arc and fewer feed-related issues (birdnesting, inconsistent starts, burnbacks). It’s a practical maintenance item for high-use MIG setups, especially when you notice increased resistance durin…
View at Arc Weld StoreRelated Weld Support Guides
MIG Gun Liner Compatibility Guide
“>
Replacement MIG gun liners look simple, but the wrong liner will cause feed drag, birdnesting, inconsistent arc start, and burnback. MIG liner compatibility depends on the gun model, feeder-to-gun connection, wire diameter, liner type, and the required liner length.
Key Takeaways
- Match the liner to the gun and feeder configuration, not just the wire diameter.
- Verify liner type: steel, graphite, or other liner material. Unknown (Verify) if the gun manual does not specify.
- Measure the required liner length from feeder connection to gun neck or tip path per the gun instructions.
- Trim only as directed by the gun or liner manufacturer. Over-trimming can create feeding problems.
- If wire feeding becomes erratic after a liner change, check for kinks, wrong diameter, poor cutoff, and incorrect installation before replacing the gun.
What MIG Liner Compatibility Actually Means
A compatible MIG liner must fit the gun physically and support the wire size you are running. A liner that is correct for .030 in. wire may not feed .035 in. wire properly, especially on longer gun leads or with softer wire. Compatibility also depends on the gun connection style, the neck style, and whether the liner is intended for steel, aluminum, or flux-cored applications.
If any of those points are unknown, verify them before ordering. Do not assume all liners in the same brand family are interchangeable.
What to Verify Before Ordering a Replacement Liner
- Gun model: Check the exact MIG gun model number.
- Feeder and connection style: Verify the rear connection at the feeder and the front connection at the neck. Unknown (Verify) if not documented.
- Wire diameter: Confirm the wire size in use, such as .030, .035, or .045 in.
- Wire type: Solid wire, flux-cored wire, or aluminum wire may require different liner behavior.
- Liner length: Match the required length to the cable and gun setup.
- End fittings: Some liners need specific end fittings or cut lengths. Unknown (Verify) if not specified.
How Wire Diameter Affects Liner Choice
The liner must support the wire diameter without excess friction or excessive clearance. Too tight, and the wire drags. Too loose, and the wire can wander, snag, or feed inconsistently. That matters more as gun length increases.
General rule: use the liner size specified for the wire you are running. If the feeder is set up for one size and the liner is sized for another, verify the whole feed path before operating.
How Liner Length Affects Feed Quality
A liner that is too short will not support the wire path correctly. A liner that is too long can buckle, bind, or prevent proper seating at the feeder or gun neck. Cut length matters. Measure and trim only to the instructions for that liner and gun.
Do not guess the cutoff point. Small errors can create intermittent feed issues that look like a bad drive roll or bad gun when the liner is the actual problem.
Installation Steps
- Turn off the power source and isolate the feeder before service.
- Remove the contact tip and nozzle.
- Back off drive roll pressure and remove the wire if needed.
- Remove the old liner and inspect the gun cable for kinks, crushed sections, or liner debris.
- Insert the new liner from the correct end.
- Seat the liner fully at the feeder end and at the gun neck end per the gun instructions.
- Trim only to the specified length. Unknown (Verify) if the gun manual does not show the cutoff method.
- Reinstall consumables and rethread wire.
- Set drive pressure and test wire feed at low speed first.
Troubleshooting Poor Wire Feeding
Symptom: Wire surges or hesitates
- Check for incorrect liner size.
- Inspect for liner kinks or crushed cable sections.
- Confirm the liner is fully seated at both ends.
- Verify drive roll tension is not too loose or too tight.
Symptom: Wire birdnests at the feeder
- Check for excessive drag in the liner.
- Confirm the liner is not blocked by debris, rust, or wire shavings.
- Verify the tip is not restricted.
- Inspect drive rolls for wear or mismatched groove type.
Symptom: Burnback or poor arc starts
- Check whether the liner is cut too short or not seated properly.
- Verify the contact tip size matches the wire.
- Confirm the wire path is smooth from feeder to tip.
Symptom: Feed is worse after liner replacement
- Confirm the replacement liner matches the gun model and wire diameter.
- Check whether the liner was trimmed to the wrong length.
- Look for a damaged cable or incorrect installation at the feeder or neck.
When to Replace the Liner
Replace the liner when wire feeding becomes inconsistent and cleaning does not restore performance. Common indicators include visible contamination, rust-colored dust, heavy wire shavings, intermittent drag, or a liner that has been kinked or overheated. If the gun has been used with spatter backflow or contaminated wire, inspect the whole feed path, not just the liner.
Product and Parts Note
For users cross-checking a replacement gun configuration, the following product is provided in the catalog for reference only:
Lincoln Electric K2951-1 Magnum PRO Curve 300 MIG Welding Gun, Semi-Automatic, 10 ft Cable
Lincoln Electric K2951-1 Magnum PRO Curve 300 MIG welding gun is built for semi-automatic MIG welding applications and includes a 10 ft cable for controlled handling and day-to-day shop use; the Curve 300 design is intended to support consistent feeding and operator comfort for fabrication and maintenance work—please confirm your welder/feeder and gun connection style match the Magnum PRO Curve 300 configuration b…
View at Arc Weld StoreConfirm the feeder connection style, gun model, and liner requirement before ordering any replacement part.
Safety Notes
- Lock out and isolate the welding power source before service.
- Wear gloves when handling cut liner ends. They can be sharp.
- Do not run wire feed tests with the nozzle removed near energized equipment without proper precautions.
- Replace damaged cables, liners, and consumables before returning the gun to service.
FAQ
Can I use any liner with the same wire diameter?
No. Wire diameter is only one part of compatibility. You must also verify gun model, feeder connection, liner type, and length.
Why does my new liner feed worse than the old one?
Common causes are wrong size, incorrect trim length, poor seating, cable damage, or drive roll setup issues.
Do I need a special liner for aluminum wire?
Often yes, but the exact requirement depends on the gun and feeder system. Unknown (Verify) unless the manufacturer states the liner type.
How do I know if the liner is too long?
Signs include binding, poor seating, and unstable feed after installation. Follow the gun instructions for the exact cutoff method.
Sources Checked
- Weld Support Parts blog: Welding Cable Connector Compatibility Guide (Dinse, Tweco, Cam-Lok & Stud Types)
- Weld Support Parts blog: Welding Electrode Holder: Stinger Guide & Stick Welding Tips
- Weld Support Parts blog: ArcOne S240-10 Auto-Darkening Welding Filter: Shade 10 Lens Support Guide
- Weld Support Parts blog: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy
Related Weld Support Guides
- Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog
- Welding Electrode Holder: Stinger Guide & Stick Welding Tips
- ArcOne S240-10 Auto-Darkening Welding Filter: Shade 10 Lens Support Guide
- Welding Cable Connector Compatibility Guide (Dinse, Tweco, Cam-Lok & Stud Types)