• ERNiCrMo-3 TIG / GTAW Filler Metal: Filler Metal Finder Notes

    ERNiCrMo-3 TIG / GTAW Filler Metal

    ERNiCrMo-3 TIG / GTAW filler metal is used on nickel-chromium-molybdenum applications where corrosion resistance and alloy matching matter. It is commonly discussed for Alloy 625-type work and corrosion-resistant overlays, but it should not be treated as a default choice. The correct selection depends on the WPS, the base metal, joint design, service environment, and the manufacturer data sheet.

    Use this page as a starting point for support and verification. It is not a substitute for procedure qualification or code compliance.

    Key Takeaways

    • ERNiCrMo-3 is a nickel alloy filler metal used in TIG / GTAW applications.
    • It is associated with Alloy 625-type work and corrosion-resistant overlays.
    • Confirm the WPS, code requirements, and base metal grade before ordering or welding.
    • Do not assume one filler covers every nickel alloy repair or overlay job.
    • Use manufacturer data sheets and the filler metal finder as selection tools, not as approval documents.

    What to Check Before You Use It

    For maintenance buying and field repair work, the most common failure point is not the weld technique. It is the selection step. Before you release a purchase order or load the machine, verify the following:

    • WPS status: Check whether ERNiCrMo-3 is actually listed on the active WPS.
    • Base metal grade: Confirm the substrate is the intended nickel alloy or overlay condition.
    • Service conditions: Identify whether the part sees corrosion, heat, dilution concerns, or chemical exposure.
    • Joint prep: Verify cleanliness, oxide removal, and access for TIG control.
    • Manufacturer data: Check the data sheet for the exact rod you plan to buy.

    Inspect: the material tag, heat number, repair record, or drawing notes. If the base metal is not clearly identified, stop and verify. Nickel alloy repairs are not the place to guess.

    Verify: whether the overlay or repair is meant to match a service requirement, a corrosion barrier, or a dimensional build-up. These are not the same thing.

    Troubleshooting and Support Notes

    If the weld procedure calls for a nickel-chromium-molybdenum filler and the job is not going as expected, work through the support checks in order.

    1) Filler selection does not match the base metal

    Check: the alloy designation on the part and the WPS callout. Some nickel alloy jobs look similar but are not interchangeable.

    Inspect: whether the job is a repair, a buildup, a joining weld, or an overlay. The target can change the filler choice.

    Verify: the required filler classification on the approved procedure. Do not substitute because the rod is commonly used on corrosion-resistant work.

    2) Poor wetting or unstable bead profile

    Check: shielding gas setup, tungsten condition, joint cleanliness, and travel speed. TIG / GTAW on nickel alloys is sensitive to contamination and technique changes.

    Inspect: the joint for oil, marker, oxide, moisture, or grinding residue.

    Verify: amperage range, arc length, and interpass control from the WPS and manufacturer guidance. If those are unknown, mark them as Unknown (Verify) and pause the job until confirmed.

    3) Unclear rod size selection

    Available sizes listed on product pages may include 1/16 in, 3/32 in, and 1/8 in, but exact offerings must be confirmed on the live product page and by the supplier.

    Check: whether the bead size, joint opening, and position support the rod diameter you plan to use.

    Inspect: whether the rod size fits the heat input control needed for the repair.

    Verify: the current page listing before ordering. If size availability is not shown, treat it as Unknown (Verify).

    Filler Metal Finder Section

    The ERNiCrMo-3 TIG / GTAW Filler Metal page should be used as a selection starting point only. It supports review, but it does not approve a procedure.

    Use the Filler Metal Finder to narrow the search, then confirm the final pick against the WPS and manufacturer data sheet. That is the correct sequence for support work:

    1. Identify the base metal and service requirement.
    2. Use the finder to locate the candidate filler family.
    3. Cross-check the WPS and code requirements.
    4. Confirm rod diameter, packaging, and current data sheet details.
    5. Release the order only after verification.

    If the application is an Alloy 625-type repair or corrosion-resistant overlay, ERNiCrMo-3 may be the starting point. If the job is outside that scope, stop and verify a different filler classification. Do not assume ERNiCrMo-3 is interchangeable with other nickel fillers.

    How to Review the Job Before Welding

    Use this practical checklist at the bench or in the maintenance shop.

    • Check the part number and repair description.
    • Inspect the joint for contamination and fit-up issues.
    • Verify the active WPS and any code limitation.
    • Check the filler classification listed on the procedure.
    • Inspect the filler rod label and packaging condition.
    • Verify that storage and handling have kept the rod clean and dry.

    Support Guidance for Buyers

    For buyers, the main risk is purchasing by name only. A product called ERNiCrMo-3 may still differ by manufacturer, package size, and documentation. Confirm the exact product page and the current data sheet before placing the order. If a required detail is missing, record it as Unknown (Verify) rather than filling in the blank.

    Safety Notes

    • Use appropriate PPE for TIG welding, including eye, face, and skin protection.
    • Maintain ventilation suitable for the work area and base material.
    • Handle nickel alloy filler metals according to site safety rules and the manufacturer instructions.
    • Do not weld on unidentified alloys without material verification.
    • Do not use this page as a substitute for code, procedure, or supervisory approval.

    FAQ

    Is ERNiCrMo-3 the right filler for every Alloy 625 job?

    No. It is commonly associated with Alloy 625-type work, but you still need to verify the base metal, service conditions, and the WPS before use.

    Can I choose ERNiCrMo-3 based on the filler metal finder alone?

    No. The finder is a selection starting point only. Always confirm the final choice against the WPS and manufacturer data sheet.

    What rod sizes are available?

    Common sizes may include 1/16 in, 3/32 in, and 1/8 in, but the current listing must be verified on the live product page. If not confirmed, treat the size as Unknown (Verify).

    Is ERNiCrMo-3 always interchangeable with other nickel filler metals?

    No. Interchangeability depends on the exact alloy, procedure, and service requirement. Verify before substitution.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • CGW Abrasives 48012, Resin Fibre Disc 4-1/2″ DIA 36 Grit (Sold in packages of 25): Replacement Part Breakdown

    CGW Abrasives 48012 is a resin fibre disc in 4-1/2 inch diameter with 36 grit, sold in packages of 25. For buyers and maintenance teams, the main question is not the label itself, but whether the disc matches the grinder, the workpiece, and the removal rate required for the job. This article breaks down how to evaluate it as a replacement abrasive, what to inspect before use, and what to verify before placing it in service.

    Key Takeaways

    • Use the disc only after confirming the grinder size, backing system, and arbor fit. Unknown (Verify) any compatibility detail not shown on the source listing.
    • A 36 grit fibre disc is typically chosen for more aggressive stock removal than finer grits, but exact cut rate depends on the application. Unknown (Verify).
    • Package quantity matters for inventory planning, especially for maintenance shelves and repetitive prep work.
    • Do not assume the disc is correct for stainless, carbon steel, or nonferrous work without checking the process plan and shop standard.

    Product and Parts Breakdown

    The listed product name identifies three primary elements: the brand family, the part number 48012, and the disc format. The disc is 4-1/2 inch diameter and 36 grit. The package quantity is 25. Beyond that, several technical points are not confirmed in the source data and should be treated as Unknown (Verify), including backing type details, maximum RPM, arbor configuration, coating type, and any special material recommendations.

    For replacement planning, confirm the disc against the actual grinder setup. Resin fibre discs generally depend on a compatible backing pad and proper mounting hardware. If the shop already runs 4-1/2 inch fibre discs, verify that the holder, nut, and pad stack are the same before swapping product families. Do not assume all 4-1/2 inch discs use the same support hardware.

    If you are comparing this disc to flap disc options for similar prep work, review the internal reference below as a process comparison point:

    Weldcote XL 4.5″ Flap Discs C-Prime Ceramic 60 Grit 7/8″ Arbor Pack of 10 for Heavy Duty Grinding (10669)

    How to Check Before You Buy or Install

    Check the grinder size. Confirm the tool is set up for 4-1/2 inch abrasives. Verify the guard and wheel dimensions for the grinder model.

    Inspect the mounting system. Identify the backing pad or support flange required for resin fibre disc use. If the pad type is not documented, mark it Unknown (Verify) and confirm with the tool or shop standard.

    Verify the arbor and fastener arrangement. Match the center opening and attachment method to the actual tool. Do not rely on assumptions from other disc families.

    Review grit selection. 36 grit is generally a more aggressive starting point than medium or fine finishing grits. Verify whether the task is weld cleanup, edge removal, blending, or heavy material removal before authorizing it for issue.

    Inspect package condition. Before receiving into stock, check packaging for crushing, moisture exposure, broken discs, or contamination. Store abrasives in a dry area.

    Troubleshooting and Support Checks

    If the disc is not cutting as expected, work through a basic support checklist before replacing the product.

    • Check: Is the disc installed in the correct rotation and seated flat against the backing support?
    • Inspect: Look for glazing, loading, edge wear, or contamination from oil, paint, or scale.
    • Verify: Confirm the grinder speed, pressure, and angle are within normal practice for the job. Specific limits are Unknown (Verify) unless documented by the manufacturer or your shop procedure.
    • Check: Is the workpiece material changing the cut behavior? Stainless, mild steel, and coated surfaces behave differently.
    • Inspect: Make sure the backing pad is not worn, cracked, or hardened. A damaged pad can reduce control and performance.

    If the disc breaks down too quickly, verify whether the operator is leaning on the tool, using the wrong angle, or starting on a contaminated surface. If the issue is inconsistent across multiple discs, the problem may be with the tool setup rather than the abrasive itself.

    Buyer Guide Notes for Maintenance Teams

    For storeroom buyers, this part is best treated as a repeat-use abrasive consumable. The package of 25 supports planned replenishment, but it also raises the need to track shelf life, rotation, and issue rate. Confirm whether your team uses the part for production grinding, repair work, or intermittent maintenance tasks. That determines whether a 25-pack is a practical stocking unit.

    When writing the internal item description, keep it simple: part number, diameter, grit, package quantity, and approved application notes. Avoid overcommitting the description to a specific base metal or finish result unless that is already proven in your shop standard.

    Safety Notes

    • Wear eye, face, hand, and body protection suitable for abrasive work.
    • Use the disc only with the correct guard and tool setup.
    • Do not install a disc that is cracked, warped, or contaminated.
    • Keep hands clear of the rotating abrasive during setup and first start.
    • Stop the tool if vibration, chatter, or abnormal noise appears.

    Always follow the grinder maker’s instructions and your site safety rules. If the disc or support hardware cannot be confirmed, treat the setup as Unknown (Verify) before use.

    FAQ

    Is CGW Abrasives 48012 a finishing disc or a heavy removal disc?
    Based on the listed 36 grit rating, it is better suited to more aggressive removal than fine finishing. Final performance depends on the material and setup.

    Does this disc fit every 4-1/2 inch grinder?
    No. Diameter alone does not confirm compatibility. Verify the arbor, backing system, guard clearance, and tool requirements before use.

    Can this be used on any metal?
    Do not assume that. Material compatibility is Unknown (Verify) unless confirmed by the product listing, the manufacturer, or your shop procedure.

    Why buy a 25-pack?
    A 25-pack can make sense for maintenance shelves, repeated prep work, and controlled stock rotation. It also helps standardize issue counts for recurring jobs.

    Sources Checked

    • Provided Amazon ASIN registry reference: B07DMFGLVW
    • Provided product name: CGW Abrasives 48012, Resin Fibre Disc 4-1/2″ DIA 36 Grit (Sold in packages of 25)
    • Allowed internal link: Weldcote XL 4.5″ Flap Discs C-Prime Ceramic 60 Grit 7/8″ Arbor Pack of 10 for Heavy Duty Grinding (10669)

    No additional specifications, certifications, prices, or compatibility claims were assumed. Any uncited technical detail should be treated as Unknown (Verify).

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 093 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 33 lb (15 kg) spool. For buyers and support teams, the main question is not whether the wire can weld mild steel—it can—but whether it matches the job’s fit-up, base-metal condition, and feeder setup. This article breaks down where this wire fits, what to verify before use, and how to troubleshoot common feeding and weld-quality issues without guessing at specifications that are not documented here.

    Key Takeaways

    • ER70S-2 is a solid MIG wire used for mild-steel fabrication, maintenance, and repair.
    • The .035 in diameter is a common general-purpose size, but final selection depends on procedure, material thickness, and wire-feed setup.
    • This product is described as triple-deoxidized with Al/Ti/Zr chemistry, which is intended to help when base metal has light mill scale or minor surface contamination.
    • The listing indicates a 33 lb spool and pack of one.
    • If your process, joint design, or code requirement is uncertain, verify the WPS, wire classification, and machine settings before welding.

    What This Wire Is For

    As listed, TC 70S-2 093 is aimed at mild-steel work in fabrication, maintenance, and repair. That makes it relevant for shops that need a practical solid wire for general production work and field repair where clean surface prep is not always perfect. The ER70S-2 classification is commonly used when a shop wants a wire that tolerates light oxidation better than a basic clean-steel setup.

    Do not assume this wire is the right answer for every joint. A MIG wire selection still depends on base metal chemistry, joint design, shielding gas, transfer mode, and the required mechanical properties of the finished weld. If any of those points are unclear, treat this product as a candidate, not a final approval.

    Inspect Before You Load the Spool

    Before installing the spool, do a basic receiving check.

    • Check the spool label against the purchase record. Confirm the product title and ER70S-2 classification.
    • Inspect the wire surface for visible rust, oil, kinks, or loose winding.
    • Verify the spool fits the feeder without forcing the hub or retainer.
    • Inspect the drive rolls, inlet guide, liner, and contact tip for wear or debris before loading the wire.
    • Verify the shielding gas, polarity, and wire-feed settings are correct for the procedure being used.

    If the shop has recurring feed issues, the wire is not the first thing to blame. Check the feeder path, tension, liner condition, and tip wear before changing consumables again.

    Troubleshooting Support: What to Check First

    Problem: Erratic feeding or birdnesting

    • Check drive-roll pressure. Too much pressure can deform the wire; too little can slip.
    • Inspect the liner for wear, contamination, or tight bends in the gun cable.
    • Verify the contact tip size matches the wire diameter. If unsure, use Unknown (Verify) until the correct tip is confirmed.
    • Check the wire path from spool to gun for sharp drag points.

    Problem: Excess spatter or unstable arc

    • Inspect shielding gas flow and nozzle condition.
    • Verify voltage and wire-feed speed against the procedure or WPS.
    • Check that the work clamp has solid contact and the joint is clean enough for the process.
    • Inspect for contamination such as paint, oil, or heavy scale.

    Problem: Porosity in the weld bead

    • Verify gas coverage at the nozzle and around the joint.
    • Check for drafts, leaks, or a damaged gas hose.
    • Inspect the base metal surface and remove moisture, oil, and heavy rust before welding.
    • Verify the filler wire is not contaminated from poor storage.

    Selection Support: Where to Confirm the Filler Metal

    If your team needs a starting point for filler selection or cross-checking wire classifications, use the WSP resources as reference tools rather than automatic approvals. When available, the filler metal finder should be treated as a selection starting point, not a guarantee that a procedure is approved for your job, code, or base metal combination.

    Use those pages to narrow down options, then verify the actual WPS, shielding gas, and wire classification before production use.

    Product and Parts Notes

    This listing is for one spool of Washington Alloy TC 70S-2 093. The documented size is .035 in and the documented spool weight is 33 lb. Beyond that, do not assume details such as drive-roll type, recommended gas mix, or exact machine compatibility unless your internal procedure sheet or manufacturer documentation confirms them. For uncertain technical details, mark them as Unknown (Verify).

    For buyers, the important points are simple: confirm the classification, confirm the diameter, confirm the spool weight, and confirm that the feeder setup matches the wire path requirements of your machine. If the wire is being purchased for a repair bay, make sure the operators know whether the work is light fabrication, maintenance welding, or a qualified procedure with tighter limits.

    Practical Use Notes

    Triple-deoxidized ER70S-2 wires are often chosen when the surface is not ideal, but that does not eliminate prep. Remove loose scale, paint, oil, moisture, and heavy corrosion whenever possible. The more contaminated the joint, the less likely any MIG wire will produce reliable results. The right response is better cleaning, not overreliance on filler metal chemistry.

    For shop support teams, the right workflow is: identify the base metal, confirm the required process, match the filler classification, and verify the feeder hardware. This wire may be a good general-purpose option, but the procedure still controls the final weld.

    Safety Notes

    • Use proper PPE for MIG welding, including eye, face, hand, and body protection.
    • Keep the work area ventilated and control fumes at the source when possible.
    • Do not weld on coated or unknown materials until hazards are identified.
    • De-energize equipment before servicing the feeder, liner, or gun components.
    • Store wire clean and dry to reduce contamination risk.

    FAQ

    Is TC 70S-2 093 suitable for mild steel?
    Yes, the listed application is mild-steel fabrication, maintenance, and repair. Final suitability still depends on the WPS and job requirements.

    Can I use this wire on material with light mill scale?
    The product description says the triple-deoxidized ER70S-2 chemistry is suited for light mill scale or minor surface contamination. That is helpful, but it is not a substitute for proper cleaning.

    Does .035 in wire work in every MIG machine?
    No. Wire diameter compatibility depends on the feeder, drive rolls, liner, contact tip, and procedure. Verify the setup before loading the spool.

    Is the shielding gas confirmed in the product listing?
    Unknown (Verify). The available product information does not document a specific gas requirement.

    Sources Checked

    • ArcWeld product listing: TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)
    • Provided product short description and source idea
    • Allowed internal links provided in the task

    This draft uses only the provided product information and internal links. Any details not explicitly documented should be treated as Unknown (Verify).

    Related Arc Weld Part

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 093 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 33 lb (15 kg) spool for mild-steel fabrication, maintenance, and repair, delivering stable arc characteristics and consistent feeding; its triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) is well-suited for producing clean welds when the base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1)…

    View at Arc Weld Store

    Related Weld Support Guides

  • Before the Machine Goes Down: A Practical Maintenance System for Welding Shops

    A machine rarely chooses a convenient time to go down. The failure lands in the middle of a production day, and the first few minutes usually sound the same: Who worked on it last? Was that cable replaced? When did the compressor start making that noise? Is the part already on order?

    In a large operation, a computerized maintenance system may answer those questions. In a smaller welding or fabrication shop, the answer is often spread across a notebook, a whiteboard, a stack of receipts, and the memory of the one person who seems to know every machine. That system works—until that person is off, the note disappears, or the same problem returns six months later.

    Good maintenance records are not office decoration. They help a shop decide what needs attention, who owns the next step, and where downtime is actually coming from. The system does not have to be complicated. It does have to be used.

    Start with four questions

    A practical shop-maintenance system should answer four questions without a scavenger hunt:

    • What equipment do we have? Record a clear asset ID, description, location, status, and the information needed to find the correct manual or service history.
    • What work is due? Keep recurring inspection and maintenance tasks in one schedule, with an owner and the correct calendar- or meter-based interval for that asset.
    • What happened last time? Document service, repairs, findings, parts, labor, outside service, and corrective action while the details are still fresh.
    • What is the interruption costing? Separate the price of the repair from the hours and production exposure created by the downtime.

    Those questions apply to more than welding power sources. Plasma systems, fume extraction, compressors, saws, positioners, ovens, material-handling equipment, and other recurring shop assets all compete for maintenance attention. Without a common record, urgent work crowds out preventive work and yesterday’s temporary repair quietly becomes today’s operating condition.

    A record should help the next person

    “Checked machine” is not a useful service entry. Neither is “fixed.” A useful record identifies the asset, the symptom or task, the work performed, the condition found, any parts used, the person or vendor involved, the result, and the next required action. If the unit remains out of service, that status should be visible instead of buried in a note.

    The goal is not paperwork for its own sake. The goal is continuity. A welder coming onto the next shift, a supervisor reviewing a repeat failure, or an outside technician arriving weeks later should be able to understand what has already happened. A consistent asset ID ties those records together even when several machines share the same model name.

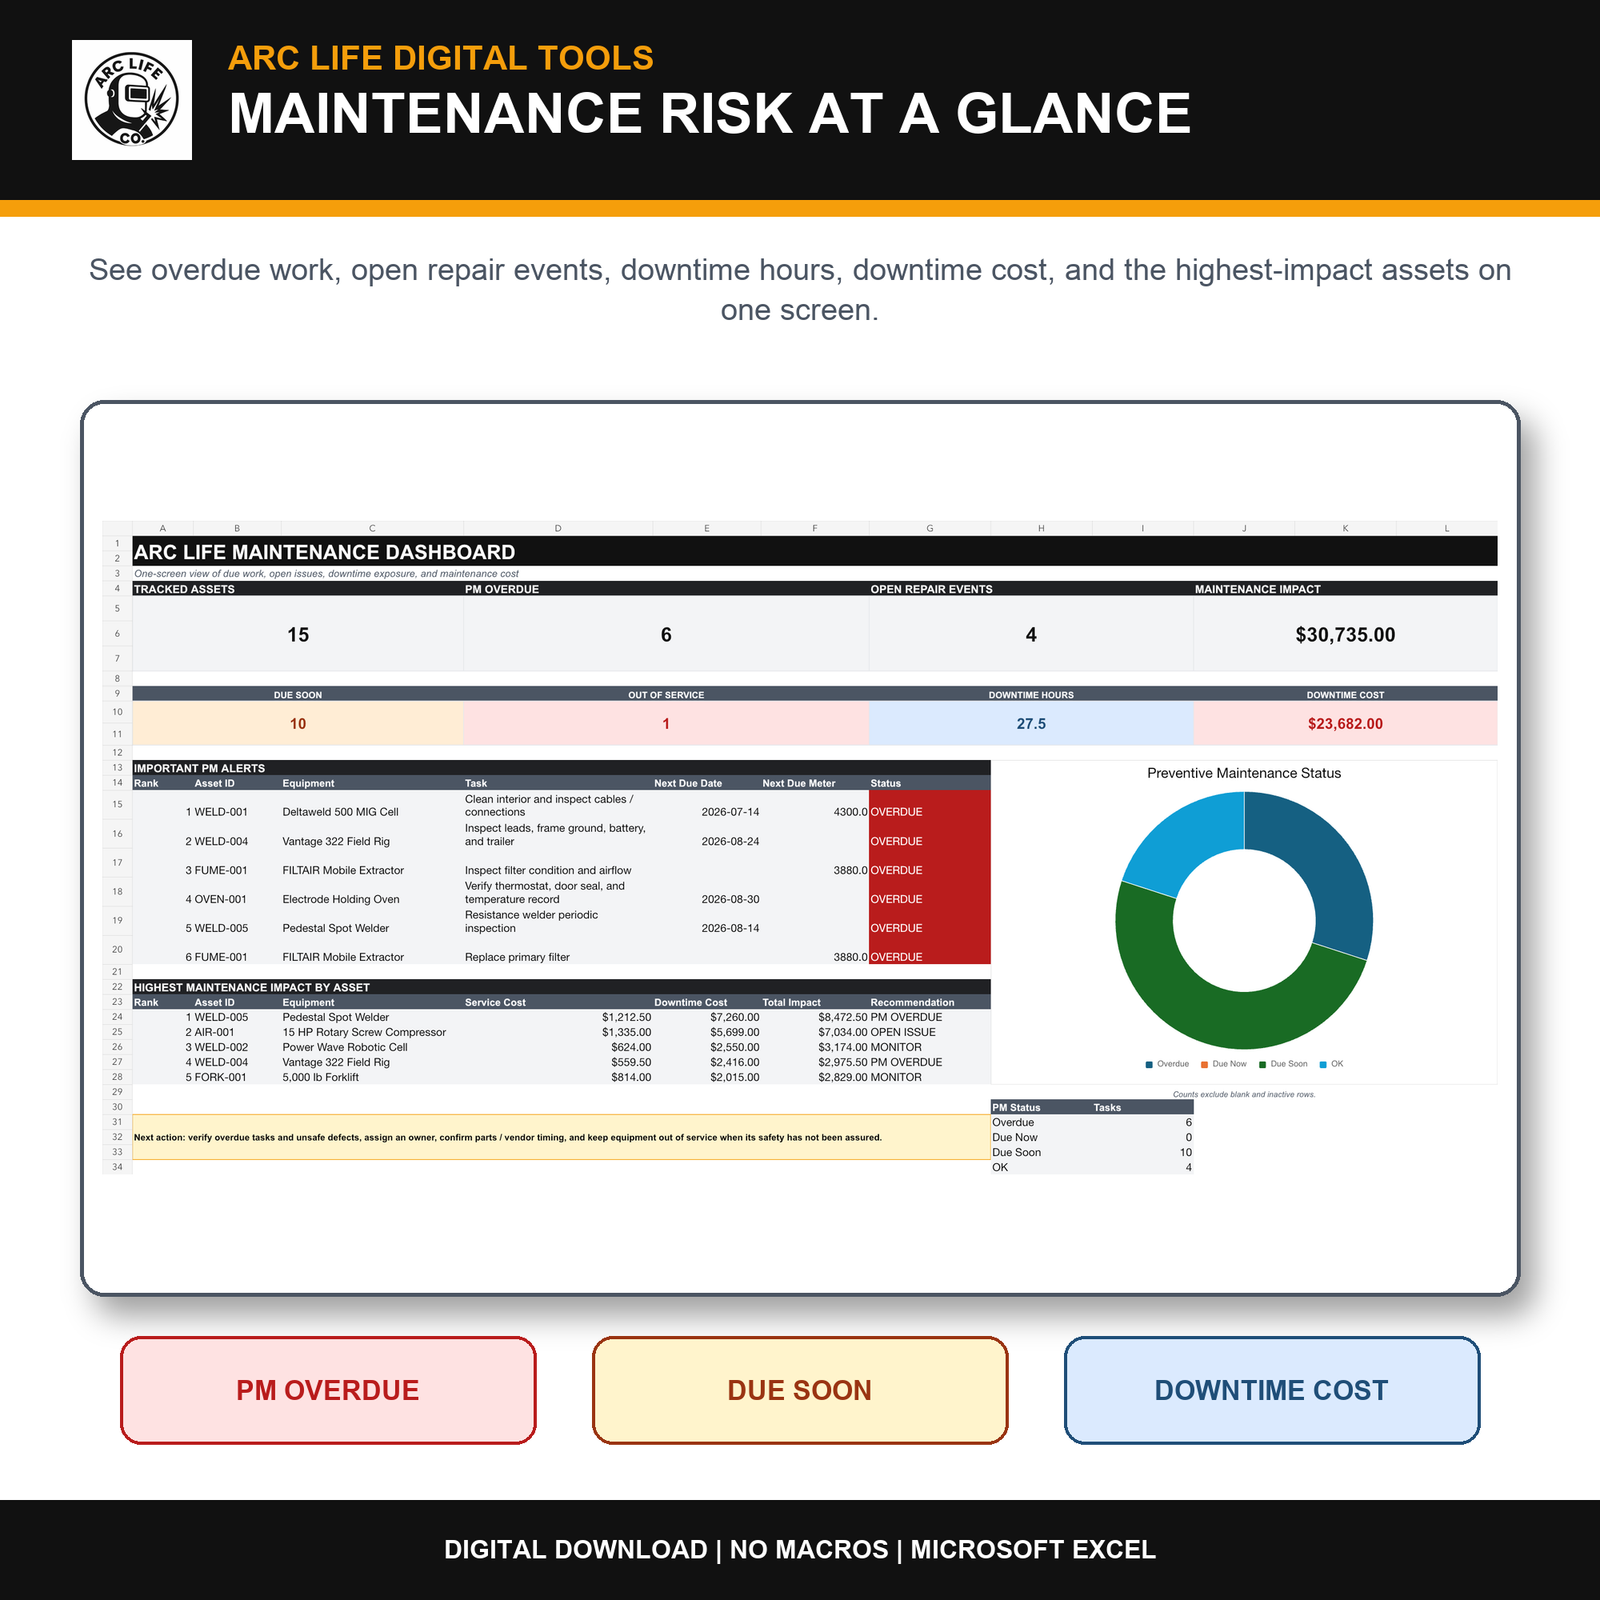
    Arc Life welding equipment maintenance dashboard showing overdue work, open repairs, downtime, and high-impact assets
    A useful dashboard should surface overdue work and open repair events without replacing the underlying service records.

    Use the dashboard as a question, not an answer

    Dashboards are valuable because they compress a lot of records into a short review. They can show overdue preventive work, open repair events, out-of-service equipment, downtime hours, and assets with unusually high maintenance impact. That makes it easier to decide where a morning meeting should begin.

    But a red cell is not a maintenance instruction. The correct task, inspection method, interval, and return-to-service decision still come from the current manufacturer documentation, qualified personnel, applicable inspection requirements, the shop’s operating conditions, and its safety program. A spreadsheet can organize those decisions. It cannot make them safely on its own.

    Where a spreadsheet fits—and where it does not

    Some shops need a full CMMS with automatic notifications, mobile scanning, work-order approvals, supplier integrations, user permissions, and enterprise controls. Others need a disciplined bridge between memory and enterprise software. That middle ground is where a well-built spreadsheet earns its place.

    The Arc Life Welding Equipment Maintenance Manager was built for that smaller-shop use case. The Excel system includes an asset register, preventive-maintenance schedule, service log, repair and downtime records, cost analysis, a dashboard, a quick-start guide, and six printable forms. It uses standard formulas rather than macros. The current version supports up to 200 assets, 500 recurring maintenance tasks, 1,000 service events, and 500 repair or defect events.

    That capacity only matters if the workflow is kept honest. Demonstration data must be replaced. After recurring service is recorded, the corresponding last-service values still need to be updated. Equipment that has not been made safe should remain out of service, regardless of what a dashboard says. The tool is a planning and recordkeeping aid—not a substitute for lockout/tagout, inspections, training, qualified maintenance, or engineering judgment.

    The habit is more important than the file

    The best maintenance file in the world becomes useless when nobody owns it. Pick one person responsible for the weekly review, define who closes tasks, and decide where paper forms or field notes enter the main record. Keep the process short enough that it survives a busy week. Then review repeat problems and high-impact assets instead of merely clearing colored cells.

    A shop will never eliminate every surprise. It can stop treating every surprise like the first time it happened.

    Shop question: What piece of equipment causes the most disruption when it goes down—and could your current records show its last three service events in less than a minute?

    Explore the full collection of practical shop systems in Arc Life Digital Tools.

  • ERNiCr-3 TIG / GTAW Filler Metal: Filler Metal Finder Notes

    ERNiCr-3 TIG / GTAW Filler Metal

    ERNiCr-3 TIG / GTAW filler metal is used as a starting point for nickel-chromium filler selection on Alloy 600-type base metals and some dissimilar high-temperature joints. It is not a substitute for the WPS, base metal identification, code review, or manufacturer data sheet. Before ordering or welding, confirm the weld joint requirements and match the filler to the application, not just the alloy name.

    Key Takeaways

    • Use the filler metal class as a starting point, not final approval.
    • Confirm the base metal grade, service temperature, and corrosion environment.
    • Verify WPS coverage, code requirements, and consumable control before production.
    • Do not assume all ERNiCr-3 rods are interchangeable across applications.
    • If the job involves dissimilar metals or elevated temperature service, review the full weld package first.

    What ERNiCr-3 Means in Practice

    ERNiCr-3 is a nickel-chromium filler metal classification used with GTAW/TIG. The class is commonly associated with nickel alloy 600-type base metals and some dissimilar joints that need high-temperature performance. The classification alone does not tell you whether the weld is acceptable for your job. It does not replace chemical compatibility checks, weld procedure qualification, or service-condition review.

    For support teams and buyers, the practical question is simple: does the weld plan require ERNiCr-3, or does the application call for another nickel filler based on the WPS and base metal? If the answer is not documented, stop and verify before release.

    How to Use the Filler Metal Finder Page

    The ERNiCr-3 TIG / GTAW Filler Metal page should be treated as a selection starting point only. It gives a useful reference for classification and general application, but it does not guarantee code acceptance or procedure approval.

    The linked filler metal finder is also a starting point. Use it to narrow candidate consumables, then verify against the WPS and the manufacturer data sheet. If your job has any of the following, do not rely on the finder alone:

    • specified corrosion limits
    • high-temperature service
    • dissimilar metal joints
    • pressure-boundary work
    • code inspection hold points

    Check, Inspect, Verify Before Welding

    Check: Confirm the WPS lists ERNiCr-3 for the joint, process, position, and thickness range. If the WPS is missing or unclear, do not start fit-up for production work.

    Inspect: Confirm the base metal grade by MTR, heat number, stamping, or positive identification method used by your shop. Alloy 600-type is the general reference in the source material, but exact grade verification is still required.

    Verify: Review service conditions. Elevated temperature, oxidation, thermal cycling, and dissimilar expansion behavior can change filler selection. If service conditions are unknown, record them as Unknown (Verify) and hold the job until engineering or the customer clarifies the requirement.

    Check: Verify consumable diameter, package condition, and storage status. The source keywords reference 1/16 in, 3/32 in, and 1/8 in, but size availability and fit are Unknown (Verify) until you confirm the actual stocked item and the welding requirement.

    Inspect: Look for damaged rod, contamination, bent sections, or compromised packaging. Nickel filler metal contamination can affect arc stability and weld quality.

    Verify: Match the filler lot and label to receiving records before issue. Do not assume an unlabeled rod tray is acceptable for controlled work.

    Troubleshooting Support Notes

    If the weld procedure calls for ERNiCr-3 but the bead profile, wetting, or cracking behavior is not as expected, pause and review the following:

    • Joint preparation: Check cleanliness, oxide removal, and fit-up.
    • Base metal ID: Verify the substrate is the intended nickel alloy or dissimilar combination.
    • Shielding gas setup: Confirm gas type and flow per the WPS. If unknown, mark Unknown (Verify).
    • Heat input control: Excessive heat can distort the joint or alter the weld surface condition.
    • Contamination sources: Check brushes, solvent residue, handling gloves, and shop dust.

    If procedure acceptance is still not clear after basic checks, stop and compare the job requirements to the approved data package. Do not attempt to “solve” a consumable mismatch with parameter changes alone.

    Selection and Ordering Notes for Buyers

    Buyers and maintenance planners should avoid ordering filler metal by classification only. Use the following control points:

    • WPS and qualification status
    • base metal identification
    • joint type and service environment
    • required diameter, if known
    • storage, traceability, and issue control

    If a request comes in as “nickel rod for high-temp work,” that description is too broad. Request the drawing, WPS, or engineering note. If none is available, write the requirement as Unknown (Verify) and escalate.

    Safety Notes

    Use normal TIG/GTAW safety controls: welding PPE, ventilation, arc flash protection, and proper handling of hot metal. Nickel alloys can generate fumes and surface oxides during welding and cleanup. Follow your site safety rules and the applicable SDS from the manufacturer. If ventilation or exposure controls are not documented, treat them as Unknown (Verify) and do not proceed until they are addressed.

    Do not rely on visual similarity between filler rods. Similar-looking nickel rods can have different intended applications. Verify the label, classification, and documentation before issue.

    FAQ

    Is ERNiCr-3 always correct for Alloy 600?
    No. The source notes point to Alloy 600-type work, but final selection still depends on the WPS, code requirements, and service conditions.

    Can I use the filler metal finder page as approval for a weld job?
    No. The finder is a selection starting point only. It does not replace procedure approval, engineering review, or manufacturer data.

    What rod diameter should I order?
    Unknown (Verify). The source keywords mention 1/16 in, 3/32 in, and 1/8 in, but the correct size must be confirmed against the job requirement and actual stocked product.

    What if the base metal is not clearly identified?
    Stop and verify. Do not issue ERNiCr-3 based on assumption. Confirm the alloy grade before welding.

    Sources Checked

    Technical details not provided in the source pages are marked Unknown (Verify) and should be confirmed from the WPS, manufacturer data sheet, and job documentation before use.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • Western 103 & 104 Oxygen Acetylene Adaptors, A Size Hose to B Torch/Regulator: Replacement Part Breakdown

    Western 103 & 104 oxygen acetylene adaptors are replacement-style support parts used in oxy-fuel setups where hose-to-torch or hose-to-regulator interface needs to match the connection style on hand. For buyers and maintenance teams, the main job is not guessing from a listing title. It is verifying thread form, gas service, sealing method, and the exact end connections before a part goes into service.

    This article breaks the part down from a support perspective. It does not assume compatibility beyond the product title. If your setup is not already documented, treat every connection detail as Unknown (Verify) until checked against the torch, regulator, hose, and plant standards.

    Key Takeaways

    • Use the product as a replacement support part, not as a substitute for confirmed connection data.
    • Verify gas service before installation: oxygen and acetylene are not interchangeable.
    • Check both ends of the connection: hose side and torch/regulator side.
    • Confirm thread condition, seal condition, and wrench engagement before putting the assembly back in service.
    • If any detail is unclear, stop and verify instead of forcing the fit.

    What to Check Before Ordering

    Support buyers often start with the name alone: “A size hose to B torch/regulator.” That description is useful, but it is not enough to approve a replacement. The field check needs to answer four questions.

    • Check the hose size: Confirm the hose end actually matches the A size hose connection used in your setup. If the existing hose fitting is worn, measure and compare against the original part record. Unknown (Verify) if no record exists.
    • Inspect the mating side: Identify whether the torch or regulator side is a B connection in your application. Do not rely on color alone.
    • Verify gas service: Oxygen and acetylene fittings must remain in the correct service path. Do not cross-connect components based only on thread similarity.
    • Inspect the seal style: Some connections seal on thread form, some on a seat, and some on a gasket or washer. Unknown (Verify) unless you have the exact mating specification.

    Troubleshooting and Support Steps

    If the old adaptor is leaking, hard to tighten, or will not start cleanly, work through the issue in order.

    1) Check the physical condition

    • Inspect the threads for galling, flattening, or impact damage.
    • Check for rust, scale, oil, or burned contamination on the connection.
    • Inspect the sealing face or cone, if present, for nicks and deformation.

    2) Inspect the fit-up

    • Hand-start the adaptor only. It should thread in without binding.
    • If it stops early, do not use force. Back out and verify thread type and orientation.
    • Confirm the wrench size and clearance. A poor tool fit can round the flats and damage the body.

    3) Verify leak control

    • After installation, pressurize the system per site procedure.
    • Use approved leak-check practice for gas service. Unknown (Verify) if your shop has a specific test method, but do not rely on sound alone.
    • If a leak appears at the threads or seat, shut down and correct the root cause before reuse.

    For regulator-side symptoms that look like fitting trouble but may actually be pressure creep or seat leakage, see Oxygen Regulator Pressure Creep Troubleshooting: Oxy-Fuel Gauge Rise, Seat Leak, and Safe Repair Path. That page is a troubleshooting reference, not a substitute for a pressure test or a qualified repair decision.

    Product and Parts Breakdown

    The Amazon product linked for this draft is Western 103 & 104 Oxygen Acetylene Adaptors, A Size Hose to B Torch/Regulator with ASIN B06X93Y1RF. The listing title indicates the intended connection family, but the fine details remain verification items for the buyer.

    • Product name: Western 103 & 104 Oxygen Acetylene Adaptors
    • Connection intent: A size hose to B torch/regulator
    • Use case: Replacement part for oxy-fuel support setup
    • ASIN: B06X93Y1RF
    • Detailed specs: Unknown (Verify)
    • Compatibility with specific torch models: Unknown (Verify)
    • Thread standard, material, and certification claims: Unknown (Verify)

    When evaluating this part for a purchase order or maintenance bin, compare it against the original assembly and the equipment tag. If the removed adaptor is still available, match end geometry, thread direction, sealing surface, and service marking before accepting the replacement.

    View the Western 103 & 104 adaptor product listing

    Installation Check List

    • Confirm gas service and correct line assignment.
    • Inspect both mating ends for damage and contamination.
    • Hand-start the adaptor to avoid cross-threading.
    • Tighten only to the level required by the connection design and site procedure.
    • Leak-check before returning the system to cutting or heating service.
    • Tag out and replace any part with cracked metal, stripped threads, or a damaged sealing face.

    Safety Notes

    • Oxygen system parts must be kept free of oil, grease, and fuel contamination.
    • Do not mix components across gas services unless the exact design allows it and the connection is verified.
    • Never force a thread that does not start cleanly.
    • Leak-check after any replacement, repair, or reassembly.
    • Follow site gas handling rules and lockout/tagout practices where required.

    FAQ

    Is this adaptor guaranteed to fit every oxy-fuel torch?

    No. The product title only shows the intended connection family. Torch compatibility is Unknown (Verify) unless you match the exact equipment and thread data.

    Can I use this part if the old adaptor almost fits?

    No. “Almost” is not acceptable on gas service fittings. Verify the connection completely before installation.

    What should I do if the fitting leaks after installation?

    Shut the system down, isolate the gas source, and inspect the threads, sealing surface, and assembly method. If the cause is unclear, remove the part and verify the specification before reuse.

    Should I choose based on hose color or torch color?

    No. Color may help identify service in the field, but it does not confirm thread type, seal method, or compatibility.

    Sources Checked

    • Provided Amazon ASIN registry entry: B06X93Y1RF
    • Provided product title: Western 103 & 104 Oxygen Acetylene Adaptors, A Size Hose to B Torch/Regulator
    • Allowed internal link: Oxygen Regulator Pressure Creep Troubleshooting

    WordPress SEO Fields

    • Focus keyword: Western 103 & 104 Oxygen Acetylene Adaptors, A Size Hose to B Torch/Regulator B06X93Y1RF
    • Category: Oxy-Fuel Cutting Support
    • Slug: western-103-104-oxygen-acetylene-adaptors-a-size-hose-to-b-torch-regulator-replacement-part-breakdown

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1) is a solid MIG wire intended for mild-steel fabrication, maintenance, and repair. The key points for buyers are straightforward: it is .035 in (0.9 mm) diameter, it is an ER70S-2 class wire, and it is supplied on a 44 lb (20 kg) spool. For welders and maintenance teams, the practical question is not just what the label says, but whether the wire fits the feeder, matches the job, and gives stable performance in the actual work environment.

    This breakdown focuses on what to check before purchase and what to inspect after the spool arrives. It does not assume machine settings, procedure approval, or certification details that are not stated on the product page. Where a detail is not confirmed in the provided source, it is marked as Unknown (Verify).

    Key Takeaways

    • TC 70S-2 104 is listed as a .035 in solid MIG wire for mild steel work.
    • The spool size is 44 lb (20 kg), which matters for feeder capacity and shop consumption rate.
    • ER70S-2 chemistry is commonly used when welders want a wire that can handle light mill scale or minor surface contamination better than basic clean-steel wire, but the actual base-metal condition still needs inspection.
    • Do not assume machine compatibility, polarity, shielding gas, or WPS approval from the product name alone. Verify those items against your equipment and procedure.

    What the Product Is Used For

    Based on the supplied product information, this wire is aimed at mild-steel fabrication, maintenance, and repair. That makes it relevant to production shops, farm and fleet repair, structural maintenance, and general fabrication work where a solid wire is preferred over flux-cored wire. The triple-deoxidized ER70S-2 chemistry is positioned for cleaner welds on steel that may have light mill scale or minor contamination. That does not remove the need for cleaning, but it may provide a wider practical window than a basic wire on less-than-perfect material.

    For buyer guidance, the first decision is whether your work is actually mild steel. If the job is stainless, aluminum, hardfacing, or a specialty alloy, this is not the right starting point. If the job is carbon steel and the feeder can handle .035 wire, it becomes a reasonable candidate for evaluation.

    Check Before You Buy

    • Check wire diameter: Confirm your feeder, drive rolls, contact tips, and gun setup are intended for .035 in wire.
    • Inspect spool capacity: Verify your feeder can physically accept a 44 lb spool. Some machines need an adapter or a different hub. Unknown (Verify).
    • Verify base metal: Confirm the job is mild steel or compatible carbon steel work.
    • Inspect the weld procedure: If you run controlled fabrication or repair work, verify the wire is allowed under your WPS or internal procedure before use.
    • Check shielding gas and polarity: Do not assume from the product name. Verify with your procedure and machine setup. Unknown (Verify).

    Troubleshooting and Support: What to Inspect if Feeding or Arc Stability Is Poor

    If the wire arrives and the arc is unstable, do not immediately blame the filler metal. Run a basic inspection sequence.

    • Inspect the drive system: Check drive-roll size, groove type, tension, and liner condition.
    • Check the contact tip: A worn or oversized tip can cause erratic feeding and arc wander.
    • Verify spool installation: Make sure the spool turns freely and is not over-tightened on the hub.
    • Inspect the gun cable: Look for kinks, tight bends, or internal liner wear.
    • Confirm wire cleanliness: If the wire has contamination, rust, or packaging damage, document it before use.

    If porosity appears, inspect the work surface, shielding gas flow, leaks in the gas path, and joint prep before changing wire type. If lack of fusion appears, verify voltage, travel speed, and joint prep. If burnback or birdnesting shows up, inspect wire feed tension, tip size, and liner friction first.

    WSP Lookup and Filler Metal Finder

    Use the Weld Support Parts lookup tools as selection starting points, not guaranteed procedure approvals. They help narrow options, but they do not replace a qualified WPS, procedure test, or equipment verification.

    WSP lookup page

    WSP filler metal finder page

    If your team uses filler metal search tools, compare the wire class, diameter, and intended base metal against your actual job. Then verify the final choice against machine limits, spool size limits, and procedure requirements.

    Product / Parts Review

    The listing provided for this article identifies TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1). The confirmed details are limited to the wire class, diameter, spool weight, and pack quantity. Other technical details such as country of origin, AWS approval language beyond the ER70S-2 class designation, exact gas recommendation, and machine compatibility are Unknown (Verify).

    For maintenance buyers, the main value of a large spool is reduced changeover time. For production or repair work, that can help reduce interruptions. The tradeoff is storage and handling. A 44 lb spool needs a feeder and shop process that can manage the larger package without feed problems.

    If you are comparing this wire against another ER70S-2 option, evaluate the following: feeder fit, spool size fit, workpiece condition, and your normal gas and procedure setup. Do not compare only on price or spool weight. Those alone do not tell you whether the wire will run well in your machine.

    Safety Notes

    • Follow your welding procedure, machine manual, and shop safety rules.
    • Verify ventilation and fume control before welding carbon steel.
    • Inspect the work area for fire hazards, especially during maintenance and repair work.
    • Use proper PPE for arc flash, spatter, and handling the spool.
    • Do not rely on product labeling alone for procedure approval or machine setup.

    FAQ

    Is TC 70S-2 104 Washington Alloy .035 meant for stainless or aluminum?
    No. Based on the provided information, it is a solid MIG wire for mild steel and general carbon-steel repair work.

    Can I assume it will run on my MIG welder?
    No. Verify feeder capacity, spool hub fit, liner condition, drive-roll size, and your machine settings. Unknown (Verify) until checked against your equipment.

    Does ER70S-2 mean I can skip metal prep?
    No. The chemistry may help with light mill scale or minor contamination, but it does not replace cleaning, fit-up, or procedure control.

    Is the 44 lb spool better than a smaller spool?
    It can be better for high-use shops because it reduces changeovers. But only if your feeder and storage setup can handle it. Verify before buying.

    Sources Checked

    • ArcWeld product page: TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)
    • Provided product source idea and short description in the task data
    • Allowed internal links list: reviewed for related Weld Support Parts content

    Final check before purchase: verify wire diameter, spool size, feeder fit, and procedure acceptance. If any of those are unknown, treat them as Unknown (Verify) until your team confirms them.

    Related Arc Weld Part

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 104 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 44 lb (20 kg) spool for mild-steel fabrication, maintenance, and repair, providing consistent feeding and a stable arc; the triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) helps produce clean welds when base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1) spool (verify your machine/spool…

    View at Arc Weld Store

    Related Weld Support Guides

  • ERNi-1 TIG / GTAW Filler Metal: Filler Metal Finder Notes

    ERNi-1 TIG / GTAW Filler Metal

    ERNi-1 is a commercially pure nickel filler metal used for TIG/GTAW applications on nickel base metals and some repair work. It is not a default choice for every nickel job. Before ordering rod or welding to procedure, verify the WPS, code requirements, base metal grade, service conditions, and manufacturer data sheet. The WSP filler metal finder page is a starting point for selection, not a procedure approval.

    Key Takeaways

    • Use ERNi-1 only when the procedure and base metal call for it.
    • Confirm AWS A5.14 classification on the product data sheet.
    • Check whether the job is Nickel 200/201, cast iron repair, or another nickel-related application.
    • Do not assume ERNi-1 is interchangeable with ERNiCu-7, ERNiFe-CI, or other nickel fillers.
    • Verify wire diameter, packaging, and shielding gas requirements from the manufacturer data sheet.

    What the ERNi-1 page is for

    The WSP ERNi-1 TIG / GTAW filler metal page is useful when you need a quick reference for commercially pure nickel rod. The page identifies ERNi-1 under AWS A5.14 and points to nickel base metal and repair starting points. Treat that as a first check only. The final selection still depends on the WPS, joint design, dilution control, service environment, and any code or customer requirements.

    If you are matching a repair job, start with the weld support page, then compare the filler classification against the base metal and service conditions. If the job involves corrosion exposure, elevated temperature, or a mixed-metal repair, do not assume the first nickel rod you find is acceptable.

    Check, inspect, verify before welding

    Check the WPS first. Confirm whether ERNi-1 is named, whether an alternate classification is allowed, and whether any postweld heat treatment is specified.

    Inspect the base metal identification. Verify the alloy grade on the part, the drawing, or the material cert. If the grade is unknown, stop and confirm it before welding.

    Verify service conditions. Temperature, corrosion exposure, and repair history can change filler selection. A rod that is acceptable for one maintenance repair may be wrong for another.

    Check the physical rod details on the product data sheet. Diameter options listed on the WSP page include 1/16 in., 3/32 in., and 1/8 in. Verify the exact size with the manufacturer data sheet before issuing material.

    Inspect storage and handling. Keep filler dry, clean, and separated from mixed stock. Contamination can create arc instability and weld defects.

    Troubleshooting and support notes

    If the weld is cracking, verify that the filler is correct for the base metal and service condition. Do not keep welding with the same consumable until the cause is identified.

    If the puddle looks overly fluid or the bead profile is poor, check heat input, tungsten condition, travel speed, and joint prep. ERNi-1 does not fix poor parameter control.

    If the repair is on cast iron or a nickel-iron mix, verify whether ERNi-1 is actually the intended filler or whether the job requires another nickel alloy classification. The WSP page should be used as a selection starting point only.

    If the rod size does not fit the job, verify the wire diameter before opening the package. Use the smallest practical size for thin sections and the size called out by the WPS when possible.

    Filler metal finder section

    Use the ERNi-1 TIG / GTAW Filler Metal page and the filler metal finder as selection tools. They help narrow the classification, process, and likely application, but they do not replace job-specific approval. Before ordering, confirm the base metal grade, procedure, and service conditions. If any technical detail is uncertain, use Unknown (Verify) until you confirm it from the WPS or manufacturer data sheet.

    For common support questions, verify whether the application is listed as Nickel 200/201 or as a cast iron repair starting point. If the job is outside those starting points, stop and re-check the filler classification. Do not infer compatibility from general nickel family naming alone.

    Selection checks for maintenance buyers and supervisors

    • Check the job traveler or WPS for the exact filler classification.
    • Inspect the material certification and base metal marking.
    • Verify whether backup consumables are allowed.
    • Confirm if a specific diameter is stocked or needs to be ordered.
    • Review the data sheet for handling and storage notes.

    Safety notes

    Follow normal TIG/GTAW welding safety practices. Use proper PPE, local exhaust ventilation, and burn protection. Nickel-containing welding consumables can create fume exposure concerns. Verify the shop’s ventilation controls and follow the applicable safety data sheet and site procedure.

    Do not weld on unidentified material. Do not rely on appearance alone to identify nickel alloys or cast iron. If the part history is unknown, stop and verify before starting arc work.

    FAQ

    Is ERNi-1 always the right choice for Nickel 200/201?
    Not always. It is a starting point, but the WPS, code requirements, and service conditions must confirm the selection.

    Can ERNi-1 be used for cast iron repair?
    It may be used as a starting point for some repair work, but that does not mean it is approved for every cast iron job. Verify the base metal, crack type, and procedure first.

    What rod sizes are available?
    The WSP page references 1/16 in., 3/32 in., and 1/8 in. Verify the actual stocked size and manufacturer packaging before order release.

    Does the finder page guarantee procedure compliance?
    No. It is a selection aid only. Final acceptance depends on the WPS, code, base metal, and manufacturer data sheet.

    Sources Checked

    • WSP product page: https://www.weldsupportparts.com/filler-metal-tig-erni-1.html
    • WSP filler metal finder: https://www.weldsupportparts.com/filler-metal-finder.html

    Note: Technical details not confirmed on the provided pages are marked as Unknown (Verify) by requirement and should be checked against the governing WPS and manufacturer documentation.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
  • Profax PX176243 Nozzle, Slip Type Tapered .375 Orif X 2.640, Pack of (1): Replacement Part Breakdown

    The Profax PX176243 nozzle is a replacement consumable part used in MIG welding torch setups. For maintenance buyers and shop support teams, the main job is not just ordering the right part, but verifying fit, condition, and wear pattern before downtime turns into a bigger torch problem. This guide keeps the focus on inspection, replacement checks, and the basic questions to answer before you install any nozzle.

    Key Takeaways

    • Confirm the nozzle style, fit method, and dimensions against the torch assembly before purchase.
    • Inspect for arc strikes, spatter buildup, taper damage, and bore distortion during regular maintenance.
    • Replace the nozzle when cleaning no longer restores gas coverage or when physical wear affects alignment.
    • Use the product listing as a part reference, not as proof of torch compatibility.
    • If a dimension or mating detail is unclear, mark it as Unknown (Verify) until the torch manufacturer or parts drawing confirms it.

    What this part is used for

    This is a nozzle replacement part for MIG welding support applications. The available product name identifies it as a slip type tapered nozzle with a .375 orifice and 2.640 overall length. Those are listing details, not a complete fit guarantee. Before stocking it in a maintenance bin, verify that your torch, diffuser, and contact tip arrangement are meant for this style of nozzle.

    Use the part as a consumable that supports shielding gas direction and torch-end protection. If the nozzle is damaged, the weld may show inconsistent shielding or visible spatter issues. If the torch uses another style of front-end hardware, do not assume interchangeability.

    Inspection and replacement checks

    Use the following routine during torch maintenance:

    1. Check the exterior. Look for spatter buildup, heat discoloration, dents, ovalizing, or arc strikes.
    2. Inspect the bore. Verify the opening is clean and round. If the bore is narrowed by spatter or warped by heat, performance can suffer.
    3. Verify the fit. Confirm the slip fit seats correctly on the torch front end. If it rocks, binds, or sits loose, stop and verify the mating parts.
    4. Inspect the taper. Damage at the taper can affect shielding gas flow and torch access in tight joints.
    5. Check cleaning history. If repeated cleaning is needed after very short run times, the nozzle may be at end of life.
    6. Verify dimensions. The listing shows .375 orifice and 2.640 length. Confirm those against your torch data before ordering in quantity.

    If you see repeated burnback, erratic gas coverage, or constant spatter accumulation, the nozzle may be part of a larger front-end issue. Check the contact tip condition, diffuser, liner condition, wire feed stability, and gas flow before blaming the nozzle alone.

    Troubleshooting support points

    Problem: Spatter builds up very quickly.
    Check for parameter imbalance, incorrect stickout, or a worn contact tip. Inspect the nozzle for arc strikes and confirm the gas flow path is not blocked. Verify the nozzle is the correct fit for the torch.

    Problem: Shielding gas seems uneven.
    Inspect the nozzle opening for deformation. Check that the nozzle seats fully and that the diffuser or internal mating parts are not damaged. Verify gas flow at the source and at the torch end.

    Problem: The nozzle will not slip on correctly.
    Inspect for damaged torch hardware, spatter on the mating surface, or dimensional mismatch. If the fit cannot be confirmed visually, mark the compatibility as Unknown (Verify) and compare against the torch parts diagram.

    Problem: Weld access is tight near the joint.
    The tapered profile may help access, but do not assume clearance is adequate. Verify the nozzle length and outside profile against the work envelope before use.

    Product and parts notes

    The product referenced here is the Profax PX176243 Nozzle, Slip Type Tapered .375 Orif X 2.640, Pack of (1). The Amazon ASIN associated with this draft is B008BJKBHY. That is a part identifier only. It does not confirm every torch family, consumable stack, or process setup.

    If you are buying for a maintenance crib, verify the following before stocking:

    • torch model and front-end part family
    • nozzle attachment style
    • orifice size and overall length
    • existing diffuser and contact tip arrangement
    • clearance requirements at the workpiece

    If any of those points are not documented, treat the match as Unknown (Verify) until confirmed by the torch manual, parts drawing, or the vendor listing details you already use internally.

    Buying and stocking guidance

    For support teams, the value of a nozzle like this is in repeatable replacement. Stock parts only after you confirm the torch family and front-end geometry. Do not buy in quantity based on shape alone. A nozzle may look close and still fail to seat properly or disrupt gas coverage.

    When a nozzle starts showing heat damage or repeated spatter adherence, replace it instead of pushing cleaning intervals too far. Cleaning is part of maintenance, but it is not a fix for distortion, a damaged bore, or fit loss.

    Safety notes

    • Allow the torch to cool before handling consumables.
    • Wear gloves when removing a hot nozzle or cleaning spatter.
    • Verify the machine is in a safe state before inspection.
    • Do not force a nozzle onto a damaged or mismatched torch front end.
    • Use standard shop procedures for gas cylinder, wire feed, and power isolation during maintenance.

    FAQ

    Is this nozzle automatically compatible with every Profax or MIG torch?
    No. The part name alone does not prove compatibility. Verify the torch model, attachment style, and front-end dimensions before installation.

    When should a nozzle be replaced instead of cleaned?
    Replace it when cleaning no longer restores a round bore, proper seating, or stable shielding gas coverage. Visible distortion is also a replacement trigger.

    Can I use the listed dimensions as a final fit check?
    Use them as reference only. The .375 orifice and 2.640 length are listing details. Final fit must be confirmed against the torch assembly and parts documentation.

    What if I cannot confirm the mating part number?
    Treat the match as Unknown (Verify). Check the torch manual, compare the front-end parts, and confirm before ordering large quantities.

    Sources Checked

    This draft is intended as a practical replacement-part reference. Final purchasing decisions should be based on verified torch documentation and shop fit checks.

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 16 is a solid MIG wire in .045 in. diameter on an 11 lb spool. The core value of this wire is straightforward: it is intended for mild-steel fabrication, maintenance, and repair where stable feeding and practical arc control matter more than marketing claims. The ER70S-2 classification is typically used for cleaner welds on steel with light mill scale or minor surface contamination, but it is not a substitute for proper joint prep. Always verify the base metal condition and welding procedure before use.

    Key Takeaways

    What This Wire Is For

    This product is positioned for general mild-steel MIG welding in fabrication and maintenance environments. The triple-deoxidized ER70S-2 chemistry is commonly used to tolerate light surface oxidation better than basic solid wires, but the practical result depends on current settings, gas coverage, and operator technique. Use it as a production filler wire when the weldment calls for solid wire MIG on steel and the setup is already aligned to .045 in wire.

    If you are comparing options for steel filler metal selection, a filler metal finder can help you narrow down the starting point. It does not replace the welding procedure or a code requirement. Use the WSP filler metal finder as a selection reference only, then verify the final match against the application requirements.

    Setup Checks Before You Load the Spool

    Check: Confirm the machine is configured for .045 in solid wire. Verify drive rolls, gun liner, and contact tip size are appropriate for the wire diameter. Unknown (Verify) if the existing setup was previously used for a different diameter.

    Inspect: Look at the spool wrap, wire surface, and feed path. Any kinks, corrosion, or contamination can cause feed irregularity and arc instability.

    Verify: Confirm shielding gas type and flow are correct for the procedure. The product details provided here do not state a gas requirement, so use Unknown (Verify) and follow the approved WPS or shop standard.

    Check: Make sure the polarity matches solid MIG wire requirements for your process. If polarity is not confirmed by procedure or machine label, treat it as Unknown (Verify).

    Inspect: Clean the work lead connection, gun neck, liner entrance, and drive rolls. Small restrictions in the feed path often show up as birdnesting or erratic burnback.

    Verify: Test feed on scrap before going to production. A short trial pass is faster than correcting a bad setup on the part.

    Troubleshooting and Support

    If the wire feeds poorly

    Check drive roll tension first. Too much pressure flattens the wire and increases drag; too little lets the rolls slip. Inspect the liner for wear, contamination, or incorrect size. Verify that the contact tip is not oversized or worn out. If the wire was stored in a humid area, inspect it for surface oxidation before loading.

    If the arc is unstable

    Inspect the contact tip, nozzle, and work clamp. Verify consistent stickout and travel speed. If the arc wanders after a spool change, confirm the wire is seated correctly in the feeder and that the gun cable is not sharply bent.

    If weld quality is inconsistent

    Check base-metal prep before changing machine settings. ER70S-2 can help with light contamination, but it cannot compensate for heavy rust, paint, oil, or poor joint alignment. Verify fit-up, cleaning method, and shielding coverage before assuming the wire is the problem.

    For surface prep support, the Weld Support Parts blog includes a wire-wheel and pen-brush article that can help with cleaning strategy: Rocaris 6 Pack Wire Wheel & Pen Brush Set: Carbon Steel for Weld Cleaning & Surface Prep. Use it as a cleaning reference, not a process approval.

    Product and Parts Notes

    The provided product is the only confirmed item for this article: TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1). The available listing information identifies it as an ER70S-2 solid MIG wire on an 11 lb spool. Any additional details about spool construction, manufacturing tolerance, or machine compatibility are Unknown (Verify) unless confirmed by the product page or your shop procedure.

    If you need to cross-check whether this wire belongs in a larger consumables strategy, use the WSP product resources and internal references already approved for your team. Do not assume that a similar-looking wire will share the same operating window.

    Safety Notes

    FAQ

    Is this wire only for mild steel?

    The confirmed product information identifies it as ER70S-2 solid MIG wire for mild-steel fabrication, maintenance, and repair. Use on other metals is Unknown (Verify) unless your procedure specifically approves it.

    Can I use this wire on rusty or dirty material?

    ER70S-2 is often selected when there is light mill scale or minor surface contamination, but heavy rust, oil, paint, or poor joint prep still need removal. Inspect the base metal and verify cleaning requirements first.

    What machine settings should I use?

    Unknown (Verify). Machine settings depend on the welding procedure, material thickness, transfer mode, shielding gas, and joint design. Start from the approved WPS or manufacturer guidance, then verify on scrap.

    Will an 11 lb spool fit my feeder?

    Unknown (Verify). Spool size and hub compatibility vary by machine and feeder design. Check the feeder documentation and compare it with the spool dimensions and adapter requirements before purchasing.

    Sources Checked

    Support note: If you are building a consumables list for steel MIG work, start with the approved procedure, then verify feeder setup, wire diameter, and base-metal condition. That sequence prevents most wire-related problems before they start.

    Related Arc Weld Part

    TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 16 is a .045 in (1.2 mm) ER70S-2 solid MIG wire on an 11 lb (5 kg) spool for mild-steel fabrication, maintenance, and repair, offering consistent feeding and a stable arc; the triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) supports clean welds when base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1) spool (set drive rolls/liner for .045 in…

    View at Arc Weld Store

    Related Weld Support Guides

  • Read with Kindle Unlimited