• CK T187GT2 2% Thoriated Tungsten Electrode 1/8″ X 7″, 10 pack: Application and Buying Checks

    CK T187GT2 2% Thoriated Tungsten Electrode 1/8" X 7", 10 pack

    If you are buying tungsten electrodes for TIG work, the CK T187GT2 2% Thoriated Tungsten Electrode 1/8" x 7", 10 pack is a straightforward consumable choice to evaluate against your current and material needs. The key is not just the alloy type. You also need to verify diameter, length, tip prep, contamination control, and whether the electrode style matches your procedure.

    This guide covers practical checks for application fit, receiving inspection, storage, and troubleshooting. It is written for welders, fabricators, maintenance buyers, and welding support teams that need a buying checklist, not a sales pitch.

    Key Takeaways

    • 2% thoriated tungsten is commonly selected for stable arc starting and high-current TIG work.
    • Use the electrode only after you verify the diameter, stickout practice, and tip geometry required by your procedure. Unknown (Verify) if not specified by your WPS.
    • Inspect each rod for straightness, surface damage, end contamination, and package integrity before issuing it to the welder.
    • Do not assume it is the right choice for every AC or DC application. Confirm procedure approval before use.
    • Handle thoriated tungsten with dust-control practices when grinding or reworking tips.

    Application Check: Where This Electrode Fits

    Based on the source summary, this electrode is intended for TIG work on carbon steel, stainless steel, nickel alloy, titanium, and copper. Treat that list as a source reference, not a blanket approval for every joint or procedure. The real question is whether your WPS or internal welding instruction supports a 2% thoriated tungsten for the job.

    Before issuing the pack, check the following:

    • Process: TIG only. Verify the procedure is gas tungsten arc welding, not another process.
    • Current demand: Confirm the amperage range needed for the joint. Unknown (Verify) if the job does not state current requirements.
    • Polarity and mode: Confirm whether the work is DC, AC, or both. Do not assume the same tip prep is acceptable in every mode.
    • Electrode diameter: 1/8 inch. Verify this matches the torch, holder, and current demand.
    • Length: 7 inch. Confirm the shop standard and whether the length clears your collet body and cup setup.

    Buying Checks Before You Order or Issue Stock

    For maintenance buyers and stores personnel, the right buying decision starts with fit and traceability. Use these checks:

    1. Confirm the electrode size on the job card. If the job does not specify 1/8 inch, verify with the weld lead before ordering.
    2. Check the package count. This product is listed as a 10 pack. Make sure that matches your consumption pattern and issue control.
    3. Verify storage conditions. Keep tungsten clean, dry, and separated from grinding debris.
    4. Confirm grinding controls. If you re-point tungsten in-house, verify you have a dedicated grinding wheel or disc and dust collection practices.
    5. Review safety controls for thoriated tungsten. Treat grinding dust as a control item. Use shop procedures for local exhaust, PPE, and cleanup.

    Inspection on Receipt

    When the shipment arrives, do not issue it directly into production. Inspect it first:

    • Package condition: Check for crushed corners, opened seals, or signs of moisture intrusion.
    • Count verification: Confirm the pack count is complete.
    • Straightness: Roll a sample rod on a flat surface to check for visible bend.
    • Surface condition: Look for scratches, chips, discoloration, or foreign contamination.
    • End condition: Inspect both ends. Unknown (Verify) if the rods are supplied pre-ground or blunt; do not assume tip prep.

    Troubleshooting: If Arc Starting or Weld Quality Is Poor

    When a tungsten electrode performs poorly, do not blame the rod immediately. Work through the system.

    1. Check the tip geometry

    If arc starting is inconsistent, inspect the point. A damaged or badly ground tip can cause wandering arc starts and poor arc focus. Verify the tip angle and finish against your procedure. Unknown (Verify) if the correct geometry is not documented.

    2. Inspect for contamination

    If the tungsten was dipped into the puddle or touched by filler metal, remove and regrind it. Contaminated tungsten can cause erratic arc behavior, soot, and unstable starts.

    3. Verify shielding gas delivery

    Do not assume the tungsten is the cause if the shield is poor. Check gas flow, cup size, gas lens condition, leaks, and torch assembly fit. Poor shielding can look like a tungsten problem.

    4. Confirm current and polarity

    If the electrode overheats, erodes quickly, or balls unexpectedly, verify amperage, polarity, and duty cycle. Unknown (Verify) if the machine settings were changed from the approved procedure.

    5. Review fit-up and joint cleanliness

    Oxide, oil, paint, and mill scale can destabilize the arc and make the electrode appear at fault. Clean the joint and retest before changing consumable type.

    WSP Lookup Reference

    Use the Weld Support Parts lookup page as a reference point for matching tungsten and related support items to the job. It is a starting point for selection, not a procedure approval.

    WSP lookup: TIG Welding Tungsten Electrodes 3/32″ (WT20 Red Tip) – Specs, Safety & Buying Guide

    Compare diameter, application notes, and tip handling practices against your own requirements before making a substitution decision.

    Filler Metal Finder Reference

    If you are pairing tungsten selection with filler selection, use the filler metal finder pages as a starting point only. They help narrow options, but they do not replace procedure review or weld-engineering approval.

    WSP reference: LaYZr Tungsten Electrode – Safer Precision for Low-Amp TIG Welding

    For filler selection, verify the base metal, joint design, service conditions, and procedure requirements before issuing any rod or wire.

    Safety Notes

    • Thoriated tungsten requires dust-control practices when grinding or re-pointing.
    • Use PPE suitable for grinding and welding tasks, including eye protection and respiratory controls required by your site procedure.
    • Keep grinding tools dedicated to tungsten work when possible to reduce cross-contamination.
    • Do not assume a damaged electrode is safe to reuse. Remove and inspect before relighting.
    • If your workplace restricts thoriated tungsten, follow site policy and regulatory guidance. Unknown (Verify) if site rules are not documented.

    FAQ

    Is 2% thoriated tungsten the right choice for every TIG job?

    No. It is a common choice for arc starting and higher-current TIG work, but you still need to confirm WPS approval, polarity, current range, and material compatibility for the job.

    Can I use this electrode for AC and DC work?

    Do not assume that. The source summary mentions low-amperage AC applications with a modified point, but your actual procedure must be checked first. Unknown (Verify) if AC use is not documented on the job.

    What should I inspect when the pack arrives?

    Check package integrity, count, straightness, surface damage, and contamination. If the rods are not clearly identified or appear damaged, quarantine the pack until it is verified.

    Why does my tungsten keep contaminating?

    Common causes include poor torch control, incorrect stickout, dirty base metal, bad shielding gas flow, or an incorrect tip geometry. Work through each variable before switching electrode type.

    Sources Checked

    • ArcWeld product summary for CK T187GT2 2% Thoriated Tungsten Electrode 1/8" x 7", 10 pack
    • Weld Support Parts internal reference: TIG Welding Tungsten Electrodes 3/32″ (WT20 Red Tip) – Specs, Safety & Buying Guide
    • Weld Support Parts internal reference: LaYZr Tungsten Electrode – Safer Precision for Low-Amp TIG Welding

    Related Arc Weld Part

    CK T187GT2 2% Thoriated Tungsten Electrode 1/8" X 7", 10 pack

    CK T187GT2 2% Thoriated Tungsten Electrode 1/8" X 7", 10 pack

    2% Throriated Tungsten offers good arc starting and is ideal for high current requirements. It is also good for low-amperage AC applications using a modified point. It is composed of 97.3% Tungsten, 1.7%-2.2% Thorium, and .5% other. Materials Welded- Carbon Steel, Stainless Steel, Nickel Alloy, Titanium, and Copper. Package of 10

    View at Arc Weld Store
    Related Weld Support Guides

  • The Notes in the Top Drawer: How Welding Shops Keep Knowledge From Walking Out

    There is a certain kind of shop drawer that does not appear on any inventory sheet. It sticks halfway open. Inside are a few shims, a dog-eared setup sketch, maybe a sample coupon with an arrow in soapstone. To a visitor, it looks like leftovers. To the crew, it may be the shortest route to getting a difficult repeat job right.

    That drawer is not a substitute for a drawing, a current procedure or an inspection plan. It holds something different: the memory of how the work actually behaves.

    Every welding shop has knowledge like that. It lives in the order a fixture gets tightened, the place a long assembly wants to pull, the sound that says a worn positioner needs attention, and the customer detail that never seems to make it onto the print. Much of it was earned through rework, long afternoons and the occasional part that taught a lesson the expensive way.

    The risk is obvious. People change shifts, change employers and retire. If the only copy of that knowledge is in one person’s head, the shop loses more than a pair of hands when that person leaves.

    The drawing is the beginning, not the whole conversation

    Welding is often described as a hands-on trade, but the hands are making decisions all day. The U.S. Department of Labor’s O*NET description of welding work includes reading drawings and specifications, aligning parts in fixtures, checking work for conformance, detecting defective equipment or material, and monitoring for distortion. Those responsibilities meet on the floor, where the information on paper has to survive heat, fit-up, handling and production pressure.

    A drawing can define the required result. A qualified procedure can define how a weld must be made. Neither one automatically tells a new crew member that the left stop on an old fixture has a few thousandths of wear, or that a particular assembly is easier to control when the clamps come off in a certain sequence. That is not permission to freelance around requirements. It is a reason to capture practical setup knowledge alongside the controlled documents that govern the job.

    The best shop notes respect that boundary. They do not say, “This is how Joe does it.” They say what was observed: which stop was used, where the first check was taken, what moved, what was adjusted and who approved the change. A useful note can be challenged, corrected and updated. A legend cannot.

    Good handoffs happen beside the work

    Knowledge transfer becomes awkward when it is treated as a farewell project. Someone who has spent 25 years solving problems is handed a blank form two weeks before leaving and asked to write down everything important. That usually produces either a mountain of detail or a page of general advice.

    The better moment is an ordinary repeat job.

    Pair the experienced hand with the person who will likely run it next. Start with the current drawing, procedure and inspection requirements. Then watch the setup. Ask simple questions while the physical evidence is still in front of both people: Why is that stop set there? Which dimension gets checked before the part comes out? What tends to move? What changed the last time the fixture was repaired?

    The newer worker should do more than take notes. Let that person run the next setup and explain it back. If the explanation falls apart, the gap is visible while there is still time to close it. A five-minute phone video of the fixture, a photograph of the clamp order, or a marked-up setup sheet can help—but only if it is stored where the next shift can find it and dated so no one mistakes an old workaround for current direction.

    This is not nostalgia for the way things used to be. It is how a shop makes experience available to people who were not present when the lesson was learned.

    Write down the exceptions, then fix what should not be exceptional

    Experienced welders often become human routing systems. A question comes up and everyone knows which person to ask. That is flattering until the person is absent and the job stops.

    One practical way to find vulnerable knowledge is to listen for the same questions:

    • Which fixture does this revision use?
    • Where is the known-good sample?
    • Who knows the customer-specific finish detail?
    • What do we check before welding the second side?
    • Why does this machine get set up differently?

    The answers do not all belong in the same place. Some require a drawing revision. Some belong in a controlled work instruction or maintenance ticket. Some are best captured as a clearly labeled fixture note. A few may reveal that the shop has been leaning on an unofficial workaround that needs engineering, quality or safety review.

    That sorting step matters. Documentation should remove ambiguity, not preserve it forever.

    Passing it down is skilled work too

    The need is not theoretical. The Bureau of Labor Statistics projects about 40,300 welding-related openings per year, on average, from 2025 through 2035. Most are expected to come from workers moving to other occupations or leaving the labor force, including retirement. Each opening is a hiring problem. It can also be a knowledge-transfer problem.

    The National Institute of Standards and Technology’s Manufacturing Extension Partnership emphasizes structured onboarding, technical training and consistent instruction as parts of workforce development. The principle fits the shop floor: repeatable teaching is not bureaucracy for its own sake. It gives the next person a fair starting point.

    There is respect in that. The experienced worker’s hard-won judgment becomes part of the shop instead of disappearing with a final timecard. The newer worker receives more than a list of motions; they get the reasons behind the sequence and enough context to notice when conditions have changed.

    And the shop gets something stronger than a single expert. It gets a crew that can carry the work together.

    So open the drawer. Keep the useful shim. Photograph the fixture. Move the approved lesson into the right document. Throw away the note that no longer applies. Then ask the question that tells you where to look next:

    What is one piece of shop knowledge your crew would lose if the most experienced person left tomorrow?

    Arc Life is built around the people, habits and small lessons that give the trade its character. Follow more stories from the welding life and bring your own shop perspective to the conversation.

    Sources

  • E6010 Stick / SMAW Filler Metal: Selection and Compatibility Checks

    E6010 Stick / SMAW Filler Metal

    E6010 is a cellulosic stick electrode commonly used for deep-penetration root passes and repair work on mild steel. It is often chosen when fit-up is imperfect, contamination is present, or a pipe root needs strong arc force and fast-freezing slag. That said, selection is not automatic. The correct choice depends on the WPS, base metal, service conditions, and the manufacturer data sheet. Treat the filler metal page as a starting point, then verify the application before ordering or striking an arc.

    Key Takeaways

    • E6010 is a starting point for carbon steel root passes and repair, not a universal approval for every joint.
    • Confirm polarity, required electrode diameter, and procedure limits on the WPS before use.
    • Check the base metal grade and thickness, then verify whether E6010 is acceptable for the job.
    • Moisture, storage condition, and rod damage can affect arc starts and weld quality.
    • If the job is code work, do not rely on a catalog description alone; verify with the governing procedure and manufacturer data.

    What to verify before selecting E6010

    Start with the job requirements, not the rod label. E6010 is identified on the Weld Support Parts filler metal page as a Stick / SMAW electrode under AWS A5.1 for mild steel, root passes, pipe, and repair work. Use that only as a selection reference. Then check the following:

    1. WPS or job traveler: Verify that E6010 is listed or allowed for the joint, position, and service.
    2. Base metal: Confirm the actual material grade, not just the general description of “steel.” If the grade is unknown, mark it as Unknown (Verify) until the paperwork or mill test report confirms it.
    3. Joint type: Root pass, open root, and repair work are common use cases, but the joint design still governs whether the rod is appropriate.
    4. Polarity and power source: Verify the required polarity on the WPS and the machine setup. Do not assume DC+ or any other setting without checking.
    5. Environmental condition: Inspect for wind, moisture, paint, rust, oil, and scale. E6010 can tolerate more surface contamination than many low-hydrogen electrodes, but dirty steel is not a free pass.

    Compatibility checks that prevent rework

    Compatibility failures usually show up as poor starts, lack of fusion, porosity, or a root that does not tie in consistently. Use a simple check/inspect/verify sequence.

    Check

    • Check the electrode designation against the WPS.
    • Check the specified diameter against the joint opening and pipe size.
    • Check whether the work is carbon steel only or if another material system is involved. If the material is uncertain, stop and verify.
    • Check the storage tube or package for damage, moisture exposure, or mixed lots.

    Inspect

    • Inspect the rod coating for chips, cracks, or swelling.
    • Inspect the joint for rust, mill scale, paint, and moisture at the root area.
    • Inspect the grounding point and lead condition. A bad ground can look like an electrode problem.
    • Inspect fit-up and root gap. E6010 can help with root control, but it will not fix a poor joint design.

    Verify

    • Verify amperage range from the machine setup and the electrode data sheet. If the exact value is not available, mark it as Unknown (Verify).
    • Verify that the job allows cellulosic electrodes for the intended pass and position.
    • Verify dry storage and handling requirements with the manufacturer data sheet before use.
    • Verify any code or customer restriction on cellulosic electrodes, especially for critical service.

    Troubleshooting support: if E6010 is not running right

    If the rod sticks, spatter is excessive, or the puddle is unstable, do not assume the electrode is defective. Work through the basic support checks first. For additional help on related start-up issues, see Stick Electrode Sticking During Arc Start: Amperage, Arc Length, Rod Condition, Polarity, Ground, and Hot Start Checks and Stick Welding Porosity Troubleshooting: Pinholes, Wormholes, Moisture, Arc Length, and Electrode Checks.

    • Sticking at arc start: Check amperage, rod condition, polarity, and ground first. Then verify whether the rod size matches the amperage range and joint access.
    • Porosity or pinholes: Inspect for moisture, oil, paint, and excessive arc length. Verify that the work area is protected from wind if applicable.
    • Poor tie-in at the root: Check travel speed, arc length, and fit-up. Verify whether the root opening is consistent along the joint.
    • Excessive spatter or harsh arc: Confirm the power setting, lead connections, and electrode diameter. If the setup is correct but the arc is still erratic, verify the rod lot and storage condition.

    Filler metal finder: use it as a selection starting point

    The Weld Support Parts filler metal finder can help narrow the search, but it does not replace the WPS or the manufacturer data sheet. Use it to confirm whether a Stick / SMAW option such as E6010 fits the general job description, then validate the final selection against the actual weld requirements. Access the finder here: Filler Metal Finder.

    The linked filler metal page for E6010 identifies the category, process, and general base material use. That is useful for sorting candidates, but it is not a procedure approval. If the job involves pressure piping, repair to in-service equipment, or a code-controlled application, the final decision still belongs to the governing procedure and responsible welding authority.

    Safety notes

    • Wear the correct PPE for arc welding, including eye, face, hand, and body protection.
    • Do not weld on unknown base metal without verification of the material and service requirements.
    • Keep the work area dry and controlled. Moisture and poor ventilation increase risk and can affect weld quality.
    • Follow lockout/tagout and hot work controls when working on maintenance repairs or equipment.
    • If you are unsure about polarity, process limits, or application suitability, stop and verify before welding.

    FAQ

    Is E6010 always acceptable for root passes?
    No. It is commonly used for root passes, but acceptability depends on the WPS, code requirements, base metal, position, and service conditions. Verify before use.

    Can E6010 be used on rusty or dirty steel?
    It is often selected when surface contamination is present, but the joint still needs proper cleaning and inspection. Rust, oil, and moisture can still cause defects.

    What polarity should I use with E6010?
    Use the polarity specified by the WPS and the electrode data sheet. If the documentation is not available, the correct setting is Unknown (Verify) until confirmed.

    How do I know if the rod size is correct?
    Check the WPS, joint fit-up, and amperage range. The correct diameter depends on access, thickness, and procedure limits, not just operator preference.

    Sources Checked

    For this draft, use the WPS, job specifications, and manufacturer data sheet as the final authority on fit, polarity, storage, and acceptance limits.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

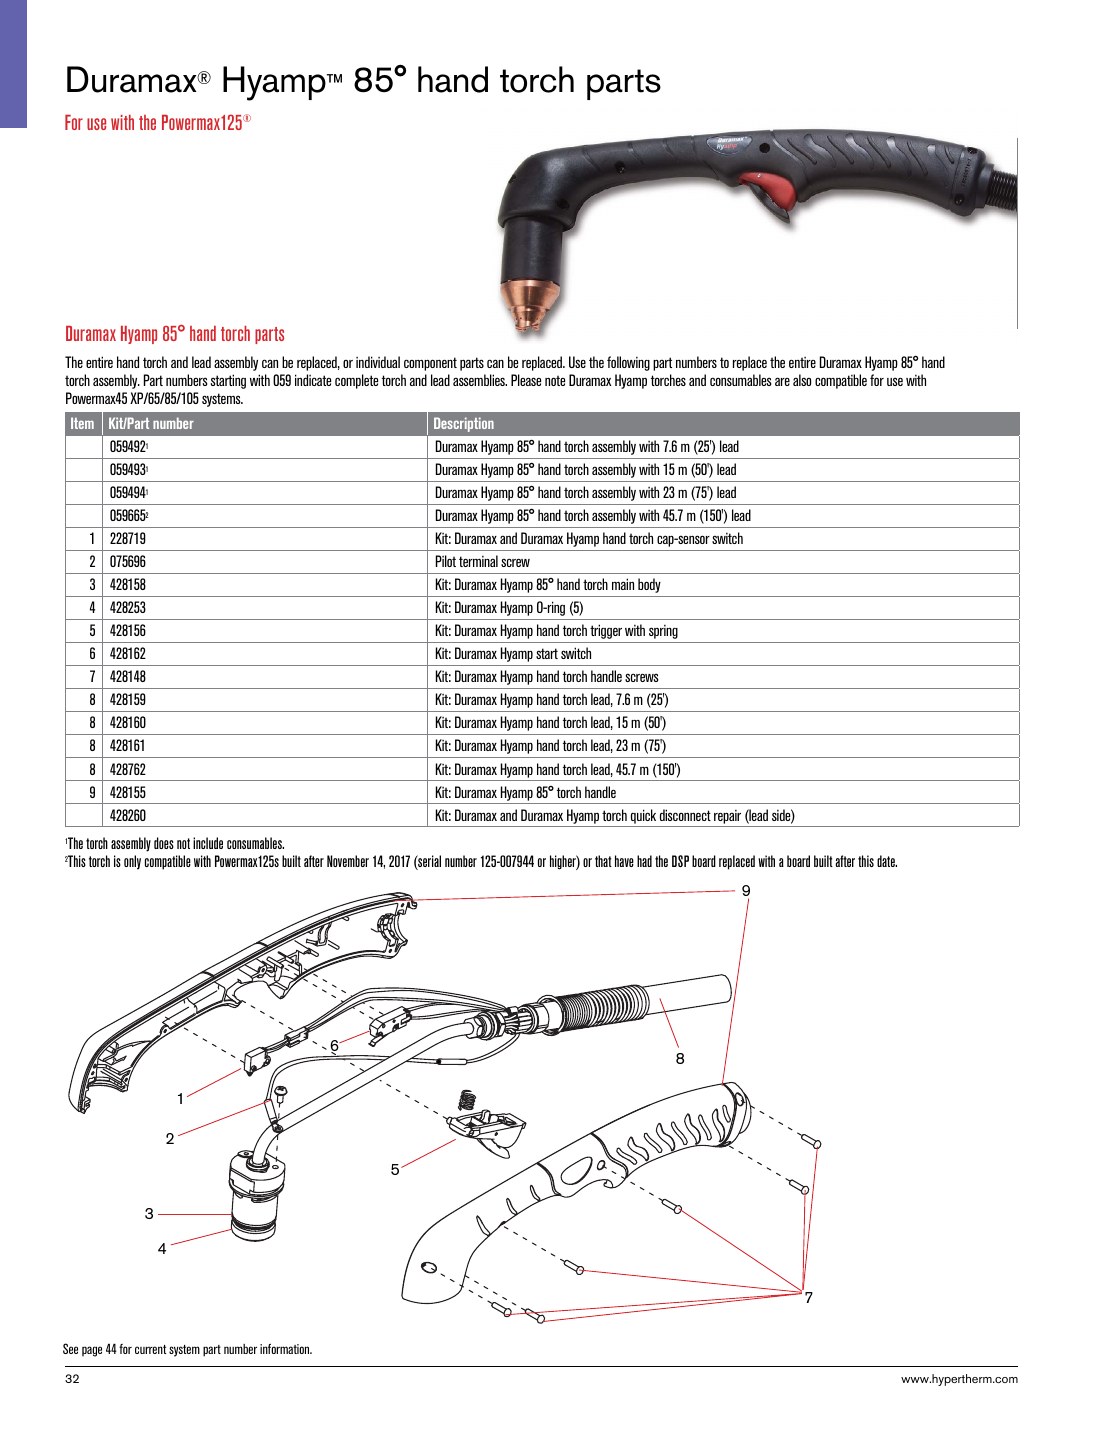
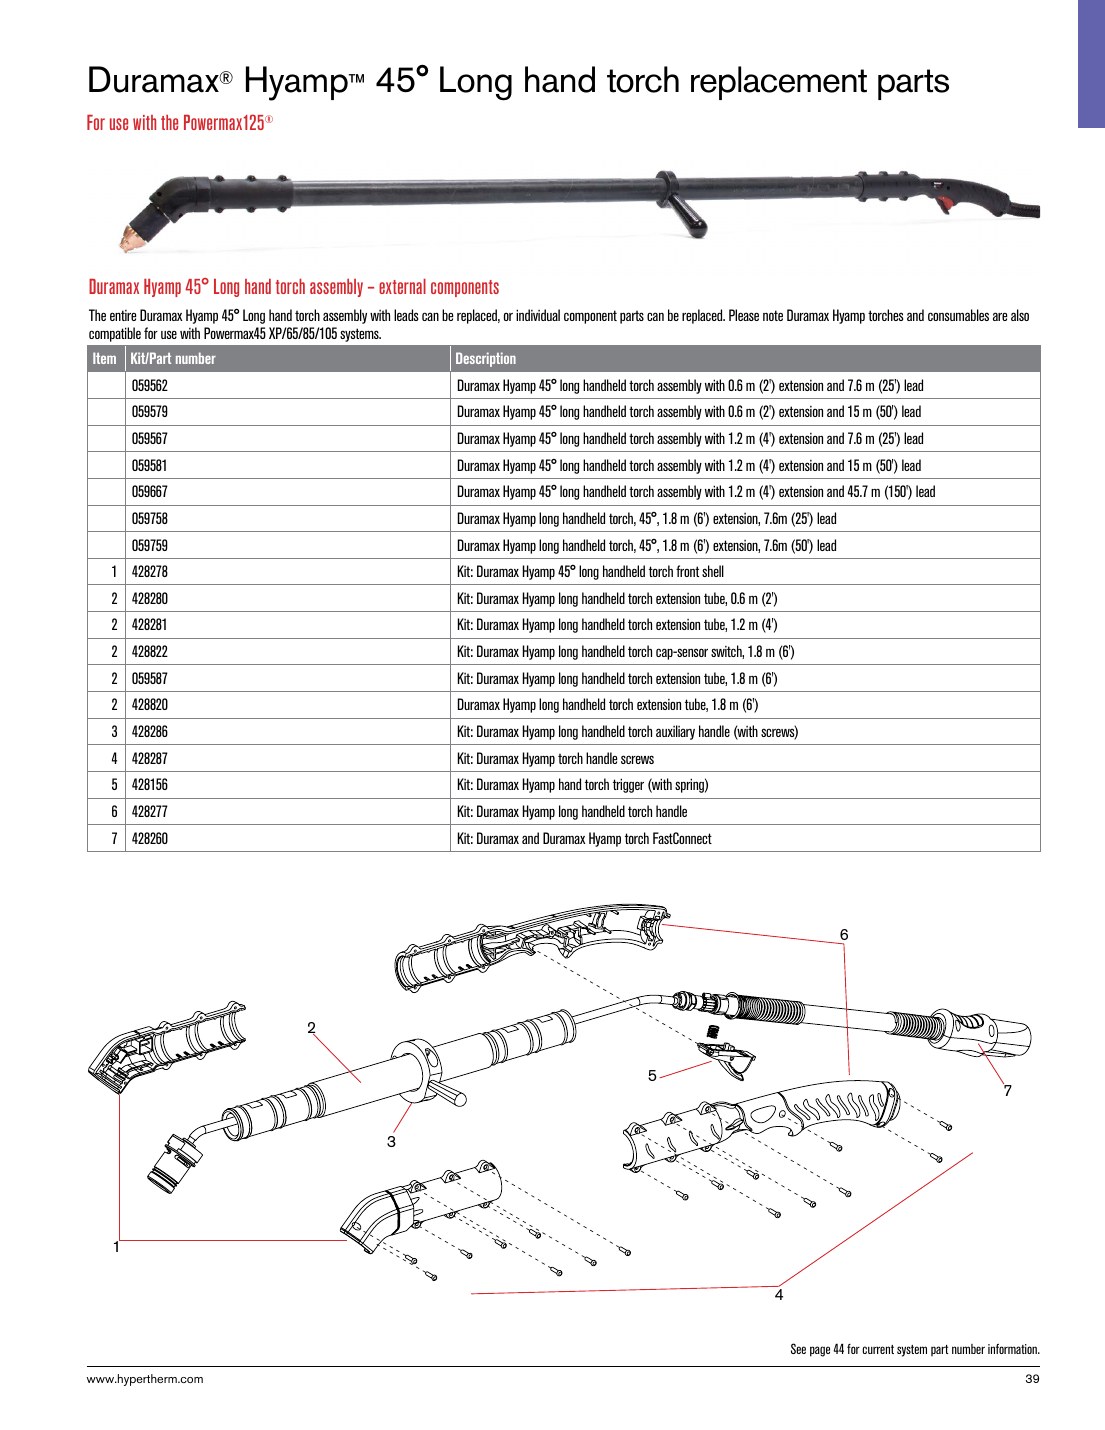
  • Hypertherm Duramax Hyamp Long Hand Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Duramax Hyamp Long Hand Torch Parts Breakdown

    When a Hypertherm Duramax Hyamp long hand torch starts cutting poorly, the first question is usually whether the problem is a worn consumable, a torch-body issue, or a machine-side fault. The right replacement decision depends on inspection, not guesswork. This guide gives a practical breakdown approach for field use: check the visible wear points, verify the torch setup against the parts lookup, and confirm the fault before ordering parts.

    Key Takeaways

    • Start with the consumables before replacing torch-body parts.
    • Inspect, clean, and verify the torch parts path from power source to nozzle.
    • Use the Weld Support Parts lookup page as the source reference for this torch family: Hypertherm Duramax Hyamp Long Hand Torch Parts Breakdown.
    • If a fit, rating, or part number is not clearly confirmed, treat it as Unknown (Verify).
    • Do not replace parts only because of arc instability; verify air supply, torch condition, and machine fault indicators first.

    Replacement decision workflow

    For a torch that is cutting poorly, follow this sequence before ordering anything:

    1. Check the consumables. Remove the torch parts and inspect for heat damage, erosion, ovalized or enlarged openings, cracked ceramics, or heavy spatter build-up.
    2. Inspect the torch body. Look for burn marks, damaged threads, loose retaining parts, cut insulation, or evidence of overheating near the head.
    3. Verify the fit. Match the torch model and consumable family to the parts breakdown page before selecting a replacement.
    4. Confirm the machine condition. If the torch fault repeats with fresh consumables, check air quality, power source output, and torch lead damage.
    5. Document the failure pattern. Note whether the issue is no-start, intermittent arc, rapid nozzle wear, excessive dross, or unstable arc transfer.

    What to inspect first

    Check the nozzle. A worn nozzle usually shows enlarged or distorted orifice shape, heat discoloration, and poor arc focus. If the nozzle has visible damage, replace it as a set with the matching consumables required by the system.

    Inspect the electrode. Look for deep crater wear, severe pitting, or an end-of-life condition that exceeds normal use. If the electrode is heavily worn, do not assume the shield or swirl ring is still serviceable.

    Inspect the shield and swirl ring area. Debris, spatter, or carbon tracking can affect arc initiation and cut quality. Clean only with methods appropriate for plasma parts; do not scrape precision surfaces aggressively.

    Verify torch assembly condition. If the retaining parts do not tighten correctly or the torch head shows heat damage, the issue may be beyond consumables. That is a torch-body replacement decision, not just a parts swap.

    How to verify before you buy

    Use this practical checklist:

    • Check model identification: confirm the torch is the Duramax Hyamp long hand torch, not another Hypertherm torch family.
    • Inspect the part path: confirm which item is worn by comparing the old part to the breakdown reference.
    • Verify machine context: make sure the torch is being used on the intended plasma system. If the machine context is unclear, mark it Unknown (Verify).
    • Inspect for system faults: repeated consumable failure can point to air contamination, incorrect installation, or lead damage.
    • Document the result: keep a simple note of which part failed and after how many starts or cutting hours.

    WSP lookup section

    The Weld Support Parts lookup page for this torch family is the starting point for catalog-backed identification and replacement decisions: Hypertherm Duramax Hyamp Long Hand Torch Parts Breakdown.

    Use that page to confirm the torch family, compare the visible parts against the breakdown, and narrow the replacement list. If a part number or subassembly is not clearly confirmed from the available record, do not assume it matches. Use Unknown (Verify) until the fit is confirmed by the manufacturer or an authorized source.

    Common support issues and what they usually mean

    No start: Check the consumables first, then verify torch lead connections, work lead condition, and machine-side error codes if available.

    Weak spark or arc dropout: Inspect the electrode and nozzle wear, then verify correct assembly order and clean contact surfaces.

    Poor cut edge quality: Check for nozzle wear, swirl ring contamination, incorrect standoff, or an air quality problem.

    Frequent consumable failure: Verify whether the torch is being run within the intended setup. Repeated failure can indicate a torch-body fault, not just normal wear.

    Safety notes

    • De-energize the machine before opening the torch or removing consumables.
    • Allow hot parts to cool before handling.
    • Do not touch plasma parts with bare hands if contamination control is required for your process.
    • Replace damaged torch parts immediately; do not keep using parts with visible heat damage or cracked insulation.
    • If the failure involves overheating, burning, or repeated arc instability, stop and inspect the full torch circuit before resuming work.

    FAQ

    How do I know whether to replace a consumable or the whole torch?
    Start with the consumables. If the failure repeats after a correct consumable replacement and the torch body shows heat damage, loose threads, or insulation damage, the torch itself may need service or replacement.

    Can I identify the correct part by visual inspection alone?
    Visual inspection is the first step, but not enough by itself. Verify the torch family and the part path against the lookup page before ordering.

    What if the torch cuts poorly even with new parts?
    Check air supply quality, torch lead condition, installation order, and machine-side faults. Poor cut quality is not always a consumable problem.

    Is the lookup page enough to approve a replacement?
    It is a starting point for identification and comparison. If compatibility or fit is not clearly confirmed, treat it as Unknown (Verify) and confirm with the manufacturer or an authorized source.

    Sources Checked

    Use the lookup page, inspect the worn parts, and verify the torch setup before ordering replacements. That approach reduces wrong-part buys and helps isolate whether the fault is in the consumables, the torch body, or the machine.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8″ X 7″, 10 Pack: Application and Buying Checks

    CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack

    CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack is a standard TIG support item for shops that need a larger-diameter tungsten for stable arc starts and controlled current delivery. The practical value of this size is simple: 1/8 in. tungsten is commonly considered when the job calls for more current capacity than smaller electrodes can handle cleanly. That said, tungsten selection is always a setup check, not a guess. Verify torch size, collet compatibility, amperage range, joint access, and the current process before you buy or install.

    Key Takeaways

    • 1/8 in. x 7 in. lanthanated tungsten is typically used in TIG setups that need a larger electrode size.
    • Lanthanated tungsten is a common general-purpose option, but final suitability depends on the welding procedure and base material.
    • Do not assume a larger tungsten is automatically better. Check amperage, torch hardware, and access around the joint.
    • If your torch or collet body is not set up for 1/8 in. tungsten, verify the hardware before ordering.
    • Use the linked reference pages as starting points for selection, not as a substitute for your procedure or WPS.

    What this electrode size is used for

    A 1/8 in. tungsten electrode is chosen when the job requires a more robust tungsten than 3/32 in. or smaller options. In many fabrication and repair settings, this size supports steadier operation at higher amperage. The 7 in. length is a common torch length format, but torch setup must still be verified against your collet, gas lens, cup, and stickout practice. Unknown (Verify) if your shop uses a nonstandard torch body or specialty holder.

    Buying checks before you order

    Use the steps below before approving the purchase:

    1. Check tungsten diameter. Confirm the torch hardware accepts 1/8 in. (3.2 mm) electrodes. Do not rely on visual fit.
    2. Check electrode length. Confirm 7 in. length works with your storage, grinding station, and torch setup. Some setups can handle multiple lengths, others cannot.
    3. Check current demand. Compare the electrode size to the amperage range in your procedure. If the weld is low current, this size may be unnecessary.
    4. Check the torch consumables. Verify collet, collet body, back cap, and cup arrangement. Unknown (Verify) if your torch uses a special series or adapter.
    5. Check alloy choice. Lanthanated tungsten is often selected for general TIG work, but material and procedure requirements still control the final choice.

    Troubleshooting and support checks

    If your tungsten performance is poor after installation, use a methodical inspection instead of changing multiple variables at once.

    Check

    • Check that the electrode is straight and free of chipped ends.
    • Check that the grind is consistent and aligned with your intended arc start method.
    • Check that the tungsten is seated fully in the collet.
    • Check for contamination from touching filler metal, joint edges, or a dirty grind surface.

    Inspect

    • Inspect the cup, collet body, and gas coverage for obstruction.
    • Inspect the electrode end after a short test start. Look for wandering arc, rapid balling, or excessive discoloration.
    • Inspect torch stickout. Excessive stickout may reduce shielding and arc stability.

    Verify

    • Verify the base material, filler choice, shielding gas, and current settings against your procedure.
    • Verify that the torch setup matches the electrode diameter. If it does not, correct the hardware before continuing.
    • Verify whether your weld schedule calls for a different tungsten type, diameter, or tip preparation.

    WSP lookup section

    For related support content and search functions, use the Weld Support Parts site resources as a starting point:

    Weld Support Parts

    Use this site to confirm related support items and internal references. It does not replace your welding procedure or manufacturer guidance.

    Filler metal finder section

    If you are matching tungsten selection to a filler strategy, start with the filler metal reference page here:

    Filler Metal Finder

    This page should be treated as a selection starting point. It is not a guaranteed approval for any specific base material, joint type, or code job. Verify final compatibility against the procedure, job requirements, and supervision rules for the work.

    Safety notes

    • Use gloves and eye protection when handling ground tungsten and sharpened ends.
    • Do not grind tungsten on contaminated wheels or surfaces used for other metals.
    • Control dust from grinding and keep the area clean.
    • Keep the electrode away from oils, dirt, and shop debris before use.
    • If the tungsten shows unusual behavior during welding, stop and inspect the torch and procedure before continuing.

    FAQ

    Is 1/8 in. tungsten too large for light TIG work?

    Often yes, but not always. For low-amperage work, a smaller electrode may be better. Verify the procedure and amperage before choosing this size.

    Does lanthanated tungsten work for every TIG job?

    No. Lanthanated tungsten is widely used, but final selection depends on material, polarity, current type, and shop procedure. Unknown (Verify) for any job-specific approval without a WPS or manufacturer reference.

    What should I confirm before putting this in stock?

    Confirm electrode diameter, length, torch consumable compatibility, and expected amperage range. Also confirm whether your team already standardizes on a different tungsten type for certain materials.

    Why does the grind matter?

    Tip preparation affects arc start and arc direction. Poor grinding can cause unstable starts and wandering arc. Keep the grind clean and consistent.

    Sources Checked

    All uncertain fit and procedure details should be verified against the job specification, WPS, and manufacturer guidance.

    Related Arc Weld Part

    CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack

    CK T187GL 1.5% Lanthanated Tungsten Electrode 1/8" X 7", 10 Pack

    CK T187GL 1.5% Lanthanated Tungsten Electrodes are built for TIG welders who need dependable arc starts and stable arc control, especially at higher amperage where a larger diameter electrode makes sense. This 10-pack includes 1/8 in. (3.2 mm) electrodes in a 7 in. length for common torch setups in fabrication and repair work. Lanthanated tungsten is widely used as a versatile, general-purpose option for many TIG…

    View at Arc Weld Store

    Related Weld Support Guides

  • The Mudroom Shift: How Welders Leave the Shop at the Door

    The shop does not always end at the time clock. Sometimes it rides home in the truck: dust in the floor mat, a jacket behind the seat, the smell of hot steel still caught in the fabric. The last task of the day happens at a different threshold, where work boots meet the doormat and a welder decides what crosses into the house.

    That small routine rarely appears in a job description. It may be a hook in the garage, a separate laundry bag, a change of shoes at work or a pause at the back door. The details depend on the job, the employer’s controls and the hazards involved. The idea underneath them is steady: the shop has a place, and home deserves a boundary.

    For welding families, that boundary is both practical and personal. It protects clean space from dirty gear. It also marks the moment a shift stops asking for a worker’s full attention.

    Work has a way of traveling

    Metalwork leaves evidence. A cuff can catch grinding dust. Boot treads find every corner of a cab. A marker, tape measure or pair of gloves can migrate from the bench to the center console without anyone making a plan for it.

    Not every welding job presents the same exposure. OSHA’s welding, cutting and brazing chemical overview notes that the metals present depend on the material being worked, welding rods, fluxes and related factors; coatings and residues can change the picture, too. That is why the safety data sheet, the employer’s hazard assessment and the site’s procedures matter more than a universal shop-floor rule.

    The larger principle is well established. The National Institute for Occupational Safety and Health explains on its current take-home exposure page that workplace chemicals can travel on skin, hair, clothes and shoes and reach vehicles or living spaces. NIOSH’s first recommendation is to keep contaminants from leaving the workplace, using measures such as protective clothing, changing before departure and keeping dirty workwear separate from clean items.

    That guidance is not a reason to panic over every dusty knee. It is a reason to know what the work involves and treat the boundary deliberately. A home routine cannot replace ventilation, exposure control, training, laundering arrangements or other employer responsibilities. It is the last handoff, not the whole safety program.

    The entryway becomes a tiny piece of shop design

    Welders tend to notice systems that either work or create friction. A fixture is useful because it gives every part a home. A shadow board makes a missing tool obvious. The best mudroom routines follow the same logic.

    The dirty side and the clean side are easy to understand. There is a reliable place for boots, a place for outerwear and a place for whatever should go back to work. Clean clothes do not have to share a pile with the day’s gear. The arrangement is simple enough to follow after a long shift, not only on the day somebody reorganizes the garage.

    That last point matters. A complicated ritual will eventually lose to fatigue, groceries or a doorbell. A useful boundary depends less on a perfect-looking room than on good placement: the boot tray where a person naturally stops, the hook that can take the weight of a jacket, the container that closes, the clean change that is already in the truck or locker.

    Specific controls should come from the hazards and the workplace plan. NIOSH publishes separate, stricter instructions for workers dealing with lead, including guidance to leave contaminated tools, scrap and packaging at work and to keep work clothes apart from household laundry. Those details are for lead exposure, not a slogan to paste onto every welding job. The broader lesson is to avoid improvising once a known contaminant is involved.

    A boundary also helps the person inside the gear

    Workwear has a way of carrying identity. A broken-in jacket fits like a record of the jobs it survived. Boots reveal the floor conditions. A helmet can feel more personal than almost anything else in the truck.

    Taking those things off is not rejecting the trade. It is changing roles.

    At the shop, awareness reaches outward: the arc, the grinder, the forklift lane, the person entering the booth. At home, attention has somewhere else to go. The dog needs out. Dinner is getting cold. Somebody wants to explain what happened at school. A short, familiar transition helps the mind catch up with the body.

    Some people use the drive. Some sit in the truck for one quiet song. Some wash up, change shirts and become available the moment the work clothes come off. None of those habits proves toughness or balance. They simply acknowledge that a person can be proud of the job without asking the whole household to live on shop time.

    There is respect in that separation. The family does not get the leftover version of the welder by default. The welder does not have to perform the shift all evening. Home can be where the shoulders drop.

    The best routine belongs to the real household

    There is no prize for the most elaborate mudroom. A one-bedroom apartment, a farmhouse, a shared rental and a house with three children will not use the same setup. The right questions are more useful than a staged answer: What hazards are actually present? What does the employer provide? Where can gear be stored without mixing it into living space? What routine can the household sustain every day?

    If the answers are unclear, the employer’s safety professional, union representative or a qualified occupational-health resource is the place to start. The point is not to shift a workplace problem onto a worker’s washing machine. It is to make the line between work and home visible enough that nobody has to guess.

    So here is the community question: what is the one end-of-shift habit that tells your household—and your own head—that the shop is staying on the other side of the door?

    Arc Life follows the trade beyond the booth, into the ordinary rituals that make a working life sustainable. Find more welding culture and shop-built perspective at The Welder’s Life.

    Sources

  • Hypertherm Duramax Hyamp Hand Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Duramax Hyamp Hand Torch Parts Breakdown

    If you service plasma cutters in the field or on the shop floor, the Hypertherm Duramax Hyamp hand torch is a parts-and-wear-item system, not a single replace-all assembly. This guide gives you a practical way to identify the common replacement decision points, verify the torch condition before ordering, and use the Weld Support Parts lookup page as the catalog reference for the hand torch page tied to this model.

    Key Takeaways

    • Start with the torch body, electrode, shield, retaining components, and swirl-ring area when diagnosing arc-start or cut-quality issues.
    • Do not assume a worn consumable is the only fault. Check the torch leads, connector condition, and visible heat damage first.
    • Use the WSP lookup page as the source reference for the Duramax Hyamp hand torch page, then confirm the exact part numbers against your machine and torch setup before ordering.
    • If fit, torch family, or cut current context is uncertain, treat it as Unknown (Verify) until confirmed by the machine manual or manufacturer support.

    What this parts breakdown is for

    The Duramax Hyamp hand torch parts breakdown is useful when a torch still powers up but starts showing weak arc transfer, rough starts, excess spatter, or shortened consumable life. In plasma service, those symptoms can come from damaged consumables, poor assembly contact, contamination, or heat damage in the torch head. A parts breakdown helps you map the visible wear point to the replacement candidate instead of swapping parts blindly.

    Initial troubleshoot: check, inspect, verify

    Before you order anything, use a simple sequence. This reduces wrong-part replacement and avoids masking a torch or power-source problem.

    Check

    • Check whether the symptom is intermittent or constant.
    • Check for start-up failure, weak pilot arc, arc dropout, or poor cut face quality.
    • Check the torch body for scorch marks, melted insulation, cracked front-end parts, or loose retaining hardware.

    Inspect

    • Inspect the electrode for deep pit wear, crater damage, or abnormal erosion.
    • Inspect the nozzle/orifice for ovaling, spatter buildup, or edge damage.
    • Inspect the shield and retaining components for heat distortion or thread damage.
    • Inspect the swirl-ring or gas-distribution parts, if present in your setup, for cracking or contamination. Exact part relationship is Unknown (Verify) without the full manufacturer assembly data.
    • Inspect the lead, trigger area, and connector interface for cuts, looseness, or overheating.

    Verify

    • Verify the torch model designation matches the Duramax Hyamp hand torch page you are using.
    • Verify whether the issue is on the torch side or the power-source side by testing with known-good consumables, if available and approved by your maintenance process.
    • Verify that the installed consumables match the torch family and operating setup. Do not assume cross-compatibility.

    How to decide what to replace first

    In most shop cases, the electrode and nozzle are the first wear items to evaluate. If both show normal wear but the torch still misbehaves, move outward into the shield, retaining hardware, and torch body inspection. If the front-end parts continue to fail early, look for air quality problems, incorrect assembly torque, or a torch issue upstream of the consumables.

    Replace the front-end consumables when wear is obvious and the torch is otherwise intact. Replace the torch parts or assembly components when you find heat damage, thread damage, internal contamination, or repeated failure after a correct consumable change. If you cannot identify the failed element confidently, stop and verify with the catalog record and the machine documentation.

    WSP lookup reference

    Use the Weld Support Parts lookup page for the Hypertherm Duramax Hyamp hand torch here:

    Hypertherm Duramax Hyamp Hand Torch Parts Breakdown

    This page should be treated as the catalog-backed reference point for the torch family and its replacement decision path. It is a starting point for identification, not a substitute for confirming the exact torch configuration in service.

    Practical replacement workflow

    1. Power down the plasma system and isolate energy sources before touching torch components.
    2. Remove the consumables and lay them out in order so wear patterns can be compared.
    3. Document abnormal wear: pitting, blackening, arc damage, cracking, or melted plastic.
    4. Check the front of the torch for debris, gas-path blockage, or physical distortion.
    5. Compare the torch model and consumable family to the WSP lookup page.
    6. Replace the worn item first, then test on a known workpiece before escalating to larger parts.
    7. If failure repeats immediately, stop and verify air supply quality, trigger function, lead condition, and torch head integrity.

    Replacement signals that should not be ignored

    • Repeated misfires after a fresh consumable install.
    • Visible arc tracking, charring, or carbonization on the torch front end.
    • Loose fit or unusual movement in the retaining stack.
    • Consumables that wear much faster than expected compared with the job pattern. Exact life is Unknown (Verify) because duty cycle and setup vary.
    • Cut quality loss that does not improve after standard cleaning and reassembly.

    Filler metal page note

    No filler metal finder page is provided for this topic. For plasma torch support, keep the focus on torch-family identification, wear-item inspection, and verified replacement sourcing rather than weld filler selection.

    Safety notes

    • Lock out and de-energize the system before removing torch parts.
    • Allow hot parts to cool before inspection; plasma front-end components can retain heat longer than expected.
    • Do not reuse parts that show cracking, melting, or severe erosion.
    • Do not force threaded parts if they resist installation. Cross-threading can damage the torch head.
    • Use only parts verified for the torch family and application. If fit is uncertain, stop and verify.

    FAQ

    What usually wears out first on a Duramax Hyamp hand torch?

    In normal service, the front-end consumables are the first items to inspect. The electrode and nozzle are common wear points, but you should confirm the entire retaining stack and torch head condition before replacing only one part.

    Can I identify the replacement part by symptom alone?

    No. Symptoms narrow the search, but they do not prove the exact failed part. Use the check, inspect, verify sequence and compare the torch against the WSP lookup page before ordering.

    What if the torch still misfires after I replace the consumables?

    Then move upstream. Inspect air quality, connector condition, trigger circuit, lead damage, and the torch body for heat-related damage. If the cause remains unclear, treat the fit or internal configuration as Unknown (Verify) until confirmed.

    Is the WSP lookup page a substitute for the manufacturer manual?

    No. It is a catalog reference and ordering starting point. Safety-critical fit and procedure details still need manufacturer review or your internal maintenance standard.

    Sources Checked

    • Weld Support Parts: Hypertherm Duramax Hyamp Hand Torch Parts Breakdown
    • Internal reference: Plasma Consumable Compatibility: How to Verify Torch Parts Before Ordering
    • Internal reference: Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks

    Keep this page as a replacement decision aid, not a substitute for machine-specific documentation. When in doubt, verify the torch family, inspect the wear pattern, and confirm the part before purchase.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • ERCoCr-A TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCoCr-A TIG / GTAW Filler Metal

    ERCoCr-A TIG / GTAW filler metal is used for cobalt-chromium hardfacing overlays where wear resistance, heat resistance, and corrosion resistance matter. It is not a default filler choice. Before anyone loads rod into a torch, the job needs a verified WPS, base metal identification, service condition review, and confirmation that the filler classification matches the application.

    This draft is written for welders, fabricators, and maintenance buyers who need a practical selection check. Treat the filler page as a starting point, not final approval. If the job is safety-critical or code-controlled, the manufacturer data sheet and governing procedure remain the authority.

    Key Takeaways

    • ERCoCr-A is a hardfacing filler used on cobalt-chromium overlay work, not a universal repair rod.
    • Confirm the WPS, base material, and service environment before ordering or welding.
    • Do not assume compatibility from classification alone; verify the substrate and overlay requirements.
    • Check rod diameter, torch setup, and heat input control before striking an arc.
    • Use the manufacturer data sheet and procedure documents for final acceptance criteria.

    Selection Checks Before You Weld

    Start with the base metal and the service condition. Hardfacing overlays fail when the filler is selected for the wrong wear mode or the wrong substrate. ERCoCr-A may be appropriate for wear and elevated-temperature service, but you still need to verify whether the job requires a different cobalt alloy, a nickel-based alloy, or a different hardfacing family.

    Check: identify the part, its duty cycle, and the dominant damage mechanism. Is the issue abrasive wear, galling, impact, corrosion, heat checking, or a combination? If the wear mode is unknown, the selection is unknown (verify).

    Inspect: look at the condition of the parent metal. Confirm whether the surface is cracked, work hardened, contaminated, or previously repaired. Previous overlays can change dilution and cracking behavior. If the history is unclear, treat the compatibility as unknown (verify).

    Verify: compare the planned weld against the WPS and the manufacturer data sheet. The summary record for this filler indicates AWS A5.21 and ERCoCr-A classification, but process details, preheat, postweld practices, and any base metal limitations must be confirmed from the controlling documents.

    Compatibility Checks on the Job

    Compatibility is more than matching a filler name to a torch process. For TIG / GTAW hardfacing, the weldor needs a stable arc, clean surface preparation, and the correct rod diameter for the joint or overlay pass. The summary record lists 1/16 in, 3/32 in, and 1/8 in as common size references, but actual stock and fit for your job are unknown (verify).

    Check: confirm the torch, cup, gas coverage, and stickout plan before starting. Poor shielding can create surface contamination, rough bead shape, or black specks. If the arc behavior is unstable, stop and inspect the setup before adding more filler.

    Inspect: clean the work area thoroughly. Remove oil, paint, oxide, scale, and grinding residue. Hardfacing overlays are sensitive to contamination because defects can be buried under a sound-looking cap.

    Verify: run a small test bead on a noncritical area or coupon if the procedure allows it. Check wetting, bead profile, and dilution expectations against the WPS. If the overlay shape or arc response looks wrong, do not proceed on production parts until the cause is identified.

    Troubleshooting Support: If the Weld Does Not Look Right

    If the weld starts cracking early, shows rough bead edges, or seems to wash too deeply into the base metal, stop and review the procedure. With hardfacing rod, the root problem is often not the rod itself but heat input, contamination, or an incorrect base metal assumption.

    Check: confirm the polarity, shielding gas, and travel speed. If those settings are not documented, they are unknown (verify).

    Inspect: evaluate bead shape, tie-in, and any signs of excessive dilution. A hardfacing overlay that mixes too deeply with the substrate may not deliver the intended wear properties.

    Verify: re-check the substrate identification and service requirement. If the part is exposed to impact or cyclic thermal loading, the filler choice may need to change.

    For tungsten-related setup problems, see TIG Tungsten Contamination Troubleshooting: Black Specks, Arc Wander, Dirty Starts, and Re-Grind Checks. For cup selection and stickout checks that affect shielding quality, see Square Wave 205 TIG Cup Size Selection Guide: Standard Cup, Gas Lens, and Stickout Checks.

    WSP Filler Metal Finder Use

    The filler metal finder page is useful as a starting point when you need to compare process and classification families. Use it to narrow down candidate filler metals, then confirm the WPS and manufacturer data sheet before release to the floor. It is not a substitute for application engineering or code review.

    Check: use the finder to locate the process family and classification path that matches your job, then verify whether the part is a cobalt hardfacing overlay, a repair weld, or a build-up pass. Those are different decisions.

    Inspect: compare the job requirements against the summary information available on the filler page. If the base metal, service temperature, or wear mechanism does not match, do not assume fit.

    Verify: keep the controlling WPS and manufacturer documentation in the job packet. If there is a conflict between the summary page and the procedure, the procedure and manufacturer data control.

    Filler metal finder: https://www.weldsupportparts.com/filler-metal-finder.html

    Filler Metal Page Reference

    The ERCoCr-A TIG / GTAW filler metal page identifies the product family as cobalt-chromium hardfacing filler for wear, heat, and corrosion-resistant overlays. Use that information to start the review, not to close it. Confirm the actual rod size, packing, and technical limits directly with the manufacturer data sheet and the job procedure.

    Check: make sure the process is TIG / GTAW and the classification is ERCoCr-A before planning the job.

    Inspect: confirm whether the part requires a hardfacing overlay or a different repair approach. If the repair objective is unclear, stop and clarify it.

    Verify: review code requirements, if any, before welding. If code acceptance applies, the filler classification alone is not enough.

    Filler metal page: ERCoCr-A TIG / GTAW Filler Metal

    Safety Notes

    • Use local exhaust ventilation and approved PPE for TIG hardfacing work.
    • Assume grinding dust, oxide, and coatings may contain hazardous contaminants until verified otherwise.
    • Do not weld on unidentified parts without confirming the base metal and service history.
    • Follow shop procedures for hot work, shielding gas handling, and fume control.
    • If cracking, spatter-like contamination, or abnormal arc behavior appears, stop and inspect before continuing.

    FAQ

    Is ERCoCr-A the right filler for every wear problem?
    No. It is a hardfacing filler family, not a universal fix. Verify the wear mode, substrate, and service temperature before selecting it.

    Can I rely on the filler metal page alone for procedure approval?
    No. Use it as a selection starting point only. The WPS, governing code, and manufacturer data sheet control the final decision.

    What if the base metal is unknown?
    Treat the job as unknown (verify). Identify the part, confirm the substrate, and review whether the overlay is allowed on that material.

    What should I inspect first when the arc looks unstable?
    Check shielding, tungsten condition, cleanliness, and torch setup. Then verify gas coverage and stickout against the procedure.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • CK T187GC2, 2% Ceriated Tungsten Electrode 1/8″ x 7″ (10 Pack): Application and Buying Checks

    CK T187GC2, 2% Ceriated Tungsten Electrode 1/8" x 7" (10 Pack)

    CK T187GC2 2% Ceriated Tungsten Electrode 1/8″ x 7″ (10 Pack) is a TIG support item aimed at operators who need consistent arc starts and stable arc control. The key buying question is not whether ceriated tungsten is useful in general, but whether this diameter, length, and alloy family match the job, the torch setup, and the current range you actually run. For buyers, maintenance teams, and welders, the right check list prevents wasted consumables and setup time.

    Key Takeaways

    • 1/8 in. electrodes are typically selected for heavier TIG work than fine-detail low-amp work.
    • Ceriated tungsten is commonly used for dependable starts and stable arc behavior, especially on DC applications.
    • Buying checks should focus on diameter, length, alloy type, grind condition, and whether the torch setup can physically accept the electrode.
    • If a fit or process detail is not confirmed by the source record, mark it as Unknown (Verify) and check the manufacturer or internal process sheet.

    What this electrode is for

    The product record identifies a 2% ceriated tungsten electrode in a 1/8 in. x 7 in. format, packaged in a 10-pack. That makes it a practical stocking item for fabrication, repair, and maintenance work where repeatable setup matters. In general TIG practice, ceriated tungsten is chosen when the operator wants easy initiation and steady arc behavior. That does not replace process approval. It only means the alloy family is commonly used for those characteristics.

    For DC TIG, this type of tungsten is often considered before moving to other electrode families. For AC aluminum work, the correct tungsten choice depends on the process plan, machine, and procedure. If those details are not established in your shop standard, the safe response is Unknown (Verify).

    Buying checks before you order

    Use the following checks before placing this item in a cart or stocking it in a crib:

    • Check the diameter: Confirm that 1/8 in. is the size your torch, collet, and current range require.
    • Check the length: Confirm that 7 in. works with your torch body and electrode stickout preferences.
    • Check the alloy family: Verify that 2% ceriated tungsten is acceptable for the process and material set in your shop.
    • Check the application: Compare against your existing tungsten standard for DC TIG, repair work, or higher-amperage fabrication.
    • Check packaging count: Make sure a 10-pack matches your consumption rate and storage control.

    If any of those items are not in your purchasing standard, do not assume fit. Record them as Unknown (Verify) and route the question to the weld coordinator or process owner.

    Application notes for shop use

    For a tungsten electrode, performance depends on more than the alloy name. The grind geometry, tip condition, cleanliness, and the machine settings all affect arc starts and arc stability. A ceriated tungsten may start well, but a damaged tip, contamination, or incorrect prep will still cause instability.

    Use these practical checks during setup:

    1. Inspect the electrode: Look for cracks, chips, contamination, or uneven ends before use.
    2. Verify the grind: Check that the tip prep matches your procedure or the shop standard.
    3. Confirm cleanliness: Keep tungsten away from grease, steel dust, and filler contamination.
    4. Check torch fit: Confirm the electrode seats correctly in the collet and does not bind.
    5. Test on scrap: Run a short arc-start check on sample material before moving to production parts.

    If the arc is wandering, hard to start, or unstable, do not blame the tungsten first. Inspect the cup size, gas coverage, shield gas flow, tip prep, and work clamp contact before changing consumables.

    Troubleshooting support: check, inspect, verify

    Problem: Poor arc starts

    • Check whether the tungsten tip is blunt, contaminated, or ground incorrectly.
    • Inspect the torch consumables for wear or poor seating.
    • Verify the machine setup and start mode against the procedure.

    Problem: Wandering arc

    • Check the tungsten for uneven grind lines or tip damage.
    • Inspect gas coverage, cup condition, and torch alignment.
    • Verify that the workpiece is clean and the ground path is solid.

    Problem: Short electrode life

    • Check for contamination from contact with filler, base metal, or the puddle.
    • Inspect whether the current, polarity, or arc length is outside the intended setup.
    • Verify whether the selected tungsten size is appropriate for the amperage demand. If not confirmed, Unknown (Verify).

    WSP lookup section

    If your workflow includes part verification, use the Weld Support Parts lookup page as a starting point for internal confirmation: WSP lookup. Treat it as a reference path for checking item identity, not as a substitute for the welding procedure or the manufacturer’s review of critical fit.

    Filler metal finder section

    When selecting a tungsten support item, it can still help to review the filler metal decision path alongside the process setup. Use the Weld Support Parts filler metal finder as a starting point for selection review: filler metal finder. It should be treated as a guide to narrow choices, not as a blanket approval for procedure use.

    Safety notes

    • Do not handle hot tungsten immediately after welding.
    • Use eye protection when grinding or dressing tungsten.
    • Avoid dust exposure from grinding operations and keep the work area clean.
    • Do not use a contaminated tungsten in production without cleaning or replacement.
    • Follow your shop’s welding procedure, gas handling rules, and electrical safety practices.

    If a procedure, material, or torch compatibility point is safety-critical and not clearly confirmed, mark it Unknown (Verify) and escalate it before use.

    FAQ

    Is CK T187GC2 mainly for DC TIG?
    The source record indicates ceriated tungsten with dependable starts and stable arc control, especially on DC applications. Exact procedure approval remains Unknown (Verify).

    Can I use 1/8 in. tungsten for any TIG job?
    No. Diameter must match the current range, torch setup, and procedure. If your shop standard does not confirm the fit, treat it as Unknown (Verify).

    What should I check first if the arc is unstable?
    Inspect tungsten tip condition, torch consumables, gas coverage, and ground connection before replacing the electrode.

    Does a 10-pack change the technical use of the electrode?
    No. It changes stocking and handling only. The welding behavior still depends on diameter, alloy, prep, and setup.

    Sources Checked

    • ArcWeld product record for CK T187GC2, 2% Ceriated Tungsten Electrode 1/8″ x 7″ (10 Pack)
    • Weld Support Parts lookup page
    • Weld Support Parts filler metal finder page
    • Provided internal links on tungsten electrode selection and TIG tungsten buying guidance

    Related Arc Weld Part

    CK T187GC2, 2% Ceriated Tungsten Electrode 1/8" x 7" (10 Pack)

    CK T187GC2, 2% Ceriated Tungsten Electrode 1/8" x 7" (10 Pack)

    CK T187GC2 2% Ceriated Tungsten Electrodes are a solid choice for TIG welding when you want dependable arc starts and steady arc control, especially on DC applications. This 10-pack includes 1/8 in. (3.2 mm) electrodes in a 7 in. length—well-suited for higher-amperage work in fabrication, maintenance, and repair. Ceriated tungsten is commonly selected for its starting characteristics and stable arc performance; co…

    View at Arc Weld Store

    Related Weld Support Guides

  • Before the Hook Comes Tight: The Trust Between Welders and Riggers

    A fabricated frame can sit on stands for days while it is fitted, tacked, squared, welded and dressed. Then the hook arrives. The room changes.

    The easy conversation thins out. One person watches the pick points. Another watches the hook. Somebody checks the travel path again. A piece that felt like a workbench problem a minute ago is about to become a moving object with weight, balance and consequences.

    That moment belongs to more than one trade. The welder knows how the assembly was built. The rigger knows how it can be handled. The operator sees the machine and the path from a different seat. A good lift depends on all three views meeting before anything leaves the dunnage.

    This is one of the quieter partnerships in fabrication. It rarely gets photographed, and it is hard to reduce to a dramatic shower of sparks. Yet the trust between welders and riggers says a great deal about how serious shop work actually gets done.

    The handoff starts before the lift

    The rigger does not simply arrive at the end and attach hardware to whatever the shop has produced. The work begins with questions the fabrication crew can help answer: Where is the weight concentrated? Is the assembly complete? Are temporary braces still doing a job? Which surfaces can tolerate contact, and which have to arrive without a scar? Is there an obvious place to control the piece once it moves?

    Those questions are not a critique of the weld. They are the bridge between making an object and moving it.

    The U.S. Department of Labor’s current O*NET profile for riggers describes the occupation across construction sites, manufacturing plants, shipyards and other settings. Its core tasks include testing rigging, selecting gear for a load, attaching loads and directing workers during hoisting. The description makes the coordination plain: this is skilled work built around equipment, judgment and communication.

    The fabricator contributes a different kind of knowledge. A drawing may show the finished dimensions, but the person who built the piece remembers the heavy end, the open side, the temporary attachment and the corner that pulled during welding. That shop-floor memory can be useful during the lift discussion. It does not replace an approved plan or a qualified person’s decisions. It makes the conversation better.

    Clear signals beat shop-floor shorthand

    Fabrication has plenty of efficient shorthand. A glance across the table can mean hold that end. A tap on a square can mean check it again. That economy is useful when everyone can see the same work at arm’s length.

    A lift is different. The operator may not share the crew’s sightline. Noise can swallow a shouted word. A familiar gesture can look like something else from a distance. The safest crews do not treat clarity as an insult to experience; they treat it as part of experience.

    Federal rules for cranes and derricks in construction draw a firm line around that responsibility. OSHA’s signal-person qualification standard requires a signal person to understand the signals being used, apply them competently, grasp relevant equipment limitations and demonstrate that knowledge through testing. Those requirements apply to the construction-crane situations covered by the rule, not automatically to every hoist in every shop. Still, the cultural lesson travels well: one clear system is stronger than a circle of people giving improvised directions.

    There is another rule worth noticing. In that same construction-crane context, OSHA says anyone who becomes aware of a safety problem must give the stop or emergency-stop signal. The authority to stop is not reserved for the loudest voice or the longest résumé.

    That principle matters because trust is not the absence of questions. Trust is knowing a question will be heard before the next move.

    The best lift looks almost uneventful

    The most memorable shop stories usually involve a save: the person who caught a bad fit before the root pass, found the reversed detail on a print or heard a bearing change tone before it failed. Those stories deserve their place. But they can make competence sound like a string of last-second rescues.

    Good lifting work is often less theatrical. The piece rises a little and pauses. Balance is confirmed. The route is already clear. People know where they belong. The operator receives one readable direction. The load reaches its next support without becoming a story anyone has to retell at lunch.

    That calm result contains a lot of invisible labor. It reflects preparation, inspected equipment, an understood plan and people willing to say they do not like what they see. It also reflects restraint. A welder who knows the assembly well still respects the rigger’s role. A rigger who knows the lift still listens when the fabricator points out something unusual in the build.

    The relationship works because neither person has to pretend to know the other’s whole job.

    What the hook reveals about a shop

    You can learn something about a shop in the minute before a heavy piece moves.

    Does the crew slow down, or does production pressure make everyone rush the handoff? Are instructions coming from one understood source? Can a newer worker raise a concern without being brushed aside? Does the fabrication team think about handling while the piece is still being built, or only after the truck is waiting?

    These are culture questions disguised as logistics. A clean bead proves that somebody controlled an arc. A calm handoff proves that several people controlled themselves.

    The work also leaves a useful reminder for welders: the finished object will have a life beyond the table. It has to be turned, coated, loaded, installed, inspected, maintained or repaired. Thinking about the next pair of hands is not extra courtesy. It is part of making something that can move through the world.

    So here is the shop-floor question: what does a good welder do during a lift that makes the rigger’s job easier—and what do the best riggers do that earns a fabricator’s trust?

    Arc Life is here for the parts of the trade that live between the formal job descriptions: the habits, handoffs and people that make a shop run. Find more of that welding culture at The Welder’s Life.

    Sources

Listen with Audible