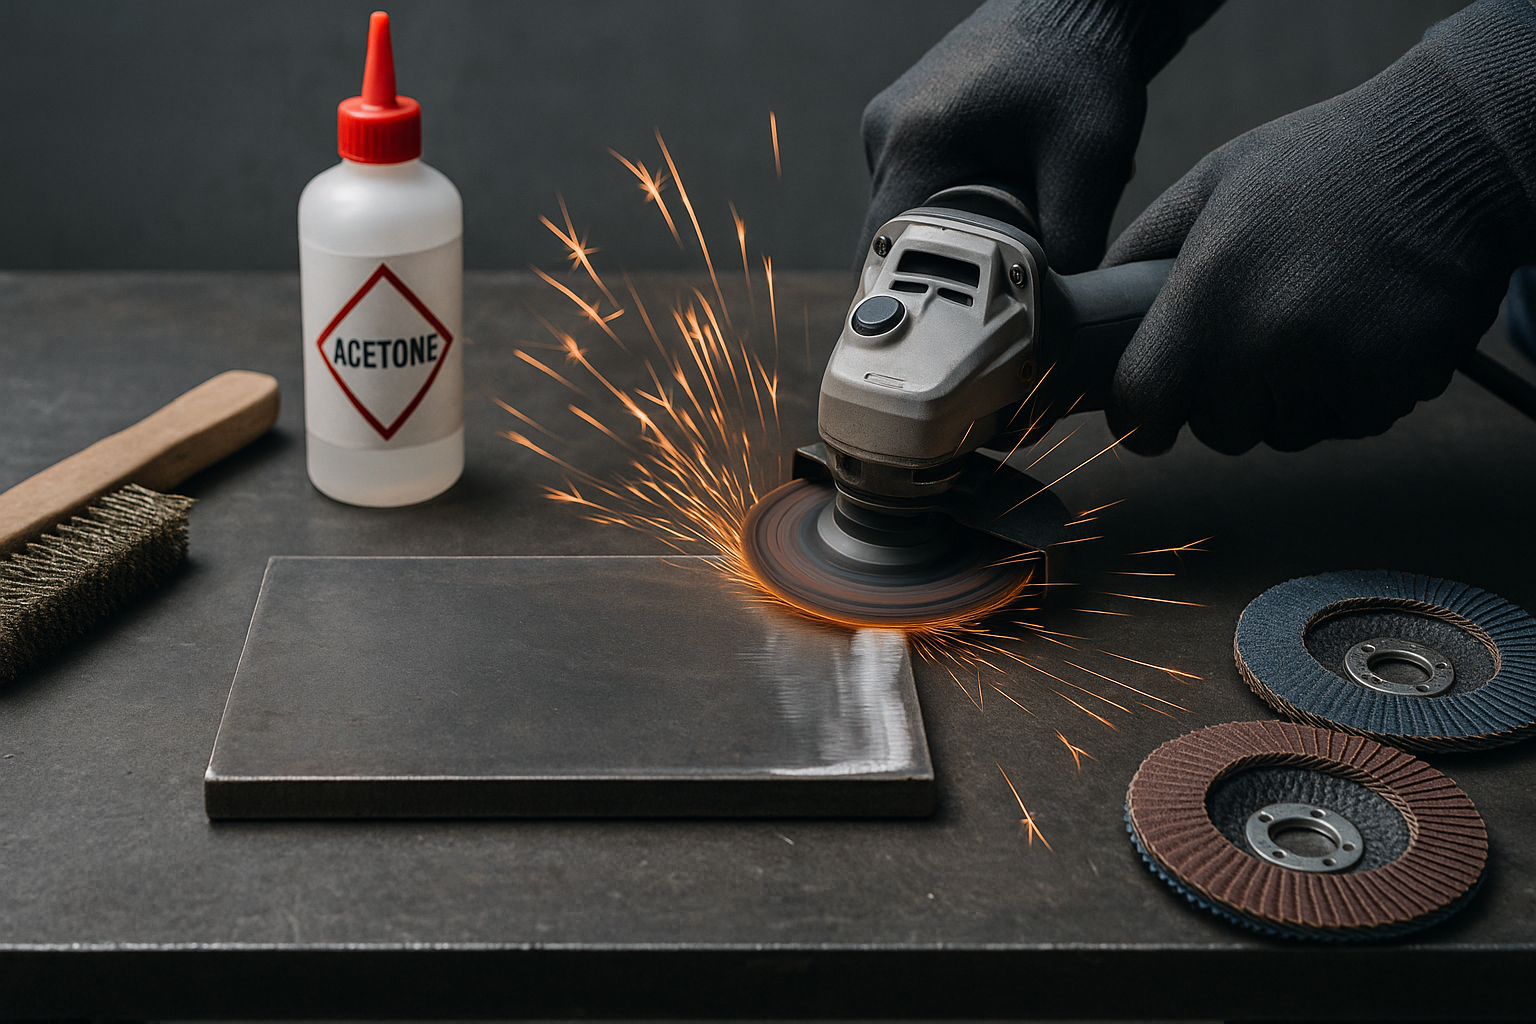
Proper metal prep is the difference between a clean, strong weld and fighting porosity, inclusions, and arc instability. This guide breaks down exactly how to clean, grind, degrease, and fit-up steel, stainless, and aluminum so you can weld with fewer defects and less rework.
Key Takeaways
- Clean metal = fewer porosity and arc-start issues. Remove mill scale, rust, paint, oil, and coatings.
- Use the right abrasives: flap discs for beveling, hard wheels for aggressive cleaning, and stainless-only tools for stainless.
- Fit-up accuracy determines distortion control and penetration.
- Always check safety: ANSI Z87.1 eye protection, proper ventilation, and PPE.
- Improper prep is one of the Top 3 causes of weld failure per AWS D1.1 commentary.
Where to Buy (Tools for Metal Prep)
Arc Weld Store:
40-grit flap discs — Heavy removal
80-grit flap discs — Finishing before weld
Amazon (options):
-
 CGW 42342 Flap Disc Z3-100% Zirconia, XL, 4 1/2″, 40 Grit, 7/8 Arbor, 13,300 RPM, T27 (10 Pack)
- CGW ABRASIVES
- 421-42342
- Flap Discs, Z3 -100% Zirconia, XL, 4 1/2″, 40 Grit, 7/8 Arbor, 13,300 rpm, T27
Last update on 2026-10-20 / Affiliate links / Images from Amazon Product Advertising API
-
 CGW Abrasives 42345 Abrasive Flap Disc 4-1/2″ x 7/8″ 80 Grit Zirconia – Pkg Qty 10, (Sold in packages of 10)
- 4.5″ x 7/8″ Arbor
- 80 Grit
- Pack of 10
Last update on 2026-10-20 / Affiliate links / Images from Amazon Product Advertising API
Affiliate Disclosure: As an Amazon Associate, we earn from qualifying purchases.
How to Prep Metal for Welding
1. Identify the Material
Different materials need different prep steps.
Carbon Steel
- Remove mill scale (blue/black surface).
- Grind out rust, paint, coatings, and galvanizing.
- Bevel edges for thicker plate (¼ in / 6 mm and up).
Stainless Steel
- Use stainless-dedicated wheels only (never shared with carbon steel).
- Remove heat tint and oxide layers.
- Clean surface oils with acetone before welding.
Aluminum
- Remove oxide layer mechanically (stainless brush).
- Degrease with acetone or alcohol.
- Wire-brush immediately before welding — oxide reforms in minutes.
2. Remove Coatings, Rust, and Mill Scale
Tools that work:
- Flap disc (40–60 grit)
- Hard grinding wheel
- Wire wheel (for light rust)
- Needle scaler (heavy rust or slag)
Remove down to bright, shiny metal. For carbon steel, AWS D1.1 recommends removing contaminants within 1 inch (25 mm) of the weld area.
3. Degrease and Clean
Oil, cutting fluid, and shop grime cause porosity.
- Use acetone or denatured alcohol.
- Avoid oily solvents like WD-40.
- Wipe until the rag stays clean.
Tip: Do solvent cleaning before grinding (to avoid driving oil into the pores) and again after to remove grinding dust.
4. Fix Edges, Bevels, and Gaps
Fit-up sets the stage for the entire weld.
- Bevel: 30–37.5° for structural steel (AWS standard).
- Root opening: 1/16–1/8 in. depending on joint.
- Remove burrs for full penetration.
- Tack weld at opposite ends to reduce movement.
5. Clean Again Before Welding
Right before striking an arc:
- Blow off dust
- Wipe with acetone (stainless + aluminum)
- Ensure the joint is dry — moisture = hydrogen
Safety Notes
- Wear ANSI Z87.1 eye protection and face shield when grinding.
- Use gloves, FR clothing, and hearing protection.
- Avoid grinding galvanized steel — zinc fumes require strong ventilation or removal + respirator (P100).
- Keep flammables away — grinding sparks can exceed 1,800°F.
- Ensure proper fume extraction for stainless to reduce hex-chrome exposure.
FAQ
Do I have to remove all mill scale?
For critical welds (per AWS D1.1), yes. For hobby MIG on light steel, partial removal can work, but expect spatter and inconsistent penetration.
Can I weld through paint?
Not recommended. Most paints give off toxic fumes and produce porosity.
How clean does aluminum need to be?
Extremely clean. Oxide melts at ~3,700°F; aluminum melts at ~1,200°F. That’s why aluminum requires brushing + solvent cleaning.
Why do my welds have porosity even after grinding?
Usually oil contamination or moisture. Try degreasing and pre-heating to ~150–200°F.
Sources Checked
- AWS D1.1 Structural Welding Code – Steel
- Miller, Lincoln, ESAB abrasive and prep guides
- ANSI Z87.1 PPE requirements
Leave a Reply