Search results for: “welding safety PPE”

  • Welding Safety Equipment Inspection Checklist for Shop PPE

    Routine PPE inspection helps reduce welding injuries, exposure incidents, arc flash risk, burns, respiratory hazards, and equipment-related downtime. This checklist is designed for fabrication shops, maintenance departments, welding booths, and industrial welding environments where daily PPE verification is required.

    The goal is simple: identify damaged, contaminated, expired, improperly fitted, or non-compliant protective equipment before welding starts.

    Key Takeaways

    • Inspect PPE before every shift and after high-exposure work.
    • Replace cracked lenses, damaged gloves, contaminated respirator filters, and heat-damaged clothing immediately.
    • Verify ANSI, OSHA, AWS, and manufacturer markings where applicable.
    • Do not assume PPE is safe because it “looks usable.”
    • Respirators, helmets, gloves, jackets, and hearing protection all have wear limits.
    • Fit, seal condition, and contamination matter as much as visible damage.

    Problem / Context

    Many welding PPE failures happen gradually. Helmet shells weaken from UV and heat exposure. Respirator seals harden. Gloves absorb oil and solvents. Auto-darkening lenses become unreliable. Grinding debris damages face shields and hearing protection.

    Without a structured inspection process, damaged PPE often stays in service longer than it should.

    Shops performing MIG, TIG, flux-core, stick, plasma cutting, carbon arc gouging, or grinding operations should maintain documented PPE inspection procedures and replacement criteria.

    Daily Welding PPE Inspection Checklist

    PPE ItemInspection CheckCommon Failure SignsAction Required
    Welding HelmetInspect shell, headgear, lens frame, sensors, and controlsCracks, loose headgear, failed auto-darkening response, damaged shellRemove from service if lens response fails or shell is damaged
    Auto-Darkening LensTest switching function before weldingFlickering, delayed darkening, inconsistent shadeReplace batteries, cover lenses, or filter cartridge
    Safety GlassesInspect lenses and side shieldsScratches, cracks, missing side shieldsReplace immediately
    Face ShieldCheck visor clarity and mountingClouding, deep scratches, loose pivotsReplace damaged visor
    RespiratorInspect seal, straps, valves, and filtersSeal deformation, cracked housing, clogged filtersReplace filters or respirator components
    PAPR SystemVerify airflow, battery condition, and filter statusLow airflow alarms, damaged hoses, weak batteryService before use
    Welding GlovesInspect palms, seams, cuffs, and insulationBurn-through, oil saturation, holes, stiff leatherReplace gloves
    Welding JacketInspect sleeves, snaps, and flame-resistant areasBurn holes, contamination, torn cuffsRepair or replace
    FR Sleeves / ApronsCheck stitching and heat damageLoose seams, spark damageReplace if compromised
    Hearing ProtectionInspect ear plugs or earmuffsDirty foam, cracked cushions, loose fitReplace disposable plugs regularly
    Welding BootsCheck soles, metatarsal guards, and lacesHeat damage, exposed toe caps, sole separationRemove from service if protection compromised
    Gas Hose PPE AreaVerify hoses do not contact clothing or hot surfacesBurn marks, abrasion, leaksReplace damaged hoses immediately

    Welding Helmet Inspection Procedure

    • Inspect helmet shell for cracks, warping, or heat damage.
    • Verify headgear tightens correctly and holds position.
    • Check cover lenses for pitting, scratches, and spatter damage.
    • Perform a safe function test on auto-darkening filters before welding.
    • Confirm shade settings match the welding process and amperage.
    • Inspect sensor areas for blockage from dirt or spatter.
    • Verify ANSI Z87.1 markings where applicable.

    Do not use a welding helmet with intermittent darkening performance, cracked filter housings, or damaged retaining frames.

    Respiratory Protection Inspection Steps

    • Inspect face seal for cracking, stiffness, or deformation.
    • Verify straps maintain proper tension.
    • Inspect inhalation and exhalation valves.
    • Check filter expiration and contamination level.
    • Confirm filters match the welding hazard.
    • Perform a seal check before entering the work area.
    • Verify airflow on powered air systems.
    • Inspect hoses and blower connections on PAPRs.

    P100 filters are commonly used for welding particulate, but gas, vapor, stainless steel, galvanized coatings, confined-space work, and chemical exposure may require additional verification.

    For workplace use, respirator selection and maintenance should follow OSHA 1910.134 requirements and the site respiratory protection program.

    Glove and Protective Clothing Inspection

    ItemWhat Usually Wears Out FirstVisual Wear IndicatorsField Fix vs Proper Fix
    MIG GlovesFinger seams and palm areaThin leather, burn-throughTape is not a safe repair — replace gloves
    TIG GlovesFinger sensitivity zonesHeat hardening, seam splitsReplace once dexterity drops
    FR JacketSleeves and front closureBurn holes, oil contaminationRepair minor stitching only if the FR rating is maintained
    Leather SleevesForearm exposure zonesHeat cracking and sparks embedded in leatherReplace if flexibility is lost
    Welding ApronsLower spark zonesBurn-through and torn strapsReplace heavily damaged aprons

    Common Wrong-PPE Mistakes

    • Using grinding face shields without safety glasses underneath.
    • Using expired or overloaded respirator filters.
    • Wearing oil-soaked gloves or jackets near sparks.
    • Using cracked auto-darkening lenses.
    • Ignoring damaged helmet headgear.
    • Using non-FR clothing around sparks or molten metal.
    • Wearing hearing protection incorrectly during grinding operations.
    • Failing to inspect PPE after plasma cutting or carbon arc gouging.

    Compatibility Notes

    Verify helmet lens size, respirator fitment, filter part number, cartridge compatibility, battery type, PAPR airflow rating, and headgear configuration before replacement.

    Compatibility may vary by helmet shell, respirator platform, welding process, and work environment.

    Unknown (Verify) for undocumented aftermarket compatibility claims.

    Related Failure Paths

    • Lens contamination is causing poor visibility and weld defects
    • Respirator seal failure increases fume exposure
    • Burn-through in gloves increases electrical and thermal injury risk
    • Helmet sensor blockage is causing flash exposure
    • Oil-contaminated clothing increases fire risk
    • Damaged hearing protection is contributing to long-term hearing loss
    • Improper boot condition increases slip and crush hazards

    Safety Notes

    • Follow ANSI Z49.1 for welding safety practices.
    • Use ANSI Z87.1-compliant eye and face protection where required.
    • Inspect PPE before every shift.
    • Replace damaged PPE immediately.
    • Maintain respirators according to OSHA respiratory protection requirements.
    • Do not modify PPE outside manufacturer guidance.
    • Do not use damaged FR clothing contaminated with oil or solvents.
    • Always maintain proper ventilation and fume extraction.

    FAQ

    How often should welding PPE be inspected?

    Basic inspection should occur before every shift. More detailed inspections should occur weekly or monthly depending on shop exposure conditions.

    When should respirator filters be replaced?

    Replace filters according to manufacturer schedules, site exposure requirements, or sooner if breathing resistance increases.

    Can cracked welding helmet shells be repaired?

    Generally no. Cracked helmet shells should be removed from service and replaced.

    Do safety glasses still matter under a welding helmet?

    Yes. Many shops require ANSI-rated safety glasses to be worn under welding helmets for additional impact protection.

    What is the most commonly ignored PPE issue in welding shops?

    Respirator fit and filter condition are commonly overlooked, especially in high-fume environments.

    Next Step

    Create a documented PPE inspection log for each welding station, grinding station, and fabrication area. Standardized inspection routines improve consistency, reduce missed hazards, and simplify safety audits.

    Internal Links

    Sources Checked

    • AWS ANSI Z49.1 Safety in Welding, Cutting, and Allied Processes
    • OSHA 1910.132 Personal Protective Equipment
    • OSHA 1910.134 Respiratory Protection
    • NIOSH respirator guidance
    • Manufacturer PPE inspection guidance
    • Weld Support Parts internal safety content
  • The Bead Is Not the Finish Line: The Craft After Welding

    The Bead Is Not the Finish Line: The Craft After Welding

    Series: Under the Hood

    The hood comes up, the arc goes quiet, and the weld gets its first honest look. In a lot of welding photographs, that is where the story ends.

    On the floor, it may only be the point where the next craft begins.

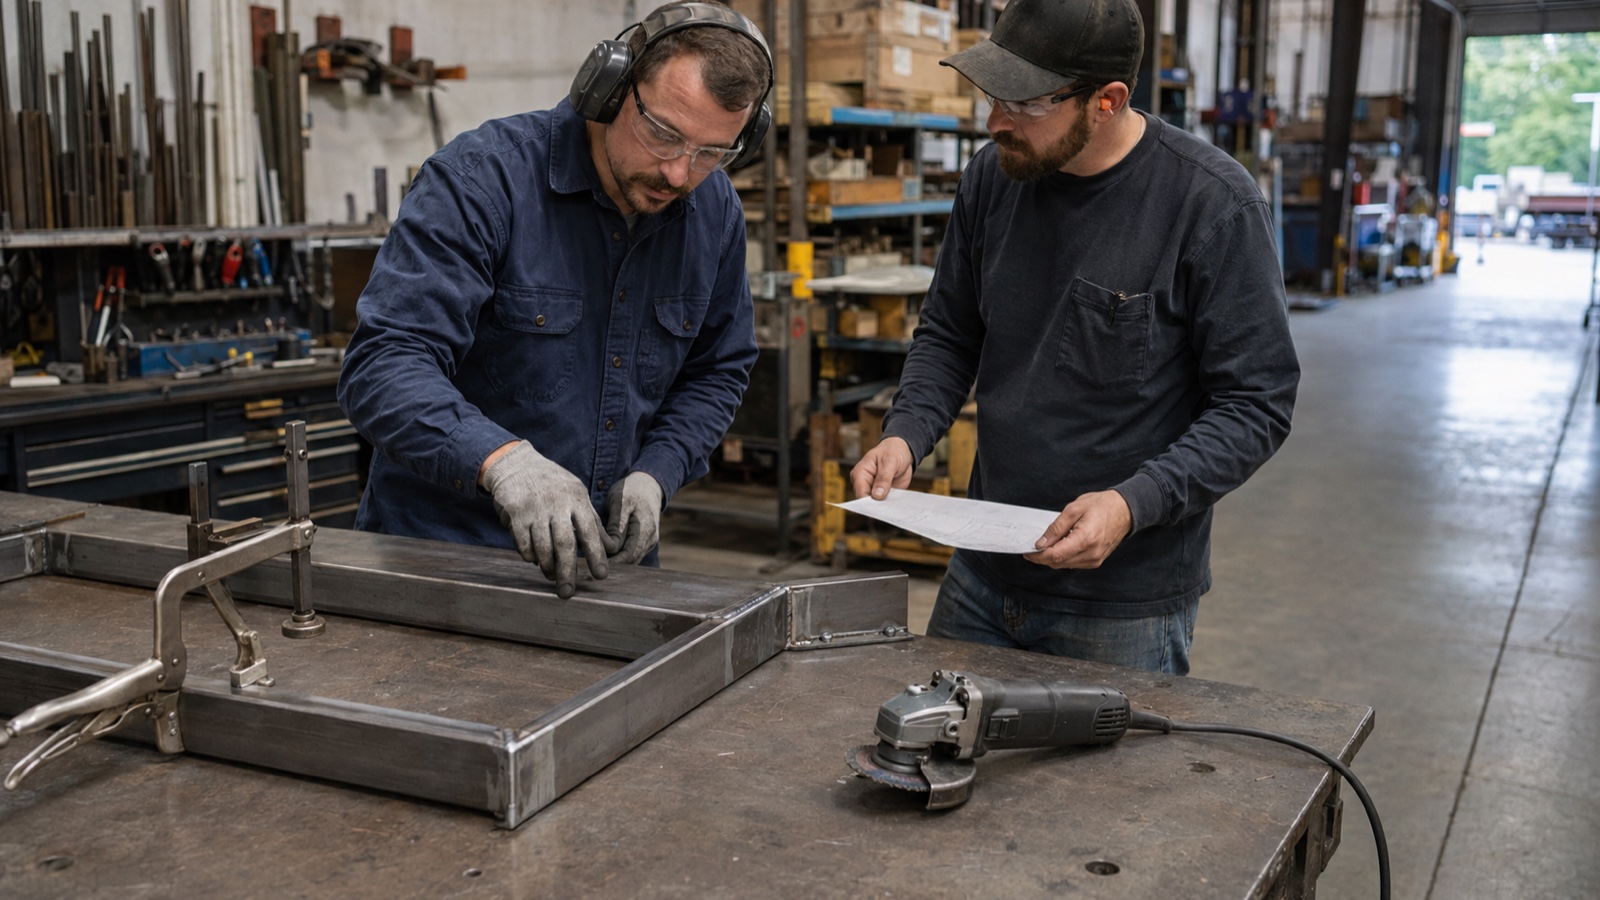
    A nearby grinder is waiting. So are a scraper, a file, a wire brush, a deburring tool or a finishing station farther down the line. The part may need spatter removed, an edge eased, a corner blended or a surface prepared for what happens next. Another job may call for the weld to remain exactly as deposited. The difference is not a matter of which finish photographs better. It belongs to the drawing, the service, the shop process and the people responsible for accepting the work.

    That is why finishing deserves more respect than the old joke gives it. The grinder is not simply an eraser for the welder. Used with judgment, it is one of the tools that carries fabricated work from “joined” to “ready.”

    The trade does not divide neatly at the last ripple

    Welding and finishing are often spoken about as separate steps, but the work overlaps in both directions. Edges may be ground so pieces fit before welding. Slag or spatter may be removed afterward. A surface may be cleaned before another operation can begin.

    The current O*NET profile for welders makes that overlap plain. Its core tasks include grinding, cutting, buffing or bending edges to help workpieces fit, as well as chipping or grinding excess weld, slag or spatter. The federal occupation profile is useful because it describes the job people actually recognize on the floor: measuring, fitting, welding, checking and finishing are connected pieces of fabrication, not isolated job titles living in separate rooms.

    The Bureau of Labor Statistics likewise describes welders as workers who read specifications, measure parts, inspect material, join or cut metal and maintain equipment. The arc is central, but it is surrounded by decisions before and after heat enters the part.

    In a small shop, one person may make every one of those decisions. In a production plant, a part may move from fitter to welder to finisher to inspector to coating. Either way, the finished object remembers the handoffs.

    A grinder is not an alibi

    Every shop knows some version of the line about a grinder and paint making a welder what they are not. It survives because everybody has seen grinding used to disguise hurried work.

    The joke misses the harder truth: good finishing is controlled work in its own right.

    Removing metal is a decision. So is leaving it alone. A person finishing a visible rail, a painted frame, a repaired machine component or a stainless counter may be aiming at very different conditions. The correct result cannot be guessed from personal taste. A polished transition may be right on one job and an unauthorized change on another.

    That puts restraint at the center of the craft. A strong finisher knows where the tool belongs, how the surface is changing and when the job has reached the required condition. They also know when the next move is not another pass, but a question for the lead, drawing, procedure or inspector.

    That last choice matters. Speed can hide uncertainty for a few minutes. Steel keeps the evidence much longer.

    The work is read through the hands

    Finishing has its own kind of attention. The sound changes as the tool crosses an edge. Resistance shifts when it leaves weld metal and reaches the surrounding surface. Reflected light makes a low spot or an uneven blend visible. A gloved hand can follow the shape after the tool is stopped and the part is safe to handle under the shop’s process.

    None of those signals replaces the job requirements or a proper inspection. They are the close-range feedback of a person learning how material responds.

    That learning is easy to underestimate because a finished surface can look simple. The best work often removes the signs of effort along with the sharp edges and tool marks. A customer sees a clean corner. The crew remembers the awkward access, the sequence that kept the frame square and the patient minutes that made the transition feel intentional.

    This is one reason experienced fabricators notice finishers. They understand how quickly an aggressive pass can create a new problem, how long a careless scratch can travel through polishing, and how much discipline it takes to make several surfaces look like one decision.

    Familiar tools still demand full respect

    Grinding is so common that it can disappear into the background noise of a shop. The hazards do not disappear with familiarity.

    A CDC/NIOSH abrasive-wheel safety checklist points shops toward required guards on portable grinders and eye protection for abrasive-wheel operators. It also calls for checking wheel fit and the machine’s spindle speed before use. The exact tool, abrasive, guarding, clothing and protection belong to the manufacturer’s instructions, the workplace hazard assessment and the applicable rules—not to a photograph or a habit carried over from a different job.

    There is a cultural point inside that safety language. Respect for finishing includes respect for the energy in the tool. A good crew does not treat removed guards, questionable abrasives, poor positioning or a shower of sparks aimed across a shared aisle as proof that somebody is tough. It treats the setup as part of the work.

    The best finish is a good handoff

    The welder helps the finisher by leaving honest work and clear information. The finisher helps inspection by knowing which condition must be seen before it changes. Inspection helps the next operation by settling the requirement instead of leaving the crew to argue from memory. Coating, assembly and installation all benefit when the surface arrives in the condition the job actually calls for.

    That chain is not glamorous, but it is where a shop builds trust. Nobody has to pretend that every weld should remain untouched. Nobody has to pretend that grinding can rescue any decision. The crew can treat finishing for what it is: a skilled step with limits, consequences and a visible effect on the final object.

    The bead may be the moment people photograph. The part still has somewhere to go.

    Shop question: What finishing job taught you the most about restraint—and what do new welders usually misunderstand about grinder work?

    Arc Life tells the stories around the arc: the people, habits and overlooked skills that make the trade whole. Visit Arc Life for more welding culture and shop-life stories.

    Sources

  • Lincoln Electric Welding Helmet Replacement Parts: What to Check Before Ordering

    Lincoln Electric Welding Helmet Replacement Parts: What to Check Before Ordering

    Lincoln PRO-Torch PTA-17 Support

    If you are searching for Lincoln Electric welding helmet replacement parts, the first step is not ordering. It is confirming what part you actually need, what helmet model you own, and whether the replacement is a direct fit or only a possible match. Helmet shells, lenses, headgear, inner covers, sweat bands, and gaskets can look similar across models, but small differences in mounting points, lens frames, or adjustment hardware can stop a part from working as expected.

    This article focuses on the checks that reduce returns, delays, and fitment mistakes. Use it as a pre-order checklist before you buy anything for a Lincoln helmet.

    Key Takeaways

    • Confirm the exact helmet model and part location before ordering.
    • Check the mounting style, dimensions, and wear pattern, not just the brand name.
    • Use the WSP lookup page as a support reference, not a substitute for model verification.
    • When details are unclear, mark them as Unknown (Verify) and inspect the helmet directly.
    • For welding procedure questions, use filler metal pages only as selection starting points, not automatic approval.

    Start with the helmet model, not the part name

    Many support calls begin with a description like “I need the inside cover for a Lincoln helmet.” That is not enough information. The same common part name can apply to multiple helmet families, but the attachment method may differ. Before ordering, inspect the label, model marking, or shell identification on the helmet itself.

    Check:

    • Helmet brand and model number
    • Any printed code on the shell, headgear, or lens frame
    • Whether the helmet is an auto-darkening model, passive lens model, or grinder-style support setup

    Inspect: The current part for distortion, cracked tabs, stretched elastic, stripped knobs, or heat damage.

    Verify: If the model marking is missing or unreadable, record it as Unknown (Verify) and compare the helmet against manufacturer documentation or a support reference before ordering.

    Check the failure point before replacing anything

    Not every worn helmet symptom means a full parts replacement. A loose headgear may only need an adjustment or strap replacement. A blurry view may point to scratched cover lenses instead of the filter cartridge. A helmet that feels unstable may have a worn pivot point, not a bad shell.

    Common checks:

    • Outer cover lens: Look for spatter pits, heat haze, scratches, and clouding.
    • Inner cover lens: Inspect for fingerprints, micro-scratches, and warp.
    • Headgear: Check strap elasticity, ratchet operation, pivot friction, and crown pad wear.
    • Gaskets and seals: Look for shrinkage, tearing, or sections that no longer sit flat.
    • Shade cartridge area: Check for loose retainers, broken clips, and housing damage.

    Verify: Replace only the failed wear item unless the helmet frame or carrier parts are also damaged.

    Measure before you order

    Part fit depends on more than the brand name. Measure the visible opening, lens frame size, pivot spacing, and any clip or tab locations if you can access them safely. Do not guess based on appearance alone.

    Check:

    • Lens width and height
    • Clip location and tab shape
    • Pivot hole spacing
    • Depth of the lens carrier or filter pocket

    Inspect: The old part for deformation. Heat-warped plastic can mislead measurements and make a replacement seem wrong when the original part is actually damaged.

    Verify: If the original part is bent or broken, measure the surrounding undamaged area and compare that with the replacement reference. If the required dimension is uncertain, treat it as Unknown (Verify).

    Troubleshooting support checks before ordering

    Use a short troubleshooting pass before you buy. This helps separate a true replacement need from an adjustment problem.

    • Helmet feels loose: Check the ratchet, crown adjustment, and side pivots.
    • Helmet slips down: Inspect headband tension and worn padding.
    • View is scratched or cloudy: Replace the outer or inner cover lens first if the filter itself is still functional.
    • Shades or visibility seem off: Inspect the cartridge mount, battery area, and lens carriers before assuming the helmet needs a shell-level part.

    Check / Inspect / Verify sequence:

    1. Check the symptom during normal use.
    2. Inspect the related wear item on the bench under good light.
    3. Verify whether the issue is the part itself, the adjustment, or a damaged mounting point.

    Use the WSP lookup page as a support reference

    For Lincoln support pages and related lookup guidance, use the Weld Support Parts reference page here:

    Lincoln PRO-Torch PTA-17 Support

    That page is a support reference and a starting point for checking compatible documentation, replacement-first guidance, and linked Lincoln lookup information. It is not a substitute for confirming the exact helmet model and part geometry.

    How to use it:

    • Open the support page while you have the helmet in hand.
    • Match the model and the part category before selecting anything.
    • Use the page as a cross-check if your current part is worn, broken, or missing markings.

    Ordering checks that prevent the wrong part

    Before finalizing an order, compare the replacement against the worn part and the helmet model record.

    Check:

    • Part name and function
    • Mounting style
    • Orientation and left/right placement
    • Any note about model-specific fit
    • Whether the part is a wear item or a structural component

    Inspect: The original part beside the product image or support reference, if available.

    Verify: If the ordering page does not clearly confirm fitment, do not assume compatibility. Record the fit as Unknown (Verify) and confirm with the seller or support documentation.

    Safety notes

    • Remove the helmet from service if the shell is cracked, the lens carrier is loose, or the headgear will not hold position.
    • Do not use a damaged lens assembly for arc welding.
    • Replace missing or failed protective components before returning the helmet to the shop.
    • If you are unsure whether a part affects eye or face protection, treat it as a safety-critical item until verified.

    FAQ

    How do I know which Lincoln helmet part I need?
    Start with the helmet model, then identify the failed component by location and function. Compare the worn part to the helmet before ordering.

    Can I order by appearance only?
    No. Similar-looking helmet parts may differ in tabs, spacing, or carrier style. Appearance alone is not enough.

    What if the model number is missing?
    Mark the model as Unknown (Verify) and inspect the shell, headgear, and lens frame for identifying marks before buying a replacement.

    Should I replace the whole helmet if one part is worn?
    Not always. Replace the failed wear item first unless the shell, carrier, or protective assembly is damaged.

    Sources Checked

    Related reading: If you are comparing helmet support approaches across brands, see Lincoln K3034-4 Viking Helmet: What to Expect and the 3M Speedglas G5-02 Welding Helmet Support Guide for additional fitment-check structure.

    Related Weld Support Guides

  • The Booth Next Door: What Welding Students Teach Each Other

    The Booth Next Door: What Welding Students Teach Each Other

    A welding booth gives one student a place to practice. A good lab also teaches a room full of future welders how to watch out for the work—and for one another.

    In a welding lab, the lesson rarely stays inside one booth. An arc goes quiet. A hood comes up. Someone studies a coupon, turns it toward the light and walks two stalls over to ask, “What are you seeing?”

    That small exchange is part of learning the trade. An instructor sets the standard and keeps the room safe, but students also learn from the work happening beside them: how another person lays out a practice piece, reacts to a bad start, organizes a lead or cleans a station before the next group arrives.

    The best peer learning is not a shortcut around instruction. It is practice in becoming the kind of shopmate other people can work beside.

    A booth looks individual. The work is shared.

    The curtain suggests solitude. The ventilation, traffic and pace of the room say otherwise.

    OSHA’s general welding requirements call for adjacent workers to be protected from arc rays by appropriate screens, shields or eye protection. The same standard says booth screens must not seriously restrict ventilation. Those are employer responsibilities, not a student rulebook, but they show why a training lab is a shared system. One person’s open curtain, misplaced screen or blocked aisle can affect somebody who never touches that person’s work.

    New students begin to understand the room through repeated, ordinary habits. Close the screen. Route leads so they do not become a surprise underfoot. Keep hot material where another person will not grab it by mistake. Return shared tools. Leave the booth ready for the next welder instead of leaving a small excavation project on the table.

    None of those habits will make a beautiful social-media clip. Every one of them makes a lab—and later a shop—easier to trust.

    Useful feedback has a shape

    “Looks good” is encouragement. It is not much of a diagnosis.

    A useful classmate points to something observable: where the arc started, how the joint was fit, what changed halfway down the coupon or which part of the finished piece deserves a closer look. The goal is not to perform expertise. It is to help the other person form a better question for the instructor.

    That distinction matters because similar-looking problems can have different causes. Copying the settings from the booth next door may change the evidence without explaining it. A student who says, “Your second half looks different from your first—what changed?” is often more helpful than one who reaches for the machine controls.

    Good peer feedback also knows where it stops. Anything involving safety, equipment condition, procedure requirements or an unfamiliar material belongs with the instructor or the person responsible for the lab. The confident move is not guessing faster. It is knowing when another set of qualified eyes is needed.

    The curriculum is bigger than the bead

    The American Welding Society describes SENSE as a framework of minimum standards and guidelines that schools can use to build welding programs. At the entry level, its subjects include welder safety and health, drawing and welding-symbol interpretation, thermal cutting and the major arc-welding processes. That list makes a quiet point: learning to weld was never only about making the face of a practice bead look right.

    Students are learning a working language. They begin connecting a drawing to a joint, a process to its hazards, and a finished coupon to an honest evaluation. The person in the next booth can help build that language by asking a clean question, comparing notes without turning the lab into a contest and accepting correction without making the correction personal.

    This is where class culture starts to matter. A room that treats every mistake as entertainment teaches people to hide evidence. A room that treats a mistake as information gives people a chance to correct it. Welding will supply enough frustration on its own; classmates do not need to add theater.

    School ends. Training does not.

    The Bureau of Labor Statistics says welders commonly enter the occupation through a combination of technical and on-the-job training. It also notes that some workers come through employer-based apprenticeships and that even people with formal technical training receive additional training after they are hired.

    In other words, the first job does not erase the student role. It changes the room.

    The booth next door becomes the fitter at the other end of the table, the senior welder on the next station, the inspector reading the same joint from another angle or the new hire watching how the crew handles a restart. The habits formed in school travel well: ask what someone sees, describe the evidence, respect the procedure and hand safety questions to the right person.

    So does the habit of leaving a place ready for whoever follows. A labeled coupon, a cleared table and a returned tool say something simple: another person’s time counts too.

    The classmate people remember

    Years later, few welders will remember every practice plate from school. They may remember the student who could explain something without showing off. The one who called an instructor over when a situation felt wrong. The one who did not laugh when somebody struggled with a process that had come easily to everyone else.

    That person is already practicing a trade skill. Not a welding process, exactly, but the human part of production: being clear, steady and useful when another worker needs a second set of eyes.

    Community question: Who helped you most when you were learning to weld—and what did they do that made the lesson stick?

    Arc Life tells the human side of the trade, from the first practice booth to the crews that keep learning on the job. Read what Arc Life is building, then visit the Arc Life collection.

  • Before the Machine Goes Down: A Practical Maintenance System for Welding Shops

    Before the Machine Goes Down: A Practical Maintenance System for Welding Shops

    A machine rarely chooses a convenient time to go down. The failure lands in the middle of a production day, and the first few minutes usually sound the same: Who worked on it last? Was that cable replaced? When did the compressor start making that noise? Is the part already on order?

    In a large operation, a computerized maintenance system may answer those questions. In a smaller welding or fabrication shop, the answer is often spread across a notebook, a whiteboard, a stack of receipts, and the memory of the one person who seems to know every machine. That system works—until that person is off, the note disappears, or the same problem returns six months later.

    Good maintenance records are not office decoration. They help a shop decide what needs attention, who owns the next step, and where downtime is actually coming from. The system does not have to be complicated. It does have to be used.

    Start with four questions

    A practical shop-maintenance system should answer four questions without a scavenger hunt:

    • What equipment do we have? Record a clear asset ID, description, location, status, and the information needed to find the correct manual or service history.
    • What work is due? Keep recurring inspection and maintenance tasks in one schedule, with an owner and the correct calendar- or meter-based interval for that asset.
    • What happened last time? Document service, repairs, findings, parts, labor, outside service, and corrective action while the details are still fresh.
    • What is the interruption costing? Separate the price of the repair from the hours and production exposure created by the downtime.

    Those questions apply to more than welding power sources. Plasma systems, fume extraction, compressors, saws, positioners, ovens, material-handling equipment, and other recurring shop assets all compete for maintenance attention. Without a common record, urgent work crowds out preventive work and yesterday’s temporary repair quietly becomes today’s operating condition.

    A record should help the next person

    “Checked machine” is not a useful service entry. Neither is “fixed.” A useful record identifies the asset, the symptom or task, the work performed, the condition found, any parts used, the person or vendor involved, the result, and the next required action. If the unit remains out of service, that status should be visible instead of buried in a note.

    The goal is not paperwork for its own sake. The goal is continuity. A welder coming onto the next shift, a supervisor reviewing a repeat failure, or an outside technician arriving weeks later should be able to understand what has already happened. A consistent asset ID ties those records together even when several machines share the same model name.

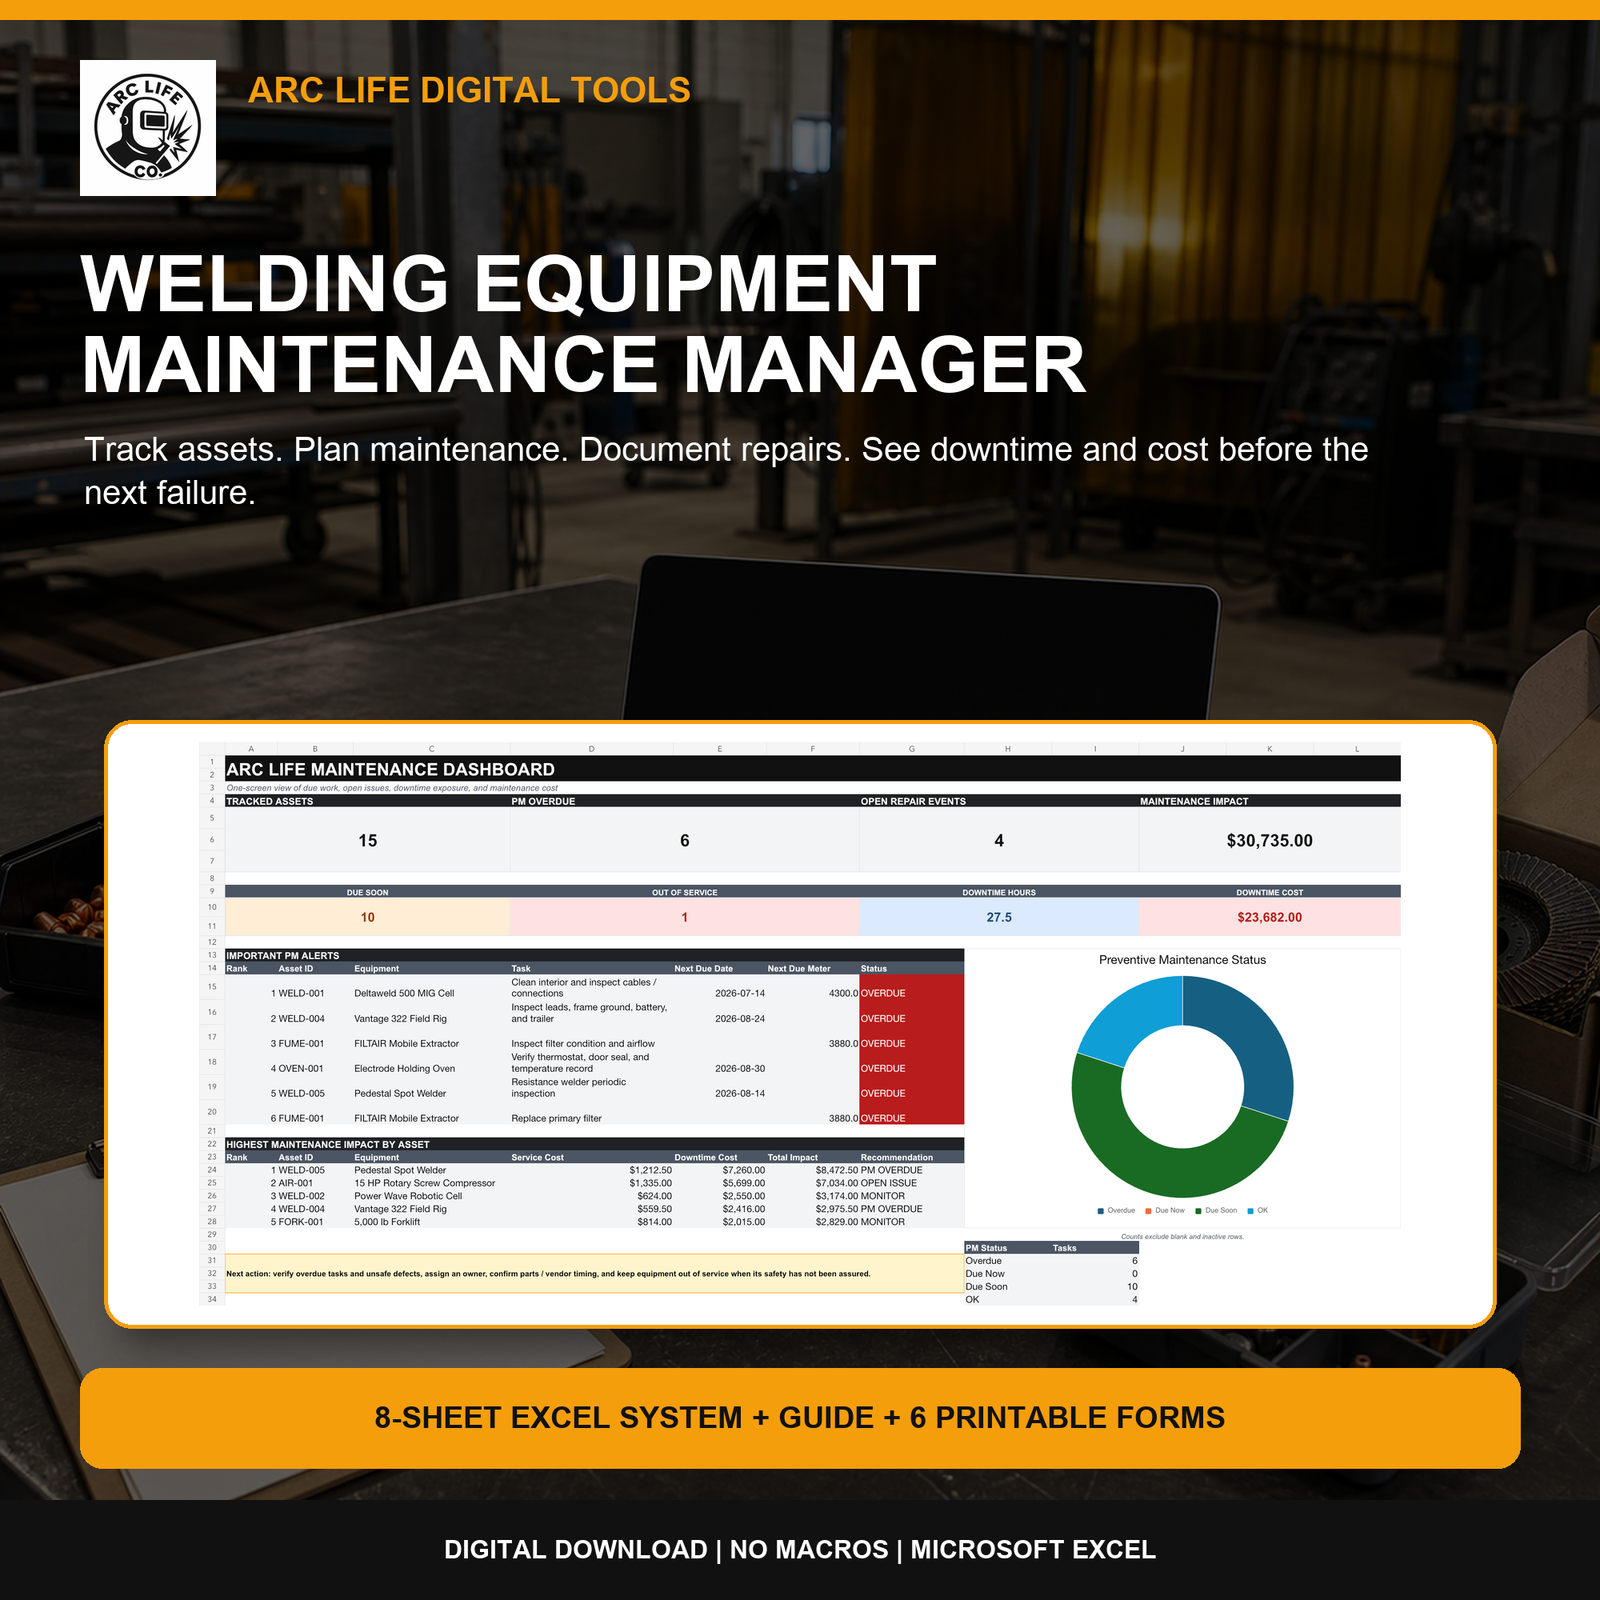
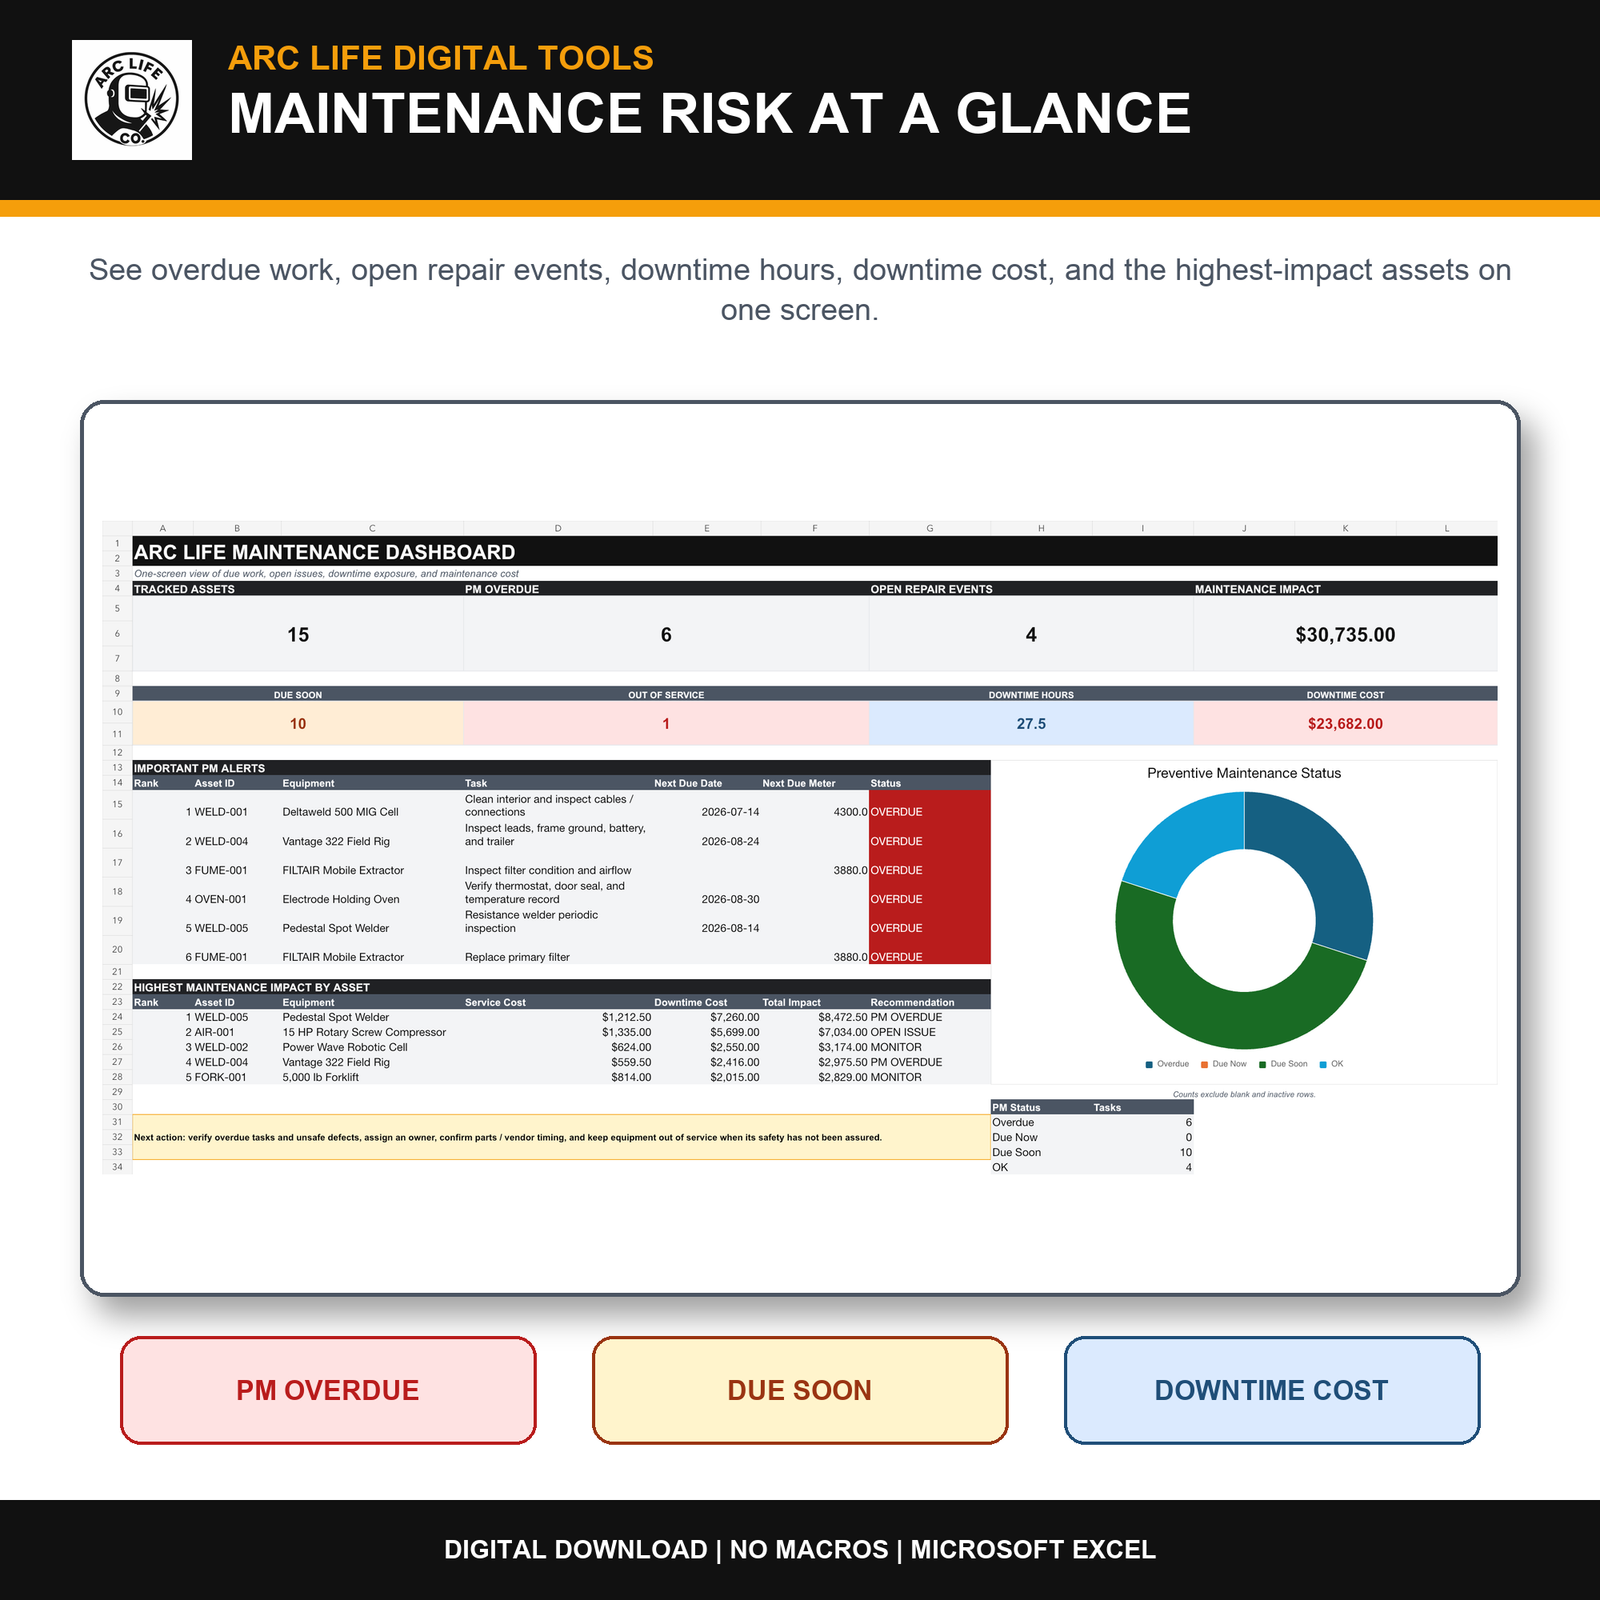
    Arc Life welding equipment maintenance dashboard showing overdue work, open repairs, downtime, and high-impact assets
    A useful dashboard should surface overdue work and open repair events without replacing the underlying service records.

    Use the dashboard as a question, not an answer

    Dashboards are valuable because they compress a lot of records into a short review. They can show overdue preventive work, open repair events, out-of-service equipment, downtime hours, and assets with unusually high maintenance impact. That makes it easier to decide where a morning meeting should begin.

    But a red cell is not a maintenance instruction. The correct task, inspection method, interval, and return-to-service decision still come from the current manufacturer documentation, qualified personnel, applicable inspection requirements, the shop’s operating conditions, and its safety program. A spreadsheet can organize those decisions. It cannot make them safely on its own.

    Where a spreadsheet fits—and where it does not

    Some shops need a full CMMS with automatic notifications, mobile scanning, work-order approvals, supplier integrations, user permissions, and enterprise controls. Others need a disciplined bridge between memory and enterprise software. That middle ground is where a well-built spreadsheet earns its place.

    The Arc Life Welding Equipment Maintenance Manager was built for that smaller-shop use case. The Excel system includes an asset register, preventive-maintenance schedule, service log, repair and downtime records, cost analysis, a dashboard, a quick-start guide, and six printable forms. It uses standard formulas rather than macros. The current version supports up to 200 assets, 500 recurring maintenance tasks, 1,000 service events, and 500 repair or defect events.

    That capacity only matters if the workflow is kept honest. Demonstration data must be replaced. After recurring service is recorded, the corresponding last-service values still need to be updated. Equipment that has not been made safe should remain out of service, regardless of what a dashboard says. The tool is a planning and recordkeeping aid—not a substitute for lockout/tagout, inspections, training, qualified maintenance, or engineering judgment.

    The habit is more important than the file

    The best maintenance file in the world becomes useless when nobody owns it. Pick one person responsible for the weekly review, define who closes tasks, and decide where paper forms or field notes enter the main record. Keep the process short enough that it survives a busy week. Then review repeat problems and high-impact assets instead of merely clearing colored cells.

    A shop will never eliminate every surprise. It can stop treating every surprise like the first time it happened.

    Shop question: What piece of equipment causes the most disruption when it goes down—and could your current records show its last three service events in less than a minute?

    Explore the full collection of practical shop systems in Arc Life Digital Tools.

  • Inweld 2 Gauge Premium Welding Cable 600 Volt – Black – Made in the USA (250 FEET): Product Breakdown

    Inweld 2 Gauge Premium Welding Cable 600 Volt – Black – Made in the USA (250 FEET): Product Breakdown

    Product not found.
    “>Inweld 2 Gauge Premium Welding Cable 600 Volt - Black - Made in the USA (250 FEET)

    Inweld 2 Gauge Premium Welding Cable 600 Volt – Black – Made in the USA (250 FEET) is a general-purpose welding lead product listed for welding, motor, generator, and battery lead use. For buyers and maintenance teams, the main questions are not just length and gauge. The real checks are conductor size, insulation condition, voltage rating, termination method, bend management, and whether the cable is being used within the equipment’s duty and current requirements. This breakdown focuses on practical inspection and support steps before installation or replacement.

    Key Takeaways

    • 2 gauge cable is a heavy lead size, but the correct application still depends on the machine, lead length, and current draw.
    • The listed product information confirms black color and 600 volt rating. Other technical details are Unknown (Verify) unless confirmed by the supplier data sheet.
    • Use the cable as a replaceable lead only after checking compatibility with lugs, connectors, and strain relief at the actual machine and work point.
    • Inspect the full cable length before service. Damage at the first few feet near the machine is common, but field abrasion can occur anywhere.
    • If the cable is used for motors, generators, or batteries, verify polarity, insulation condition, and termination security before energizing.

    What the Product Listing Tells You

    The available product description identifies this as a 2 gauge premium welding cable, black, rated 600 volts, and sold in a 250 foot length. The short description also notes use for welding leads plus motors, generators, and batteries. Nominal diameter is listed as .420 inch. Anything beyond that, including strand construction, jacket material, temperature rating, ampacity, or certification status, is Unknown (Verify) unless you have the manufacturer data sheet in hand.

    For purchasing, that means you should not assume the cable is suitable for every lead replacement job just because the gauge looks right. Verify the machine output, lead routing, and termination hardware before release to the floor.

    Practical Check, Inspect, Verify Steps

    Before purchase or issue from stock

    • Check the required lead length against the job. Do not cut a 250 foot reel without confirming the actual takeoff plan.
    • Inspect the end use: welding lead, generator lead, battery lead, or other equipment lead. Unknown (Verify) for each specific application unless the equipment manual approves it.
    • Verify the connector style needed at both ends. Lugs, clamps, and receptacles must match the machine and cable size.

    During installation

    • Check that the cable path avoids sharp edges, hot work zones, and moving equipment.
    • Inspect for kinks, flat spots, jacket cuts, burned areas, and crushed sections before pulling the cable into service.
    • Verify all terminations are mechanically secure and properly crimped or attached per your shop standard.

    During service

    • Check the first sign of overheating at plugs, lugs, and connection points.
    • Inspect for insulation wear where the cable crosses floors, carts, or hang points.
    • Verify that the cable is not being loaded beyond the equipment’s intended duty cycle. Current capacity is Unknown (Verify) for this listing without a published data sheet.

    Troubleshooting Common Cable Problems

    Problem: cable feels stiff or difficult to route

    • Check whether the cable was stored tightly coiled or exposed to cold conditions.
    • Inspect for jacket cracking or flat memory from improper storage.
    • Verify the routing path is not forcing too-tight bends. Rework the path before blaming the cable.

    Problem: connection runs hot

    • Check the lug or clamp fit at the termination.
    • Inspect for oxidation, looseness, and damaged strands near the crimp.
    • Verify the connection is clean, tight, and sized for 2 gauge cable.

    Problem: visible jacket damage

    • Check whether the damage is only surface abrasion or if strands are exposed.
    • Inspect the entire run, not just the obvious fault point.
    • Verify the cable is removed from service if the conductor is compromised. Do not continue use based on appearance alone.

    Product and Parts Section

    For this article, the referenced product is the only listed ArcWeld item:

    Product not found.

    “>Inweld 2 Gauge Premium Welding Cable 600 Volt – Black – Made in the USA (250 FEET)

    ArcWeld product shortcode:

    Inweld 2 Gauge Premium Welding Cable 600 Volt - Black - Made in the USA (250 FEET)

    Inweld 2 Gauge Premium Welding Cable 600 Volt – Black – Made in the USA (250 FEET)

    2 Gauge Premium Welding Cable – Black – 600 Volts – Welding lead- Leads for Motors, Generators, Batteries – Nominal Diameter is .420"

    View at Arc Weld Store

    Use the product page as the source of record for the listing details. If your purchasing team needs confirmation on strand count, jacket type, or agency approvals, request the datasheet or manufacturer confirmation. Do not assume those details from gauge and voltage rating alone.

    How Buyers Should Evaluate This Cable

    For maintenance buyers, the right process is simple: match the cable to the actual job, then verify the connection hardware and routing. A 250 foot reel is useful in fabrication shops, service trucks, and plant maintenance areas where long lead runs or multiple cut lengths are needed. The tradeoff is inventory control. Once a long reel is cut, the remaining stock must still be tracked by size and condition.

    When replacing damaged leads, compare the old lead to the new one only as a starting point. The old cable may have been undersized, overloaded, or repaired incorrectly. Use the replacement as an opportunity to correct the root cause: poor routing, poor storage, or wrong connector selection.

    Safety Notes

    • De-energize equipment before handling or replacing any lead.
    • Do not use damaged cable with exposed conductors, burned jacket, or loose terminations.
    • Keep cables out of pinch points, hot slag paths, and traffic lanes.
    • Use only termination methods approved by your shop procedure and the equipment manufacturer.
    • If the cable is used outside welding service, verify the application with the equipment manual. Unknown (Verify) where not documented.

    FAQ

    Is this cable only for welding?

    No. The listing also mentions motors, generators, and batteries. That does not mean every installation is approved. Verify the end use against the equipment manual and your internal standards.

    Can I assume the ampacity from the 2 gauge size?

    No. Ampacity depends on insulation type, duty cycle, installation conditions, ambient temperature, and lead length. The listing does not provide enough data for a reliable ampacity claim. Unknown (Verify).

    What should I inspect first on a used welding lead?

    Start with the terminations, then inspect the first several feet near the machine, then walk the full length looking for cuts, burns, crushing, and splices. Verify continuity and insulation condition before returning it to service.

    Is the 250 foot length a finished assembly?

    The available listing shows a 250 foot cable product, but assembly details such as end fittings are Unknown (Verify). Confirm whether you are buying bulk cable or a pre-terminated lead set before ordering.

    Sources Checked

    • ArcWeld product page: Inweld 2 Gauge Premium Welding Cable 600 Volt – Black – Made in the USA (250 FEET)
    • Provided product short description and listing data from the task record

    This draft uses only the provided product reference. No WSP lookup pages or filler metal finder pages were provided for this task, so none were included.

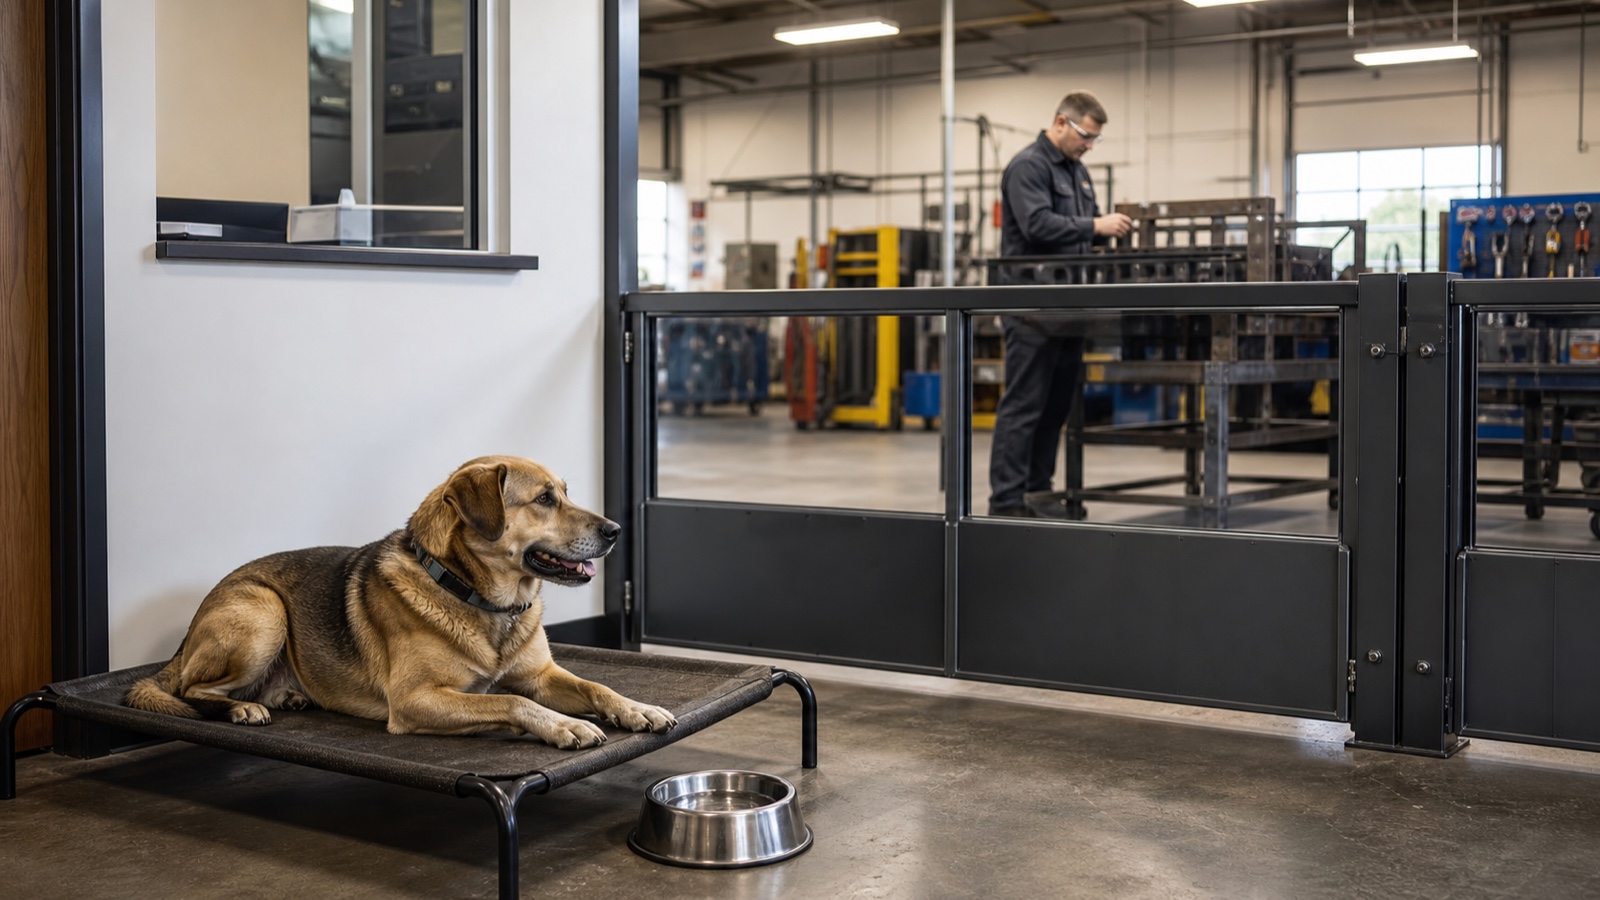
  • The Shop Dog Is Part of the Crew—But Not Part of the Welding Area

    The Shop Dog Is Part of the Crew—But Not Part of the Welding Area

    The social-media version of a shop dog is almost too easy to picture: paws stretched under a welding table, sparks in the background, a battered water bowl beside the toolbox. It looks warm, loyal, and unmistakably blue collar.

    It is also the wrong picture.

    A dog can be part of a shop’s personality without roaming through its active work area. In fact, the clearest sign that a crew truly cares about its unofficial four-legged member is not a good photo. It is a boring, consistent boundary.

    That feels worth saying on August 26. National Dog Day, founded in 2004, celebrates dogs of all breeds and calls attention to dogs that need rescue. The day’s official site also honors family dogs and working dogs. Welding shops have their own familiar version: the dog that recognizes the morning trucks, knows who drops food at lunch, and appears when the office door opens.

    The best place for that dog is still on the safe side of the door.

    The photo and the shop are not the same thing

    The shop-dog image works because it softens an industrial place. A dog can make an office feel less corporate, give the first person through the door a familiar greeting, and become part of the routine customers remember. None of that requires the animal to share space with hot work.

    The Occupational Safety and Health Administration lists metal fumes and ultraviolet radiation among the health hazards of welding, cutting, and brazing. Its safety-hazard list includes burns, eye damage, electrical shock, cuts, and crushed toes and fingers. OSHA also points to noise exposure, personal protective equipment, ventilation, and fire controls as parts of managing that environment.

    Those rules and resources are written to protect people at work. They are not a pet policy. Still, the logic is hard to miss: if trained workers need barriers, PPE, ventilation, and controlled work practices, an animal without those protections should not be inside the active area.

    This is not about treating every fabrication shop as the same. It is about recognizing that a dog cannot read a hot-work permit, understand why a plate is still hot, or know that a lead stretched across an aisle is attached to a live job.

    If people need PPE, the dog needs distance

    Human workers can be trained to stop at a screen, wear the right lens, recognize a lift route, and stay clear of a grinder. A dog moves by sound, smell, habit, curiosity, and the location of its favorite person. That unpredictability does not belong near a process where one quick step can cross a cable, enter a forklift path, or reach fresh-cut steel.

    Noise deserves the same clear thinking. OSHA’s general-industry standard requires a hearing-conservation program when employee exposure reaches an eight-hour time-weighted average of 85 decibels. That does not establish a pet limit, and it should not be borrowed as one. It does show that industrial noise is measured and managed—not dismissed as atmosphere.

    The right response is not a novelty pair of dog earmuffs and a good caption. It is separation from grinding, air-arc work, hammering, plasma cutting, and other loud operations. Pet-specific health questions belong with a veterinarian; shop access belongs in the shop’s safety plan.

    Floor conditions matter, too. OSHA requires walking-working surfaces to stay orderly and free of hazards such as sharp or protruding objects. A well-kept floor protects employees. It also removes fewer chances for a paw to find a sharp drop, a sliver, or spilled material—but housekeeping alone does not turn a production floor into a pet area.

    Good shop-dog culture is boring on purpose

    A responsible setup does not need to be complicated. The dog has a defined place in the front office, enclosed yard, or another separated area. The barrier closes. Water and bedding stay away from chemicals, oily rags, metal debris, and traffic. Deliveries do not depend on somebody remembering to grab a collar at the last second.

    The rule stays the same on slow days. That is important. A dog that is allowed onto the floor while the machines are quiet cannot understand why the same doorway becomes off-limits when the first grinder starts. Consistency is kinder than a rule that changes with the workload.

    The crew also resists staging the animal for a dramatic photo near sparks or an open arc. Welding culture already has enough imagery that turns hazards into decoration. A shop dog does not need to be made into another prop.

    Some facilities cannot support a dog at all. Customer rules, lease terms, allergies, sanitation requirements, insurance, traffic, or the layout may settle the question before the crew does. “No shop dog” is not anti-dog. Sometimes it is the most honest answer the building can give.

    Part of the crew means worthy of a rule

    The value of a shop dog is not productivity. The dog is there because people spend a large part of their lives at work, and a familiar animal can make that place feel more human. It can mark the difference between the production floor and the small community gathered around it.

    That community owes the dog more than affection. It owes the dog a boundary that does not disappear for a photo, a visitor, or a quiet afternoon.

    There is something deeply consistent about that idea. Welders already understand controlled zones. They know the difference between an active booth and a clear aisle, between hot metal and finished work, between a barrier that is inconvenient and one that prevents a bad day. Extending that discipline to a dog is not overthinking the culture. It is taking the culture seriously.

    Does your shop have a dog, and what rule keeps it safe? Office only? Fenced yard? Home before hot work starts? Tell us the boundary that actually works—not just the picture that looks good.

    Arc Life pays attention to the people, routines, and off-the-clock details that make welding culture recognizable. You can also visit the Arc Life collection, but today’s best piece of shop gear is a closed gate between the dog and the work.

    Sources

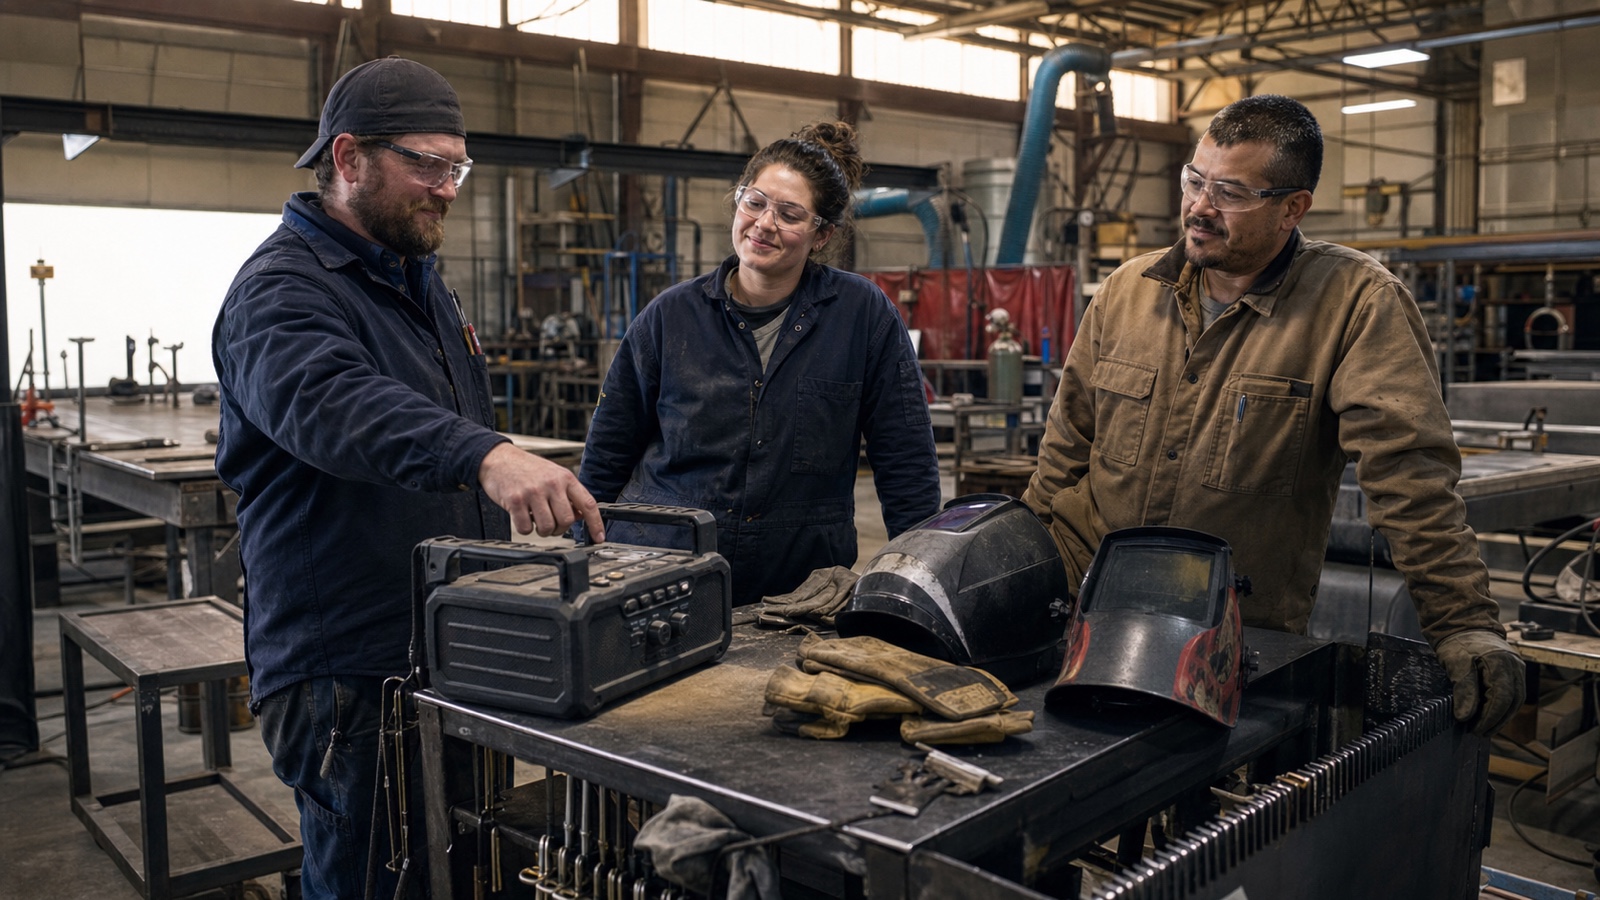
  • Who Gets the Shop Radio? The Unwritten Rules of a Welding Shift

    Who Gets the Shop Radio? The Unwritten Rules of a Welding Shift

    Before the first helmet goes down, somebody usually settles one of the day’s smaller questions: what are we listening to?

    The answer might be country before breakfast, old rock after the first break, or a station nobody loves enough to defend. A phone connects. A speaker crackles awake. Somebody asks for one song and gets an entire afternoon of somebody else’s playlist.

    The shop radio looks like background noise. It rarely stays that simple. In a shared workspace, music becomes a daily test of judgment: how loud is too loud, who gets a turn, which songs do not belong, and when the radio needs to disappear behind the work.

    That is why the person holding the phone is not just picking music. For a little while, they are reading the room.

    One Speaker, a Dozen Opinions

    A welding crew can agree on a fit-up and disagree completely on the next song.

    That disagreement is part of the fun when the crew handles it well. The radio gives people something harmless to argue about between real decisions. Somebody knows every word. Somebody groans at the opening riff. The newest person discovers that one unlikely song can get three generations singing the same chorus.

    Nobody has to share a taste in music to share a shift. The better rule is rotation without ceremony. The person who connected first does not own the speaker until clock-out. The loudest opinion does not automatically win. A request is not a challenge to the entire identity of whoever built the playlist.

    This is basic give-and-take, but small habits reveal a lot. A shop that can pass control of the radio without turning it into a contest has usually learned something useful about sharing space.

    Music Gives the Shift Its Edges

    Shop work has its own sounds before the radio joins in: ventilation moving air, a grinder starting and stopping, clamps hitting a table, carts crossing seams in the floor, and short conversations rising above it all.

    Music sits inside that rhythm. It marks the quiet setup at the beginning of the day, the middle hours when everybody settles into their work, and the cleanup stretch when tools start finding their way home. A familiar song can make a long repetitive task feel less solitary. A bad selection can make three minutes seem impressively long.

    The radio does not make difficult work easy, and it does not create a good crew by itself. It gives the day edges. Years later, a song can bring back a particular shop more quickly than a photograph: the light, the smell of steel dust, the bench you worked at, and the people who were there.

    That connection is worth something. So is knowing when nostalgia should stay at a reasonable volume.

    The Operator Is Not the Owner

    The fairest shop-radio rules are rarely posted. They are demonstrated.

    The person running the playlist watches for reactions instead of assuming silence means approval. They skip the song that clearly changes the room. They do not treat every request like an interruption. They understand that lyrics booming across a shared workplace land differently than the same song played alone in a truck.

    They also leave room for the coworker who wants less sound, not more. Some people concentrate better without music. Others may be carrying a headache, learning a new task, listening for instructions, or simply tired of the same twenty songs. A respectful crew does not make somebody present a courtroom case to get the volume turned down.

    The practical standard is simple: the radio belongs to the room. Whoever touches the controls is taking a turn, not claiming territory.

    There Are Times the Radio Loses

    The best song of the day still comes second to a job briefing, a handoff, an alarm, a spotter, or a coworker trying to warn somebody. Site rules come first. Required hearing protection stays in place. Personal audio does not get to isolate somebody from the signals and communication the job depends on.

    This is not just an etiquette question. The Occupational Safety and Health Administration says employers in general industry must implement a hearing-conservation program when worker exposure reaches an eight-hour time-weighted average of 85 dBA. OSHA points employers toward measuring workplace sound and controlling exposure; guessing by the position of a volume knob is not a noise assessment.

    A radio may be the least powerful sound source in the room, but it is still part of the sound environment. If music has to fight the shop to be heard, turning it higher is not proof that the mix is working. It may be proof that the radio has already lost.

    Good crews know how to enjoy music without asking it to overpower the work. They turn it down before the conversation becomes a shouting match. They shut it off when clarity matters. Then, when the moment passes, somebody reaches for play again.

    Small Rules Build a Shared Place

    Shop culture is often described through the big things: standards, output, skill, safety, and the way a crew handles pressure. Those matter most. The smaller customs show how that culture feels on an ordinary Tuesday.

    Who gets the radio is one of those customs. The answer says something about seniority, hospitality, patience, and how much room a crew makes for different people. A good setup does not require identical taste. It requires enough awareness to keep the music from becoming another machine one person operates and everybody else endures.

    The radio is at its best when it stays in the background but still belongs to the memory of the shift. It carries a little personality through a hard room. It gives people a reason to laugh, complain, request a track, and discover that the quietest welder in the bay knows every word.

    So here is the Arc Life shop question: what is the unwritten radio rule where you work—and who actually gets the final pick?

    Arc Life covers the habits, personalities, and shared details that make welding more than a process. Read the story behind the community on About Arc Life, or explore the current Arc Life collection.

    Source

  • Starlite Safety Glasses, Gray Temple, Red Mirror Lens, Ultra Lightweight, 461M: Replacement Part Breakdown

    Starlite Safety Glasses, Gray Temple, Red Mirror Lens, Ultra Lightweight, 461M, are an eye protection item that may be used around welding support work, grinding, fabrication, and general shop handling. This article is a practical breakdown for buyers and support teams who need to inspect the part, confirm the right use case, and avoid ordering errors.

    The main point: treat this as a PPE item with limited technical data available in the source record. Do not assume compatibility with welding helmets, face shields, or prescription inserts unless you verify it directly from the product listing and your site safety requirements.

    Key Takeaways

    • Verify the exact product identity before purchase: Starlite Safety Glasses, Gray Temple, Red Mirror Lens, Ultra Lightweight, 461M.
    • Do not assume lens shade, impact rating, anti-fog treatment, or UV performance if not stated in your source. Unknown (Verify).
    • For welding support work, confirm whether the glasses are for general shop safety only or for use under additional face protection.
    • Check frame condition, lens clarity, temple alignment, and surface damage on receipt.
    • Use the Amazon ASIN reference only as a product identifier: B00839ZNZ2.

    What to Verify Before You Buy

    For maintenance buyers and weld support teams, the first step is to verify the use case. Safety glasses can be suitable for grinding bays, parts handling, or shop transit, but they are not automatically suitable for every hot-work task.

    Check: the job task, exposure type, and whether the wearer needs additional side protection or face coverage.

    Inspect: the product listing for lens material, frame style, temple design, and any stated compliance language.

    Verify: whether the red mirror lens is intended for indoor use, outdoor use, glare reduction, or visual comfort. Unknown (Verify) if the listing does not state this clearly.

    Do not rely on color alone. A red mirror lens may affect visible light differently than clear or shaded eyewear, but the actual performance depends on the manufacturer’s stated design. If the data is not provided, treat it as unknown.

    Replacement Part Breakdown

    This product listing is a finished eyewear item, not a service kit. There are no confirmed replacement subcomponents provided in the source data. If a buyer is looking for parts-level support, use the following breakdown approach:

    • Frame/temples: Confirm the gray temple design, fit tension, and any visible warping.
    • Lenses: Inspect for scratches, coating wear, distortion, or pitting.
    • Nose contact area: Verify comfort and stability during head movement.
    • Fasteners or hinges: Unknown (Verify). No internal construction details were provided.

    If your team normally stocks replacement eyewear parts, note that this product record does not confirm serviceable components. Replacement decision should be based on wear, damage, and whether the full eyewear unit remains safe to use.

    Inspection and Support Checks

    Use these practical checks on receiving inspection and during routine PPE audits:

    1) Packaging and identity check

    Check: that the item matches the listed name and ASIN B00839ZNZ2.

    Inspect: any item labeling for the exact model designation 461M.

    Verify: the lens color and temple color match the ordered product. Do not substitute based on appearance alone.

    2) Lens condition check

    Check: for scratches, haze, cracks, chips, or coating defects.

    Inspect: by holding the lens at multiple angles under shop lighting.

    Verify: that visual distortion is not present. If distortion is seen, remove the item from service.

    3) Frame and temple fit check

    Check: whether the temples hold position without excessive side pressure.

    Inspect: the temple alignment and hinge movement, if applicable. Unknown (Verify) for hinge design specifics.

    Verify: a stable fit when the wearer looks down, turns the head, and lifts a welding hood or face shield.

    4) Task suitability check

    Check: whether the job involves grinding, cutting, overhead work, or exposure to flying debris.

    Inspect: if the glasses provide the level of coverage your safety program requires.

    Verify: that the eyewear is acceptable under site rules before assigning it to active work.

    Buyer Guidance for Welding Support Teams

    Welding support buyers should treat this product as a shop PPE line item, not as a guaranteed substitute for welding-specific eye protection. If your standard requires shade-specific protection, confirm that requirement separately.

    For procurement, the safest approach is simple: order only when the product identity is confirmed, then receive-inspect before issue. If the listing does not state performance details you need, mark those fields as Unknown (Verify) and request documentation from the supplier or internal safety team.

    For related support topics, see these internal guides:

    Safety Notes

    • Eye protection must match the hazard. General safety glasses are not a substitute for task-specific protection when the job requires more coverage.
    • Remove damaged eyewear from service immediately.
    • Do not assume the lens tint is appropriate for welding arc exposure. Unknown (Verify).
    • Use site PPE rules and the manufacturer’s instructions as the final authority.

    FAQ

    Is this product confirmed for welding arc protection?

    No. The provided source data does not confirm welding arc protection. Unknown (Verify).

    Can I use these glasses as a replacement for a welding helmet?

    No. Safety glasses and welding helmets serve different protection functions. Verify your site requirement before assigning the item to a welding task.

    What replacement parts are available for this model?

    No replacement subcomponents were confirmed in the source data. Treat this as a finished eyewear item unless the manufacturer documentation states otherwise. Unknown (Verify).

    What should I check when the glasses arrive?

    Check the ASIN reference, lens condition, frame integrity, temple fit, and whether the product matches the ordered model name and color description.

    Sources Checked

    • Provided Amazon product record reference: B00839ZNZ2
    • Allowed internal links listed in the task
    • No WSP lookup page provided
    • No filler metal finder page provided

    Product reference:

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

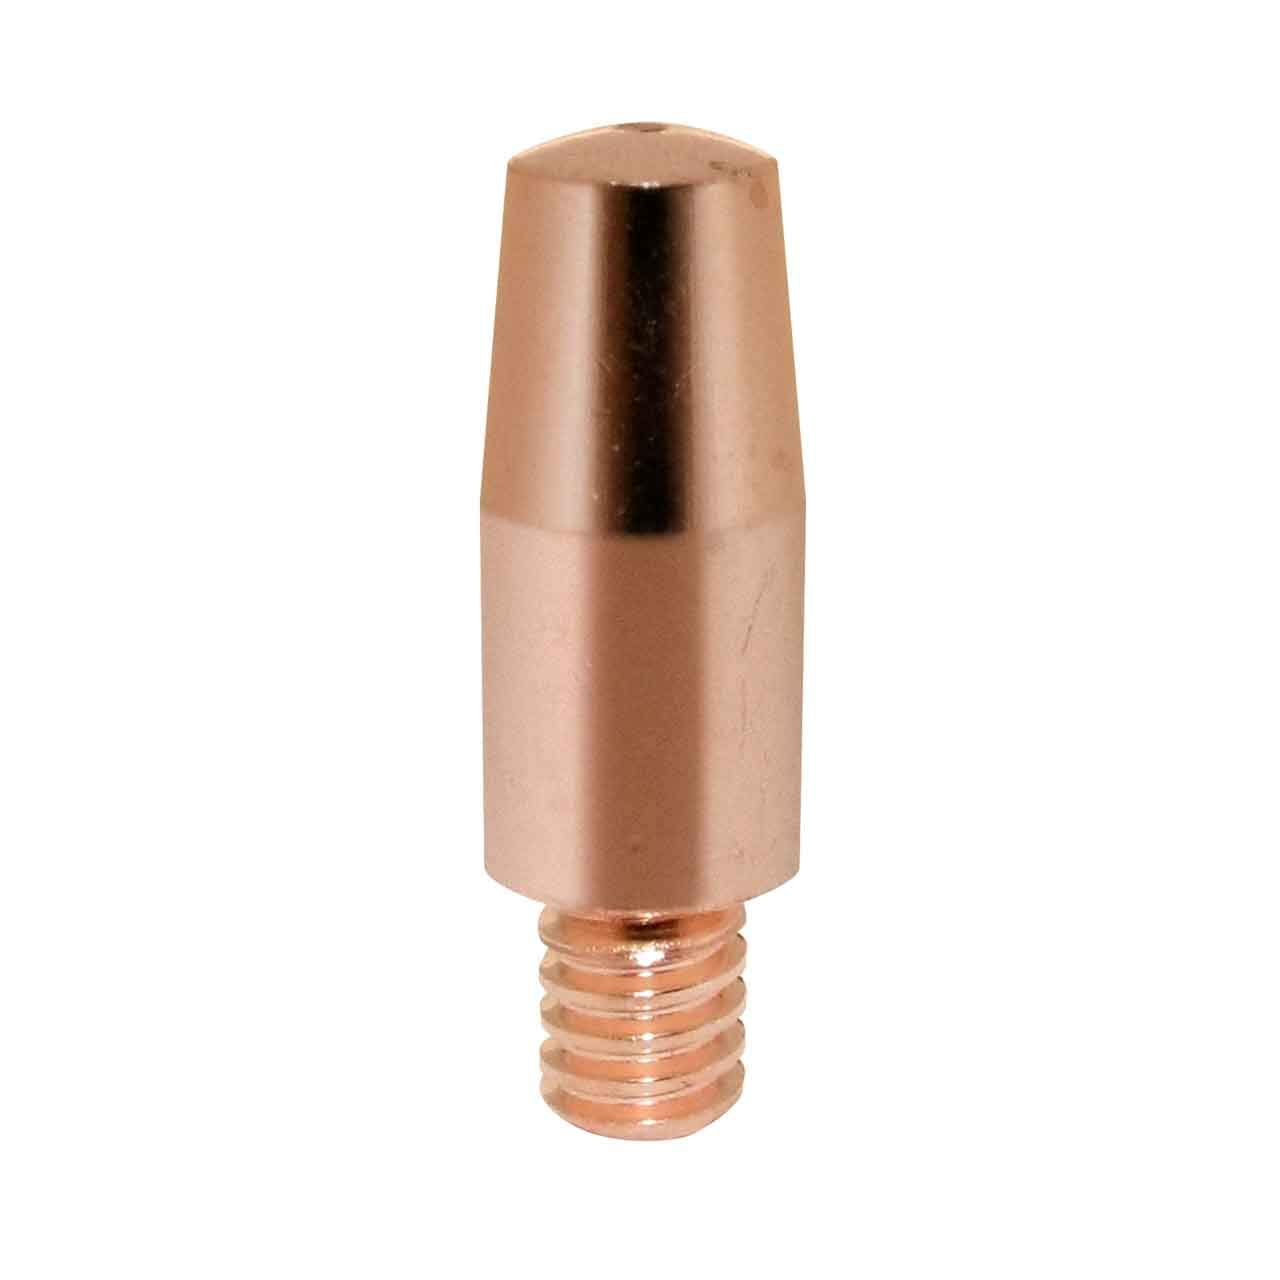
  • Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack: Product Breakdown

    Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack: Product Breakdown

    Product not found.
    “>Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack

    The Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack is a MIG consumable used to transfer current to the electrode wire at the gun front end. For buyers and maintenance teams, the main job is simple: keep the wire feeding smoothly and maintain a stable electrical path. When a contact tip is the wrong size, worn, or contaminated, the result is usually inconsistent arc behavior, feeding drag, or premature tip failure.

    This breakdown stays focused on what to check before you buy, install, or troubleshoot this tip in service. The listing indicates a 350A rating and .040 in (1.0 mm) wire size. Any other fit or application detail should be treated as Unknown (Verify) unless confirmed by your torch, gun, and OEM documentation.

    Key Takeaways

    What a Contact Tip Does

    A contact tip serves two functions. First, it conducts welding current into the wire. Second, it constrains wire guidance at the point where the arc starts. If the internal bore is oversized, worn, or distorted, the wire can wander and the arc can become erratic. If the bore is undersized or contaminated, wire feed drag rises and the wire may bind.

    For production and repair welding, the practical goal is not just arc starts. It is repeatable current transfer over time with minimal interruption. That means the tip condition matters as much as the wire size printed on the package.

    Check Before You Install

    1. Check wire diameter. Verify the feeder is loaded with .040 in (1.0 mm) wire. Do not rely on setup memory. Read the spool label and measure if needed.
    2. Inspect the gun front end. Verify the diffuser, nozzle, and tip adapter threads are clean and not cross-threaded.
    3. Inspect the old tip. Look for burnback, spatter bridging, oval wear, or blue heat discoloration. These are signs of poor current transfer or excessive heat load.
    4. Verify seating. The tip should install fully and seat squarely. If it rocks, binds, or bottoms out incorrectly, stop and verify the torch parts.
    5. Confirm the part number. Match the replacement tip to the gun system and consumable family in the OEM reference. Unknown (Verify) if the torch family is not documented.

    Inspect During Service

    Routine inspection prevents avoidable downtime. A quick daily check is enough for many shops, with more frequent checks in high-duty production cells.

    Troubleshooting Support

    If the weld system is not behaving normally, the contact tip is one of the first consumables to verify. Use a simple check/inspect/verify sequence.

    Problem: Wire feed hesitation

    Problem: Burnback at the tip

    Problem: Unstable arc or spatter increase

    Product and Parts Notes

    The Lincoln Electric KP2744-040 Copper Plus Contact Tip is listed as a 350A, standard-style MIG contact tip for .040 in (1.0 mm) wire. Beyond that, any torch-family compatibility, current-duty interpretation, or service-life claim should be treated as Unknown (Verify) unless confirmed by the manufacturer or gun documentation.

    For buyers, the practical value of this type of tip is in consistency. A consistent contact tip reduces unnecessary troubleshooting time because it removes one variable from the front-end system. For maintenance teams, that means fewer false alarms when a feeding issue is really a wear issue at the tip.

    If you need to compare this consumable against a broader wire or process plan, a related internal resource may help with wire selection context: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog. Use that page as a starting point for material selection context, not as a procedure approval for this tip.

    Maintenance Buying Considerations

    For stocked spares, contact tips should be treated as high-turn consumables. Keep them organized by wire diameter and torch family. Do not mix bins or assume one .040 in tip matches every gun. That mistake causes time loss at the workbench and at the machine.

    When building a PM kit, include the tip, diffuser, nozzle, and any related front-end consumables that commonly wear together. If the root cause of tip failure is recurring, look upstream at wire cleanliness, drive roll setup, liner condition, and gun angle.

    Safety Notes

    FAQ

    Is the KP2744-040 only for .040 in wire?
    The listed size is .040 in (1.0 mm). Use that as the primary match point. Any other wire size should be treated as Unknown (Verify).

    Can I use this tip in any MIG gun?
    No. Compatibility depends on the torch, diffuser, and thread style. Verify against the gun manufacturer’s consumable chart before installing.

    What are the first signs that the tip should be replaced?
    Watch for wire feed hesitation, burnback, unstable starts, visible bore wear, spatter bridging, and damaged threads.

    Should I replace the tip when changing wire?
    Not automatically. Inspect the tip first. Replace it if wear, sizing mismatch, or contamination is present.

    Sources Checked

    Related Arc Weld Part

    Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack

    Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack

    The Lincoln Electric KP2744-040 Copper Plus Contact Tip is a 350A, standard-style MIG contact tip engineered for consistent wire transfer and stable arc performance in high-amperage applications. Built from Lincoln’s Copper Plus material, this tip is designed to deliver reliable electrical conductivity and extended service life in production and repair environments where tip wear, spatter adhesion, and thread gall…

    View at Arc Weld Store

    Related Weld Support Guides

  • More posts

    Watch with Prime Video