Search results for: “welding gloves PPE”

  • The Small Part That Stops the Shift: A Better Way to Track Welding Consumables

    The Small Part That Stops the Shift: A Better Way to Track Welding Consumables

    The part that stops a welding shift is not always expensive. Sometimes it is a contact tip, a plasma electrode, a grinding wheel, a tungsten size nobody checked, or the last pair of the correct gloves. The dollar value may be small. The interruption is not.

    That is what makes shop consumables easy to underestimate. Individually, they look like minor purchases. Together, they form the daily operating layer between a stocked shop and a stalled one. When no one has a dependable count, ordering becomes a cycle of emergency runs, overbuying familiar items, and discovering shortages only after the job is already set up.

    A useful inventory system does not need to behave like a warehouse platform. For many welding and fabrication shops, it needs to do a few basic things consistently: identify the item, record what is physically on hand, define when attention is required, show what should be reviewed for reorder, and preserve enough usage history to spot a pattern.

    The physical count remains the truth

    Usage logs are helpful, but welding shops are messy places for perfect transaction data. A contact tip gets handed to another booth. A sleeve of electrodes moves to a field truck. Abrasives are pulled during second shift and entered later—or not at all. If every missed entry automatically changes the official count, the spreadsheet becomes confidently wrong.

    A better small-shop approach is to keep the physical count authoritative. Use logged usage to understand velocity and forecast pressure, then reconcile the master quantity through an actual count. That separation makes the forecast useful without pretending the log captured every movement.

    A reorder point is a decision trigger

    A reorder point is not the same as an automatic purchase order. It is the quantity that tells someone to stop and review the item. The right threshold depends on usage, supplier lead time, package quantity, job requirements, storage limits, and the cost of being wrong.

    For a steady-use item with a dependable supplier, the threshold may be simple. A specialized torch component or PPE item with a long lead time deserves more margin. A useful reorder list should bring those decisions together: current count, reorder point, suggested quantity, estimated cost, preferred supplier, and the person responsible for approving the purchase.
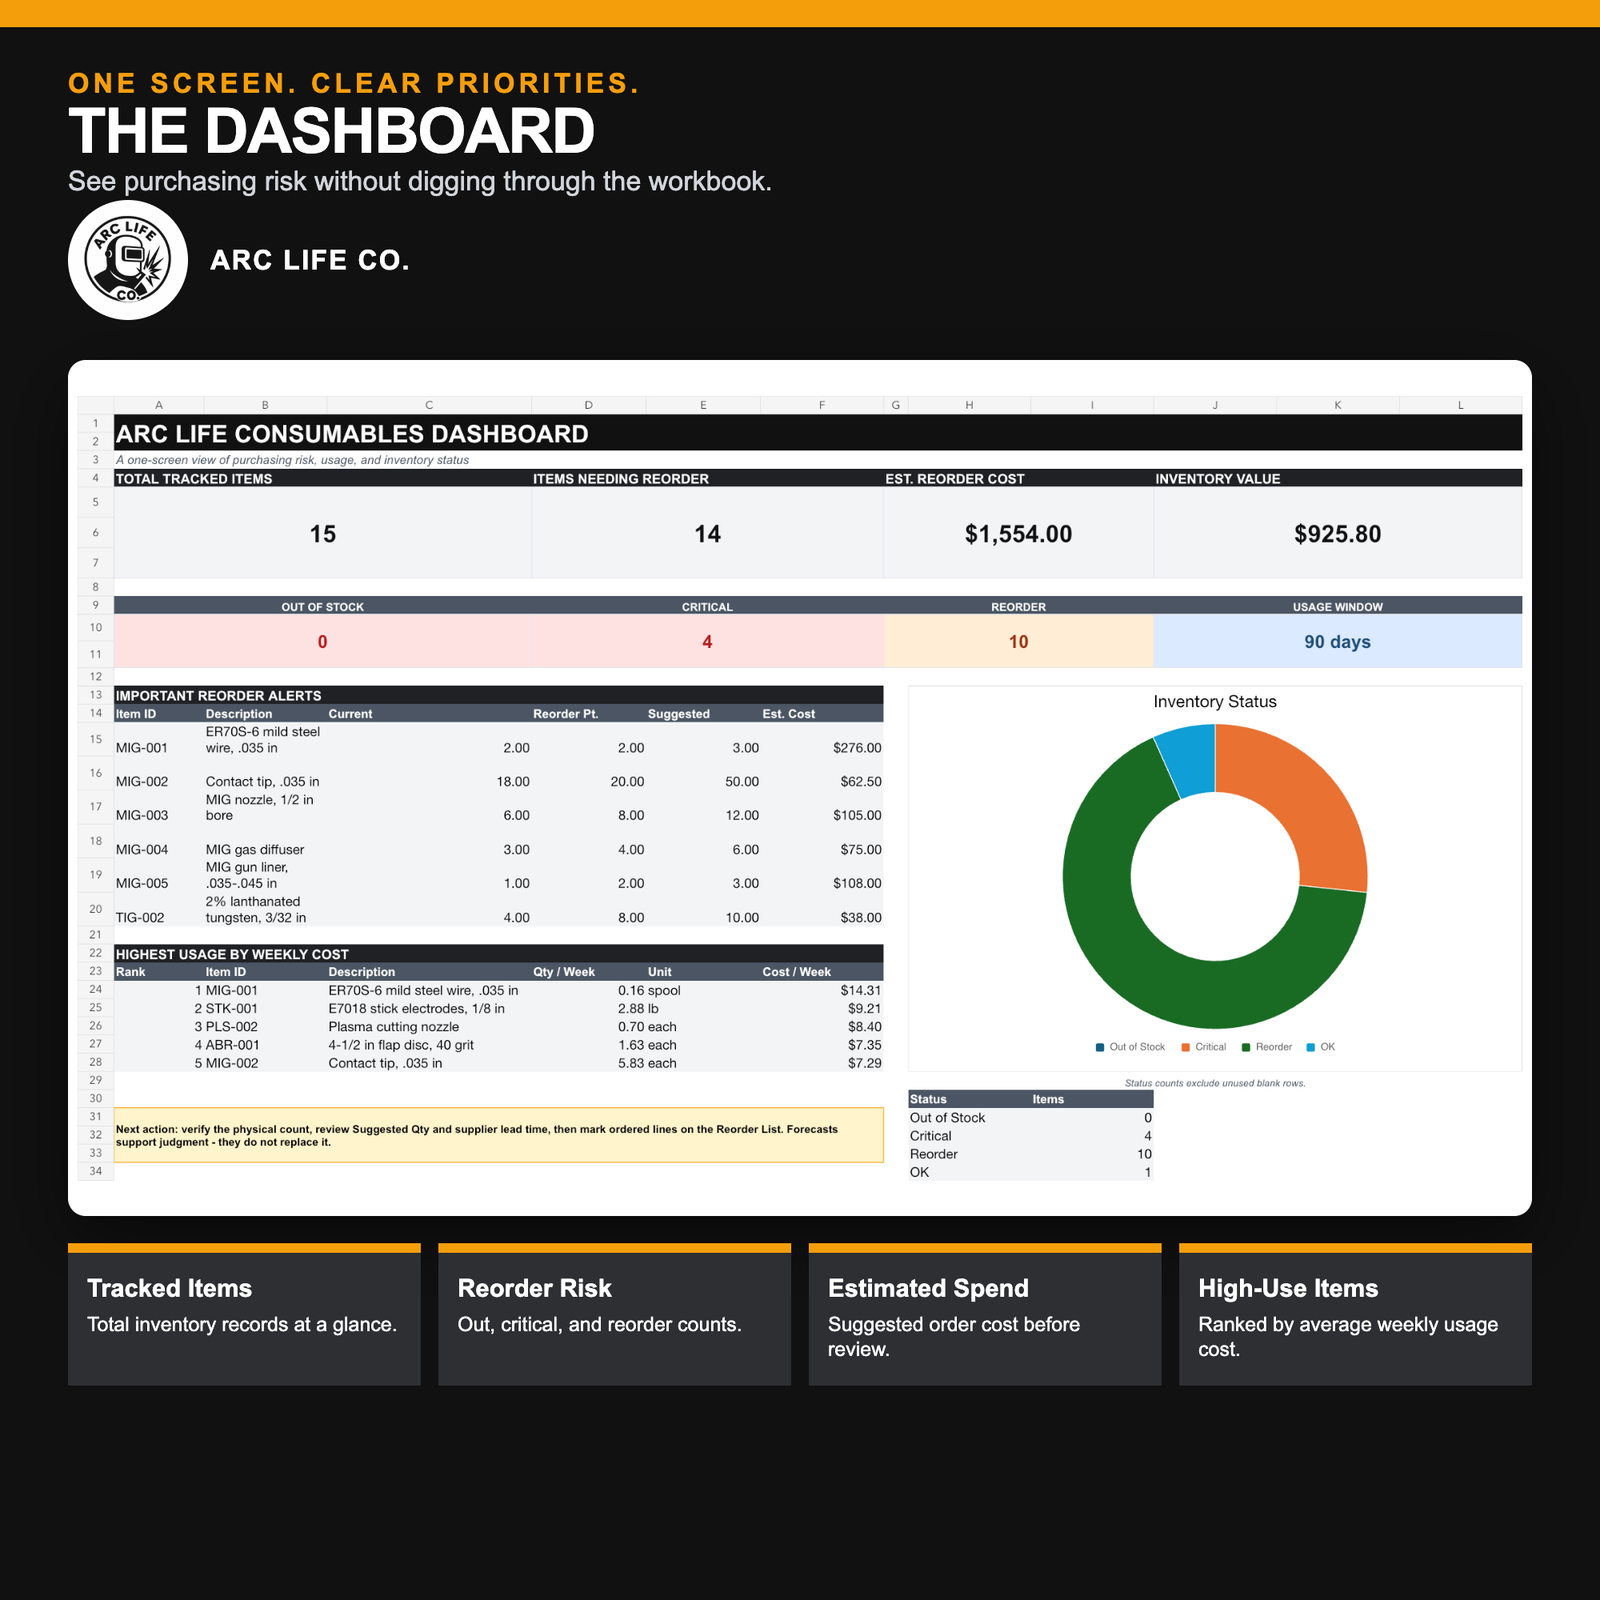
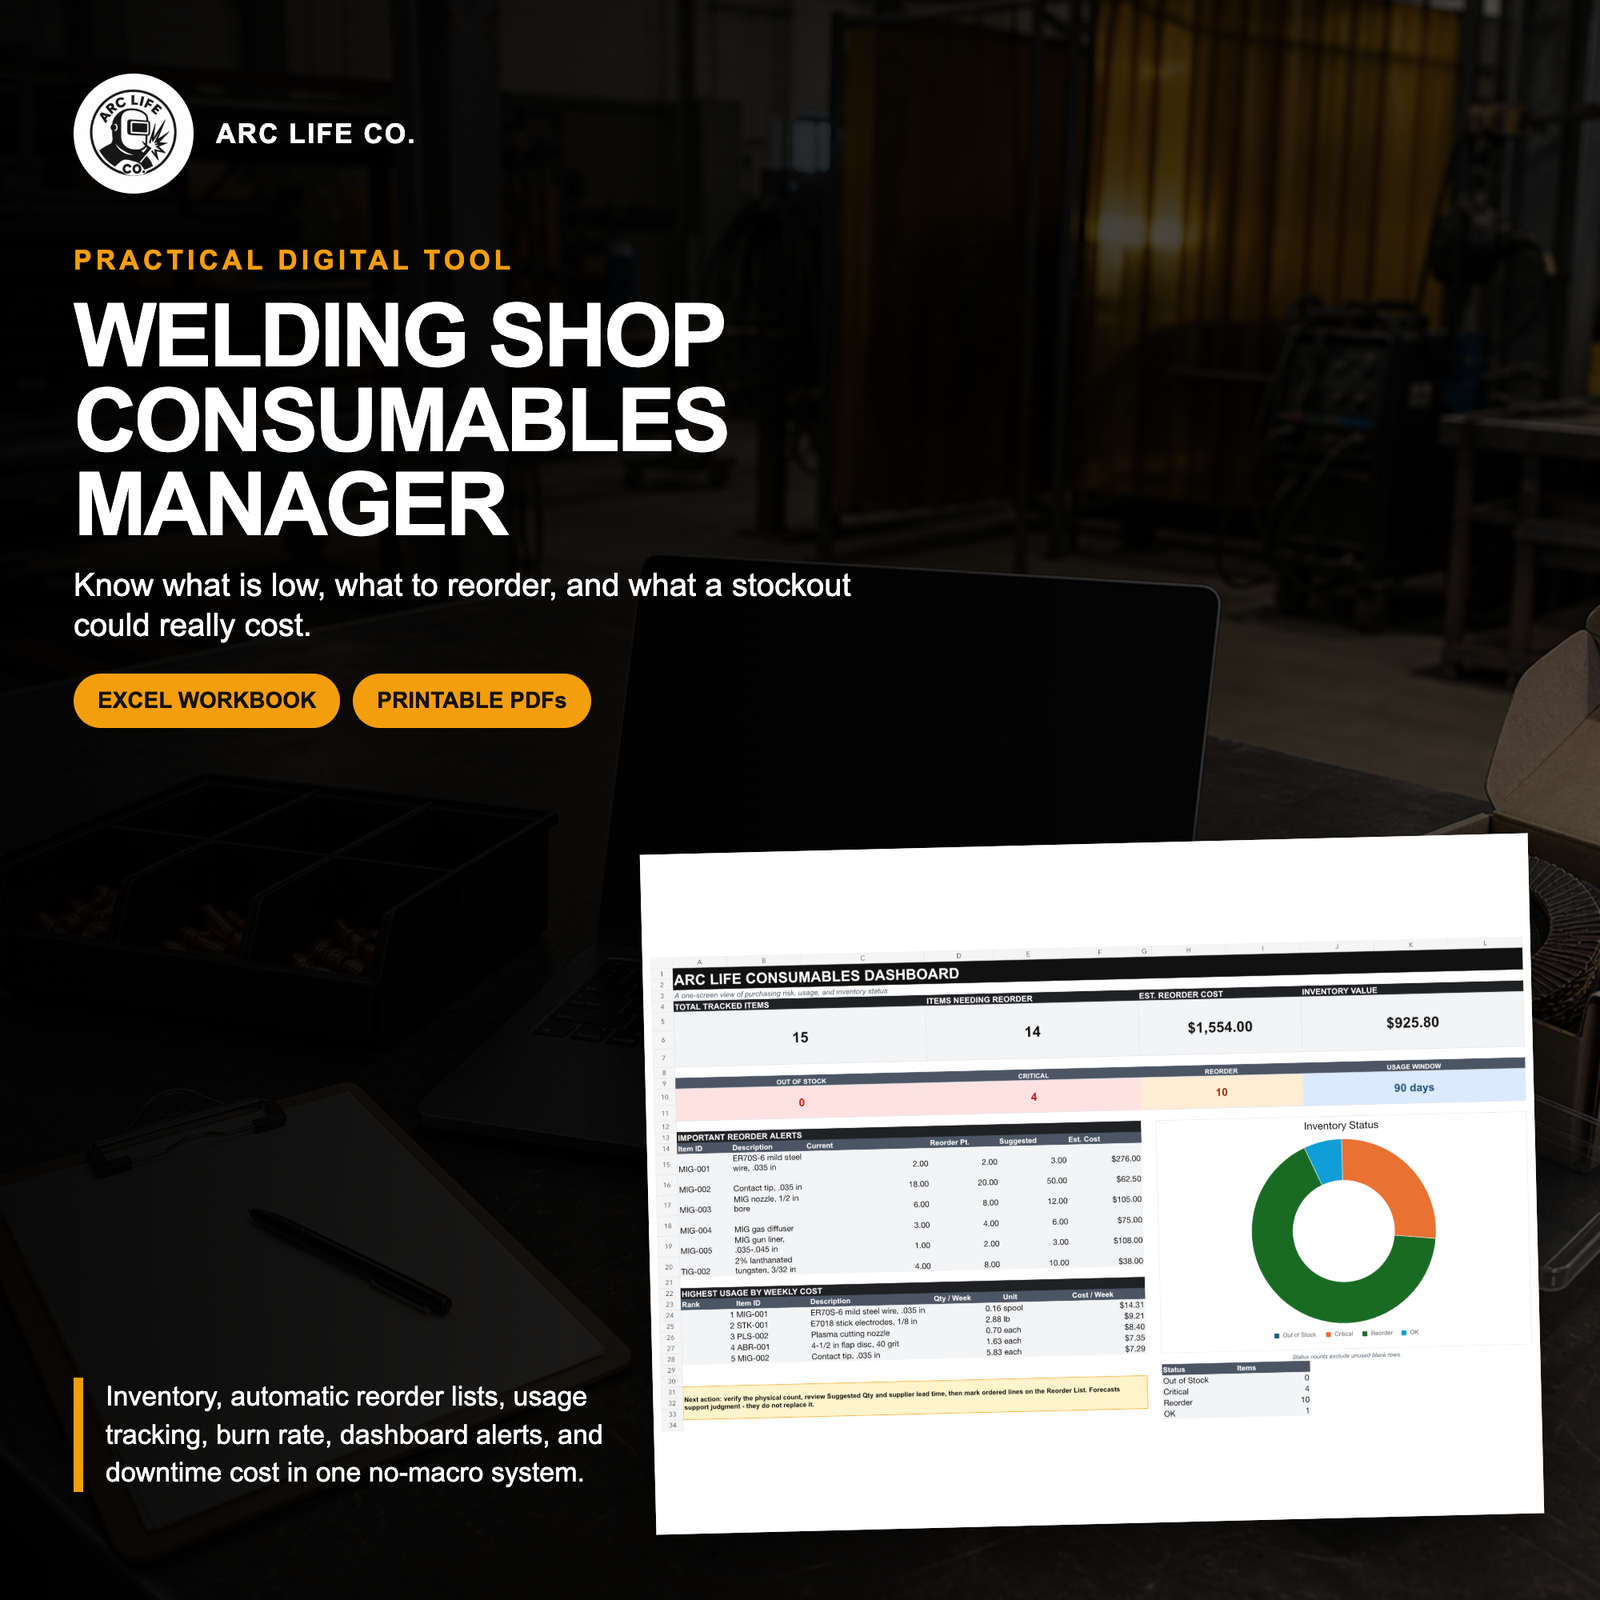
    Arc Life welding shop consumables dashboard showing reorder alerts, estimated spend, inventory status, and high-use items
    The dashboard turns count and usage records into a short purchasing-risk review; it does not place or approve an order.

    Burn rate is useful when it stays humble

    Average weekly usage can help identify items that deserve closer attention. It can also estimate how many days of stock may remain. Those numbers are planning signals, not promises. A rush job, a new operator, a process change, scrap, or an incomplete log can shift the result quickly.

    The same restraint applies to downtime estimates. Multiplying labor and production exposure by the hours lost can make a cheap stockout visible to management. It does not turn the estimate into an accounting entry. The point is to compare the cost of reasonable stock with the operational consequence of having none.

    One review beats five emergency messages

    The process works best when it has a cadence. Count the critical items, review anything at or below its reorder point, verify suggested quantities and supplier details, mark what has been ordered, and check high-use items for unusual movement. A ten-minute review on a fixed day is more dependable than waiting for five people to report shortages in five different ways.

    That review should include more than filler metal and torch parts. Plasma consumables, abrasives, PPE, gas-handling accessories, shop chemicals, saw blades, and other recurring items all compete for attention. The useful categories are the ones that match the way the shop actually buys, stores, and uses material—not the categories that look neat in a template.

    A practical starting system

    The Arc Life Welding Shop Consumables Manager is an Excel-based system designed around that small-shop workflow. It includes a master inventory, reorder list, usage log, burn-rate analysis, downtime cost calculator, dashboard, setup lists, a quick-start guide, and five printable forms. It uses standard formulas and contains no macros. The current workbook supports up to 200 recurring consumables.

    It deliberately does not subtract every logged use from the official count, connect to suppliers, create purchase orders, or place orders. Those limits matter. The physical count remains authoritative, and a person still verifies the unit, quantity, price, supplier, and purchasing decision before acting. Excel 2019 or later is recommended because other spreadsheet applications may alter formulas, charts, validation, or print settings.

    The value is not that the workbook “knows” what to buy. It gives the shop one place to see what is low, what is moving, and what deserves a decision before the next shift starts looking for a part that should have been on the shelf.

    Shop question: Which low-cost consumable has caused the most expensive interruption in your shop?

    See both shop-management systems in the Arc Life Digital Tools collection.
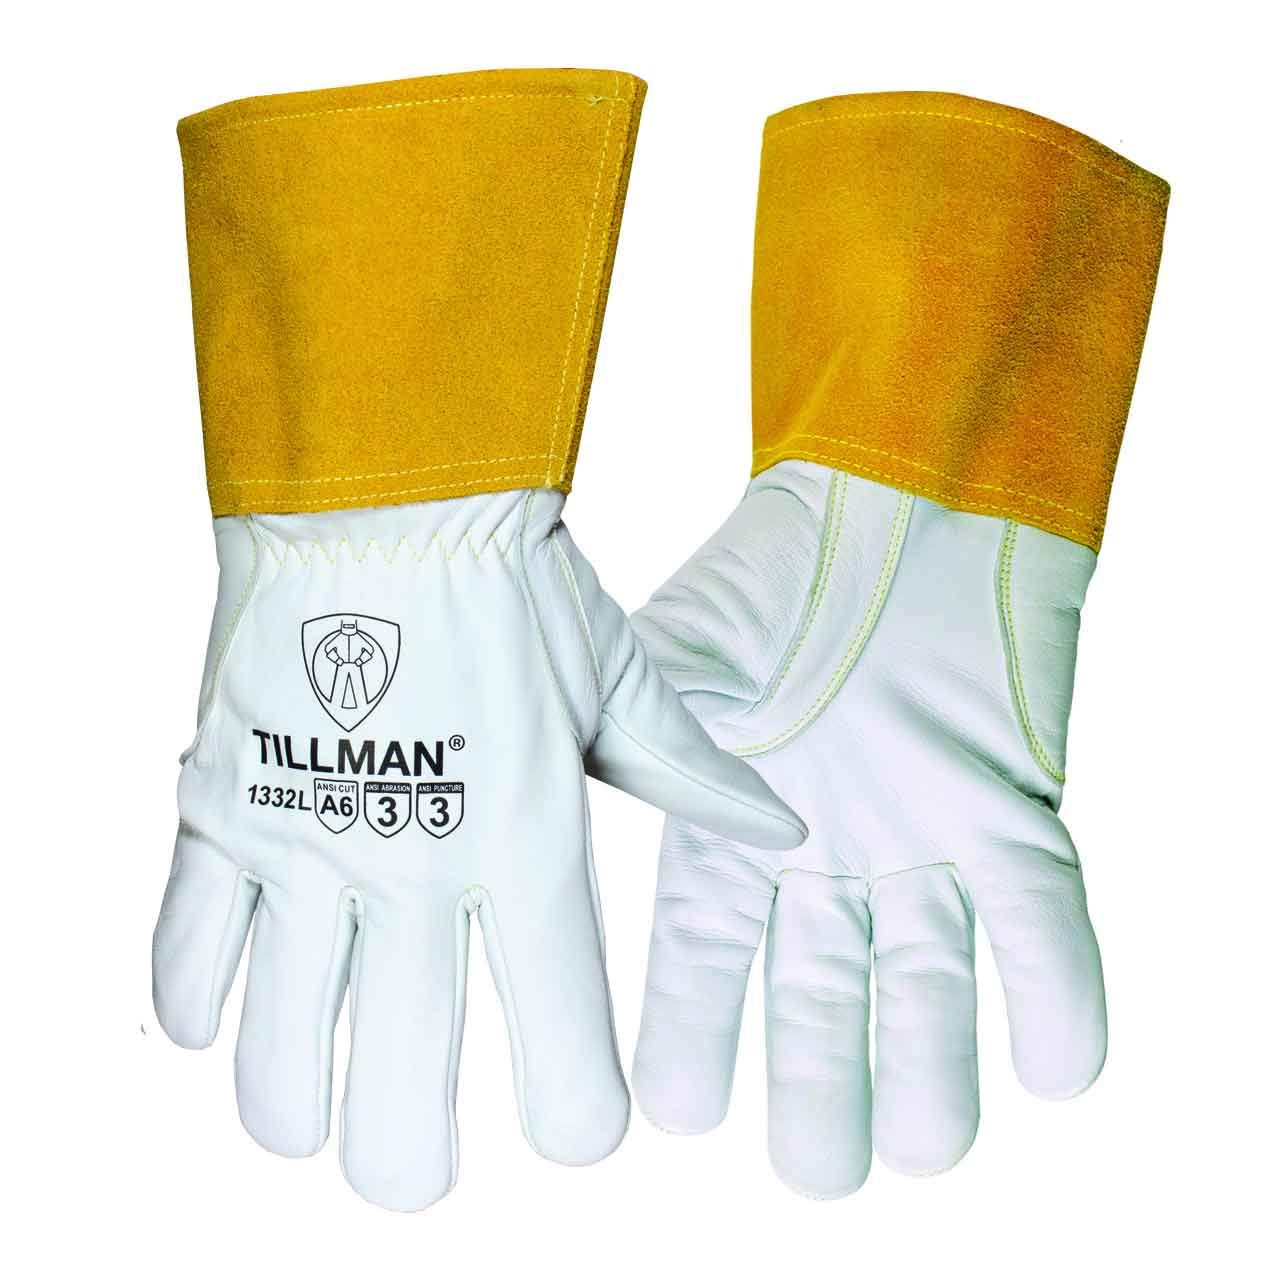
  • Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large: Product Breakdown

    Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large: Product Breakdown

    Product not found.
    “>Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large

    The Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large are positioned for welders who need a glove that supports fine control during TIG work while adding a higher level of cut protection for handling sharp material. For shops that move between setup, fit-up, light fabrication, and torch work, the practical question is not just whether the glove feels good in hand. It is whether the glove helps reduce cuts, supports grip, and still lets the user feel the work.

    This breakdown stays focused on what matters in the shop: fit, dexterity, cut resistance, use-case fit, and what to check before putting the gloves into rotation. Some technical details are not confirmed in the provided source material, so those are marked Unknown (Verify).

    Key Takeaways

    • Premium goatskin is selected for softness and flexibility, which supports fingertip control during TIG work.
    • ANSI/ISEA 105 A6 cut resistance is a meaningful indicator for handling sharp sheet edges and fabricated parts, but it does not make the glove cut-proof.
    • Large size may improve comfort for some users, but fit should be checked at the fingers, palm, and cuff before production use.
    • This glove is best viewed as a TIG support glove for handling and setup tasks, not as a replacement for task-specific PPE where higher heat or impact exposure exists.

    What the Glove Is Built to Do

    Based on the provided product description, the Tillman 1332 is intended to balance dexterity with cut resistance. That matters in TIG environments because the operator often handles sharp coupons, tacked assemblies, clamps, filler rod packaging, and sheet material before the arc is ever started. A glove that is too bulky can slow fit-up and reduce control. A glove that is too light may expose the hand to edge cuts during handling.

    Premium goatskin is commonly used where softness and tactile feel matter. In practical terms, that can help with torch handling, small part manipulation, and general shop work. The cut-resistance claim is the main differentiator here. ANSI/ISEA 105 A6 indicates a high cut-resistance level relative to lower-rated gloves, but it should still be treated as a risk reduction feature, not a guarantee.

    Practical Check, Inspect, Verify Steps

    Before assigning these gloves to a welder or fabricator, use the following checks.

    Check

    • Check glove size against the user’s hand. Large should not collapse at the fingertips or create excess material in the palm.
    • Check whether the glove allows normal torch grip, trigger control, and filler rod handling without forcing the wrist into an awkward angle.
    • Check whether the work includes frequent handling of sharp edges, burrs, or sheet metal where cut resistance is relevant.

    Inspect

    • Inspect stitching, seams, and finger gussets before first use.
    • Inspect the palm and fingertips for weak spots, finish defects, or early wear.
    • Inspect for contamination from oil, grinding dust, or metal fines that could affect grip.

    Verify

    • Verify the glove meets the internal task requirement for the job. If the job includes heavy heat exposure, grinding sparks, or severe abrasion, Unknown (Verify) if this glove is the correct PPE choice.
    • Verify the cut hazard present at the workstation. A6 helps, but the user still needs safe handling methods.
    • Verify local PPE rules, supervisor approval, and task-specific risk assessment before broad rollout.

    Troubleshooting and Support Considerations

    If a user reports that the glove is not performing well, start with the work conditions rather than the glove alone.

    If dexterity feels too low

    • Check whether the glove is the correct size.
    • Inspect for excessive break-in stiffness or contamination.
    • Verify whether the task requires finer control than a cut-resistant glove can comfortably support.

    If cut protection still appears inadequate

    • Check the actual hazard: sharp edges, burrs, or unfinished parts can exceed the user’s handling technique.
    • Inspect the glove for wear through the fingertips or palm.
    • Verify whether a different control method, part deburring step, or higher-protection PPE is needed.

    If grip is inconsistent

    • Check for oil, coolant, or fine dust on the glove surface.
    • Inspect whether the material is worn smooth from repeated handling.
    • Verify that the glove is being used for the right task; a glove designed for TIG support may not suit wet or heavily abrasive conditions.

    Product and Parts Notes

    This draft is based on the provided ArcWeld product listing for the Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large. The available description indicates premium goatskin construction and ANSI/ISEA 105 A6 cut resistance. Other technical details such as liner content, cuff style, insulation, and heat-rating claims are Unknown (Verify) because they were not supplied in the source material.

    Use the product page as the primary reference when confirming whether the glove is suitable for a given TIG workflow, especially if the user is selecting gloves for production work, maintenance outages, or repetitive handling of cut metal.

    Related product reference:

    Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large

    Tillman 1332 Premium Goatskin TIG Gloves with ANSI A6 Cut Resistance, Large

    The Tillman 1332 Premium Goatskin TIG gloves are built for welders who need a balance of dexterity and serious cut protection during TIG setup, handling sharp material, and light fabrication work. Made with premium goatskin for a soft, flexible feel, these gloves are designed to maintain fingertip control while adding ANSI/ISEA 105 A6 cut resistance to help reduce risk when working around sheet metal edges and bur…

    View at Arc Weld Store

    For users comparing glove styles, the internal article below may help as a related reference point for goatskin glove construction in TIG or MIG support work:

    How Maintenance Buyers Should Evaluate This Glove

    Maintenance buyers should treat this glove as a task-specific hand protection option for light fabrication, TIG setup, and material handling where cut resistance matters. The first filter is the actual hand hazard at the jobsite. If the main risk is sharp edges, the A6 rating is relevant. If the main risk is thermal exposure or heavy abrasion, additional review is needed.

    Use a short pilot test with real users. Ask three things: does the glove fit correctly, does it preserve torch control, and does it reduce nuisance cuts during handling? Those answers are more useful than a catalog description alone.

    Safety Notes

    • Cut-resistant gloves reduce risk; they do not eliminate it.
    • Keep hands away from sharp edges, moving parts, and hot surfaces.
    • Do not assume a TIG glove is suitable for grinding, heavy heat, or every fabrication task.
    • Replace gloves that show wear, seam damage, or loss of dexterity.
    • Follow site PPE rules and task hazard analysis before use.

    FAQ

    Is the Tillman 1332 glove meant only for TIG welding?

    No. Based on the source description, it is best suited for TIG support work and handling tasks where dexterity and cut resistance matter. Exact task limits are Unknown (Verify).

    Does ANSI A6 mean the glove is cut-proof?

    No. ANSI/ISEA 105 A6 means the glove has a high cut-resistance level, but sharp edges and improper handling can still cause injury.

    Can this glove replace general welding PPE?

    No. It should be evaluated as one part of the PPE program. Other hazards such as heat, sparks, abrasion, and impact may require different protection.

    What should I verify before buying for a crew?

    Verify fit, task compatibility, and site PPE requirements. Also verify whether users need more heat resistance or more abrasion resistance than this glove is intended to provide.

    Sources Checked

    Note: No WSP lookup page or filler metal finder page was provided for this draft. No assumptions were made about certifications, compatibility, pricing, or availability.

    Related Weld Support Guides

  • Tillman 1477 TrueFit Cut Resistant Premium Goatskin Performance Gloves, Large: Replacement Part Breakdown

    Welders and maintenance buyers do not need marketing language when selecting gloves. They need a glove that fits, holds up to the task, and is replaced before wear becomes a safety problem. The Tillman 1477 TrueFit Cut Resistant Premium Goatskin Performance Gloves, Large, should be evaluated the same way: by fit, stitch integrity, palm wear, finger wear, and whether the glove still supports the job without reducing dexterity.

    This guide is a practical breakdown for inspection, replacement, and support decisions. It does not assume performance beyond what is verifiable from the product listing. Where technical details are not confirmed here, they are marked Unknown (Verify).

    Key Takeaways

    • Check fit first. A glove that is too loose can reduce grip control and catch on edges.
    • Inspect goatskin wear points before every shift: fingertips, thumb crotch, palm, and seams.
    • Replace gloves when liner exposure, seam opening, or palm thinning affects safe use.
    • Do not assume cut resistance equals protection from all hazards. Confirm the glove is appropriate for the task.
    • Use the product listing as a starting point for selection, then verify size and task fit in the field.

    Product and Part Breakdown

    The product identified for this guide is the Tillman 1477 TrueFit Cut Resistant Premium Goatskin Performance Gloves, Large, ASIN B08BSTWP7P. The listing name indicates a goatskin performance glove with cut-resistant construction, but detailed construction data such as liner material, reinforcement pattern, cuff length, and certification status are Unknown (Verify) from the information provided here.

    For maintenance buyers, the important part is not just the glove name. It is whether the glove matches the work envelope. Verify the following before placing into service:

    • Size: Large, as listed.
    • Hand fit: full finger reach without excess slack at fingertips.
    • Grip: dry-hand and tool-hand contact with no rolling in the palm.
    • Dexterity: ability to hold small consumables, torch leads, hand tools, and fasteners.
    • Coverage: verify cuff and wrist coverage for the specific job.

    If you need a product reference for the listing, use the approved product shortcode:

    No products found.

    . Do not use that as a substitute for inspection or task verification.

    Check, Inspect, Verify: Pre-Use Routine

    Check the glove condition before the shift starts. Look for dirt buildup, embedded metal splatter, cuts, and stiffness that can limit hand movement.

    Inspect the high-wear zones closely:

    • Fingertips for pinholes, split seams, or worn-through leather.
    • Thumb crotch for tearing from repeated clamp, rod, or tool handling.
    • Palm surface for thinning, glazing, or cracking.
    • Seams along the fingers and back of hand for opening stitches.
    • Cuff and wrist area for fraying or edge damage.

    Verify the glove still matches the job. If the glove is intended for welding support, confirm that the current task does not require a different glove type, longer cuff, or higher heat protection. Unknown (Verify) whether this glove is suited for direct welding arc exposure, heavy spatter, or prolonged high-heat contact. Do not assume.

    Troubleshooting Support for Wear and Fit Problems

    Problem: glove feels loose at the fingers.
    Check whether the glove is oversized or stretched from use. Inspect for material softening and finger tip collapse. Verify that the user can still handle fasteners and torch controls without excess movement.

    Problem: grip feels slick.
    Inspect the palm surface for oil, coolant, grinding dust, or wear glazing. Clean the glove only if the care method is allowed by the manufacturer. If grip remains poor after cleaning, replace the glove.

    Problem: seam failure starts at the thumb or palm.
    Check for repetitive torque loads, tool carry habits, and pinch points. Verify whether a different glove style or reinforcement pattern is required. If the seam has opened, the glove is out of service.

    Problem: glove still looks usable but comfort dropped.
    Inspect for internal lining bunching, hardening from contamination, or shrinkage from cleaning or heat exposure. Verify whether the glove still allows full hand closure. Loss of comfort often shows up before visible failure.

    Replacement Decision Rules

    Replace the glove when any of the following are true:

    • There are holes, split seams, or exposed inner layers.
    • Leather has thinned enough that protection is reduced.
    • Finger movement is restricted by hardening or deformation.
    • Contamination cannot be removed and affects grip or handling.
    • The glove no longer fits the worker safely.

    For buyers managing stock, standardize replacement based on condition, not calendar time alone. A glove used for sharp edges, abrasive handling, or frequent tool contact will wear out faster than a glove used for light support tasks.

    How to Evaluate Before Buying

    Before placing this glove in a cart, verify three things: task fit, size fit, and replacement rhythm. Task fit means the glove suits the actual work. Size fit means the Large size works for the intended user without reducing control. Replacement rhythm means the glove can be inspected and removed from service before damage reaches the hand.

    If you are comparing this product to another Tillman glove style, use the related internal reference for context only: Tillman 48 MIG Gloves Review: Goatskin Fleece Comfort. That article is a separate product reference and should not be treated as a compatibility match for this glove.

    Safety Notes

    • Do not use damaged gloves for sharp-edge handling, hot work, or general shop tasks.
    • Verify the glove type against the hazard before use. Cut-resistant does not mean cut-proof.
    • Keep gloves free of oil and grinding residue where possible.
    • Remove from service if stitches open or leather is worn through.
    • Do not rely on a glove listing alone for compliance decisions.

    FAQ

    Is the Tillman 1477 suitable for welding?
    Unknown (Verify). The product name suggests performance use and cut resistance, but direct welding suitability, heat resistance, and spatter performance are not confirmed here.

    What should buyers check first on arrival?
    Check size marking, inspect seams, and verify that the glove has no shipping damage, contamination, or obvious manufacturing defects.

    When should the glove be replaced?
    Replace it when leather thins, seams open, holes appear, or fit changes enough to reduce control.

    Can this glove be treated as a universal shop glove?
    No. Verify the task. Different jobs may require different levels of dexterity, coverage, or thermal protection.

    Sources Checked

    • Provided Amazon product reference for Tillman 1477 TrueFit Cut Resistant Premium Goatskin Performance Gloves, Large, ASIN B08BSTWP7P
    • Provided internal link: Tillman 48 MIG Gloves Review: Goatskin Fleece Comfort

    This guide is intended as a field-use buying and inspection reference. Confirm any uncertain construction or performance details directly from the current product listing or manufacturer documentation before purchase or issue.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • What the Lunchbox Knows About a Welding Shift

    What the Lunchbox Knows About a Welding Shift

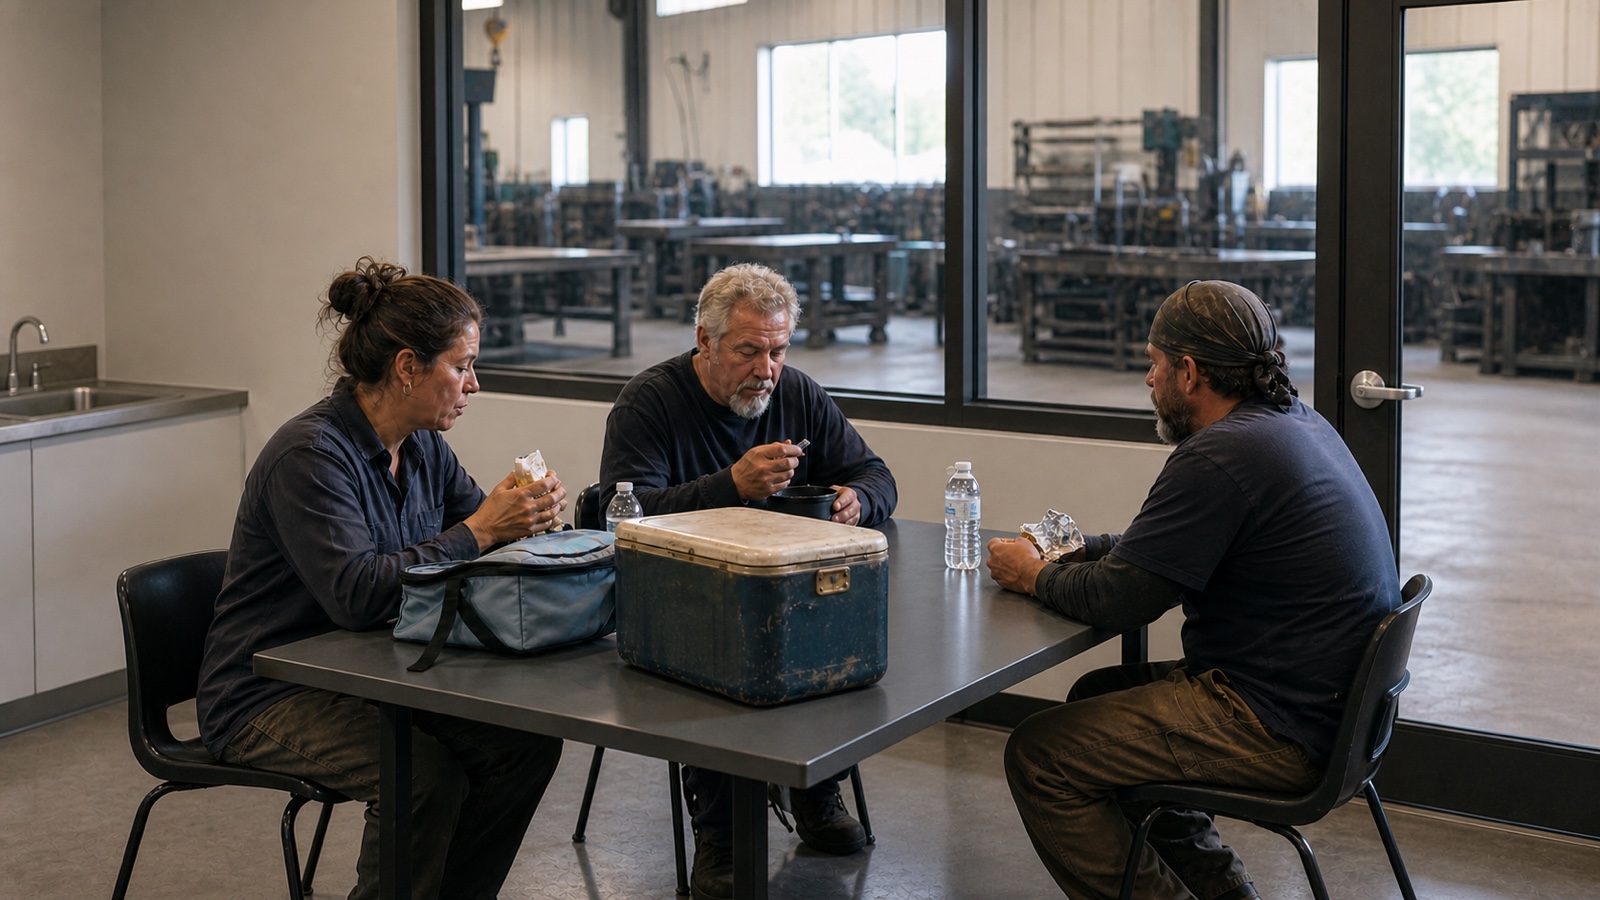
    Before the hood goes down, before a machine gets turned on, before the first piece of steel moves across the table, a lunchbox usually gets parked somewhere.

    It might be a hard cooler with one good hinge left, a soft bag wedged behind the truck seat, or a plain grocery sack in the break-room refrigerator. It is not the most impressive object in the shop. Nobody asks what amperage it can handle. Nobody compares duty cycles. Still, that lunchbox can tell you a surprising amount about the shift ahead.

    A long day requires more than skill. It requires enough fuel, a place to reset, and a routine that can survive changing jobs, weather, overtime, and the occasional schedule that falls apart before 9 a.m. The lunchbox belongs to that less visible side of welding—the part that keeps the person behind the hood ready for the next pass.

    A Small Piece of the Day You Can Control

    Shop work is full of variables. Material arrives late. Fit-up takes longer than the drawing suggested. A repair reveals another problem underneath. The next department needs the part sooner than expected. Even a well-run day can turn quickly.

    Packing a lunch is a modest counterweight to all that. It is one part of the shift decided before the first interruption. The food may be simple, but the act of bringing it says something practical: this day will ask for energy, and somebody thought ahead.

    That kind of preparation is not glamorous. Neither is laying out extra gloves, checking consumables before a job, or filling a water bottle before the heat builds. Trades run on hundreds of ordinary decisions made before they become urgent. The lunchbox fits naturally among them.

    There is also no single “welder’s lunch.” A night-shift fabricator, a pipe hand moving between sites, an instructor with twenty students, and a maintenance welder waiting on a shutdown all work different days. Some people pack carefully. Some grab whatever can be eaten in ten minutes. Some carry enough for unexpected overtime because experience has taught them that the promised quitting time is only a proposal.

    The common thread is not what is inside. It is that the bag has been packed for the reality of the work.

    Break Time Has Its Own Shop Language

    The break area is one of the few places where the crew can see each other without a helmet, face shield, screen, or machine between them. The conversation changes there.

    Sometimes it is shop talk: a strange print, a stubborn fit, a better way to stage the next assembly. Sometimes it has nothing to do with welding. There are ball scores, home projects, fishing reports, family logistics, and the kind of running jokes that would make no sense outside one particular crew.

    That pause matters even when nobody says much. Sitting down for a few minutes can be a reset after a noisy morning. The apprentice who has been concentrating hard gets a chance to breathe. The experienced hand who has answered questions all shift gets a quiet minute. People who work different processes or stations share the same table.

    The break does not erase rank, responsibility, or pressure. It does reveal the people carrying them. That is part of how a workplace turns into a community instead of a collection of job titles.

    Keep the Lunch Away From the Work

    There is one boundary worth stating plainly: the lunchbox does not belong beside the welding table, grinding dust, coatings, chemicals, or other contamination.

    OSHA’s general-industry sanitation standard says food and beverages cannot be consumed or stored in areas exposed to toxic material. The same standard requires potable water for drinking and washing, sanitary washing facilities, and appropriate waste containers where employees eat. A designated clean area is not a fussy extra. It separates lunch from the dirt and hazards the job creates.

    The practical version is familiar: wash up, leave contaminated gloves and work gear out of the eating area, and keep food and drink protected. The shop can be gritty without putting grit in somebody’s sandwich.

    The Marks on the Outside Tell a Story Too

    Lunchboxes age like other working objects. Corners wear white. Zippers get replaced with wire rings or short pieces of cord. Names are written in marker because three people bought the same model. Stickers fade. Handles get repaired instead of admired.

    None of that makes the cooler sacred. It does make it recognizable.

    A bag that has ridden to the same plant for five years carries a different kind of history than a welding hood or a favorite square. It has been present for early starts, long shutdowns, first days, last days, and the shifts that were completely ordinary. It may have held a note from home, an extra snack for a coworker, or the last cold drink at the end of a hot afternoon. Those details rarely make the job report, but they belong to the working life all the same.

    The trade is often represented by its loudest moments: bright arcs, heavy steel, sparks, cranes, and finished structures. The lunchbox is a reminder that the work is also built around quieter things—planning ahead, taking care of yourself, sharing a table, and getting ready to go back out there.

    Packed for the Next Half

    After break, lids close and chairs scrape back. The crew separates. Hoods come down again. Machines start. Whatever was difficult before lunch is probably still waiting.

    But the second half of the shift begins with a little more fuel and, on a good day, a clearer head.

    That is the question for the Arc Life community: what is the one thing that always earns a place in your lunchbox on a long welding shift? Not the ideal answer—the real one. The dependable sandwich, the giant water bottle, the hot sauce, the piece of fruit that sometimes makes it home untouched, or the backup snack reserved for overtime.

    Arc Life pays attention to the whole working life, not only the moment the arc is lit. Read more about the people and purpose behind the brand on About Arc Life, or explore the current Arc Life collection.

    Source

  • Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack: Product Breakdown

    Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack: Product Breakdown

    Product not found.
    “>Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack

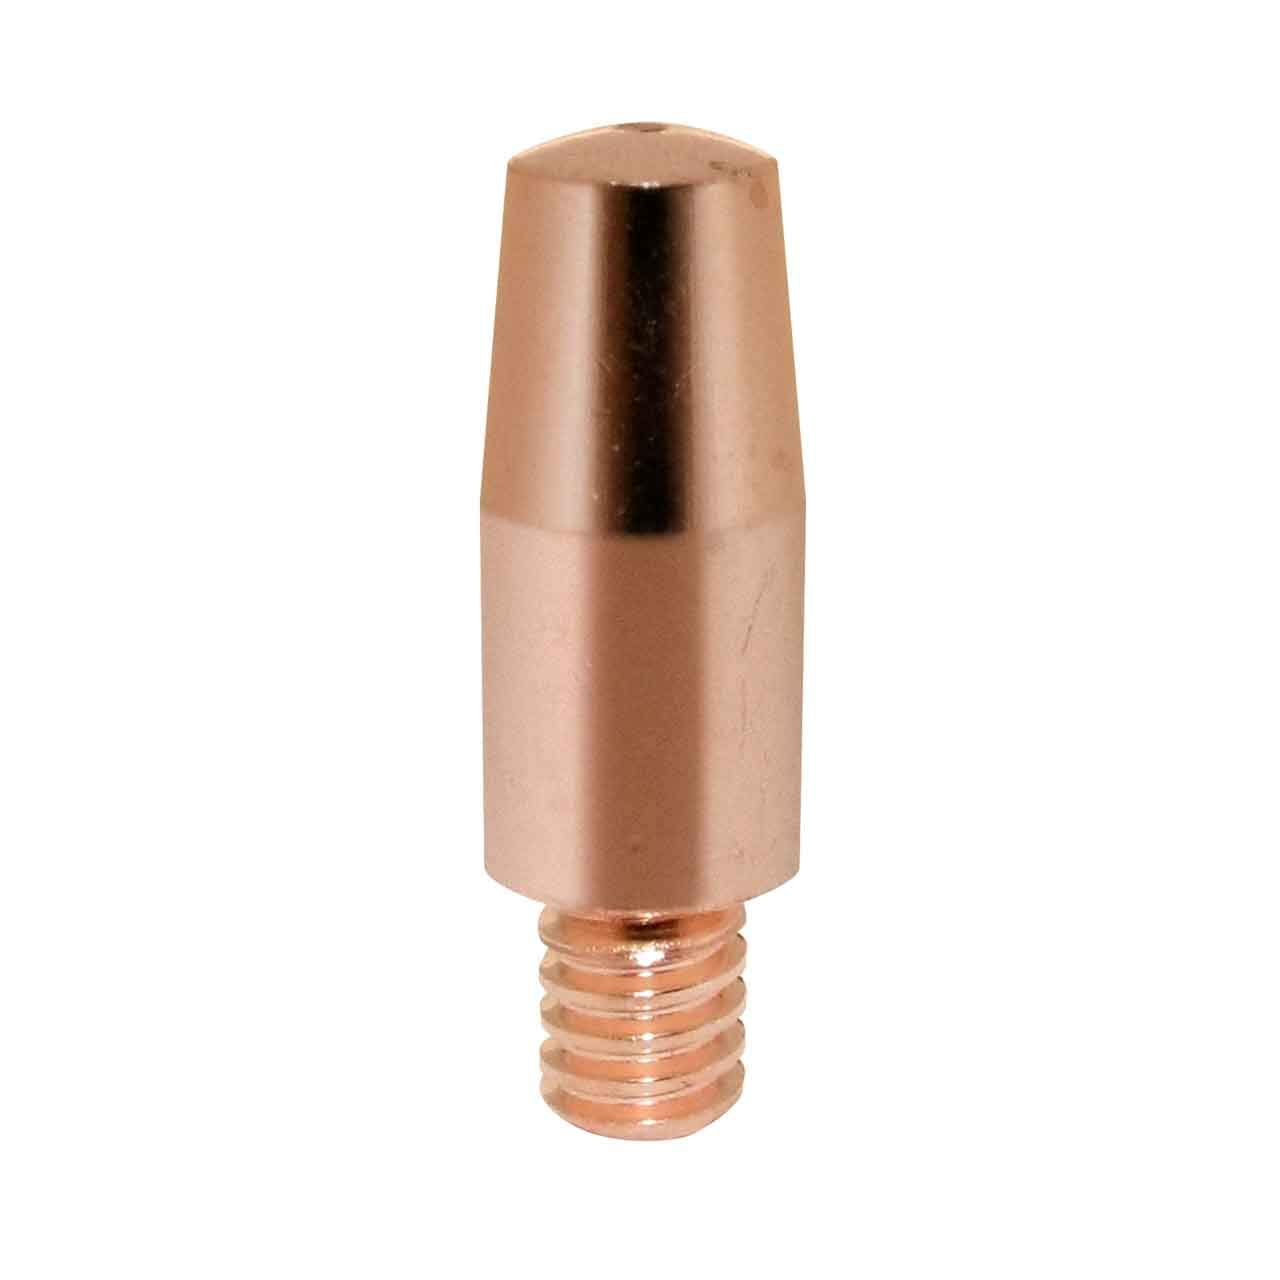
    The Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack is a MIG consumable used to transfer current to the electrode wire at the gun front end. For buyers and maintenance teams, the main job is simple: keep the wire feeding smoothly and maintain a stable electrical path. When a contact tip is the wrong size, worn, or contaminated, the result is usually inconsistent arc behavior, feeding drag, or premature tip failure.

    This breakdown stays focused on what to check before you buy, install, or troubleshoot this tip in service. The listing indicates a 350A rating and .040 in (1.0 mm) wire size. Any other fit or application detail should be treated as Unknown (Verify) unless confirmed by your torch, gun, and OEM documentation.

    Key Takeaways

    • The KP2744-040 is a standard MIG contact tip for .040 in (1.0 mm) wire.
    • Contact tips are wear items. Plan inspection and replacement as part of routine gun maintenance.
    • Stable performance depends on correct wire diameter, correct tip seating, and clean current transfer surfaces.
    • Do not assume compatibility with every gun, neck, diffuser, or gas nozzle. Verify part match before installation.

    What a Contact Tip Does

    A contact tip serves two functions. First, it conducts welding current into the wire. Second, it constrains wire guidance at the point where the arc starts. If the internal bore is oversized, worn, or distorted, the wire can wander and the arc can become erratic. If the bore is undersized or contaminated, wire feed drag rises and the wire may bind.

    For production and repair welding, the practical goal is not just arc starts. It is repeatable current transfer over time with minimal interruption. That means the tip condition matters as much as the wire size printed on the package.

    Check Before You Install

    1. Check wire diameter. Verify the feeder is loaded with .040 in (1.0 mm) wire. Do not rely on setup memory. Read the spool label and measure if needed.
    2. Inspect the gun front end. Verify the diffuser, nozzle, and tip adapter threads are clean and not cross-threaded.
    3. Inspect the old tip. Look for burnback, spatter bridging, oval wear, or blue heat discoloration. These are signs of poor current transfer or excessive heat load.
    4. Verify seating. The tip should install fully and seat squarely. If it rocks, binds, or bottoms out incorrectly, stop and verify the torch parts.
    5. Confirm the part number. Match the replacement tip to the gun system and consumable family in the OEM reference. Unknown (Verify) if the torch family is not documented.

    Inspect During Service

    Routine inspection prevents avoidable downtime. A quick daily check is enough for many shops, with more frequent checks in high-duty production cells.

    • Inspect the bore: Look for ovaling, enlarged entry, or visible erosion at the wire path.
    • Inspect the face: Look for spatter buildup that can change wire exit geometry.
    • Inspect the threads: Look for galling, damaged starts, or evidence that the tip has been over-tightened.
    • Inspect the wire feed: Verify the wire exits without hesitation when jogging the feeder.
    • Inspect arc starts: Note hard starts, wandering starts, or intermittent loss of conductivity.

    Troubleshooting Support

    If the weld system is not behaving normally, the contact tip is one of the first consumables to verify. Use a simple check/inspect/verify sequence.

    Problem: Wire feed hesitation

    • Check: Does the wire drag at the gun front end?
    • Inspect: Look for tip bore damage, spatter blockage, or a wire size mismatch.
    • Verify: Confirm the liner, drive rolls, and tip are all matched to the same wire size.

    Problem: Burnback at the tip

    • Check: Is the arc starting too close to the tip face?
    • Inspect: Look for worn internal bore, excessive stickout variation, or poor feed consistency.
    • Verify: Confirm procedure settings and front-end consumable condition before changing process variables.

    Problem: Unstable arc or spatter increase

    • Check: Is the tip worn, loose, or contaminated?
    • Inspect: Look for oxidation, thread damage, and tip-to-diffuser seating problems.
    • Verify: Confirm the contact tip is the correct diameter and style for the torch system.

    Product and Parts Notes

    The Lincoln Electric KP2744-040 Copper Plus Contact Tip is listed as a 350A, standard-style MIG contact tip for .040 in (1.0 mm) wire. Beyond that, any torch-family compatibility, current-duty interpretation, or service-life claim should be treated as Unknown (Verify) unless confirmed by the manufacturer or gun documentation.

    For buyers, the practical value of this type of tip is in consistency. A consistent contact tip reduces unnecessary troubleshooting time because it removes one variable from the front-end system. For maintenance teams, that means fewer false alarms when a feeding issue is really a wear issue at the tip.

    If you need to compare this consumable against a broader wire or process plan, a related internal resource may help with wire selection context: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog. Use that page as a starting point for material selection context, not as a procedure approval for this tip.

    Maintenance Buying Considerations

    For stocked spares, contact tips should be treated as high-turn consumables. Keep them organized by wire diameter and torch family. Do not mix bins or assume one .040 in tip matches every gun. That mistake causes time loss at the workbench and at the machine.

    When building a PM kit, include the tip, diffuser, nozzle, and any related front-end consumables that commonly wear together. If the root cause of tip failure is recurring, look upstream at wire cleanliness, drive roll setup, liner condition, and gun angle.

    Safety Notes

    • De-energize the welding system before changing front-end consumables.
    • Allow hot parts to cool before handling.
    • Use gloves when removing spatter-contaminated tips.
    • Do not force threaded parts. Cross-threading can damage the gun and the consumable.
    • Use approved PPE and follow your shop’s lockout and welding safety procedures.

    FAQ

    Is the KP2744-040 only for .040 in wire?
    The listed size is .040 in (1.0 mm). Use that as the primary match point. Any other wire size should be treated as Unknown (Verify).

    Can I use this tip in any MIG gun?
    No. Compatibility depends on the torch, diffuser, and thread style. Verify against the gun manufacturer’s consumable chart before installing.

    What are the first signs that the tip should be replaced?
    Watch for wire feed hesitation, burnback, unstable starts, visible bore wear, spatter bridging, and damaged threads.

    Should I replace the tip when changing wire?
    Not automatically. Inspect the tip first. Replace it if wear, sizing mismatch, or contamination is present.

    Sources Checked

    Related Arc Weld Part

    Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack

    Lincoln Electric KP2744-040 Copper Plus Contact Tip 350A .040 in (1.0 mm), 10 pack

    The Lincoln Electric KP2744-040 Copper Plus Contact Tip is a 350A, standard-style MIG contact tip engineered for consistent wire transfer and stable arc performance in high-amperage applications. Built from Lincoln’s Copper Plus material, this tip is designed to deliver reliable electrical conductivity and extended service life in production and repair environments where tip wear, spatter adhesion, and thread gall…

    View at Arc Weld Store

    Related Weld Support Guides

  • Miller 263348 Welding Gloves, 3D, Wing, 11In, White/Blue, Pack of (1 Pair): Replacement Part Breakdown

    This draft is a practical buyer guide for the Miller 263348 Welding Gloves, 3D, Wing, 11In, White/Blue, Pack of (1 Pair). Use it as a support and purchasing reference when you are matching a glove set for welding work, maintenance tasks, or general hot-work handling. The product reference in the registry is the ASIN-linked item B00I4Z44RS. Any field not confirmed in the provided source should be treated as Unknown (Verify).

    Key Takeaways

    • Use the product listing as the primary reference before you order replacements or duplicates.
    • Verify fit, cuff style, seam condition, and heat exposure needs against your job task.
    • Do not assume the listing covers every welding process or every shop condition.
    • If a glove is being replaced after damage, inspect the cause of failure first so the same issue does not repeat.

    What This Product Reference Tells You

    The provided item name identifies a pair of welding gloves in a 3D wing style, 11 in. length, white and blue colorway. The registry does not confirm material makeup, reinforcement pattern, liner details, stitch type, or heat rating. Treat those fields as Unknown (Verify) until you confirm them from the product page or packaging.

    For buyers and support teams, that means the first step is not just to order a replacement. It is to compare the glove against the task, the current wear pattern, and the actual work environment. A glove can be the wrong choice even when it matches the basic size and shape on paper.

    Check, Inspect, Verify

    Use this sequence before you issue the glove to a welder or maintenance tech:

    1. Check the task: Determine whether the glove will be used for MIG, TIG, stick, grinding, torch handling, or general hot work. If the process is not confirmed, mark it Unknown (Verify).
    2. Inspect the fit area: Confirm hand size, finger reach, cuff clearance, and how the glove interfaces with jacket sleeves or gauntlets.
    3. Verify coverage needs: An 11 in. glove may be suitable for some hand and wrist protection needs, but do not assume it is enough for every spark, slag, or splash exposure.
    4. Inspect construction: Look for loose stitching, worn palms, seam separation, heat damage, hardening, and contamination from oil or grinding residue.
    5. Verify replacement timing: Replace gloves when insulation, dexterity, or seam integrity is degraded. Do not wait for a full failure.

    Troubleshooting and Support Notes

    If the glove is not performing as expected, isolate the failure mode.

    • Problem: Reduced dexterity. Check whether the glove is too large, too stiff, or contaminated. Verify that the task does not require a thinner glove style.
    • Problem: Premature seam failure. Inspect whether the glove is being used beyond its intended duty or exposed to repeated flexing, abrasion, or sharp edges.
    • Problem: Heat discomfort. Verify whether the work produces more heat, spatter, or contact exposure than the glove can manage. Do not use comfort alone as the selection rule.
    • Problem: Wet or oily handling issues. Inspect the work area for contamination. Cleaning the glove may not restore safe performance if the structure is already degraded.

    When support teams handle glove complaints, document the task, the failure location, and the wear timeline. That record helps determine whether the issue is product selection, process change, or operator misuse.

    Product and Parts Breakdown

    This item is listed as a pair of welding gloves. No replacement sub-parts are confirmed in the provided source. For this reason, any breakdown beyond the glove pair itself is Unknown (Verify).

    • Primary item: Welding glove pair
    • Style: 3D wing, as stated in the product name
    • Length: 11 in., as stated in the product name
    • Color: White/Blue, as stated in the product name
    • Material details: Unknown (Verify)
    • Stitching and reinforcement: Unknown (Verify)
    • Heat and cut performance claims: Unknown (Verify)

    If you are building a purchasing record, keep the glove name, ASIN reference, and observed wear condition together. That makes it easier to reorder the same item or to replace it with a better-matched option later.

    Buyer Support Checklist

    • Check the work process first.
    • Inspect the hand and wrist coverage needed for the actual task.
    • Verify whether the glove can be worn with sleeves, cuffs, or other PPE.
    • Confirm whether the wearer needs dexterity for small parts, torch adjustments, or clamp handling.
    • Review previous glove failures for burn-through, seam split, or abrasion.

    Safety Notes

    Welding gloves are PPE, not universal protection. Match them to the hazard. Inspect before use. Remove from service if they are burned through, stiffened, torn, or contaminated in a way that cannot be corrected. For hot work, make sure the rest of the PPE set is also appropriate, including jacket, sleeves, face protection, and footwear.

    Do not assume any glove description confirms suitability for a specific code requirement, procedure, or site rule. If you need a compliance answer, verify it against your site safety program and the manufacturer documentation.

    FAQ

    Is this glove pair confirmed for a specific welding process?

    No. The provided source does not confirm process-specific approval. Treat process compatibility as Unknown (Verify).

    Can I rely on the listed 11 in. length for full forearm protection?

    No. An 11 in. length does not automatically mean full forearm protection for every task. Verify the actual exposure, sleeve overlap, and job hazard before use.

    Are the material and heat-resistance details confirmed?

    No. The provided source does not confirm those technical details. Use Unknown (Verify) until you check the product page or packaging.

    What should I inspect before replacing a worn pair?

    Inspect seams, palm wear, burn marks, stiffness, contamination, and fit. If the same failure repeats, verify whether the task or glove selection needs to change.

    Sources Checked

    • Provided ASIN registry entry for Miller 263348 Welding Gloves, 3D, Wing, 11In, White/Blue, Pack of (1 Pair), ASIN B00I4Z44RS
    • Provided product name and task metadata in the request

    Any technical detail not confirmed in those sources remains Unknown (Verify).

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • The Last Ten Minutes of a Welding Shift Matter More Than They Look

    The Last Ten Minutes of a Welding Shift Matter More Than They Look

    There is a point near the end of a welding shift when the shop starts telling the truth about its culture. The clock is getting loud. Gloves come off. The next crew is walking in. A half-built frame is still on the table, one clamp has been moved, a machine setting changed, and the easy thing would be to leave the whole story for somebody else to decode.

    That is where a good handoff begins—not with a long speech, but with respect for the person who has to pick up the work next.

    Welding culture talks a lot about individual skill. The trade also depends on continuity: what one person notices, records, stages, protects, and explains before the next set of hands takes over. The last ten minutes of a shift may not make the highlight reel, but they can decide whether the next crew starts with confidence or confusion.

    A handoff is part of the work

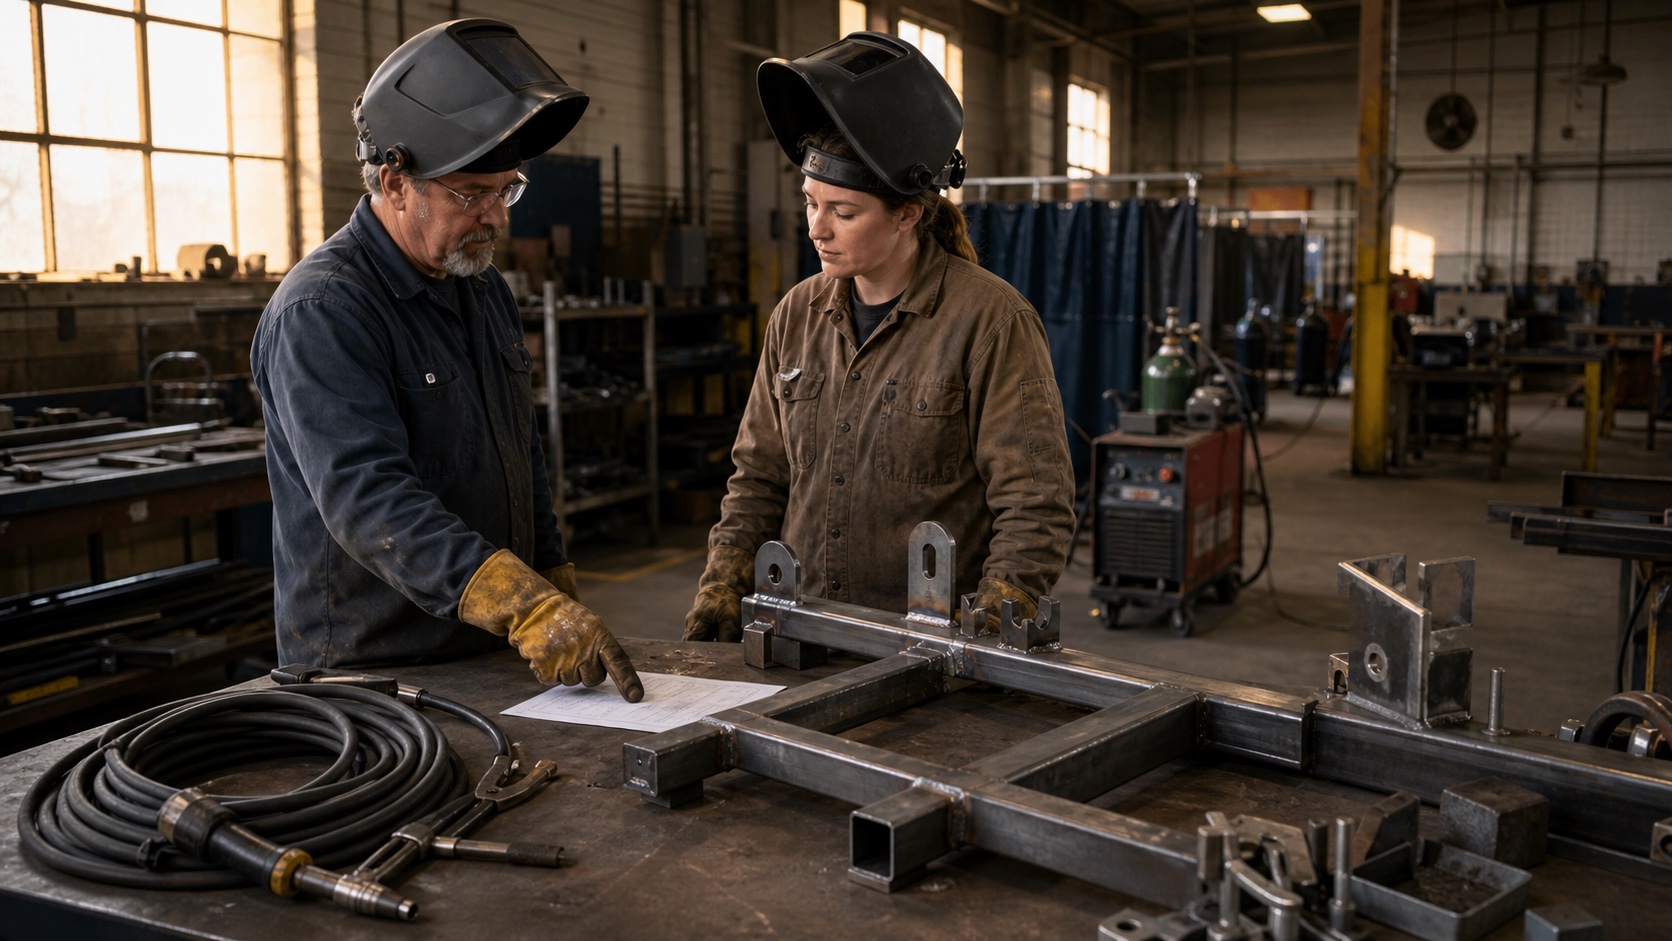
    A finished bead is visible. A good handoff is quieter. It might mean marking where the drawing changed, identifying which dimension still needs confirmation, pointing out a fixture that was moved, or saying plainly that a problem is not solved yet. It might mean leaving the leads coiled, consumables where they belong, and the bench clear enough for someone to see what comes next.

    None of that is glamorous. All of it is professional.

    The UK Health and Safety Executive describes effective shift handover as preparation by the outgoing crew, an exchange of task-relevant information, and cross-checking by the incoming crew. Its guidance recommends face-to-face, two-way communication supported by both verbal and written information. The point is not paperwork for its own sake. It is shared understanding.

    That principle reaches far beyond one industry. In a fabrication shop, the useful question is simple: what does the next person need to know to take responsibility for this work without guessing?

    The bench carries a story

    A workbench at shift change can look like a random pile to anyone passing through. To the person leaving, every clamp and chalk line may make sense. The incoming welder does not have that private map.

    A strong handoff turns the private map into a shared one. What has been fit? What is only tacked? Which surface is a reference? What was checked, and what still needs checking? Did the job change direction? Is there a concern that needs a lead person, inspector, or supervisor before work continues?

    The outgoing welder does not need to bury the next shift in every detail from the day. Good communication is selective. It separates what is merely interesting from what changes the next decision. The incoming welder has a job too: ask, repeat back the critical point, and look at the work rather than pretending the message was obvious.

    Fatigue makes clarity more valuable

    Shift change often happens when one crew is ready to leave and another is still getting oriented. That is exactly when memory and assumptions deserve less trust. The National Institute for Occupational Safety and Health notes that work-related fatigue can reduce attention, short-term memory, reaction time, and judgment. Hot work, demanding tasks, long hours, and nonstandard schedules can all be part of that picture.

    The answer is not to blame tired people for being human. It is to build a handoff that does not depend on someone remembering everything at the worst possible moment. A short written note, an updated traveler, a marked drawing, and a direct conversation give the next crew more than one way to understand the condition of the job.

    Just as important, an honest handoff gives people permission to say, “I am not sure.” Concealing uncertainty may feel faster. Naming it keeps a question from hardening into somebody else’s assumption.

    Leave it ready does not mean pretend it is perfect

    A ready bench is not necessarily an empty bench. A ready job is not necessarily a completed job. “Leave it ready” means the condition is understandable. Tools are staged with purpose. Loose ends are identified. Problems are visible. The next person can tell what belongs to the job and what does not.

    That standard also protects pride. There is a difference between inheriting another person’s work and inheriting another person’s mess. A clean, clear handoff says that the incoming crew is trusted with the next decision—not tested with a scavenger hunt.

    The best shops pass down habits, not just jobs

    New welders learn what matters by watching what experienced people do when nobody is taking a photograph. If a veteran stops long enough to explain an unusual fit, returns the fixture to a known condition, and leaves a useful note, that behavior teaches a version of craftsmanship that no bend test can measure by itself.

    The lesson travels in both directions. A new person may ask the question that exposes a vague assumption. A second-shift welder may see a sequence differently. A good handoff is two-way because good work is not protected by ego; it is protected by information moving clearly between people.

    The question for the shop

    What is the one thing you wish the previous shift would always leave clear: job status, machine condition, drawing changes, material location, fixture setup, or something else?

    The answers will be different from shop to shop. The principle holds: the work continues after one person clocks out. Leaving the bench ready is a small act of respect for whoever keeps the arc moving next.

    Arc Life tells the human stories behind the hood—the habits, identity, humor, and standards that turn a trade into a community. You can also explore the current Arc Life collection, built around that shared shop-floor culture.

    Sources

  • Black Stallion Red/yellow Nitrile-Coated Knit Gloves Large: Replacement Part Breakdown

    Black Stallion Red/yellow Nitrile-Coated Knit Gloves Large B07DM8P9P4 are a general-purpose hand protection item used in shop, maintenance, and material handling tasks. For buyers and support teams, the main question is not just whether the glove is available, but whether the glove size, coating type, knit backing, and grip level match the task. This guide breaks down the item as a replacement or reorder reference and focuses on what to check before you buy or issue the glove to a crew.

    Because glove performance depends on fit and work environment, this is a selection guide, not a procedure approval for any specific welding, cutting, or chemical exposure task. If your application has cut-risk, heat-risk, arc exposure, or chemical exposure, verify the glove against your site requirements before use.

    Key Takeaways

    • Use the glove as a general-duty hand protection option, not as a substitute for task-specific PPE.
    • Verify fit first. A large size that is too tight or too loose can reduce grip and control.
    • Nitrile-coated knit gloves are commonly chosen for dry handling and light abrasion resistance. Exact performance for this product is Unknown (Verify).
    • For replacement planning, confirm the exact product name and ASIN before reordering.
    • If the glove is used near welding work, confirm that the glove meets your local safety and job hazard requirements.

    Product and Parts Breakdown

    This item is a finished glove, so there are no serviceable replacement parts in the usual sense. For procurement and support records, track the following identifiers and check them against the supplier listing:

    • Product name: Black Stallion Red/yellow Nitrile-Coated Knit Gloves Large
    • ASIN: B07DM8P9P4
    • Size: Large
    • Coating: Nitrile-coated knit, as stated in the product name
    • Color: Red/yellow, as stated in the product name

    Any additional technical details such as fiber blend, cuff style, coating coverage, grip pattern, cut rating, or heat resistance are Unknown (Verify). Do not assume those attributes from the product name alone.

    How to Check the Right Fit Before You Reorder

    A glove that looks close on paper can still fail in use if the fit is wrong. Use this simple check process before issuing replacements.

    1. Inspect the old glove in service. Look for wear in the palm, fingertips, thumb saddle, and seams.
    2. Check hand size and hand shape. Compare the current user’s hand to the large size issue history. If the worker reports finger tip pressure, palm bunching, or thumb pull, the size may be wrong.
    3. Verify task demands. Confirm whether the glove is used for parts handling, shop cleanup, assembly, or another low- to moderate-abrasion task.
    4. Inspect grip needs. If the work involves oily surfaces, wet handling, or fine manipulation, verify whether nitrile coating is still the correct choice for that task.
    5. Verify replacement quantity. If the glove is consumed quickly, determine whether the root cause is fit, task severity, or improper storage.

    Troubleshooting and Support Checks

    If the glove is not performing as expected, use a basic support review before changing product families.

    Issue: Grip feels poor

    • Check: Is the surface dry, dusty, oily, or wet?
    • Inspect: Look for worn coating on the palm and fingers.
    • Verify: Confirm whether the task requires a different coating style or a different glove category.

    Issue: Glove tears early

    • Check: Is the glove being used on sharp edges, sheet metal, or rough stock?
    • Inspect: Look for puncture points and seam failure.
    • Verify: If the task has cut hazard, confirm the required cut-resistance level with your safety program. This product’s cut performance is Unknown (Verify).

    Issue: Hand fatigue or poor dexterity

    • Check: Is the glove too tight across the knuckles or too long in the fingers?
    • Inspect: Review whether the user is gripping harder to compensate for poor fit.
    • Verify: Try the next size up or a task-specific glove style only after confirming job requirements.

    Selection Notes for Maintenance Buyers

    When this item is being considered as a replacement, keep the purchase decision tied to the actual duty cycle. A nitrile-coated knit glove can be a practical general-use option, but it should not be treated as a universal answer for all shop tasks. Verify the following before standardizing the item:

    • What the glove is used for most often
    • Whether the main hazard is abrasion, grip loss, cut risk, heat, or contamination
    • Whether workers need more dexterity or more protection
    • Whether your site requires a documented PPE review

    If you already stock a different Black Stallion glove style for TIG or light mechanical work, compare the task profile rather than the brand name alone. For a related reference point, see Black Stallion GX5015 TIG/Mechanics Gloves Review & Buying Guide (L & XL).

    Safety Notes

    • Do not assume nitrile coating makes the glove suitable for cutting, welding spatter, or hot-surface contact.
    • Do not use glove color as a performance indicator.
    • Replace gloves that are torn, contaminated, stiffened, or heavily worn.
    • Verify all PPE selections against site hazard controls and supervisor guidance.
    • If the glove is used in a welding area, keep it away from direct arc exposure and hot slag unless the glove is specifically approved for that use. Approval status for this product is Unknown (Verify).

    FAQ

    Is this glove suitable for welding?

    Not enough information is provided to confirm that. For welding use, verify heat resistance, splice construction, and hazard approval before issue. Those details are Unknown (Verify).

    Can I reorder by ASIN?

    Yes. For internal tracking, use ASIN B07DM8P9P4 and the full product name to reduce reorder errors. Confirm the supplier listing at time of purchase because listings can change.

    What should I check if the glove wears out quickly?

    Check the task severity, surface sharpness, fit, and storage conditions. If the glove is being used beyond general-duty handling, it may need a different product class.

    Does this glove have cut protection?

    Cut protection is not confirmed from the provided product data. Treat it as Unknown (Verify) until you check the supplier listing or manufacturer documentation.

    Sources Checked

    • Provided Amazon registry reference for Black Stallion Red/yellow Nitrile-Coated Knit Gloves Large, ASIN B07DM8P9P4
    • Allowed internal link: Black Stallion GX5015 TIG/Mechanics Gloves Review & Buying Guide (L & XL)

    Final verification should always come from the live product listing and your site PPE requirements before purchase or issue.

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Black Stallion JF1012-LM Hi-Vis Safety FR Cotton Welding Jacket with FR Reflective Tape, Lime, 2X-Large: Product Breakdown

    Black Stallion JF1012-LM Hi-Vis Safety FR Cotton Welding Jacket with FR Reflective Tape, Lime, 2X-Large: Product Breakdown

    Product not found.
    “>Black Stallion JF1012-LM Hi-Vis Safety FR Cotton Welding Jacket with FR Reflective Tape, Lime, 2X-Large

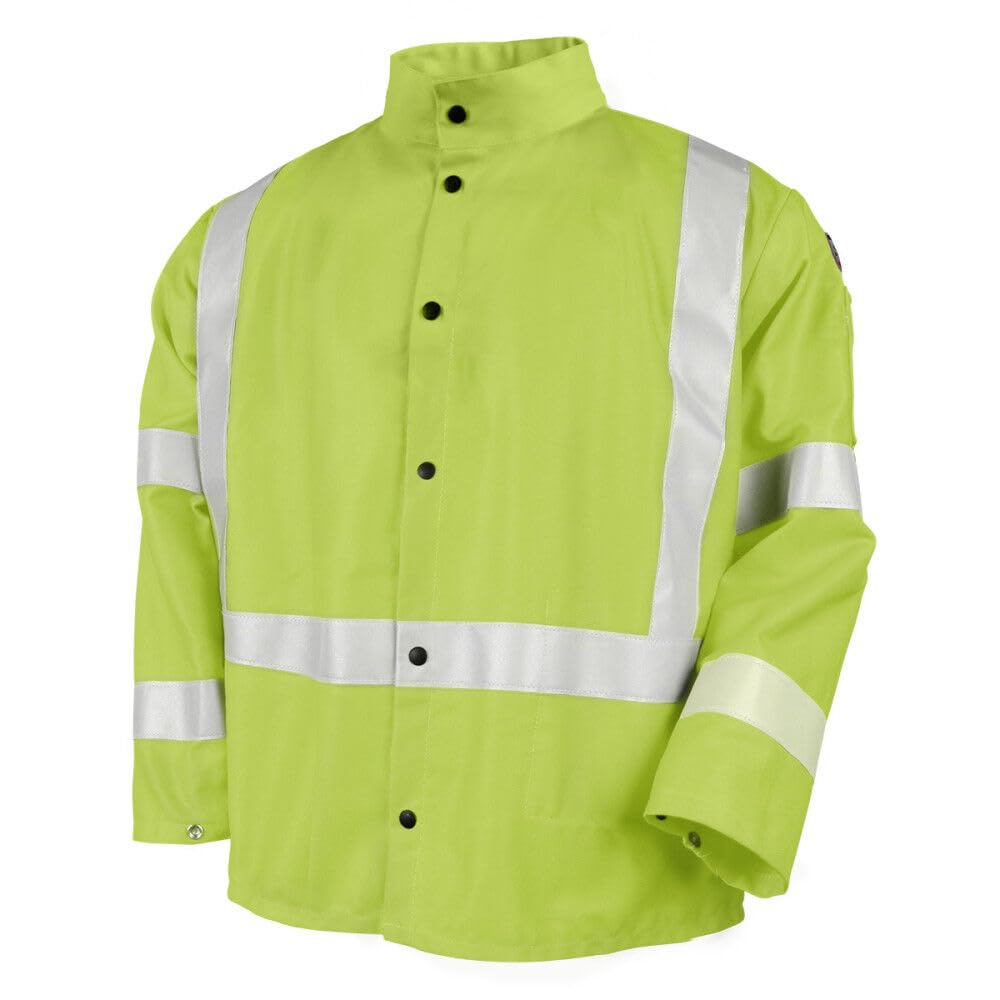
    The Black Stallion JF1012-LM Hi-Vis Safety FR Cotton Welding Jacket with FR Reflective Tape, Lime, 2X-Large is a jobsite garment built for visibility and basic flame-resistant coverage in light welding environments. Based on the product information provided by ArcWeld, this jacket uses flame-resistant treated cotton and FR reflective tape in a hi-vis layout, including an “X” on the back. It is described as a standard 30-inch jacket and as suitable where being seen matters, such as construction and traffic zones.

    For buyers, the main question is not only whether the jacket is FR-rated in general terms, but whether it fits the task. In welding support work, jacket selection should match exposure level, work posture, overhead spatter risk, and the visibility requirements of the site. This breakdown keeps the focus on what can be verified from the product listing and what should be checked before use.

    Key Takeaways

    What the Product Listing Supports

    The ArcWeld product description identifies the jacket as a Black Stallion safety welding jacket made with flame-resistant treated cotton. It is positioned for light welding applications where being seen is critical. That makes it relevant for maintenance crews, fabrication shops, field service teams, and construction environments with mixed pedestrian and vehicle traffic.

    The available details support the following practical interpretation:

    Anything beyond those points should be verified from the supplier page or internal product records before purchase.

    Check, Inspect, Verify Before Use

    Before a jacket goes into service, use a simple inspection routine. Do not assume a new garment is ready just because it is labeled FR.

    If any damage is found, remove the jacket from service until the issue is evaluated. FR clothing can lose usefulness if it is dirty, contaminated, or physically damaged.

    Troubleshooting Support Issues

    Issue: Jacket feels too hot or restrictive.
    Check whether the size is correct over the base layer. Inspect the work posture being used. Verify whether the task requires a lighter garment or a different FR layer arrangement.

    Issue: Visibility is reduced in real shop conditions.
    Inspect the jacket under the actual lighting used on site. Verify whether dirt, soot, grinding dust, or oil film is dulling the lime color or reflective tape. Clean only per the garment care instructions from the seller or manufacturer.

    Issue: Reflective tape looks worn.
    Inspect the tape for peeling, cracking, or contamination. Verify whether the garment is still acceptable under site PPE rules. If the tape is damaged, replace the jacket rather than trying to patch visibility features.

    Issue: Jacket coverage is short when bending or reaching.
    Check the 30-inch length against your torso and typical movements. Verify whether seated welding, crawling, or overhead positioning changes the effective coverage area.

    Product / Parts Notes

    This draft is based on a single listed product: the Black Stallion JF1012-LM jacket in lime, 2X-Large. The available source does not provide a parts breakdown, replaceable components, or accessory list. Those details are Unknown (Verify).

    Use the ArcWeld product page as the primary product reference for final purchasing review: Product not found.

    “>Black Stallion JF1012-LM product page.

    When buying for a crew, verify the following before ordering multiple units:

    How to Evaluate Fit for the Job

    Buyer guides should separate garment construction from actual work use. A jacket can be suitable on paper and still fail in practice if the use case is wrong.

    Do not assume the jacket is approved for every welding process or every exposure level. That determination depends on the employer, task, and site policy.

    Safety Notes

    FAQ

    Is this jacket for heavy welding?
    The provided description supports light welding applications. Heavy spatter or more severe exposure should be verified against the job requirements before purchase.

    Does the jacket improve visibility on the jobsite?
    Yes, the listing describes a lime hi-vis design with FR reflective tape and an “X” on the back. Actual visibility still depends on lighting, contamination, and site conditions.

    What size is covered in this product breakdown?
    The product named here is the 2X-Large version. Fit should still be checked against the wearer’s layers and range of motion.

    Is the jacket certification listed in the supplied data?
    No. Certification status is Unknown (Verify) based on the information provided here.

    Sources Checked

    Related Arc Weld Part

    Black Stallion JF1012-LM Hi-Vis Safety FR Cotton Welding Jacket with FR Reflective Tape, Lime, 2X-Large

    Black Stallion JF1012-LM Hi-Vis Safety FR Cotton Welding Jacket with FR Reflective Tape, Lime, 2X-Large

    Description Black Stallion's Safety Welding Jacket with FR Reflective Tape is made with comfortable flame-resistant treated cotton and is perfect for light welding applications where being "seen" is critical (construction, traffic zones, etc.). It also features silver FR reflective tape, with an "X" design on back for hi-visibility. This standard 30" jacket is made of 9 oz. flame resistant cotton. It features an i…

    View at Arc Weld Store

    Related Weld Support Guides

  • Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3: Product Breakdown

    Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3: Product Breakdown

    Product not found.
    “>Lincoln Viking 1740 Auto-Darkening Welding Helmet - K3282-3

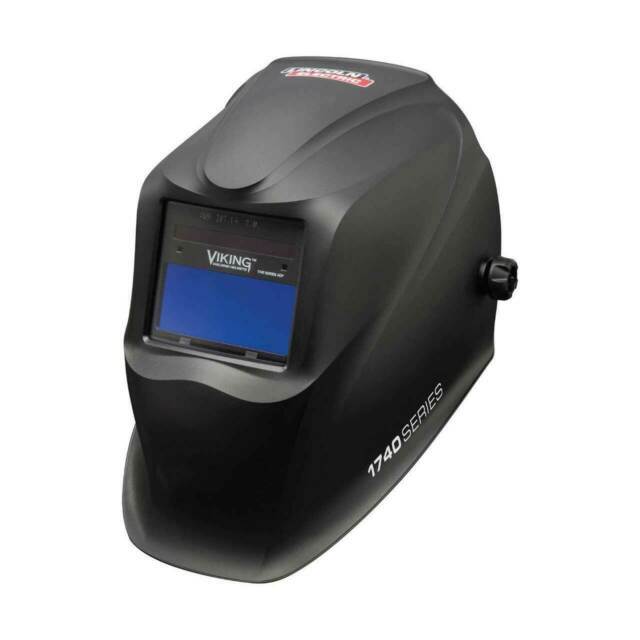
    The Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3 is a welding PPE item intended for day-to-day fabrication and repair work where a stable view of the weld zone matters. For buyers and support teams, the main question is not whether the helmet is “advanced,” but whether it fits the job, the user, and the maintenance routine. On a shop floor, consistent lens response, proper fit, and basic inspection discipline matter more than marketing terms.

    Key Takeaways

    What this helmet is for

    Based on the product description provided, this helmet is aimed at general fabrication and repair, shop work, field welding, and common arc processes such as MIG, TIG, and stick. The practical value of an auto-darkening helmet is simple: it lets the welder see the work area clearly before the arc starts, then darkens when the arc is struck. That reduces the need to repeatedly nod the hood up and down and can help reduce eye strain during repetitive work.

    For maintenance buyers, the priority is not just the helmet model name. It is whether the unit supports the welders’ actual tasks, how often consumable parts are checked, and whether the team has a repeatable inspection routine. If the application includes grinding, overhead welds, tight access work, or frequent start-stop cycles, the helmet must stay comfortable and reliable enough to avoid operator workarounds.

    Product / parts notes

    This article is limited to the product listing provided. Specific technical specs, lens sizes, shade ranges, sensor counts, and certification details were not supplied here, so they are Unknown (Verify). Do not assume compatibility with aftermarket headgear, cover lenses, or cartridge-style replacements unless the manufacturer documentation confirms it.

    For shop support, verify the following before issue or deployment:

    Troubleshooting and support checks

    1) Lens does not darken consistently

    2) Helmet feels loose or shifts during work

    3) Visibility is poor even when the hood is up

    How to inspect before use

    1. Visual check: look over the shell for cracks, heat damage, and spatter.
    2. Lens check: inspect both cover surfaces for scratches, haze, or debris.
    3. Fit check: put the helmet on and verify secure headgear contact without pressure points that force the user to loosen the hood.
    4. Function check: perform a controlled arc-response test if shop procedure allows it.
    5. Record check: note any recurring issue, especially if the same helmet is being reassigned between shifts.

    Related support references

    If you are comparing this model to adjacent Lincoln helmet support content, these internal pages may help with broader helmet selection and setup context:

    Safety notes

    FAQ

    Is the Lincoln Viking 1740 K3282-3 suitable for MIG, TIG, and stick welding?

    The provided product description says it is intended for daily MIG, TIG, and stick work. Specific duty limits, settings, and procedure approvals are Unknown (Verify).

    Can I use this helmet as a direct replacement for other Lincoln Viking models?

    Not without verification. Compatibility with other models, covers, headgear parts, or accessories is Unknown (Verify) unless the manufacturer documentation confirms it.

    What should I inspect first if the helmet starts acting up?

    Start with the basics: lens cleanliness, cover condition, sensor obstruction, headgear fit, and shell damage. In many cases, the issue is a contaminated cover lens or a loosened adjustment point.

    How often should the helmet be checked?

    At minimum, check it before each use. For shared helmets or high-volume shops, add shift-start and post-incident checks after drops, spatter strikes, or heavy grinding exposure.

    Sources Checked

    For procurement or support decisions, keep the focus on fit, function, and inspection discipline. If a technical detail is not documented in the available source material, treat it as Unknown (Verify) before buying or issuing the helmet to the floor.

    Related Arc Weld Part

    Lincoln Viking 1740 Auto-Darkening Welding Helmet - K3282-3

    Lincoln Viking 1740 Auto-Darkening Welding Helmet – K3282-3

    Lincoln Viking 1740 Auto-Darkening Welding Helmet (K3282-3) is a professional-grade auto-darkening hood built for daily MIG, TIG, and stick work where clear visibility and consistent shade response matter. It’s designed to reduce eye strain by giving you a bright, high-clarity view of the puddle and joint before and during the arc. What it’s for General fabrication and repair Shop and field welding Processes with…

    View at Arc Weld Store

    Related Weld Support Guides

  • More posts

    Try Amazon Prime Free