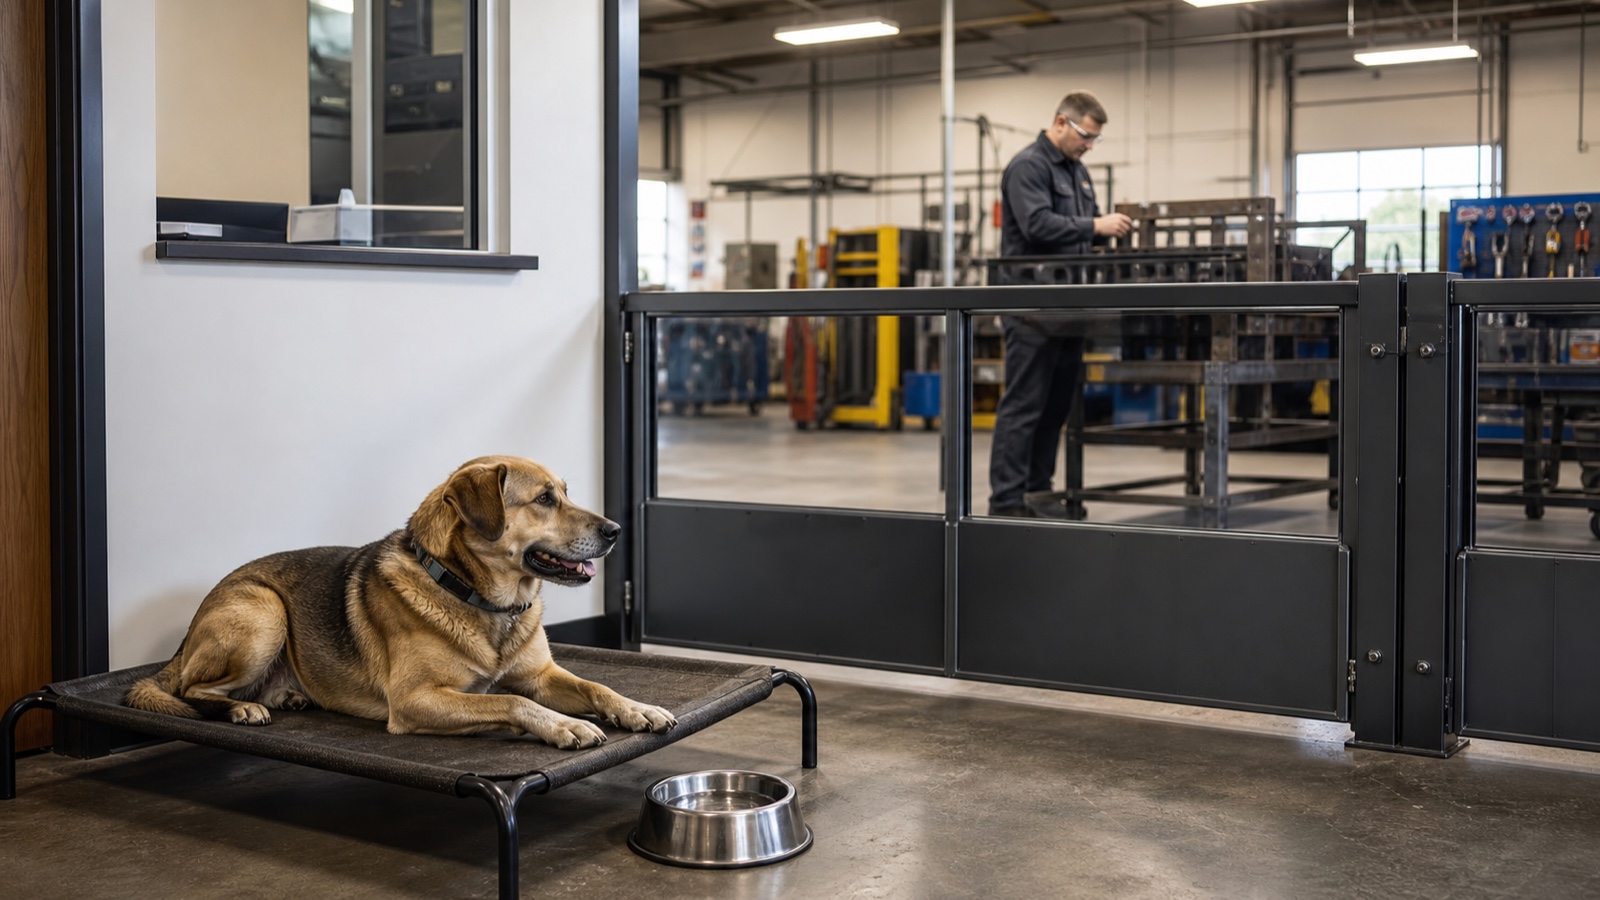
The social-media version of a shop dog is almost too easy to picture: paws stretched under a welding table, sparks in the background, a battered water bowl beside the toolbox. It looks warm, loyal, and unmistakably blue collar.
It is also the wrong picture.
A dog can be part of a shop’s personality without roaming through its active work area. In fact, the clearest sign that a crew truly cares about its unofficial four-legged member is not a good photo. It is a boring, consistent boundary.
That feels worth saying on August 26. National Dog Day, founded in 2004, celebrates dogs of all breeds and calls attention to dogs that need rescue. The day’s official site also honors family dogs and working dogs. Welding shops have their own familiar version: the dog that recognizes the morning trucks, knows who drops food at lunch, and appears when the office door opens.
The best place for that dog is still on the safe side of the door.
The photo and the shop are not the same thing
The shop-dog image works because it softens an industrial place. A dog can make an office feel less corporate, give the first person through the door a familiar greeting, and become part of the routine customers remember. None of that requires the animal to share space with hot work.
The Occupational Safety and Health Administration lists metal fumes and ultraviolet radiation among the health hazards of welding, cutting, and brazing. Its safety-hazard list includes burns, eye damage, electrical shock, cuts, and crushed toes and fingers. OSHA also points to noise exposure, personal protective equipment, ventilation, and fire controls as parts of managing that environment.
Those rules and resources are written to protect people at work. They are not a pet policy. Still, the logic is hard to miss: if trained workers need barriers, PPE, ventilation, and controlled work practices, an animal without those protections should not be inside the active area.
This is not about treating every fabrication shop as the same. It is about recognizing that a dog cannot read a hot-work permit, understand why a plate is still hot, or know that a lead stretched across an aisle is attached to a live job.
If people need PPE, the dog needs distance
Human workers can be trained to stop at a screen, wear the right lens, recognize a lift route, and stay clear of a grinder. A dog moves by sound, smell, habit, curiosity, and the location of its favorite person. That unpredictability does not belong near a process where one quick step can cross a cable, enter a forklift path, or reach fresh-cut steel.
Noise deserves the same clear thinking. OSHA’s general-industry standard requires a hearing-conservation program when employee exposure reaches an eight-hour time-weighted average of 85 decibels. That does not establish a pet limit, and it should not be borrowed as one. It does show that industrial noise is measured and managed—not dismissed as atmosphere.
The right response is not a novelty pair of dog earmuffs and a good caption. It is separation from grinding, air-arc work, hammering, plasma cutting, and other loud operations. Pet-specific health questions belong with a veterinarian; shop access belongs in the shop’s safety plan.
Floor conditions matter, too. OSHA requires walking-working surfaces to stay orderly and free of hazards such as sharp or protruding objects. A well-kept floor protects employees. It also removes fewer chances for a paw to find a sharp drop, a sliver, or spilled material—but housekeeping alone does not turn a production floor into a pet area.
Good shop-dog culture is boring on purpose
A responsible setup does not need to be complicated. The dog has a defined place in the front office, enclosed yard, or another separated area. The barrier closes. Water and bedding stay away from chemicals, oily rags, metal debris, and traffic. Deliveries do not depend on somebody remembering to grab a collar at the last second.
The rule stays the same on slow days. That is important. A dog that is allowed onto the floor while the machines are quiet cannot understand why the same doorway becomes off-limits when the first grinder starts. Consistency is kinder than a rule that changes with the workload.
The crew also resists staging the animal for a dramatic photo near sparks or an open arc. Welding culture already has enough imagery that turns hazards into decoration. A shop dog does not need to be made into another prop.
Some facilities cannot support a dog at all. Customer rules, lease terms, allergies, sanitation requirements, insurance, traffic, or the layout may settle the question before the crew does. “No shop dog” is not anti-dog. Sometimes it is the most honest answer the building can give.
Part of the crew means worthy of a rule
The value of a shop dog is not productivity. The dog is there because people spend a large part of their lives at work, and a familiar animal can make that place feel more human. It can mark the difference between the production floor and the small community gathered around it.
That community owes the dog more than affection. It owes the dog a boundary that does not disappear for a photo, a visitor, or a quiet afternoon.
There is something deeply consistent about that idea. Welders already understand controlled zones. They know the difference between an active booth and a clear aisle, between hot metal and finished work, between a barrier that is inconvenient and one that prevents a bad day. Extending that discipline to a dog is not overthinking the culture. It is taking the culture seriously.
Does your shop have a dog, and what rule keeps it safe? Office only? Fenced yard? Home before hot work starts? Tell us the boundary that actually works—not just the picture that looks good.
Washington Alloy 2 Lb. Spool Mig Welding Wire 308L Stainless Steel (.023 x 2 lb.) is a small-format stainless MIG wire option used in support and maintenance workflows where a compact spool makes sense. For buyers and welders, the important part is not the spool label alone. The wire has to match the base metal, shielding gas, feeder setup, and the actual welding procedure in use. If any one of those points is off, the result is usually birdnesting, unstable arc starts, excessive spatter, or a weld that does not meet job requirements.
This breakdown focuses on what to verify before ordering or loading the spool, what to inspect during setup, and how to troubleshoot common issues without guessing at compatibility. Product-specific procedure approval is always governed by the job spec or WPS. If the procedure is not documented, treat the selection as a starting point and verify before use.
Key Takeaways
ER308L stainless MIG wire is commonly evaluated as a starting point for austenitic stainless work, but procedure approval depends on the job.
.023 in wire is a small-diameter option; feeder condition and contact tip size matter more at this scale.
A 2 lb spool is useful for short runs, repair work, and limited feeder capacity, but verify your feeder can handle the spool format.
Do not assume stainless wire will run like carbon steel wire. Cleanliness, gas coverage, and liner condition are critical.
Unknown (Verify) on exact machine compatibility, shielding gas mix, and all procedure limits unless your WPS or equipment manual confirms them.
What This Wire Breakdown Means for the Shop
For maintenance buyers, replacement-part breakdown starts with function. This spool is a consumable, not a standalone solution. The wire only performs correctly when the feeder, drive rolls, gun liner, contact tip, shielding gas, and workpiece prep are in line with stainless requirements. If the shop uses multiple wire types, label storage and feeder changeover steps clearly to prevent cross-contamination.
Check: confirm the wire designation, diameter, and spool size before it goes into the crib or on the machine. If the printout, bin tag, and package do not match, stop and verify. Inspect: the spool for shipping damage, loose wraps, and contamination. Verify: the feeder, tip size, and liner are suitable for a .023 in stainless wire installation.
Setup and Troubleshooting Support
Stainless wire problems usually show up fast. If the arc is unstable or the wire feed feels rough, work through the system in order rather than changing multiple variables at once.
Check the feeder first
Check: drive roll type and tension. Over-tight drive pressure can deform smaller wire.
Inspect: the inlet and outlet guides for burrs, dust, or metal fines.
Verify: the wire path is clean from spool hub to contact tip.
Check the gun consumables
Check: contact tip wear, heat damage, and tip size.
Inspect: liner condition if feed resistance is present.
Verify: the gun neck and torch routing do not create sharp bends that can cause feed instability.
Check the weld environment
Check: shielding gas supply and flow at the machine and gun end.
Inspect: for drafts, fan turbulence, or poor nozzle coverage.
Verify: the base metal is clean and free of oil, rust, paint, and carbon steel transfer.
If porosity appears, do not assume the wire is defective. First verify gas coverage, nozzle cleanliness, and surface prep. If the wire hesitates or birdnests, inspect the drive system, liner, and tip condition before changing feed speed or voltage. If burnback occurs, verify stickout, contact tip wear, and feed consistency. These are routine support checks, not guarantees of correction.
Replacement Part Considerations
As a replacement item, the spool should be matched against the feeder and the application, not just the product description. The most common support questions are about spool mounting, feed performance, and whether the wire is appropriate for a given stainless job. Without the machine model and WPS, those details remain Unknown (Verify).
Check: the spool hub, drive roll groove, and gun liner diameter handling for .023 in wire. Inspect: whether the feeder has been used with carbon steel wire previously and clean any contamination. Verify: the internal job requirements before putting stainless wire into production use.
For team reference on stainless filler selection, use the Weld Support Parts article Best MIG Wire for Stainless Steel (ER308L vs ER309L) as a selection starting point. It is not a procedure approval document.
Use proper eye, hand, and body protection when loading wire and setting up the feeder.
Do not touch live electrical components or feed mechanisms without following lockout or machine shutdown procedures.
Stainless welding can generate fumes and metal particulates. Use local exhaust ventilation and follow site safety rules.
Keep wire and consumables clean. Do not store stainless wire where it can pick up carbon steel dust or grinding debris.
FAQ
Is this wire automatically approved for stainless steel repair work?
No. It may be a candidate, but approval depends on the WPS, base metal, and service requirements. Verify before use.
Can .023 in wire run in any MIG feeder?
No. Feeder condition, drive roll setup, liner condition, and tip sizing all matter. Machine-specific fit is Unknown (Verify) unless confirmed by the equipment manual.
What should I check first if the arc is erratic?
Check the contact tip, liner, drive roll pressure, and shielding gas flow. Inspect the spool for feed damage and verify the wire path is clean.
Is the 2 lb spool format better for production?
Not necessarily. It is often more practical for short jobs, repairs, and limited feeder capacity. Production suitability depends on job volume and feeder setup.
Sources Checked
Provided Amazon ASIN registry entry: B081XDF1LM
Provided product title and target keyword
Allowed internal Weld Support Parts links listed in the task
Product link for reference:
No products found.
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
This guide covers the Washington Alloy 2 lb. spool MIG welding wire in 308L stainless steel, .035 diameter, as a replacement consumable for maintenance and fabrication work. The main question is not whether the wire exists on the shelf, but whether it is the right filler metal for the job, the feeder, and the base metal condition. For stainless work, selection errors usually show up as poor wetting, slag or soot issues, contamination, or welds that do not meet the service requirement.
Product reference: Washington Alloy 2 Lb. Spool Mig Welding Wire 308L Stainless Steel (.035 X 2lb.) ASIN B081X4F6BV. Use the product page as the item reference only. Do not assume process approval, machine compatibility, or base-metal coverage without checking the actual welding procedure or weld requirement.
Key Takeaways
308L stainless MIG wire is a filler metal choice, not a universal stainless solution.
.035 wire size must match the feeder setup, drive rolls, liner, and contact tip condition.
Use it only when the weld requirement, shielding gas, and base metal call for 308L stainless filler.
Verify storage and handling first; stainless wire contamination can create avoidable defects.
If the base metal or procedure is unclear, stop and verify before welding.
What this wire is used for
308L stainless filler is commonly selected when joining compatible stainless materials. The “L” designation indicates low carbon, which is used to reduce the risk of sensitization in the weld zone. That does not mean it is interchangeable with every stainless grade or every joint. The correct choice depends on the base metal, service environment, corrosion requirement, and the approved welding procedure. If any of those inputs are unknown, treat the filler selection as Unknown (Verify).
Check: confirm the base metal grade from drawings, tags, or material certs. Inspect: look for contamination, rust, carbon steel residue, oil, or chloride-bearing cleaners. Verify: confirm whether the job calls for 308L, 309L, or a different filler before loading the spool.
Fit-up and machine support checks
A 2 lb spool in .035 diameter may be correct for bench work, repair work, or light fabrication, but the feeder setup still matters. Do not assume the spool will run well just because it fits the hub. Check the drive rolls, liner, torch cable routing, contact tip size, and tension. If the wire birds-nests, hesitates, or feeds inconsistently, the issue is often mechanical rather than chemical.
Check: drive roll groove size against .035 wire.
Inspect: liner wear, debris, and sharp bends in the gun cable.
Verify: contact tip bore is correct for the wire size and not worn oversize.
Check: spool brake tension and feed pressure before changing settings.
Troubleshooting support section
If weld quality is inconsistent, isolate the problem in order: material, wire, shielding gas, feeder, then technique. Stainless MIG issues are often traced to poor surface preparation or the wrong gas setup, not the spool itself.
Common symptoms and what to check
Poor bead wetting: Check base-metal cleanliness, joint fit-up, and whether the filler choice matches the job. Verify shielding gas setup.
Excessive spatter or soot: Inspect gas coverage, nozzle condition, and stickout. Verify the machine is configured for the process in use.
Wire feeding problems: Check liner, drive roll tension, and tip wear. Verify the spool is installed without side loading.
Discoloration or contamination: Inspect storage, handling, and whether stainless wire has been exposed to carbon steel dust or moisture.
Product and parts considerations
This is a consumable wire product, not a complete system. The spool is only one part of the welding chain. For support teams and buyers, the real replacement question is whether the feeder package, gun parts, and gas setup support stainless wire reliably.
Before purchasing, confirm the following:
Wire diameter: .035
Material type: 308L stainless
Spool size: 2 lb
Machine feed capability for small stainless spools: Unknown (Verify)
Shielding gas requirement: Unknown (Verify)
Base metal compatibility for the job: Unknown (Verify)
If any of those values do not match the welding instruction, do not force the part into service. A wire can be physically compatible with the feeder and still be wrong for the weld requirement.
How to evaluate before you install the spool
Check the label. Confirm the wire type, diameter, and spool weight before opening the package.
Inspect the package. Look for damage, moisture exposure, or visible contamination.
Verify the machine setup. Confirm drive rolls, liner, and tip size for .035 wire.
Clean the work area. Keep stainless wire away from carbon steel grinding dust.
Test feed. Run a short feed test before striking an arc.
Verify weld result. Inspect bead appearance, fusion, and discoloration after the first test weld.
Use approved PPE for MIG welding, including eye, hand, and body protection.
Stainless welding can generate fumes that require adequate ventilation or local exhaust.
Keep stainless consumables away from carbon steel contamination.
Do not rely on general assumptions for process approvals, gas mix, or corrosion performance.
Follow the site weld procedure and supervisor instructions where applicable.
FAQ
Is this wire automatically correct for all stainless steel jobs?
No. 308L is a specific stainless filler choice. Confirm the base metal and weld requirement before use. If the specification is not available, mark it as Unknown (Verify).
Can I use .035 wire in any MIG machine?
Not automatically. The machine must support the spool format, wire size, liner, drive rolls, and torch configuration. Verify the feeder package before purchase or installation.
What should I check if the wire feeds poorly?
Check the drive rolls, liner, contact tip, spool tension, and cable routing first. Feeding problems are often mechanical rather than caused by the wire alloy.
Does 308L mean the wire is approved for my application?
No. Alloy designation alone does not approve a weld. The final decision depends on the welding procedure, joint design, service environment, and base metal.
Sources Checked
Amazon product reference for Washington Alloy 2 Lb. Spool Mig Welding Wire 308L Stainless Steel (.035 X 2lb.), ASIN B081X4F6BV
Weld Support Parts internal article: Best MIG Wire for Stainless Steel (ER308L vs ER309L)
Weld Support Parts internal article: Stainless Steel Wire Wheel Brush for Welding Surface Prep
Weld Support Parts internal article: Best Flux Core Wire for Stainless Steel Welding
Bottom line: treat this spool as a targeted stainless filler metal option, not a universal replacement part. Confirm the job requirements, verify the feeder setup, and keep the wire clean from the moment it is opened.
Matched Replacement Option
No products found.
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
Washington Alloy 9018-M 10lbs Welding Stick Electrode (3/32″) is a low-hydrogen stick electrode intended for demanding structural and repair work where weld quality and toughness matter. The product description identifies it as an all-position, iron-powder electrode with manganese, molybdenum, and nickel, and notes it is aimed at low alloy, high tensile, quenched, and tempered steels such as T1, HY80, and HY90. That puts it in a class of consumables that buyers often choose for stronger base metals, but the final selection still depends on the job procedure, material condition, and code requirements.
This article breaks down what the product description tells you, what you should verify before use, and how to support the electrode in the shop. It is a buyer guide, not a procedure approval. If the job is code work, match the electrode to the WPS, base metal, joint design, and preheat/postheat requirements.
Key Takeaways
9018-M is described as an all-position, low-hydrogen, iron-powder electrode.
The listed alloying elements are manganese, molybdenum, and nickel.
It is intended for low alloy, high tensile, quenched, and tempered steels, including T1, HY80, and HY90 as listed by the source.
The product description says weld deposits have excellent impact properties and are X-ray quality.
Preheat and postheat are application dependent; exact requirements are Unknown (Verify).
What the Product Breakdown Means
The term low-hydrogen matters because hydrogen control is a common concern on higher-strength steels and restrained joints. In practical terms, the electrode should be stored and handled to limit moisture pickup. The listing also calls it iron-powder. That usually signals higher deposition efficiency than a plain general-purpose rod, but exact deposition behavior for this specific product is Unknown (Verify) unless you are working from the manufacturer data sheet or a qualified procedure.
The alloy content listed in the product summary suggests the rod is intended to support strength and toughness requirements. That does not mean it is the correct filler for every high-strength steel. Verify the base metal specification, thickness, restraint, service temperature, and any code or customer requirements before issuing it to production.
Practical Check / Inspect / Verify Steps
Check the base metal spec and the job traveler. Confirm the material actually calls for a low-hydrogen high-strength electrode.
Inspect the joint fit-up, bevel, root gap, and cleanliness. Remove rust, oil, mill scale, and moisture before striking an arc.
Verify the required preheat and interpass controls. The source indicates preheating and postheating may be needed depending on thickness and hardening characteristics, but exact temperatures are Unknown (Verify).
Check rod condition before use. Bent, contaminated, or moisture-exposed electrodes should not be treated as production-ready.
Inspect the storage method. Low-hydrogen electrodes should be kept in a dry controlled environment or holding container as required by your procedure.
Verify polarity and amperage from the manufacturer data or qualified procedure. Do not assume settings from another 9018-family rod transfer directly.
Troubleshooting Support for Shop Use
If the arc is unstable, the first checks should be basic. Inspect the electrode for moisture damage, verify the machine output, and confirm the work lead and stinger connections. If slag is difficult to remove, check travel speed and bead shape against the procedure. If cracking appears, stop and verify preheat, interpass control, restraint, and hydrogen management before continuing.
The product referenced here is Washington Alloy 9018-M 10lbs Welding Stick Electrode (3/32″). The provided source description indicates the rod is designed for low alloy, high tensile, quenched, and tempered steels and highlights impact performance and X-ray quality deposits. No further technical specifications were provided in the source set, so current diameter, length, current range, recovery rate, and storage limits are Unknown (Verify).
Use this product as a support item when your procedure and material call for this family of electrode. It is not a universal replacement for general-purpose rods. If you need a different structural stick option for comparison, a related support article on a 7014 electrode is available here: Washington Alloy 7014 Stick Electrode – Smooth Welding with High Deposition. That article is a selection reference, not a procedure approval.
Support Buying Notes
For maintenance buyers, the key question is not only whether the electrode is available, but whether it matches the weld requirement. Before buying, verify the joint type, service condition, and whether the job uses a qualified WPS. If purchasing for stock, label it by electrode family and keep usage notes by job type so the next shift does not have to guess. If the work mixes general fabrication and high-strength repair, separate the stock clearly to avoid mix-ups.
If you are also reviewing related equipment, the stinger and holder should be matched to expected duty and cable condition. A good electrode will not compensate for poor current transfer or damaged leads.
Safety Notes
Follow the applicable WPS, SDS, and site hot-work rules.
Keep low-hydrogen electrodes dry and protected from contamination.
Use proper PPE, including eye, face, hand, and body protection.
Do not assume preheat or postheat values; verify them for the specific job.
Watch for fume control, especially in confined or poorly ventilated spaces.
FAQ
Is Washington Alloy 9018-M the same as every other 9018 rod? No. The designation suggests a similar electrode family, but you should not assume identical performance, polarity, or settings. Verify against the manufacturer data and the job procedure.
Can this rod be used on any high-strength steel? No. The listing names certain high-strength and quenched-and-tempered steels, but actual suitability depends on the base metal, service conditions, and procedure approval. Verify before use.
Does the listing guarantee X-ray quality welds? No guarantee can be assumed from a product summary alone. The source says the deposits are X-ray quality, but the final result depends on fit-up, technique, cleanliness, parameters, and inspection requirements.
What should I verify before putting it into production? Check the WPS, base metal spec, preheat needs, storage condition, and current settings. Also verify that the joint prep and operator qualifications match the task.
Internal WSP blog article: Welding Electrode Holder: Choose the Best for Stick Welding
Internal WSP blog article: Washington Alloy 7014 Stick Electrode – Smooth Welding with High Deposition
Note: No WSP lookup page or filler metal finder page was provided for this draft. Technical details not present in the supplied sources are marked Unknown (Verify).
Related Arc Weld Part
Washington Alloy 9018-M 10lbs Welding Stick Electrode (3/32")
9018M is an all-position, low-hydrogen, iron-powder electrode containing manganese, molybdenum, and nickel. 9018M is designed for welding low alloy, high tensile, quenched, and tempered steels such as T1, HY80, and HY90. Weld deposits have excellent impact properties and are X-ray quality. PREHEATING AND POSTHEATING Depending upon the thickness and hardening characteristics of the workpiece, preheating at a temper…
Washington Alloy 33 Lb. Spool Mig Welding Wire 80S-D2 Mild Steel (.045 X 33 lb.) is a solid MIG wire aimed at joining and buildup work on mild steel and some low alloy steels. The product description identifies it as 80S-D2 wire and notes use on problem steels, including material with higher sulfur content and certain carbon and low alloy Cr-Mo base metals. Treat that description as a starting point, not a procedure approval. Final suitability depends on the base metal, joint design, shielding gas, welding position, and code or customer requirements.
If you are buying wire for production, maintenance, or repair work, the first question is not spool size. It is whether the filler metal matches the job. Check the work order, the base metal identification, and the required weld properties before loading the gun.
Key Takeaways
80S-D2 is described as a low alloy solid MIG wire for mild steel and select low alloy steels.
The product description points to higher strength output, stable arc, low spatter, and a flat bead profile.
.045 in. wire is a common production diameter, but machine settings and feed system capacity must be verified.
Do not assume this wire is approved for every carbon or Cr-Mo repair. Verify the procedure first.
When the job is critical, confirm weld procedure, shielding gas, and mechanical property targets before welding.
What This Wire Is Intended For
Based on the supplied product information, this wire is meant for general welding on mild steel and low alloy steels where a stronger deposit is desired than a basic mild steel filler may provide. The description also mentions good arc stability and low spatter. That can help in production work, but only if the machine, drive rolls, liner, and gas coverage are set correctly.
Use the product page as the primary reference for the seller’s intended use:
Washington Alloy 33 Lb. Spool Mig Welding Wire 80S-D2 Mild Steel (.045 X 33 lb.)
80S-D2 is a low alloy designed to produce high strengths on a wide range of base metals such as problem steels containing high sulfur to the basic carbon and low alloy Cr-Mo base metals. Its silicon level with molybdenum and manganese gives you excellent arc stability, low spatter, yielding a flat bead with excellent impact values and high ductile tensile strengths in the 100,000 psi range. 80S-D2 produces X-ray q…
Typical decision points for a shop buyer or lead welder include maintenance welds, fabrication on mild steel structures, repair work on unknown or mixed-condition carbon steel, and selected low alloy applications. That said, “problem steels” is a broad label. It does not replace material verification. If the base metal is unknown, suspect, or heat-treated, inspect the job requirements before choosing wire.
Troubleshooting and Support Checks
When a weld does not look right, work through the system in order.
1) Check the base metal
Check: Is the base metal mild steel, low alloy steel, or something else?
Inspect: Look for mill scale, rust, oil, galvanizing, coatings, or prior repairs.
Verify: Confirm the material spec or job ticket before assuming 80S-D2 is appropriate.
2) Check the procedure
Check: Is there a WPS or repair instruction for this joint?
Inspect: Confirm joint type, thickness, position, and preheat requirements if any are listed.
Verify: Do not use this article or the product description as procedure approval. Unknown (Verify).
3) Check the machine and feed path
Check: Is the feeder sized and set up for .045 wire?
Inspect: Look at drive roll type, liner condition, contact tip wear, and spool tension.
Verify: Wire feed must be smooth and consistent before production welding starts.
4) Check shielding gas and coverage
Check: Is the gas type set for the wire and procedure being used?
Verify: Gas selection is not provided in the source data. Unknown (Verify).
5) Check weld appearance
Check: Does the bead show excessive spatter, undercut, porosity, or poor tie-in?
Inspect: Travel speed, voltage, wire feed speed, and gun angle.
Verify: If defects continue, stop and correct the root cause before continuing.
Selection Notes for Buyers
For purchasing, the main value of a wire like this is its application range and the expected deposit behavior. The supplied description claims strong mechanical performance in the 100,000 psi range and good impact values, but those statements should be treated as manufacturer or seller claims unless your own procedure, test report, or spec sheet confirms them. Unknown (Verify).
Also verify spool handling details before ordering. The product title lists a 33 lb. spool and .045 diameter, but any other machine compatibility details are not provided here. Unknown (Verify).
How to Use Internal Guidance Pages
If you are still deciding between filler metals, use the Weld Support Parts blog library as a selection aid. These pages help compare wire families and identify likely candidates, but they are not guaranteed approvals for your job.
Use these pages to compare wire families, then verify against the job spec. Selection aid only. Not procedure approval.
Safety Notes
Ventilation matters. Fume control is required for MIG welding operations.
Clean the work area before welding to reduce spatter ignition and contaminant-related porosity.
Wear appropriate eye, hand, body, and hearing protection.
Do not weld on unknown plated, coated, or contaminated material without verifying the hazard.
Follow shop lockout, hot work, and fire watch rules where required.
FAQ
Is Washington Alloy 80S-D2 the same as a basic ER70S-6 wire?
No. The product is identified as 80S-D2, which is a different filler metal designation from ER70S-6. Compare the job requirements before choosing between them.
Can I use this wire on any mild steel repair?
No. Base metal condition, thickness, joint design, shielding gas, and procedure requirements all matter. Verify the repair specification first.
Does the product description guarantee high-strength welds?
No. The description claims high-strength performance, but actual results depend on procedure, machine setup, and base metal. Unknown (Verify).
Is .045 in. wire always the right size for production work?
No. Wire diameter must match the welding machine, feeder, transfer mode, and part thickness. Verify the setup before use.
Sources Checked
Washington Alloy 33 Lb. Spool Mig Welding Wire 80S-D2 Mild Steel (.045 X 33 lb.) product page:
Product not found.
Weld Support Parts internal article: Blue Demon ER70S-6 Mild Steel MIG Welding Wire (ER70S-6)
Weld Support Parts internal article: E70S-6 Solid MIG Wire vs E71T-1 Flux Core Wire
Weld Support Parts internal article: Best MIG Wire for Stainless Steel (ER308L vs ER309L)
Use 8018W when the weld must weather with ASTM A588, A242, Cor-Ten-type, or similar atmospheric-corrosion-resistant steel. Use 8018-C3 when the job calls for an 80 ksi low-hydrogen electrode with nickel-based toughness, especially low-temperature service, but do not assume it will match the corrosion behavior or color of weathering steel unless the welding procedure or engineer approves it.
Practical Selection Rule
Job condition
Better starting choice
Why
Exposed weathering steel, visible welds, no paint
8018W
Designed for weathering-steel weld deposits and color match
Weathering steel that will be painted
8018W or approved alternate
Verify project WPS; corrosion color match may matter less
Low-temperature toughness requirement
8018-C3
Nickel-bearing deposit is commonly selected for notch toughness
Bridge, structural, or code work
WPS-specified electrode only
Do not substitute by “close enough” classification
Unknown base metal
Unknown (Verify)
Identify grade before choosing filler
What These Electrodes Do
8018W is a low-hydrogen SMAW electrode intended for weathering steels. The “W” family is used where the weld metal needs atmospheric corrosion resistance closer to the base metal. It is the better match for exposed A588, A242, Cor-Ten-type plate, outdoor sculptures, architectural panels, bridge repair, and unpainted weathering assemblies.
8018-C3 is also an 80 ksi low-hydrogen SMAW electrode, but the C3 classification is commonly associated with a nominal 1% nickel weld deposit. Its strength and toughness can be excellent, but it is not automatically the same as a weathering-steel filler. For exposed weathering steel, treat 8018-C3 as Unknown (Verify) unless the WPS, engineer, or filler manufacturer confirms suitability for that application.
Common Symptoms of the Wrong Rod
Weld bead stays visibly different after surrounding steel weathers.
Rust staining forms around the weld instead of a uniform patina.
Repair area corrodes faster than adjacent A588 or A242 steel.
Low-temperature impact requirements are missed because the wrong filler family was selected.
Inspector rejects the work because the electrode does not match the WPS.
Compatibility Notes
Base metal: Verify ASTM grade, mill cert, or drawing callout. Do not rely on “it looks like Corten.”
Electrode classification: Confirm AWS A5.5 classification printed on the container.
Procedure: Use the WPS/PQR for structural, bridge, lifting, pressure, or code-controlled work.
Service exposure: Unpainted outdoor weathering steel usually favors 8018W-type filler.
Temperature: If CVN impact toughness is specified, use the exact filler and heat input range listed by the procedure.
Storage: Both are low-hydrogen electrodes; moisture pickup can raise cracking risk.
What To Verify Before Ordering
Check
Why it matters
AWS classification
8018W and 8018-C3 are not the same selection basis
Base metal grade
A588, A242, and other low-alloy steels may require specific filler
Exposure condition
Unpainted weathering steel needs corrosion-compatible weld metal
Diameter
Match amperage, joint access, position, and machine output
Polarity
Most low-hydrogen 18-type rods run DCEP or AC, but verify package data
Lot certification
Critical work may require certs and traceability
Rod condition
Opened, damp, or damaged containers can cause hydrogen problems
Common Wrong-Part Mistakes
Buying 8018-C3 because it says “Cor-Ten” in a broad application list, without checking exposed corrosion requirements.
Using standard 7018 on unpainted weathering steel because the weld strength seems close.
Mixing 8018W and 8018-C3 in the same visible repair without documentation.
Ignoring the WPS because both rods are 80 ksi low-hydrogen electrodes.
Selecting by tensile strength only instead of corrosion behavior, toughness, and base-metal chemistry.
Inspection Steps
Confirm the steel grade from drawings, stampings, or mill documentation.
Read the electrode can: AWS class, diameter, heat/lot number, and storage instructions.
Check whether the weld will remain exposed, painted, buried, or sealed.
Compare the rod against the approved WPS before striking an arc.
Inspect opened electrodes for damaged flux, rust, oil, moisture exposure, or loose coating.
After welding, inspect bead profile, tie-in, slag removal, and any undercut before the patina hides detail.
Test Procedures
For non-code shop work, run a small test coupon using the same base metal, rod diameter, polarity, position, and cleaning method. Break or bend a sample only as a shop confidence check, not as a substitute for qualified procedure testing. For structural or code work, follow the approved WPS and required inspection method: visual, magnetic particle, ultrasonic, bend testing, tensile testing, or CVN impact testing as specified.
Field Fix vs Proper Fix
Situation
Field fix
Proper fix
Wrong rod opened but no weld made
Stop and relabel material
Order the WPS-specified electrode
Short noncritical tack made with wrong rod
Hold work and mark location
Remove tack and reweld with approved filler
Visible weathering weld made with mismatched filler
Do not bury problem with cosmetics
Engineer review, remove/repair if required
Damp low-hydrogen rods
Segregate from usable stock
Recondition only per manufacturer limits or discard
Corrosion mismatch: wrong filler can leave a weld that does not form the same protective oxide layer.
Impact failure risk: low-temperature service requires verified toughness, not just matching tensile strength.
Appearance rejection: architectural weathering steel often fails visually before it fails structurally.
Replacement Notes
When replacing electrodes for a weathering-steel job, match the AWS classification, diameter, package condition, cert requirements, and project WPS. If the old can is missing or illegible, do not assume 8018-C3 replaces 8018W. Mark it Unknown (Verify) until the base metal, design exposure, and required weld-metal properties are confirmed.
Use ventilation and respiratory protection appropriate for low-alloy SMAW fumes.
Remove coatings, oil, paint, and trapped moisture before welding.
Follow low-hydrogen storage rules from the electrode manufacturer.
Do not weld structural weathering steel without approved procedure control.
Hot weathering steel looks dull quickly; mark hot work and control fire exposure.
Bottom Line
For exposed weathering steel, 8018W is normally the safer first choice because it is built around weathering-steel compatibility. 8018-C3 is valuable when nickel toughness and low-temperature service are the controlling requirements, but it should not be treated as a direct weathering-steel substitute unless the job documents approve it.
Handheld Laser Welding vs MIG for Sheet Metal Repair: Where Each Process Fails
Handheld laser welding is rapidly gaining attention for thin-gauge fabrication, stainless repair, HVAC work, and cosmetic welding because it can produce narrow welds with lower heat input and minimal post-cleaning. MIG welding still remains the more forgiving process for field repair, poor fit-up conditions, contaminated metal, outdoor welding, and structural fabrication.
The biggest mistake shops make when comparing handheld laser welding to MIG is assuming laser welding is simply a faster replacement for wire welding. In reality, the two processes fail differently. Laser welding is far less tolerant of gaps, edge mismatch, reflective contamination, unstable shielding gas coverage, dirty surfaces, and poor joint preparation. MIG is slower and creates more heat distortion, but it usually handles repair conditions better when parts are imperfect.
Where Handheld Laser Welding Performs Best
Thin stainless fabrication
Sheet metal assemblies with tight fit-up
Cosmetic visible welds
Low-distortion repair work
HVAC and light manufacturing
Repeatable production welding
Modern handheld laser systems can produce significantly faster travel speeds than TIG welding with reduced post-processing requirements. Systems like the Miller OptX handheld laser platform also include preset parameters and integrated wire-feed capability for production-oriented applications.
Why Laser Welding Fails on Poor Fit-Up
Fit-up tolerance is one of the biggest differences between handheld laser welding and MIG welding.
MIG can bridge moderate gaps because filler deposition is relatively forgiving
Laser welding depends heavily on precise edge alignment
Gap variation destabilizes penetration consistency
Excessive gaps can create underfill, lack of fusion, or burn-through
Laser welding usually performs best when parts are tightly fitted with consistent edge preparation. Rust scale, warped sheet metal, uneven flange alignment, and damaged edges often create immediate process instability.
Gap Tolerance: MIG vs Handheld Laser
Condition
MIG Welding
Handheld Laser
Poor edge fit-up
Usually manageable
Often problematic
Dirty steel
More forgiving
Requires cleaner surface
Outdoor welding
Possible with precautions
More sensitive to environmental conditions
Thin gauge distortion
Higher risk
Lower heat input
Visible cosmetic welds
Requires cleanup
Often cleaner appearance
Structural gap filling
Better suited
Limited tolerance
Reflective Metals and Laser Instability
Reflective materials such as aluminum, polished stainless, copper alloys, and galvanized surfaces can create instability during laser welding.
Surface reflectivity affects beam absorption
Contamination changes penetration behavior
Inconsistent prep creates weld variation
Highly reflective surfaces may require different parameter tuning
MIG welding is generally more tolerant of inconsistent surface reflectivity, although contamination can still create porosity and instability.
Shielding Gas Requirements
Shielding gas selection matters significantly in both processes, but handheld laser systems can become unstable much faster if gas flow is incorrect.
The Miller OptX platform specifies argon and nitrogen process gases depending on the application. Incorrect shielding gas flow, nozzle contamination, or turbulence can quickly affect weld consistency and surface quality.
MIG welding generally tolerates small shielding inconsistencies better, especially during repair work.
Heat-Affected Zone Comparison
One major advantage of handheld laser welding is reduced heat input.
Smaller heat-affected zones
Reduced panel distortion
Less grinding and finishing
Lower visible discoloration on stainless
MIG welding remains more practical for thicker repair work, larger gaps, and inconsistent joint conditions where deposition volume matters more than minimal heat input.
Consumable Cost Differences
MIG systems typically use inexpensive consumables with broad availability:
Contact tips
Nozzles
Diffusers
Drive rolls
Liners
Handheld laser systems often involve higher replacement costs for optics protection components, specialty nozzles, cleaning consumables, and system maintenance parts.
Laser systems also introduce downtime considerations that many repair shops underestimate.
The Learning Curve Myth
Some handheld laser marketing claims the process is easier than MIG or TIG welding. While laser welding may simplify travel consistency and cosmetic appearance on properly prepared material, successful operation still requires process discipline.
Joint preparation matters more
Fit-up consistency becomes critical
Safety requirements increase significantly
Operators still need welding knowledge
Parameter selection still affects penetration and fusion quality
Repairability in Field Conditions
MIG welding remains the better process for many field repair environments.
Better tolerance for dirty or painted material
More forgiving outdoors
Easier generator compatibility
Better for inconsistent repair joints
Less sensitive to exact edge condition
Laser systems often perform best in controlled fabrication environments with consistent power quality and clean material preparation.
Power Requirements and Shop Limitations
Many handheld laser systems require significant input power compared to compact MIG systems. The Miller OptX 2kW platform specifies 32A single-phase 240V input requirements.
Small repair shops may need electrical upgrades before installing a handheld laser system safely.
Laser Welding PPE and Safety Concerns
Handheld laser systems create different safety requirements than conventional arc welding.
Class 4 laser hazards require strict eye protection protocols
Reflective surfaces increase risk exposure
Controlled welding zones may be required
Operators and nearby personnel need proper shielding protection
Fume extraction remains important despite lower visible smoke
Laser welding should never be treated as a casual replacement for conventional welding without proper training and safety controls.
When MIG Is Still the Better Choice
Farm repair
Heavy fabrication
Outdoor repair work
Structural welding
Poor fit-up conditions
Dirty or inconsistent material
Lower-budget repair environments
Where Handheld Laser Welding Makes Sense
Thin-gauge stainless fabrication
Cosmetic weld production
HVAC manufacturing
Precision fabrication
Automated or repeatable workflows
Applications where post-processing reduction matters
Sources Checked
Miller OptX handheld laser documentation, welding safety references, fabrication process comparisons, shielding gas guidance, and practical sheet metal repair workflows were reviewed for this article.
If a PAPR welding helmet has weak airflow, a low-flow alarm, fogging, heat buildup, or reduced breathing comfort, stop welding and troubleshoot before continuing. A PAPR depends on a battery-powered blower, correct filter, sealed hose, clean airflow path, and compatible helmet/headtop. Common causes are loaded filters, blocked spark arrestors or prefilters, weak batteries, loose hose connections, damaged breathing tubes, clogged inlet screens, poor face seal or shroud fit, and blower faults.
Do not silence or ignore a low-airflow alarm. Install a fully charged battery, replace the prefilter and main filter if loaded, inspect the hose and seals, verify the headtop connection, and perform the manufacturer’s airflow check with the correct flow indicator. If the unit still fails the airflow test, remove it from service and replace the failed component or send it for qualified service.
Battery capacity issue or filter loading under load
Test with fresh battery and clean filters
Blower runs louder than normal
Filter restriction or blower working against blockage
Inspect filter stack and inlet screen
No blower operation
Dead battery, bad contacts, switch/blower failure
Check battery seating and contacts
What the PAPR Airflow System Does
A powered air-purifying respirator uses a fan/blower to pull air through approved filters and deliver filtered air into the helmet or headtop. The filter protects against the approved hazard class only when the correct filter is installed, the blower delivers required airflow, the breathing tube is sealed, and the headtop is worn as designed. A PAPR is not a substitute for ventilation, fume extraction, confined-space controls, or correct filter selection.
Inspection Steps
Leave the weld area if airflow drops. Do not keep welding through a low-flow alarm.
Check battery charge and seating. Confirm the battery is fully charged, latched, and making clean contact.
Inspect the filter stack. Replace loaded, wet, damaged, expired, or wrong filters. Check prefilter and spark arrestor if equipped.
Inspect blower inlet and outlet. Remove dust, grinding debris, tape, bags, or blocked screens.
Inspect the breathing tube. Look for kinks, crushed sections, pinholes, cracks, loose swivels, and damaged O-rings.
Check headtop connection. The hose must lock into the helmet or hood without leaks.
Check face seal, shroud, or hood skirt. Tears, poor fit, or worn elastic can reduce protection and comfort.
Perform the airflow check. Use the manufacturer’s required flow indicator and procedure before welding.
Confirm the alarm works. Follow the manual’s alarm-check procedure; do not block hoses or sensors except as instructed.
Filter Loading and Airflow Loss
Welding fume, grinding dust, metal dust, and shop debris load filters faster than clean-air use. A clogged prefilter or spark arrestor can trigger alarms even when the main filter still looks usable. If airflow improves after replacing the prefilter but drops again quickly, check the work process, fume extraction, filter type, and whether grinding dust is overloading the system.
Field Fix vs Proper Fix
Problem
Field Fix
Proper Fix
Low-flow alarm
Stop welding and move to clean air
Replace loaded filters and pass airflow test
Weak battery
Install charged spare battery
Test charger, contacts, and battery runtime
Kinked hose
Reroute hose
Replace crushed or cracked breathing tube
Fogging in helmet
Check head seal and fan speed
Fix airflow restriction and worn shroud/seal
Alarm remains after new filters
Remove from service
Inspect blower, sensors, hose seals, and service parts
Common Wrong-Part Mistakes
Installing a filter from the wrong PAPR system because it appears to fit.
Using a particulate-only filter where gas/vapor cartridge protection is required.
Replacing the main filter but leaving a packed spark arrestor or prefilter in place.
Using a non-compatible breathing tube or helmet adapter.
Assuming a charged battery is good without checking runtime under blower load.
Using damaged head seals, shrouds, or hose O-rings and blaming the blower.
Compatibility Notes
PAPR parts must match the complete system approval: blower, battery, charger, filter/cartridge, prefilter, spark arrestor, breathing tube, belt, helmet/headtop, face seal or shroud, and airflow indicator. Do not mix 3M, Miller, Lincoln, ESAB, ArcOne, Jackson, or other PAPR components unless the manufacturer specifically approves the configuration. For verified WSP category references, see welding helmet and PAPR support by brand and ESAB welding helmet support.
What To Verify Before Ordering
PAPR brand, model, and approval label.
Blower unit part number and serial/date information.
Filter type required for welding fume and any coating, metal, or gas/vapor hazard.
Battery and charger model.
Breathing tube connection style and length.
Helmet/headtop model and face seal or shroud style.
Required airflow indicator or test kit.
Whether the system is still within service life and approved configuration.
Related Failure Paths
Low-flow alarm caused by filter loading.
Helmet fogging caused by weak airflow or seal damage.
Battery runtime collapse during long weld shifts.
Fume exposure caused by wrong filter type.
Blower overwork from blocked inlet screens or packed prefilters.
Loss of protection from torn shrouds, loose hoses, or mixed-brand parts.
Safety Notes
Do not use a PAPR that fails airflow, alarm, battery, or fit checks.
Do not bypass low-flow alarms, sensors, filters, or manufacturer interlocks.
Use only filters approved for the hazard; welding fume, stainless, galvanized, coatings, and solvents may require different controls.
PAPRs do not supply oxygen and are not for oxygen-deficient or immediately dangerous atmospheres unless specifically designed and approved for that use.
Maintain ventilation and fume extraction; a respirator is the last line of protection, not the only control.
Sources Checked
NIOSH PAPR overview.
3M PAPR system overview.
Weld Support Parts PAPR welding safety and helmet replacement support pages.
Weld Support Parts ESAB and welding helmet/PAPR support pages.
Welding helmet PAPR blog references for airflow, filter, and battery status.
If a welding helmet is hard to see through, will not stay up, flickers, fails to darken, or feels loose on the head, the repair usually starts with replacement parts—not a new helmet. The most common welding helmet replacement parts are outside cover lenses, inside cover lenses, sweatbands, headgear assemblies, batteries, ADF cartridges, lens seals, shell parts, magnifying lenses, hard hat adapters, and PAPR filters. The part must match the exact helmet series, lens size, cartridge style, and shell design before ordering.
Do not order by appearance alone. Two helmets can look similar and use different inside lenses, ADF cartridges, gasket profiles, or headgear hardware. Verify the brand, helmet series, model number, lens dimensions, ADF part number, battery type, and whether the hood is passive, auto-darkening, flip-front, grind-shield, hard-hat compatible, or PAPR-equipped.
Loaded filters, low battery, blocked hose, poor seal
What This Part Does
The outside cover lens protects the ADF or passive filter from spatter, sparks, grinding dust, and scratches. It is the part most shops replace first because it directly affects puddle visibility. The inside cover lens protects the rear side of the filter from dust, fingerprints, and fumes trapped inside the hood.
The ADF cartridge is the auto-darkening filter. If the helmet powers on but does not darken reliably after batteries and sensors are checked, the cartridge may be the failed component. The headgear assembly controls fit, balance, lift tension, and working position. A worn headgear can make a good helmet feel unsafe or unusable.
Sweatbands are low-cost wear items. They do not just improve comfort; they help keep the helmet stable on the head. Lens seals, gaskets, holders, and front frames keep the filter seated correctly and help prevent light leaks around the cartridge.
What Wears Out First
Outside cover lens: usually the first part to replace on MIG, flux-core, stick, and grinding-heavy work.
Sweatband: absorbs sweat and shop contamination; replace when it slips, smells, or loses shape.
Headgear: fails at ratchets, pivots, tension knobs, and adjustment slots.
Batteries: weak batteries cause delayed darkening, flicker, or failure to power the ADF.
Lens seals and holders: wear after repeated lens changes or heat exposure.
PAPR filters and pre-filters: load with fume and dust; replacement interval depends on exposure and manufacturer guidance.
Compatibility Notes
Helmet replacement parts are not universal unless the manufacturer states that they are. Lincoln VIKING 2450 and VIKING 3350 helmets both use KP2898-1 outside cover lenses and KP2930-1 sweatbands in the Lincoln parts data, but their inside cover lenses and ADF cartridges differ. The VIKING 2450 listing uses KP2931-1 inside cover lenses and KP2932-4 ADF cartridge, while the VIKING 3350 listing uses KP3044-1 inside cover lenses and KP3045-4 ADF cartridge.
The VIKING 3250D FGS uses larger front protection parts than standard VIKING shells, including KP3700-1 outside cover lenses, KP3701-1 inside cover lenses, KP3702-1 grind shield clear lens, KP3703-3 ADF cartridge, KP3704-1 replacement shell, and KP3706-1 headgear assembly.
Miller Performance and Classic helmet families use their own shell, lens cover, gasket, lens assembly, headgear, and battery tray part numbers. 3M Speedglas helmets also have series-specific outside plates, inside plates, filters, batteries, headbands, and hard-hat adapters. Dynaflux lists replacement cover lenses and auto-darkening replacement lenses by helmet family, including Miller, Jackson, and Speedglas-compatible listings. Treat every brand and series as its own parts system.
What To Verify Before Ordering
Helmet brand and exact series
Helmet model number or product number
ADF cartridge part number
Inside and outside cover lens dimensions
Battery type, if replaceable
Headgear style and pivot hardware
Shell version or graphic series, if shell replacement is needed
Hard hat adapter requirement
PAPR model, blower, filter, pre-filter, hose, and face seal style
Whether the helmet is passive, auto-darkening, flip-front, grind-shield, or PAPR
Common Wrong-Part Mistakes
Ordering a standard VIKING lens for an FGS grind-shield helmet.
Ordering an outside cover lens when the damaged part is the inside cover lens.
Replacing the ADF cartridge before checking batteries, sensors, and cover lens condition.
Assuming all 4-1/2 x 5-1/4 lenses fit every shell.
Buying a headgear assembly without confirming the pivot hardware.
Using a non-rated clear plastic sheet instead of a manufacturer lens cover.
Mixing PAPR parts from different blower or helmet systems.
Visual Wear Indicators
Replace the outside lens when scratches, spatter pits, fogging, distortion, or heat waves make it harder to see the puddle. Replace the inside lens when it is cloudy, cracked, coated with fume residue, or no longer locks flat in the filter frame. Replace headgear if the helmet drops unexpectedly, feels unbalanced, or cannot hold adjustment.
Inspect the shell for cracks around the lens frame, pivot mounts, and top edge. A cracked shell can allow light entry or fail to support the filter. On PAPR helmets, inspect the face seal, breathing tube, filter cover, pre-filter, and battery connection before assuming the blower is bad.
Inspection Steps
Clean the outside lens with a soft cloth and mild cleaner.
Remove the outside cover lens and inspect it under shop light.
Inspect the inside cover lens and ADF window.
Check ADF sensors for smoke film, tape, stickers, or spatter.
Replace batteries if the helmet uses serviceable batteries.
Cycle weld, grind, shade, delay, and sensitivity settings.
Inspect the headgear pivots, knobs, ratchet band, and sweatband.
Look for light gaps around the ADF holder and lens seal.
For PAPR systems, check airflow alarms, filter loading, hose connection, and face seal.
Test Procedures
After replacing helmet parts, perform a safe function check before welding. Confirm the ADF powers up, shade and delay controls respond, grind mode turns off before welding, and the helmet darkens consistently from multiple arc angles. Do not weld with a cracked lens, missing cover plate, missing gasket, damaged shell, or uncertain ADF response.
For PAPR helmets, follow the manufacturer airflow check procedure. If the low-flow alarm triggers after replacing the pre-filter or particle filter, inspect the breathing tube, battery charge, filter seating, and face seal. Do not treat a loaded filter as a comfort issue; it is a respiratory protection issue.
Field Fix vs Proper Fix
Problem
Field Fix
Proper Fix
Scratched outside lens
Clean lens to finish a non-critical task
Replace with correct outside cover lens
Loose helmet
Tighten knobs
Replace worn headgear assembly
Dirty sweatband
Wipe down
Replace sweatband
Weak ADF battery
Stop and replace battery
Use specified battery and confirm operation
Light leak
Do not weld
Replace seal, holder, lens, or shell as needed
PAPR low flow
Leave weld area
Replace filters or repair system per manufacturer procedure
For Lincoln VIKING 2450 and 3350 families, start by confirming whether the part needed is KP2898-1 outside cover lens, KP2930-1 sweatband, the correct inside lens, or the correct ADF cartridge for that series. For Miller helmets, use the correct Miller series breakdown before ordering shells, lens covers, gaskets, headgear, or ClearLight lens assemblies. For Speedglas, confirm the exact helmet family because 9002, 9100, G5, and PAPR systems do not share every part.
Unknown (Verify): cross-brand ADF cartridge swaps, non-OEM lens thickness, imported clone shell fitment, and hard-hat adapter fitment unless confirmed by the manufacturer or a verified parts breakdown.
Safety Notes
Do not weld with a cracked, missing, or improvised lens cover.
Do not bypass an ADF problem by increasing shade only; confirm the cartridge darkens correctly.
Turn grind mode off before welding.
Use only helmet parts rated for welding protection.
For PAPR equipment, follow employer respiratory protection rules and manufacturer service intervals.
If eye irritation, flash symptoms, or repeated ADF failure occurs, stop welding and inspect the helmet before reuse.
Sources Checked
Lincoln Electric 2024 Expendable Parts Guide
Lincoln Electric Accessories 2024 Product Catalogue
Miller Accessories and Consumables Catalog data
3M Speedglas welding helmet parts references
Dynaflux replacement lenses, faceshields, and headgear catalogue
Weld Support Parts helmet breakdown pages
Weld Support Parts Blog helmet visibility and helmet selection support pages
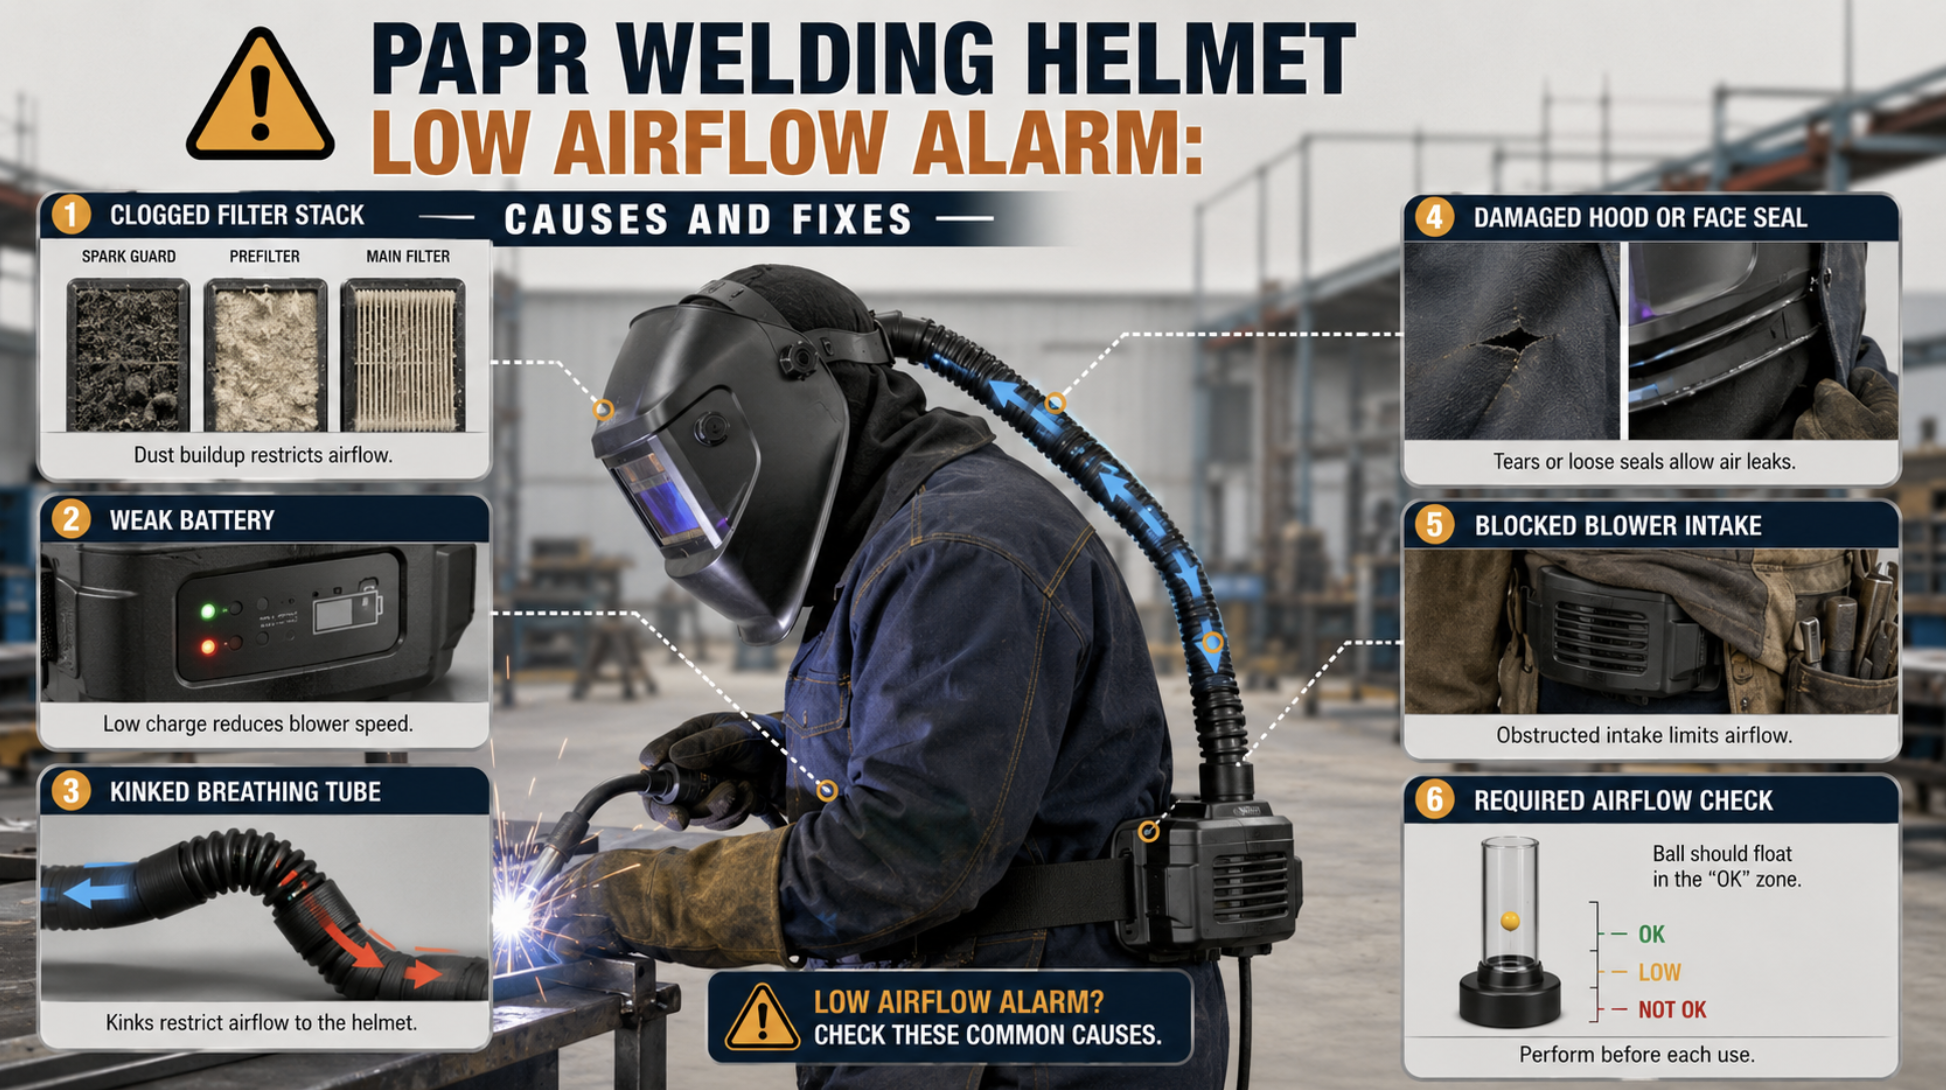
A PAPR welding helmet’s low airflow alarm usually means the blower cannot deliver the required air volume through the hood, breathing tube, filter stack, or battery-powered blower system. The most common causes are clogged filters, blocked prefilters, a weak battery, a kinked breathing tube, a damaged face seal or hood seal, or a system that has not passed its required airflow check before use.
A low airflow alarm should be treated as a stop-work warning, not a nuisance sound.
Clogged prefilters, spark guards, and main filters are the first items to inspect.
A charged battery does not prove the blower is delivering enough air.
Loose-fitting PAPR welding helmets still require correct assembly, airflow checks, and a respiratory protection program when used for required protection.
Do not mix non-approved filters, hoses, batteries, helmets, or blower parts across systems.
PAPR systems do not supply oxygen and must not be used in oxygen-deficient, unknown, or IDLH atmospheres.
Problem / Context
PAPR welding helmets are used to reduce exposure to welding fumes and particulates while improving comfort during long weld, grind, and fabrication work. A powered air-purifying respirator uses a battery-powered blower to pull contaminated air through approved filters or cartridges and deliver filtered air to the wearer’s breathing zone.
When the low airflow alarm sounds, the system may not be moving enough air through the breathing zone. That can happen during high-fume MIG, flux-core, stainless, galvanized, hardfacing, gouging, or grinding work. If the shop is also struggling with source capture, review welding fume extractor airflow troubleshooting because a PAPR should not be used as the only control when ventilation and fume extraction are required.
Root Causes
1. The Prefilter or Spark Guard Is Loaded
Grinding dust, spatter, smoke residue, and shop debris can load the outer protection layers before the main filter is fully used. A dirty prefilter or spark guard can restrict airflow enough to trigger the alarm even when the main filter looks usable.
2. The Main Filter Is Clogged or Wrong for the System
Main PAPR filters have specific fitment, approval, and service requirements. A clogged filter increases resistance and makes the blower work harder. A non-approved substitute may fit physically but fail the system approval or airflow requirement. Only use filters listed for the exact blower and helmet assembly.
3. The Battery Is Weak Under Load
A battery can show charge but still fail under blower load, especially if it is old, cold, damaged, or not fully seated. Low airflow alarms that appear late in a shift often trace back to battery capacity, dirty contacts, or a charger problem.
4. The Breathing Tube Is Kinked, Crushed, or Leaking
The breathing tube must move air from the blower to the helmet without restriction. Kinks behind the shoulder, crushed sections under a harness, loose bayonet fittings, torn cuffs, or heat damage can reduce airflow or leak filtered air before it reaches the helmet.
5. The Hood, Head Seal, or Face Seal Is Damaged
Loose-fitting PAPR helmets depend on the complete hood or head seal assembly. A torn seal, missing cape, worn head seal, or poorly seated helmet can disrupt the intended airflow pattern around the breathing zone. If the issue is mostly helmet fit and visibility, compare it with auto-darkening helmet fit and lens standards before assuming the blower is the only problem.
6. The Blower Inlet Is Blocked by Clothing or Position
A jacket, tool belt, harness, welding curtain, or body position can partially cover the blower intake. This can happen when welding out of position, crawling inside equipment, or leaning against a workpiece. The alarm may stop when the welder stands up because the intake is no longer blocked.
7. The System Was Not Flow-Tested Before Use
Many PAPR systems require a pre-use airflow check with a manufacturer-specified airflow indicator or procedure. Skipping this step can hide clogged filters, weak batteries, damaged tubes, or incorrect assembly until the alarm sounds during welding.
Solution
Step 1: Stop Welding and Move to Clean Air
Do not keep welding through a low airflow alarm. Stop the arc, leave the fume area when safe, and inspect the PAPR in clean air. A low airflow alarm means the respirator may not be performing as intended.
Step 2: Check the Filter Stack in the Correct Order
Inspect the spark guard, prefilter, main filter, filter cover, gasket, and latch. Replace loaded or damaged consumables according to the manufacturer’s instructions. Do not blow filters clean with compressed air unless the manufacturer specifically allows it. Compressed air can damage filter media or drive contamination deeper into the filter.
Step 3: Confirm Battery Seating, Charge, and Contacts
Remove and reseat the battery. Inspect contacts for dirt, corrosion, heat damage, or looseness. Confirm the charger is the correct charger for the battery. If the low-airflow alarm appears on one battery but not the other, tag the questionable battery out of service.
Step 4: Inspect the Breathing Tube
Run a hand along the full breathing tube. Look for flattened sections, cracks, melted spots, loose swivel fittings, missing O-rings, or damaged cuffs. Re-route the tube so it does not pinch when the welder bends, kneels, or turns the head.
Step 5: Inspect the Helmet Seal and Headgear
Check the hood seal, cape, head seal, sweatband, headgear, and helmet shell. Replace torn or contaminated soft goods. Do not tape over damaged seals as a permanent repair. If the helmet is uncomfortable enough that workers loosen or misposition it, the respiratory protection may not be used consistently. For half-mask alternatives under a hood, compare P100 welding respirator options and low-profile respirator fit under welding helmets.
Step 6: Run the Required Airflow Check
Use the manufacturer’s airflow indicator, test tube, or built-in test procedure. Pass/fail values are system-specific. Do not estimate airflow by feel. A helmet can feel breezy and still fail the required test, especially if the flow path is leaking or assembled incorrectly.
Step 7: Remove the System From Service if It Fails
If the PAPR fails the airflow check after filters, battery, tube, and seals are inspected, remove it from service. Tag the blower, battery, hose, or helmet assembly and follow the employer’s repair procedure. Do not return a failed respirator to production because replacement parts are inconvenient.
Specs / Verification Notes
Item to Verify
Why It Matters
Field Note
NIOSH approval
PAPR protection depends on approved complete assemblies.
Verify exact blower, helmet, filter, battery, and tube combination.
Airflow test method
Low airflow checks are system-specific.
Unknown (Verify in manual).
Filter part number
Wrong filters can void approval or restrict airflow.
Use manufacturer-listed filters only.
Prefilter and spark guard
Loaded outer layers can cause alarms before the main filter is fully spent.
Inspect before each shift.
Battery runtime
Runtime varies by battery age, filter load, airflow setting, and temperature.
Unknown (Verify).
Breathing tube condition
Kinks, leaks, and heat damage reduce delivered airflow.
Inspect full length.
Helmet seal or hood seal
Damaged soft goods can disrupt airflow pattern.
Replace damaged seals.
Hazard type
Particulate filters may not control gases or vapors.
Verify exposure and cartridge/filter selection.
Product Section
If the existing PAPR welding helmet repeatedly fails airflow checks or replacement parts are no longer available, a complete manufacturer-matched PAPR welding helmet system may be a better path than mixing parts. The listing below is for a Lincoln Electric VIKING 3350 XG PAPR welding helmet system. Confirm part number, battery type, included filters, replacement consumables, approval status, and workplace requirements before ordering.
No products found.
Comparison Table
Symptom
Likely Cause
Check First
Do Not Do
Alarm starts as soon as blower turns on
Blocked filter stack, wrong assembly, failed airflow test
Filter cover, prefilter, main filter, airflow indicator
Do not weld until it passes the test.
Alarm starts late in the shift
Battery sag or filter loading
Battery charge, charger, filter condition
Do not assume the battery is good by indicator lights only.
Alarm changes when bending or kneeling
Kinked tube or blocked blower intake
Tube routing, belt position, clothing interference
Do not route the tube under straps that crush it.
Helmet feels drafty but fails flow check
Leak, missing seal, wrong setup, or incorrect test method
OSHA 29 CFR 1910.134 requires an appropriate respiratory protection program when respirators are necessary to protect employee health. That program includes selection, medical evaluation, fit testing where required, use procedures, maintenance, training, and program evaluation. Loose-fitting PAPR hoods and helmets may not require fit testing, but they still require correct selection, training, inspection, cleaning, storage, and maintenance.
NIOSH describes PAPRs as reusable respirators that use a battery-powered blower to pull air through filters, cartridges, or canisters before delivering it to the breathing zone. PAPRs can protect against gases, vapors, or particles only when equipped with the correct approved filter, cartridge, or canister. A particulate PAPR filter should not be assumed to protect against gases, vapors, oxygen deficiency, or unknown atmospheres.
PAPR welding helmets do not supply oxygen. Do not use a PAPR in oxygen-deficient spaces, immediately dangerous to life or health atmospheres, confined spaces without proper evaluation, or areas with unknown contaminants. Welding stainless, galvanized, painted, coated, or plated materials may require exposure assessment, ventilation, source capture, and specific respiratory protection beyond a basic particulate setup.
FAQ
Can a PAPR welding helmet be used after the low airflow alarm sounds?
No. Stop welding and move to clean air when safe. Inspect the PAPR and run the required airflow check before returning it to service.
Does a full battery mean the PAPR airflow is safe?
No. Battery charge is only one part of the system. Filters, prefilters, tubes, seals, blower condition, and assembly all affect delivered airflow.
Can PAPR filters be cleaned with compressed air?
Do not clean filters with compressed air unless the manufacturer specifically allows it. Many filters are replaceable consumables, and compressed air can damage the media or spread contamination.
Do loose-fitting PAPR welding helmets require fit testing?
Loose-fitting PAPR hoods and helmets generally do not require fit testing, while tight-fitting PAPR facepieces do. OSHA respiratory protection requirements still apply when the respirator is required for workplace protection.
Can a PAPR replace fume extraction?
No. A PAPR is respiratory PPE, not source capture. Use ventilation, local exhaust, process controls, and exposure assessment as required by the job and employer program.
Can filters, batteries, or hoses be mixed between PAPR brands?
No. Use only parts approved for the exact PAPR assembly. Mixing parts can affect airflow, approval status, and respiratory protection.
Next Step
If the low airflow alarm keeps going off, start with the filter stack, battery, breathing tube, intake blockage, helmet seal, and required airflow test. If the system fails after approved replacement consumables are installed, remove it from service. For broader shop exposure control, pair this check with fume extractor troubleshooting and verify whether the job requires a PAPR, half-mask respirator, ventilation change, or process control.
Sources Checked
Weld Support Parts Blog: Lincoln K3930-1 PAPR Powered Air Purifying Respirator with Black Viking 3350 Welding Helmet.
Weld Support Parts Blog: ArcOne AP1K-V-BFFVX AirPlus w/Vison BFFVX Kit.
Weld Support Parts Blog: Welding Fume Extractor Not Pulling Smoke: Causes and Fixes.
Weld Support Parts Blog: Best Welding Respirator for Fumes (P100) – Top 3 3M Picks.
Weld Support Parts Blog: Miller LPR-100 Gen II Half Mask Respirator.
Weld Support Parts Blog: Welding Galvanized: Safe Fume Control Tactics.
Weld Support Parts Blog: Auto-Darkening Welding Helmet Buying Guide 2025.
OSHA 29 CFR 1910.134 Respiratory Protection.
NIOSH Powered Air-Purifying Respirators page.
3M Powered Air Purifying Respirator overview.
Lincoln Electric VIKING 3350 PAPR / VIKING 3350 XG PAPR product and operator manual references.
Amazon listing checked for ASIN B0FC2PRFV8: Lincoln Electric VIKING 3350 XG PAPR with Standard Battery.
To provide the best experiences, we use technologies like cookies to store and/or access device information. Consenting to these technologies will allow us to process data such as browsing behavior or unique IDs on this site. Not consenting or withdrawing consent, may adversely affect certain features and functions.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.