Search results for: “troubleshooting”

  • Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown: Troubleshooting and Buying Checks

    Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown: Troubleshooting and Buying Checks

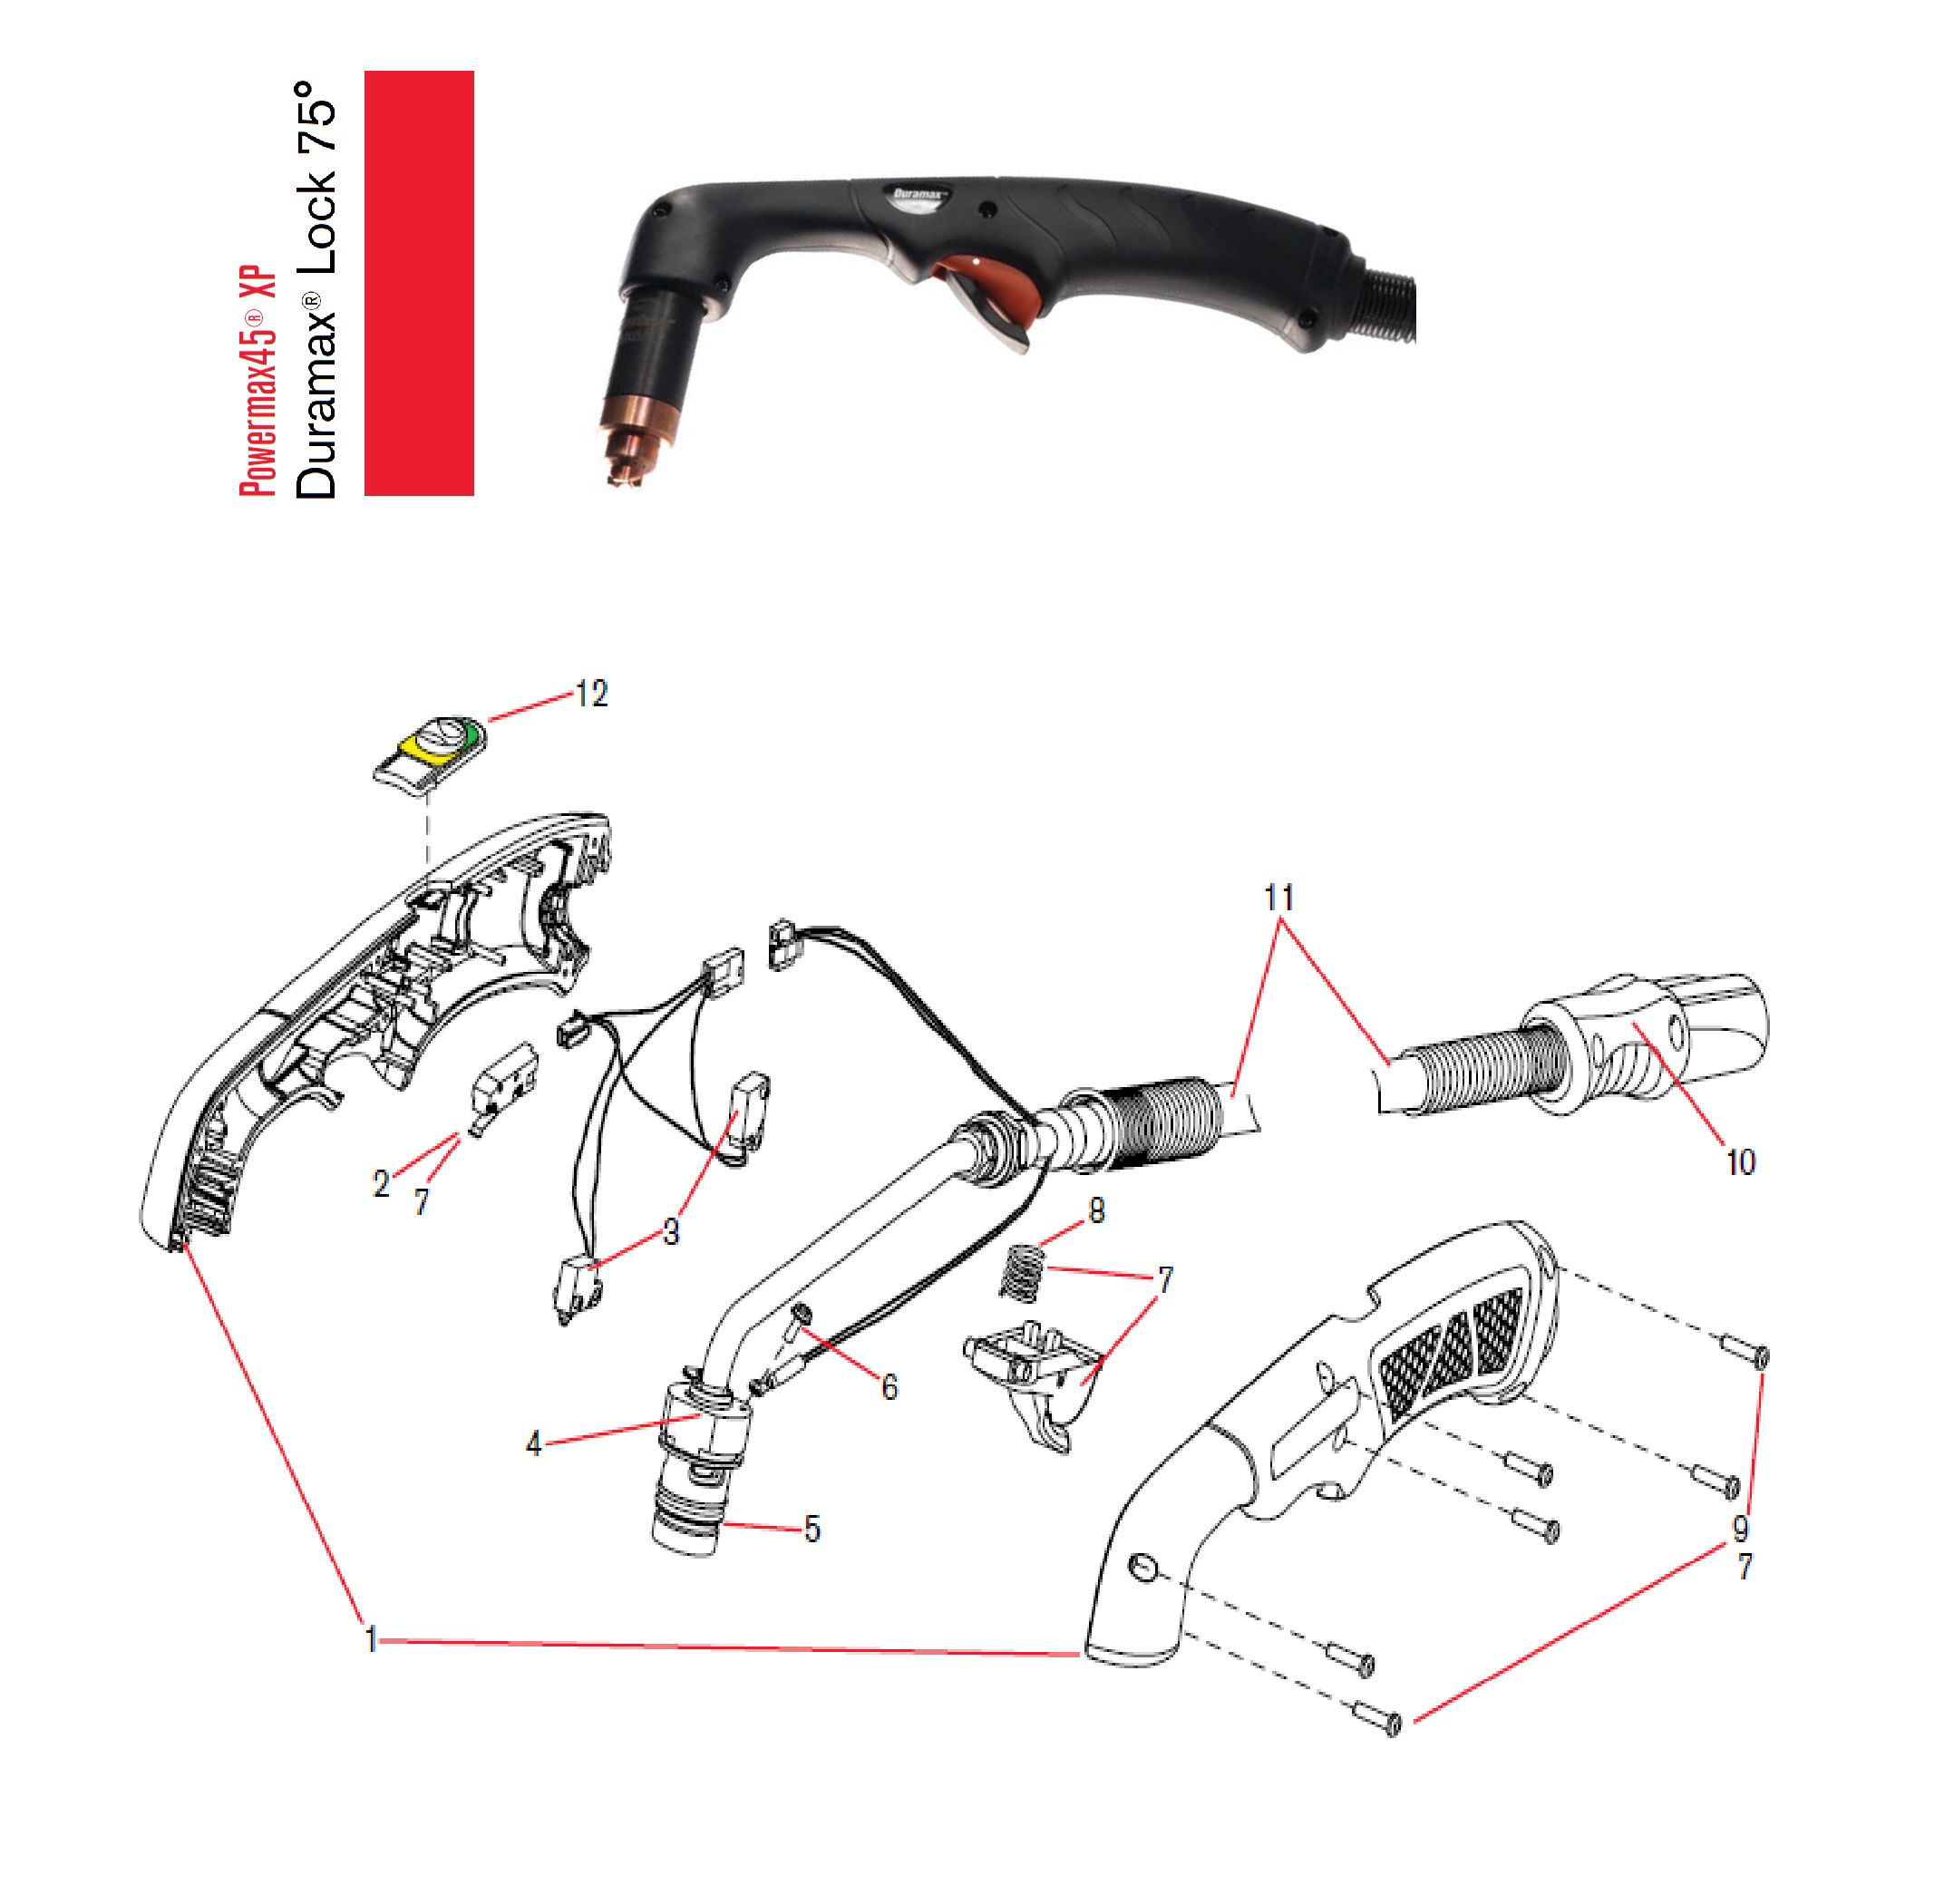
    Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown

    If a Hypertherm Duramax Lock 75 degree hand torch is cutting poorly, the first problem is often not the power source. In many cases the issue is in the torch head, consumables, lead connection, or shield/nozzle stack. This guide gives a practical parts breakdown and a buying check process for maintenance teams and support staff who need to verify what to inspect before ordering replacements.

    Key Takeaways

    • Start with the torch side: consumables, retaining hardware, and visible damage around the head.
    • Confirm the torch family and cut mode before ordering anything.
    • Use the WSP lookup page as the source-backed starting point for part identification.
    • Do not assume a consumable is correct because it looks similar; verify against the torch and machine context.
    • If fit is uncertain, mark it Unknown (Verify) and keep the review with the manufacturer or approved supplier.

    Parts breakdown: what to inspect first

    For a 75 degree hand torch setup, begin at the working end and move back toward the lead. The exact internal stack can vary by torch family and machine context, so treat this as a check sequence, not a universal assembly map.

    • Shield or drag shield: Inspect for heat damage, heavy spatter, distortion, and worn edges.
    • Nozzle: Check for orifice wear, pitting, ovality, and side damage.
    • Electrode: Look for deep wear, abnormal erosion, and arc instability symptoms.
    • Swirl ring / gas distribution part: Verify that it is present, seated correctly, and free of cracks or burn marks.
    • Retaining cap or retaining hardware: Confirm threads, seating faces, and torque condition are not damaged.
    • Torch head and locking interface: Inspect for looseness, cracked plastic, damaged seals, or signs of overheating.
    • Lead and strain relief: Check for cuts, kinks, softened insulation, or intermittent operation near the handle.

    Troubleshooting sequence: check, inspect, verify

    1) Check the symptom pattern

    Before replacing parts, identify the failure mode. A no-start condition, weak pilot arc, arc dropout, poor cut quality, or excessive dross can point to different causes. Do not jump to a torch-head replacement until the symptom is matched to the wear pattern.

    2) Inspect consumables as a set

    Remove the front-end parts and inspect them together. A single damaged nozzle may be the visible fault, but a worn electrode or damaged swirl ring can be the root cause. Check for:

    • Mismatch in wear between electrode and nozzle.
    • Evidence of overheating, such as discoloration or warped edges.
    • Carbon tracking, spatter buildup, or contamination in the torch head.
    • Loose fit or poor seating that could interrupt gas flow.

    Verify that the parts being removed match the torch family in service. If the part numbers are not clearly readable, Unknown (Verify) applies until the WSP lookup or approved documentation confirms the match.

    3) Inspect the torch head and lock interface

    The 75 degree hand torch head can see mechanical stress from repeated handling, workpiece contact, and lead movement. Check the lock area for wear that may prevent the consumables from seating correctly. If the retaining cap does not tighten smoothly, do not force it. Cross-threading, damaged threads, or a heat-warped seat can create intermittent arc faults.

    4) Verify gas and electrical continuity indirectly

    Without assuming hidden specs, verify the practical conditions that support a stable arc: the front-end parts are clean, seated, and undamaged; the lead is not pinched; and the machine displays no unrelated fault that points away from the torch. If the torch behavior changes when the lead is moved, treat the lead and strain relief as suspect.

    WSP lookup: use it before buying

    The WSP lookup page for this torch family is the best source-backed starting point for parts identification and buying checks:

    Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown on WSP

    Use that page to confirm the torch family, part naming, and catalog-backed item numbers where shown. Do not treat a visual match alone as enough proof. If a component is listed in the lookup but your torch head shows a different geometry, mark the fit as Unknown (Verify) and confirm with the supplier or manufacturer before ordering.

    Buying checks for maintenance teams

    When purchasing torch parts, use these checks in order:

    1. Match the torch family: Confirm the torch is the Hypertherm Duramax Lock 75 degree hand torch variant referenced by the lookup page.
    2. Match the machine context: Use the actual machine and torch pairing in service, not a similar setup from another bay.
    3. Match the wear pattern: Replace the damaged front-end part plus any companion part that shows related wear.
    4. Check the lock and seating surfaces: If the interface is damaged, parts alone may not fix the fault.
    5. Verify the buy link path: Use only approved links from the source page or internal support references.

    If a replacement is being considered because of repeated arc failure, review the torch-side troubleshooting first. Related guidance is available here: Plasma Cutter Pilot Arc Failure Troubleshooting and Plasma Drag Shield Compatibility Guide.

    Safety notes

    • De-energize the system before removing or handling consumables.
    • Allow hot parts to cool before inspection.
    • Do not file, force, or modify front-end parts to make them fit.
    • If a torch head is cracked, burned, or electrically unstable, remove it from service until reviewed.
    • Use manufacturer review for any fit or safety-critical uncertainty.

    FAQ

    Why does a new consumable set still cut poorly?

    A new set can still perform badly if the torch head is damaged, the retaining hardware does not seat correctly, the lead is compromised, or the wrong consumable family was installed. Inspect the whole front end, not just the nozzle.

    What should I replace first when the torch shows arc dropout?

    Start with the consumables and the torch-side seating surfaces. If those are clean and the problem continues, inspect the lead, strain relief, and the machine-side fault indications. Do not assume the power source is the root cause.

    How do I confirm I am buying the right part?

    Use the WSP lookup page, confirm the torch family and item naming, and compare the existing installed parts to the lookup record. If anything does not align, mark it Unknown (Verify) and confirm before purchase.

    Can I use a similar-looking shield or nozzle from another torch?

    No. Similar appearance is not enough. Verify the exact torch family, geometry, and use case before ordering or installing any replacement part.

    Sources Checked

    Where exact fit or part identity could not be confirmed from the provided source record, the correct status is Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Troubleshooting Weld Quality Before Replacing Parts

    Tweco MSAK-354 Control Wire Assembly for MIG Guns - High Quality Welding Parts
    “>Tweco MSAK-354 Control Wire Assembly for MIG Guns - High Quality Welding Parts

    If weld quality drops, do not start by replacing parts. Most issues come from process settings, consumables, shielding gas, ground connection, wire feed, or operator technique. Use this weld quality troubleshooting guide to isolate the cause before you spend time and money on parts.

    Key Takeaways

    • Check the process first: voltage, wire feed speed, polarity, gas flow, and work lead condition.
    • Inspect consumables and wire path before replacing gun parts.
    • Confirm the base metal, joint prep, and fit-up are correct.
    • Look for contamination, drafts, or poor shielding before changing hardware.
    • Replace parts only after the problem is isolated.

    Start With the Welding Process

    Many weld defects are process related, not part failures. Verify the following before opening the gun or feeder.

    • Voltage and wire feed speed: Check that settings match the procedure or WPS. Incorrect balance can cause spatter, lack of fusion, burn-through, or cold lap.
    • Polarity: Confirm polarity is correct for the wire type. Incorrect polarity can create unstable arc behavior.
    • Travel speed: Too fast can cause undercut or lack of fusion. Too slow can create excess reinforcement or burn-through.
    • Stickout / CTWD: Excessive stickout can reduce arc stability and increase spatter.

    Check Shielding Gas First

    Shielding gas problems can look like bad consumables or a failing gun. Verify gas setup before replacing parts.

    • Gas type: Confirm the gas matches the wire and procedure. Unknown (Verify).
    • Flow rate: Set the flow according to the application and nozzle size. Unknown (Verify).
    • Leaks: Inspect hoses, fittings, and the gun connection for leaks.
    • Drafts: Air movement around the weld area can break shielding and cause porosity.
    • Nozzle condition: Spatter buildup or damage can disturb gas coverage.

    Inspect the Wire Feed System

    Wire feed instability can create arc fluctuation, burnback, and inconsistent bead shape.

    • Drive rolls: Check for correct size and wear. Unknown (Verify).
    • Drive pressure: Too loose causes slipping. Too tight can deform wire.
    • Liner condition: A dirty or worn liner can cause feeding issues and inconsistent current transfer.
    • Spool tension: Excess drag can cause jerky feed.
    • Wire quality: Rust, contamination, or kinks can create feeding problems.

    Review Consumables and Contact Surfaces

    Before replacing a control wire assembly or gun component, inspect the basic wear items first.

    • Contact tip: A worn, oversized, or blocked tip can cause erratic arc behavior.
    • Nozzle: Spatter buildup can restrict gas coverage and reduce visibility.
    • Diffuser / retaining parts: Loose or damaged components can affect alignment and shielding.
    • Work clamp: A poor ground connection can cause arc instability and poor penetration.

    Check the Base Metal and Joint Prep

    Weld quality problems often start at the joint.

    • Surface contamination: Oil, paint, rust, mill scale, and moisture can cause porosity and fusion problems.
    • Joint fit-up: Excessive gap or poor alignment can lead to inconsistent bead profile.
    • Material thickness: Unknown (Verify) if the selected process and settings are suitable.
    • Preheat / interpass temperature: Unknown (Verify) where required by procedure.

    Common Symptoms and What to Check

    • Porosity: Check gas coverage, leaks, contamination, drafts, and nozzle condition.
    • Excess spatter: Check voltage, wire feed speed, polarity, stickout, and contact tip wear.
    • Wire burnback: Check wire feed speed, tip condition, liner drag, and drive roll pressure.
    • Erratic arc: Check ground connection, liner, contact tip, gas flow, and spool drag.
    • Lack of fusion: Check voltage, travel speed, joint prep, and cleaning.

    When a Part Replacement Makes Sense

    Replace parts only after the problem follows the component or shows clear wear. For MIG gun control and feed-related issues, the Tweco MSAK-354 Control Wire Assembly for MIG Guns may be a relevant replacement option when the original assembly is damaged or no longer performing as expected. Use the part only if it matches the existing setup. Compatibility is Unknown (Verify).

    Tweco MSAK-354 Control Wire Assembly for MIG Guns - High Quality Welding Parts

    Tweco MSAK-354 Control Wire Assembly for MIG Guns – High Quality Welding Parts

    Introducing the MSAK-354 Control Wire Assembly, a premium component designed to enhance your MIG welding experience. This high-quality control wire assembly is manufactured by Tweco, a reputable name in the welding industry. Precision-engineered, the MSAK-354 provides reliable performance and durability that meets the demands of both professional welders and DIY enthusiasts. The MSAK-354 is essential for ensuring…

    View at Arc Weld Store

    Do not assume the control wire assembly is the cause of poor weld quality until you have checked process settings, gas coverage, wire feed, and consumables.

    Support Workflow for Maintenance Teams

    1. Document the defect type: porosity, spatter, lack of fusion, undercut, burnback, or instability.
    2. Verify machine settings against the procedure or WPS.
    3. Inspect gas, wire feed, liner, tip, nozzle, and work clamp.
    4. Clean the joint and verify fit-up.
    5. Run a test weld after each change so you know what corrected the issue.
    6. Replace parts only after the fault is isolated.

    Safety Notes

    • Lock out and tag out equipment before inspecting internal components where required by site rules.
    • Allow hot parts to cool before handling.
    • Wear proper PPE when checking weld equipment and performing test welds.
    • Do not bypass safety interlocks or use damaged cables, connectors, or gas hoses.
    • Use ventilation and follow your shop’s fume control procedures.

    FAQ

    Why does the weld look bad if the machine seems fine?
    Weld appearance can be affected by shielding gas, contamination, wire feed instability, joint prep, or technique. A machine can operate normally while the process is still out of control.

    Should I replace the gun first?
    No. Check the consumables, wire path, work clamp, gas delivery, and settings first. Replace the gun or its components only after you isolate the fault.

    Can a bad ground cause porosity?
    Yes. A poor work connection can contribute to unstable arc behavior and poor bead quality.

    What is the fastest way to narrow it down?
    Make one change at a time and run a short test weld. That is the most reliable way to separate process issues from hardware issues.

    Sources Checked

    • ArcWeld product information for Tweco MSAK-354 Control Wire Assembly for MIG Guns
    • Internal drafting requirements provided for this article
  • Lincoln Electric FlexCut 45 Plasma Cutter Troubleshooting, Consumables, and Air Supply Setup

    If your Lincoln Electric FlexCut 45 plasma cutter is producing excessive dross, struggling to maintain arc stability, refusing to transfer the pilot arc, or rapidly consuming tips and electrodes, the problem is often related to air quality, consumable wear, grounding issues, or incorrect setup. Operators commonly mistake these symptoms for a failed torch or power supply when the root cause is frequently restricted airflow, incorrect consumable installation, poor work clamp connection, or moisture contamination in the air system.

    The FlexCut 45 is designed for handheld plasma cutting applications where consistent air delivery, proper consumable fitment, and clean electrical connections are critical. Before replacing expensive components, verify the torch consumables, inspect swirl rings and retaining caps, confirm compressor output, and check for contamination inside the torch head. Many intermittent arc faults and poor cut quality complaints are resolved during basic inspection and setup verification.

    Common FlexCut 45 Symptoms

    • Pilot arc starts but will not transfer to the workpiece
    • Heavy bottom-edge dross during mild steel cutting
    • Uneven kerf width or wandering cut path
    • Torch consumables burning up quickly
    • Intermittent torch shutdowns during extended cutting
    • Arc sputtering or unstable plasma stream
    • Difficulty piercing thicker material
    • Poor cut edge quality on clean steel
    • Excessive moisture inside torch consumables
    • Torch overheating during continuous operation

    Most Likely Causes

    • Low inlet air pressure or restricted airflow
    • Moisture contamination from the compressor system
    • Incorrect tip and electrode installation
    • Worn electrode hafnium insert
    • Damaged retaining cap or swirl ring
    • Poor work clamp grounding
    • Torch lead damage or excessive bending
    • Incorrect amperage selection for material thickness
    • Improper torch stand-off distance
    • Using damaged or mixed consumable sets

    Quick Diagnostic Checks

    Inspection AreaWhat To CheckTypical Problem
    Air SupplyDry, stable compressed airMoisture causing unstable arc
    ElectrodeInspect hafnium pit depthHard starts and weak arc
    Tip OrificeRound, undamaged openingWandering or angled cuts
    Ground ClampClean metal contactPilot arc will not transfer
    Torch CableKinks, cuts, heat damageIntermittent cutting
    Cooling AirflowVentilation openings clearThermal shutdown

    Consumable Wear Indicators

    One of the most common FlexCut 45 service mistakes is replacing only the electrode or only the tip after severe wear. Plasma consumables function as a matched system. If the electrode is deeply worn, the tip orifice may already be distorted from unstable arc behavior. Running mixed-wear consumables often creates poor cut quality and shortens the life of new parts.

    • Electrode pit becoming excessively deep
    • Tip opening becoming oval-shaped
    • Visible torch spatter buildup inside retaining cap
    • Burn marks on swirl ring surfaces
    • Difficulty maintaining consistent stand-off
    • Double arcing inside the torch

    Air System Problems and Moisture Contamination

    Compressed air quality directly affects plasma cutter performance. Oil contamination, excessive moisture, and fluctuating compressor output will dramatically reduce consumable life. Operators frequently assume the plasma cutter itself has failed when the actual issue originates upstream in the air system.

    Install a properly sized filter and dryer system whenever possible. Drain compressor tanks regularly and inspect inline separators for saturation. If the torch begins cutting inconsistently after long run times, moisture buildup may be accumulating in the airline.

    Cut Quality Problems

    Excessive dross and bevel angle are usually setup-related rather than machine failure. Travel speed, torch height, consumable condition, and amperage selection all affect cut quality. Dragging the torch incorrectly or holding excessive stand-off distance can quickly produce rough edges and slag accumulation.

    • Slow travel speed often creates heavy bottom dross
    • Excessive stand-off can widen the kerf and reduce penetration
    • Worn tips produce angled or uneven cuts
    • Poor grounding causes unstable transfer arc behavior
    • Dirty steel surfaces may reduce arc consistency

    Field Fix vs Proper Repair

    Some operators temporarily restore cutting performance by cleaning consumables or increasing air pressure, but these fixes usually provide limited improvement if the consumables are already damaged. Severely worn electrodes and distorted tips should be replaced rather than reused.

    Likewise, wrapping leaking air fittings with thread tape may reduce leakage temporarily, but recurring pressure instability should be corrected with proper regulator, hose, or fitting replacement.

    Related Failure Paths

    • Dirty air systems accelerate torch wear
    • Damaged consumables increase nozzle overheating
    • Poor grounding stresses pilot arc components
    • Overheating from blocked ventilation may shorten internal component life
    • Incorrect extension cord sizing can create voltage instability

    Compatibility and Setup Notes

    • Machine Model: Lincoln Electric FlexCut 45
    • Process Type: Air plasma cutting
    • Input Requirements: Verify OEM specifications before installation
    • Compressed Air Requirement: Clean and dry compressed air required
    • Torch Compatibility: OEM consumables recommended
    • Extension Cord Compatibility: Verify conductor size and amperage rating
    • Generator Compatibility: Unknown (Verify)

    Safety Notes

    Plasma cutting systems generate intense ultraviolet radiation, molten metal spray, noise, and electrically energized components. Operators should use approved welding PPE including shaded eye protection, gloves, flame-resistant clothing, and respiratory protection where required. Keep combustible materials away from cutting areas and ensure adequate ventilation for fumes and airborne particulates.

    Never service torch consumables with power connected to the machine. Allow components to cool before inspection and replacement.

    Frequently Asked Questions

    Why does the pilot arc start but not transfer?

    The most common causes are poor grounding, contaminated material surfaces, worn consumables, or insufficient air pressure.

    Why are my consumables wearing out so fast?

    Moisture contamination, incorrect torch distance, excessive pierce height, or damaged airflow components are common causes of premature wear.

    Can dirty compressed air damage the torch?

    Yes. Moisture and oil contamination can destabilize the plasma stream and rapidly damage electrodes and tips.

    Sources Checked

    • Lincoln Electric FlexCut 45 OEM product information
    • Lincoln Electric equipment catalogues
    • Lincoln Electric expendable parts guide
    • General welding safety guidance and PPE documentation
  • Stick Welding Undercut Troubleshooting

    Stick Welding Undercut Troubleshooting

    Undercut in stick welding appears as a groove melted into the base metal along the weld toe that is not filled properly by weld metal. It is commonly caused by excessive amperage, incorrect rod angle, excessive travel speed, poor weave control, or improper electrode manipulation. Undercut weakens weld strength, creates stress concentration points, and can cause weld rejection on structural and code work.

    Common Symptoms

    • Visible groove along the weld toe.
    • Sharp edge transitions beside the weld bead.
    • Weld bead appears narrow or rope-like.
    • Undercut worsens near restarts or weave edges.
    • Grinding reveals reduced weld toe thickness.
    • Excessive spatter and aggressive arc behavior.

    Likely Causes

    • Amperage too high: Excess heat melts the base metal faster than filler metal can refill the edges.
    • Travel speed too fast: Rapid movement prevents the puddle from filling the weld toes completely.
    • Incorrect rod angle: Excessive drag or push angle concentrates heat on one edge.
    • Excessive weave width: Wide weaving cools the puddle unevenly and leaves the edges underfilled.
    • Arc length too long: Long arcs create unstable puddles and aggressive sidewall washout.
    • Poor pause timing: Insufficient pause at weave edges prevents toe fill.

    Inspection Steps

    1. Inspect both weld toes for grooves or sharp edge transitions.
    2. Verify amperage settings match the electrode size and position.
    3. Check rod angle during welding.
    4. Review travel speed and weave width.
    5. Inspect restarts for localized undercut.
    6. Inspect work clamp connection and arc stability.
    7. Verify electrode condition and storage.

    Visual Wear Indicators

    • Sharp grooves along weld edges.
    • Thin weld toes.
    • Overly convex or narrow bead profile.
    • Irregular weave spacing.
    • Excessive sidewall washout.

    Common Wrong-Part Mistakes

    • Using oversized electrodes on thin material.
    • Running low-hydrogen rods at excessive amperage.
    • Using the wrong polarity for the electrode type.
    • Trying to cover undercut with additional cold passes instead of grinding and repairing properly.

    Field Fix vs Proper Fix

    Field fix: Lower amperage slightly, shorten arc length, slow travel speed, and pause briefly at weave edges. Proper fix: Grind out severe undercut, correct the welding procedure, improve rod manipulation technique, and match electrode size to the joint geometry and material thickness.

    Related Failure Paths

    • Slag inclusion
    • Lack of fusion
    • Toe cracking
    • Porosity
    • Cold lap

    Safety Notes

    Grinding out undercut creates sparks, debris, and airborne particles. Use proper eye protection, gloves, hearing protection, and ventilation during weld repair and cleanup operations.

    Sources Checked

    • Lincoln consumables catalogs
    • Lincoln welding equipment references
    • Uploaded welding safety and consumable references
  • MIG Birdnesting Troubleshooting Guide: Causes, Fixes & Wire Feed System Compatibility

    MIG wire birdnesting is one of the most common wire feed failures in both hobby and production welding environments. The problem usually appears as tangled welding wire packed behind the drive rolls or inside the feeder area after the wire stops feeding correctly.

    Birdnesting is trending heavily across welding forums, repair searches, and support communities because modern inverter MIG welders, long gun cables, soft aluminum wire, worn liners, and incorrect drive roll tension continue creating feed reliability problems.

    This guide explains the most common causes of MIG birdnesting, how to diagnose the failure correctly, compatibility issues between consumables and feeder systems, and what to inspect before replacing parts.

    Key Takeaways

    • Most birdnesting starts because wire feed resistance exceeds drive roll control.
    • Incorrect drive roll tension is one of the most common causes.
    • Worn liners frequently create intermittent feed drag.
    • Soft aluminum wire increases birdnesting risk dramatically.
    • Long MIG gun cables increase feed resistance.
    • Oversized or damaged contact tips commonly trigger burnback and birdnesting.
    • Poor wire spool tension can overload the drive system.
    • Knurled rolls used on solid wire can deform wire and worsen feeding.

    What MIG Birdnesting Looks Like

    Birdnesting occurs when welding wire stops moving through the gun normally while the drive rolls continue feeding wire. The wire then collapses and tangles near the feeder assembly, creating a compact “bird nest” of wire.

    This usually happens:

    • Behind the drive rolls
    • At the inlet guide
    • Inside the feeder housing
    • Near the gun connection block

    Common Symptoms

    SymptomLikely CauseSeverityCommon Related Part
    Wire bunches at feederExcessive feed resistanceHighLiner
    Burnback into tipFeed interruptionHighContact tip
    Intermittent feedingDirty or worn linerMediumMIG liner
    Wire shavingIncorrect drive rollsMediumDrive rolls
    Feed motor slippingImproper tension settingsMediumDrive assembly
    Aluminum wire collapsingPush distance too longHighMIG gun

    Most Common Causes of MIG Birdnesting

    1. Incorrect Drive Roll Tension

    Excessive drive roll pressure crushes welding wire and increases drag inside the liner. Insufficient pressure allows slipping.

    Proper tension normally allows the wire to stop against resistance without severe wire deformation.

    2. Worn or Dirty MIG Liner

    Liners collect metal dust, rust particles, wire shavings, and contamination over time. Increased liner resistance is one of the leading causes of feed instability.

    Steel liners eventually wear grooves internally, especially with high wire volume production welding.

    3. Wrong Drive Roll Type

    Drive roll selection must match wire type.

    Wire TypeRecommended Roll TypeNotes
    Solid steel wireV-grooveMost common MIG setup
    Flux-core wireKnurledImproves traction
    Aluminum wireU-groovePrevents wire deformation
    Soft alloy wireU-grooveReduces crushing

    4. Contact Tip Restrictions

    Undersized, worn, or partially blocked contact tips create wire drag and feed stoppage.

    Burnback often starts after wire movement slows at the contact tip.

    5. Long MIG Gun Cable Length

    Long gun assemblies increase wire friction. This becomes significantly worse with aluminum wire and small-diameter solid wire.

    Many birdnesting issues appear after upgrading from a 10 ft gun to a 15–25 ft assembly without adjusting feeder settings.

    6. Aluminum Wire Feeding

    Soft aluminum wire is highly prone to collapsing under drive roll pressure. Push-only feeding systems commonly struggle with aluminum over long cable distances.

    Spool guns and push-pull systems are often used specifically to reduce aluminum birdnesting problems.

    Compatibility Notes

    Before replacing MIG feed components, verify:

    • Wire diameter
    • Drive roll style
    • Liner diameter
    • MIG gun length
    • Wire type
    • Contact tip size
    • Feeder compatibility
    • Gun amperage rating
    • Spool gun compatibility
    • Drive roll groove sizing

    Unknown (Verify) for imported MIG gun consumable interchangeability unless OEM documentation confirms compatibility.

    Inspection & Troubleshooting Steps

    1. Disconnect welding power.
    2. Remove the contact tip.
    3. Feed wire manually through the gun.
    4. Check for drag or resistance.
    5. Inspect drive roll wear.
    6. Verify drive roll type matches wire.
    7. Reduce excessive tension pressure.
    8. Inspect liner contamination.
    9. Check inlet guide alignment.
    10. Inspect spool brake tension.
    11. Replace damaged contact tips.
    12. Test feed speed under load.

    Parts Most Commonly Responsible

    PartFailure ModeCommon Wear SignsVerify Before Ordering
    MIG linerFeed dragErratic wire movementWire diameter & gun length
    Drive rollsWire slippingPolished groovesGroove style & wire size
    Contact tipBurnbackOval openingWire diameter
    Gun neckFeed restrictionExcessive heatGun series
    Inlet guideWire shavingSharp edgesFeeder compatibility
    Spool hub brakeExcess dragJerky spool movementMachine model

    What Usually Wears Out First

    • Contact tips
    • MIG liners
    • Drive roll grooves
    • Inlet guides
    • Gun neck strain points
    • Feeder tension springs

    Field Fix vs Proper Fix

    ProblemTemporary FixProper Repair
    Minor liner dragBlow out linerReplace liner
    BurnbackTrim wire and replace tipCorrect feed restriction
    Wire slippingIncrease tension slightlyReplace worn drive rolls
    Aluminum birdnestingShorten gun cableUse spool gun or push-pull system

    Common Wrong-Part Mistakes

    • Using knurled rolls with solid wire
    • Installing oversized liners
    • Using incorrect contact tip size
    • Running aluminum wire through worn steel liners
    • Using excessively long MIG guns for soft wire
    • Installing generic consumables without verifying fitment

    Related Failure Paths

    • Burnback failures
    • Porosity from unstable arc
    • Drive motor overload
    • Excess spatter
    • Wire shaving contamination
    • Contact tip overheating
    • Gun neck overheating

    Safety Notes

    • Disconnect machine power before feeder inspection.
    • Sharp wire ends can puncture gloves and skin.
    • Do not adjust drive rolls while feeding wire.
    • Overheated contact tips remain hot after welding stops.
    • Damaged liners can create erratic arc behavior.

    FAQ

    Why does aluminum wire birdnest more easily?
    Aluminum wire is softer and collapses more easily under feed pressure.

    Can a dirty liner cause birdnesting?
    Yes. Increased drag inside the liner is one of the most common causes.

    Should I increase drive roll tension to stop slipping?
    Excessive tension often worsens birdnesting by deforming the wire.

    Do spool guns help prevent birdnesting?
    Yes. Spool guns reduce wire push distance and improve aluminum feed reliability.

    Can incorrect contact tips cause feed issues?
    Yes. Undersized or damaged tips frequently create wire drag and burnback.

    Next Step

    Most MIG birdnesting problems can be solved by correcting liner condition, drive roll setup, wire path resistance, and consumable compatibility before replacing the entire gun assembly.

    Sources Checked

    • WeldingWeb symptom discussions
    • Reddit MIG wire feed troubleshooting discussions
    • Manufacturer MIG gun documentation
    • Drive roll compatibility references
    • Field troubleshooting reports
    • MIG feeder setup documentation
  • Flap Disc Edge Wear Troubleshooting

    Flap Disc Edge Wear Troubleshooting

    Flap disc edge wear usually happens when the grinder angle is too steep, pressure is excessive, the wrong disc type is being used, or the operator is grinding primarily on the disc edge instead of the face. Premature edge wear reduces abrasive life, creates uneven grinding performance, increases heat buildup, and can damage both the workpiece and grinder.

    Common Symptoms

    • Outer edge of the flap disc wears much faster than the center.
    • Grinding becomes uneven or difficult to control.
    • Disc cuts aggressively at first but loses performance quickly.
    • Visible flap tearing or uneven flap separation.
    • Increased vibration during grinding.
    • Excessive heat discoloration on the workpiece.

    Likely Causes

    • Grinding angle too steep: Excessive angle concentrates force on the outer edge of the disc.
    • Too much pressure: Heavy force overheats and overloads the abrasive flaps.
    • Incorrect flap disc style: Type 27 and Type 29 discs perform differently depending on grinding angle and application.
    • Wrong grit selection: Coarse grits used for finishing work can wear unevenly.
    • Improper grinder RPM: Overspeeding increases edge stress and heat generation.
    • Using the edge like a grinding wheel: Flap discs are designed primarily for face contact, not aggressive edge digging.

    Inspection Steps

    1. Inspect flap wear pattern across the full disc face.
    2. Verify grinder RPM matches the flap disc rating.
    3. Check grinding angle during operation.
    4. Inspect for excessive heat discoloration or flap glazing.
    5. Verify correct flap disc style and grit for the application.
    6. Inspect grinder spindle and backing flange condition.

    Visual Wear Indicators

    • Outer edge worn down faster than the center.
    • Missing or torn abrasive flaps.
    • Glazed abrasive surface from overheating.
    • Uneven flap height around the disc.
    • Discoloration from excessive grinding heat.

    Common Wrong-Part Mistakes

    • Using Type 27 discs where Type 29 geometry is more appropriate.
    • Running flap discs above rated RPM.
    • Using coarse grinding discs for fine finishing applications.
    • Using worn backing flanges that create disc instability.

    Field Fix vs Proper Fix

    Field fix: Reduce grinding pressure, flatten the grinder angle slightly, and rotate the disc contact area more evenly. Proper fix: Select the correct flap disc geometry, grit, RPM range, and grinder setup for the application while correcting operator technique issues.

    Ignored Failure Consequences

    Ignoring uneven edge wear reduces abrasive life, increases grinding cost, creates inconsistent surface finish quality, overheats the workpiece, and increases vibration-related grinder wear.

    Safety Notes

    Always follow abrasive RPM ratings and grinder compatibility requirements. Use face shields, gloves, hearing protection, and safety glasses when grinding. Never use damaged or delaminating flap discs.

    Sources Checked

    • Norton abrasive solutions catalog
    • Weiler abrasive catalog
    • Lincoln welding accessories catalog
  • Acetylene Regulator Freezing Troubleshooting

    Acetylene Regulator Freezing Troubleshooting

    An acetylene regulator that freezes or develops frost during use is usually caused by excessive gas withdrawal rates, rapid pressure drop, moisture contamination, restricted gas flow, or operating too close to the cylinder withdrawal limit. Freezing regulators can cause unstable flame behavior, reduced cutting performance, regulator damage, and unsafe fuel-gas delivery conditions.

    Common Symptoms

    • Frost or ice forming on the regulator body.
    • Flame weakens during long cuts or heating cycles.
    • Pressure fluctuates while cutting.
    • Torch pops or backfires intermittently.
    • Regulator output drops unexpectedly.
    • Fuel flow decreases as the regulator gets colder.

    Likely Causes

    • Excessive withdrawal rate: Pulling acetylene too quickly from the cylinder causes rapid cooling and regulator icing.
    • Moisture contamination: Water vapor inside the gas system can freeze during pressure drop.
    • Restricted hoses or flashback arrestors: Flow restrictions increase pressure differential and cooling effects.
    • Undersized cylinders: Small acetylene cylinders may not support heavy cutting or heating demand continuously.
    • Damaged regulator internals: Worn seats or diaphragms can create unstable flow behavior.
    • Cold ambient conditions: Low temperatures increase icing risk during high-demand operation.

    Inspection Steps

    1. Shut down the torch and allow the regulator to warm naturally.
    2. Inspect the regulator body for frost patterns or condensation.
    3. Check hose routing for kinks or restrictions.
    4. Inspect flashback arrestors and check valves for contamination.
    5. Verify cylinder size is adequate for the cutting or heating load.
    6. Check regulator outlet pressure stability during operation.
    7. Inspect for signs of oil, grease, or contamination in the gas system.

    Compatibility Notes

    • Acetylene withdrawal rate should remain within safe cylinder limits.
    • Large heating tips may require manifolded cylinders instead of single-cylinder setups.
    • Fuel-gas hose grade must match acetylene service requirements.
    • Flashback arrestors and check valves must match the torch system flow capacity.

    Common Wrong-Part Mistakes

    • Using undersized regulators for heavy heating applications.
    • Installing restrictive or contaminated flashback arrestors.
    • Using damaged hoses with internal collapse.
    • Attempting to thaw regulators with open flame or direct heat.

    Field Fix vs Proper Fix

    Field fix: Reduce gas demand temporarily, allow the regulator to warm naturally, and inspect for flow restrictions. Proper fix: Increase cylinder capacity, service contaminated components, replace damaged regulators, and ensure the complete fuel-gas system matches the required flow demand.

    Ignored Failure Consequences

    Ignoring regulator freezing can cause unstable torch operation, reduced cutting quality, flashback conditions, regulator damage, hose stress, and unsafe fuel-gas delivery during cutting or heating operations.

    Safety Notes

    Never heat frozen acetylene regulators with torches, heaters, or open flame. Keep oil and grease away from oxygen and fuel-gas equipment. Always bleed the system before servicing hoses, arrestors, or regulators.

    Sources Checked

    • Lincoln accessories and welding support catalogs
    • Uploaded welding safety references
    • Existing oxy-fuel troubleshooting content
  • Push-Pull Gun Motor Overheating Causes and Troubleshooting

    Push-Pull Gun Motor Overheating Causes and Troubleshooting

    A push-pull gun motor that overheats usually points to excessive wire-feed resistance, incorrect drive roll tension, liner drag, overloaded duty cycle, damaged armature components, or poor electrical connections. Most push-pull systems rely on synchronization between the feeder and gun motor. When resistance increases anywhere in the wire path, the gun motor compensates by drawing more current and generating excessive heat.

    Common Symptoms

    • Handle becomes hot during welding.
    • Wire feed slows down after several minutes.
    • Motor cuts in and out intermittently.
    • Burnback increases during long welds.
    • Drive rolls slip even with increased tension.
    • Motor protection or thermal shutdown activates.

    Likely Causes

    • Drive roll tension too tight: Excessive tension overloads the gun motor and flattens soft aluminum wire.
    • Contaminated or kinked liner: Aluminum debris, dirt, or crushed liners increase drag dramatically.
    • Worn contact tip: A partially fused or undersized tip increases feed resistance and current draw.
    • Oversized spool drag: Brake tension too high on spool systems forces the motor to work harder.
    • Duty cycle overload: Continuous welding beyond rated duty cycle overheats internal motor windings.
    • Poor cable routing: Tight bends in the gun cable increase wire friction and feeding resistance.

    Inspection Steps

    1. Remove the contact tip and verify free wire movement through the gun.
    2. Inspect the liner for aluminum shavings or crushed sections.
    3. Check spool brake tension. The spool should coast slightly without freewheeling.
    4. Inspect drive rolls for wear, wrong groove type, or contamination.
    5. Verify gun cable routing does not include tight loops or severe bends.
    6. Check cooling airflow around the power source and feeder.

    Common Wrong-Part Mistakes

    • Using steel drive rolls on soft aluminum wire.
    • Installing oversized contact tips that create unstable arc starts.
    • Running standard MIG liners instead of push-pull compatible liners.
    • Using incorrect U-groove or V-groove roll profiles.

    Field Fix vs Proper Fix

    Field fix: Reduce drive roll pressure, shorten cable bends, clean the liner, and lower spool drag. Proper fix: Replace worn liners, damaged tips, failing motors, or overloaded feeder components and verify the complete wire-feed setup matches the wire diameter and alloy being used.

    Ignored Failure Consequences

    Continuing to weld with an overheating push-pull motor can damage internal windings, weaken feeder synchronization, increase burnback frequency, and destroy expensive control boards or motor assemblies.

    Safety Notes

    Disconnect input power before servicing feeders, drive systems, or gun motors. Aluminum feeding systems contain rotating drive components that can pinch gloves or fingers during troubleshooting.

  • Spool Gun Trigger Delay Troubleshooting

    Spool Gun Trigger Delay Troubleshooting

    A spool gun trigger delay usually shows up as slow wire-feed startup, delayed arc initiation, intermittent trigger response, or a noticeable pause between pulling the trigger and wire movement. In most cases, the problem is caused by a failing trigger switch, damaged control wiring, dirty connections, relay problems, worn gun connections, or feeder communication issues between the spool gun and power source.

    Common Symptoms

    • Trigger pulled but wire feed starts late.
    • Gas flows before wire movement begins.
    • Arc starts inconsistently or sputters on startup.
    • Trigger response changes when cable is bent.
    • Intermittent dead trigger with occasional normal operation.
    • Wire feed hesitates during tack welds.

    Likely Causes

    • Worn trigger microswitch: Internal trigger contacts can become intermittent from repeated use.
    • Broken control wires: Repeated cable flexing near the handle or connector can fracture low-voltage control wiring.
    • Dirty gun connector pins: Oxidized or loose pins create inconsistent trigger signal transmission.
    • Failing feeder relay or contactor: Delayed relay engagement can cause noticeable startup lag.
    • Poor spool brake adjustment: Excessive spool drag can delay initial wire acceleration.
    • Drive roll slippage: Worn rolls or incorrect tension delay wire movement during startup.

    Inspection Steps

    1. Disconnect power and inspect the trigger wiring at the handle and connector.
    2. Check gun pins for looseness, corrosion, or overheating discoloration.
    3. Verify spool brake tension is not excessive.
    4. Inspect drive rolls for wear and confirm correct groove type for aluminum wire.
    5. Test trigger continuity while flexing the gun cable gently.
    6. Listen for delayed relay clicking inside the feeder or power source.

    Common Wrong-Part Mistakes

    • Installing oversized contact tips that slow startup and increase burnback.
    • Using standard steel drive rolls on aluminum wire.
    • Replacing the gun before testing trigger circuits and relay functions.
    • Using incorrect spool gun adapters or incompatible control harnesses.

    Field Fix vs Proper Fix

    Field fix: Clean connector pins, reduce spool drag, tighten drive roll settings correctly, and reposition damaged cable sections temporarily. Proper fix: Replace damaged trigger switches, broken control wires, worn relays, or failing feeder boards and verify gun compatibility with the machine.

    Related Failure Paths

    • Aluminum burnback
    • Erratic wire feed speed
    • Birdnesting near drive rolls
    • Contact tip overheating
    • Motor overload shutdown

    Safety Notes

    Disconnect input power before opening feeder cabinets or servicing trigger circuits. Spool guns contain moving feed components and electrically live trigger systems that can cause injury or accidental arc initiation during testing.

  • Grinding Wheel Wobble Causes and Troubleshooting

    Grinding Wheel Wobble Causes and Troubleshooting

    A grinding wheel that wobbles during operation is usually caused by damaged flanges, incorrect wheel mounting, bent spindles, worn bearings, improper wheel storage, or using the wrong wheel for the grinder. Even minor wheel runout can reduce grinding accuracy, overload bearings, increase vibration, and create a dangerous wheel failure risk at operating RPM.

    Common Symptoms

    • Visible side-to-side wheel movement during rotation.
    • Vibration through the grinder body or handle.
    • Uneven grinding marks or gouging.
    • Premature edge wear on flap discs or grinding wheels.
    • Difficulty maintaining straight cuts.
    • Excessive operator fatigue from vibration.

    Likely Causes

    • Improper wheel mounting: Dirt, burrs, or metal debris trapped behind the wheel prevent proper seating.
    • Damaged mounting flanges: Bent or worn flanges create uneven clamping pressure.
    • Bent spindle shaft: Impact damage from dropped grinders commonly bends spindle assemblies.
    • Worn grinder bearings: Bearing play allows oscillation under load.
    • Wheel damage: Cracked, warped, moisture-damaged, or expired wheels may not rotate true.
    • Incorrect wheel selection: Oversized or incompatible wheels create instability and imbalance.

    Inspection Steps

    1. Disconnect grinder power before inspection.
    2. Remove the wheel and clean both flange surfaces completely.
    3. Inspect the abrasive wheel for cracks, chips, or uneven wear.
    4. Check spindle runout manually while rotating the shaft slowly.
    5. Verify wheel RPM rating exceeds grinder RPM.
    6. Inspect arbor fitment and mounting hardware compatibility.

    Common Wrong-Part Mistakes

    • Installing wheels with incorrect arbor sizes.
    • Running cut-off wheels sideways as grinding wheels.
    • Using missing or incorrect flange washers.
    • Using moisture-damaged abrasive wheels from poor storage.

    Field Fix vs Proper Fix

    Field fix: Remove and remount the wheel correctly, clean flange surfaces, and replace visibly damaged abrasives. Proper fix: Replace bent spindles, worn bearings, damaged flanges, or incorrect wheel assemblies. Persistent wobble should never be ignored on high-speed grinders.

    Ignored Failure Consequences

    Operating with a wobbling grinding wheel increases the chance of wheel breakage, grinder damage, poor surface finish, operator fatigue, and severe injury from abrasive wheel fragmentation.

    Safety Notes

    Always follow abrasive RPM ratings and mounting instructions. Never use cracked wheels. Use face shields, gloves, hearing protection, and safety glasses when troubleshooting grinders and abrasive equipment.

    Sources Checked

    • Norton welding abrasive solutions catalog
    • Weiler abrasive and surface conditioning catalog
    • Lincoln Electric welding accessories catalog
  • More posts

    Read with Kindle Unlimited