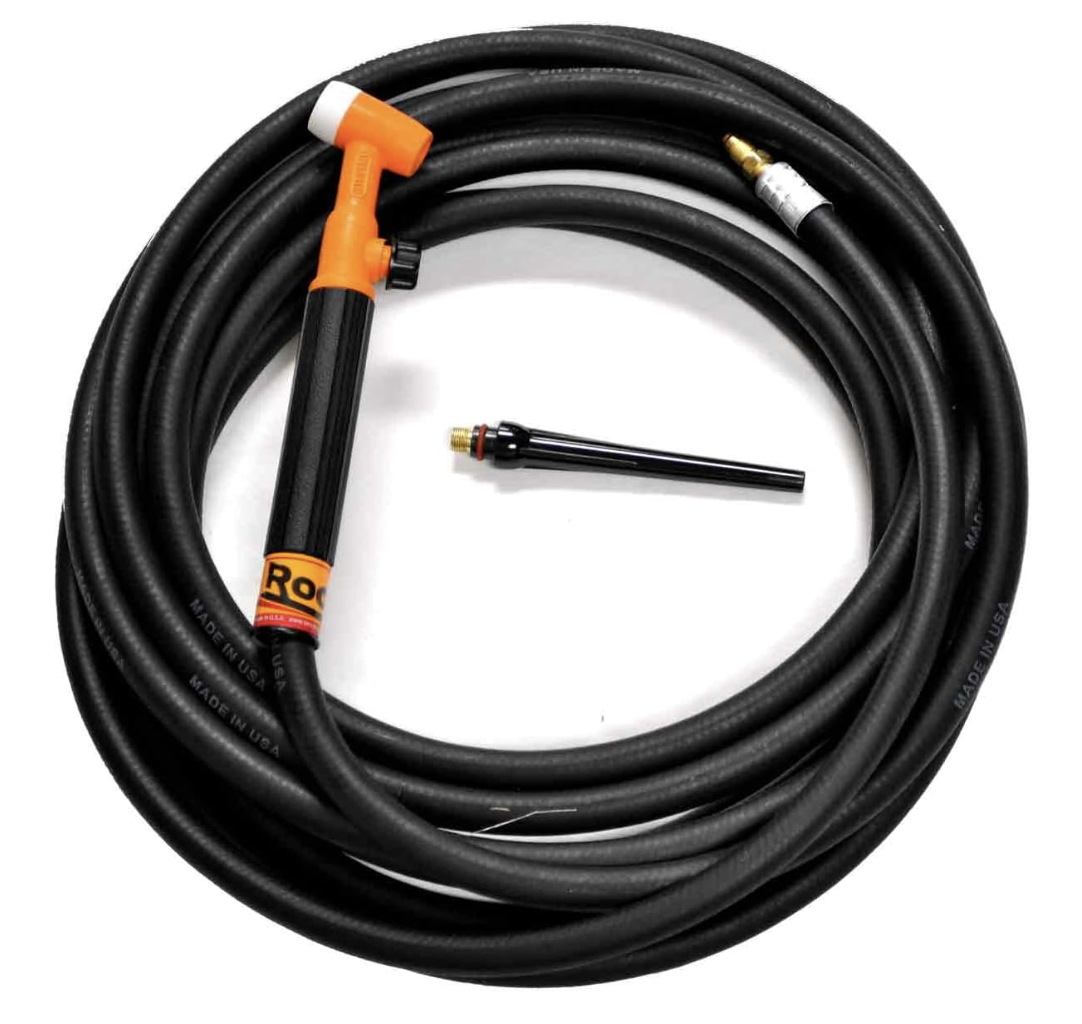
The Rocker R-17FV-25R is a 180-amp, air-cooled TIG torch kit built for fabricators who want a flexible head, built-in gas valve, and a durable 25-ft single-line rubber lead. Below is a breakdown of where it fits, who it’s for, and what to look at before buying.
Key Takeaways
180A air-cooled torch — fits most hobbyist and professional TIG setups running ≤180A.
Flex-head + valve gives control when welding off a power source with no remote gas solenoid.
25′ rubber single-line lead improves reach and reduces bulk compared to multi-line sets.
Works with common 17-series consumables.
Good upgrade for shops wanting a better-feeling head and better ergonomics than OEM torches.
Performance & Use Cases
The R-17FV-25R hits the sweet spot for stainless, carbon steel, and thinner aluminum work where you don’t need a water-cooled rig. At 180A DC/AC, it handles most shop TIG work without overheating if you manage duty cycle. The flex-head helps for out-of-position welding—frame work, brackets, bike parts, handrails, benches, etc.
The integrated gas valve is essential if you’re running a power source without a built-in solenoid (older transformer machines, small inverter units, portable repair rigs).
What You Get (Kit)
Rocker 17-series flex-head torch
25′ rubber single-line cable
Inline gas valve
Standard 17-series consumable compatibility
What’s NOT included
Tungsten
Cups/collets/collet bodies
Dinse connector type may vary by machine (verify before purchasing)
Selecting the Right Torch
Consider:
Machine output: Stay ≤180A for air-cooled longevity.
Duty cycle: Long AC aluminum runs may overheat air-cooled torches—upgrade to water-cooled if needed.
Lead length: 25′ is ideal for shops needing reach across a table or fixture without constant repositioning.
Valved vs. non-valved: Choose valved if your machine doesn’t control gas electronically.
Affiliate disclosure: As an Amazon Associate, I earn from qualifying purchases.
Safety Notes
Follow AWS A5.12 tungsten recommendations for type and diameter.
Keep torch leads away from sharp edges and hot plate.
Air-cooled torches heat rapidly—allow cooldown to avoid damage.
Ensure proper PPE under ANSI Z87.1 for eye protection and ANSI Z49.1 welding safety guidelines.
FAQ
Is this torch compatible with my machine? If your machine accepts 17-series torches and matches the connector type (Dinse 25 or 35), it should fit. Always confirm connector style.
Does this include consumables? No. Plan to add 17-series cups, collets, and tungsten.
Can this run aluminum? Yes—up to the torch’s duty cycle limits. For heavy AC aluminum at high amps, water-cooled is better.
Can I use a foot pedal with this torch? Yes. The inline valve is only for gas control—not amperage.
ERTi-2 TIG / GTAW filler metal is used as a starting point for commercially pure titanium welding where the procedure, base metal grade, and service conditions support that choice. It is not a substitute for WPS review or manufacturer data. Before you load a rod, confirm what the base material actually is, what the code allows, and whether the service environment calls for a different titanium filler.
This draft is focused on selection and compatibility checks. The practical issue is not just whether the rod is labeled ERTi-2, but whether it matches the job after you verify the base metal, joint condition, shielding plan, and cleanliness standard.
Key Takeaways
Use ERTi-2 only after confirming the base metal grade and WPS.
Commercially pure titanium applications need tight control of contamination, shielding, and heat input.
Do not assume a filler grade is acceptable for every CP titanium repair or fabrication job.
Manufacturer data sheet review is still required before order release or weld start.
If a detail is not confirmed, mark it as Unknown (Verify) and stop until it is checked.
What the ERTi-2 designation means for the shop
The provided filler metal record identifies this item as ERTi-2 for TIG / GTAW use, with an AWS A5.16 reference and a base material description of commercially pure titanium Grade 2. That gives you a useful starting point, but not final approval for any job.
For titanium work, the filler selection normally depends on the exact base metal, the joint design, the service environment, and the governing procedure. If any of those inputs are missing, treat compatibility as Unknown (Verify) until the WPS, code requirements, or manufacturer literature confirms the match.
Selection checks before you order rod
Use the following checks before releasing ERTi-2 to the floor:
Check the base metal identification. Verify the heat number, mill cert, or purchase record. If the base metal is only described as CP titanium, stop and confirm the grade. If the grade is not established, compatibility remains Unknown (Verify).
Inspect the WPS. Confirm the procedure calls for ERTi-2 or equivalent filler for the exact joint and service condition.
Verify code or customer requirements. Some jobs control filler selection by specification, qualification record, or purchaser note. Do not rely on generic material family matching.
Inspect the joint condition. Titanium requires clean, oxide-free, contamination-free surfaces. Oil, marker residue, abrasive dust, and moisture can become weld defects.
Verify shielding strategy. Confirm primary shielding, trailing coverage if required, purge requirements if applicable, and gas quality before welding starts.
Troubleshooting and support checks
If the job is already in motion and the welds are not meeting expectations, work through the issue in a controlled order.
1) If the arc starts poorly or the bead looks unstable
Inspect the tungsten condition, cup setup, and gas delivery.
Check for drafts, loose hoses, or inadequate coverage.
Verify that the filler rod is dry, clean, and not contaminated by shop handling.
2) If the weld surface discolors excessively
Inspect the shield coverage at the weld pool and trailing edge.
Check travel speed and heat input against the WPS.
Verify that the purge and torch shielding remain in place until the joint cools enough for the procedure requirements.
3) If the filler does not appear to match the job requirement
Inspect the material traceability documents.
Check whether the base metal is truly Grade 2 CP titanium or another titanium grade.
Verify with the manufacturer data sheet and the approved procedure before continuing.
WSP lookup and filler metal finder
Use the filler metal record as a starting point for selection review:
Use the finder page when you need to cross-check the filler family against other listed options and confirm whether the job should stay with ERTi-2 or move to another approved material:
These pages support selection. They do not replace the WPS, code review, or manufacturer data sheet.
Practical shop handling points
Titanium filler handling is a contamination control task. Keep the rod package closed until needed. Store rods so they are not exposed to dirt, moisture, grinding debris, or mixed-metal contact. If a rod has dropped to an unclean floor or has visible contamination, treat it as Unknown (Verify) until it is cleaned or replaced according to shop practice and procedure requirements.
During setup, confirm the following before striking an arc:
Base metal identity is confirmed.
Filler designation is confirmed.
Gas supply is verified and suitable for the procedure.
Joint surfaces are clean and ready.
Operator knows the cooling and shielding requirements.
Safety notes
Titanium welding is sensitive to contamination and shielding failure. Do not improvise filler choice on critical work. Do not assume CP titanium grades are interchangeable. Do not weld over questionable surface contamination. If the procedure, service condition, or material grade is unclear, stop and verify before welding.
Use standard welding PPE, keep the work area clean, and maintain gas safety and cylinder handling practices. If a weld shows unusual discoloration, cracking, or surface contamination, quarantine the part for review rather than passing it to inspection without a documented decision.
FAQ
Is ERTi-2 always correct for commercially pure titanium?
No. It is a starting point for CP titanium applications, but final selection depends on the WPS, the exact base metal grade, and service requirements. If any of those are unconfirmed, the compatibility is Unknown (Verify).
Can I use ERTi-2 if the base metal is only labeled titanium?
Not without more information. You need the actual grade, traceability, or approved procedure. “Titanium” alone is not enough to confirm filler compatibility.
Do I need to check the manufacturer data sheet if the listing already says ERTi-2?
Yes. The listing is a reference point, not final approval. Verify the data sheet, the WPS, and any customer or code requirements before welding or purchasing.
What should I do if the weld color looks off?
Stop and inspect shielding, purge, cleanliness, and heat input. Discoloration on titanium often points to coverage or contamination issues. Verify the procedure before continuing.
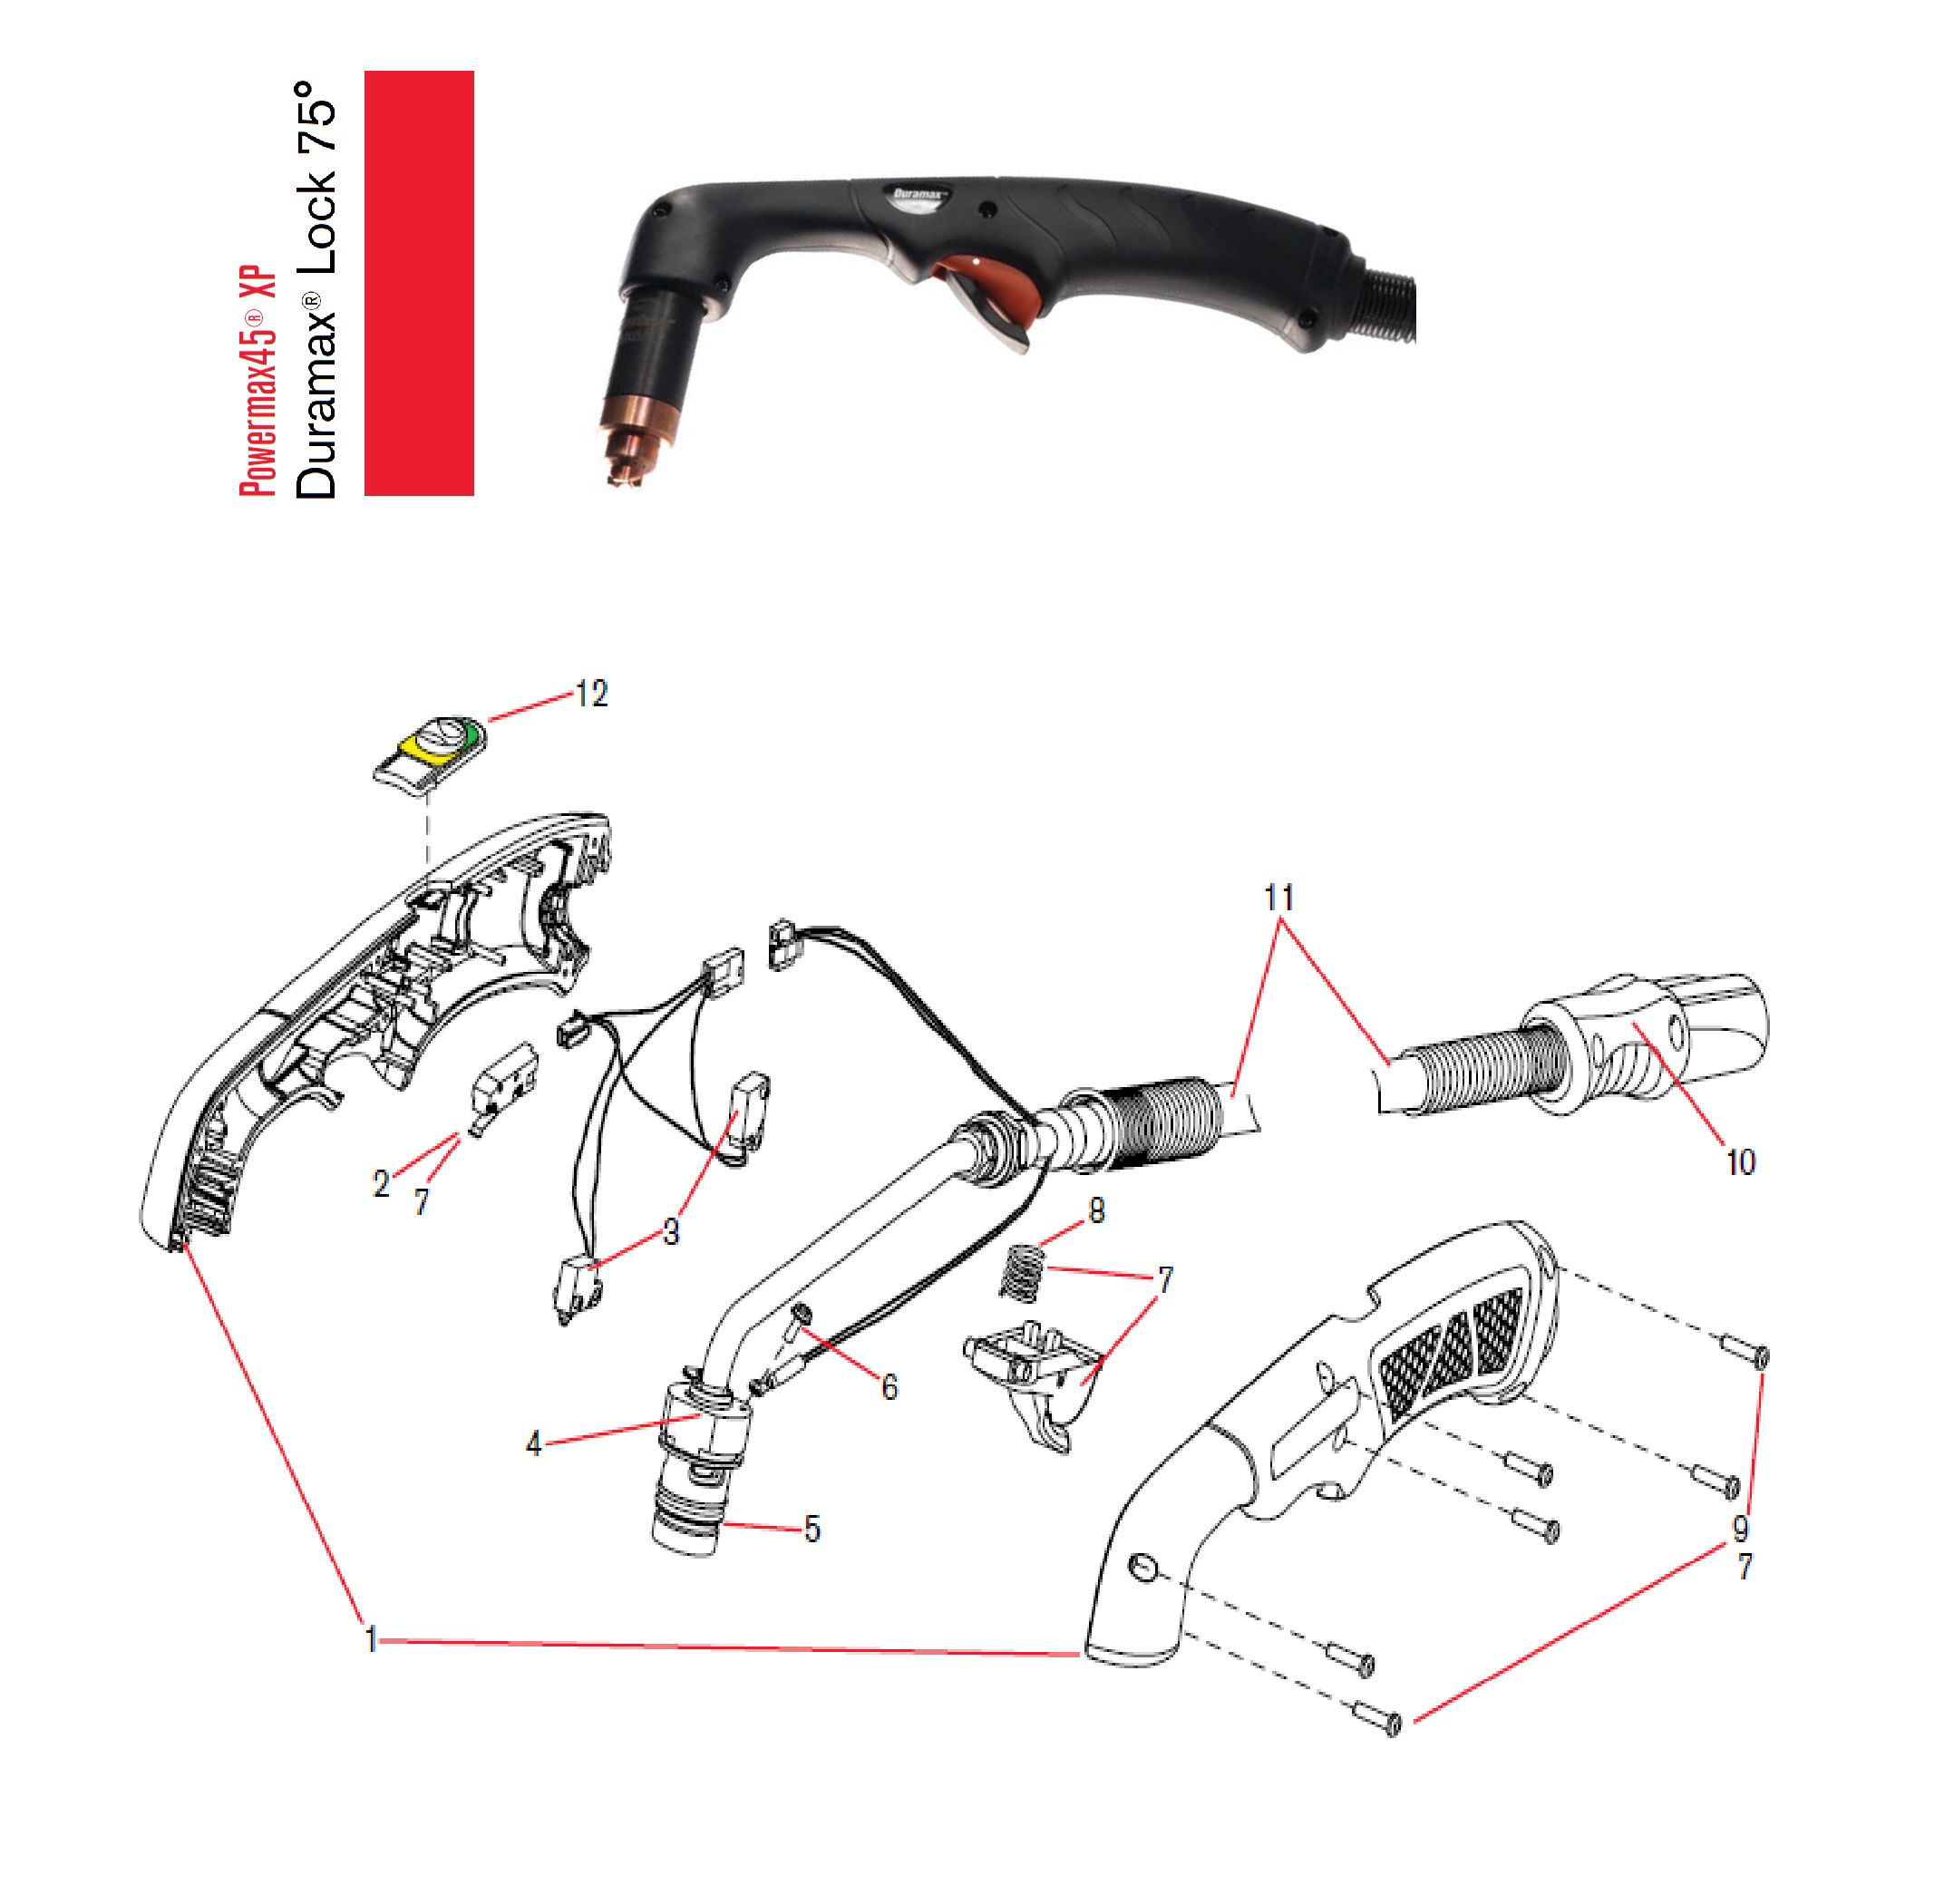
If a Hypertherm Duramax Lock 75 degree hand torch is cutting poorly, the first problem is often not the power source. In many cases the issue is in the torch head, consumables, lead connection, or shield/nozzle stack. This guide gives a practical parts breakdown and a buying check process for maintenance teams and support staff who need to verify what to inspect before ordering replacements.
Key Takeaways
Start with the torch side: consumables, retaining hardware, and visible damage around the head.
Confirm the torch family and cut mode before ordering anything.
Use the WSP lookup page as the source-backed starting point for part identification.
Do not assume a consumable is correct because it looks similar; verify against the torch and machine context.
If fit is uncertain, mark it Unknown (Verify) and keep the review with the manufacturer or approved supplier.
Parts breakdown: what to inspect first
For a 75 degree hand torch setup, begin at the working end and move back toward the lead. The exact internal stack can vary by torch family and machine context, so treat this as a check sequence, not a universal assembly map.
Shield or drag shield: Inspect for heat damage, heavy spatter, distortion, and worn edges.
Nozzle: Check for orifice wear, pitting, ovality, and side damage.
Electrode: Look for deep wear, abnormal erosion, and arc instability symptoms.
Swirl ring / gas distribution part: Verify that it is present, seated correctly, and free of cracks or burn marks.
Retaining cap or retaining hardware: Confirm threads, seating faces, and torque condition are not damaged.
Torch head and locking interface: Inspect for looseness, cracked plastic, damaged seals, or signs of overheating.
Lead and strain relief: Check for cuts, kinks, softened insulation, or intermittent operation near the handle.
Troubleshooting sequence: check, inspect, verify
1) Check the symptom pattern
Before replacing parts, identify the failure mode. A no-start condition, weak pilot arc, arc dropout, poor cut quality, or excessive dross can point to different causes. Do not jump to a torch-head replacement until the symptom is matched to the wear pattern.
2) Inspect consumables as a set
Remove the front-end parts and inspect them together. A single damaged nozzle may be the visible fault, but a worn electrode or damaged swirl ring can be the root cause. Check for:
Mismatch in wear between electrode and nozzle.
Evidence of overheating, such as discoloration or warped edges.
Carbon tracking, spatter buildup, or contamination in the torch head.
Loose fit or poor seating that could interrupt gas flow.
Verify that the parts being removed match the torch family in service. If the part numbers are not clearly readable, Unknown (Verify) applies until the WSP lookup or approved documentation confirms the match.
3) Inspect the torch head and lock interface
The 75 degree hand torch head can see mechanical stress from repeated handling, workpiece contact, and lead movement. Check the lock area for wear that may prevent the consumables from seating correctly. If the retaining cap does not tighten smoothly, do not force it. Cross-threading, damaged threads, or a heat-warped seat can create intermittent arc faults.
4) Verify gas and electrical continuity indirectly
Without assuming hidden specs, verify the practical conditions that support a stable arc: the front-end parts are clean, seated, and undamaged; the lead is not pinched; and the machine displays no unrelated fault that points away from the torch. If the torch behavior changes when the lead is moved, treat the lead and strain relief as suspect.
WSP lookup: use it before buying
The WSP lookup page for this torch family is the best source-backed starting point for parts identification and buying checks:
Use that page to confirm the torch family, part naming, and catalog-backed item numbers where shown. Do not treat a visual match alone as enough proof. If a component is listed in the lookup but your torch head shows a different geometry, mark the fit as Unknown (Verify) and confirm with the supplier or manufacturer before ordering.
Buying checks for maintenance teams
When purchasing torch parts, use these checks in order:
Match the torch family: Confirm the torch is the Hypertherm Duramax Lock 75 degree hand torch variant referenced by the lookup page.
Match the machine context: Use the actual machine and torch pairing in service, not a similar setup from another bay.
Match the wear pattern: Replace the damaged front-end part plus any companion part that shows related wear.
Check the lock and seating surfaces: If the interface is damaged, parts alone may not fix the fault.
Verify the buy link path: Use only approved links from the source page or internal support references.
De-energize the system before removing or handling consumables.
Allow hot parts to cool before inspection.
Do not file, force, or modify front-end parts to make them fit.
If a torch head is cracked, burned, or electrically unstable, remove it from service until reviewed.
Use manufacturer review for any fit or safety-critical uncertainty.
FAQ
Why does a new consumable set still cut poorly?
A new set can still perform badly if the torch head is damaged, the retaining hardware does not seat correctly, the lead is compromised, or the wrong consumable family was installed. Inspect the whole front end, not just the nozzle.
What should I replace first when the torch shows arc dropout?
Start with the consumables and the torch-side seating surfaces. If those are clean and the problem continues, inspect the lead, strain relief, and the machine-side fault indications. Do not assume the power source is the root cause.
How do I confirm I am buying the right part?
Use the WSP lookup page, confirm the torch family and item naming, and compare the existing installed parts to the lookup record. If anything does not align, mark it Unknown (Verify) and confirm before purchase.
Can I use a similar-looking shield or nozzle from another torch?
No. Similar appearance is not enough. Verify the exact torch family, geometry, and use case before ordering or installing any replacement part.
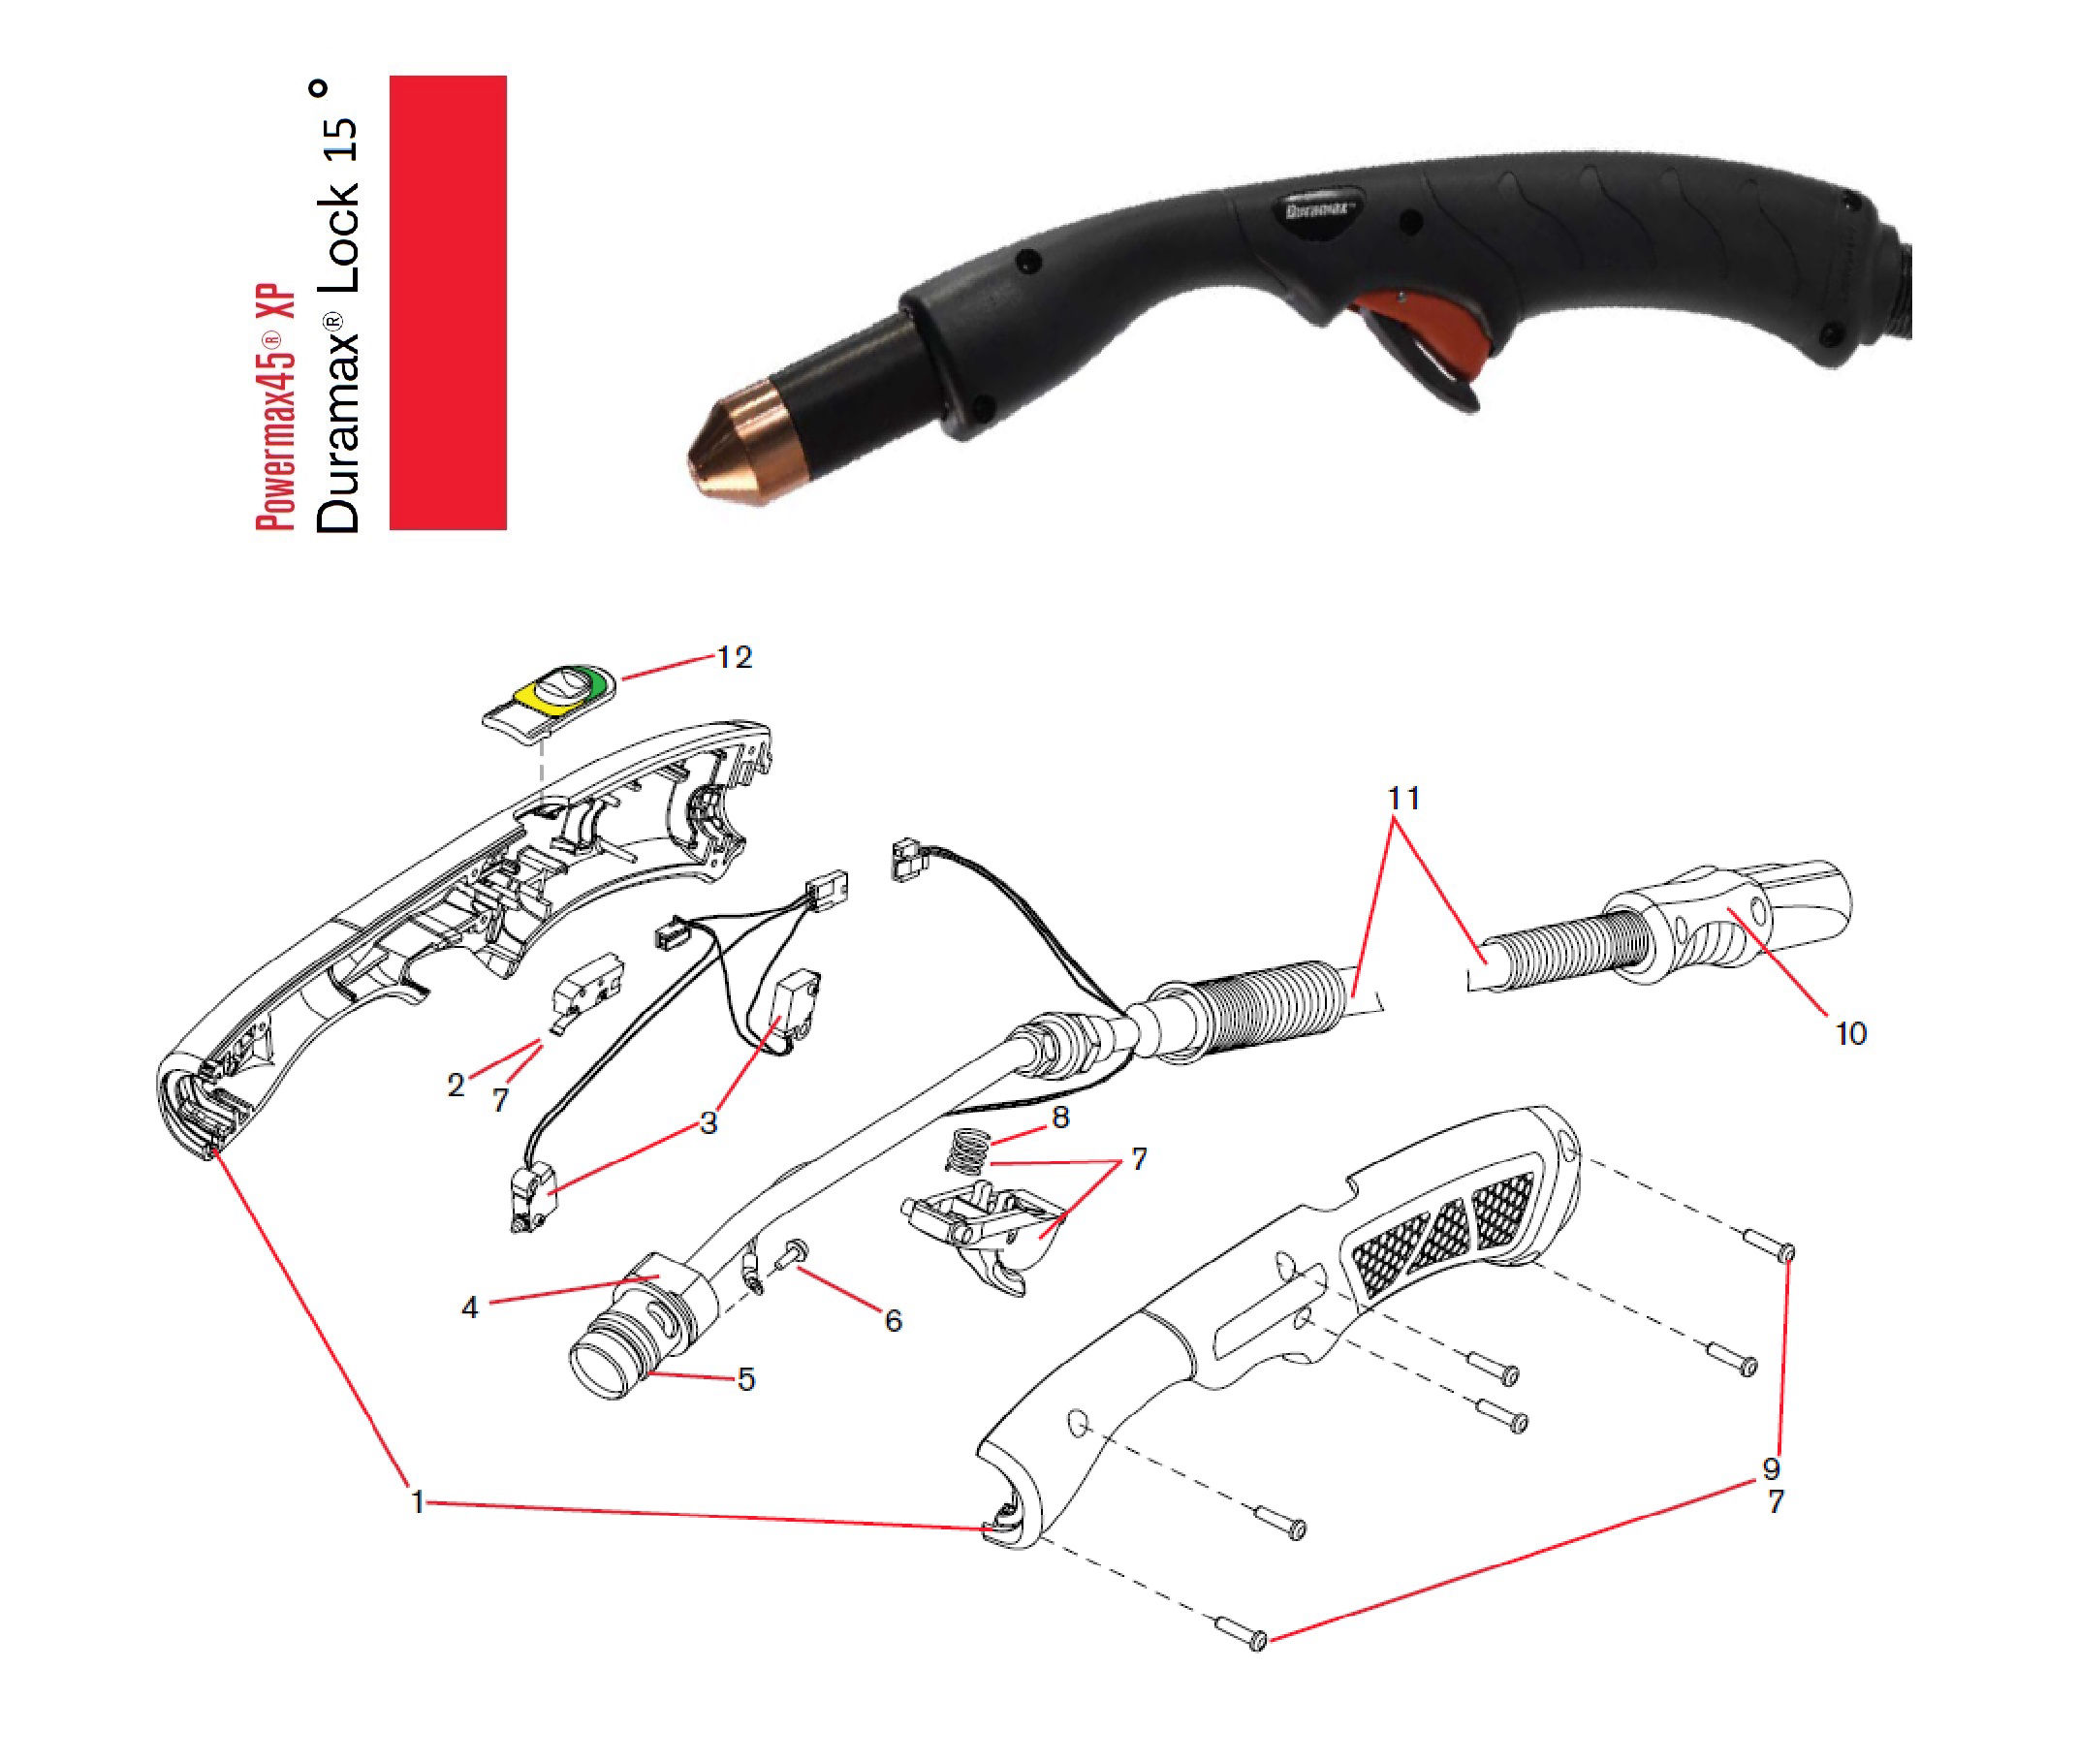
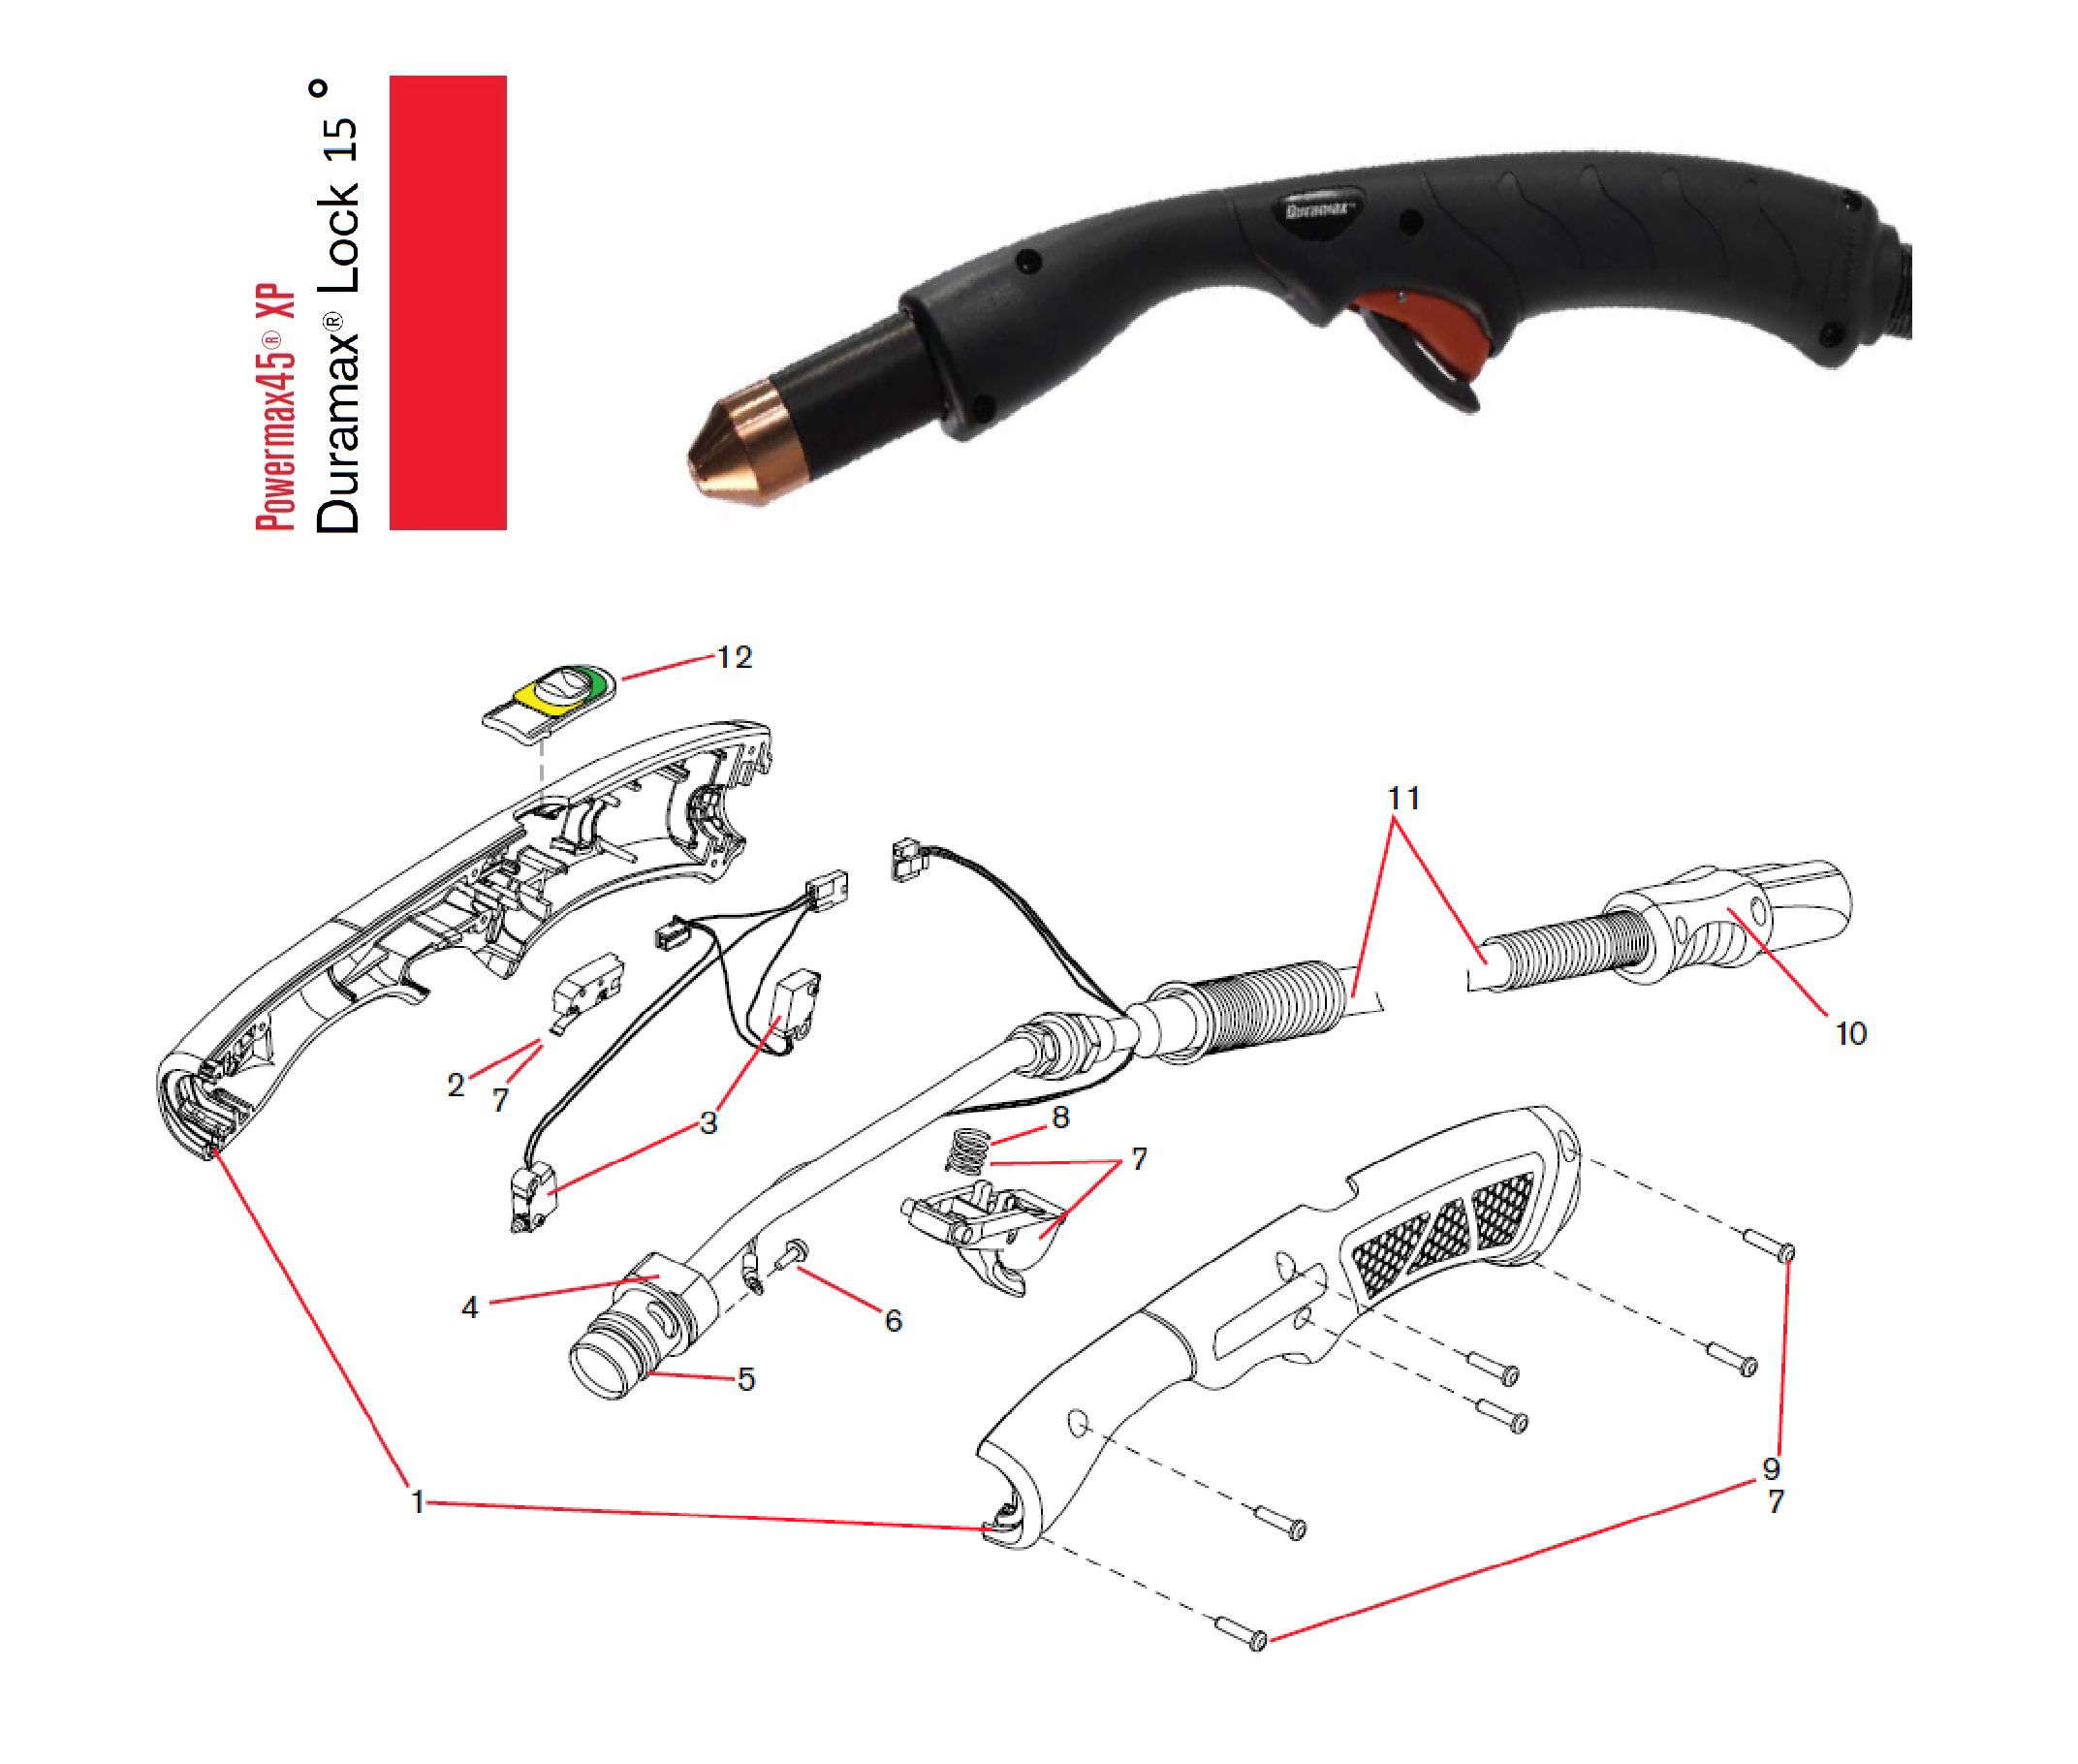
If you are maintaining a Hypertherm Duramax Lock 15 Degree hand torch, the main job is not guessing part numbers. It is identifying the wear path, matching the torch to the machine context, and confirming the replacement against the catalog before anything is ordered. This is a consumable replacement problem first, and a parts-compatibility problem second.
Key Takeaways
Use the torch’s breakdown page as the starting point, not the final approval step.
Confirm the torch style, angle, and lock style before comparing parts.
Inspect the nozzle, electrode, shield, swirl ring, and retaining hardware for heat damage, arc misalignment, and physical wear.
If fitment is uncertain, stop and verify against the WSP lookup page before ordering.
Do not assume a part from another Duramax family torch will fit. Verify each item by catalog reference.
What This Torch Parts Breakdown Is For
The Hypertherm Duramax Lock 15 Degree hand torch parts breakdown is useful when you need to replace worn consumables or identify a damaged torch component after poor cut quality, arc instability, or visible heat distortion. In practice, the breakdown helps you separate routine wear items from parts that may indicate a deeper torch issue.
For this torch, the critical point is to match the exact torch configuration shown on the source page: Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown. That page is the verified lookup source for the torch context provided here.
How to Work the Replacement Decision
Start with a visual inspection. Then move to part-by-part verification. Do not replace parts only because cut quality changed; verify the torch condition and the machine setup first.
Check
Check the torch head for heat discoloration, cracks, or arc tracking marks.
Check the consumable stack for uneven wear, melted edges, or carbon buildup.
Check the lead and handle area for cuts, crushed sections, or loose strain relief.
Check the retaining hardware for cross-threading, distortion, or seizure.
Inspect
Inspect the electrode tip for deep crater wear or a collapsed center. If the wear pattern is abnormal, replace and verify arc transfer behavior.
Inspect the nozzle orifice for ovality, spatter blockage, or visible deformation.
Inspect the shield for heat damage, edge warping, or fit issues at the torch front end.
Inspect any swirl ring or internal alignment part for cracks, burns, or contamination.
Verify
Verify the torch model and angle match the catalog listing before selecting a replacement.
Verify the part number from the lookup page or linked breakdown page, not from memory.
Verify the machine context if the torch is being used on a specific plasma system. If the machine is not clearly identified, treat compatibility as Unknown (Verify).
Verify that the replacement set matches the wear pattern you found. If only one part is damaged, do not automatically replace the full stack unless the inspection supports it.
Common Failure Signs That Point to Consumable Replacement
Most maintenance calls on plasma torches start with cut quality. That is useful, but not enough. Use the symptoms to guide inspection, then confirm with the part breakdown.
Rough edge or heavy dross: often points to nozzle wear, incorrect standoff, or an electrode nearing end of life.
Weak start or intermittent arc: may involve the torch front end, pilot arc behavior, or worn internal components. See the related troubleshooting guide for more on arc loss and no-start conditions: Pilot Arc Failure Troubleshooting.
Excessive spatter in the front end: check the nozzle and shield for contamination and fit.
Unexpected heat at the torch head: inspect for poor consumable seating or a damaged component stack.
If the torch is producing unstable arc behavior across more than one set of consumables, do not assume the consumables are the only issue. Confirm machine settings, air quality, and lead condition. If the cause is unclear, mark the condition as Unknown (Verify) and cross-check with the machine manual and torch breakdown.
WSP Lookup Section
Use the verified WSP source page below to review the torch breakdown and item context before ordering:
This lookup page should be treated as the catalog-backed starting point for identifying the correct parts. If a replacement item is not clearly confirmed on the page, do not guess. Record it as Unknown (Verify) and confirm before purchase.
Replacement Workflow for Maintenance Teams
Identify the torch style and front-end layout.
Remove the torch consumables and document the wear pattern.
Compare the damaged parts against the breakdown page.
Check whether wear is isolated to the consumables or extends into the torch head and lead.
Verify the replacement part number against the WSP lookup page.
Only then release the order.
Safety Notes
Power down and isolate the plasma system before handling the torch head.
Allow the torch and consumables to cool before inspection.
Use eye protection when removing hot or stuck consumables.
Do not force threaded parts. If a component binds, inspect for damage instead of tightening harder.
Use compressed air and cleaning methods that do not introduce debris into the torch front end.
FAQ
How do I know if I need a full torch consumable set or only one part?
Inspect the wear pattern first. If only the nozzle shows normal end-of-life wear and the electrode is still within acceptable condition, a partial replacement may be enough. If multiple parts show heat damage or arc instability, verify whether the full stack should be replaced.
Can I use another Duramax torch part if it looks similar?
No. Similar appearance does not confirm compatibility. Use the exact breakdown page and verify each item number before ordering. If the match is not clear, treat it as Unknown (Verify).
What should I check before blaming the consumables for poor cut quality?
Check air quality, torch seating, work lead condition, standoff, and machine settings. Consumables are a common cause, but not the only one. If the issue persists after replacement, inspect the torch and power source path.
Where do I confirm the correct parts?
Use the verified lookup page linked above. That is the reference source for this torch breakdown.
ERCuNi TIG / GTAW filler metal is used on copper-nickel work where the joint design, service environment, and procedure call for a copper-nickel filler rather than a general-purpose bronze or nickel alloy. For maintenance buyers and welders, the main risk is assuming the rod name alone is enough. It is not. Selection has to follow the WPS, the base metal grade, the service conditions, and the manufacturer data sheet.
Use this page as a starting point for compatibility checks only. Before ordering or welding, verify the exact joint requirements and confirm the filler against the procedure and governing code. If any of those inputs are unclear, stop and resolve them first.
Key Takeaways
ERCuNi is a filler selection starting point, not automatic approval for every copper-nickel job.
Confirm the base metal grade before matching filler to the joint.
Check the WPS, service environment, and corrosion requirements before release to weld.
Do not assume a rod labeled for copper-nickel will fit every 70/30 or 90/10 application without review.
When technical details are uncertain, use Unknown (Verify) rather than guessing.
What ERCuNi is used for in practice
The allowed filler metal page identifies ERCuNi as a TIG / GTAW filler for copper-nickel alloys and related applications. That makes it relevant where the work involves copper-nickel piping, tube, or fabrications that call for this classification. The page also points to common diameter references and brand names, but those details still need to be checked against the actual job package and supplier data sheet.
For shop use, treat the filler metal page as a quick reference, not a procedure substitute. It helps narrow the field, but it does not confirm the WPS, the exact alloy compatibility, or whether the weld is intended for corrosion service, seawater service, or another duty. Those are job-specific decisions.
Check the job before you select the rod
Start with the base metal. Identify the copper-nickel grade from the drawing, MTR, or vessel/piping documentation. If the alloy is not clearly defined, mark it as Unknown (Verify). Do not rely on appearance alone. Copper-nickel alloys can be misidentified in maintenance work, especially after service exposure, coating, or repair prep.
Next, check the WPS. Verify that the procedure actually permits ERCuNi for the joint. Confirm any limits on base material, thickness, welding position, backing, heat input, and shielding gas. If the WPS references a specific classification or alternate filler family, follow that document. The filler rod choice must match the procedure, not the other way around.
Then verify service conditions. Copper-nickel joints can be sensitive to the intended environment, especially where corrosion resistance is a key requirement. If the weld will see marine exposure, process fluid contact, or elevated temperature service, make sure the filler selection is still acceptable for that duty. If the service requirement is not clearly documented, treat it as Unknown (Verify).
Troubleshooting and support checks
If the filler metal seems right but the job still does not line up, use this sequence:
Check the base metal identification. Confirm the alloy grade from paperwork or positive identification. If you cannot verify it, stop and escalate.
Inspect the WPS. Verify the exact filler classification, process, and essential variables. Make sure the procedure has not been superseded.
Verify the service requirement. Confirm whether the weld is for general fabrication, corrosion service, or another controlled application.
Inspect the rod condition. Look for contamination, moisture, damaged packaging, or mix-up with another alloy.
Verify the shielding setup. GTAW shielding gas, cup selection, tungsten prep, and arc stability all affect the weld outcome. If the gas setup is uncertain, use Unknown (Verify) until confirmed.
If weld quality problems show up after setup, do not assume the rod is the root cause. Check for contamination, poor joint cleaning, incorrect fit-up, and wrong procedure settings first. For general TIG support on arc stability and tungsten condition, see the related guide on TIG tungsten contamination troubleshooting. For gas shielding and stickout control on cup selection, see the Square Wave 205 TIG cup size selection guide.
Use the filler metal page as a starting point
The ERCuNi filler metal page at https://www.weldsupportparts.com/filler-metal-tig-ercuni.html is the right place to begin a selection review. It identifies the process as TIG / GTAW, the classification as ERCuNi, the AWS specification as AWS A5.7, and the intended base material family as copper-nickel alloys. It also lists common search terms that may help narrow down a stock match.
Use the filler metal finder when you need to compare options across filler families or confirm the route to a better match. That page is also a starting point only. It does not replace the WPS, the code requirement, or the manufacturer data sheet.
If the filler name on the job ticket does not match the procedure, do not substitute based on naming similarity. ERCuNi, ERNiCu-7, and other copper-based filler families are not interchangeable without verification. If the selection is unclear, tag it Unknown (Verify) and route it through the welding engineer or responsible supervisor.
Practical shop checks before release
Check the base metal grade against the drawing or MTR.
Inspect the WPS for permitted filler classification and process.
Verify the service environment and corrosion requirement.
Confirm rod size from the job package or manufacturer data sheet.
Inspect packaging for damage, contamination, or shelf exposure.
Confirm shielding gas, cup, tungsten, and joint prep before arc start.
Safety notes
Do not weld from assumptions. Copper-nickel work can carry process and service requirements that are not visible at the joint. Follow the site hot-work controls, ventilation requirements, and PPE rules. Keep filler metals clean and dry. If the alloy, service condition, or procedure requirement is uncertain, stop and verify before use.
Grinding, cleaning, and surface prep can also expose residue or contamination from prior service. Treat unknown residues as a hazard until identified. If the joint has been in corrosive or marine service, verify cleaning and handling requirements before fit-up.
FAQ
Is ERCuNi always correct for 70/30 copper-nickel?
No. ERCuNi may be a common starting point, but the correct choice depends on the WPS, the base metal grade, and the service condition. Verify the procedure before welding.
Can I use the filler metal page as approval to weld?
No. The filler metal page is a selection starting point only. It does not replace the WPS, code requirements, or manufacturer data sheet.
What if the base metal is not clearly identified?
Mark it Unknown (Verify). Do not guess the alloy. Confirm the material from documentation or approved identification methods before selecting the filler.
Are ERCuNi and ERNiCu-7 interchangeable?
Not by default. They are different filler families and should only be used when the WPS and supporting technical documents allow it. Verify compatibility before release.
Metadata note: if the exact rod size, brand approval, or compatibility detail is not confirmed in the job packet or manufacturer data sheet, use Unknown (Verify).
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
A TIG gas lens collet body is a small part, but it controls two things that matter: tungsten retention and shielding gas flow. When the collet body is the wrong size, worn, or clogged, the torch can still arc, but the setup becomes harder to control. For buyers and maintenance teams, the main job is not to guess. It is to verify torch series, tungsten size, and the condition of the existing consumables before ordering.
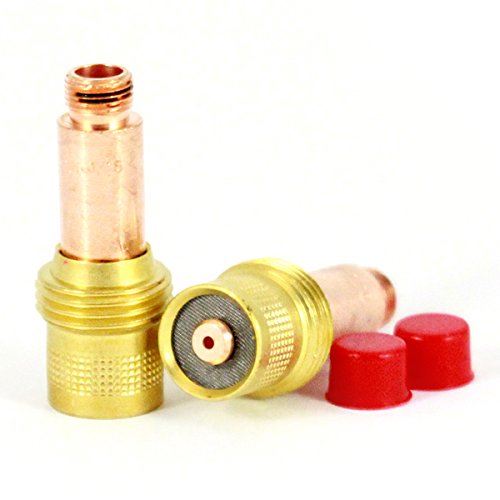
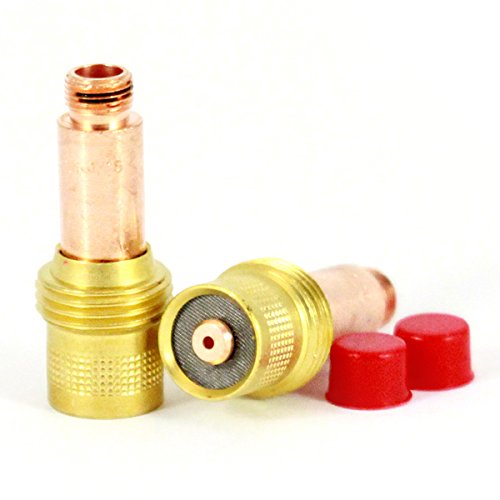
The TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32″) is listed as a standard size gas lens collet body for TIG torch #17, #18, and #26. The critical buying point is the 3/32 in. tungsten size in the part title. If your torch, cup, collet, or back-end hardware does not match that setup, stop and verify before purchase.
Key Takeaways
Confirm torch series first: #17, #18, or #26.
Confirm tungsten diameter: 3/32 in. on this part title.
Inspect the current collet body for burn marks, thread damage, gas passage blockage, and slip-related wear.
Do not assume all gas lens parts interchange across every TIG torch variant.
Use the torch manual and existing consumable stack as the final check, not memory.
What This Part Does
A gas lens collet body holds the collet and tungsten in the torch head and supports shielding gas distribution through the lens assembly. In normal service, the part should clamp the tungsten securely, support consistent gas coverage, and let the operator maintain a stable arc without tungsten movement. If the collet body is worn, the tungsten may slip, gas coverage may become uneven, or the torch may feel inconsistent from one setup to the next.
Before ordering, check the torch and the current hardware in the hand. Do not rely only on the torch body label if the torch has been rebuilt or mixed with aftermarket consumables.
Check
Check the torch series marking or manual: #17, #18, or #26.
Check the tungsten size currently used: 3/32 in. or Unknown (Verify).
Check whether the torch is built around a gas lens stack or a standard collet setup.
Check the cup, collet, and back cap for matching wear patterns or mixed parts.
Inspect
Inspect the existing collet body threads for galling, rounding, or heat distortion.
Inspect the gas lens screen or passage for clogging, soot, or spatter contamination.
Inspect the tungsten seating surface for slip marks or deformation.
Inspect the cup fit. If the cup feels loose or bottoms oddly, the stack may be mismatched.
Verify
Verify the replacement part title matches the torch series and tungsten size you actually use.
Verify the collet body style matches the rest of the consumable stack already on the torch.
Verify gas flow path cleanliness before blaming the torch body for poor shielding.
Verify the machine settings and gas delivery are correct before replacing parts unnecessarily.
Buying Checks for Maintenance Teams
For stocked consumables, the safest approach is to compare the failed part with the replacement before issuing it to production. A part can look close and still be wrong in the details that matter. If the torch is a repair item coming in from the floor, tag it with the torch series, tungsten size, and any cup or back-cap part numbers that were on the assembly.
When reviewing an order, confirm the following:
Torch family: #17, #18, or #26.
Tungsten size: 3/32 in. for this listed part.
Gas lens requirement: Only buy gas lens hardware when the torch setup is designed for it.
Current consumable stack: Unknown (Verify) if the torch has mixed components or no part markings.
If your team keeps alternative consumable families on hand, label bins clearly. Do not mix standard collet bodies and gas lens collet bodies in the same tray unless they are separated by torch series and tungsten size.
Shut down the welding power source before disassembly.
Let the torch cool before handling burned or discolored consumables.
Do not force a tungsten or collet into a damaged body.
Replace contaminated parts if they cannot be cleaned back to a reliable condition.
Use eye protection when disassembling hot or spattered torch components.
FAQ
Is this collet body only for #17, #18, and #26 torches?
The part title lists #17, #18, and #26 torch compatibility. If your torch is a different series, verify the manual or the existing consumables before ordering. Unknown (Verify) for any other torch family.
Does the 45V26-3/32″ title mean it is for 3/32 in. tungsten?
Yes, the part title indicates 3/32 in. tungsten size. Still verify the complete consumable stack on your torch, especially if the machine has been rebuilt or mixed with non-original parts.
How do I know if my old collet body is worn out?
Look for tungsten slip, rough threads, heat damage, clogged gas passages, or inconsistent shielding behavior. If the torch runs better after replacing the collet body, the old part was likely the problem. For a deeper wear checklist, use the consumable wear signs article linked above.
Can I use this part if my gas lens setup is not confirmed?
Do not assume. Confirm whether your torch is built for a gas lens assembly. If that is unclear, inspect the current hardware and verify the part stack before purchase.
Sources Checked
ArcWeld product listing: TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32″)
Final check: match the torch series, confirm 3/32 in. tungsten sizing, and inspect the existing consumable stack before placing the order. If any of those details are unclear, mark them Unknown (Verify) and verify from the torch itself or the manual before buying.
Related Arc Weld Part
TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32")
Standard Size Gas Lens Collet Body for TIG torch #17, 18, 26
ERCuAl-A2 is a TIG/GTAW filler metal used in copper and bronze repair, overlay, and buildup work where aluminum bronze chemistry is the right fit. It is not a general-purpose rod. Before you order wire or strike an arc, confirm the base metal, the service condition, and the welding procedure requirements. The wrong match can create cracking, dilution problems, or a repair that will not hold up in service.
This draft focuses on selection checks and compatibility verification for ERCuAl-A2 TIG / GTAW filler metal. Use it as a starting point only. Confirm the WPS, code requirements, base metal grade, and manufacturer data sheet before welding.
Key Takeaways
ERCuAl-A2 is for aluminum bronze and related overlay work, not for every copper alloy job.
Verify the exact base metal grade before selecting the filler.
Check whether the repair is a deposit, a buildup, or a joining weld; the service duty changes the filler choice.
Do not assume compatibility from color, appearance, or old shop habits.
Use the WPS and the filler manufacturer data sheet as the final authority.
Start With the Base Metal
The first compatibility check is the parent metal. ERCuAl-A2 is associated with aluminum bronze and overlay work, but the exact fit depends on the alloy family and the service requirements. If the base metal is unknown, identify it before you weld. If the part has a casting number, mill cert, or in-house repair record, review that data first. If not, use positive material identification, shop records, or a qualified lab method as required by your procedure.
Check: Is the base metal aluminum bronze, a copper alloy, or something else? If the alloy is unknown, mark it as Unknown (Verify) and do not assume ERCuAl-A2 is correct.
Inspect: Look for previous repair welds, mixed-alloy sections, corrosion products, and wear patterns. These clues can change the deposit requirement.
Verify: Confirm the alloy family against the WPS and the manufacturer’s filler data sheet. If the procedure does not list the base metal, stop and get approval.
Match the Service Condition
Aluminum bronze filler is often considered for wear and corrosion overlays, but service conditions drive the final decision. A filler that works for one environment may fail in another. Temperature, abrasion, seawater exposure, chemical contact, impact, and galvanic pairing all matter. If the part runs hot, sees sliding wear, or sits in a corrosive environment, review whether the deposit chemistry and hardness range are suitable. If those details are not listed in the available data, treat them as Unknown (Verify).
Check: Is the job repair, buildup, surfacing, or joining? Different duties can require different filler metal selection.
Inspect: Review wear direction, crack location, and corrosion pattern. These details tell you whether you need a ductile deposit, a harder overlay, or a different repair method.
Verify: Confirm with the WPS or engineering note that ERCuAl-A2 is approved for the service environment.
Review the Welding Procedure Before You Order Rod
Do not buy filler metal first and hope it fits the procedure later. The WPS controls what you can use. Check the base metal range, joint type, preheat requirements, interpass limits, shielding gas, polarity, and any postweld requirements. If the WPS is missing, outdated, or written for a different alloy family, stop and get it corrected.
Check: Does the WPS specifically allow ERCuAl-A2 or an equivalent filler classification?
Inspect: Confirm whether the weld is governed by code, internal repair practice, or OEM instruction.
Verify: Match the rod diameter, process, and technique to the procedure. If rod size is not stated, use Unknown (Verify) until the document is reviewed.
Use the WSP Filler Metal Finder as a Starting Point
The WSP filler metal finder can help narrow the selection, but it does not replace procedure approval. Use it to compare classification, process, and intended application, then cross-check the result with the WPS and the base metal data.
Open the WSP filler metal finder and compare ERCuAl-A2 against the job requirements. Treat the finder as a selection aid, not a guarantee that the filler is approved for your part or code.
Check: Does the finder entry align with your process, material family, and repair intent?
Inspect: Look for any mismatch between the finder result and the procedure sheet.
Verify: If the finder suggests alternatives, confirm those alternatives before changing wire.
Review the ERCuAl-A2 Filler Page
The ERCuAl-A2 filler page is another starting point for selection. It identifies the product family as TIG/GTAW filler metal for aluminum bronze and overlay work, with AWS A5.7 referenced on the page. That is useful, but it is not the same as weld approval. Final compatibility still depends on the WPS, the base metal grade, and the service conditions.
Open the ERCuAl-A2 filler metal page and compare the page details with your repair requirement. Use it to confirm the classification and general application only. Do not treat it as automatic approval for a specific job.
Check: Does the page description match aluminum bronze and overlay work?
Inspect: Compare the page information with the filler data sheet from the manufacturer.
Verify: If the exact rod diameter, package size, or manufacturer is needed, use Unknown (Verify) until the actual item and datasheet are confirmed.
Practical Setup Checks Before Welding
Compatibility is not only about chemistry. TIG/GTAW setup affects the result. Clean the joint, remove oxides, and control fit-up. Use a clean tungsten, correct gas coverage, and stable torch technique. If the part shows porosity, arc wandering, or contamination, stop and correct the setup rather than continuing to add filler.
Check: Is the joint free of grease, oxide, paint, and embedded debris?
Inspect: Confirm torch angle, shielding coverage, and work lead placement.
Review the SDS and manufacturer instructions before use.
Use fume control and local exhaust ventilation.
Wear eye, hand, and skin protection suitable for hot metal and arc exposure.
Do not weld on unknown alloys until the material and procedure are verified.
Follow hot-work, confined-space, and lockout rules where applicable.
FAQ
Is ERCuAl-A2 a universal bronze filler? No. It is a specific TIG/GTAW filler metal for aluminum bronze and overlay work. Confirm the base metal and procedure before using it.
Can I choose ERCuAl-A2 based on the part color or previous repair history? No. Visual clues are not enough. Verify the alloy family and service condition first.
Does the WSP filler metal finder approve the weld? No. It is a selection aid only. Final approval comes from the WPS, code requirements, and manufacturer data.
What if the base metal grade is not known? Mark it as Unknown (Verify) and identify it before welding. Do not assume ERCuAl-A2 is correct.
For ERCuAl-A2 TIG / GTAW filler metal selection, the order of work is simple: identify the base metal, confirm the service duty, verify the WPS, then cross-check the filler page and data sheet. If any step is unclear, stop and mark the detail as Unknown (Verify) until it is proven.
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
Gas lens collet bodies are small parts, but they control a lot of TIG torch performance. If the fit is wrong, the tungsten may slip, shielding gas flow can be uneven, and the arc can become harder to manage. For buyers and maintenance teams, the main job is not just to order a replacement. It is to confirm the torch family, thread or consumable style, and the wear condition before parts are pulled from stock or installed.
The TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8″) is listed as a standard size gas lens collet body for TIG torch #17, #18, and #26. Beyond that, any deeper fitment detail should be treated as Unknown (Verify) unless it is confirmed in the torch and consumable documentation you are using.
Key Takeaways
Confirm the torch model before ordering. Do not assume all #17, #18, and #26 setups use the same consumables in every torch configuration.
Check the tungsten retention parts for wear if the tungsten slips, arcs wander, or the cup area looks damaged.
Verify the gas lens style, thread/series match, and cup compatibility before installation.
Use replacement as a controlled maintenance step, not just a cleanup task after arc problems appear.
If any compatibility point is uncertain, mark it Unknown (Verify) and confirm against the torch manual or the supplier listing.
Where this part fits in the torch
A gas lens collet body supports the tungsten and helps shape shielding gas flow through the front end of the torch. In practice, it is part of the consumable stack that includes the collet, cup or cup adapter, and tungsten. When the collet body is worn, dirty, or the wrong style, you may see inconsistent gas coverage, difficulty holding tungsten position, or an unstable arc.
For this item, the title indicates use with torch sizes #17, #18, and #26. That is the first check. The second check is whether your torch uses the same consumable family as the part you are buying. If your shop keeps mixed torch brands or mixed front-end setups, do not rely on torch size alone. Verify the series from the torch body, the old consumable, or the parts sheet.
Buying checks before you place the order
Use the steps below before you approve purchase or pull from stock:
Check the torch model. Read the torch tag, handle marking, or parts breakdown. Confirm it is a #17, #18, or #26 torch family.
Inspect the current front end. Remove the cup and look at the collet body for heat discoloration, thread damage, cracks, or contamination.
Verify the consumable series. Match the old part to the new part. If the old item is worn beyond legible markings, compare dimensions and thread style to the supplier description.
Check tungsten size and setup. The tungsten diameter and collet size must match the torch setup. If that match is uncertain, mark it Unknown (Verify).
Confirm gas lens versus standard collet body. This article is about a gas lens style. Do not substitute a standard collet body unless the torch setup is designed for it.
Check stock handling. Keep consumables clean, dry, and separated by torch series so front-end parts are not mixed during issue.
Troubleshooting: signs the collet body needs attention
If TIG performance has changed, inspect the collet body before replacing other parts at random. Common clues include tungsten slip, poor gas coverage, black soot near the cup, or repeated arc wandering. Those symptoms can also come from contaminated tungsten, poor gas supply, a damaged cup, or loose assembly. Do not assume the collet body is the only fault.
Check: Remove the consumables and look for carbon, spatter, or grinding dust in the gas path.
Inspect: Examine the collet body threads and contact surfaces for deformation, wear, or cross-threading.
Verify: Confirm that the collet, cup, and tungsten are assembled in the correct stack and tightened to normal shop practice. If the part style is unclear, stop and verify against the torch documentation.
Installation and support checks
When installing a new collet body, keep the work clean. Metal chips, lubricant, and abrasive dust can all affect front-end performance. Use a clean bench or a clean tray. Do not force threads. If the part does not start smoothly by hand, back out and verify the match rather than tightening through resistance.
After installation:
Check that the tungsten seats straight and does not rotate or slip under normal handling.
Inspect the cup interface for gaps, damage, or misalignment.
Verify gas flow at the torch before welding on production work.
Depressurize and isolate the torch/gas system before removing front-end parts.
Let hot consumables cool before handling.
Do not use damaged threads or cracked consumables in service.
Keep tungsten and consumables clean; contamination can affect arc stability and weld quality.
If the torch setup is unfamiliar, verify the parts breakdown before energizing the system.
FAQ
Q: Is this collet body automatically correct for every #17, #18, and #26 torch?
A: No. The title indicates those torch families, but you still need to verify the exact torch series and consumable stack used on your setup.
Q: What are the main signs of a worn gas lens collet body?
A: Tungsten slip, unstable arc behavior, poor shielding gas coverage, thread damage, and visible contamination in the front end are common signs. Other causes are possible, so inspect the full setup.
Q: Can I swap in a standard collet body instead of a gas lens collet body?
A: Not by assumption. Gas lens and standard front-end parts are not interchangeable in every setup. Verify the torch and cup configuration first.
Q: What should I do if I cannot confirm compatibility?
A: Treat the part as Unknown (Verify) until you match it against the torch parts breakdown, the removed consumable, or supplier documentation.
Sources Checked
ArcWeld product page: TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8″)
Internal support articles on TIG consumable wear and collet body troubleshooting
Related Arc Weld Part
TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8")
Standard Size Gas Lens Collet Body for TIG torch #17, 18, 26
ERCuSn-A TIG / GTAW filler metal is a starting point for phosphor bronze and copper-alloy repair and fabrication work. It is not a stand-alone approval to weld. Before you order rod or strike an arc, verify the WPS, code requirements, base metal grade, service conditions, and the manufacturer data sheet. If any of those inputs are unclear, stop and confirm them first.
This matters because bronze and copper-alloy jobs often look similar at the bench but behave differently in service. A filler that seems reasonable for one component can be wrong for another if the part sees wear, pressure, corrosive exposure, seawater, elevated temperature, or load-bearing service. Use the filler metal page as a selection starting point only.
Key Takeaways
ERCuSn-A is a selection starting point, not a procedure approval.
Verify the base metal family before matching filler to joint.
Check service conditions before welding bronze or copper alloys.
Confirm the WPS, code requirement, and manufacturer data sheet before use.
If compatibility is uncertain, document it as Unknown (Verify) and escalate.
What ERCuSn-A is used for
ERCuSn-A is listed on the Weld Support Parts filler metal page as a TIG / GTAW option for phosphor bronze and copper-alloy applications. That description is useful for narrowing the search, but it does not tell you whether the rod is approved for your job. The final decision belongs to the governing procedure, drawing, code, or OEM repair instruction.
For the source listing, review the filler metal page here: ERCuSn-A TIG / GTAW Filler Metal. Use the page as a reference point only. Confirm the base metal, diameter, and service requirement before ordering or welding.
Check the job before you choose the rod
Start with the part itself. Many compatibility errors happen because the base metal is assumed instead of verified.
Check the part drawing, BOM, or maintenance record for the base metal grade.
Inspect the failed part, if available, for color, wear pattern, and prior repair evidence.
Verify whether the component is phosphor bronze, copper alloy, or another bronze family. If the grade is not confirmed, record it as Unknown (Verify).
Check whether the joint is a repair, buildup, fillet, overlay, or fit-up weld. Different geometries create different dilution and heat-input concerns.
Verify whether the service includes corrosion exposure, seawater, electrical conductivity requirements, or sliding wear. Those conditions can change filler selection.
Compatibility checks at the bench
Before setup, compare the rod choice against the WPS and available documentation. Do not rely on memory or on a similar part that was welded in the past.
Check the WPS for the allowed filler classification.
Inspect the manufacturer data sheet for the filler metal family and any stated limitations.
Verify whether the code or job spec allows ERCuSn-A for the specific application.
Check whether alternate fillers are listed, such as ERCuSi-A, only if the procedure or spec names them. Do not substitute by assumption.
Verify rod diameter against joint access, heat input, and bead placement needs. Common sizes may exist, but any specific size for your job is Unknown (Verify) unless documented.
Procedure support: what to inspect before welding
Bronze and copper-alloy work is sensitive to contamination, fit-up, and heat control. A good filler cannot compensate for poor prep.
Inspect the joint for oil, oxide, paint, corrosion, and embedded dirt.
Check that the joint faces are bright and mechanically clean where required by the procedure.
Verify clamp stability and heat-sink needs before starting.
Inspect tungsten condition and grind quality. Contamination problems can create arc instability that looks like a filler issue. See TIG Tungsten Contamination Troubleshooting.
WSP lookup and cross-check workflow
If your internal purchasing or support process includes a Weld Support Parts lookup step, use it to confirm the current listing and related guidance before release to the floor. For this topic, the allowed filler metal source page is the primary reference. When a WSP lookup page is available in your workflow, compare the lookup result against the filler listing and the job documentation. If there is a mismatch, stop and investigate. If no lookup page is provided, note that as Unknown (Verify) and proceed only after the responsible engineer or supervisor confirms the selection.
Use the filler metal finder here as a starting point for narrowing the choice: WSP Filler Metal Finder. It helps direct the search, but it does not approve a procedure, a code case, or a repair plan.
Field troubleshooting when ERCuSn-A is being considered
If the part has already failed once, the wrong filler may not be the only issue. Work through the job in sequence.
Check whether the original failure was caused by overload, corrosion, wear, or poor fit-up.
Inspect the fracture surface and heat-affected area for signs of previous contamination or overheating.
Verify that the repair method matches the duty cycle. A cosmetic repair is not the same as a structural or wear repair.
Check whether preheat or interpass controls are specified. If not specified, do not assume values; mark them Unknown (Verify).
Verify final acceptance criteria before post-weld cleanup and return to service.
Safety notes
Use normal TIG/GTAW PPE, including eye protection, gloves, and skin coverage.
Control fumes, especially in confined areas or on contaminated bronze/copper components.
Do not weld unknown materials until the base metal is identified.
Do not substitute filler based on color, habit, or availability alone.
If the job is safety-critical, stop and verify approval before welding.
FAQ
Q: Is ERCuSn-A automatically correct for any bronze repair?
A: No. It is only a starting point. Confirm the base metal, the WPS, and the service condition before use.
Q: Can I swap in a similar bronze filler if ERCuSn-A is unavailable?
A: Not without procedure approval. If the filler is not named on the WPS or job spec, treat the substitute as Unknown (Verify) until it is approved.
Q: What should I check first on a copper-alloy repair job?
A: Check the base metal identification, then inspect the joint for contamination, then verify the WPS and service requirements.
Q: Does the filler metal page guarantee code compliance?
A: No. The filler page is a selection guide, not a code or procedure approval.
Before release to production, verify the job against the current WPS and the manufacturer data sheet. If any input is missing, document it as Unknown (Verify) and hold the work until it is confirmed.
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
ERCuSi-A TIG / GTAW filler metal is a common starting point for silicon bronze braze-welding and certain copper-alloy applications. It is often selected when the job calls for lower base-metal dilution, improved cosmetic appearance, or joining sheet metal with controlled heat input. That said, the filler metal name alone does not make it a qualified choice. The weld support team still needs to verify the WPS, the base metal, the service environment, and the manufacturer data sheet before the first arc starts.
This guide is for selection checks, not procedure approval. If the material, joint design, or service condition is uncertain, stop and verify before welding.
Key Takeaways
ERCuSi-A is a starting point for silicon bronze TIG/GTAW work, not a blanket approval for every copper or sheet metal job.
Check the WPS first. If no WPS exists, verify whether the job requires one and whether ERCuSi-A is permitted.
Confirm base metal grade, thickness, and service conditions before selecting wire size or travel plan.
Use the filler metal finder and manufacturer data sheet to confirm the intended use, not just the classification name.
For uncertain compatibility, mark the detail as Unknown (Verify) and route it for review.
Where ERCuSi-A Fits
ERCuSi-A is typically associated with silicon bronze filler selection for TIG/GTAW. In support work, it is often evaluated for braze-welding, sheet metal repair, cosmetic build-up, and compatible copper-alloy work. The practical benefit is usually lower heat input than a fusion weld on thin or sensitive base metal. That does not mean it is suitable for every repair. Joint design, fit-up, corrosion exposure, fatigue loading, and post-weld requirements can change the decision.
If the base metal is not clearly identified, treat it as Unknown (Verify). Do not assume a bronze filler is acceptable just because the material looks similar to copper or brass.
Check the WPS Before You Select Wire
Start with the welding procedure specification if one exists. The WPS should define whether the job allows braze-welding, which filler metal classifications are approved, and whether any preheat, shielding gas, or joint limits apply. If the WPS is missing, incomplete, or outdated, stop and verify before ordering wire or setting up the torch.
Check:
WPS number, revision, and job scope
Approved filler metal classification
Base metal group and thickness range
Required shielding gas and process limits
Any code or customer restrictions
Inspect: the joint area for contamination, paint, plating, oxide buildup, oil, and moisture. Silicon bronze work is sensitive to surface condition. Dirty edges can give poor wetting, unstable arc behavior, or weak cosmetic results.
Verify: whether the repair is structural, cosmetic, or service-critical. If the repair carries load, pressure, or corrosion exposure, the filler choice may require formal approval. Unknown (Verify) is the correct status until that review is complete.
Base Metal Compatibility Checks
ERCuSi-A is not a universal match for all copper alloys or all mixed-metal joints. The support team should confirm the actual base metal grade before proceeding. That includes checking whether the part is copper, brass, bronze, or a coated steel assembly. If the part was previously repaired, identify the existing filler if possible. Mixed chemistry can change wetting behavior and service performance.
Check:
Base metal identification from print, mill cert, tag, or site record
Thickness and heat sensitivity
Whether dissimilar metal joining is involved
Whether the application is decorative, low-load, or service-critical
Inspect: edges and joint fit-up. Large gaps may push the repair outside the intended use of the filler. If fit-up is inconsistent, verify whether build-up or backing is needed, or whether the repair should be reworked before welding.
Verify: the service temperature, corrosion exposure, and any downstream finishing steps. A filler that wets well during welding may still be the wrong choice if the assembly sees chemicals, high wear, or code-controlled service.
Filler Metal Finder as a Selection Starting Point
Use the WSP filler metal finder as a selection starting point only. It can help narrow the search by process, classification, or base-material family, but it does not replace the WPS or manufacturer data sheet. If the finder suggests ERCuSi-A for the job, treat that as a lead to review, not a final approval.
When comparing options, confirm whether the application needs silicon bronze, a different copper-alloy filler, or another repair method entirely. If the part is aluminum, steel, stainless, cast iron, or an unknown alloy, do not assume ERCuSi-A is appropriate. Mark the fit as Unknown (Verify) until the compatibility question is resolved.
Practical Setup and Handling Checks
Before welding, check the wire condition and setup. Filler rod should be clean, dry, and free of heavy oxidation or contamination. Keep rods separated from steel grinding dust, oil, and shop debris. Use the size called out by the WPS or job plan. If the wire diameter is not specified, verify the required size before selecting from stock.
Check: torch setup, cup size, tungsten condition, and shielding gas flow. For general TIG setup support, see the Square Wave 205 TIG Cup Size Selection Guide for cup size, gas lens, and stickout checks. Although that article is not specific to ERCuSi-A, the setup discipline is the same: stable shielding, clean arc starts, and correct torch geometry.
Inspect: tungsten for contamination or improper grind. If the arc wanders, starts dirty, or black specks appear, review the tungsten and gas path before blaming the filler. See the TIG Tungsten Contamination Troubleshooting guide for re-grind and contamination checks.
Verify: arc stability, wetting behavior, and bead shape on a test coupon when the application is new, thin-gauge, or service-critical.
Troubleshooting Support Checks
If the bead is rough, the wetting is poor, or the repair lifts at the edges, work through the basic checks in order:
Check joint cleanliness again.
Inspect shielding gas coverage and torch angle.
Verify travel speed and heat input.
Confirm that the base metal and filler are actually compatible.
Review whether the job should be braze-welded or repaired by another method.
For arc wander or unstable starts, grounding and torch setup can also matter. The TIG arc wandering causes guide covers tungsten, gas, ground, and AC setup checks that apply broadly to GTAW troubleshooting.
Safety Notes
Follow standard welding safety practices. Use eye and face protection, gloves, and flame-resistant clothing. Provide ventilation appropriate for the work area. Clean coatings, oils, and plated surfaces before welding only if the site procedure allows it. If there is any chance of unknown coating chemistry, treat the job as a fume risk and verify controls before proceeding.
Do not weld on pressure-containing, load-bearing, or regulated parts without confirming the required procedure and approval path. If the job classification is uncertain, stop and verify with the supervisor, engineer, or quality contact.
FAQ
Q: Is ERCuSi-A the right choice for every copper repair?
A: No. It is a starting point for silicon bronze TIG/GTAW selection. Confirm the exact base metal, joint design, and service condition first.
Q: Can I use ERCuSi-A just because the finder suggests it?
A: No. The filler metal finder is a selection aid, not procedure approval. The WPS and manufacturer data sheet still control the final choice.
Q: What should I do if the base metal is not clearly identified?
A: Treat it as Unknown (Verify). Do not assume compatibility from appearance alone.
Q: Does ERCuSi-A automatically fit structural or code work?
A: Not automatically. Verify code requirements, WPS limits, and customer approval before using it on regulated work.
Notes: AWS spec listed on the source page: AWS A5.7. Any additional technical detail not confirmed on the provided source pages should be treated as Unknown (Verify).
Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
To provide the best experiences, we use technologies like cookies to store and/or access device information. Consenting to these technologies will allow us to process data such as browsing behavior or unique IDs on this site. Not consenting or withdrawing consent, may adversely affect certain features and functions.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.