Search results for: “respirator guide”

  • Flux-Core Respirator Guide: P100 vs Nuisance Vapor vs PAPR

    Flux-core welding can create a heavier visible fume plume than many short-circuit MIG jobs, especially with self-shielded wire, higher amperage, long beads, poor ventilation, coated steel, or outdoor work where the welder keeps chasing the plume. Choosing a respirator for flux-core work should start with the exposure, not the mask style.

    This guide explains when a P100 half-mask may be appropriate, when nuisance organic vapor relief is only an odor-control add-on, and when a PAPR becomes the better decision. For under-hood fit issues, see the WSP guide to welding respirators that fit under a welding helmet. If fumes are still noticeable through the mask, troubleshoot respirator seal leaks and fume smell before continuing to weld.

    Key Takeaways

    • P100 filters are commonly used for welding fume particulate, including flux-core welding fume, when the hazard assessment supports that choice.
    • Nuisance organic vapor relief is not the same as certified organic vapor protection. It is for low-level odor relief only when concentrations are below applicable exposure limits.
    • A PAPR is the stronger decision point for long flux-core shifts, stainless or hardfacing work, high fume volume, poor hood comfort, facial hair conflicts, or failed half-mask fit tests.
    • Ventilation still comes first. Respirators do not replace local exhaust, fume extraction, clean base metal, or keeping the head out of the plume.
    • For workplace use, respirator selection must follow the employer’s OSHA respiratory protection program, fit testing, training, filter change schedule, and medical clearance process.

    Problem / Context

    Flux-core welding creates a fume exposure problem that changes with wire type, base metal, voltage, amperage, arc length, shielding method, coatings, ventilation, and body position. A small repair bead outside is not the same exposure as all-day FCAW production welding inside a bay.

    The wrong respirator decision usually shows up in one of four ways: the welder smells fumes, the hood fogs, breathing resistance increases quickly, or the mask gets removed because it does not fit under the hood. For filter-specific background, see the WSP article on P100 respirators for welding fumes. For coated steel, also review safe fume-control tactics for welding galvanized material.

    Root Causes of Bad Respirator Decisions in Flux-Core Welding

    • Treating all flux-core welding as the same exposure.
    • Using a P100 filter for fumes without checking whether gases, vapors, coatings, or stainless alloy constituents are also present.
    • Confusing nuisance organic vapor relief with full organic vapor cartridge protection.
    • Relying on smell as the only warning sign of exposure.
    • Using a tight-fitting half-mask without a fit test where workplace rules require one.
    • Welding over paint, oil, primer, galvanizing, brake cleaner residue, or unknown coatings.
    • Working in a corner, tank, trailer, pit, or enclosed structure without proper ventilation evaluation.
    • Running self-shielded flux-core at high output while positioned directly above the plume.

    Decision Point 1: When P100 Makes Sense

    A P100 half-mask is commonly considered for flux-core welding when the main concern is particulate welding fume and the work environment allows a tight-fitting respirator to seal correctly. P100 filters are rated for at least 99.97% filtration efficiency against airborne particles when used as part of an approved respirator system.

    • Use P100 as the baseline when the hazard is welding fume particulate and the respirator is correctly selected, fitted, and maintained.
    • Choose a low-profile mask if the respirator must fit under a welding hood.
    • Perform a seal check every time the respirator is worn.
    • Replace filters when breathing resistance increases, filters are damaged, filters are dirty, or the written change schedule requires replacement.
    • Do not assume P100 covers gases, vapors, solvents, coatings, or oxygen-deficient atmospheres.

    Decision Point 2: When Nuisance Organic Vapor Relief Helps

    Nuisance organic vapor relief can help reduce low-level odors from some welding environments, but it should not be treated as a gas-and-vapor cartridge. Manufacturer guidance for nuisance-level organic vapor relief generally limits it to odor relief where organic vapor concentrations do not exceed OSHA permissible exposure limits or other applicable exposure limits.

    For flux-core welding, nuisance OV relief may be useful when the welder is dealing with mild odor from trace contaminants or shop conditions and the actual exposure has already been evaluated. It is not the right answer for unknown coatings, paint burning, solvent residue, confined spaces, or work where an organic vapor cartridge or supplied-air solution is required.

    • Use nuisance OV relief for odor comfort only after the hazard is known.
    • Do not use nuisance OV relief as proof of protection from organic vapors.
    • Do not weld over solvents, degreasers, paint, or coatings because a nuisance OV filter is installed.
    • Escalate to the correct cartridge, PAPR configuration, supplied-air system, or industrial hygiene review when vapors are part of the exposure.

    Decision Point 3: When a PAPR Is the Better Choice

    A PAPR can be the better decision for flux-core welding when the job creates sustained fume, the welder needs longer wear time, a tight-fitting half-mask does not work, or the exposure assessment calls for a higher assigned protection factor than a half-mask provides. A PAPR also avoids the under-hood fit conflict because respiratory protection is built into the hood system.

    • Choose a PAPR for long-duration FCAW production work with visible sustained fume.
    • Consider a PAPR for stainless flux-core, hardfacing, high-manganese consumables, or unknown alloy work after reviewing the SDS and exposure data.
    • Use a PAPR when a half-mask repeatedly breaks seal under the hood.
    • Use a PAPR when facial hair prevents a tight-fitting half-mask from sealing, if the selected PAPR configuration is appropriate for the workplace program.
    • Use a PAPR when heat, breathing resistance, or comfort causes workers to remove half-mask protection.
    • Do not use a PAPR in oxygen-deficient or IDLH conditions unless the system is specifically approved for that condition. Many PAPRs are not.

    Specs / Verification Notes

    OptionWhat It HandlesBest Flux-Core Use CaseVerification Note
    P100 half-maskParticulate welding fume when properly selected and sealedShort to moderate FCAW work where the main hazard is particulate fumeFilter class, facepiece approval, fit test status, and hood clearance must be verified.
    P100 with nuisance OV reliefParticulate fume plus nuisance-level organic vapor odor reliefFlux-core work where odor relief is desired and vapor exposure is confirmed below applicable limitsNuisance OV relief is not full organic vapor respiratory protection.
    Organic vapor or combination cartridgeSpecific gases or vapors when the cartridge is approved for that hazardOnly when the hazard assessment identifies a gas or vapor that the cartridge is approved to addressDo not guess. Match cartridge to SDS, exposure data, and manufacturer instructions.
    Welding PAPRFiltered airflow through an approved powered systemLong FCAW shifts, high visible fume, half-mask seal problems, or higher protection needsConfirm filter type, assigned protection factor, battery condition, airflow check, and workplace program requirements.
    Supplied-air respiratorBreathing air supplied from an approved sourceSituations where air-purifying respirators are not adequateRequired for some atmospheres; must be selected by a qualified safety professional.

    Product Section

    Check Arc Weld Store first for Miller LPR-100 Gen. II respirators and replacement filters. Amazon fallback boxes are included only for verified ASINs.

    No products found.

    The Miller LPR-100 is the practical half-mask option for flux-core welders who need a low-profile P100 respirator under a hood. The verified Amazon listing identifies nuisance-level OV relief, P100 filtration, and under-helmet welding use. Confirm size, filter version, and workplace approval before purchase.

    No products found.

    The 3M Adflo and Versaflo welding PAPR kit is the escalation option when a half-mask is not enough for the job conditions, fit, comfort, or exposure assessment. Confirm the exact configuration, filters, assigned protection factor, and welding helmet setup before using it for flux-core production work.

    Comparison Table: P100 vs Nuisance OV vs PAPR

    QuestionP100 Half-MaskP100 with Nuisance OV ReliefPAPR
    Is the main problem particulate welding fume?Usually the starting pointAlso possiblePossible, often stronger for long work
    Is odor the main complaint?May not help odorMay reduce nuisance-level odor onlyMay help depending on filter setup
    Are coatings, solvents, or unknown vapors present?Do not assume coverageNot enough by itselfVerify approved cartridge/filter or use another control
    Does the welder have facial hair on the seal area?Usually a problem for tight-fitting masksUsually a problem for tight-fitting masksMay be a better route depending on selected hood and program rules
    Is the job all-day FCAW production?Possible but may be uncomfortablePossible but still tight-fittingOften the better comfort and compliance choice
    Does the hood hit the mask?Low-profile model requiredLow-profile model requiredIntegrated hood system avoids this conflict

    Flux-Core Respirator Selection Workflow

    • Identify the wire type: self-shielded flux-core, gas-shielded flux-core, stainless, hardfacing, or specialty alloy.
    • Review the SDS for the wire, base metal, coatings, cleaners, and any nearby process contaminants.
    • Improve ventilation and position the work so the plume moves away from the breathing zone.
    • Select P100 only when particulate fume is the hazard being addressed.
    • Add nuisance OV relief only for nuisance-level odor relief, not for certified vapor protection.
    • Move to a PAPR when exposure level, comfort, seal, production duration, facial hair, or helmet interference makes a half-mask the wrong tool.
    • Use industrial hygiene sampling when exposure level is uncertain.

    Related Failure Paths

    Safety Notes

    Flux-core welding fume can contain metal oxides and other constituents from the electrode, base metal, coatings, flux ingredients, and process conditions. AWS guidance emphasizes keeping the head out of the fumes and using ventilation or other controls to keep fumes and gases away from the breathing zone. OSHA guidance states that respiratory protection may be required when work practices and ventilation do not reduce exposures to safe levels.

    • Do not weld in confined spaces without proper evaluation, ventilation, monitoring, and rescue planning.
    • Do not weld over chlorinated solvent residue, brake cleaner residue, paint, galvanizing, plating, oil, or unknown coatings.
    • Do not treat a nuisance OV filter as an organic vapor cartridge.
    • Do not use a tight-fitting half-mask without a clean sealing surface.
    • Do not keep welding if the respirator shifts, leaks, smells wrong, becomes hard to breathe through, or causes eye and throat irritation.
    • Use fit testing, medical evaluation, training, written procedures, inspection, cleaning, and storage when required by OSHA respiratory protection rules.

    FAQ

    Is a P100 respirator enough for flux-core welding?

    A P100 respirator may be appropriate when the main hazard is particulate welding fume and the respirator is properly selected, fitted, sealed, and maintained. It is not automatically enough for gases, vapors, coatings, solvents, stainless alloy work, confined spaces, or oxygen-deficient atmospheres.

    What does nuisance organic vapor relief mean?

    Nuisance organic vapor relief means the filter may reduce low-level organic vapor odors. It does not mean the filter is approved as full organic vapor respiratory protection. Use it only within the manufacturer’s stated limitations and the workplace respiratory protection program.

    When should a flux-core welder use a PAPR?

    A PAPR is a stronger choice for long-duration flux-core production, high fume volume, failed half-mask fit, facial hair conflicts, comfort problems, helmet interference, or exposure conditions that call for a higher level of respiratory protection.

    Does self-shielded flux-core need more respiratory protection than gas-shielded flux-core?

    Not automatically. Self-shielded flux-core often produces a visible fume plume, but protection decisions should be based on the wire SDS, base metal, coatings, amperage, ventilation, work position, exposure monitoring, and applicable limits.

    Can a respirator fix poor ventilation?

    No. Respirators are part of exposure control, not a replacement for ventilation. Use local exhaust, fume extraction, clean material, better body positioning, and process changes before relying only on respiratory PPE.

    Next Step

    For general flux-core work where particulate fume is the main verified hazard, start with a properly fitted low-profile P100 respirator and confirm hood clearance. Add nuisance OV relief only when odor relief is appropriate and exposure limits are not exceeded. Move to a welding PAPR when flux-core work is long, smoky, uncomfortable, difficult to fit, or high enough exposure that a half-mask is no longer the right decision.

    Sources Checked

    • AWS Safety and Health Fact Sheet No. 1, Fumes and Gases: https://aws-p-001-delivery.sitecorecontenthub.cloud/api/public/content/Fact-Sheet-No.1
    • AWS Safety and Health Fact Sheet, When to Use Respiratory Protection: https://aws-p-001-delivery.sitecorecontenthub.cloud/api/public/content/c09ba1fbf05a4badb79b2a9c2b47df9d
    • AWS Safety and Health Fact Sheet No. 36, Ventilation for Welding and Cutting: https://aws-p-001-delivery.sitecorecontenthub.cloud/api/public/content/Fact-Sheet-No.36
    • OSHA, Controlling Hazardous Fume and Gases during Welding: https://www.osha.gov/sites/default/files/publications/OSHA_FS-3647_WELDING.pdf
    • OSHA, 29 CFR 1910.134 Respiratory Protection: https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.134
    • OSHA, Appendix B-1 User Seal Check Procedures: https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.134AppB1
    • 3M, Welding Disposable and Reusable Respirator Sample: https://www.3m.com/3M/en_US/worker-health-safety-us/personal-protective-equipment/welding-disposable-and-reusable-respirator-sample/
    • 3M, Particulate Filter 2097 P100 with Nuisance Level Organic Vapor Relief: https://multimedia.3m.com/mws/media/5188O/3m-particulate-filter-2097-p100.pdf
    • Lincoln Electric SDS example for welding fume constituents: https://www.lincolnelectric.com/assets/US/EN/MSDS_lib/ZLE_SDS_NA-EN-200000000177.pdf
    • MillerWelds, PAPR with T94-R: https://www.millerwelds.com/safety/respiratory/powered-air-purifying-respirators-m00482
    • MillerWelds, Powered Air-Purifying Respirator owner manual: https://www.millerwelds.com/files/owners-manuals/o235936m_mil.pdf
    • Arc Weld Store, Air Cleaning Equipment and Respirators: https://www.arcweld.store/collections/air-cleaning-equipment-and-respirators
  • Miller 295274 LPR-100 Gen II Respirator Review & Guide

    Miller 295274 LPR-100 Gen II Respirator Review & Guide

    Miller 295274 LPR-100 Gen II Respirator Review & Guide

    Note for Readers: This post may contain affiliate links. If you purchase through them, we may earn a small commission at no cost to you. Thank you for supporting our site.

    Introduction

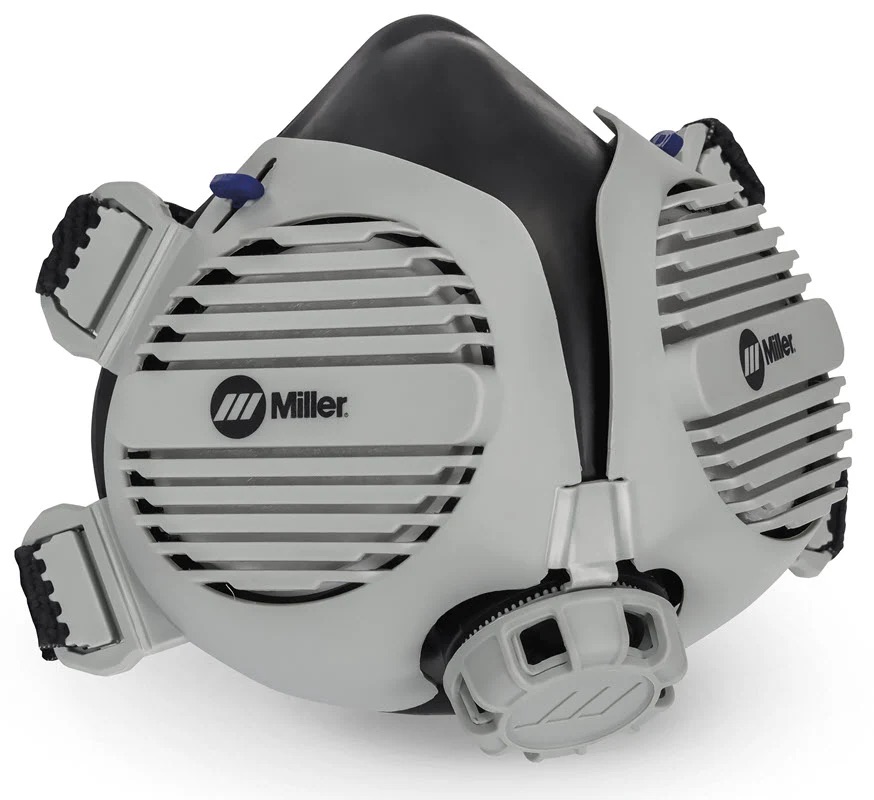
    The Miller 295274 LPR-100 Gen II Respirator is a next-generation low-profile respirator designed specifically for welding and metal fabrication environments. Built for professionals who need superior respiratory protection without sacrificing comfort, visibility, or mobility, this advanced PPE (personal protective equipment) is ideal for high-particulate operations such as grinding, cutting, plasma arc cutting (PAC), GMAW (MIG), GTAW (TIG), FCAW (flux-cored), and SMAW (stick welding).

    This respirator is commonly used by:
    Professional welders
    Fabrication technicians
    Welding instructors and students
    Industrial maintenance crews
    Engineers and inspectors working on active job sites

    Whether you’re welding galvanized steel or cutting aluminum, the LPR-100 Gen II offers a critical level of respiratory protection against harmful metal fumes and airborne particulates.

    Types / Variants / Models

    While the Miller LPR-100 series has multiple models, the 295274 Gen II version is an upgraded design that builds upon the success of the original LPR-100 respirator. Here’s how the Gen II compares to earlier versions:

    LPR-100 Gen I: Original model with basic comfort and protection features; widely used for general welding applications.
    LPR-100 Gen II (295274):
    – Redesigned headgear and improved face seal for better comfort and fit
    Adjustable straps with quick-release buckles
    – Integrated adjustable exhaust valves for better breathability
    Optional HEPA filter compatibility

    The 295274 Gen II version delivers improved ergonomics and safety specs that make it more suitable for long-term wear in high-use industrial environments.

    Key Features or Specifications

    The Miller 295274 LPR-100 Gen II Respirator is built to meet rigorous workplace demands. Below are key features and what they mean for welders:

    Low-Profile Design:
    – Fits under most welding helmets, including Miller Digital Infinity and Digital Elite series.
    – Great for tight workspaces and precise fabrication jobs.

    Two-Stage Filtration System:
    – P100/HEPA filters capture ≥99.97% of airborne particulates.
    – Protects against metal fumes from mild steel, stainless, aluminum, and galvanized metals.

    Replaceable Filters:
    – Easy twist-on design promotes hygienic filter changes.
    – Compatible with P100 filters specific to Miller (sold separately).

    Superior Seal Design:
    – Medical-grade silicone face seal minimizes leakage, remains soft and conformable during extended wear.

    Durable Construction:
    – Built from impact- and heat-resistant materials for rugged environments.

    Certifications:
    NIOSH Certified P100 – verified filtration and safety system compliant with U.S. occupational safety standards.

    Specs Overview:
    – Weight: ~7.5 oz
    – Compatibility: Most major welding helmet brands (especially Miller)
    – Size Options: One size fits most (adjustable strap system)
    – ASIN: B0DKLYQRL4

    Usage & Compatibility

    The LPR-100 Gen II is exceptionally versatile across welding processes. Here’s how and where it fits in:

    SMAW (Stick Welding): Great for outdoor or shielded applications where heavy particle exposure is likely.
    GMAW (MIG) and FCAW (Flux-Cored): Ideal when welding galvanized or painted steel where zinc oxide fumes are a hazard.
    GTAW (TIG): Low-profile allows unimpeded head movement and close-up focus, making it suitable for precision TIG work.
    Plasma Cutting & Grinding: Combines with face shields or auto-darkening helmets to maintain respiratory protection without bulk.

    Compatibility Notes:
    – Fits under most Miller helmets, including the Digital Infinity, T94i, and Titanium 9400i.
    – Compatible with grinding shields and face protection systems.
    – Not designed for use with supplied air or powered air-purifying respirator (PAPR) systems.

    Pros:
    – Excellent fit and comfort for long shifts.
    – Easy filter replacement and maintenance.
    – Superior low-profile ergonomics.

    Cons:
    – Filters must be purchased separately.
    – Not for use in oxygen-deficient or IDLH environments.

    Common Applications

    The Miller 295274 LPR-100 Gen II shines in metalworking sectors where clean breathing air is critical:

    Heavy Fabrication & Structural Welding:
    – Protects against thick fume concentrations in shipbuilding, steel bridges, and structural metalwork.

    Vehicle & Equipment Repair:
    – Ideal for tasks involving rusted or painted metal surfaces that emit chemical fumes or particulates.

    Industrial Maintenance:
    – Great for routine welding or grinding during plant turnarounds or refinery shutdowns.

    Welding Schools and Training Shops:
    – Lightweight and student-friendly, the Gen II is popular in welding education for extended learning environments.

    Tips & Best Practices

    To get the most from your Miller LPR-100 Gen II:

    Fit Check Before Each Use:
    – Ensure a snug seal around the nose and cheeks; perform a positive/negative pressure test.

    Change Filters Regularly:
    – Replace filters after 40 hours of use or sooner if breathing becomes difficult. Don’t wait for visible signs of clogging.

    Clean After Each Day:
    – Wipe the inner seal and shell with a damp cloth.
    – Avoid harsh chemicals that can degrade the silicone.

    Helmet Compatibility:
    – Test fit with your welding helmet before field use. Make sure the face seal doesn’t interfere with the helmet’s down position.

    Storage:
    – Keep in a sealed plastic bag or respirator case between uses to prevent dirt and dust accumulation.

    Avoid These Common Mistakes:
    – Using damaged or expired filters.
    – Wearing over facial hair, which can break the seal.
    – Failing to flush exhaust valves if breath condensation builds up.

    Conclusion

    The Miller 295274 LPR-100 Gen II Respirator is a top-tier choice for welders, metalworkers, and fabrication professionals who need compact, comfortable, and effective respiratory protection. Its improved Gen II fit, certified filtration, and low-profile design make it ideal for daily use in high-fume applications—without compromising helmet compatibility or range of motion.

    Whether you’re laying down MIG welds on mild steel or TIG-ing stainless pipe in a tight corner, this respirator helps you breathe easier and stay compliant with workplace safety guidelines.

    If you’re serious about protecting your lungs on the job, the LPR-100 Gen II is an investment in both safety and comfort.

    No products found.

    **Check the latest price and read (Incomplete: max_output_tokens)

  • Washington Alloy THF-700HT-173 Hard Face Flux-Cored MIG Wire Fitment Guide

    Washington Alloy THF-700HT-173 is a .045 in. hard face flux-cored MIG wire supplied on a 33 lb spool for rebuilding worn steel parts exposed to metal-to-metal abrasion. This article is built to help maintenance shops, repair departments, and industrial buyers verify whether this hardfacing wire matches the job before ordering.

    For current availability, order verification, and shipping details, Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

    “>view this product at Arc Weld Store.

    Key Takeaways

    • Product: Washington Alloy THF-700HT-173 hard face flux-cored MIG wire.
    • Size: .045 in. wire on a 33 lb spool.
    • Primary use: high metal-to-metal abrasion applications.
    • Deposit structure: martensitic; designed to work harden in service.
    • Common applications include rollers, conveyor screws, crusher rolls, and mill hammers.
    • Verify machine capacity, drive rolls, liner size, polarity, shielding gas, and base metal condition before ordering.

    Product Overview

    Washington Alloy 700HT is a hardfacing flux-cored wire intended for wear-facing work where abrasion resistance is more important than general fabrication weld strength. The Arc Weld Store listing describes this product as primarily used for high metal-to-metal abrasion. The manufacturer technical data states that 700HT produces martensitic weld deposits that work harden in service and bond well with fatigued or older hard-faced deposits.

    This is not a general-purpose ER70S-6 replacement. It should be selected when the repair objective is wear resistance on appropriate steel components, not when the job requires a mild steel structural filler wire.

    Upper-middle CTA: Need the .045 in. 33 lb spool? Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

    “>check current stock at Arc Weld Store before scheduling the repair.

    Best For

    • Industrial maintenance hardfacing.
    • Metal recovery on worn steel components.
    • High abrasion areas where parts see metal-to-metal wear.
    • Crusher rolls, mill hammers, conveyor screws, rollers, and similar wear parts.
    • Repair departments that need a full 33 lb spool for recurring hardface work.

    Key Specs

    FieldVerified Detail
    BrandWashington Alloy
    ProductTHF-700HT-173 Hard Face Flux-Cored MIG Wire
    SKUTHF-700HT-173 – 1 SPOOL
    Wire diameter.045 in.
    Spool weight33 lb
    Wire typeHardfacing flux-cored wire
    Polarity from manufacturer procedureDCEP
    Typical .045 in. procedure rangeWire speed 195–475 ipm; amps 125–245; volts 25–29; electrical stickout 1/2–1 in.; CO2 35–45 cfh
    Mixed gas noteManufacturer TDS notes 1–2 volts lower used with mixed gas
    Typical hardnessRockwell C 58–61 per manufacturer TDS
    Typical weld metal chemistryCarbon, chromium, manganese, silicon, molybdenum, tungsten, nickel, vanadium, phosphorus, sulfur listed by manufacturer TDS
    AWS classificationUnknown (Verify)
    CertificationsUnknown (Verify)

    Compatibility / Fitment Notes

    Fitment for this product is less about torch model and more about whether your MIG or FCAW system can correctly feed and run .045 in. hardfacing flux-cored wire. Before ordering, verify that your feeder accepts 33 lb spools, your drive rolls match .045 in. flux-cored wire, your gun liner is sized correctly, and your power source can run the required amperage and voltage range.

    Compatibility with a specific welding machine, feeder, gun, liner, drive roll, contact tip, shielding gas blend, or base metal is Unknown (Verify) unless confirmed against your equipment documentation and the manufacturer procedure data.

    Before You Order

    • Machine model: Confirm your welder can run .045 in. FCAW hardfacing wire in the required output range.
    • Wire feeder: Verify 33 lb spool capacity and hub compatibility.
    • Drive rolls: Confirm the correct .045 in. flux-cored drive roll style. Compatibility: Unknown (Verify).
    • Gun liner: Confirm the liner supports .045 in. wire and is clean enough for consistent feed.
    • Contact tips: Use contact tips sized for .045 in. wire. Brand and series compatibility: Unknown (Verify).
    • Polarity: Manufacturer procedure data lists DCEP.
    • Shielding gas: Manufacturer procedure data lists CO2 ranges and notes lower voltage with mixed gas. Verify your exact procedure.
    • Base metal: Confirm the part is suitable for hardfacing and that previous deposits, cracking, or contamination are addressed.
    • Preheat/interpass: Manufacturer TDS notes that 300–500°F preheat/interpass may yield superior properties.
    • Application: Confirm the job is abrasion-focused rather than a structural joining weld.
    • Safety documentation: Review the SDS before use and confirm shop ventilation, PPE, and fume controls.

    Accessories / Compatible Products

    Because consumable fit depends on your exact MIG gun, feeder, and wire path, do not order tips, liners, nozzles, or drive rolls by wire diameter alone. Match the consumable series to your gun and confirm the .045 in. size before purchase.

    Weld Support Parts Breakdown Reference

    No torch-specific parts breakdown is required to identify this wire because the product is a welding consumable, not a gun or torch assembly. For safety documentation, review the confirmed hardfacing flux-cored SDS before use.

    If you are replacing contact tips, liners, nozzles, diffusers, or drive rolls at the same time, use the parts breakdown for your specific MIG gun or feeder before ordering those items.

    Common Applications

    • Crusher roll repair.
    • Mill hammer hardfacing.
    • Conveyor screw rebuilding.
    • Roller wear-facing.
    • Industrial equipment repair where metal-to-metal abrasion is the primary failure mode.
    • Maintenance welding on older hard-faced deposits when procedure and base metal condition are verified.

    Shipping / Returns Notes

    The Arc Weld Store product page lists free ground shipping to the lower 48 on qualifying orders, shipment from Corydon, Indiana, typical 1–2 business day shipping unless noted, and returns accepted on unused items in original packaging. Confirm current shipping, pickup, and return details on the product page before purchasing.

    FAQ

    Is Washington Alloy THF-700HT-173 a general MIG wire?

    No. It is a hardfacing flux-cored MIG wire intended for abrasion-resistant deposits. Use a general-purpose filler only when the application calls for it.

    What wire size is this spool?

    The Arc Weld Store listing identifies this product as .045 in. wire on a 33 lb spool.

    What polarity does the manufacturer procedure list?

    The Washington Alloy technical data sheet lists DCEP for the typical FCAW welding procedures.

    Can I use my existing MIG gun consumables?

    Compatibility is Unknown (Verify). Confirm your gun series, liner size, contact tip size, drive roll style, and feeder capacity before ordering replacement consumables.

    Does this wire require shielding gas?

    The manufacturer procedure table lists CO2 flow ranges and notes voltage adjustment when using mixed gas. Verify the exact gas recommendation for your procedure, position, machine, and base metal.

    Where should I buy Washington Alloy THF-700HT-173?

    For this product, use Arc Weld Store as the primary ordering source: Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

“>view Washington Alloy THF-700HT-173 at Arc Weld Store.

Safety Notes

Hardfacing flux-cored welding produces fumes, gases, arc radiation, sparks, heat, and electrical hazards. Review the SDS, follow your employer’s welding safety practices, use appropriate welding helmet, gloves, protective clothing, respiratory protection when required, and maintain adequate ventilation. The SDS references ANSI Z49.1 and OSHA Hazard Communication requirements. Always follow the manufacturer instructions and the safety program for your site.

Sources Checked

End CTA: Ready to order the verified .045 in. 33 lb spool? Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

“>view this product at Arc Weld Store and confirm current stock, shipping, and fitment before checkout.

  • Hypertherm Powermax45 SYNC 088560 Plasma Cutter Fitment and Consumables Guide

    The Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    “>Hypertherm Powermax45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560 is a 45 amp professional plasma cutting system built for metalworkers who need simplified setup, single-piece cartridge consumables, and reliable hand cutting performance. This guide is focused on ordering accuracy: power input, torch configuration, cut capacity, cartridge selection, air supply, and the fitment checks to complete before purchasing consumables or accessories.

    Key Takeaways

    Product Overview

    The Hypertherm Powermax45 SYNC 088560 is a portable plasma cutting system for fabrication, repair, maintenance, education, HVAC/mechanical work, agricultural repair, and metal shop use. Arc Weld Store lists this configuration with a 20 ft handheld torch and identifies it as a professional plasma cutter for metalworking applications.

    The main advantage of the SYNC platform is simplified consumable management. Instead of stacking separate plasma consumables, Hypertherm’s SmartSYNC platform uses a single-piece cartridge system. Hypertherm also identifies RFID-enabled SmartSYNC torches and cartridges that automatically set amperage and operating mode when correctly paired with the system. That reduces setup mistakes, but it does not remove the need to verify the correct cartridge for the cut type, amperage, torch, and material thickness.

    Upper-middle CTA: Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    “>View this product at Arc Weld Store.

    Best For

    Key Specs

    ProductHypertherm Powermax45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch
    Arc Weld Store SKU088560
    BrandHypertherm
    ConfigurationCSA 200–240 V standard power supply with 75-degree hand torch and 20 ft torch lead
    ProcessesPlasma cutting, gouging, and marking when set up with the correct torch/cartridge configuration
    Input voltage200–240 V, 1-phase, 50/60 Hz
    Input current at 6.9 kW39/32 A at 200–240 V, 1-phase
    Output current9–45 A
    Rated output voltage155 VDC
    Duty cycle at 104°F / 40°C50% at 45 A; 60% at 41 A; 100% at 32 A
    Recommended cut capacity5/8 in. at 20 ipm
    Severance capacity1-1/8 in. at 5 ipm
    Pierce capacity1/2 in. for handheld use or with automatic torch height control
    Typical gouge capacity7.5 lb per hour metal removal; 0.12 in. deep x 0.26 in. wide groove profile
    Gas supplyClean, dry, oil-free air or nitrogen for cutting and gouging; marking gas support depends on setup and cartridge
    Recommended gas inlet flow rate / pressure188 l/min at 5.9 bar; 400 scfh / 6.7 scfm at 90 psi
    Input power cable length10 ft
    Power supply typeInverter – IGBT
    Engine drive requirement12.5 kVA / 10 kW for full 45 A output
    Dimensions with handles17.4 in. D x 6.8 in. W x 14.1 in. H
    Weight with 20 ft torch31 lb
    Warranty listed by Hypertherm literaturePower supply: 6-year; Torch: 1-year
    CPC / voltage divider / serial portNot listed for 088560 standard configuration; verify before ordering for CNC or mechanized integration

    Compatibility / Fitment Notes

    This product is a complete plasma cutting system configuration, but consumables and accessories still require fitment verification. The most important checks are system part number, torch style, input power, cartridge amperage, gas supply, material thickness, and intended cutting process.

    Before You Order

    Accessories / Compatible Products

    Consumables and accessories should be selected by system part number, torch type, process, and material thickness. Do not assume every SmartSYNC cartridge is correct for this 45 amp hand system. Compatibility must be verified against the Powermax45 SYNC documentation before ordering.

    Weld Support Parts Breakdown Reference

    For torch and consumable identification support, review the Hypertherm plasma torch parts breakdown. The page includes Powermax 45 Sync Smart Sync torch listings, including 75-degree hand torch and other torch styles. Use this only as a technical breakdown reference; order from Arc Weld Store after confirming the exact torch, cartridge, and system configuration.

    Common Applications

    Shipping / Returns Notes

    Arc Weld Store lists this product as typically shipping within 1–2 business days, shipping from Corydon, Indiana, with free ground shipping to the lower 48 on qualifying orders. Returns are listed as accepted on unused items in original packaging. For fitment help, Arc Weld Store advises emailing sales@arcweldinc.com with the part number, equipment model, and application before opening an incorrect item.

    FAQ

    What is the Arc Weld Store SKU for this Hypertherm Powermax45 SYNC?

    Arc Weld Store lists the SKU as 088560.

    What torch comes with Hypertherm 088560?

    Hypertherm ordering information identifies 088560 as the CSA 200–240 V standard power supply configuration with a 75-degree hand torch and 20 ft torch lead.

    What input power does the Powermax45 SYNC 088560 require?

    The verified CSA specification is 200–240 V, 1-phase, 50/60 Hz. Confirm your electrical service, plug, receptacle, circuit protection, and local code requirements before ordering.

    How thick can the Powermax45 SYNC cut?

    Hypertherm lists recommended cut capacity at 5/8 in. at 20 ipm, severance capacity at 1-1/8 in. at 5 ipm, and pierce capacity at 1/2 in. for handheld use or with automatic torch height control.

    Does the 088560 package include CNC ports?

    Not confirmed for this standard 088560 configuration. Hypertherm lists separate configurations with CPC port, voltage divider, and serial port options. Verify before buying for mechanized or CNC use.

    Which SmartSYNC cartridge should I buy?

    Choose by process, amperage, torch type, and material thickness. For example, Hypertherm lists cartridge options for 45 A drag cutting, FineCut hand cutting, mechanized/standoff cutting, and gouging. Compatibility: Unknown (Verify) until the exact torch, system, and application are confirmed.

    Can I use shop air with this plasma cutter?

    Yes, when the air supply meets Hypertherm requirements. The system requires clean, dry, oil-free air or nitrogen. Verify compressor capacity, moisture control, filtration, and regulator setup before use.

    Safety Notes

    Sources Checked

    End CTA: Ready to verify power, torch configuration, and consumables? Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    $3,077.61

    In Stock

    View Product
    “>Check current stock at Arc Weld Store.

  • ESAB Rogue ES 151iP PRO Stick Welder: Fitment, Specs, and Ordering Guide

    The Product not found.

    %C2%AE-rogue-es-151ip-pro-stick-welder?utm_source=blog&utm_medium=internal&utm_campaign=esab-rogue-es-151ip-pro-stick-welder-guide”>ESAB Rogue ES 151iP PRO Stick Welder is a portable inverter-based welding power source built for Stick/SMAW, MMA pulse, and Live TIG/GTAW use. This guide focuses on ordering accuracy: input power, output range, electrode size limits, included items, TIG limitations, and the checks to make before you add it to a shop, field service truck, maintenance department, or training lab.

    Key Takeaways

    Product Overview

    The ESAB Rogue ES 151iP PRO is a compact DC Stick/TIG power source for users who need a portable welder with controlled arc characteristics, dual-voltage flexibility, and pulse Stick capability. Arc Weld Store describes the machine as using high-performance power electronics and digital control to provide a precise, consistent arc. It is intended for professional users welding alloyed steel, non-alloyed steel, stainless steel, and cast iron.

    For buyers comparing this machine to a higher-output Stick welder, the main ordering question is electrode size and available input power. The 151iP PRO is the smaller Rogue PRO option in this comparison, with Arc Weld Store noting electrode capacity up to 1/8 in. If your work regularly requires 5/32 in. electrodes, compare the ESAB 0705002022, Rogue ES 201IP PRO Stick Welder

    “>ESAB Rogue ES 201iP PRO Stick Welder before ordering.

    Upper-middle CTA: Product not found.%C2%AE-rogue-es-151ip-pro-stick-welder?utm_source=blog&utm_medium=internal&utm_campaign=esab-rogue-es-151ip-pro-stick-welder-guide”>View this product at Arc Weld Store.

    Best For

    Key Specs

    ProductESAB Rogue ES 151iP PRO Stick Welder
    Arc Weld Store SKU0705002021
    Processes listed by ESAB manualMMA / SMAW / Stick, MMA pulse, TIG / GTAW
    Input voltage230 V ±15%, 1-phase, 50/60 Hz; 120 V ±15%, 1-phase, 50/60 Hz
    Stick setting range20–150 A at 230 V; 20–110 A at 120 V
    Live TIG setting range10–150 A at 230 V; 10–140 A at 120 V
    Stick duty cycle at 230 V150 A / 26 V at 25%; 97 A / 23.9 V at 60%; 75 A / 23 V at 100%
    Stick duty cycle at 120 V110 A / 24.4 V at 25%; 70 A / 22.8 V at 60%; 55 A / 22.2 V at 100%
    Maximum electrode size stated by Arc Weld Store3.2 mm / 1/8 in.
    Dimensions15.8 x 6 x 10.4 in.
    Weight20.28 lb
    Enclosure classIP23S
    Generator noteESAB manual recommends generators with AVR or equivalent/better regulation and 7 kW rated power
    Included equipment per ESAB manualPower source, work clamp leadset, electrode holder leadset, power adapter, shoulder strap, instruction manual, quick start guide
    TIG torchSold separately per Arc Weld Store product description

    Compatibility / Fitment Notes

    This is a welding power source, so the most important fitment checks are electrical supply, electrode size, process setup, cable connections, duty cycle, and accessory selection.

    Before You Order

    Accessories / Compatible Products

    Only order accessories after confirming process, electrode size, PPE needs, and TIG setup details. Do not assume TIG torch consumables fit this machine unless the torch model and consumable family are verified.

    Weld Support Parts Breakdown Reference

    No confirmed Weld Support Parts breakdown page was found for the ESAB Rogue ES 151iP PRO power source during source checking. Because the Arc Weld product page states that the TIG torch is sold separately and does not identify a torch model, TIG torch parts and consumables should be verified by torch model before ordering.

    Common Applications

    Shipping / Returns Notes

    Arc Weld Store lists this product as typically shipping within 1–2 business days, shipping from Corydon, Indiana, with free ground shipping to the lower 48 on qualifying orders. Returns are listed as accepted on unused items in original packaging. For ordering support, Arc Weld Store advises contacting sales@arcweldinc.com with the part number, equipment model, and application before opening an incorrect item.

    FAQ

    What is the Arc Weld Store SKU for the ESAB Rogue ES 151iP PRO?

    Arc Weld Store lists the SKU as 0705002021.

    Can the Rogue ES 151iP PRO run on 120 V and 230 V?

    Yes. The ESAB manual lists the Rogue ES 151iP PRO for 120 V ±15% and 230 V ±15%, single-phase, 50/60 Hz input. Always verify the rating plate and electrical setup before use.

    What size Stick electrodes can this welder run?

    Arc Weld Store states that the Rogue ES 151iP PRO welds electrodes up to 3.2 mm / 1/8 in.

    Does the ESAB Rogue ES 151iP PRO include a TIG torch?

    No. Arc Weld Store states that the machine can TIG weld mild steel or stainless steel through Live TIG functionality, but the TIG torch is sold separately.

    What comes with the Rogue ES 151iP PRO?

    The ESAB manual lists the included equipment as the power source, work clamp leadset, electrode holder leadset, power adapter, shoulder strap, instruction manual, and quick start guide.

    Should I buy the Rogue ES 151iP PRO or the Rogue ES 201iP PRO?

    Choose based on verified output needs, electrode diameter, input power, and duty cycle. Arc Weld Store states that the 151iP PRO welds up to 1/8 in. electrodes, while the 201iP PRO is listed for electrodes up to 5/32 in.

    Safety Notes

    Sources Checked

    End CTA: Ready to verify the model and order? Product not found.%C2%AE-rogue-es-151ip-pro-stick-welder?utm_source=blog&utm_medium=internal&utm_campaign=esab-rogue-es-151ip-pro-stick-welder-guide”>Check current stock at Arc Weld Store.

  • Square Wave 205 TIG Cup Size Selection Guide: Standard Cup, Gas Lens, and Stickout Checks

    For a Lincoln Square Wave 205 TIG setup, cup size controls how well argon shields the tungsten and weld puddle. Use a smaller cup when access is tight, amperage is low, and tungsten stickout is short. Use a larger cup or gas lens setup when the joint needs more coverage, longer tungsten stickout, better visibility, or cleaner stainless/aluminum shielding. Cup size will not fix a gas leak, dirty tungsten, wrong argon flow, cracked cup, worn collet, or contaminated base metal.

    The Square Wave 205 is an AC/DC TIG and Stick machine with AC frequency, AC balance, pulse, and post-flow control. Those machine controls help tune the arc, but TIG cup fitment depends on the installed torch series. Do not order cups by “Square Wave 205” alone. Verify whether the torch is 9/20-style, 17/18/26-style, Caliber 17, Caliber 26, or another torch before buying cups, collets, gas lenses, insulators, or back caps.

    Common Cup Selection Symptoms

    • Tungsten turns black: Cup too small, too much stickout, gas leak, poor post-flow, or bad argon coverage.
    • Stainless turns gray: Shielding coverage is weak, travel is too slow, or cup/gas lens setup is too small for the heat zone.
    • Arc wanders: Tungsten prep, gas turbulence, excessive stickout, or poor work clamp may be involved.
    • Cup blocks visibility: Cup may be too large for joint access; try a smaller cup or gas lens/stubby setup if compatible.
    • Porosity near edges: Gas is not covering the puddle at corners, outside edges, or draft-exposed joints.
    • Good welds on flat joints but poor welds in corners: Cup size, torch angle, and tungsten stickout may need adjustment.

    What TIG Cup Size Does

    The TIG cup directs argon around the tungsten and weld puddle. Smaller cups concentrate gas in tight access areas, but they tolerate less tungsten stickout. Larger cups cover a wider area, but they need the correct torch setup, cup clearance, and flow rate. A gas lens smooths the gas stream and can make larger cups or longer stickout more stable.

    Compatibility Notes for the Square Wave 205

    Lincoln literature lists the Square Wave 205 with TIG features including AC frequency, AC balance, pulse, and post-flow. Lincoln also lists Caliber 17/18/26 torch parts support and optional Caliber 26 and Caliber 9 flexible torch options. That does not mean every torch on a used Square Wave 205 uses the same cup. Torch-series verification is required before ordering.

    For related machine and TIG setup support, see the Lincoln Square Wave 205 overview, why TIG tungsten turns black, unstable TIG arc from poor tungsten prep, gas lens support, and TIG cup support.

    General TIG Cup Size Starting Points

    Cup SizeTypical UseNotes
    #4Very tight access, low amperageShort stickout only; limited gas coverage.
    #5Thin steel, stainless, light aluminumGood compact starting point.
    #6General TIG workCommon all-around cup for short to moderate stickout.
    #7More coverage and visibilityOften better for stainless color control and corners.
    #8Gas lens work, longer stickoutUseful when access or coverage breaks down.
    #10–#12Large coverage / specialty TIGVerify torch setup and gas lens compatibility.

    Cup Size by Job Type

    JobGood Starting CupWhen To Go Larger
    DC steel practice#5 or #6Longer stickout, corners, poor shielding.
    DC stainless#6 or #7Gray weld color or heat tint control issue.
    AC aluminum sheet#5 or #6Edge porosity or wider heat-affected zone.
    Aluminum fillets#6 or #7Puddle is exposed by torch angle or joint shape.
    Inside corners#6 gas lens or #7/#8 gas lensNeed more stickout and smoother gas flow.
    Tight access repair#4 or #5Only if visibility and access allow larger cup.

    Gas Lens vs Standard Cup Setup

    A standard collet body with a #5 or #6 cup is often enough for clean, easy-access joints. A gas lens becomes useful when the arc area needs smoother shielding, longer tungsten stickout, or better puddle visibility. Larger cups work best when paired with a compatible gas lens because the gas stream is more controlled.

    • Use standard cup: Short stickout, normal access, low-to-moderate amperage, basic steel/aluminum practice.
    • Use gas lens: Stainless color control, outside corners, tube work, longer stickout, hard-to-reach fillets.
    • Avoid oversized cups: When the cup blocks access, traps heat, or encourages excessive flow.

    Argon Flow and Cup Size

    Use the torch and procedure guidance as the final reference. Larger cups usually need more argon than small cups, but too much flow can cause turbulence and pull air into the shielding envelope. If increasing cup size makes the weld worse, check for excessive flow, drafts, gas leaks, cup cracks, or a damaged gas lens screen.

    What To Verify Before Ordering Cups

    • Installed torch series: 9/20, 17/18/26, Caliber 17, Caliber 26, or other.
    • Standard collet body or gas lens setup.
    • Tungsten diameter: .040, 1/16, 3/32, or 1/8 in.
    • Cup thread/style for that torch and collet body.
    • Correct insulator/gasket for standard or gas lens cups.
    • Back cap and O-ring condition.
    • Material: steel, stainless, aluminum, or thin sheet.
    • Expected amperage and tungsten stickout.

    Common Wrong-Part Mistakes

    • Buying 17/18/26 cups for a 9/20-style torch.
    • Buying gas lens cups without the matching gas lens collet body.
    • Mixing standard cups, gas lens bodies, and wrong insulators.
    • Using a large cup with excessive argon flow and creating turbulence.
    • Using a small cup with long tungsten stickout.
    • Trying to fix dirty tungsten with cup size when the torch has a gas leak.
    • Assuming every Square Wave 205 has the same torch package.

    Selection Test Procedure

    1. Start with a clean tungsten, correct collet, and a #5 or #6 cup if the torch setup allows it.
    2. Use short stickout and run a bead on clean scrap.
    3. If shielding is stable but visibility is poor, test a larger cup or gas lens setup.
    4. If tungsten turns black, check post-flow, leaks, cup cracks, and argon flow before changing cup size again.
    5. If a larger cup improves weld color and arc stability, coverage was likely part of the issue.
    6. If a larger cup makes the arc unstable, reduce flow and inspect for turbulence or drafts.
    7. Document cup size, tungsten size, gas flow, stickout, material, and Square Wave 205 settings.

    Field Fix vs Proper Fix

    Field fix: Use a clean #5 or #6 cup, short tungsten stickout, correct argon flow, and fresh tungsten. Move up one cup size only if coverage or visibility requires it.

    Proper fix: Match cup, collet, gas lens or standard collet body, insulator, and tungsten diameter to the verified torch series. Then test on clean scrap and record the setup that keeps the tungsten clean and the arc stable.

    Safety Notes

    • Disconnect power before torch service.
    • Let cups and torch parts cool before handling.
    • Do not use cracked ceramic cups or damaged gas lens screens.
    • Use eye and respiratory protection when grinding tungsten.
    • Use ventilation and keep your head out of fumes.
  • Miller Multimatic 220 AC/DC Support Guide: Consumables, Setup, and Common Failure Points

    The Miller Multimatic 220 AC/DC is a multi-process inverter welder supporting MIG, Flux-Cored, DC Stick, DC TIG, and AC TIG welding. Its portability and broad process capability make it common in fabrication shops, mobile repair, motorsports, aluminum work, and home garages.

    This support guide focuses on practical setup verification, consumable identification, wear inspection, and common troubleshooting paths.

    What This Machine Does

    • MIG welding steel and stainless
    • Flux-core welding
    • AC TIG aluminum welding
    • DC TIG steel and stainless welding
    • Stick welding with common SMAW electrodes

    Common Consumables and Wear Components

    ComponentCommon Wear SymptomsWhat To Verify
    MIG contact tipBurnback, erratic arc, wire stutterWire size match
    MIG nozzlePoor shielding gas coverageSpatter buildup
    MIG linerWire feeding issuesCorrect wire diameter
    TIG cupTurbulent shielding gasCracks and heat damage
    TIG colletPoor tungsten gripTungsten size compatibility
    Tungsten electrodeArc instabilityContamination or incorrect grind
    Drive rollsWire slipping or shavingWire type and groove style

    What Usually Wears Out First

    • MIG contact tips from heat and burnback
    • Liners from dirty wire or kinked cables
    • TIG cups from impact damage
    • Drive rolls from incorrect tension settings
    • Ground clamp connections from heat cycling

    Common Symptoms and Likely Causes

    Wire Feeds but Arc Is Unstable

    • Worn contact tip
    • Incorrect polarity
    • Dirty liner
    • Poor work clamp connection
    • Contaminated shielding gas

    TIG Arc Wanders During Aluminum Welding

    • Contaminated tungsten
    • Improper AC balance settings
    • Damaged gas cup
    • Insufficient gas flow
    • Loose collet body

    Excessive MIG Spatter

    • Incorrect voltage/wire speed balance
    • Wrong shielding gas
    • Poor stickout control
    • Worn nozzle or diffuser

    Compatibility Notes

    The Multimatic 220 AC/DC supports multiple torch and consumable configurations depending on process setup.

    • MIG gun compatibility depends on the connector configuration and trigger wiring
    • TIG torch compatibility depends on amperage rating and connector style
    • Spool gun compatibility should be verified against Miller-approved models
    • Drive rolls must match wire type and diameter
    • Tungsten selection depends on AC or DC process use

    Unknown (Verify) for non-OEM gun and torch compatibility unless manufacturer documentation confirms fitment.

    What To Verify Before Ordering Parts

    • Machine serial number
    • MIG gun model
    • TIG torch series
    • Wire diameter
    • Connector type
    • Consumable family
    • Input voltage setup
    • Shielding gas type

    Common Wrong-Part Mistakes

    • Using the wrong liner diameter
    • Installing flux-core polarity incorrectly
    • Mixing diffuser and nozzle series
    • Using pure tungsten for modern inverter DC TIG
    • Overtightening contact tips

    Inspection Steps

    • Inspect drive rolls for wire shaving
    • Check liner resistance by hand-feeding wire
    • Inspect contact tip bore for oval wear
    • Check gas hoses for leaks
    • Inspect Dinse-style connections for overheating
    • Verify cooling airflow through side vents

    Field Fix vs Proper Fix

    ProblemTemporary Field FixProper Repair
    Birdnested wireTrim and reload wireReplace liner and inspect drive rolls
    Gas leakTighten fittingsReplace damaged hose or regulator seal
    Arc instabilityRegrind tungstenReplace contaminated consumables

    Related Failure Paths

    • Dirty wire causes liner wear and feed instability
    • Poor grounding overheats cables and connectors
    • Incorrect gas flow contributes to porosity and tungsten contamination
    • Excessive drive tension damages wire and liner assemblies

    Safety Notes

    • Disconnect input power before servicing internal components
    • Allow torch consumables to cool before handling
    • Use approved respiratory protection when welding coated metals
    • Inspect cables regularly for insulation damage

    Related Parts Breakdown

    No confirmed WSP breakdown found.

    Sources Checked

    • Miller Multimatic 220 AC/DC product documentation
    • Miller setup and process references
    • Confirmed Weld Support Parts blog references
  • Welding Helmet Replacement Parts: Lens, Headgear, Shell, Battery, and ADF Fitment Guide

    If a welding helmet is hard to see through, will not stay up, flickers, fails to darken, or feels loose on the head, the repair usually starts with replacement parts—not a new helmet. The most common welding helmet replacement parts are outside cover lenses, inside cover lenses, sweatbands, headgear assemblies, batteries, ADF cartridges, lens seals, shell parts, magnifying lenses, hard hat adapters, and PAPR filters. The part must match the exact helmet series, lens size, cartridge style, and shell design before ordering.

    Do not order by appearance alone. Two helmets can look similar and use different inside lenses, ADF cartridges, gasket profiles, or headgear hardware. Verify the brand, helmet series, model number, lens dimensions, ADF part number, battery type, and whether the hood is passive, auto-darkening, flip-front, grind-shield, hard-hat compatible, or PAPR-equipped.

    Common Symptoms

    SymptomLikely PartWhat To Check First
    Cloudy view or hazeOutside cover lens / inside cover lensScratches, smoke film, spatter pits, heat warping
    Helmet will not stay upHeadgear assemblyStripped knobs, cracked pivots, worn ratchet band
    ADF flickers or goes lightBattery, sensors, ADF cartridgeBattery condition, sensor blockage, mode setting
    Light leaks around lensLens seal / gasket / ADF holderMissing seal, warped holder, wrong cover lens thickness
    Sweatband torn or soakedSweatbandContamination, odor, slipping headgear
    Helmet shell crackedReplacement shellImpact damage, heat damage, broken lens frame
    Need closer puddle viewCheater / magnifying lensCorrect diopter and compatible lens slot
    PAPR airflow warningFilter, pre-filter, battery, breathing tubeLoaded filters, low battery, blocked hose, poor seal

    What This Part Does

    The outside cover lens protects the ADF or passive filter from spatter, sparks, grinding dust, and scratches. It is the part most shops replace first because it directly affects puddle visibility. The inside cover lens protects the rear side of the filter from dust, fingerprints, and fumes trapped inside the hood.

    The ADF cartridge is the auto-darkening filter. If the helmet powers on but does not darken reliably after batteries and sensors are checked, the cartridge may be the failed component. The headgear assembly controls fit, balance, lift tension, and working position. A worn headgear can make a good helmet feel unsafe or unusable.

    Sweatbands are low-cost wear items. They do not just improve comfort; they help keep the helmet stable on the head. Lens seals, gaskets, holders, and front frames keep the filter seated correctly and help prevent light leaks around the cartridge.

    What Wears Out First

    • Outside cover lens: usually the first part to replace on MIG, flux-core, stick, and grinding-heavy work.
    • Sweatband: absorbs sweat and shop contamination; replace when it slips, smells, or loses shape.
    • Headgear: fails at ratchets, pivots, tension knobs, and adjustment slots.
    • Batteries: weak batteries cause delayed darkening, flicker, or failure to power the ADF.
    • Lens seals and holders: wear after repeated lens changes or heat exposure.
    • PAPR filters and pre-filters: load with fume and dust; replacement interval depends on exposure and manufacturer guidance.

    Compatibility Notes

    Helmet replacement parts are not universal unless the manufacturer states that they are. Lincoln VIKING 2450 and VIKING 3350 helmets both use KP2898-1 outside cover lenses and KP2930-1 sweatbands in the Lincoln parts data, but their inside cover lenses and ADF cartridges differ. The VIKING 2450 listing uses KP2931-1 inside cover lenses and KP2932-4 ADF cartridge, while the VIKING 3350 listing uses KP3044-1 inside cover lenses and KP3045-4 ADF cartridge.

    The VIKING 3250D FGS uses larger front protection parts than standard VIKING shells, including KP3700-1 outside cover lenses, KP3701-1 inside cover lenses, KP3702-1 grind shield clear lens, KP3703-3 ADF cartridge, KP3704-1 replacement shell, and KP3706-1 headgear assembly.

    Miller Performance and Classic helmet families use their own shell, lens cover, gasket, lens assembly, headgear, and battery tray part numbers. 3M Speedglas helmets also have series-specific outside plates, inside plates, filters, batteries, headbands, and hard-hat adapters. Dynaflux lists replacement cover lenses and auto-darkening replacement lenses by helmet family, including Miller, Jackson, and Speedglas-compatible listings. Treat every brand and series as its own parts system.

    What To Verify Before Ordering

    • Helmet brand and exact series
    • Helmet model number or product number
    • ADF cartridge part number
    • Inside and outside cover lens dimensions
    • Battery type, if replaceable
    • Headgear style and pivot hardware
    • Shell version or graphic series, if shell replacement is needed
    • Hard hat adapter requirement
    • PAPR model, blower, filter, pre-filter, hose, and face seal style
    • Whether the helmet is passive, auto-darkening, flip-front, grind-shield, or PAPR

    Common Wrong-Part Mistakes

    • Ordering a standard VIKING lens for an FGS grind-shield helmet.
    • Ordering an outside cover lens when the damaged part is the inside cover lens.
    • Replacing the ADF cartridge before checking batteries, sensors, and cover lens condition.
    • Assuming all 4-1/2 x 5-1/4 lenses fit every shell.
    • Buying a headgear assembly without confirming the pivot hardware.
    • Using a non-rated clear plastic sheet instead of a manufacturer lens cover.
    • Mixing PAPR parts from different blower or helmet systems.

    Visual Wear Indicators

    Replace the outside lens when scratches, spatter pits, fogging, distortion, or heat waves make it harder to see the puddle. Replace the inside lens when it is cloudy, cracked, coated with fume residue, or no longer locks flat in the filter frame. Replace headgear if the helmet drops unexpectedly, feels unbalanced, or cannot hold adjustment.

    Inspect the shell for cracks around the lens frame, pivot mounts, and top edge. A cracked shell can allow light entry or fail to support the filter. On PAPR helmets, inspect the face seal, breathing tube, filter cover, pre-filter, and battery connection before assuming the blower is bad.

    Inspection Steps

    1. Clean the outside lens with a soft cloth and mild cleaner.
    2. Remove the outside cover lens and inspect it under shop light.
    3. Inspect the inside cover lens and ADF window.
    4. Check ADF sensors for smoke film, tape, stickers, or spatter.
    5. Replace batteries if the helmet uses serviceable batteries.
    6. Cycle weld, grind, shade, delay, and sensitivity settings.
    7. Inspect the headgear pivots, knobs, ratchet band, and sweatband.
    8. Look for light gaps around the ADF holder and lens seal.
    9. For PAPR systems, check airflow alarms, filter loading, hose connection, and face seal.

    Test Procedures

    After replacing helmet parts, perform a safe function check before welding. Confirm the ADF powers up, shade and delay controls respond, grind mode turns off before welding, and the helmet darkens consistently from multiple arc angles. Do not weld with a cracked lens, missing cover plate, missing gasket, damaged shell, or uncertain ADF response.

    For PAPR helmets, follow the manufacturer airflow check procedure. If the low-flow alarm triggers after replacing the pre-filter or particle filter, inspect the breathing tube, battery charge, filter seating, and face seal. Do not treat a loaded filter as a comfort issue; it is a respiratory protection issue.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Scratched outside lensClean lens to finish a non-critical taskReplace with correct outside cover lens
    Loose helmetTighten knobsReplace worn headgear assembly
    Dirty sweatbandWipe downReplace sweatband
    Weak ADF batteryStop and replace batteryUse specified battery and confirm operation
    Light leakDo not weldReplace seal, holder, lens, or shell as needed
    PAPR low flowLeave weld areaReplace filters or repair system per manufacturer procedure

    Related Failure Paths

    • Poor puddle visibility → scratched cover lens → wrong shade setting → bad bead placement.
    • Helmet slipping → worn headgear → neck strain → inconsistent arc position.
    • ADF flicker → weak battery or blocked sensors → arc flash risk.
    • Missing lens seal → light leak → eye fatigue and unsafe viewing.
    • Loaded PAPR filter → low airflow alarm → reduced respiratory protection.

    Replacement Notes

    For Lincoln VIKING 2450 and 3350 families, start by confirming whether the part needed is KP2898-1 outside cover lens, KP2930-1 sweatband, the correct inside lens, or the correct ADF cartridge for that series. For Miller helmets, use the correct Miller series breakdown before ordering shells, lens covers, gaskets, headgear, or ClearLight lens assemblies. For Speedglas, confirm the exact helmet family because 9002, 9100, G5, and PAPR systems do not share every part.

    Unknown (Verify): cross-brand ADF cartridge swaps, non-OEM lens thickness, imported clone shell fitment, and hard-hat adapter fitment unless confirmed by the manufacturer or a verified parts breakdown.

    Safety Notes

    • Do not weld with a cracked, missing, or improvised lens cover.
    • Do not bypass an ADF problem by increasing shade only; confirm the cartridge darkens correctly.
    • Turn grind mode off before welding.
    • Use only helmet parts rated for welding protection.
    • For PAPR equipment, follow employer respiratory protection rules and manufacturer service intervals.
    • If eye irritation, flash symptoms, or repeated ADF failure occurs, stop welding and inspect the helmet before reuse.

    Sources Checked

    • Lincoln Electric 2024 Expendable Parts Guide
    • Lincoln Electric Accessories 2024 Product Catalogue
    • Miller Accessories and Consumables Catalog data
    • 3M Speedglas welding helmet parts references
    • Dynaflux replacement lenses, faceshields, and headgear catalogue
    • Weld Support Parts helmet breakdown pages
    • Weld Support Parts Blog helmet visibility and helmet selection support pages
  • 3M Speedglas G5-02 Welding Helmet Support Guide: Fitment, Lens Protection, and Ordering Checks

    The 3M Speedglas G5-02, Auto Darkening Welding Helmet, Pack of (1)

    “>3M Speedglas G5-02 Auto Darkening Welding Helmet is a professional welding helmet built around the Speedglas G5-02 platform. This support article is intended to help buyers confirm the correct helmet, understand the verified specs, and avoid ordering the wrong lens protection or replacement accessory.

    Key Takeaways

    Product Overview

    The 3M Speedglas G5-02 is an auto-darkening welding helmet listed by Arc Weld Store under SKU 08-0100-50IC. The product page identifies the brand as 3M and describes the helmet with Natural Color Technology, adjustable arc detection sensitivity, a delay function, and Bluetooth connectivity through the 3M Connected Equipment App.

    For commercial buyers, the important ordering point is simple: this is a complete G5-02 helmet listing, not a cover plate, not a replacement ADF, and not a generic welding hood. Confirm that your shop needs the helmet assembly before purchasing.

    View this product at Arc Weld Store: 3M Speedglas G5-02, Auto Darkening Welding Helmet, Pack of (1)

    “>3M Speedglas G5-02 Auto Darkening Welding Helmet

    Best For

    Key Specs

    Product3M Speedglas G5-02 Auto Darkening Welding Helmet, Pack of 1
    Brand3M
    Arc Weld SKU08-0100-50IC
    Helmet SeriesSpeedglas G5-02
    Auto-DarkeningYes
    Dark Shade Range8 to 12
    Natural Color TechnologyListed by Arc Weld Store
    Adjustable Arc Detection SensitivityListed by Arc Weld Store
    Delay FunctionListed by Arc Weld Store
    Bluetooth ConnectivityListed by Arc Weld Store
    Included ItemsUnknown (Verify)
    CertificationsUnknown (Verify)
    Viewing AreaUnknown (Verify)
    Battery TypeUnknown (Verify)
    WeightUnknown (Verify)

    Compatibility / Fitment Notes

    The product page identifies this helmet as the 3M Speedglas G5-02. For replacement parts, do not assume that other Speedglas series accessories will fit. G5-01, G5-03, 9100, and 9002NC components may use different filter, cover lens, or shell designs. Confirm the helmet series and part number before ordering replacement plates, ADF components, headgear, or accessories.

    3M lists a G5-02 curved auto-darkening filter under alternative ID 08-0000-50iC, but the Arc Weld product URL supplied for this article is the helmet listing with SKU 08-0100-50IC. If you need only the filter, verify the exact replacement filter part number before purchasing.

    Before You Order

    Accessories / Compatible Products

    Technically relevant accessories should be selected by confirmed helmet series and part number. The most direct Arc Weld accessory found for this product family is the G5-02 outside protection plate.

    Related ItemUse CaseCompatibility Note
    3M Speedglas G5-02 Outside Protection Plate 08-0200-52, Scratch Resistant, 5 ea/Case “>3M Speedglas G5-02 Outside Protection Plate 08-0200-52, Scratch Resistant, 5 ea/CaseReplacement outside protection plates for the G5-02 helmet family.Listed by Arc Weld as designed specifically for the 3M Speedglas G5-02 welding helmet.
    3M Speedglas G5-03 Pro Welding Helmet 10-0100-30TW with G5TW ADF with Grind Mode, TAP, Natural Color, Tack Weld Mode “>3M Speedglas G5-03 Pro Welding Helmet 10-0100-30TWCompare another Speedglas helmet option.Not a replacement part for the G5-02. Compatibility: Unknown (Verify).
    Inside and Outside Cover Lens CollectionFind cover lenses and protection plates.Filter by exact helmet model and part number before ordering.
    Welding Helmet CollectionCompare welding helmet options.Compare by process, shade range, viewing area, and safety requirements.

    Common Applications

    Shipping / Returns Notes

    Arc Weld Store lists this product as typically shipping within 1–2 business days, shipping from Corydon, Indiana, with free ground shipping to the lower 48 on qualifying orders. Returns are listed as accepted on unused items in original packaging. Always check the live product page before ordering because shipping, pricing, and availability can change.

    FAQ

    Is this a complete welding helmet or a replacement lens?

    The Arc Weld listing is for the 3M Speedglas G5-02 Auto Darkening Welding Helmet, Pack of 1. Replacement lens and cover plate requirements should be verified separately by part number.

    What is the Arc Weld SKU?

    The Arc Weld SKU shown on the product page is 08-0100-50IC.

    What shade range is listed?

    The Arc Weld product page lists a variable dark shade range of 8 to 12.

    Which outside protection plate was found for the G5-02?

    Arc Weld lists the 3M Speedglas G5-02 Outside Protection Plate 08-0200-52, Scratch Resistant, 5 ea/Case as designed specifically for the 3M Speedglas G5-02 welding helmet.

    Can G5-03 parts be used on the G5-02?

    Compatibility: Unknown (Verify). Do not substitute G5-03 parts for G5-02 parts unless the manufacturer or Arc Weld confirms the fitment.

    Safety Notes

    Welding helmets and filter lenses must be selected for the welding process, amperage, radiant energy exposure, impact hazards, and workplace safety requirements. OSHA welding guidance references filter lens requirements and appropriate eye and face protection. Confirm jobsite PPE requirements before use, and wear approved safety glasses or goggles under the helmet when required by your safety program.

    Sources Checked

    End CTA: 3M Speedglas G5-02, Auto Darkening Welding Helmet, Pack of (1)

    3M Speedglas G5-02, Auto Darkening Welding Helmet, Pack of (1)

    $1,152.82

    In Stock

    View Product
    “>Check current stock at Arc Weld Store

  • Do I Need a Respirator If I Already Have a Fume Extractor?

    A welding fume extractor reduces airborne fume at the source, but it does not automatically replace a respirator. The right answer depends on whether the extractor is capturing the plume before it reaches the breathing zone, what material is being welded, how long the weld lasts, whether coatings are present, and whether exposure levels are below applicable limits.

    For many shop and field welders, the practical answer is: use the fume extractor first, then add respiratory protection when extraction is not enough, not practical, poorly positioned, or not verified. If the extractor is not pulling smoke well, start with the WSP guide on why a welding fume extractor is not pulling smoke. If the respirator is already in use but fumes are still noticeable, check respirator seal leaks and fume smell.

    Key Takeaways

    • A fume extractor is an engineering control. A respirator is personal protective equipment. They solve different parts of the exposure problem.
    • Extraction reduces the amount of fume in the breathing zone, but capture depends on hood position, airflow, filter loading, weld position, drafts, and plume direction.
    • A respirator may still be needed for stainless, galvanized, hardfacing, flux-core, coated material, enclosed areas, long weld shifts, poor extraction capture, or unknown exposure levels.
    • P100 filters are commonly used for welding fume particulate, but gases, vapors, coatings, and confined-space hazards require separate verification.
    • For workplace use, respirator selection must follow the OSHA respiratory protection program, including medical evaluation, fit testing, training, and written procedures when required.

    Problem / Context

    The common mistake is treating a fume extractor like a guarantee. A portable arm can be rated correctly and still fail at the weld if the hood is too far away, positioned behind the plume, blocked by the workpiece, overloaded with dust, or competing with cross-drafts. In that situation, the welder may still inhale fume even though the machine is running.

    The opposite mistake is relying only on a respirator when local capture could reduce the fume load for everyone nearby. A respirator protects the wearer only when it seals correctly and uses the correct filter. A fume extractor helps reduce airborne contamination at the source. The strongest setup often uses both: capture at the arc plus properly selected respiratory PPE when exposure conditions require it.

    Root Causes: Why a Fume Extractor May Not Be Enough

    • The capture hood is too far from the arc.
    • The hood is not positioned so the plume moves away from the breathing zone.
    • The extractor filter is loaded, clogged, damaged, or overdue for replacement.
    • The duct, hose, nozzle, or prefilter is restricted.
    • Cross-drafts from fans, doors, or shop airflow pull fumes past the welder’s face.
    • The weld position puts the welder’s head directly above the plume.
    • The process produces high fume volume, such as some flux-core, stick, stainless, galvanized, or hardfacing work.
    • The base metal has paint, oil, zinc coating, primer, plating, solvent residue, or unknown contamination.
    • The job occurs in a corner, tank, trailer, pit, booth, or enclosed structure where plume behavior changes.

    Solution: Use This Decision Path

    Start by asking whether the fume extractor is actually controlling exposure at the breathing zone. Visible smoke moving away from the welder is a good sign, but it is not the same as exposure verification. When the material, process, or exposure level is uncertain, treat the answer as Unknown (Verify) until the shop safety plan, SDS data, and exposure assessment confirm the control method.

    • Use a fume extractor whenever indoor welding or high-fume work makes local capture practical.
    • Add a respirator when extraction is not verified to keep exposure below applicable limits.
    • Add a respirator when welding stainless, galvanized, coated, hardfacing, or high-fume flux-core work unless the hazard assessment supports another control plan.
    • Use a PAPR or other approved system when a tight-fitting half mask does not seal, causes repeated removal, or does not meet the required protection level.
    • Do not use a fume extractor or air-purifying respirator as a substitute for confined-space evaluation, oxygen monitoring, or required supplied-air protection.

    Specs / Verification Notes

    ControlWhat It DoesWhat It Does Not ProveVerification Needed
    Portable fume extractorCaptures fume near the arc when positioned and maintained correctlyDoes not prove exposure is below limitsHood position, airflow, filter condition, capture direction, and exposure assessment
    Fume extraction gunCaptures near the weld while weldingDoes not eliminate all plume exposure in every positionGun setup, nozzle condition, weld access, and airflow balance
    Downdraft tablePulls fumes downward through the work surfaceDoes not protect well when the plume rises around large parts or poor work positioningPart size, table airflow, work height, and plume path
    P100 half-mask respiratorFilters particulate when properly selected and sealedDoes not automatically cover gases, vapors, oxygen deficiency, or unknown coatingsFilter class, fit test, seal check, cartridge choice, and change schedule
    Welding PAPRProvides filtered powered airflow through an approved systemDoes not automatically solve oxygen-deficient or IDLH conditionsFilter setup, airflow check, battery condition, assigned protection factor, and program approval

    Product Section

    Check Arc Weld Store first for Miller respirators, replacement filters, and fume-control equipment when available. Amazon fallback boxes are included only for verified ASINs.

    No products found.

    The Miller LPR-100 is a practical low-profile P100 respirator option when a welder already uses local fume extraction but still needs under-hood respiratory protection for particulate welding fume. Confirm size, filter version, fit-test requirements, and workplace approval before use.

    No products found.

    The 3M Adflo and Versaflo welding PAPR kit is an escalation option when a half-mask is not enough because of fit issues, comfort problems, long weld shifts, facial hair conflicts, or a higher respiratory protection need. Confirm the exact configuration, filter type, assigned protection factor, airflow check procedure, and welding helmet compatibility before use.

    Comparison Table: Extractor Only vs Extractor Plus Respirator

    Job ConditionExtractor Only May Be Enough?Respirator Should Be Considered?
    Short mild steel welds in open air with verified capturePossiblyUnknown (Verify)
    Flux-core welding indoorsNot assumedYes, especially if visible fume remains near the breathing zone
    Stainless weldingNot assumedYes, based on exposure assessment and applicable limits
    Galvanized or plated steelNot assumedYes, plus coating removal and strong local capture
    Painted, oily, primed, or solvent-contaminated materialNoStop and identify the hazard first
    Confined or enclosed spaceNoRequires confined-space evaluation and approved respiratory plan
    Extractor smoke capture is visibly poorNoYes, but fix extraction instead of relying only on PPE
    Long production welding shiftNot assumedOften yes, especially if monitoring has not verified exposure control

    How to Check Whether the Extractor Is Doing Its Job

    • Place the capture hood as close to the arc as the work allows without disturbing the weld.
    • Position the hood so the plume moves away from the welder’s breathing zone.
    • Watch the plume during actual welding, not just while the extractor is idling.
    • Check for cross-drafts from fans, open doors, air conditioning, or nearby equipment.
    • Inspect the hose, nozzle, prefilter, main filter, spark arrestor, and seals for restriction or damage.
    • Confirm the extractor is rated and configured for welding fume, not just general dust collection.
    • Use exposure monitoring when the process, material, or ventilation effectiveness is uncertain.

    Related Failure Paths

    Safety Notes

    OSHA guidance says local exhaust ventilation can remove fumes and gases from the welder’s breathing zone, but respiratory protection may be required if work practices and ventilation do not reduce exposures to safe levels. AWS guidance also emphasizes keeping the head out of the plume, using ventilation or exhaust controls, and wearing an appropriate NIOSH-approved respirator when ventilation is not adequate or practical.

    • Do not weld over coatings, paint, solvent residue, oil, plating, or unknown contamination without identifying the hazard.
    • Do not assume outdoor welding is automatically safe; plume direction and body position still matter.
    • Do not use room fans as a substitute for source capture; they may push fumes through the breathing zone.
    • Do not use a tight-fitting respirator over facial hair that crosses the sealing surface.
    • Do not rely on odor to prove protection. Some hazardous exposures do not provide a reliable warning smell.
    • Do not use an air-purifying respirator in oxygen-deficient or IDLH conditions unless it is specifically approved for that use.

    FAQ

    Does a fume extractor replace a respirator?

    No, not automatically. A fume extractor reduces airborne fume at the source, while a respirator protects the wearer when correctly selected and sealed. A respirator may still be required if extraction does not keep exposure below safe limits.

    How do I know if my fume extractor is enough?

    Visible capture is helpful, but the stronger answer comes from correct hood placement, airflow verification, filter maintenance, SDS review, and exposure assessment. If the answer is uncertain, label it Unknown (Verify) and do not assume the extractor alone is enough.

    Should I wear a P100 respirator while using a fume extractor?

    Often yes for high-fume or higher-risk work such as flux-core, stainless, galvanized, hardfacing, coated material, enclosed work, or long production welding. P100 addresses particulate fume when properly selected and sealed, but it does not automatically cover gases or vapors.

    Why can I still smell fumes with the extractor running?

    The hood may be too far away, the plume may be passing through the breathing zone before capture, the filter may be loaded, or cross-drafts may be moving fumes toward the welder. A respirator smell complaint can also point to a poor face seal or the wrong filter for the hazard.

    Is a PAPR better than a half-mask if I already have extraction?

    A PAPR can be better when half-mask fit, facial hair, heat, comfort, long weld shifts, or exposure level makes a tight-fitting respirator the wrong tool. It still must be selected for the actual hazard and used under the workplace respiratory protection program.

    Next Step

    Use the fume extractor as the first control, then verify whether it keeps fumes out of the breathing zone during real welding. If capture is uncertain, fumes remain visible near the face, the material is stainless or galvanized, the work is enclosed, or the shift is long, add properly selected respiratory protection instead of assuming extraction alone is enough.

    Sources Checked

    • OSHA, Controlling Hazardous Fume and Gases during Welding: https://www.osha.gov/sites/default/files/publications/OSHA_FS-3647_WELDING.pdf
    • OSHA, 29 CFR 1910.134 Respiratory Protection: https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910.134
    • OSHA, 1926.353 Ventilation and protection in welding, cutting, and heating: https://www.osha.gov/laws-regs/regulations/standardnumber/1926/1926.353
    • AWS Safety and Health Fact Sheet No. 38, Respiratory Protection Basics for Welding Operations: https://aws-p-001-delivery.sitecorecontenthub.cloud/api/public/content/c09ba1fbf05a4badb79b2a9c2b47df9d
    • AWS Safety and Health Fact Sheet No. 36, Ventilation for Welding and Cutting: https://aws-p-001-delivery.sitecorecontenthub.cloud/api/public/content/Fact-Sheet-No.36
    • AWS Safety and Health Fact Sheet No. 1, Fumes and Gases: https://aws-p-001-delivery.sitecorecontenthub.cloud/api/public/content/Fact-Sheet-No.1
    • NIOSH Engineering Controls Database, Welding Operations: Local Exhaust Ventilation Systems: https://www.cdc.gov/niosh/engcontrols/ecd/detail44.html
    • 3M Adflo Powered Air Purifying Respirator System: https://www.3m.com/3M/en_US/speedglas-welding-helmets-us/adflo/
    • Arc Weld Store, Air Cleaning Equipment and Respirators: https://www.arcweld.store/collections/air-cleaning-equipment-and-respirators
    • WSP, Welding Fume Extractor Not Pulling Smoke: https://blog.weldsupportparts.com/2026/05/05/welding-fume-extractor-not-pulling-smoke-causes-and-fixes/

  • More posts

    Watch with Prime Video