Search results for: “porosity in welds”

  • TIG Filler Rod Contamination Problems: Porosity, Dirty Welds, Black Tungsten, and Wrong Alloy Checks

    If TIG filler rod is contaminated, the weld can show porosity, black specks, gray bead color, soot, oxide islands, unstable arc behavior, or cracking even when the tungsten and argon flow look correct. Filler rod contamination comes from oil, moisture, fingerprints, shop dust, aluminum oxide, rust, mill scale, grinding grit, marker, solvent residue, mixed-alloy storage, or using the wrong filler metal for the base material.

    The fast fix is to stop welding, switch to a known-clean filler rod from sealed storage, clean the base metal to bright material, regrind contaminated tungsten, verify shielding gas coverage, and run a controlled test bead. Do not keep feeding a dirty rod into the puddle and adjust amperage around it. Filler contamination goes directly into the weld pool. For related TIG contamination checks, see why your TIG weld is getting contaminated, TIG porosity troubleshooting, and TIG shielding gas coverage troubleshooting.

    Common Symptoms

    • Small pinholes or bubbles appear in the TIG bead.
    • Weld puddle pops, spits, or forms black flecks when filler is added.
    • Weld looks clean during autogenous fusion but turns dirty when filler is introduced.
    • Tungsten turns black shortly after filler touches the puddle.
    • Aluminum welds show black soot, gray islands, or peppery porosity.
    • Stainless welds lose color control or show sugar/oxidation at the edge of coverage.
    • Carbon steel welds show porosity even after gas flow and cup size are checked.
    • Cracking appears after using filler from an unknown tube or mixed rack.
    • Rod end smokes, flakes, rusts, or leaves residue before it melts into the puddle.

    Likely Causes

    CauseWhat It DoesQuick Check
    Oil or fingerprints on rodIntroduces hydrocarbons into the weld poolWipe rod with clean solvent-compatible cloth
    Moisture on fillerCan contribute hydrogen and porosityCheck storage, condensation, open tubes, and wet benches
    Rust or oxideCreates inclusions, poor wetting, and porosityInspect rod surface under good light
    Aluminum oxide on fillerResists melting cleanly and contaminates puddleClean rod and base metal before welding
    Grinding dust or shop debrisAdds foreign material directly to puddleCheck rods stored near grinders or plasma tables
    Wrong filler alloyCan cause cracking, wrong color, corrosion issues, or strength mismatchVerify AWS class and base metal
    Mixed rods in one tubeCreates unknown chemistrySeparate by marked package and rod stamp where available
    Dirty gloves handling clean rodTransfers oil, cutting fluid, or carbon dustUse clean TIG gloves for filler handling

    Fast Diagnosis Sequence

    1. Run a short autogenous bead on clean base metal with no filler.
    2. If the autogenous bead is clean, add filler from the suspect rod.
    3. If contamination appears only when filler is added, remove that filler from service.
    4. Switch to known-clean filler from original packaging or controlled storage.
    5. Regrind tungsten if the contaminated puddle touched or vapor-coated the electrode.
    6. Clean the base metal and filler rod with the correct method for the material.
    7. Verify argon flow at the cup and check for drafts, leaks, cracked cups, or damaged gas lens.
    8. Confirm filler alloy matches the base metal and service requirement.
    9. Run a second test bead with clean filler and compare bead appearance.
    10. If contamination remains, troubleshoot shielding gas, base metal, tungsten, and torch parts next.

    Inspection Steps

    • Rod surface: Look for rust, white aluminum oxide, dark fingerprints, oil film, dust, grinding grit, paint marker, tape adhesive, or unknown residue.
    • Rod ends: Cut off ends that were dropped, dragged across a bench, touched to the floor, or stored open in a dirty tube.
    • Packaging: Check whether rods are still in labeled packaging or mixed loose in an unmarked container.
    • Storage: Open tubes, damp cabinets, welding carts, and benches near grinders are common contamination sources.
    • Gloves: Dirty gloves can transfer oil, carbon dust, anti-spatter, coolant, or aluminum oxide to otherwise clean filler.
    • Base metal match: Verify filler class before assuming the problem is dirt. Wrong filler selection can look like contamination or cracking.
    • Shielding gas: Filler contamination and poor shielding can look similar. Confirm gas coverage before scrapping a full tube of rod.
    • Tungsten: Contaminated filler can dirty the tungsten. A bad tungsten can then contaminate the next test bead.

    Test Procedures

    • No-filler test: Weld a clean fusion bead without filler. If it stays clean, the base metal, tungsten, and shielding may be acceptable.
    • Known-good filler test: Repeat with fresh filler from controlled storage. If the bead improves, the original rod was suspect.
    • Wipe test: Pull the rod through a clean white cloth with approved cleaner. Dark residue means the rod is carrying oil, oxide, or shop dust.
    • Cut-end test: Clip 1 to 2 inches off the filler end and retest. Rod ends often collect the most handling contamination.
    • Alloy verification test: Compare package label, AWS classification, heat/lot marking, and procedure requirement. Unknown filler should not be used on critical work.
    • Shielding comparison test: Hold the same clean filler under proper cup coverage and then outside gas coverage. If the hot rod end oxidizes outside the gas, technique is contributing.

    Cleaning Filler Rod Correctly

    Clean filler rod only with a method compatible with the material and procedure. For many steel and stainless TIG applications, a clean lint-free wipe and approved solvent may be enough to remove oil. For aluminum, remove oil first, then address oxide with a dedicated stainless brush or approved mechanical cleaning method. Do not use a carbon steel brush on aluminum or stainless filler.

    • Use clean gloves after cleaning the rod.
    • Keep cleaned rods off dirty benches and welding tables.
    • Do not dip cleaned rods into solvent containers that already contain shop grit.
    • Do not use oily rags, shop towels with cutting fluid, or compressed air from oily lines.
    • Store cleaned rods back in a labeled dry tube or sealed container.

    Material-Specific Contamination Problems

    MaterialCommon Filler ContaminationTypical Weld Symptom
    AluminumOxide, oil, moisture, dirty wire surfaceBlack soot, porosity, poor wetting
    Stainless steelCarbon steel dust, oil, wrong alloy mix-upRust staining, poor color, corrosion risk, cracking
    Carbon steelRust, oil, mill scale dust, paint markerPorosity, dirty puddle, inclusions
    Nickel alloysWrong filler, sulfur/chloride contamination, shop dustCracking, corrosion-performance loss, dirty puddle
    TitaniumOil, oxygen exposure, dirty filler handlingColor shift, embrittlement risk, unacceptable oxidation

    Root Cause Analysis

    TIG filler rod melts directly into the weld puddle. Any contamination on the rod becomes part of the molten metal or decomposes in the arc. Oil, grease, paint, and moisture can form gas and porosity. Oxides and grinding dust can become inclusions. Wrong alloy selection can cause cracking, color mismatch, reduced corrosion resistance, or mechanical-property problems that look like a welding technique failure.

    Filler contamination is often missed because the welder checks the gas bottle, tungsten, cup, and base metal first. A useful separation test is to weld without filler, then add filler from a known-good tube. If the weld only becomes dirty when filler is introduced, the filler rod, filler handling, or filler selection is part of the failure path.

    Compatibility Notes

    Do not order TIG filler rod by diameter alone. Verify AWS classification, base metal, service temperature, corrosion requirement, strength requirement, post-weld finishing, anodizing expectations, and procedure requirements. Aluminum examples include ER4043, ER5356, ER1100, ER5556, ER2319, ER5554, and ER5654, but the correct selection depends on base alloy and service. Stainless, nickel, copper, magnesium, and titanium filler selection must be verified by material and procedure.

    Also verify packaging and storage needs. Solid MIG wires and TIG rods should be protected from humid environments and contamination with moisture, dirt, and oil. Rods left loose on a bench, mixed into open tubes, or stored near grinders should be treated as Unknown (Verify) for critical welds.

    What To Verify Before Ordering

    • Base metal alloy or material grade.
    • Required AWS/ASME filler classification.
    • Rod diameter and length.
    • Weld process: TIG, oxyfuel, MIG, or multiprocess use.
    • Shielding gas and purge requirements.
    • Service environment: structural, food service, marine, high temperature, corrosion, pressure, or cosmetic.
    • Post-weld finishing: anodizing, polishing, machining, passivation, or painting.
    • Lot/heat traceability requirement.
    • Storage condition and packaging condition.
    • Whether the rod is clean enough for procedure-qualified or code work.

    Common Wrong-Part Mistakes

    • Using unmarked filler from a mixed rack.
    • Using ER4043 when the job requires ER5356, or using ER5356 where service temperature or base alloy makes it unsuitable.
    • Using carbon-contaminated filler on stainless work.
    • Handling cleaned filler with oily gloves.
    • Using rods stored open in humid shop air for critical work.
    • Assuming a clean-looking rod is clean enough for aluminum or stainless.
    • Using filler rod from a damaged package without checking rust, moisture, or oxide.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Rod dropped on floorCut off contaminated endClean or discard depending on procedure criticality
    Porosity starts when filler is addedSwitch to known-clean fillerVerify filler storage, alloy, cleaning, and gas coverage
    Aluminum filler is oxidizedClean rod and test weldUse fresh, dry, properly stored filler and clean base metal
    Unknown rods in tubeDo not use on critical workReplace with labeled filler with traceability where required
    Stainless filler contaminated by carbon steel dustClean if allowed for noncritical workSegregate stainless filler and tools from carbon steel contamination

    Related Failure Paths

    • TIG porosity: Oil, moisture, oxides, and dirty filler introduce gas or inclusions into the weld pool.
    • Black tungsten: Contaminated puddle vapor and poor gas coverage can dirty the tungsten.
    • Sooty TIG welds: Dirty filler, dirty base metal, or poor shielding can all create surface contamination.
    • Arc instability: Contamination changes puddle behavior and can cause popping or arc wander.
    • Cracking: Wrong filler selection or contamination can create weld-metal chemistry problems.
    • Corrosion failure: Wrong stainless, nickel, or aluminum filler can pass appearance inspection but fail service requirements.

    Safety Notes

    • Use compatible cleaners and allow solvents to evaporate before welding.
    • Keep flammable cleaners away from arcs, hot metal, and grinding sparks.
    • Do not weld over chlorinated solvents or unknown cleaning residue.
    • Wear gloves when handling cleaned filler rod to avoid cuts and oil transfer.
    • Use ventilation and respiratory protection appropriate for the base metal, filler, coating, and cleaner.
    • Segregate filler metals by alloy and label to avoid wrong-metal welds.
    • For code, pressure, food-grade, aerospace, or critical repair work, use verified filler with required traceability.

    Sources Checked

    Sources checked include TIG porosity and contamination references, aluminum welding guidance, filler metal catalog data, and related Weld Support Parts TIG troubleshooting articles. Final filler rod selection must be verified by base metal alloy, AWS classification, rod diameter, procedure requirement, storage condition, traceability requirement, shielding gas, and service environment.
  • Why Your TIG Welds Have Porosity (And How to Fix It in 15 Minutes)

    Why Your TIG Welds Have Porosity (And How to Fix It in 15 Minutes)

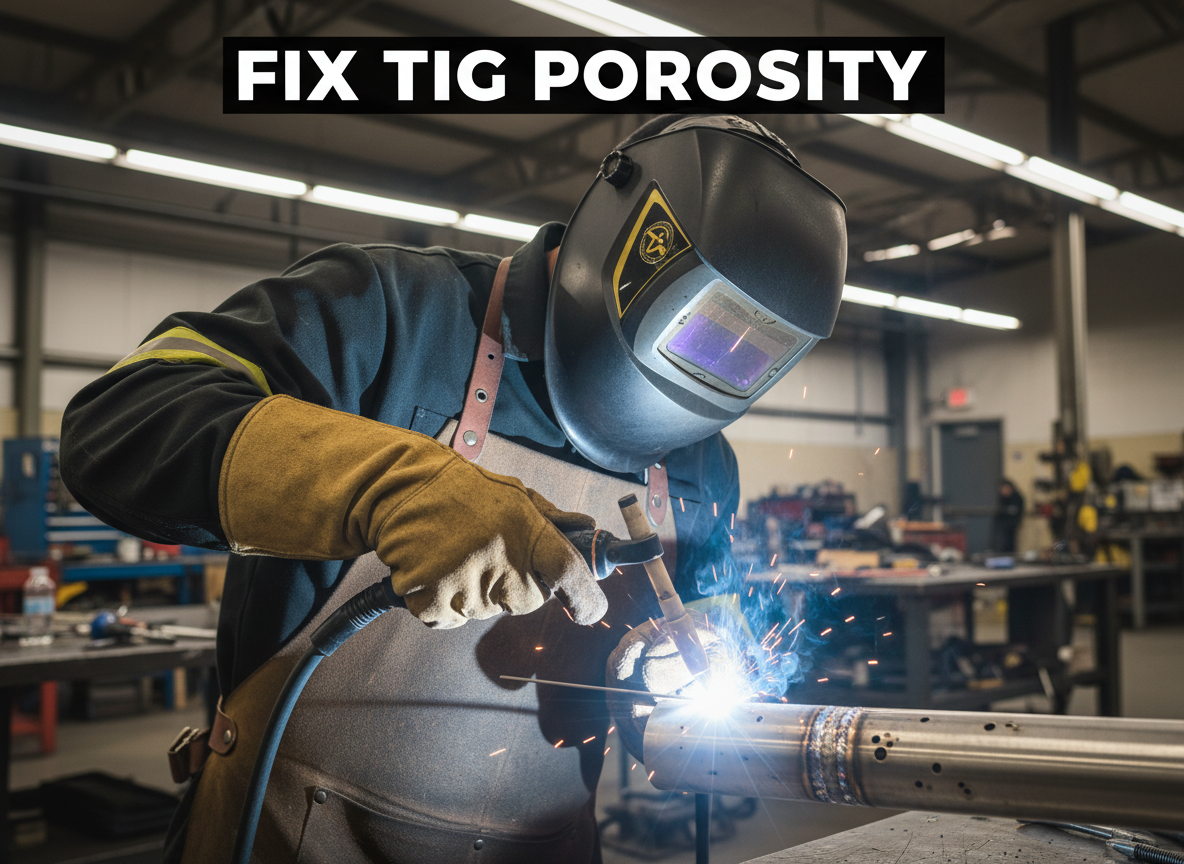
    Porosity in TIG welds—those small gas pockets trapped in the bead—kills strength and fails inspections. The good news: most porosity is caused by three fixable issues: contaminated gas, weak shielding coverage, or dirty base metal. Fix these, and your welds clean up fast.

    Key Takeaways

    • Porosity is caused by gas entrapment, not arc problems—focus on shielding and cleanliness
    • Diagnose in 5 minutes: check gas flow, inspect the torch, and clean your base metal
    • Most fixes cost under $20 and take less than 15 minutes
    • Gas lens collet bodies improve shielding coverage and reduce porosity risk
    • Test on scrap before returning to production

    Quick Diagnosis

    What you’ll see:

    • Small holes or bubbles in the weld bead (visible after cooling)
    • Bead surface looks rough or pitted
    • Porosity appears randomly or consistently across the weld

    Likely causes (ranked by frequency):

    1. Gas flow too low or regulator leaking
    2. Contaminated filler wire or tungsten
    3. Weak gas shielding (torch too far from work, wind, or bad gas lens)
    4. Dirty base metal (rust, mill scale, oil)
    5. Arc length too long or tungsten dipped in the puddle

    Safety Notes

    • Eye Protection: Use ANSI Z87.1-rated helmet with correct shade (typically #10–#12 for TIG). Porosity inspection requires close-up viewing—use a magnifying glass if needed.
    • Ventilation: TIG produces less fume than MIG or stick, but always weld in ventilated space or use a fume extractor. Tungsten inert gas (argon) is inert but displaces oxygen—ensure adequate air circulation.
    • Electrical Safety: Disconnect the welder before inspecting the torch or changing consumables.
    • Compressed Gas: Argon cylinders are pressurized. Never drop or expose to heat. Check regulator connections for leaks using soapy water (never a flame).

    Step-by-Step Troubleshooting

    Step 1: Check Gas Flow (Free)

    • Set regulator to 15–20 CFH (cubic feet per hour) for TIG.
    • Listen for a steady hiss at the torch nozzle.
    • If flow is weak or silent, check for kinks in the gas line or a leaking regulator.
    • Why: Low gas flow leaves the weld unshielded, allowing oxygen and nitrogen to enter the puddle and form gas pockets.

    Step 2: Inspect the Torch and Gas Lens (Free)

    • Remove the torch from the cable and look inside the nozzle.
    • Check for spatter buildup, cracks, or discoloration on the gas lens or collet body.
    • If the gas lens is damaged or heavily spattered, replace it (see “Recommended Fix” below).
    • Why: A damaged or dirty gas lens creates turbulence in the shielding gas stream, reducing coverage and trapping gas in the weld.

    Step 3: Clean the Base Metal (Free)

    • Use a wire brush, grinding wheel, or stainless steel brush to remove rust, mill scale, and oxidation.
    • Wipe with a clean cloth to remove dust and oils.
    • Weld within a few minutes of cleaning (oxidation returns quickly).
    • Why: Contaminants on the base metal release gases when heated, which get trapped in the molten puddle.

    Step 4: Test Arc Length and Technique (Free)

    • Keep the tungsten 1/8″ to 3/16″ above the base metal.
    • Maintain a steady, smooth arc without dipping the tungsten into the puddle.
    • Avoid moving the torch too fast or too far from the work.
    • Why: Long arc length weakens gas coverage. Dipping the tungsten introduces tungsten oxide and moisture, causing porosity.

    Step 5: Check Filler Wire and Tungsten (Low Cost)

    • Inspect the filler wire for dirt, rust, or kinks. Replace if contaminated.
    • Check the tungsten for cracks, balling, or discoloration. Replace if damaged.
    • Use the correct tungsten size for your amperage (typically 1/16″ to 3/32″ for most hobby/shop work).
    • Why: Contaminated consumables introduce gases and oxides directly into the weld.

    Fix Options (Ranked)

    1. Adjustment (Free)

    • Increase gas flow to 15–20 CFH.
    • Clean the base metal thoroughly.
    • Reduce arc length and improve torch angle.
    • Best for: First-time porosity or occasional issues.

    2. Consumable Replacement (~$10–$30)

    • Replace the filler wire spool if old or contaminated.
    • Replace the tungsten electrode if cracked or balled.
    • Best for: Consistent porosity after adjustments fail.

    3. Gas Lens Collet Body Replacement (~$15–$25)

    • Replace the gas lens and collet body to restore shielding coverage.
    • Improves gas flow pattern and reduces turbulence.
    • Best for: Persistent porosity despite clean base metal and correct gas flow.

    Recommended Fix (Product Section)

    Why a gas lens collet body works: A gas lens is a small brass component inside the torch that organizes the shielding gas flow into a smooth, laminar stream. Over time, spatter and oxidation clog the lens, creating turbulence and weak coverage. Replacing it restores full shielding and eliminates porosity caused by weak gas coverage.

    When to use it:

    • After cleaning the base metal and confirming gas flow are correct, but porosity persists.
    • When the old gas lens shows visible spatter, cracks, or discoloration.
    • As routine maintenance every 50–100 hours of welding.

    When NOT to use it:

    • If gas flow is low—fix the regulator first.
    • If the base metal is dirty—clean it before replacing the lens.
    • If the tungsten is dipped in the puddle—improve technique first.

    What to check before buying:

    • Verify your torch model (WP-17, WP-18, WP-26, WP-9, WP-20, WP-25, or SR series).
    • Confirm the collet size matches your tungsten diameter (typically 3/32″ for standard work).
    • Check that the package includes both the gas lens and collet body (some sell lens only).
    • Ensure the product is in stock and ships quickly (you’ll want to test immediately).
    • Look for 4+ star reviews from verified welders.

    No products found.

    Comparable Options

    If you prefer a larger pack or different torch size, consider:

    • 10-Pack 45V26 Collet Bodies (B07KCXHF4G): Same specs, larger quantity for shops doing frequent replacements.
    • Assorted Gas Lens Kit (B081LKNHGS): Multiple sizes (45V26, 45V27, 45V43) if you run different torch models.

    Common Mistakes

    • Assuming porosity is an arc problem. It’s not—porosity is a gas/contamination problem. Check shielding first.
    • Running gas flow too high. Above 25 CFH, excess gas creates turbulence and actually increases porosity. Stick to 15–20 CFH.
    • Skipping base metal cleaning. Rust and mill scale are the #1 cause of porosity in production shops. Always clean before welding.
    • Replacing the gas lens without checking the regulator. If the regulator leaks or is set too low, a new lens won’t help.
    • Ignoring tungsten contamination. If the tungsten is cracked or oxidized, replace it. A bad tungsten will cause porosity no matter how clean the base metal is.

    FAQ (Snippet-Optimized)

    Q: What causes porosity in TIG welding? Porosity is caused by gas entrapment—usually from weak shielding (low gas flow, damaged gas lens, wind), contaminated base metal, or a dipped tungsten. Fix shielding and cleanliness first.

    Q: How do I know if my gas lens is bad? Look inside the torch nozzle. If you see spatter buildup, cracks, or heavy discoloration, replace it. A clean lens should look bright and smooth.

    Q: Can I fix porosity by adjusting amperage? No. Amperage doesn’t cause porosity—gas coverage and cleanliness do. Adjust gas flow, clean the base metal, and check the torch instead.

    Q: How often should I replace my gas lens? Every 50–100 hours of welding, or whenever you see visible spatter or discoloration. Shops doing high-volume work replace them weekly.

    Q: Will a new gas lens fix all my porosity? Only if the porosity is caused by weak shielding. If the base metal is dirty or gas flow is low, a new lens alone won’t fix it. Address all three: gas flow, cleanliness, and torch condition.

    Next Steps

    For more TIG troubleshooting and gear guidance, check out these related posts:

    For more welding fixes and gear options, see our full resource page: https://blog.weldsupportparts.com/links/

  • Stick Welding Porosity Checklist

    Washington Alloy 308L Welding Electrode 10 LB Stick Package - High Quality Stainless Steel Welding
    “>Washington Alloy 308L Welding Electrode 10 LB Stick Package - High Quality Stainless Steel Welding

    Porosity in stick welding shows up as gas pockets in the weld metal. The usual causes are moisture, contamination, poor technique, or unstable shielding from the electrode. Use this checklist to isolate the cause before you change settings or replace parts.

    Key Takeaways

    • Start with moisture control. Wet electrodes and damp base metal are common causes of stick welding porosity.
    • Check cleanliness. Oil, rust, paint, mill scale, and solvent residue can trap gas in the weld.
    • Keep arc length short and consistent. A long arc can pull in air and increase porosity.
    • Verify travel speed and amperage. Too fast, too slow, or unstable current can affect shielding and bead formation.
    • If the issue persists, confirm electrode type, storage condition, and work lead placement.

    Troubleshooting Checklist

    1) Check electrode condition

    • Inspect rods for moisture exposure, damaged flux, or contamination.
    • Use only electrodes stored according to the manufacturer’s guidance. Exact storage limits are Unknown (Verify).
    • If rods were left open to shop humidity, treat moisture as a likely cause.

    2) Check base metal cleanliness

    • Remove oil, grease, water, paint, heavy rust, and scale from the weld area.
    • Clean beyond the joint line, not just the immediate arc start point.
    • Check for condensation on cold material, especially in humid shops or after outdoor exposure.

    3) Check arc length

    • Keep the arc short and controlled.
    • If the arc is too long, the weld pool is more likely to pull in atmospheric contamination.
    • If the electrode sticks or the arc is erratic, verify amperage and technique before increasing arc length.

    4) Check travel speed

    • Traveling too fast can leave gas trapped in the bead.
    • Traveling too slow can overheat the puddle and disturb slag flow.
    • Watch bead shape. A narrow, rough bead with pinholes often points to technique or contamination.

    5) Check amperage and polarity

    • Set amperage within the electrode range recommended by the manufacturer. Exact range for this application is Unknown (Verify).
    • Confirm polarity matches the electrode type and procedure being used.
    • If the arc is harsh, unstable, or digging too much, recheck machine settings before continuing.

    6) Check work lead and ground connection

    • Make sure the ground clamp is on clean metal.
    • Move the clamp closer to the weld if the current path is long or unstable.
    • Loose or dirty connections can make the arc inconsistent and worsen porosity.

    7) Check joint design and fit-up

    • Excessive gaps can make shielding and puddle control harder.
    • Confirm root opening, bevel, and alignment are consistent.
    • Deep corrosion or trapped debris in the joint can create localized porosity.

    Common Causes and What to Fix First

    • Moist electrodes: Replace, dry, or reopen only after verifying correct storage method.
    • Dirty steel: Grind or wire-brush to clean metal.
    • Long arc: Shorten the arc and stabilize hand motion.
    • Poor ground: Clean the clamp point and improve contact.
    • Incorrect technique: Slow down and keep a steady travel angle.

    Support Section: Electrode Selection

    If porosity keeps returning after cleaning and technique corrections, check whether the electrode matches the job. This draft includes one available product option from Weld Support Parts:

    Washington Alloy 308L Welding Electrode 10 LB Stick Package

    Product: Washington Alloy 308L Welding Electrode 10 LB Stick Package – High Quality Stainless Steel Welding

    Use case: Stainless steel welding applications only as described by the product listing. Other compatibility details are Unknown (Verify).

    Shopify handle: 308l-welding-electrode-10lb

    Shortcode:

    Washington Alloy 308L Welding Electrode 10 LB Stick Package - High Quality Stainless Steel Welding

    Washington Alloy 308L Welding Electrode 10 LB Stick Package – High Quality Stainless Steel Welding

    Elevate your welding projects with the Washington Alloy 308L-16 10lbs Welding Stick Electrode. Designed for stainless steel applications, this high-quality electrode ensures superior arc stability and a clean finish for every weld. Whether you're a professional welder or a DIY enthusiast, this product is a must-have in your welding toolkit. The 308L welding electrode is known for its excellent low carbon content,…

    View at Arc Weld Store

    Note: Confirm base material, procedure, polarity, and storage requirements before use.

    Safety Notes

    • Do not handle hot electrodes or weldments without proper PPE.
    • Use ventilation when welding to reduce fume exposure.
    • Keep solvents, oils, and cleaning chemicals away from the weld area until fully evaporated.
    • Follow the equipment manual for polarity, current range, and lead connection.
    • If you suspect contaminated rods or unsafe storage, remove them from service until verified.

    FAQ

    What does porosity look like in stick welding?

    It usually appears as small holes, pinholes, or worm-like voids in the weld bead or after grinding.

    Can moisture cause porosity in stick welding?

    Yes. Moisture in the electrode, base metal, or surrounding environment is a common cause.

    Should I increase amperage to fix porosity?

    Not first. Check contamination, electrode condition, arc length, and ground quality before changing amperage.

    Does arc length affect porosity?

    Yes. A long arc increases exposure to air and can make porosity worse.

    What should I check first when porosity appears?

    Start with electrode dryness, joint cleanliness, and arc length.

    Sources Checked

    If porosity continues after these checks, stop and verify the procedure, consumable condition, and machine setup before production welding.

    Related Weld Support Guides

  • MIG Porosity Causes and Fixes

    Washington Alloy E71T-GS .045 Gasless MIG Welding Wire 11 LB Spool for Easy Welding Tasks
    “>Washington Alloy E71T-GS .045 Gasless MIG Welding Wire 11 LB Spool for Easy Welding Tasks

    MIG porosity is gas trapped in the weld metal as it solidifies. It usually shows up as pinholes, worm tracks, or a rough weld surface. The main causes are shielding gas problems, contamination, incorrect gun setup, and poor technique.

    Key Takeaways

    • Most MIG porosity starts with shielding gas loss or contamination.
    • Check gas flow, leaks, nozzle blockage, stickout, and torch angle first.
    • Clean base metal and filler wire storage matter.
    • Use consistent travel speed and arc length to keep shielding stable.

    Common MIG Porosity Causes

    1. Shielding gas contamination or loss

    If shielding gas is not reaching the arc, air will mix into the weld pool. That creates porosity. Common reasons include an empty cylinder, a closed valve, a leaking hose, loose fittings, or a damaged gun neck.

    2. Excessive stickout

    Stickout that is too long reduces shielding effectiveness and can make the arc unstable. Long stickout also increases electrical resistance and can change the way the wire melts.

    3. Dirty base metal

    Rust, oil, mill scale, paint, galvanizing residue, moisture, and cutting fluids can all cause porosity. Contamination vaporizes in the arc and gets trapped in the weld.

    4. Moisture on the work or wire

    Condensation, wet storage, or damp wire can introduce hydrogen and other gases into the weld. This can create visible porosity or internal defects.

    5. Incorrect torch angle or excessive travel speed

    Too much angle or moving too fast can pull shielding gas away from the puddle. That leaves the weld exposed to the atmosphere.

    6. Nozzle blockage or spatter buildup

    Spatter, soot, and debris in the nozzle can disrupt gas coverage. A restricted nozzle can cause erratic shielding even when gas flow looks normal at the regulator.

    7. Drafts and air movement

    Fans, open doors, shop airflow, and outdoor wind can blow shielding gas away from the weld zone. Gasless flux-cored wire can reduce this issue, but it does not solve contamination on the workpiece.

    Troubleshooting Steps

    Step 1: Inspect the weld defect

    Look at the porosity pattern. Scattered pinholes often point to contamination or gas disturbance. Linear porosity can point to travel issues, nozzle problems, or gas coverage loss along the weld path.

    Step 2: Check shielding gas delivery

    Verify the cylinder is open, the regulator is set correctly, and the flowmeter is working. Inspect hoses, fittings, and the gun for leaks. Unknown (Verify): specific recommended flow rate depends on wire type, joint position, and shielding gas mix.

    Step 3: Clean the nozzle and contact tip area

    Remove spatter and buildup from the nozzle, diffuser, and tip. Make sure gas ports are not blocked. Replace worn parts if cleaning does not restore a clear gas path.

    Step 4: Shorten stickout if needed

    Keep wire stickout within the range recommended for your process and consumable. If porosity appears after a setup change, reduce stickout and re-test.

    Step 5: Clean the joint and surrounding area

    Remove oil, rust, paint, moisture, and heavy scale before welding. Clean beyond the weld zone so contamination does not get pulled into the arc.

    Step 6: Reduce drafts

    If possible, block crossflow from fans or doors. For field work, reposition the setup or use wind protection that does not disturb the arc.

    Step 7: Review travel technique

    Use steady travel speed and maintain a consistent torch angle. Avoid weaving so wide that the shielding gas cannot cover the full puddle.

    Support Parts and Consumables

    If you need a wire option for gasless MIG work, this product may be relevant for certain applications:

    • Washington Alloy E71T-GS .045 Gasless MIG Welding Wire 11 LB Spool for Easy Welding Tasks

      Washington Alloy E71T-GS .045 Gasless MIG Welding Wire 11 LB Spool for Easy Welding Tasks

      The Washington Alloy E71T-GS Gasless Mig Welding Wire is your go-to solution for all your welding needs. This 11 LB. spool, with a diameter of .045 inches, is engineered to deliver excellent results in various welding applications without the hassle of gas tanks. Ideal for both professionals and home users alike, this high-performance welding wire is designed to make your welding experience smoother and more effec…

      View at Arc Weld Store

    Washington Alloy E71T-GS .045 Gasless MIG Welding Wire 11 LB Spool for Easy Welding Tasks. Verify suitability for your material, thickness, polarity, and procedure before use.

    Safety Notes

    • Shut off and secure shielding gas cylinders before servicing the system.
    • Do not weld on contaminated or unknown coated materials without proper hazard review.
    • Use ventilation and respiratory protection as required by the job.
    • Hot metal, spatter, and sharp slag can cause burns and cuts.
    • Follow the welding procedure, machine manual, and site safety rules.

    FAQ

    What is the most common cause of MIG porosity?

    Shielding gas loss or contamination is the most common cause. Start with gas delivery, nozzle condition, and airflow around the weld.

    Can dirty steel cause porosity?

    Yes. Rust, oil, paint, moisture, and mill scale can all create gas pockets in the weld.

    Does long stickout cause porosity?

    Yes. Excessive stickout can reduce shielding gas effectiveness and destabilize the arc.

    Will gasless wire fix porosity?

    Not automatically. Gasless wire can help when wind makes gas shielding difficult, but dirty material, poor technique, and moisture can still cause defects.

    Sources Checked

    • Weld Support Parts internal product listing for Washington Alloy E71T-GS .045 Gasless MIG Welding Wire 11 LB Spool
    • Weld Support Parts internal knowledge patterns for MIG troubleshooting topics
    • Related Weld Support Parts articles on welding troubleshooting and defect causes

    Related Weld Support Guides

  • TIG Torch Gas Leak Troubleshooting: Argon Loss, Black Tungsten, Porosity, and Torch Seal Checks

    If a TIG torch has a gas leak, the weld may show black tungsten, gray weld color, porosity, sugaring on stainless, unstable starts, or a loud uneven gas hiss even when the regulator shows normal flow. Start at the cylinder and work forward to the cup. A TIG gas leak can be at the regulator, machine inlet, solenoid, torch hose, power cable/gas hose, torch head, collet body, gas lens, cup seal, back cap O-ring, or torch valve.

    The fast check is to verify 100% argon, confirm flow at the torch with a flow tester, inspect the cup/gas lens/collet body/back cap, then leak-test fittings with approved leak-check solution. Do not raise flow to hide a leak. Too much flow can pull air into the shielding envelope and make the weld dirtier. For related TIG shielding symptoms, see TIG shielding gas coverage troubleshooting, why TIG tungsten turns black, and TIG welds looking sooty.

    Common Symptoms

    • Tungsten turns black, blue, gray, or chalky after welding.
    • Weld bead has porosity, soot, oxidation, or gray color.
    • Stainless shows sugaring, crusting, or dark heat tint near the root.
    • Arc starts unstable even with clean tungsten.
    • Gas hiss sounds loud, weak, pulsed, or uneven at the cup.
    • Regulator flow reads normal, but flow at the cup is low.
    • Shielding improves when the torch hose is moved or held straight.
    • Back cap area hisses during post-flow.
    • Gas flow stops too early and tungsten discolors after arc-off.

    Likely Causes

    CauseWhat It DoesQuick Check
    Loose regulator or hose fittingLeaks argon before it reaches the machine or torchLeak-check fittings with solution
    Cracked TIG gas hosePulls air or loses shielding gas before the cupFlex hose during post-flow and check for bubbles
    Loose collet body or gas lensLeaks inside the torch head or disrupts flowRemove cup and verify body is seated tight
    Damaged back cap O-ringLeaks around the rear of the torch headInspect O-ring for cuts, flattening, heat damage, or missing seal
    Cracked cup or wrong insulatorBreaks the gas seal and creates turbulenceReplace cup and confirm correct gasket/insulator stack
    Plugged gas lens screenRestricts or distorts argon flowHold lens to light and inspect screen
    Bad torch valveLeaks or fails to shut off on valve-style torchesClose valve and check if gas continues
    Short post-flowLets hot tungsten oxidize after weldingIncrease post-flow and hold torch over weld

    Fast Diagnosis Sequence

    1. Confirm the cylinder is 100% argon for normal TIG work unless the procedure calls for another approved shielding gas.
    2. Check the regulator, flowmeter, and cylinder connection.
    3. Confirm gas flow at the torch cup, not only at the regulator.
    4. Inspect the cup for cracks, chips, heat damage, wrong size, or poor seating.
    5. Remove and inspect the collet body or gas lens. It must seat fully in the torch head.
    6. Inspect the back cap O-ring and back cap threads.
    7. Check torch hose, power cable/gas hose, machine inlet, and torch valve for leaks.
    8. Use leak-check solution on fittings. Do not use flame.
    9. Reduce excessive flow if the gas sounds like a hard blast instead of a smooth shield.
    10. Retest with clean tungsten, normal stickout, and no drafts.

    Inspection Steps

    • Regulator and flowmeter: Confirm proper connection, stable flow reading, no damaged CGA fitting, and no cracked hose barb.
    • Machine gas inlet/outlet: Inspect loose fittings, cracked internal hose, and gas solenoid area only with power disconnected.
    • Torch hose: Look for cuts, burned sections, kinks, loose crimps, or leaks that appear only when the hose is flexed.
    • Torch head: Inspect threads, heat damage, loose head-to-body connection, and valve packing on valve torches.
    • Collet body/gas lens: Verify it is the correct type for the torch series and cup system. A loose or mismatched body can leak or disturb gas flow.
    • Back cap: Check O-ring, cap length, threads, and whether the tungsten is clamped without bottoming the cap incorrectly.
    • Cup and insulator: Confirm the cup is not cracked and the correct gasket/insulator is installed for standard or gas-lens setup.
    • Post-flow: Gas must continue long enough to shield the hot tungsten and cooling weld area.

    Test Procedures

    • Cup flow test: Use a TIG flow tester at the cup. A regulator reading alone does not prove flow at the torch.
    • Bubble leak test: Apply approved leak-check solution to fittings during flow or post-flow. Bubbles identify leakage.
    • Hose flex test: Run post-flow and gently flex the hose. If flow or bubbles change, replace damaged hose or cable assembly.
    • Back cap test: Listen and check around the back cap during post-flow. Replace damaged O-rings and verify correct cap.
    • Front-end swap test: Install a known-good cup, collet body/gas lens, collet, back cap, and insulator. If shielding improves, the leak or turbulence was in the torch front end.
    • Post-flow test: Hold the torch still after arc-off. If the tungsten stays bright after increasing post-flow, the issue was hot tungsten oxidation.

    Root Cause Analysis

    TIG shielding must protect the tungsten, arc, filler rod end, and weld puddle from oxygen and nitrogen. A leak before the torch wastes argon and can lower flow at the cup. A leak or bad seal inside the torch head can mix air into the shielding zone. A damaged gas lens or cracked cup can create turbulence even when flow volume looks correct.

    Gas leaks are often mistaken for bad tungsten or dirty filler. The tungsten turns black, the weld gets sooty, and the operator increases gas flow. If the actual problem is a cracked cup, missing O-ring, loose gas lens, or leaking hose, more gas may make turbulence worse. Correct the seal and gas path first, then tune cup size, flow, torch angle, and stickout.

    Compatibility Notes

    Do not order TIG torch gas parts by cup size alone. Verify torch series, cooling type, torch head style, collet size, collet body style, gas lens style, cup thread or push-on style, back cap length, O-ring, gasket/insulator, power connector, gas connector, and machine connection. Common 9/20 and 17/18/26-style parts are not automatically interchangeable.

    Gas-lens conversions also require the correct insulator, cup, collet body, collet, and sealing ring where used. Mixing standard collet bodies with gas-lens cups, or using the wrong insulator stack, can create leaks at the torch head. If the torch model or consumable system is not confirmed, mark the part as Unknown (Verify).

    What To Verify Before Ordering

    • TIG torch series: 9, 17, 18, 20, 26, or manufacturer-specific equivalent.
    • Air-cooled or water-cooled torch.
    • Valve torch or machine-solenoid torch.
    • One-piece or two-piece cable/hose arrangement.
    • Back cap length and O-ring style.
    • Collet size matching tungsten diameter.
    • Standard collet body or gas lens collet body.
    • Cup style, cup size, insulator/gasket, and sealing ring.
    • Machine gas connector, quick connector, or separate gas hose fitting.
    • Argon regulator/flowmeter outlet fitting and hose size.

    Common Wrong-Part Mistakes

    • Installing a gas-lens cup without the correct gas-lens body and insulator.
    • Using a 17/18/26 front-end kit on a 9/20 torch.
    • Replacing tungsten repeatedly while leaving a cracked cup in service.
    • Using a back cap with a missing, cut, or flattened O-ring.
    • Over-tightening ceramic cups until they crack.
    • Using a MIG flowmeter or wrong-pressure flow device on a TIG torch setup.
    • Raising argon flow too high and creating turbulence instead of fixing the leak.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Back cap leakReseat cap and reduce movementReplace O-ring or correct back cap
    Cracked cupInstall spare cupVerify correct cup, insulator, and torch angle/stickout
    Loose gas lensSnug gas lens bodyReplace damaged gas lens, filter, seal, or torch threads
    Leaking hoseStop using the torchReplace hose, cable assembly, or torch
    Black tungsten after arc-offAdd post-flowCorrect post-flow, leaks, drafts, and cup coverage

    Related Failure Paths

    • Black tungsten: Hot tungsten is exposed to oxygen from poor shielding, leaks, or short post-flow.
    • Porosity: Air enters the weld puddle through a leak, draft, bad cup seal, or contaminated gas path.
    • Arc instability: Gas turbulence and tungsten oxidation make starts and arc focus inconsistent.
    • Sugaring on stainless: Shielding loss at the puddle or root side allows heavy oxidation.
    • Short consumable life: Leaks and overheating damage cups, collets, gas lenses, and O-rings.

    Safety Notes

    • Close the cylinder valve and bleed pressure before removing gas fittings.
    • Disconnect input power before opening machine covers or checking internal gas hoses.
    • Use approved leak-check solution. Never use flame to find gas leaks.
    • Argon can displace oxygen in confined spaces. Maintain ventilation.
    • Do not weld with cracked torch hoses, burned cables, or leaking torch heads.
    • Hot cups and torch heads can burn skin and gloves; allow cooling before disassembly.
    • Use correct PPE and follow the torch and machine manual for service limits.

    Sources Checked

    Sources checked include TIG torch parts catalog data, TIG shielding gas flow references, torch manual troubleshooting notes, and related Weld Support Parts TIG shielding articles. Final replacement must be verified by torch series, cable/hose style, back cap/O-ring, cup system, collet body or gas lens type, tungsten diameter, machine connection, and shielding gas setup.

  • MIG Nozzle Spatter Buildup Troubleshooting: Poor Gas Coverage, Porosity, Burnback, and Arc Instability

    MIG nozzle spatter buildup is not just a cleaning issue. When spatter packs inside the nozzle, bridges toward the contact tip, or blocks the diffuser ports, shielding gas flow becomes restricted or turbulent. The weld can then show porosity, black soot, erratic arc starts, excess spatter, contact tip overheating, and repeated burnback even when the gas cylinder and regulator look normal.

    The fast fix is to shut the machine off, let the gun cool, remove the nozzle, clean or replace the nozzle, inspect the diffuser holes, and replace the contact tip if it is worn, arc-marked, or spatter-packed. Do not compensate for a blocked nozzle by raising gas flow first. High gas flow can also create turbulence. Clean the front end, verify nozzle bore and tip recess, then test weld on clean material. For related front-end failures, see MIG diffuser clogging symptoms, MIG porosity troubleshooting, and MIG wire burnback into the contact tip.

    Common Symptoms

    • Pinholes, wormholes, or scattered porosity appear after several welds.
    • Nozzle bore is packed with BB-like spatter or slag-colored deposits.
    • Gas sounds normal at the regulator, but the weld acts unshielded.
    • Arc starts rough, pops, or wanders before stabilizing.
    • Spatter increases even though settings have not changed.
    • Contact tip turns blue, burns back, or fuses wire more often.
    • Nozzle sticks to the work or fills faster in corners and short stickout work.
    • Weld bead has black soot or an oxidized surface around the toes.

    Likely Causes

    CauseWhat It DoesQuick Check
    Spatter-packed nozzleRestricts or redirects shielding gasRemove nozzle and inspect bore with light
    Blocked diffuser portsCreates uneven gas flow around the tipLook for plugged side holes behind the nozzle
    Nozzle too small for applicationFills quickly and limits gas envelopeCompare bore size to wire size, amperage, and joint access
    Tip recess or stickout wrongChanges gas coverage and arc behaviorVerify contact tip position for the gun/nozzle style
    Voltage/WFS imbalanceCreates excessive spatter at the arcAdjust one variable at a time after cleaning front end
    Too short stickoutRuns nozzle too close and overheats the front endHold a consistent contact-tip-to-work distance
    Too much anti-spatter or nozzle dipCan contaminate gas path or collect debrisUse a light coating only on approved areas
    Damaged nozzle insulationCan cause arcing to the nozzleReplace nozzles with cracked or burned insulation

    Inspection Steps

    1. Turn off the welder and let the gun front end cool.
    2. Remove the nozzle. Do not twist against a hot, seized nozzle with bare hands.
    3. Look inside the nozzle bore. Replace it if spatter is fused, the bore is distorted, or the insulation is damaged.
    4. Inspect the contact tip. Replace it if the bore is oval, rough, arc-marked, or partially plugged.
    5. Inspect the diffuser. Gas holes must be open and threads must hold the tip square.
    6. Check whether spatter is bridging between the nozzle, tip, and diffuser.
    7. Confirm the nozzle bore and contact tip recess match the gun setup and weld access needs.
    8. Reassemble with clean parts, then test on clean scrap before changing machine settings.

    A nozzle that repeatedly packs with spatter may be a symptom of another problem. After the nozzle is clean, check work clamp contact, wire feed consistency, polarity, stickout, travel angle, voltage, wire-feed speed, shielding gas type, and base-metal cleanliness. If the wire feed is slipping or surging, use MIG wire feed slipping troubleshooting before blaming the nozzle alone.

    Test Procedures

    • Clean-front-end test: Clean or replace the nozzle, tip, and diffuser, then run the same weld settings. If porosity and spatter drop immediately, the nozzle/diffuser area was the active failure.
    • Gas-flow path test: With the nozzle removed, inspect for blocked diffuser holes. Gas must flow evenly around the contact tip, not from one restricted side.
    • Nozzle comparison test: Install a clean correct-size nozzle. If the problem disappears, the previous nozzle was either blocked, damaged, undersized, or wrong for the job.
    • Stickout test: Run a short bead while keeping a consistent contact-tip-to-work distance. If buildup returns quickly when the nozzle is too close, operator distance is contributing.
    • Settings test: After front-end parts are clean, adjust voltage and wire-feed speed one variable at a time. Excessive spatter from poor settings will refill the nozzle fast.

    Visual Wear Indicators

    • Spatter ring inside the nozzle bore.
    • Spatter bridge touching the contact tip or diffuser.
    • One side of the nozzle packed more heavily than the other.
    • Burned, cracked, loose, or missing nozzle insulation.
    • Nozzle bore out-of-round from pliers, impact, or overheating.
    • Contact tip blue, mushroomed, ovaled, or loose in the diffuser.
    • Diffuser ports plugged with spatter or wire shavings.

    Root Cause Analysis

    The nozzle’s job is to direct shielding gas around the wire and weld pool. When spatter narrows the bore, the gas stream can lose coverage or become turbulent. That exposes the molten weld pool to air and can create porosity even when the flowmeter still shows gas. A dirty nozzle can also trap heat around the contact tip, which increases burnback and can make the wire stick inside the tip.

    Spatter buildup also feeds itself. A rough arc creates spatter, the spatter blocks gas, poor gas coverage makes the arc and weld puddle less stable, and the unstable arc throws more spatter into the nozzle. Break that loop by cleaning the front end first, then correcting the cause of excessive spatter.

    Compatibility Notes

    Do not order MIG nozzles by bore size alone. Verify gun brand, gun series, nozzle connection style, slip-on or threaded design, contact tip position, diffuser style, amperage range, wire size, shielding gas, and joint access. A bottleneck nozzle may help reach a tight joint, but a smaller bore can pack faster and may reduce gas coverage if used outside its intended range.

    Also verify whether the job needs flush, recessed, or protruding contact tip position. Wrong tip recess can change stickout, arc stability, gas coverage, and spatter collection. If the nozzle, diffuser, and contact tip are from mixed consumable systems, replace them as a matched front-end set for the installed gun.

    What To Verify Before Ordering

    • MIG gun manufacturer and exact gun series.
    • Nozzle style: slip-on, threaded, heavy-duty, tapered, bottleneck, or flush style.
    • Nozzle bore diameter and required joint access.
    • Contact tip position: flush, recessed, or extended.
    • Diffuser or retaining head style used by the gun.
    • Wire diameter, wire type, amperage range, and duty cycle.
    • Shielding gas and expected gas flow range.
    • Whether the nozzle insulation is separate or built into the nozzle.
    • Paint, galvanizing, or coating requirements if anti-spatter is used on workpieces.

    Common Wrong-Part Mistakes

    • Using a small bottleneck nozzle for high-spatter welding because it improves visibility.
    • Replacing only the nozzle while leaving a plugged diffuser in place.
    • Mixing nozzles, tips, and diffusers from different consumable systems.
    • Using too much nozzle dip and contaminating the gas path.
    • Spraying anti-spatter into the contact tip bore or threaded electrical contact area.
    • Ignoring nozzle insulation damage that allows arcing between the nozzle and work.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Light spatter in nozzleClean with MIG pliersAdd routine cleaning interval and correct settings
    Spatter fused inside boreInstall spare nozzleReplace nozzle and inspect diffuser/tip for heat damage
    Porosity after several weldsClean nozzle and check gasVerify gas path, diffuser, nozzle size, drafts, and base-metal prep
    Repeated burnbackReplace contact tipCorrect feed drag, stickout, diffuser blockage, and tip size
    Nozzle packs fast in cornersClean more oftenReview joint access, gun angle, nozzle bore, and anti-spatter method

    Anti-Spatter Use

    Anti-spatter spray or nozzle gel can slow buildup, but it should not be used to hide bad settings, poor wire feed, or a blocked diffuser. Apply only a light amount and follow the product directions. Keep product out of the contact tip bore, electrical thread contact areas, and gas passages unless the manufacturer specifically allows that use. For paint-sensitive work, verify silicone-free or paint-compatible chemistry before spraying workpieces.

    Ignored-Failure Consequences

    • Porosity and rejected welds from poor shielding gas coverage.
    • Burnback and downtime from overheated contact tips.
    • More spatter from unstable arc starts and poor gas flow.
    • Damaged diffuser threads or seized front-end consumables.
    • Premature gun neck heating and shorter consumable life.
    • False troubleshooting of regulators, gas cylinders, or machine output when the nozzle is the real restriction.

    Safety Notes

    • Turn off the welder before removing nozzles, tips, or diffusers.
    • Hot nozzles can burn gloves and skin; allow cooling time before service.
    • Wear eye protection when chipping, brushing, or clipping wire.
    • Do not use flammable cleaners near the arc or on hot parts.
    • Use ventilation or local exhaust during welding and testing.
    • Read anti-spatter and cleaner safety data sheets before use.

    Sources Checked

    Sources checked include OEM MIG troubleshooting guidance, welding safety references, uploaded anti-spatter and accessory catalogs, and related Weld Support Parts troubleshooting articles. Nozzle replacement must still be verified by gun series, nozzle connection, diffuser style, contact tip position, wire size, amperage, shielding gas, and application access.

  • Stick Welding Porosity Troubleshooting: Pinholes, Wormholes, Moisture, Arc Length, and Electrode Checks

    Stick welding porosity usually comes from gas trapped in the weld metal before the puddle freezes. With SMAW, start with the electrode, base metal, arc length, amperage, polarity, and technique before blaming the welder. Pinholes after slag removal, wormholes in the bead, rough starts, popping arc behavior, and scattered pits usually point to moisture, contamination, long arc length, wrong rod handling, or welding over paint, oil, rust, zinc, primer, or damp steel.

    The repair path is simple: stop welding, identify whether the porosity is surface-only or through the bead, clean the joint to bright metal, switch to known-good electrodes, shorten the arc, verify amperage and polarity, and run a controlled test bead on clean scrap. For low-hydrogen rods, especially 7018, porosity must be treated as a storage and hydrogen-control issue, not only a bead appearance problem. See the related WSP guide on 7018 rod moisture contamination when damp rods, sticking, or cracking risk are present.

    Common Symptoms

    SymptomLikely CauseFirst Check
    Small pinholes after chipping slagMoisture, contamination, or long arcTry dry rods on clean scrap
    Wormholes or tunnels in beadSevere contamination or trapped gasGrind out and clean joint
    Porosity starts after rod changeBad rod batch, damp coating, wrong rod storageCompare against sealed rods
    Porosity only at startsPoor restart, long arc, damp rod tipClip/restrike properly and shorten arc
    Porosity on rusty or painted steelSurface contamination burning into puddleRemove coating and re-test
    Porosity with 7018 plus stickingLow amperage, damp coating, bad arc lengthCheck storage and amperage

    Likely Causes

    Moisture in electrodes: Damp coating can release hydrogen and other gases into the weld pool. Low-hydrogen electrodes are especially sensitive. Opened 7018 should be stored according to the electrode manufacturer, code, and WPS requirements.

    Dirty base metal: Oil, grease, paint, primer, rust, mill scale, cutting fluid, galvanized coating, and moisture can create gas pockets when heated. Stick welding is more tolerant than TIG or MIG, but it is not immune to contamination.

    Long arc length: A long arc can reduce shielding from the electrode coating and pull air into the arc zone. This is common with new operators trying to see the puddle.

    Wrong rod manipulation: Excessive whipping with low-hydrogen rods can cause porosity. Some cellulose rods tolerate whip-and-pause technique, but 7018 should normally be run with a short, steady arc.

    Wrong amperage or polarity: Too-low amperage can leave a cold, sluggish puddle that traps gas. Wrong polarity can create instability, spatter, poor penetration, and porous starts. If the symptom includes sticking, review 7018 rod sticking causes and solutions.

    Quick Checks

    • Use fresh, known-good electrodes from sealed or properly stored packaging.
    • Clean the weld area to bright metal at least 1/2 in beyond the weld zone.
    • Remove oil, paint, primer, zinc, moisture, rust, and grinding dust before welding.
    • Shorten the arc until the puddle is controlled and the arc sounds steady.
    • Verify polarity: 6010 commonly requires DCEP, while many 7018 rods run on AC or DCEP depending on formulation.
    • Check amperage against the rod diameter, position, and manufacturer chart.
    • Run one test bead on clean scrap with one change at a time.

    Root Cause Analysis

    If porosity disappears on clean scrap with fresh rods, the welder is probably not the root cause. The problem is usually the workpiece surface, electrode condition, or joint environment. If porosity follows one rod container but not another, quarantine the suspect rods. If porosity appears only in vertical or overhead work, look at arc length, travel speed, rod angle, and slag control.

    For rod selection, the difference between cellulose and low-hydrogen electrodes matters. WSP’s 6010 vs 7018 guide explains that 6010 is used for digging penetration and root work, while 7018 is used for low-hydrogen structural welds. Do not store or run them the same way. Mixing 6010 and 7018 in the same oven or job box can create wrong-rod and wrong-storage problems.

    Inspection Steps

    1. Chip and wire-brush the weld. Confirm whether holes are isolated surface pits or continuous porosity.
    2. Grind one defect open. If holes continue below the surface, remove the weld until sound metal is reached.
    3. Inspect rod coating. Reject rods with cracked, swollen, oily, soft, rusty, chipped, or wet coating.
    4. Check base metal. Look for paint, oil, water, galvanizing, primer, heavy rust, cutting fluid, and laminations.
    5. Check machine setup. Confirm amperage, polarity, lead connections, work clamp contact, and cable condition.
    6. Check technique. Look for long arc, excessive weave, whipping with low-hydrogen rods, or travel speed too fast for gas escape.
    7. Make a comparison weld using clean scrap and fresh rods. If the test is sound, return to the workpiece and correct cleaning or joint conditions.

    Test Procedures

    Use a clean scrap coupon of the same material when possible. Run three beads: one with the suspect rod, one with a fresh rod from sealed storage, and one after changing arc length and amperage. Keep polarity, rod diameter, and base metal consistent. If only the suspect rod creates porosity, remove that rod batch from critical work. If all beads are porous, inspect work clamp contact, machine output, arc length, and surface preparation.

    For 7018, test beads are not proof of low-hydrogen compliance. A rod can make an acceptable-looking bead and still be unacceptable for code, pressure, structural, lifting, or restrained work if exposure history is unknown. Follow the WPS, inspector, electrode manufacturer, or engineer requirement.

    Visual Wear Indicators

    • Electrode coating cracks: moisture cycling, impact damage, or old stock.
    • Soft or powdery coating: moisture damage; do not use for critical welds.
    • Rust on exposed core wire: storage failure or aged rods.
    • Oily rod surface: contamination that can create porosity and fumes.
    • Blackened start pits: poor restart, contamination, or arc instability.
    • Glassy irregular slag on 7018: possible damp coating or incorrect settings.

    Compatibility Notes

    Verify electrode classification, rod diameter, polarity, amperage range, base metal, position, and storage requirement before ordering or welding. E6010, E6011, E7014, E7018, E7018-1, E7018AC, stainless electrodes, nickel cast-iron rods, and hardfacing electrodes do not share the same storage, polarity, or technique rules. When the rod is unknown, label it Unknown (Verify) and do not use it on critical welds.

    What To Verify Before Ordering

    • Exact electrode class and brand required by the WPS or repair procedure.
    • Rod diameter that matches material thickness, position, and available amperage.
    • Machine output and polarity compatibility.
    • Whether 7018AC is required for an AC-only transformer machine.
    • Whether low-hydrogen storage, sealed cans, rod oven, or quiver control is required.
    • Base metal condition: clean mild steel, rusty repair work, galvanized, coated, cast iron, hardfacing, or unknown alloy.

    Common Wrong-Part Mistakes

    • Using old open 7018 from a toolbox on a structural repair.
    • Buying standard 7018 for a machine that only runs AC poorly.
    • Using 6010 because it burns through contamination instead of cleaning the joint.
    • Running a specialty electrode like nickel or hardfacing without checking polarity and procedure.
    • Assuming porosity is always caused by amperage when the rod is damp or the base metal is contaminated.

    Field Fix vs Proper Fix

    ConditionField FixProper Fix
    Pinholes with 7018Try fresh dry rods on clean scrapCorrect rod storage and follow WPS exposure limits
    Porosity over paint or rustGrind test area cleanRemove coating from full weld zone before welding
    Long arc porosityShorten arc and reduce travel speedRetrain technique and verify settings
    Damp rods in the fieldUse sealed fresh rods for noncritical testingUse approved oven/quiver procedure or discard
    Wormholes in finished weldStop and mark defectGrind out to sound metal and reweld under corrected conditions

    Related Failure Paths

    Porosity often travels with rod sticking, slag inclusions, lack of fusion, undercut, arc blow, cracking, and failed visual inspection. A bad ground or unstable arc can make the operator hold a longer arc, which then creates porosity. Damp 7018 can create porosity and increase hydrogen-cracking risk. Poor fume control is also common when welding dirty, coated, or contaminated steel; review welding fume extractor troubleshooting when smoke is not being captured at the arc.

    Safety Notes

    Do not weld over unknown coatings, paint, solvent residue, oil, galvanized coating, plating, or contaminated steel without identifying the hazard. Use ventilation, fume extraction, correct helmet shade, dry gloves, fire watch, and electrical safety practices. Keep your head out of the plume. Do not use wet rods, improvised rod heating, torch-baked electrodes, microwave drying, or truck-dash drying for low-hydrogen work.

    Sources Checked

    • Washington Alloy electrode catalog sections on 6010, 7018, low-hydrogen welding tips, and porosity warnings related to whipping low-hydrogen electrodes.
    • Lincoln Electric consumables storage and handling guidance for covered electrodes and moisture-resistant packaging.
    • Weld Support Parts stick welding support articles on 7018 moisture contamination, 7018 sticking, 6010 vs 7018 selection, and fume extraction troubleshooting.
  • 7018 Rod Moisture Contamination Troubleshooting: Porosity, Rod Sticking, Arc Instability, and Hydrogen Cracking Risk

    7018 rod moisture contamination is a low-hydrogen failure, not just a storage inconvenience. Damp E7018 electrodes can cause porosity, rough arc starts, excessive spatter, slag trouble, underbead cracking risk, and welds that fail inspection even when the bead looks acceptable. If 7018 rods have been left open in humidity, stored in a toolbox, rained on, or mixed with high-moisture rods, treat them as suspect before welding structural, code, pressure, lifting, or restrained joints.

    The fast field decision is simple: use fresh rods from a sealed container for critical work, keep opened low-hydrogen rods in a rod oven, and do not assume a warm shop shelf or sealed plastic tube restores low-hydrogen condition. If rods are wet, oily, rusty, chipped, or unknown, discard them for critical work. Reconditioning must follow electrode manufacturer and code requirements, not a torch, microwave, job box, truck dash, or improvised heater.

    Related stick welding checks include 7018 rod sticking causes, 6010 vs 7018 storage differences, rod oven storage support, and 7018 electrode support.

    Common Symptoms

    SymptomLikely Moisture LinkFirst Check
    Porosity or pinholesHydrogen/moisture in coating or contaminated jointUse fresh oven-held rods and clean base metal
    Rod sticks on startsDamp coating, low amperage, poor restart prepTry known-dry rod at correct amperage
    Rough unstable arcMoisture-altered coatingCompare sealed rods against suspect rods
    Excess spatterDamp coating or wrong arc length/amperageCheck rod storage and machine settings
    Slag acts glassy or irregularFlux coating condition problemInspect coating for chips, cracks, dampness
    Delayed crackingHydrogen in restrained/high-strength weldStop using exposed rods for critical work

    Why Moisture Matters on 7018

    E7018 is designed as a low-hydrogen electrode. Its coating must stay dry so the weld deposit stays low in diffusible hydrogen. When the coating absorbs moisture, hydrogen can enter the weld metal and heat-affected zone. That matters most on thicker steel, high-strength steel, cold material, restrained joints, hardenable base metal, repair welds, and code work where hydrogen cracking risk must be controlled.

    Quick Checks

    • Package condition: Use rods from intact hermetically sealed or manufacturer-approved packaging for critical work.
    • Exposure history: If the rod exposure time is unknown, treat it as Unknown (Verify), not acceptable.
    • Surface condition: Reject rods with cracked, chipped, swollen, oily, rusty, or soft coatings.
    • Storage oven: Opened 7018 should be stored in a holding oven at the manufacturer/code-required temperature.
    • Comparison test: Strike a fresh dry rod and a suspect rod on clean scrap. Rough arc, spatter, sticking, or porosity points to rod condition.
    • Job requirement: If the weld is structural or code-controlled, follow WPS, AWS code, and electrode manufacturer instructions.

    Inspection Steps

    1. Identify the electrode. Confirm E7018, E7018-1, E7018 H4R, E7018M, or other exact classification and brand.
    2. Check the container. Confirm whether the package was sealed, vacuum packed, damaged, or previously opened.
    3. Verify exposure time. Record how long rods were outside the oven and the shop humidity/rain exposure.
    4. Inspect the coating. Look for cracks, chips, powdering, swelling, discoloration, oil, rust, or soft flux.
    5. Separate suspect rods. Do not mix them back into the dry low-hydrogen oven inventory.
    6. Check the rod oven. Verify temperature with a reliable thermometer, not just the dial setting.
    7. Confirm rebake rules. Use the electrode manufacturer and job code. Do not invent a rebake schedule.
    8. Run a controlled test only for noncritical screening. Test beads cannot prove low-hydrogen compliance.
    9. Document disposition. Mark rods as fresh, oven-held, rebaked per procedure, downgraded to noncritical use, or discarded.

    Storage and Reconditioning Notes

    Low-hydrogen electrodes commonly require storage in a holding oven after opening. Manufacturer guidance often places low-hydrogen holding ovens in the 225–300°F range, but the exact temperature and exposure limits depend on electrode class, moisture-resistant suffix, manufacturer, and code. Some exposed rods may be rebaked one time under controlled conditions. Rods that became wet, oil-contaminated, cracked, or physically damaged should not be trusted for critical welds.

    Field Fix vs Proper Fix

    ConditionField FixProper Fix
    Opened rods sat out overnightUse fresh sealed rods for critical workFollow manufacturer/code rebake or discard rule
    Rods exposed to rainRemove from low-hydrogen stockDiscard for code/critical work unless procedure permits otherwise
    Rod sticks and spattersCheck amperage and try fresh rodCorrect storage, oven temp, and rod handling
    No rod oven availableUse sealed rods only as openedAdd approved holding oven and exposure log
    Mixed 6010 and 7018 in one warm boxSeparate immediatelyStore low-hydrogen rods separately at required temperature

    Common Wrong-Part and Wrong-Process Mistakes

    • Using damp 7018 on restrained structural joints because the bead still looks smooth.
    • Storing 6010/6011 cellulosic rods in the same oven as 7018 low-hydrogen rods.
    • Believing sealed plastic tubes equal a code-compliant rod oven.
    • Rebaking rods without confirming the electrode classification and manufacturer rule.
    • Using exposed 7018 for pressure, lifting, structural, or code welds without WPS approval.
    • Blaming amperage for sticking when the rod coating is damp or damaged.

    What To Verify Before Welding

    • Electrode classification and brand.
    • Whether the package was factory sealed or already opened.
    • Rod oven temperature and calibration status.
    • Maximum allowed exposure time from the WPS/code/manufacturer.
    • Whether rebake is allowed and exact rebake schedule.
    • Base metal strength, thickness, restraint, preheat, and hydrogen-cracking risk.
    • Whether the job permits reconditioned rods or requires fresh sealed/oven-held electrodes.

    Related Failure Paths

    • Porosity from hydrogen/moisture contamination.
    • Rod sticking from damp coating and unstable starts.
    • Delayed hydrogen cracking in restrained or high-strength welds.
    • Slag irregularity from damaged coating.
    • Arc instability from wrong current, poor ground, or wet rods.
    • Failed inspection from undocumented electrode exposure control.

    Safety Notes

    • Do not use wet or unknown 7018 rods for critical welds.
    • Do not heat rods with open flame, torches, microwaves, or uncontrolled shop heaters.
    • Use rod ovens according to manufacturer instructions and electrical safety requirements.
    • Use ventilation and keep your head out of welding fumes.
    • Follow the WPS, AWS code, engineer, or inspector requirement when low-hydrogen control is specified.

    Sources Checked

    • Lincoln Electric low-hydrogen electrode storage and redrying guidance.
    • ESAB low-hydrogen electrode storage and redrying guidance.
    • Weld Support Parts 7018 sticking, 6010 vs 7018, rod oven, and 7018 electrode pages.
    • Hobart 7018 electrode performance guidance.
  • ESAB MIG Gas Flow Troubleshooting: Porosity, Nozzle Blockage, Gas Leaks, Flowmeter Settings, and Torch Checks

    ESAB MIG gas flow problems usually show up as porosity, pinholes, black soot, popping starts, oxidized welds, or welds that look contaminated even when the wire feed feels normal. On ESAB Rebel, Rogue, Fabricator, and Tweco-style MIG gun setups, check the gas cylinder, regulator/flowmeter, rear gas hose, machine gas valve, torch connection, diffuser, nozzle, gun cable, and weld-area drafts before changing drive rolls or replacing the liner.

    Gas trouble is not always low flow. Too much flow can create turbulence, a spatter-packed nozzle can choke coverage, a loose rear fitting can leak before gas reaches the gun, and wind can strip shielding from the puddle. Pull the trigger, confirm steady gas at the nozzle, inspect the diffuser ports and nozzle bore, soap-test external fittings, then run a clean indoor test weld with fans off.

    Related MIG support checks include nozzle spatter and blocked gas flow, MIG consumable inspection, welding troubleshooting checks, and MIG wire feed stuttering fixes.

    Common Symptoms

    SymptomLikely CauseFirst Check
    Pinholes or wormholesAir entering weld pool, low/unstable gas, contaminationConfirm gas at nozzle and clean base metal
    Black soot around beadWrong gas, poor coverage, dirty material, excessive stickoutVerify gas type and nozzle position
    Porosity comes and goesLoose fitting, damaged hose, drafts, intermittent gas valveSoap-test fittings and weld indoors
    No gas heard at nozzleClosed cylinder, empty bottle, regulator closed, blocked hose, valve faultCheck cylinder, regulator, and inlet hose
    Flowmeter moves but weld is porousLeak after regulator, blocked diffuser/nozzle, windCheck torch connection and front-end parts
    Porosity near corners or edgesShielding envelope pulled away by joint geometry or gun angleAdjust angle, stickout, and nozzle distance

    What the ESAB MIG Gas System Does

    The shielding gas system protects the molten MIG weld pool from oxygen, nitrogen, and moisture in air. Gas must travel from the cylinder through the regulator/flowmeter, gas hose, machine inlet, solenoid valve, torch connection, torch cable, diffuser, and nozzle. A restriction, leak, wrong part, or blocked gas port anywhere in that path can create the same visible defect at the bead.

    Quick Checks

    • Cylinder: Confirm the bottle is not empty and the valve is open.
    • Gas type: Verify the shielding gas matches wire and process. Do not run solid steel MIG with 100% argon.
    • Flowmeter: Set flow with the trigger pulled, not just at static pressure.
    • External leaks: Use leak-detection solution or soapy water on cylinder/regulator/hose fittings.
    • Nozzle: Remove spatter, anti-spatter gel buildup, slag, or deformation that disrupts coverage.
    • Diffuser: Replace if gas holes are blocked, damaged, or uneven.
    • Work area: Turn off fans and block drafts before blaming the welder.

    Inspection Steps

    1. Secure the cylinder upright. Never troubleshoot with an unsecured shielding-gas cylinder.
    2. Confirm gas and wire match. C25 or CO2 may be used for many mild-steel short-circuit setups; stainless, aluminum, and specialty wires require different gas guidance.
    3. Open the cylinder and set the flowmeter. Pull the trigger and watch for stable flow while gas is moving.
    4. Listen and feel at the nozzle. You should have steady gas at the front end before welding.
    5. Inspect the nozzle bore. Clean or replace if spatter is reducing the opening or causing uneven gas direction.
    6. Inspect diffuser ports. Spatter inside the diffuser can make gas flow out one side and leave the puddle exposed.
    7. Check the torch connection at the machine. Loose seating, damaged O-rings, or wrong rear connector can leak gas before it reaches the gun.
    8. Inspect gas hoses. Look for cracked hose, loose clamps, kinked line, blocked inlet hose, or damage from heat and grinding.
    9. Check gun angle and stickout. Long stickout and excessive push/pull angle can move the nozzle too far from the puddle.
    10. Run a controlled test bead. Use clean scrap indoors, same wire/gas, fans off, and one setting change at a time.

    Flow Rate Notes

    Use the ESAB manual, wire data sheet, and procedure as the final authority. ESAB defect guidance commonly references proper shielding coverage and a typical MIG gas-flow range around 25–40 CFH, but the correct setting depends on gas mix, nozzle bore, amperage, wire size, joint access, travel speed, and air movement. Do not fix wind by cranking flow excessively; high flow can become turbulent and pull air into the shielding envelope.

    Compatibility Notes

    Do not order ESAB MIG gas parts by machine name alone. Rebel EMP/EM machines, Fabricator machines, Rogue MIG units, and replacement Tweco-style guns can use different rear connectors, nozzles, diffusers, contact tips, liners, and gas seals. WSP lists a general ESAB MIG machine support page, but Rebel-specific gas-flow parts should be verified by exact machine model, serial/product number, and installed torch.

    If a Rebel has a replacement Tweco-style gun, verify the actual gun before ordering front-end parts. WSP’s Tweco Fusion 180 gun breakdown lists Rebel rear-connector versions and separate gun consumable references, which means the torch identity matters. A gasless flux-core nozzle, wrong diffuser, missing O-ring, or loose gun connection can all cause MIG gas coverage complaints.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Nozzle packed with spatterClean bore and retestReplace nozzle and inspect diffuser/tip seating
    Loose hose fittingTighten fitting and soap-testReplace damaged hose, clamp, or fitting
    Porosity outdoorsBlock windUse correct process control, wind protection, or self-shielded wire where appropriate
    Unstable gas flowCheck bottle and regulatorInspect regulator, solenoid, hose, and torch gas path
    Wrong gas mixStop and swap cylinderDocument gas/wire/material setup for repeat jobs

    Common Wrong-Part Mistakes

    • Using a gasless flux-core nozzle while trying to run solid wire with shielding gas.
    • Ordering nozzles or diffusers by “ESAB Rebel” instead of installed torch model.
    • Replacing the liner when porosity is from a blocked diffuser or loose gas fitting.
    • Using 100% argon for short-circuit mild-steel MIG.
    • Increasing CFH too high and creating turbulent shielding.
    • Ignoring a damaged gun O-ring or loose torch connector.

    What To Verify Before Ordering

    • Exact ESAB machine model and serial/product number.
    • Installed MIG gun brand, model, rear connector, and cable length.
    • Nozzle type, bore size, and recess/flush/stickout style.
    • Gas diffuser type and condition.
    • Contact tip series and wire size.
    • Gas hose size, fittings, clamps, and O-rings.
    • Shielding gas type and flowmeter/regulator condition.
    • Whether the machine is being used with solid wire, gas-shielded flux-core, or self-shielded flux-core.

    Safety Notes

    • Secure gas cylinders upright with caps installed during transport.
    • Do not use damaged regulators, flowmeters, hoses, or fittings.
    • Keep shielding gas away from confined-space oxygen-displacement hazards.
    • Use ventilation and keep your head out of welding fumes.
    • Disconnect input power before internal machine service.
    • Use leak-detection solution, not open flame, to check fittings.

    Sources Checked

    • ESAB Rebel EMP 215ic / EM 215ic instruction manual.
    • ESAB GMAW porosity guidance.
    • ESAB MIG defect troubleshooting guidance.
    • Weld Support Parts ESAB MIG support and Tweco Fusion gun pages.
    • Weld Support Parts MIG nozzle, consumable, and troubleshooting pages.
  • TIG Post-Flow Setting Troubleshooting: Black Tungsten, Porosity, Gas Waste, and Torch Cooling

    TIG post-flow is the shielding gas that keeps flowing after the arc stops. If it is too short, the hot tungsten and cooling weld crater are exposed to air, causing black, blue, gray, or crusty tungsten, rough restarts, porosity, and contaminated weld starts. If post-flow is too long, weld quality may be fine, but argon usage goes up fast during tack welding or short beads.

    Start by watching the tungsten after arc stop. If the tungsten is still glowing when argon shuts off, increase post-flow. If the tungsten stays clean but gas keeps flowing long after the torch cools, reduce post-flow in small steps. Do not fix black tungsten by only increasing flow rate; a cracked cup, leaking back cap O-ring, clogged gas lens, or loose torch fitting can still expose the electrode to oxygen.

    Related TIG checks include why TIG tungsten turns black, TIG porosity troubleshooting, sooty TIG weld gas coverage fixes, and TIG cup size and gas lens selection.

    Common Symptoms

    SymptomLikely Post-Flow IssueFirst Check
    Tungsten turns black after weldPost-flow too short or gas leakIncrease post-flow and inspect gas path
    Tungsten turns blue or grayHot tungsten exposed during coolingWatch whether gas stops before glow is gone
    Rough arc restartOxidized tungsten from previous stopRegrind tungsten and extend post-flow
    Porosity at crater or restartWeld pool loses shielding while coolingHold torch over crater during post-flow
    Argon bottle empties quicklyPost-flow too long for short weldsReduce time gradually after tungsten stays clean

    What Post-Flow Does

    Post-flow protects three hot areas after the arc shuts off: the tungsten, the weld crater, and the end of the filler rod if it remains inside the gas envelope. Tungsten can oxidize after the bead looks finished because the electrode remains hot longer than many operators expect. The goal is enough shielding to let the tungsten cool without discoloration, not maximum gas flow for every weld.

    Starting Point for Post-Flow

    A common field rule is about 1 second of post-flow per 10 amps of welding current. Some Miller GTAW guidance also lists 10–15 seconds as a corrective range when inadequate post-flow is causing tungsten or arc problems. Use those as starting points, then tune by tungsten color, material, torch heat, tungsten size, and weld length.

    Welding CurrentCommon Starting RangeWhat To Watch
    50 amps5 secondsTungsten should not color after gas stops
    80 amps8 secondsGood range for many light TIG jobs
    120 amps12 secondsCheck torch heat and tungsten color
    150 amps15 secondsOften needs longer protection on hot torch setups
    200 amps20 secondsVerify torch rating and cooling; gas use increases quickly

    Inspection Steps

    1. Confirm the gas. Most TIG work uses 100% argon. Do not use MIG gas with CO2 or oxygen for TIG.
    2. Watch tungsten color. Black, gray, blue, or crusted tungsten after arc stop points to oxygen exposure, contamination, or too little post-flow.
    3. Hold the torch still. Keep the cup over the crater until post-flow ends. Moving away early defeats the setting.
    4. Check flow at the cup. A regulator reading does not prove gas is reaching the tungsten.
    5. Inspect the cup. Replace cracked, chipped, loose, or overheated cups.
    6. Inspect the gas lens or collet body. Blocked screens or damaged gas passages can cause poor coverage even with long post-flow.
    7. Check the back cap O-ring. A damaged O-ring can pull air into the torch and oxidize tungsten.
    8. Check hoses and fittings. Use approved leak-check methods and repair leaks before welding.
    9. Adjust gradually. Add or subtract a few seconds at a time, then retest on clean material.

    Post-Flow Too Short vs Too Long

    ConditionResultCorrective Action
    Too shortBlack tungsten, rough restarts, crater oxidationIncrease time and hold torch over weld
    Too longHigh argon consumption with no quality gainReduce time after tungsten remains clean
    Correct time but black tungstenLeak, cracked cup, bad O-ring, dirty gas lensInspect torch and gas path
    Correct time but porosityDraft, contamination, wrong cup, no purgeCheck shielding coverage and base-metal prep

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Tungsten blackens after stopAdd post-flow timeSet time by amps and repair leaks or worn torch parts
    Gas wastes during tacksLower post-flow slightlyUse a repeatable tack schedule that still protects tungsten
    Crater porosityHold torch over crater longerCorrect post-flow, torch angle, cup size, and cleanliness
    Blue tungsten on aluminumAdd post-flowCheck AC heat, torch cooling, gas lens, and cup size
    Soot remains after increasing post-flowClean cup and tungstenFix gas coverage, contaminated material, or wrong gas

    Common Wrong-Part Mistakes

    • Replacing tungsten repeatedly while ignoring a leaking back cap O-ring.
    • Using a cracked cup and trying to compensate with longer post-flow.
    • Installing gas lens parts that do not match the torch series or cup setup.
    • Using a collet that does not match tungsten diameter, causing poor alignment and overheating.
    • Turning gas flow too high and creating turbulence instead of fixing post-flow time.

    Compatibility Notes

    Post-flow is a machine setting, but the correct result depends on torch family, cup size, gas lens or standard collet body, tungsten diameter, amperage, material, and torch cooling. Consumables for WP-9/20-style torches and WP-17/18/26-style torches are not automatically interchangeable. Verify torch series and tungsten diameter before replacing cups, collets, gas lenses, or back caps.

    Related Failure Paths

    • Black tungsten from oxygen exposure after arc stop.
    • Rough arc starts from oxidized tungsten.
    • TIG porosity at crater or restart.
    • Sooty TIG welds caused by poor gas coverage.
    • Cracked cups or clogged gas lenses mistaken for bad post-flow.
    • High argon use from excessive post-flow during tack welding.

    Safety Notes

    • Let tungsten, cups, and torch parts cool before handling.
    • Secure argon cylinders upright and protect regulators from impact.
    • Argon can displace oxygen in confined areas; use ventilation and confined-space controls where required.
    • Use eye protection when grinding tungsten.
    • Do not weld through suspected gas leaks or damaged hoses.

    Sources Checked

    • Weld Support Parts TIG tungsten discoloration support page.
    • Weld Support Parts TIG porosity and soot troubleshooting pages.
    • Weld Support Parts TIG cup size and gas lens support page.
    • CK Worldwide TIG troubleshooting and gas shielding guidance.
    • Miller GTAW troubleshooting guidance.
  • More posts

    Listen with Audible