Search results for: “plasma cutter parts”

  • Hobart AirForce 27i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 27i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 27i Plasma Cutter Support

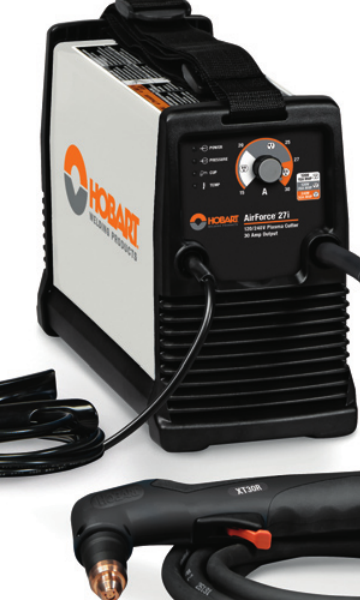
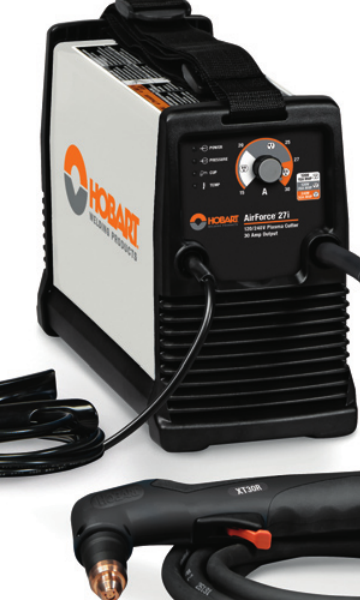
    If you maintain a Hobart AirForce 27i, the fastest way to avoid wrong-parts orders is to verify the machine identifier, torch family, power input, and air-side support items before you buy. The AirForce 27i support page from Weld Support Parts is set up as a lookup starting point for those checks. It lists the unit support page, the stock reference 500575, 120/240 V information, an XT30R replacement torch reference, consumables, MVP adapters, an air filter kit, cutting guides, and plasma support links.

    Key Takeaways

    • Use the support page to confirm the AirForce 27i parts path before ordering.
    • Verify torch model, consumable style, and power input at the machine nameplate and on the existing torch.
    • Air quality matters. Inspect the air filter path before troubleshooting arc problems.
    • Do not assume adapter or torch compatibility from appearance alone.
    • When details are unclear, mark them as Unknown (Verify) and confirm against the machine and torch labels.

    What the Support Page Is Useful For

    The Weld Support Parts AirForce 27i page is a parts lookup and support reference, not a substitute for the machine manual. It is useful when you need to match the cutter to support items such as the replacement torch, consumables, and air-side accessories. For this model, the page references stock 500575 and indicates 120/240 V support information. Treat those details as lookup cues and verify them on the machine before purchasing or installing parts.

    Open the Hobart AirForce 27i support page

    Buying Checks Before You Order Parts

    Before a maintenance buyer releases an order, do these checks in order:

    1. Check the machine data plate. Verify the exact model is Hobart AirForce 27i and confirm input power requirements. If the plate is unclear, record Unknown (Verify).
    2. Inspect the torch neck and handle label. Confirm whether the installed torch matches the XT30R family reference shown on the support page. Do not assume the torch is original.
    3. Pull the consumable set and compare wear patterns. Look at the nozzle, electrode, swirl ring, shield, and retaining parts. Replace only with the correct style for the torch in use.
    4. Check the air delivery path. Inspect filters, fittings, hoses, and water or oil contamination. A plasma cutter with poor air quality will often show unstable arc behavior.
    5. Confirm adapter needs. If the shop uses an alternate power plug or input arrangement, check whether the MVP adapter reference is relevant to your setup. Compatibility details not shown on the support page should stay Unknown (Verify).

    Troubleshooting and Support Checks

    Use these checks when the cutter starts to misbehave or when you are deciding which support part to buy.

    1) Torch and Consumable Check

    • Inspect: Look for heat damage, cracked cups, eroded electrodes, and loose retaining parts.
    • Verify: Match the torch consumables to the actual torch family on the machine. If the torch label is unreadable, mark the torch type Unknown (Verify) until confirmed.
    • Replace: Only the parts that are visibly worn or listed for the identified torch family.

    2) Air Supply Check

    • Inspect: Air filter kit condition, bowl contamination, hose leaks, and regulator settings.
    • Verify: The shop air is dry and clean enough for plasma use. If you see oil, water, or heavy debris, correct that before blaming the torch.
    • Check: Flow remains stable during trigger pull. A pressure drop can mimic a bad torch or bad consumable.

    3) Power and Input Check

    • Inspect: Input cord, plugs, adapters, and receptacle condition.
    • Verify: The machine is connected to the correct input class shown for the AirForce 27i support reference. If the exact electrical setup is not confirmed, note it Unknown (Verify).
    • Check: Any adapter or extension is rated and approved for the actual jobsite setup. Do not use an adapter just because the plug shape fits.

    4) Cut Quality Check

    • Inspect: Edge squareness, dross, and arc consistency.
    • Verify: The torch is held at a consistent standoff and travel speed.
    • Check: The cut guide or drag shield is appropriate for the work method you are using.

    WSP Lookup Page Notes

    The AirForce 27i support page is the correct first stop when you need a parts and support overview for this machine. It identifies the machine support page, stock 500575, the XT30R replacement torch reference, consumables, MVP adapters, air filter kit, cutting guides, and other plasma support links. Use those references to narrow the search, then confirm exact fitment against the machine and torch markings.

    Important: This page is a selection aid, not a blanket approval for every installed torch or accessory. If the part family is not confirmed from labels or existing component markings, the correct status is Unknown (Verify).

    Go to the Hobart AirForce 27i support page

    Practical Inspection Routine for Shops

    For routine maintenance, use a short inspection routine before each parts order or service ticket:

    • Record the machine model and serial tag information.
    • Compare torch markings to the support page reference.
    • Pull the last installed consumables and note wear pattern.
    • Inspect air filters and moisture traps.
    • Check the power plug, adapters, and cord strain relief.
    • Confirm any cutting guides or accessories are intended for the actual torch setup.

    Safety Notes

    • De-energize the machine before inspecting internal or electrical components.
    • Bleed pressure from the air system before opening filters or fittings.
    • Do not touch hot consumables immediately after cutting.
    • Use eye, hand, and body protection suitable for plasma cutting and grinding cleanup.
    • Do not bypass safety devices or use unverified adapters in an attempt to make a part fit.

    FAQ

    Is the XT30R replacement torch definitely the correct torch for every AirForce 27i?

    No. The support page references XT30R as a replacement torch reference, but you should still verify the torch family on the machine and existing torch. If the installed torch is not confirmed, mark it Unknown (Verify).

    Can I order consumables just by machine model?

    Not safely. Consumables must match the actual torch family and installed setup. Start with the AirForce 27i support page, then verify the torch label and worn parts before ordering.

    What should I check first if the cutter will not make a stable arc?

    Start with the consumables and the air supply. Inspect electrode and nozzle wear, then verify that air is clean, dry, and steady. If those checks are inconclusive, move to power input and torch condition.

    Are the MVP adapters universal?

    Do not assume that. The support page lists MVP adapters as a support reference, but any actual compatibility must be confirmed against the machine and power setup. If it is not confirmed, use Unknown (Verify).

    Sources Checked

    For maintenance teams, the key is simple: verify the machine, verify the torch, verify the air, then buy the parts that match what is actually installed. That is the cleanest way to support a Hobart AirForce 27i without creating avoidable returns or downtime.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

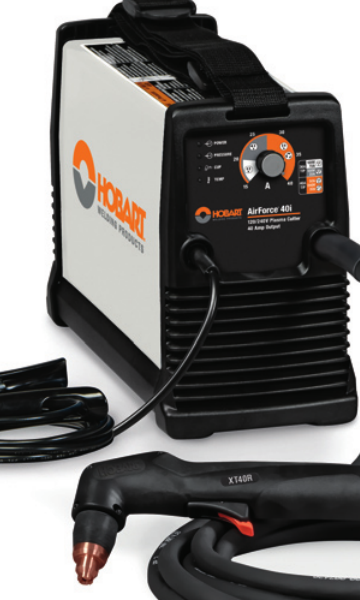
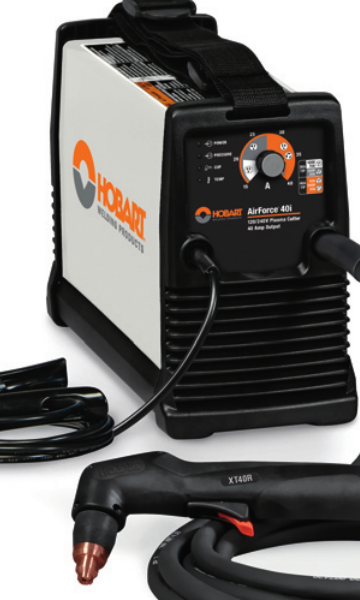
  • Hobart AirForce 40i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 40i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 40i Plasma Cutter Support

    The Hobart AirForce 40i is a compact plasma cutter support topic that usually comes down to four checks: input power, torch condition, consumable wear, and air quality. If the machine is cutting poorly or not starting, the fastest path is to verify the torch setup and the air supply before replacing parts. This guide is built for parts lookup and buying checks, not a repair manual. Use it to confirm what to inspect, what to match, and what to verify before ordering.

    Key Takeaways

    • Confirm the machine identification and stock reference before ordering any support part.
    • The listed support page for this unit references a replacement XT40R torch, consumables, MVP adapters, an air filter kit, and cutting guide support.
    • Do not assume a torch, adapter, or consumable is correct from appearance alone. Verify by model reference and connector style.
    • For cutting problems, check air pressure/flow, torch consumables, lead condition, and work lead attachment before replacing the power source.
    • Use the WSP lookup page as the primary reference for the support page and linked parts path.

    What to verify first on a Hobart AirForce 40i

    Start with the machine nameplate and the support reference. The provided WSP lookup page identifies the Hobart AirForce 40i support page with stock 500576 and 120/240 V specifications. Verify the exact unit label on your machine, because buying decisions depend on the input version and the torch package, not just the model name. If the machine has been moved between shops, it may be wired differently than expected. Unknown (Verify) whether your specific installation is set up for 120 V or 240 V service until you check the nameplate and receptacle.

    Check: machine name, serial or stock reference, input voltage, torch type, and connector style.

    Inspect: power cord, plug, torch lead, trigger cable, and air line for damage or heat discoloration.

    Verify: the torch package against the support page before ordering consumables or adapters.

    Troubleshooting and support checks

    1) No start or weak arc

    If the torch does not initiate, or the arc starts weakly and drops out, isolate the basics first.

    • Check that the machine is powered correctly and the breaker is not marginal under load.
    • Inspect the torch tip, electrode, and swirl ring for wear, erosion, or contamination.
    • Verify the air supply is dry and clean. Moisture or oil can shorten consumable life and cause arc instability.
    • Check the work clamp connection and the cut table contact path.

    If the torch parts are visibly worn, replace the full consumable set rather than mixing old and new parts. Mixed wear states can make troubleshooting harder.

    2) Poor cut quality

    When the machine starts but cut quality is inconsistent, focus on air and consumables before assuming a power source fault.

    • Inspect the nozzle for oval wear or spatter damage.
    • Check whether the torch stand-off or hand motion is too fast or too slow for the material being cut.
    • Verify the air filter kit condition if water or debris is present in the line.
    • Inspect the torch lead for cuts, tight bends, or repeated abrasion at the work area.

    Do not buy replacement parts until you confirm which failure mode is present. A bad nozzle, dirty air, and low input power can produce similar symptoms.

    3) Torch and adapter fit checks

    The support page references an XT40R replacement torch and MVP adapters. Those items should be treated as model-specific support parts. Before ordering, match the torch family, connector interface, and any adapter callout shown on the support page. Unknown (Verify) whether any adapter is required for your existing setup until you confirm the current torch package and machine configuration.

    • Check the printed torch model reference.
    • Inspect the connector ends for wear, bent pins, or damaged locking features.
    • Verify the replacement torch is the exact support path listed for this machine.

    WSP lookup page: use it as the starting point

    The provided WSP lookup page is the main source for this support topic:

    Hobart AirForce 40i Plasma Cutter Support

    Use that page to confirm the machine support path, the stock 500576 reference, and the listed support categories. The page references consumables, XT40R replacement torch support, MVP adapters, an air filter kit, cutting guides, and related plasma support links. That makes it a parts lookup starting point, not a blanket approval for every accessory you may see elsewhere.

    Buying check: match the item to the machine and torch package before adding it to a quote or cart.

    Verify: whether the part is a direct replacement, a service accessory, or a support accessory that only applies to a specific configuration.

    Practical part selection checks

    • Consumables: replace as a set when wear is visible or cut quality changes.
    • Torch assembly: confirm the torch model before ordering. Do not assume a different torch in the same family will fit without verification.
    • Air filter kit: choose this when the air line shows moisture, particulate, or oil contamination.
    • MVP adapters: verify the machine-side and torch-side connection points before buying.
    • Cutting guides: confirm the guide style works with your hand technique and work envelope.

    Safety notes

    Plasma cutters involve high voltage, hot metal, compressed air, and intense arc radiation. Disconnect input power before opening access panels or handling internal connections. Bleed stored air pressure before servicing the air system. Replace damaged torch leads or worn consumables before operation. Use approved eye, face, hand, and body protection for plasma cutting. Keep the work area dry and free of flammables.

    FAQ

    What is the first part I should inspect on an AirForce 40i with arc issues?

    Inspect the consumables first, then verify air quality and work lead connection. Those are the most common support checks before replacing the torch or power source.

    Can I order a replacement torch from appearance alone?

    No. Verify the torch model reference and connector style first. The support page references an XT40R replacement torch, but you should confirm the exact machine and torch package before buying.

    Do the listed accessories mean every item is required?

    No. The support page is a parts lookup starting point. Some items, such as an air filter kit or MVP adapter, may only be needed if your current setup has a matching need. Verify against your machine configuration.

    How do I know if the input power is correct?

    Check the machine nameplate and the site wiring. The provided support page references 120/240 V specifications, but your installed service must still be verified at the machine and receptacle.

    Sources Checked

    Use the support page as the primary reference, then verify the machine condition and part match before ordering. That reduces avoidable returns and prevents mismatched torch or consumable purchases.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

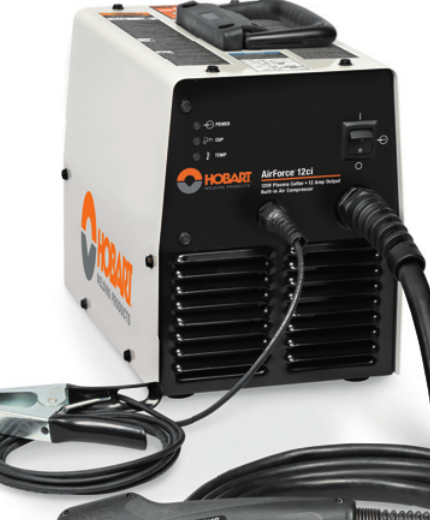
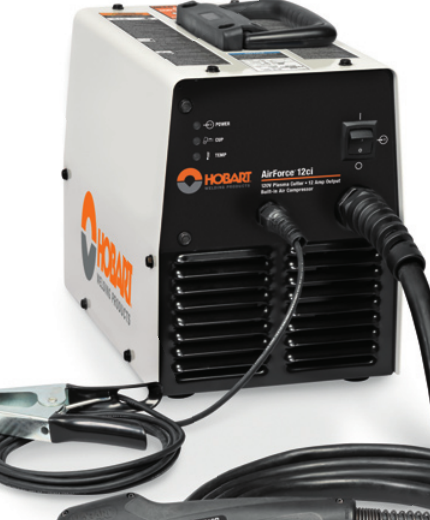
  • Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 12ci Plasma Cutter Support

    The Hobart AirForce 12ci is a compact plasma cutter support case where the buying risk is usually not the cutter itself, but the parts that keep it running: torch fitment, consumables, protective gear, and whether the replacement item matches the machine’s input and torch family. This guide is built to help welders, fabricators, and maintenance buyers verify the basics before ordering.

    Key Takeaways

    • Use the Hobart AirForce 12ci support page as the first parts reference before you buy.
    • Verify torch model, consumable type, and input power before ordering any replacement item.
    • Do not assume a plasma torch, consumable kit, or cover fits because it looks similar.
    • Check wear items first: nozzle, electrode, shield, swirl ring, retaining parts, air supply, and cable condition.
    • Safety glasses and a protective cover are support items, not optional extras.

    Start with the WSP lookup page

    The primary support page for this unit is here: Hobart AirForce 12ci Plasma Cutter Support. The page indicates stock 500564 and lists 120 V specs, XT12R replacement torch, consumable kits, safety glasses, and a protective cover. Treat those listings as the starting point for verification, not as a substitute for checking your exact machine and torch tag.

    Check before you order

    • Inspect the machine label: confirm the model is Hobart AirForce 12ci, not a similar unit.
    • Verify input power: the support page shows 120 V specs. Confirm your unit nameplate and outlet setup match.
    • Inspect the torch tag: confirm whether the unit uses the XT12R replacement torch listed on the support page.
    • Check consumable wear: look for recessed electrode, enlarged nozzle orifice, heat damage, cracks, or unstable arc start.
    • Verify cable and lead condition: cuts, melted sections, or loose strain reliefs can mimic consumable failure.

    Troubleshooting and support checks

    If the cutter is not performing well, the fastest path is a basic inspection sequence. Start simple and document what you find.

    1) No start or weak start

    • Check: power source status, plug condition, and supply voltage at the receptacle.
    • Inspect: trigger switch, torch lead, and any visible torch damage.
    • Verify: the consumables are installed correctly and are not worn beyond serviceable condition.

    2) Arc starts but cut quality is poor

    • Check: air pressure and air quality at the cutter.
    • Inspect: nozzle, electrode, shield, and retaining parts for spatter buildup or heat distortion.
    • Verify: the work clamp is clean and attached to bare metal.

    3) Arc drops out during cutting

    • Check: thermal condition of the machine and duty cycle usage pattern.
    • Inspect: torch lead for intermittent breaks or damaged insulation.
    • Verify: the air supply is steady and dry. Moisture can cause unstable operation and consumable damage.

    4) Consumables wear too quickly

    • Check: cutting technique, standoff distance, and travel speed.
    • Inspect: whether the nozzle is being run beyond normal wear indicators.
    • Verify: you are using the correct consumable kit for the torch family. If uncertain, use Unknown (Verify) until the exact kit is matched.

    Parts lookup buying checks for this model

    For the Hobart AirForce 12ci, the most useful parts categories are torch replacement, consumable kits, and protective items. The support page points to an XT12R replacement torch, but buyers should verify the torch family, connector style, and lead length against the existing machine before ordering. Unknown (Verify) should be used for any detail that is not confirmed by the machine label or the support page.

    Replacement torch check

    • Inspect: the old torch for model markings, connector type, and damage location.
    • Verify: the new torch is listed for the same support page and matches the original torch family.
    • Confirm: no modification is required for fitment unless the manufacturer states otherwise.

    Consumable kit check

    • Inspect: all wear components removed from the torch.
    • Compare: thread shape, size, and seating surfaces.
    • Verify: the kit is intended for the same torch model, not just a similar plasma system.

    Protective gear and cover

    • Check: whether the shop already stocks plasma-rated eye protection.
    • Inspect: the machine’s storage location for dust, slag, and moisture exposure.
    • Verify: a protective cover will not trap heat when the machine is warm after use.

    Use the internal guides as support references

    If the cutter is giving you symptoms beyond basic wear, these related articles can help narrow the fault before you order parts:

    Safety notes

    • Disconnect power before inspecting torch leads, consumables, or internal connections.
    • Use eye protection and hand protection when checking the torch or removing worn parts.
    • Do not use damaged leads, cracked torch bodies, or loose consumable assemblies.
    • Verify ventilation and keep flammables clear of the cutting area.
    • If a part fitment is uncertain, mark it Unknown (Verify) and confirm through the machine label, torch tag, or support listing before use.

    FAQ

    What should I verify first for Hobart AirForce 12ci parts?

    Verify the machine model, input power, and torch family first. Then check consumables, cable condition, and air supply quality.

    Is the XT12R replacement torch listed on the support page the correct part for every unit?

    Unknown (Verify). The support page lists XT12R, but you should confirm the torch tag and connector style on your specific machine before ordering.

    How do I know if the problem is consumables or the torch?

    Inspect the nozzle, electrode, and shield first. If wear is visible or the arc is unstable, consumables are often the first suspect. If the lead, trigger, or torch body is damaged, the torch may need replacement.

    Can I buy based on similar-looking plasma parts?

    No. Similar appearance does not confirm fitment. Match the part to the support page and the machine tag, then verify before purchasing.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

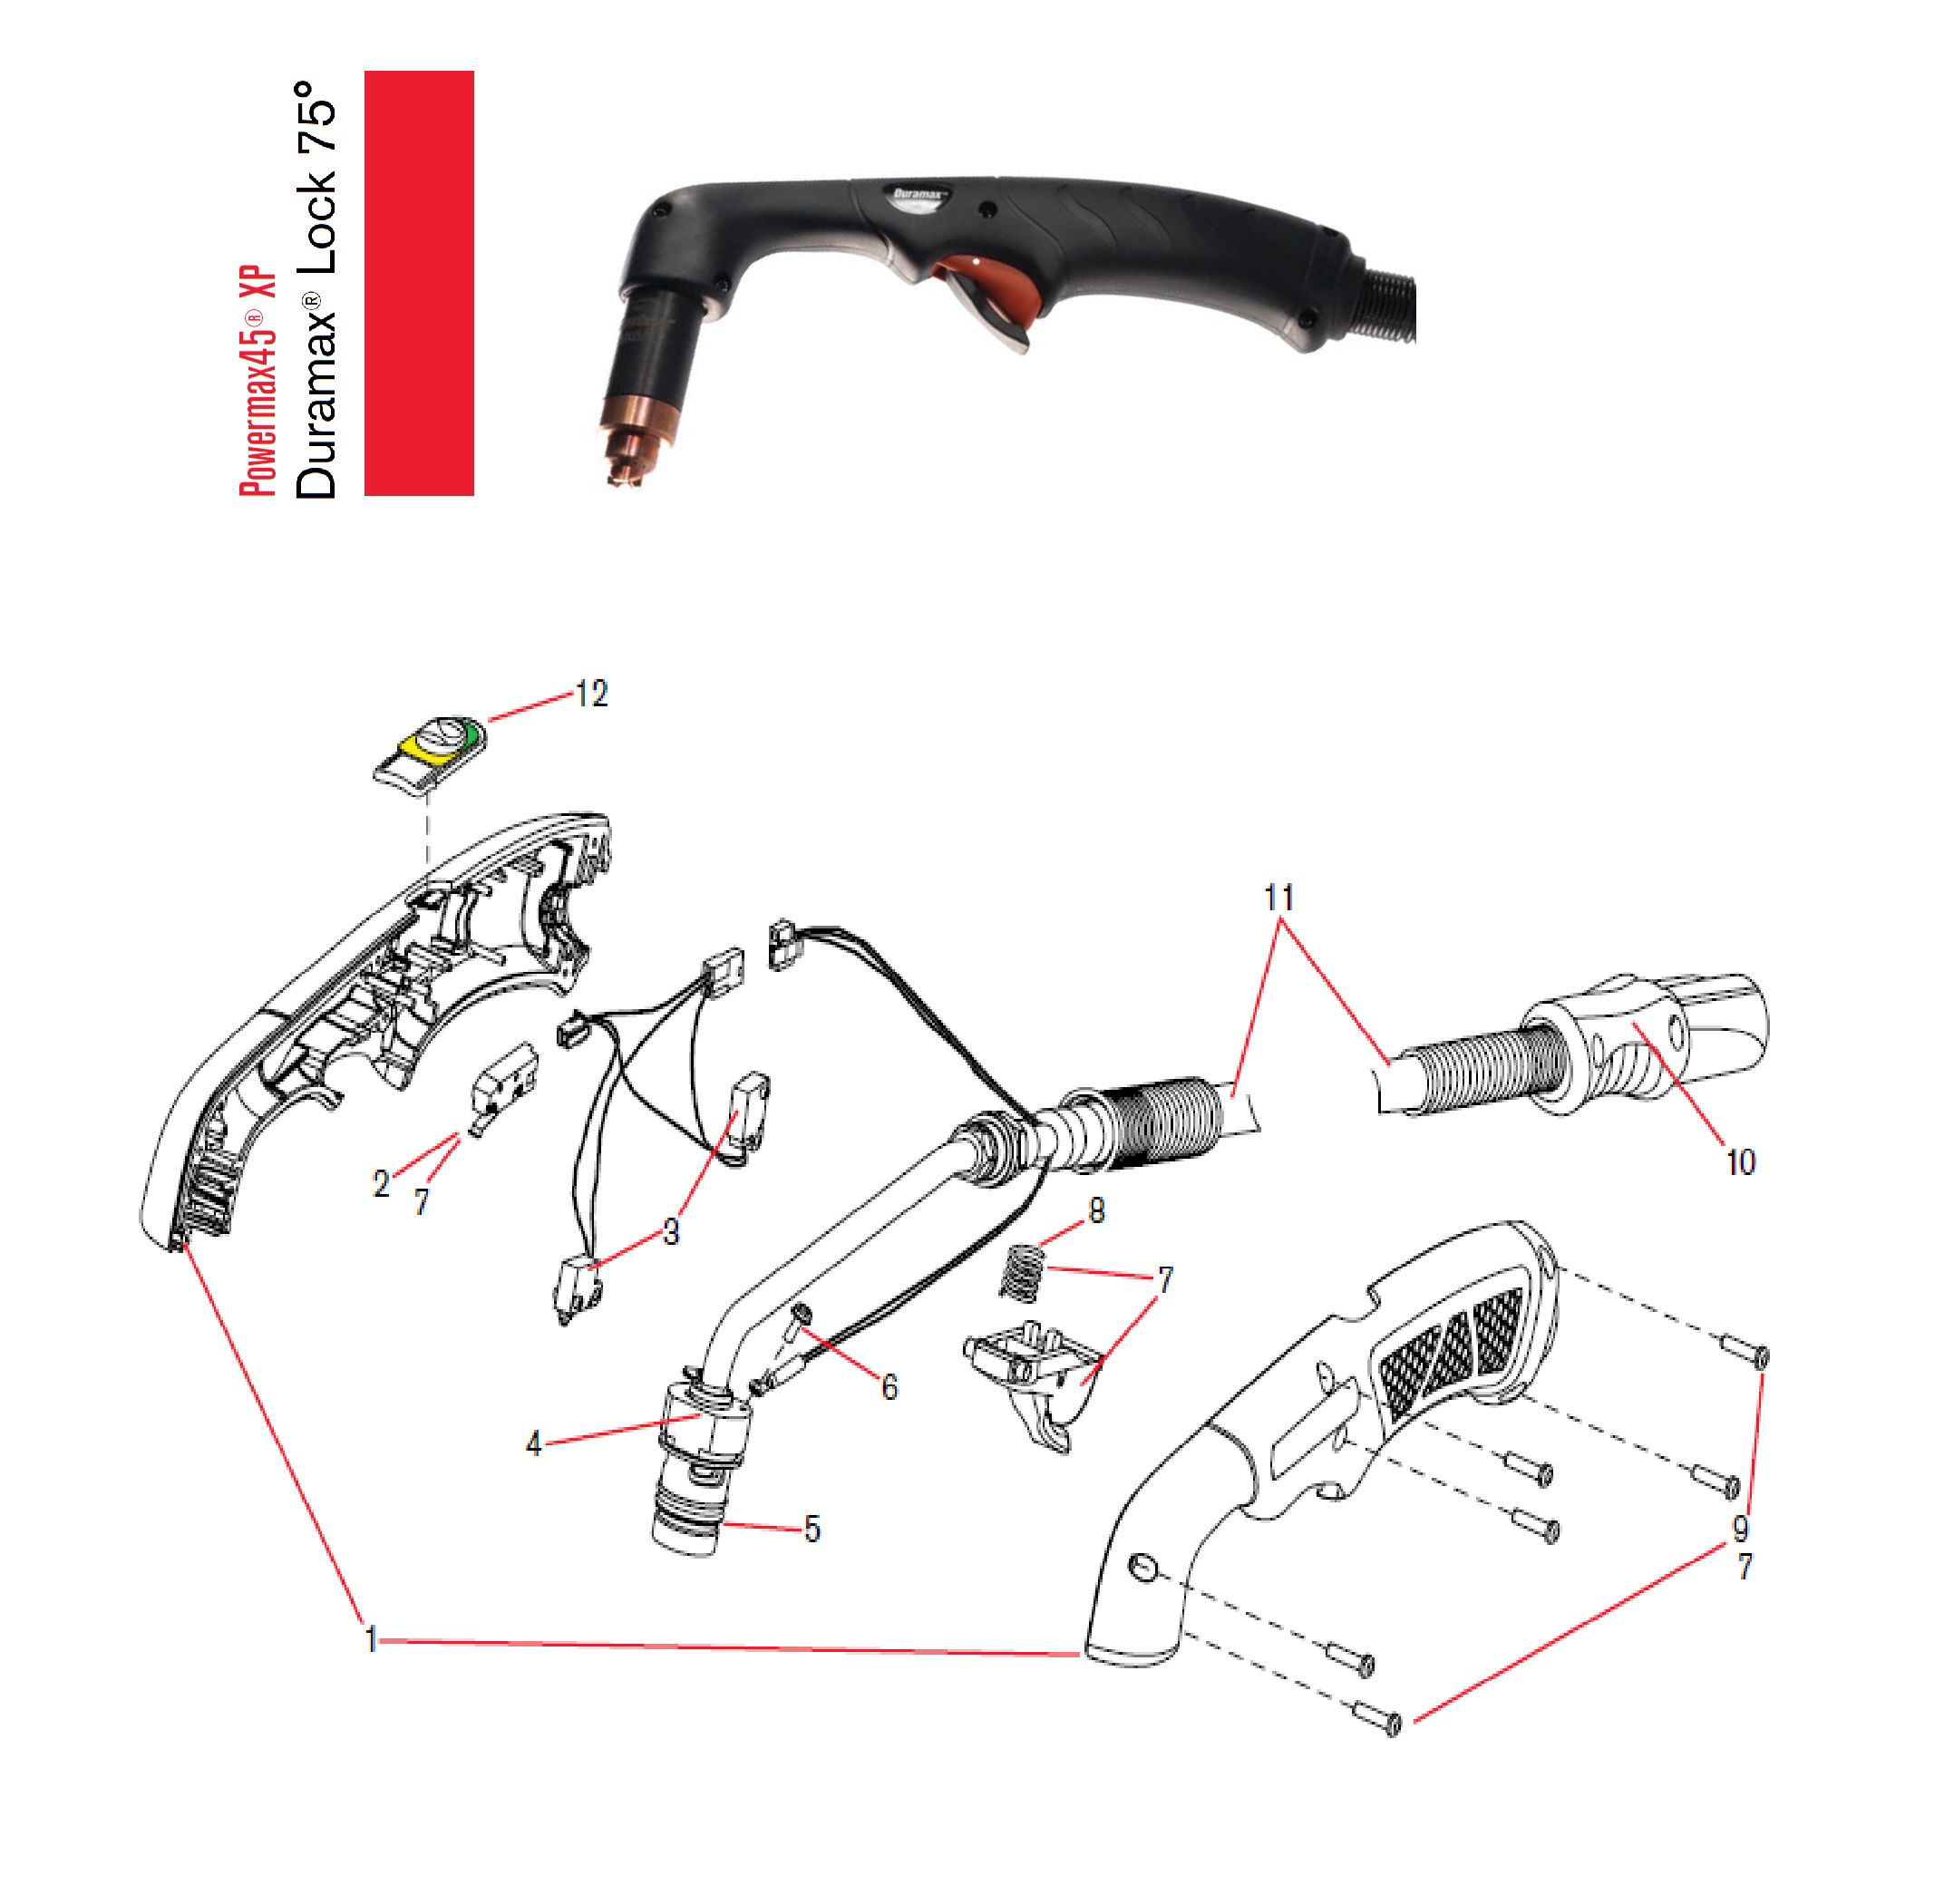
  • Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown: Troubleshooting and Buying Checks

    Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown: Troubleshooting and Buying Checks

    Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown

    If a Hypertherm Duramax Lock 75 degree hand torch is cutting poorly, the first problem is often not the power source. In many cases the issue is in the torch head, consumables, lead connection, or shield/nozzle stack. This guide gives a practical parts breakdown and a buying check process for maintenance teams and support staff who need to verify what to inspect before ordering replacements.

    Key Takeaways

    • Start with the torch side: consumables, retaining hardware, and visible damage around the head.
    • Confirm the torch family and cut mode before ordering anything.
    • Use the WSP lookup page as the source-backed starting point for part identification.
    • Do not assume a consumable is correct because it looks similar; verify against the torch and machine context.
    • If fit is uncertain, mark it Unknown (Verify) and keep the review with the manufacturer or approved supplier.

    Parts breakdown: what to inspect first

    For a 75 degree hand torch setup, begin at the working end and move back toward the lead. The exact internal stack can vary by torch family and machine context, so treat this as a check sequence, not a universal assembly map.

    • Shield or drag shield: Inspect for heat damage, heavy spatter, distortion, and worn edges.
    • Nozzle: Check for orifice wear, pitting, ovality, and side damage.
    • Electrode: Look for deep wear, abnormal erosion, and arc instability symptoms.
    • Swirl ring / gas distribution part: Verify that it is present, seated correctly, and free of cracks or burn marks.
    • Retaining cap or retaining hardware: Confirm threads, seating faces, and torque condition are not damaged.
    • Torch head and locking interface: Inspect for looseness, cracked plastic, damaged seals, or signs of overheating.
    • Lead and strain relief: Check for cuts, kinks, softened insulation, or intermittent operation near the handle.

    Troubleshooting sequence: check, inspect, verify

    1) Check the symptom pattern

    Before replacing parts, identify the failure mode. A no-start condition, weak pilot arc, arc dropout, poor cut quality, or excessive dross can point to different causes. Do not jump to a torch-head replacement until the symptom is matched to the wear pattern.

    2) Inspect consumables as a set

    Remove the front-end parts and inspect them together. A single damaged nozzle may be the visible fault, but a worn electrode or damaged swirl ring can be the root cause. Check for:

    • Mismatch in wear between electrode and nozzle.
    • Evidence of overheating, such as discoloration or warped edges.
    • Carbon tracking, spatter buildup, or contamination in the torch head.
    • Loose fit or poor seating that could interrupt gas flow.

    Verify that the parts being removed match the torch family in service. If the part numbers are not clearly readable, Unknown (Verify) applies until the WSP lookup or approved documentation confirms the match.

    3) Inspect the torch head and lock interface

    The 75 degree hand torch head can see mechanical stress from repeated handling, workpiece contact, and lead movement. Check the lock area for wear that may prevent the consumables from seating correctly. If the retaining cap does not tighten smoothly, do not force it. Cross-threading, damaged threads, or a heat-warped seat can create intermittent arc faults.

    4) Verify gas and electrical continuity indirectly

    Without assuming hidden specs, verify the practical conditions that support a stable arc: the front-end parts are clean, seated, and undamaged; the lead is not pinched; and the machine displays no unrelated fault that points away from the torch. If the torch behavior changes when the lead is moved, treat the lead and strain relief as suspect.

    WSP lookup: use it before buying

    The WSP lookup page for this torch family is the best source-backed starting point for parts identification and buying checks:

    Hypertherm Duramax Lock 75 Degree Hand Torch Parts Breakdown on WSP

    Use that page to confirm the torch family, part naming, and catalog-backed item numbers where shown. Do not treat a visual match alone as enough proof. If a component is listed in the lookup but your torch head shows a different geometry, mark the fit as Unknown (Verify) and confirm with the supplier or manufacturer before ordering.

    Buying checks for maintenance teams

    When purchasing torch parts, use these checks in order:

    1. Match the torch family: Confirm the torch is the Hypertherm Duramax Lock 75 degree hand torch variant referenced by the lookup page.
    2. Match the machine context: Use the actual machine and torch pairing in service, not a similar setup from another bay.
    3. Match the wear pattern: Replace the damaged front-end part plus any companion part that shows related wear.
    4. Check the lock and seating surfaces: If the interface is damaged, parts alone may not fix the fault.
    5. Verify the buy link path: Use only approved links from the source page or internal support references.

    If a replacement is being considered because of repeated arc failure, review the torch-side troubleshooting first. Related guidance is available here: Plasma Cutter Pilot Arc Failure Troubleshooting and Plasma Drag Shield Compatibility Guide.

    Safety notes

    • De-energize the system before removing or handling consumables.
    • Allow hot parts to cool before inspection.
    • Do not file, force, or modify front-end parts to make them fit.
    • If a torch head is cracked, burned, or electrically unstable, remove it from service until reviewed.
    • Use manufacturer review for any fit or safety-critical uncertainty.

    FAQ

    Why does a new consumable set still cut poorly?

    A new set can still perform badly if the torch head is damaged, the retaining hardware does not seat correctly, the lead is compromised, or the wrong consumable family was installed. Inspect the whole front end, not just the nozzle.

    What should I replace first when the torch shows arc dropout?

    Start with the consumables and the torch-side seating surfaces. If those are clean and the problem continues, inspect the lead, strain relief, and the machine-side fault indications. Do not assume the power source is the root cause.

    How do I confirm I am buying the right part?

    Use the WSP lookup page, confirm the torch family and item naming, and compare the existing installed parts to the lookup record. If anything does not align, mark it Unknown (Verify) and confirm before purchase.

    Can I use a similar-looking shield or nozzle from another torch?

    No. Similar appearance is not enough. Verify the exact torch family, geometry, and use case before ordering or installing any replacement part.

    Sources Checked

    Where exact fit or part identity could not be confirmed from the provided source record, the correct status is Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

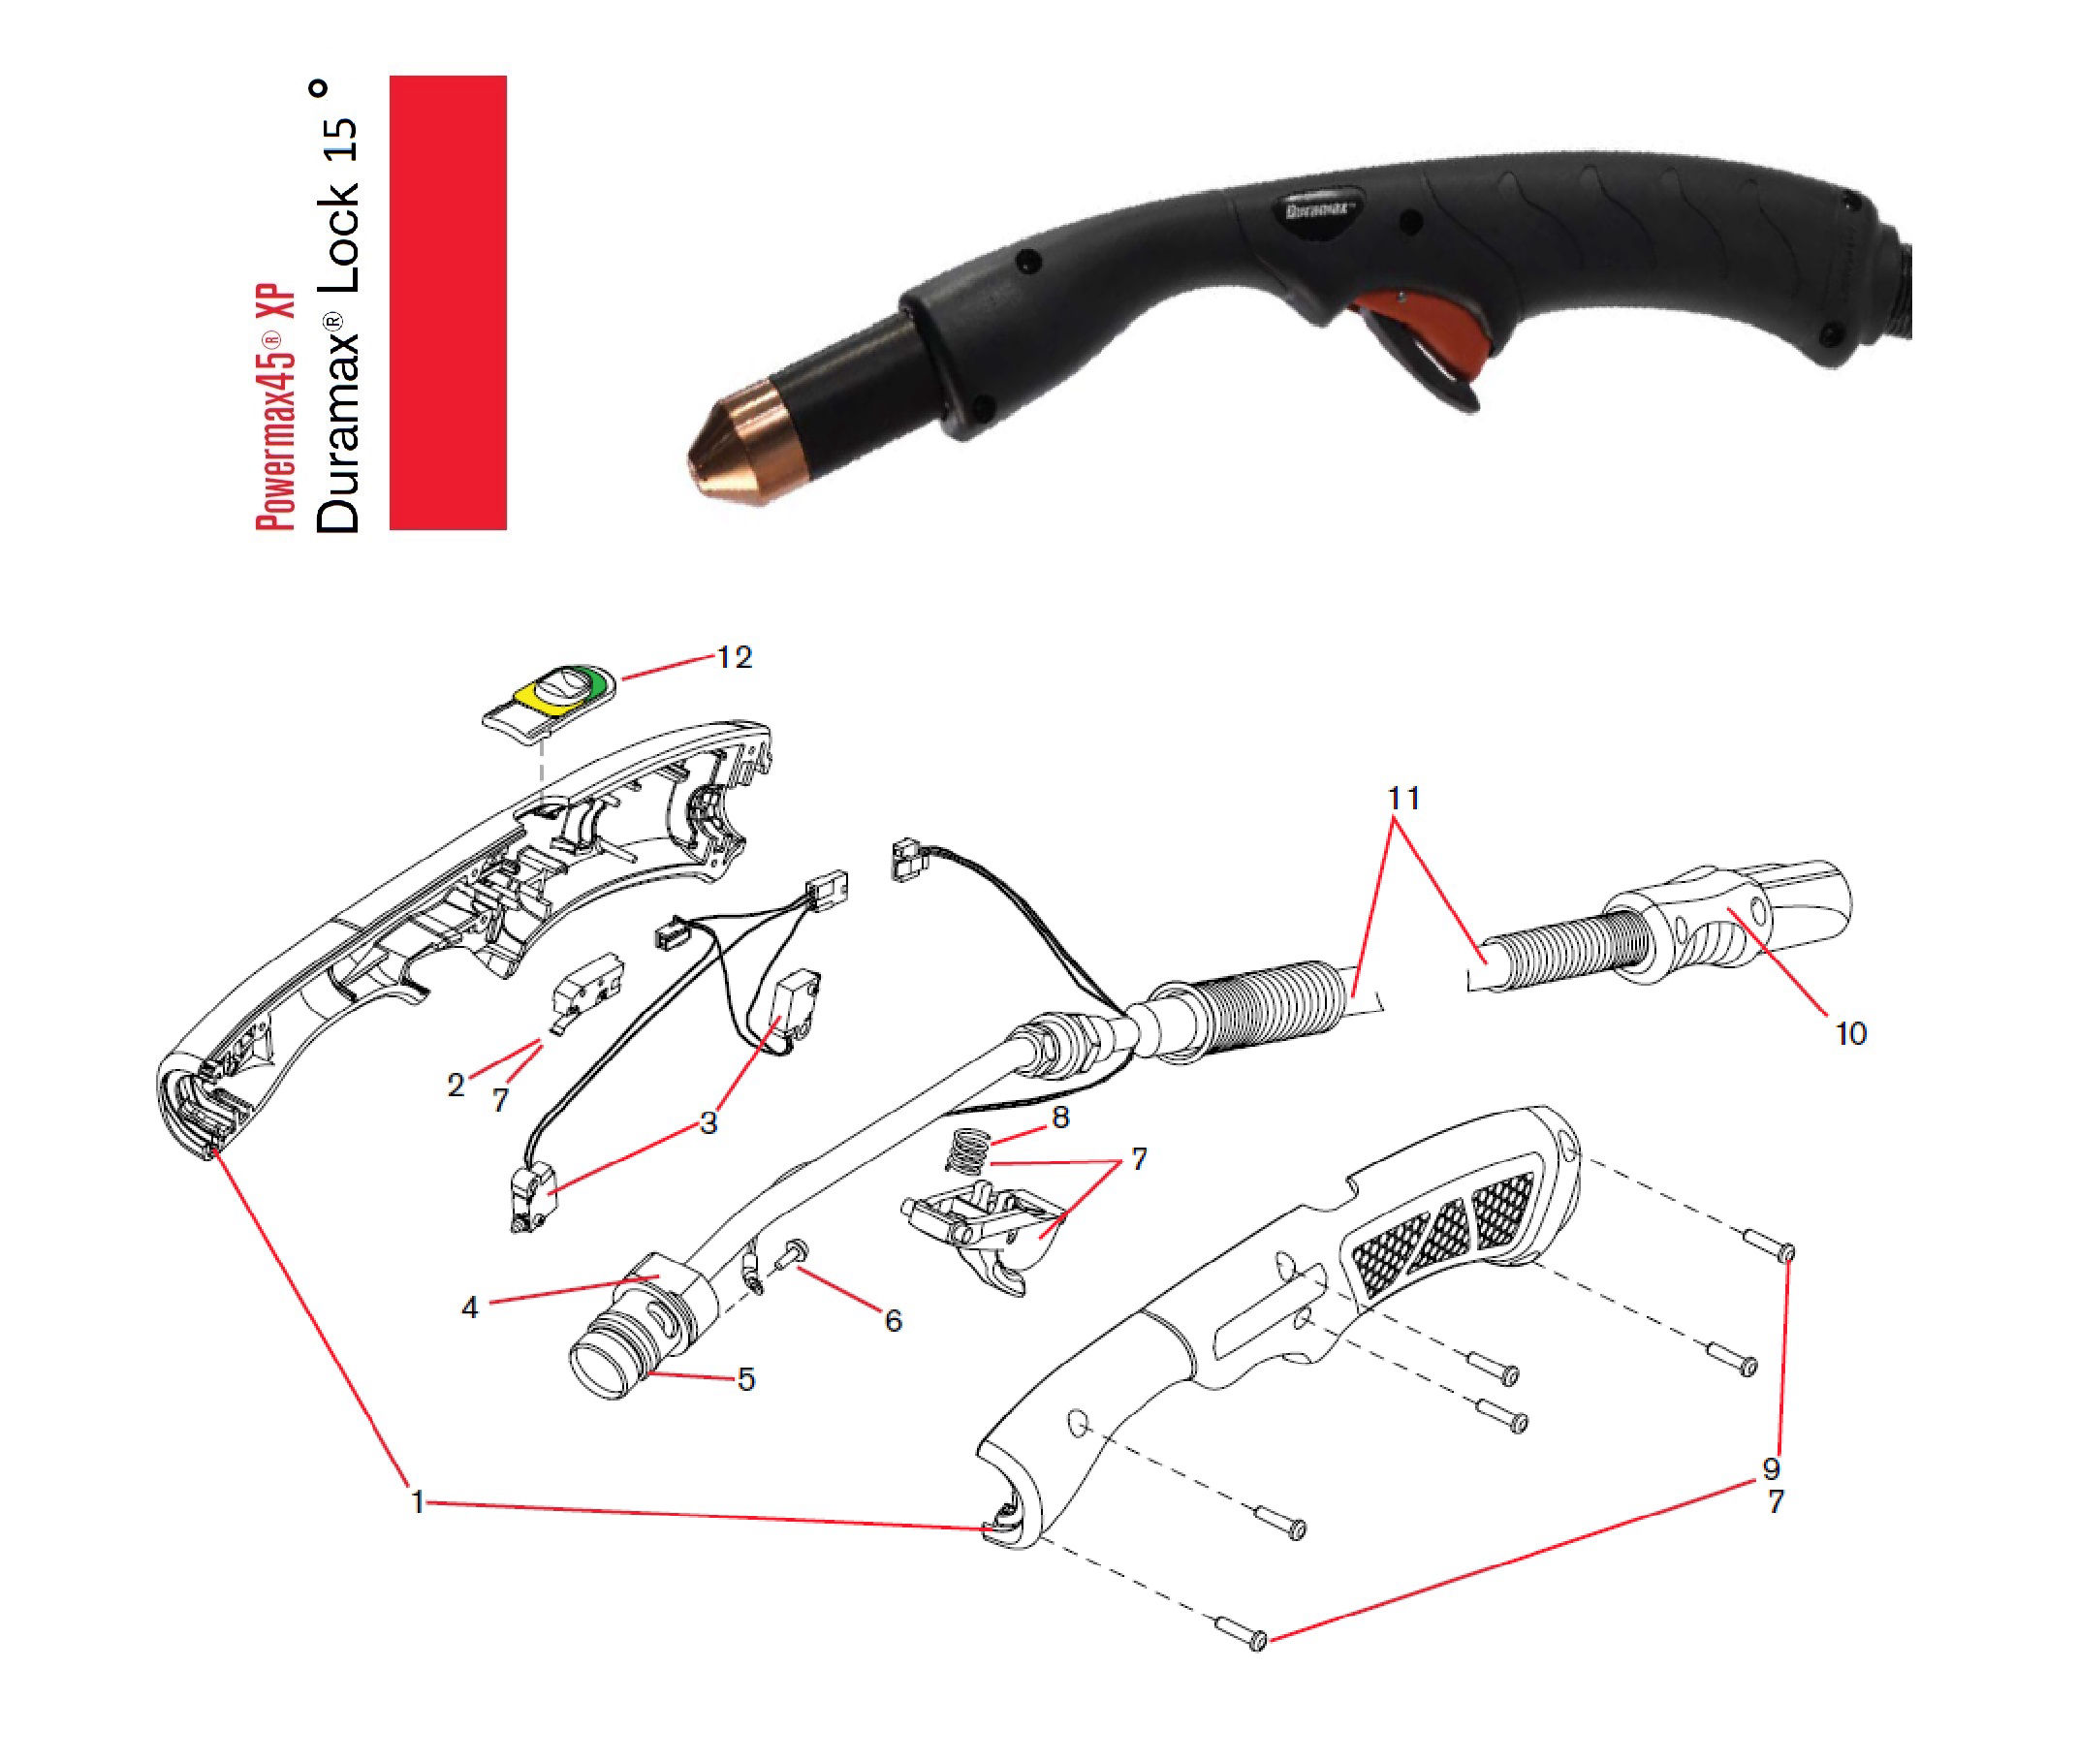
  • Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown

    If you are maintaining a Hypertherm Duramax Lock 15 Degree hand torch, the main job is not guessing part numbers. It is identifying the wear path, matching the torch to the machine context, and confirming the replacement against the catalog before anything is ordered. This is a consumable replacement problem first, and a parts-compatibility problem second.

    Key Takeaways

    • Use the torch’s breakdown page as the starting point, not the final approval step.
    • Confirm the torch style, angle, and lock style before comparing parts.
    • Inspect the nozzle, electrode, shield, swirl ring, and retaining hardware for heat damage, arc misalignment, and physical wear.
    • If fitment is uncertain, stop and verify against the WSP lookup page before ordering.
    • Do not assume a part from another Duramax family torch will fit. Verify each item by catalog reference.

    What This Torch Parts Breakdown Is For

    The Hypertherm Duramax Lock 15 Degree hand torch parts breakdown is useful when you need to replace worn consumables or identify a damaged torch component after poor cut quality, arc instability, or visible heat distortion. In practice, the breakdown helps you separate routine wear items from parts that may indicate a deeper torch issue.

    For this torch, the critical point is to match the exact torch configuration shown on the source page: Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown. That page is the verified lookup source for the torch context provided here.

    How to Work the Replacement Decision

    Start with a visual inspection. Then move to part-by-part verification. Do not replace parts only because cut quality changed; verify the torch condition and the machine setup first.

    Check

    • Check the torch head for heat discoloration, cracks, or arc tracking marks.
    • Check the consumable stack for uneven wear, melted edges, or carbon buildup.
    • Check the lead and handle area for cuts, crushed sections, or loose strain relief.
    • Check the retaining hardware for cross-threading, distortion, or seizure.

    Inspect

    • Inspect the electrode tip for deep crater wear or a collapsed center. If the wear pattern is abnormal, replace and verify arc transfer behavior.
    • Inspect the nozzle orifice for ovality, spatter blockage, or visible deformation.
    • Inspect the shield for heat damage, edge warping, or fit issues at the torch front end.
    • Inspect any swirl ring or internal alignment part for cracks, burns, or contamination.

    Verify

    • Verify the torch model and angle match the catalog listing before selecting a replacement.
    • Verify the part number from the lookup page or linked breakdown page, not from memory.
    • Verify the machine context if the torch is being used on a specific plasma system. If the machine is not clearly identified, treat compatibility as Unknown (Verify).
    • Verify that the replacement set matches the wear pattern you found. If only one part is damaged, do not automatically replace the full stack unless the inspection supports it.

    Common Failure Signs That Point to Consumable Replacement

    Most maintenance calls on plasma torches start with cut quality. That is useful, but not enough. Use the symptoms to guide inspection, then confirm with the part breakdown.

    • Rough edge or heavy dross: often points to nozzle wear, incorrect standoff, or an electrode nearing end of life.
    • Weak start or intermittent arc: may involve the torch front end, pilot arc behavior, or worn internal components. See the related troubleshooting guide for more on arc loss and no-start conditions: Pilot Arc Failure Troubleshooting.
    • Excessive spatter in the front end: check the nozzle and shield for contamination and fit.
    • Unexpected heat at the torch head: inspect for poor consumable seating or a damaged component stack.

    If the torch is producing unstable arc behavior across more than one set of consumables, do not assume the consumables are the only issue. Confirm machine settings, air quality, and lead condition. If the cause is unclear, mark the condition as Unknown (Verify) and cross-check with the machine manual and torch breakdown.

    WSP Lookup Section

    Use the verified WSP source page below to review the torch breakdown and item context before ordering:

    Open the Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown lookup

    This lookup page should be treated as the catalog-backed starting point for identifying the correct parts. If a replacement item is not clearly confirmed on the page, do not guess. Record it as Unknown (Verify) and confirm before purchase.

    Replacement Workflow for Maintenance Teams

    1. Identify the torch style and front-end layout.
    2. Remove the torch consumables and document the wear pattern.
    3. Compare the damaged parts against the breakdown page.
    4. Check whether wear is isolated to the consumables or extends into the torch head and lead.
    5. Verify the replacement part number against the WSP lookup page.
    6. Only then release the order.

    Safety Notes

    • Power down and isolate the plasma system before handling the torch head.
    • Allow the torch and consumables to cool before inspection.
    • Use eye protection when removing hot or stuck consumables.
    • Do not force threaded parts. If a component binds, inspect for damage instead of tightening harder.
    • Use compressed air and cleaning methods that do not introduce debris into the torch front end.

    FAQ

    How do I know if I need a full torch consumable set or only one part?
    Inspect the wear pattern first. If only the nozzle shows normal end-of-life wear and the electrode is still within acceptable condition, a partial replacement may be enough. If multiple parts show heat damage or arc instability, verify whether the full stack should be replaced.

    Can I use another Duramax torch part if it looks similar?
    No. Similar appearance does not confirm compatibility. Use the exact breakdown page and verify each item number before ordering. If the match is not clear, treat it as Unknown (Verify).

    What should I check before blaming the consumables for poor cut quality?
    Check air quality, torch seating, work lead condition, standoff, and machine settings. Consumables are a common cause, but not the only one. If the issue persists after replacement, inspect the torch and power source path.

    Where do I confirm the correct parts?
    Use the verified lookup page linked above. That is the reference source for this torch breakdown.

    Sources Checked

    When the torch condition is unclear, do not force a replacement decision. Inspect, verify, then order. That is the safe path for plasma support work.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Hypertherm Air T30 Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Air T30 Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Air T30 Torch Parts Breakdown

    The Hypertherm Air T30 torch is a serviceable plasma cutting consumable path, but replacement decisions should start with inspection, not guesswork. A wrong nozzle, electrode, swirl ring, shield, or retaining component can create arc instability, poor cut quality, and repeated part failure. For maintenance buyers and shop support teams, the goal is simple: identify what is worn, confirm what is actually compatible, and replace only the parts that match the torch setup in service.

    Key Takeaways

    • Inspect the torch stack before ordering replacements.
    • Match parts to the exact torch and system path in use; do not assume cross-compatibility.
    • Most plasma consumable issues show up as arc start trouble, unstable cutting, excess dross, or accelerated wear.
    • Use the WSP lookup page as the starting point for the Air T30 service path.
    • When technical details are not confirmed, treat them as Unknown (Verify).

    What to Check First on an Air T30 Torch

    Before replacing anything, isolate the torch from power, shut down the cutter, and allow the system to cool. Then inspect the consumable stack in sequence. Start with the nozzle or tip, electrode, shield, swirl ring, and retaining components. Look for pitting, deformation, heat tint beyond normal service wear, cracked insulating surfaces, or a loose fit at assembly.

    Check the air path as well. Restricted or contaminated air can mimic worn consumables. Verify the air filter, regulator settings, hose condition, and any evidence of oil or water in the line. If air quality is poor, new parts may fail early even when the torch hardware is correct.

    Replacement Decision Guide

    Inspect: Remove the front-end parts and compare them to the torch configuration currently installed. Missing pieces, mixed wear patterns, or uneven burn marks often indicate the torch has been run with mismatched or overdue consumables.

    Verify: Confirm the torch model path against the WSP page for the Hypertherm Air T30. Do not rely on visual similarity alone. Two parts that look close can still differ in dimensions, thread form, or gas flow design. If a part detail is not stated clearly, mark it as Unknown (Verify) rather than assuming a fit.

    Replace: Replace components as a matched set when wear is uneven or when repeated arc transfer issues point to more than one damaged part. A single worn electrode can damage the nozzle, and a damaged nozzle can shorten the life of the next electrode.

    Recheck: After installation, verify that the stack is seated correctly, all retaining parts are secure, and the torch tip is clean. Run a controlled test cut on known material before returning the machine to production.

    Common Symptoms and What They Usually Mean

    Hard start or no start: Check electrode wear, nozzle condition, air pressure, and torch connections. If the pilot arc does not transfer consistently, inspect for contamination, loose assembly, or internal damage.

    Weak or wandering arc: Inspect the nozzle orifice, swirl ring, and air quality. A damaged air path can distort the arc even when the torch appears mechanically sound.

    Excess dross or bevel angle changes: Verify cut speed, torch height, and consumable condition. If the parts are worn unevenly, replace the full front-end stack rather than only the most visible part.

    Repeated consumable failure: Check for overloaded duty conditions, piercing technique problems, poor air quality, or incorrect part pairing. If the failure pattern repeats after replacement, the root cause is usually upstream of the torch tip.

    WSP Lookup Page: Start Here

    Use the WSP lookup page for the Hypertherm Air T30 torch as the first reference point for service part identification and standard consumables in this support path:

    Hypertherm Air T30 Torch Parts Breakdown

    This page should be used as a parts identification starting point, not as a substitute for verifying the actual torch in hand. If a part detail is not fully specified on the page, treat it as Unknown (Verify) and confirm against the torch body, existing consumables, or the machine documentation.

    Practical Inspection Steps Before Ordering

    • Clean the torch front end and remove spatter or dust before inspection.
    • Check the electrode and nozzle for crater wear, chipping, or ovalized openings.
    • Verify that the swirl ring or insulator has no cracks, burns, or distortion.
    • Inspect the retaining cup or shield for heat damage and thread condition.
    • Compare the old part to the replacement by form, seat, and visible geometry, not by part name alone.
    • Confirm the air supply is dry, clean, and within the system requirement; if the requirement is not confirmed, mark it Unknown (Verify).
    • After assembly, check for smooth fit and no cross-threading before energizing the cutter.

    Safety Notes

    Plasma torch parts can remain hot long after shutdown. Wear gloves and eye protection when removing used consumables. Do not handle damaged electrodes or nozzles barehanded if they are still warm. Disconnect power before service. If you see cracked insulation, exposed conductors, or signs of internal torch damage, remove the torch from service until it is inspected by qualified personnel.

    Do not test-fire a torch with uncertain part compatibility. If the part stack is not verified, the machine can arc unpredictably and damage the torch, workpiece, or operator PPE.

    Related Troubleshooting References

    For deeper diagnosis, these related guides can help separate consumable wear from machine-side faults:

    FAQ

    How do I know whether to replace one part or the whole consumable set?
    If wear is isolated and the rest of the stack checks clean, a single part may be enough. If the electrode, nozzle, and shield all show heat damage or uneven wear, replace the set and verify the air supply.

    Can I match parts by appearance only?
    No. Visual similarity is not enough. Verify the torch path, seat geometry, and any stated part details. If a detail is not confirmed, mark it Unknown (Verify) before ordering.

    What if the torch still cuts poorly after new parts are installed?
    Check air quality, work lead condition, cut speed, torch height, and machine output. Consumables are often the symptom, not the root cause.

    Is the WSP page enough to approve a replacement order?
    It is a starting point for identification, but final approval should still be based on the torch in hand, the machine setup, and any confirmed part details.

    Sources Checked

    • WSP lookup page: https://www.weldsupportparts.com/hypertherm-air-t30-torch.html
    • Internal link: Plasma Consumable Compatibility: How to Verify Torch Parts Before Ordering
    • Internal link: Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
    • Internal link: Plasma Torch Nozzle Damage Causes: Orifice Wear, Double Arcing, Piercing, and Air Problems

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Hypertherm Air T30 Torch Parts Breakdown: Parts Lookup and Buying Checks

    Hypertherm Air T30 Torch Parts Breakdown: Parts Lookup and Buying Checks

    Hypertherm Air T30 Torch Parts Breakdown

    The Hypertherm Air T30 torch support path is a parts-lookup problem before it is a buying problem. For maintenance buyers and weld shop support teams, the main risk is ordering a consumable or service part by name instead of confirming the torch family, cut mode, and part interface. The result is wasted time, mismatched hardware, or a torch that will not assemble correctly.

    This guide is a practical breakdown for the Hypertherm Air T30 Torch Parts Breakdown process. It focuses on what to inspect, what to verify before ordering, and how to use the Weld Support Parts lookup page as a starting point for parts identification.

    Key Takeaways

    • Start with torch family identification, not the cut tip alone.
    • Verify retaining hardware, shield style, nozzle style, and electrode condition before ordering.
    • Do not assume compatibility from a similar Hypertherm torch name.
    • Use the WSP lookup page as the source page for parts identification, then confirm against the torch in hand.
    • When a detail is uncertain, mark it as Unknown (Verify) and confirm from the machine, torch label, or service documentation.

    What the Air T30 Parts Breakdown Should Cover

    For a torch service check, the useful breakdown is the set of wear parts and torch-side service items that affect arc start, cut quality, and torch assembly. That usually includes the electrode, nozzle, shield or drag shield style if used, retaining cap or retaining hardware, swirl ring or gas distribution component if used, and any torch body or lead-side service items that are specific to the torch family.

    For this support path, the source page is the place to begin the lookup:

    Hypertherm Air T30 hand torch support on Weld Support Parts

    Use that page to identify the support path, then verify the exact torch and consumable set before placing an order.

    Check the Torch Before You Buy

    Do not order from memory. A fast visual inspection often prevents the wrong part from being purchased.

    • Check the torch label. Confirm the torch family and any visible model marking. If unreadable, note it as Unknown (Verify).
    • Inspect the retaining hardware. Verify whether the cap, shield, or front-end hardware matches the torch you have in service.
    • Inspect the nozzle and electrode wear. Look for pit wear, heat discoloration, erosion, and arc damage.
    • Verify the front-end stack-up. Count the parts in the assembly as removed, and compare that stack to the lookup page or service parts breakdown.
    • Check for cut-quality symptoms. Heavy dross, arc wandering, or repeated pilot-arc issues may indicate worn consumables rather than a power supply fault.

    Troubleshooting Support: Where Parts Checks Matter

    Many torch problems look electrical at first but are actually consumable-related. Before replacing components upstream, inspect the torch front end.

    1) No-start or weak start

    • Inspect the electrode and nozzle for obvious wear or burn damage.
    • Verify the torch stack is assembled correctly and tightened to the correct feel for the design, not over-torqued.
    • Check for contamination, moisture, or debris in the torch front end.

    2) Pilot arc dropout

    • Inspect the retaining hardware and front-end fit.
    • Verify the consumables are the correct family for the Air T30 support path.
    • Check lead condition, damage at the torch neck, and any visible burn-through.

    3) Poor cut quality

    • Inspect nozzle orifice wear and edge damage.
    • Verify the shield or drag shield style against the torch setup in use.
    • Check the work clamp, air quality, and cut technique before replacing parts again.

    For a deeper fault tree, the internal support article on pilot arc issues is a useful follow-up:

    Plasma Cutter Pilot Arc Failure Troubleshooting

    Buying Checks for Service Parts

    When you move from inspection to purchasing, treat every line item as a verification step.

    • Check part family first. The torch family must match the support path.
    • Inspect the old part. Compare shape, thread style, contact surfaces, and overall length. If the old part is damaged beyond comparison, mark the detail Unknown (Verify).
    • Verify the assembly count. Some torch fronts use multiple small parts that are easy to miss.
    • Confirm the use case. Drag cutting, standoff cutting, or shielded use may require different front-end hardware. If not confirmed, the requirement is Unknown (Verify).
    • Do not substitute by brand alone. Similar plasma parts are not interchangeable without verification.

    If you need a methodical way to compare drag-shield and front-end configurations, use this internal reference:

    Plasma Drag Shield Compatibility Guide

    WSP Lookup Section

    Use the Weld Support Parts lookup page as the starting point for the Air T30 support path:

    View the Hypertherm Air T30 hand torch support page

    Practical workflow:

    1. Open the lookup page.
    2. Match the torch family to the machine and torch in service.
    3. Remove and inspect the worn parts.
    4. Compare the old parts to the page listing and any internal support notes.
    5. Only then place the order.

    Any item that cannot be confirmed from the torch, the page, or service paperwork should remain Unknown (Verify) until checked.

    Safety Notes

    • De-energize the plasma system before removing torch parts.
    • Allow the torch to cool before handling front-end consumables.
    • Do not inspect burned parts by touch immediately after use.
    • Use eye protection when cleaning the torch front end.
    • Do not mix unknown parts into a live torch assembly.

    FAQ

    How do I know if the Air T30 part I need is a consumable or a service part?

    Check the wear pattern and location. Front-end items such as electrodes, nozzles, shields, and retaining hardware are consumable-facing. Torch-body, lead-side, or connector items are service parts. If the category is unclear, label it Unknown (Verify) and compare against the lookup page.

    Can I order by torch name only?

    No. Torch name alone is not enough. Verify the exact torch family, front-end stack, and cut mode before ordering.

    What should I do if the old part is too damaged to identify?

    Use the torch label, machine model, and the support page as reference points. If a detail still cannot be confirmed, keep it as Unknown (Verify) until checked against service documentation or a known-good assembly.

    Why does a torch sometimes fail even when the power supply is fine?

    Worn or mismatched consumables can cause no-start, weak arc, dropout, and poor cut quality. Start with the torch front end before replacing larger components.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • ESAB PT-39 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-39 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-39 Torch Parts Breakdown

    The ESAB PT-39 Torch Parts Breakdown is a practical reference for maintenance buyers, welders, and support teams who need to identify replacement consumables before ordering. Plasma torches fail for simple reasons: worn electrodes, damaged nozzles, loose retaining parts, air leaks, or a torch assembly that does not match the machine setup. The right buying step is to verify the torch family and item number first, then inspect the worn parts against the parts breakdown before you place an order.

    This guide is not a substitute for the machine manual or the torch documentation. Use it as a buying and inspection aid. If a detail is not confirmed, treat it as Unknown (Verify).

    Key Takeaways

    • Confirm the exact torch model before ordering any PT-39 replacement part.
    • Match the item number on the parts breakdown to the worn component, not just the visual shape.
    • Inspect electrodes, nozzles, shields, and retaining hardware as a set.
    • Check lead condition, torch body damage, and air delivery before replacing consumables again.
    • Use the WSP lookup page as the primary source for part identification.

    How to Use the PT-39 Parts Breakdown

    Start with the parts lookup page and identify the component by item number, not by assumption. On plasma torches, two parts can look similar but differ in thread style, length, seat profile, or torch-family match. If you only compare pictures, the risk of ordering the wrong part is high.

    Check: the torch label, machine documentation, and worn part geometry.
    Inspect: the nozzle orifice, electrode pit depth, shield face, and retaining cap threads.
    Verify: the replacement item number against the WSP lookup page before purchase.

    Troubleshooting and Support Checks

    When a PT-39 torch starts cutting poorly, do not assume the consumables are the only issue. Plasma cut quality problems often come from a combination of wear and setup errors.

    1) No start or weak start

    • Check the torch lead connection and power source setup.
    • Inspect the electrode and nozzle for heavy wear, burn marks, or contamination.
    • Verify the consumables are seated correctly and tightened to the proper hand-tight condition per the equipment manual.

    If the torch parts are new and the problem remains, the issue may be in air supply, trigger circuit, or internal torch damage. Unknown (Verify) if the source is torch-related until the upstream system is checked.

    2) Arc dropout during cutting

    • Check for loose retaining parts or poor contact between consumables.
    • Inspect the nozzle opening for distortion and the electrode tip for uneven erosion.
    • Verify that the air supply is stable and clean.

    Arc dropout is often caused by consumable wear, but supply instability can produce the same symptom. Replace only the parts that are actually worn or damaged.

    3) Poor cut edge or excessive dross

    • Check cut speed, torch standoff, and work lead condition.
    • Inspect nozzle wear and shield damage.
    • Verify that the torch setup matches the intended cut mode and amperage range. Unknown (Verify).

    Do not buy consumables only by amperage label or general appearance. Match the parts breakdown first, then compare the physical wear pattern.

    Buying Checks Before Ordering Parts

    For buyers and storeroom teams, the important step is reducing return risk. Use these checks before placing an order:

    • Check the torch family: Confirm it is PT-39 and not another ESAB torch model.
    • Check item numbers: Use the parts breakdown item number for the replacement part.
    • Check wear history: If the torch repeatedly burns the same part, the upstream issue may be air quality or handling.
    • Check the machine record: Match the torch to the cutter or power source documentation.
    • Check packaging notes: If the listing does not clearly match the item number, do not guess.

    If a part description is unclear, keep it as Unknown (Verify) until the item number and torch family are confirmed.

    WSP Lookup Section

    Use the official Weld Support Parts page for the ESAB PT-39 torch to review the parts breakdown and item-number lookup:

    ESAB PT-39 Torch Parts Breakdown on Weld Support Parts

    This page is the starting point for identifying replacement consumables and related torch parts. Use it to compare the worn component to the listed item number before you buy.

    Practical Inspection Steps at the Torch

    Before replacing consumables, do a short field inspection:

    1. Lock out the system and make sure the torch cannot fire.
    2. Remove the consumables and lay them out in order.
    3. Inspect the electrode for crater wear, pitting, and heat damage.
    4. Inspect the nozzle for ovality, enlarged orifice, or spatter damage.
    5. Inspect the shield/retaining parts for cracks, thread wear, and burn marks.
    6. Inspect the torch body for heat damage, cracks, and contamination.
    7. Verify that the part numbers on the replacement order match the lookup page.

    This sequence helps prevent unnecessary parts swaps. If the consumables fail early, verify the air supply quality and torch handling before assuming the replacement parts are wrong.

    Safety Notes

    • De-energize the cutter before removing torch consumables or opening covers.
    • Let hot parts cool before inspection. Plasma tips and electrodes can retain heat.
    • Use eye protection and gloves when handling used consumables with sharp or hot edges.
    • Do not fire a torch with missing or loose parts.
    • If a torch shows burn-through, cracked insulation, or exposed conductors, remove it from service until repaired by qualified personnel.

    FAQ

    How do I confirm the correct PT-39 replacement part?

    Use the WSP PT-39 parts breakdown, then match the item number to the worn component. Do not order by appearance alone.

    What if the torch looks like another ESAB model?

    Treat it as Unknown (Verify) until the torch label, machine manual, and parts breakdown all match. Similar torch parts are not interchangeable by default.

    Should I replace only the electrode?

    Only if inspection shows the electrode is the only worn part. If the nozzle or retaining hardware is damaged, replace the matching consumables as needed after verification.

    Why do new consumables sometimes fail early?

    Early failure can come from air contamination, improper torch setup, loose parts, or handling damage. Inspect the whole torch system before ordering the same parts again.

    Sources Checked

    • Weld Support Parts: ESAB PT-39 Torch Parts Breakdown — https://www.weldsupportparts.com/esab-pt-39-torch.html
    • Internal link: Plasma Consumable Compatibility: How to Verify Torch Parts Before Ordering
    • Internal link: Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
    • Internal link: Plasma Drag Shield Compatibility Guide: Torch Family, Amperage, Nozzle, Retaining Cap, and Cut Mode Checks

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • ESAB PT-38 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-38 Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-38 Torch Parts Breakdown

    If you are maintaining an ESAB PT-38 torch, the main job is not just finding a part number. The job is matching the torch body, head, consumables, shields, and accessory rows to the exact setup on the machine before you order. A wrong consumable can look close enough to install and still fail in cut quality, arc stability, or wear life.

    This guide is a practical parts-lookup and buying-check article for the ESAB PT-38 Torch Parts Breakdown. Use it to verify what you have, compare the layout to the Weld Support Parts lookup page, and avoid ordering by appearance alone.

    Key Takeaways

    • Start with the torch family and item-number lookup, not the part photo.
    • Verify the torch model, amperage class, and cut process before ordering consumables.
    • Check the nozzle, electrode, shield, retaining cap, swirl ring, and handle-side accessories as a set.
    • If any fitment detail is unclear, treat it as Unknown (Verify) until you confirm it against the lookup page or the torch itself.
    • Use the parts breakdown for replacement planning, not as proof that two similar-looking parts are interchangeable.

    What the PT-38 parts breakdown is good for

    The Weld Support Parts page for the ESAB PT-38 is a lookup reference for replacement parts, consumables, kits, and accessory rows with item-number lookup. That makes it useful for maintenance buyers and shop support teams who need to match what is installed on the torch to what should be ordered next.

    Use the page to identify:

    • Consumable rows tied to the PT-38 torch family
    • Replacement items for wear parts
    • Kit rows or grouped accessory rows, if listed
    • Item numbers that help cross-check your internal stock labels

    Important: the lookup page is a starting point for identification. It is not a substitute for confirming the torch variant in the field.

    Practical check steps before you order

    Use these checks at the bench, not from memory.

    1. Check the torch nameplate or body marking. Verify that the torch is actually PT-38. If the marking is missing or worn, note it as Unknown (Verify).
    2. Inspect the consumable stack. Remove the nozzle, electrode, shield, and retaining components as needed and lay them out in order. Compare that stack to the parts breakdown.
    3. Verify wear pattern. Look for rounded nozzle orifice, heat distortion, pit marks, or thread damage. If the wear pattern is abnormal, do not assume the next size up or down is correct.
    4. Match item numbers. Use the Weld Support Parts lookup rows to confirm the item numbers before purchase.
    5. Check for accessory dependence. Some torch setups rely on specific shields, caps, or adapters. Verify each row individually.
    6. Confirm the machine-side connection. The torch body can only be matched correctly if the lead, connector, and machine interface are also verified. If you do not have that information, record it as Unknown (Verify).

    Troubleshooting and support checks

    If the torch is cutting poorly, do not start with the most expensive part. Start with the consumable stack and the torch condition.

    No start or unstable start

    • Inspect electrode condition and seating.
    • Verify the nozzle is not damaged, clogged, or oversized from wear.
    • Check shield and retaining parts for heat damage or loose fit.
    • Verify the torch cable, trigger circuit, and machine connection. If the machine-side details are not known, mark them Unknown (Verify).

    Weak arc or arc dropout

    • Inspect the consumable stack for improper assembly.
    • Verify that the parts match the PT-38 breakdown and not a similar torch family.
    • Look for excessive nozzle erosion or electrode wear.
    • Confirm gas or air delivery conditions only if your setup uses them and the machine instructions support that check.

    Rough cut edge or rapid consumable wear

    • Inspect nozzle alignment and seating.
    • Verify the shield and retaining components are correct for the torch head.
    • Check for contamination, heat damage, or mechanical impact.
    • Compare the installed parts against the lookup page before ordering a full consumable kit.

    How to use the WSP lookup page

    Use the Weld Support Parts PT-38 lookup page here: ESAB PT-38 Torch Parts Breakdown.

    Use that page as your first pass for part identification. Review each row carefully and compare the item number to the physical part in your hand. If a row is unclear, do not guess. Mark the detail Unknown (Verify) and confirm it against the torch body, existing packaging, or your maintenance records.

    For shops managing multiple plasma torches, this page is useful for reducing mix-ups between similar torch families. The main check is still the same: torch model first, consumable stack second, order third.

    Buying checks for maintenance teams

    Before you release a purchase order, verify the following:

    • Model match: PT-38 confirmed, or Unknown (Verify) if not confirmed.
    • Part-level match: nozzle, electrode, shield, cap, and any adapter or spacer verified by row.
    • Usage history: record whether the failed part was damaged by heat, impact, poor seating, or normal wear.
    • Stock control: confirm the warehouse label matches the item number on the lookup page.
    • Machine-side details: verify cable length, connector style, or system interface only from documented records. If not documented, use Unknown (Verify).

    Do not approve a replacement just because the part looks close. Plasma torch consumables are often similar by appearance and still not interchangeable.

    Safety notes

    • Disconnect power and follow plant lockout procedures before opening torch assemblies.
    • Allow hot parts to cool before handling.
    • Wear eye protection and gloves when removing worn consumables.
    • Do not reuse parts with cracked threads, heavy heat distortion, or visible structural damage.
    • If the torch condition is uncertain, stop and verify rather than forcing a fit.

    FAQ

    How do I know which PT-38 part I need?

    Start with the torch marking, then compare the installed consumables to the parts breakdown. Match the item numbers on the lookup page to the parts in your hand.

    Can I order by appearance alone?

    No. Similar plasma consumables can look alike and still differ in fitment or function. Verify the row, item number, and torch model first.

    What if my torch label is missing?

    Treat the model as Unknown (Verify) until you confirm it from records, machine documentation, or a direct parts comparison.

    Is the parts breakdown enough to approve a replacement?

    It is a good starting point, but not enough by itself if the torch or machine interface is unclear. Confirm all uncertain details before ordering.

    Sources Checked

    For the ESAB PT-38, the safe buying process is simple: verify the torch, verify the consumable stack, verify the item number, then order. If any detail is not confirmed, keep it as Unknown (Verify) until you have the right match.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • ESAB PT-17A / PT-17AM Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-17A / PT-17AM Torch Parts Breakdown: Parts Lookup and Buying Checks

    ESAB PT-17A / PT-17AM Torch Parts Breakdown

    When an ESAB PT-17A hand torch or PT-17AM machine torch stops cutting cleanly, the first task is not to guess at a replacement part. The correct approach is to identify the torch model, confirm the item number on the parts breakdown, and compare the worn component against the torch family before ordering. The Weld Support Parts lookup page for the ESAB PT-17A / PT-17AM Torch Parts Breakdown is the starting point for that check.

    Key Takeaways

    • PT-17A and PT-17AM are different torch configurations; verify the torch type before ordering parts.
    • Use the item-number lookup on the WSP parts page, not a visual guess from the outside of the torch.
    • Most torch complaints trace back to wear items, loose connections, contamination, damaged leads, or the wrong consumable stack.
    • If a part cannot be confirmed from the breakdown, treat it as Unknown (Verify) and check the exact torch nameplate or machine documentation.

    Start with the torch ID

    Before you pull parts, verify the torch identity at the handle, lead, or machine connection point. Check the torch name, model marking, and any service label on the lead assembly. If the marking is missing or unreadable, compare the physical torch layout against the parts breakdown. Do not assume a PT-17A hand torch uses the same service items as a PT-17AM machine torch without confirming the item numbers.

    Inspect: torch body, head angle, trigger or machine interface, lead condition, and connector style.
    Verify: the model designation and item number on the WSP breakdown before placing an order.

    Troubleshooting and support checks

    For plasma torch complaints, work from the outside in. Start with condition, then fit, then function.

    1) Check the consumable stack

    • Inspect the nozzle, electrode, shield, retaining cap, and any swirl or spacer components for burn damage, oval wear, arc marks, or heavy spatter.
    • Verify that every part is seated fully and matches the torch family listed on the breakdown.
    • If the stack is mixed, damaged, or unknown, stop and identify the item number from the lookup page before reuse.

    2) Inspect the torch head and threads

    • Look for cross-threading, carbon tracking, cracked insulators, or heat distortion.
    • Verify that retaining parts tighten smoothly by hand before using tools.
    • If a part binds, do not force it. Damaged threads can make a correct consumable stack unusable.

    3) Check lead condition and connections

    • Inspect the lead jacket for cuts, flattening, heat damage, and bend fatigue near the torch neck and strain relief.
    • Verify tight electrical and air connections at the torch and machine end.
    • Confirm there are no leaks, loose fittings, or signs of overheating at the connector points.

    4) Verify the symptom against the part

    • Weak start or arc dropout: inspect electrode wear, nozzle condition, and torch connections first.
    • Poor cut face or excessive dross: verify consumable condition and correct torch setup before changing machine settings.
    • Air leakage or unstable operation: inspect seals, O-rings, and connection points if the torch design uses them. Unknown (Verify) if not listed on your specific breakdown.

    If the problem persists after these checks, compare the failed part to the item number in the parts breakdown. Do not order from description alone when the torch family is unclear.

    Using the WSP lookup page

    The WSP page for the ESAB PT-17A / PT-17AM Torch Parts Breakdown provides the item-number structure needed to match a worn part to the correct replacement. Use it as a lookup tool, not as a substitute for confirming the torch model.

    How to use it:

    1. Identify the torch as PT-17A or PT-17AM.
    2. Open the parts breakdown and find the item number on the exploded view or parts list.
    3. Match the failed part to the exact description and location.
    4. Confirm the part before ordering. If the match is incomplete, mark the part Unknown (Verify).

    This matters because plasma consumables and torch hardware can look similar across torch families while still being non-interchangeable. For general verification methods, see Plasma Consumable Compatibility: How to Verify Torch Parts Before Ordering.

    Buying checks before you place the order

    Support teams and maintenance buyers should confirm four points before purchasing any torch part:

    • Torch family: PT-17A or PT-17AM.
    • Item number: match the breakdown, not a generic description.
    • Wear condition: confirm the failed component and any adjacent parts that may be heat-damaged.
    • Machine setup: verify whether the torch is used in hand or machine service, since that can affect the required hardware. Unknown (Verify) if the setup is not documented.

    If the torch is cutting through a drag shield style setup, review the related guidance in Plasma Drag Shield Compatibility Guide: Torch Family, Amperage, Nozzle, Retaining Cap, and Cut Mode Checks before choosing consumables.

    Common failure patterns

    • Repeated nozzle damage: inspect standoff control, torch angle, and consumable fit.
    • Electrode wear that returns quickly: verify air quality, torch assembly condition, and correct part stack.
    • Hard starts or unstable arc: check electrode, nozzle, and internal torch connections.
    • Frequent replacement of the same item: inspect for misassembly, cross-threading, or incorrect torch identification.

    If the torch is showing pilot-arc style failure behavior, the troubleshooting sequence in Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks is a useful support reference.
    Safety notes

    • De-energize the machine before inspecting the torch or changing consumables.
    • Allow hot parts to cool before handling.
    • Do not inspect internal torch components with the power on.
    • Use proper eye protection and hand protection when checking spent consumables and cut hardware.
    • If you find a damaged lead, exposed conductor, or burned connector, remove the torch from service until it is verified safe.

    FAQ

    Are PT-17A and PT-17AM parts automatically interchangeable?

    No. Verify the torch model and match the item number on the WSP breakdown. If the exact match is not clear, treat the part as Unknown (Verify).

    What should I check first when the torch will not cut properly?

    Check the consumable stack first: electrode, nozzle, shield, retaining parts, and fit. Then inspect connections and the torch lead for damage or looseness.

    Can I order by appearance if the old part looks the same?

    No. Similar-looking plasma parts can differ by torch family or configuration. Use the parts breakdown and confirm the item number before ordering.

    Do the linked support articles approve a specific setup?

    No. They are verification guides. Use them as selection starting points, not guaranteed procedure approvals.

    Sources Checked

    Internal note: no filler metal page or product listing was provided for this topic, so none was added.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

Watch with Prime Video