Search results for: “plasma cutter guide”

  • Hypertherm Powermax45 SYNC 088560 Plasma Cutter Fitment and Consumables Guide

    The Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    “>Hypertherm Powermax45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560 is a 45 amp professional plasma cutting system built for metalworkers who need simplified setup, single-piece cartridge consumables, and reliable hand cutting performance. This guide is focused on ordering accuracy: power input, torch configuration, cut capacity, cartridge selection, air supply, and the fitment checks to complete before purchasing consumables or accessories.

    Key Takeaways

    • Arc Weld Store lists this system as Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, SKU 088560.
    • Hypertherm identifies the Powermax45 SYNC as a system for cutting, gouging, and marking with SmartSYNC torch communication and single-piece cartridge consumables.
    • Part number 088560 is the CSA 200โ€“240 V, 1-phase standard power supply configuration with a 75-degree hand torch and 20 ft torch lead.
    • Hypertherm lists recommended cut capacity at 5/8 in. at 20 ipm, severance capacity at 1-1/8 in. at 5 ipm, and pierce capacity at 1/2 in.
    • The system uses clean, dry, oil-free air or nitrogen for cutting and gouging. Air quality should be verified before use to protect cut quality and cartridge life.
    • Cartridge selection matters. Do not order cartridges by appearance alone; verify amperage, process, torch type, and material thickness.

    Product Overview

    The Hypertherm Powermax45 SYNC 088560 is a portable plasma cutting system for fabrication, repair, maintenance, education, HVAC/mechanical work, agricultural repair, and metal shop use. Arc Weld Store lists this configuration with a 20 ft handheld torch and identifies it as a professional plasma cutter for metalworking applications.

    The main advantage of the SYNC platform is simplified consumable management. Instead of stacking separate plasma consumables, Hyperthermโ€™s SmartSYNC platform uses a single-piece cartridge system. Hypertherm also identifies RFID-enabled SmartSYNC torches and cartridges that automatically set amperage and operating mode when correctly paired with the system. That reduces setup mistakes, but it does not remove the need to verify the correct cartridge for the cut type, amperage, torch, and material thickness.

    Upper-middle CTA: Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    “>View this product at Arc Weld Store.

    Best For

    • Fabrication shops cutting mild steel, stainless steel, and aluminum within verified capacity limits.
    • Maintenance teams that need a portable plasma cutter for repair and plant work.
    • HVAC and mechanical contractors cutting sheet, plate, brackets, and field-fit parts.
    • Farm, equipment, and trailer repair where portability and clean cuts reduce grinding time.
    • Training programs that want simplified cartridge selection and reduced consumable stack errors.
    • Metalworkers who want hand cutting first and may later compare compatible mechanized configurations.

    Key Specs

    ProductHypertherm Powermax45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch
    Arc Weld Store SKU088560
    BrandHypertherm
    ConfigurationCSA 200โ€“240 V standard power supply with 75-degree hand torch and 20 ft torch lead
    ProcessesPlasma cutting, gouging, and marking when set up with the correct torch/cartridge configuration
    Input voltage200โ€“240 V, 1-phase, 50/60 Hz
    Input current at 6.9 kW39/32 A at 200โ€“240 V, 1-phase
    Output current9โ€“45 A
    Rated output voltage155 VDC
    Duty cycle at 104ยฐF / 40ยฐC50% at 45 A; 60% at 41 A; 100% at 32 A
    Recommended cut capacity5/8 in. at 20 ipm
    Severance capacity1-1/8 in. at 5 ipm
    Pierce capacity1/2 in. for handheld use or with automatic torch height control
    Typical gouge capacity7.5 lb per hour metal removal; 0.12 in. deep x 0.26 in. wide groove profile
    Gas supplyClean, dry, oil-free air or nitrogen for cutting and gouging; marking gas support depends on setup and cartridge
    Recommended gas inlet flow rate / pressure188 l/min at 5.9 bar; 400 scfh / 6.7 scfm at 90 psi
    Input power cable length10 ft
    Power supply typeInverter โ€“ IGBT
    Engine drive requirement12.5 kVA / 10 kW for full 45 A output
    Dimensions with handles17.4 in. D x 6.8 in. W x 14.1 in. H
    Weight with 20 ft torch31 lb
    Warranty listed by Hypertherm literaturePower supply: 6-year; Torch: 1-year
    CPC / voltage divider / serial portNot listed for 088560 standard configuration; verify before ordering for CNC or mechanized integration

    Compatibility / Fitment Notes

    This product is a complete plasma cutting system configuration, but consumables and accessories still require fitment verification. The most important checks are system part number, torch style, input power, cartridge amperage, gas supply, material thickness, and intended cutting process.

    • System configuration: 088560 is the standard CSA 200โ€“240 V, 1-phase configuration with a 75-degree hand torch and 20 ft lead.
    • Hand cutting: The 75-degree hand torch configuration is appropriate for manual cutting applications when paired with the correct cartridge.
    • Mechanized cutting: Do not assume this 088560 package has CPC, voltage divider, serial communication, machine torch, or remote pendant features. Verify before purchasing for CNC table use.
    • Cartridge fitment: Hypertherm lists Powermax cartridge options for drag cutting, mechanized/standoff cutting, max removal gouging, max control gouging, and FineCut applications. Match the cartridge to the process and amperage.
    • Gas quality: Poor air quality can shorten consumable life and degrade cut quality. Confirm clean, dry, oil-free air before cutting.
    • Power supply: Confirm 200โ€“240 V single-phase power and circuit requirements before ordering. This is not a 120 V plasma cutter.

    Before You Order

    • Confirm the exact Arc Weld Store product SKU: 088560.
    • Confirm your available input power is 200โ€“240 V, 1-phase, 50/60 Hz.
    • Confirm breaker, wiring, plug, receptacle, and extension cord requirements against Hypertherm documentation and local electrical code.
    • Confirm whether you need handheld cutting only or CNC/mechanized capability.
    • Confirm the torch style: this configuration is listed with a 75-degree hand torch and 20 ft torch lead.
    • Confirm the cut thickness range: recommended 5/8 in., severance 1-1/8 in., and pierce 1/2 in.
    • Confirm air compressor capacity, dryness, oil separation, and regulator/filter setup.
    • Confirm cartridge family and amperage before ordering consumables.
    • Confirm whether you need drag cutting, FineCut, gouging, marking, or mechanized/standoff cartridges.
    • Confirm PPE requirements for plasma arc radiation, sparks, fumes, noise, and hot slag.

    Accessories / Compatible Products

    Consumables and accessories should be selected by system part number, torch type, process, and material thickness. Do not assume every SmartSYNC cartridge is correct for this 45 amp hand system. Compatibility must be verified against the Powermax45 SYNC documentation before ordering.

“>Hypertherm SmartSYNC Cartridge or Adapter 45 A Drag Cutting 428927 โ€” relevant for 45 A drag cutting where the cartridge and torch/system fitment are confirmed.
  • Hypertherm SmartSYNC Cartridge or Adapter 30-45 A Hand FineCut 428928
  • “>Hypertherm SmartSYNC Cartridge or Adapter 30โ€“45 A Hand FineCut 428928 โ€” relevant for fine feature hand cutting on thin mild steel and stainless steel where fitment is confirmed.
  • Hypertherm Powermax 30 AIR Portable Plasma Cutter with 15' Lead & Internal Compressor

    Hypertherm Powermax 30 AIR Portable Plasma Cutter with 15' Lead & Internal Compressor

    $2,733.22

    In Stock

    View Product
    “>Hypertherm Powermax 30 AIR Portable Plasma Cutter with 15 ft Lead and Internal Compressor โ€” compare if portability and built-in air supply are more important than 45 amp output.
  • Hypertherm 428162 Kit, Duramax Hyamp Hand Torch Triggger Start Switch Replacement

    Hypertherm 428162 Kit, Duramax Hyamp Hand Torch Triggger Start Switch Replacement

    $29.78

    In Stock

    View Product
    “>Hypertherm 428162 Duramax Hyamp Hand Torch Trigger Start Switch Replacement โ€” replacement torch part category example; compatibility with Powermax45 SYNC SmartSYNC torch is Unknown (Verify).
  • Weld Support Parts Breakdown Reference

    For torch and consumable identification support, review the Hypertherm plasma torch parts breakdown. The page includes Powermax 45 Sync Smart Sync torch listings, including 75-degree hand torch and other torch styles. Use this only as a technical breakdown reference; order from Arc Weld Store after confirming the exact torch, cartridge, and system configuration.

    Common Applications

    Shipping / Returns Notes

    Arc Weld Store lists this product as typically shipping within 1โ€“2 business days, shipping from Corydon, Indiana, with free ground shipping to the lower 48 on qualifying orders. Returns are listed as accepted on unused items in original packaging. For fitment help, Arc Weld Store advises emailing sales@arcweldinc.com with the part number, equipment model, and application before opening an incorrect item.

    FAQ

    What is the Arc Weld Store SKU for this Hypertherm Powermax45 SYNC?

    Arc Weld Store lists the SKU as 088560.

    What torch comes with Hypertherm 088560?

    Hypertherm ordering information identifies 088560 as the CSA 200โ€“240 V standard power supply configuration with a 75-degree hand torch and 20 ft torch lead.

    What input power does the Powermax45 SYNC 088560 require?

    The verified CSA specification is 200โ€“240 V, 1-phase, 50/60 Hz. Confirm your electrical service, plug, receptacle, circuit protection, and local code requirements before ordering.

    How thick can the Powermax45 SYNC cut?

    Hypertherm lists recommended cut capacity at 5/8 in. at 20 ipm, severance capacity at 1-1/8 in. at 5 ipm, and pierce capacity at 1/2 in. for handheld use or with automatic torch height control.

    Does the 088560 package include CNC ports?

    Not confirmed for this standard 088560 configuration. Hypertherm lists separate configurations with CPC port, voltage divider, and serial port options. Verify before buying for mechanized or CNC use.

    Which SmartSYNC cartridge should I buy?

    Choose by process, amperage, torch type, and material thickness. For example, Hypertherm lists cartridge options for 45 A drag cutting, FineCut hand cutting, mechanized/standoff cutting, and gouging. Compatibility: Unknown (Verify) until the exact torch, system, and application are confirmed.

    Can I use shop air with this plasma cutter?

    Yes, when the air supply meets Hypertherm requirements. The system requires clean, dry, oil-free air or nitrogen. Verify compressor capacity, moisture control, filtration, and regulator setup before use.

    Safety Notes

    Sources Checked

    End CTA: Ready to verify power, torch configuration, and consumables? Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    Hypertherm Powermax 45 SYNC Plasma Cutter for Metalworking, 20 Ft. Handheld Torch, 088560

    $3,077.61

    In Stock

    View Product
    “>Check current stock at Arc Weld Store.

  • Plasma Cutter Buying Guide 2025 | Duty Cycle, Cut Capacity & Air Requirements

    Plasma Cutter Buying Guide 2025 | Duty Cycle, Cut Capacity & Air Requirements

    Plasma cutters use ionized gas to cut conductive metals. Choosing the right cutter depends on material thickness, duty cycle, air supply, and cut quality requirementsโ€”not just amperage rating.

    Key Specifications Explained

    Amperage Rating & Cut Capacity

    AmperageRecommended CutMaximum CutTypical Material
    20-30A1/8โ€-3/16โ€1/4โ€Sheet metal, auto body, HVAC
    40-50A1/4โ€-3/8โ€1/2โ€Light fabrication, farm repair
    60-80A3/8โ€-1/2โ€3/4โ€General fabrication, structural steel
    85-100A1/2โ€-3/4โ€1โ€Heavy fabrication, thick plate

    Recommended cut = Clean cut with minimal dross (slag on bottom edge)
    Maximum cut = Severance cut (rough edge, heavy cleanup required)

    Rule of thumb: Buy 20-30% more amperage than your typical material thickness for clean cuts and longer consumable life.

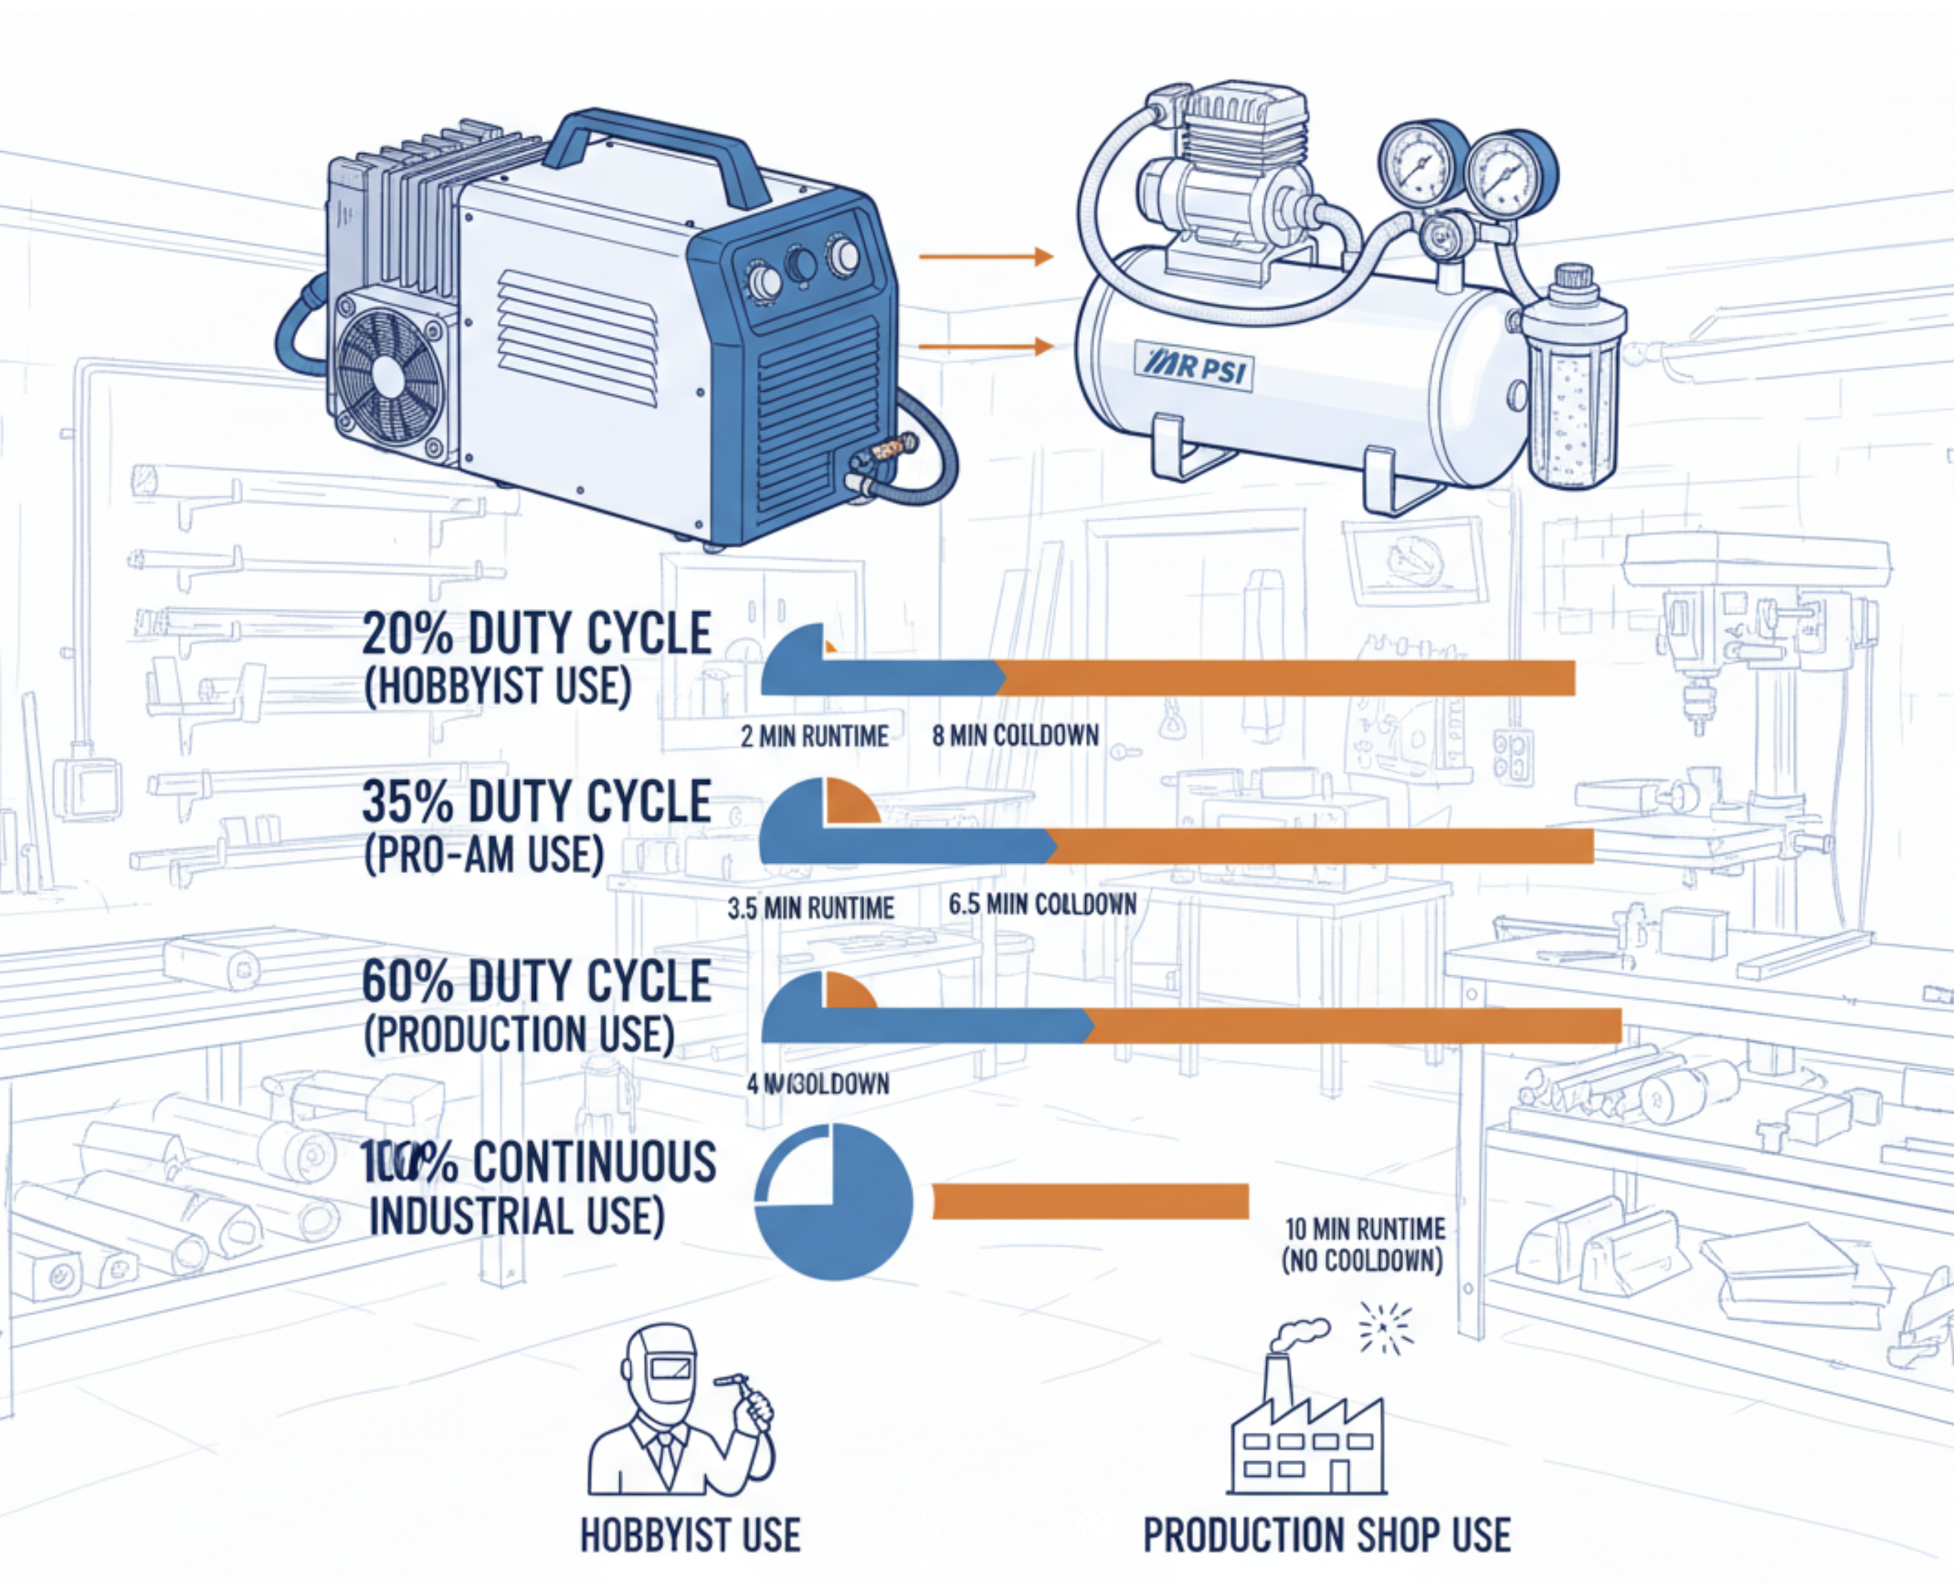
    Duty Cycle

    Definition: Percentage of 10-minute period the machine can run at rated amperage before requiring cooldown.

    Duty CycleRuntime @ Max AmpsCooldownUse Case
    20%2 min8 minHobbyist, occasional use
    35%3.5 min6.5 minLight fabrication, DIY
    60%6 min4 minProduction shop, frequent use
    100%10 min0 minIndustrial, continuous operation

    Example: 50A cutter with 35% duty cycle can run 3.5 minutes at 50A, then must cool 6.5 minutes.
    At lower amperage: Duty cycle increases (50A cutter at 30A may have 60-80% duty cycle).

    Air Supply Requirements

    Compressed Air Specs:Pressure: 60-90 PSI (4-6 bar) – Flow rate: 4-8 CFM @ 90 PSI (varies by amperage) – Quality: Clean, dry, oil-free

    Compressor Sizing:

    Plasma AmperageMinimum CFM @ 90 PSIRecommended Tank Size
    20-30A4 CFM20 gallon
    40-50A5 CFM30 gallon
    60-80A6 CFM60 gallon
    85-100A8 CFM80 gallon

    Air quality issues: – Moisture = premature consumable failure and poor cut quality – Oil contamination = torch tip clogging – Solution: Install inline air dryer/filter between compressor and plasma cutter

    Input Power Requirements

    120V Plasma Cutters:Amperage range: 12-40A – Cut capacity: Up to 3/8โ€ recommended, 1/2โ€ maximum – Advantage: Portable, runs on standard outlets – Limitation: Lower duty cycle, reduced cut speed

    240V Plasma Cutters:Amperage range: 40-100A+ – Cut capacity: 1/2โ€-1โ€+ recommended – Advantage: Higher duty cycle, faster cutting, thicker material – Requirement: Dedicated 240V circuit (30-50A breaker)

    Dual Voltage (120V/240V): – Runs on both voltages with reduced performance on 120V – Example: 50A on 240V, 30A on 120V – Best for: Portable use + shop capability

    Cut Quality Factors

    Pilot Arc vs. Contact Start

    Pilot Arc (High-Frequency Start): – Arc initiates without touching workpiece – Pros: Cuts expanded metal, grating, rusty/painted steel – Cons: Higher cost, can interfere with electronics – Best for: Versatile cutting, field work

    Contact Start (Scratch Start): – Requires torch tip contact with workpiece to start arc – Pros: Lower cost, no electronic interference – Cons: Cannot cut expanded metal or start on edge – Best for: Budget cutters, clean flat plate

    Inverter vs. Transformer Technology

    Inverter-Based:Weight: 10-40 lbs (portable) – Efficiency: High (lower power consumption) – Duty cycle: Typically higher (35-60%) – Cost: Moderate to high – Best for: Modern shops, portability required

    Transformer-Based:Weight: 80-200 lbs (stationary) – Efficiency: Lower (higher power draw) – Duty cycle: Often 100% (industrial use) – Cost: Higher upfront, lower long-term maintenance – Best for: Heavy industrial, continuous operation

    Consumable Costs & Life

    Consumable Components

    PartFunctionTypical LifeCost per Set
    ElectrodeConducts current to arc1-3 hours cutting time$3-$8
    Nozzle (tip)Focuses plasma stream1-3 hours cutting time$2-$5
    Swirl ringStabilizes gas flow5-10 hours$1-$3
    Shield cupProtects nozzle10-20 hours$2-$5

    Consumable life factors: – Amperage setting (higher amps = shorter life) – Air quality (moisture/oil reduces life 50%+) – Arc-on time (duty cycle) – Proper technique (perpendicular torch angle, correct standoff)

    Annual consumable cost estimate: – Hobbyist (20 hours/year): $50-$100 – Light fabrication (100 hours/year): $250-$500 – Production shop (500+ hours/year): $1,500-$3,000

    Material Compatibility

    MaterialPlasma CutNotes
    Mild steelโœ“Best cut quality, minimal dross
    Stainless steelโœ“Clean cuts, some dross on thick sections
    Aluminumโœ“Requires higher amperage than steel (30% thicker capacity)
    Copperโœ“High thermal conductivity = slower cut speed
    Brassโœ“Similar to copper, produces toxic fumes (ventilation required)
    Cast ironโœ“Brittle, may crack from rapid heating
    Galvanized steelโœ“Toxic zinc fumes (ventilation mandatory)

    Cannot cut: Non-conductive materials (wood, plastic, concrete, glass)

    Torch Styles & Ergonomics

    Hand Torch (Standard)

    • Cable length: 10-25 feet
    • Weight: 1-3 lbs
    • Best for: Freehand cutting, portability
    • Limitation: Less precise than machine torch

    Machine Torch (CNC-Compatible)

    • Mounting: Designed for CNC table or track system
    • Standoff: Adjustable height control for consistent cut quality
    • Best for: Automated cutting, production runs
    • Cost: $200-$800 (in addition to hand torch)

    Ergonomic Features

    • Trigger lock: Reduces hand fatigue during long cuts
    • Swivel head: Prevents cable twist, improves maneuverability
    • Insulated grip: Protects from heat during extended use

    Common Mistakes

    Undersizing amperage for material thickness
    40A cutter on 1/2โ€ steel = slow, rough cuts and rapid consumable wear. Size cutter 20-30% above typical thickness for clean cuts.

    Using contaminated air supply
    Moisture and oil in compressed air destroy consumables in 10-20% of normal life. Always use inline air dryer/filter.

    Running at maximum amperage continuously
    Exceeds duty cycle, triggers thermal shutdown. Run at 70-80% of rated amperage for longer duty cycle and consumable life.

    Buying Checklist

    • โœ“ Amperage rating 20-30% above typical material thickness
    • โœ“ Duty cycle matches usage frequency (35%+ for regular use)
    • โœ“ Input voltage compatible with available power (120V or 240V)
    • โœ“ Pilot arc start for versatile cutting (expanded metal, rusty steel)
    • โœ“ Inverter technology for portability and efficiency
    • โœ“ Compressor meets CFM and PSI requirements
    • โœ“ Air dryer/filter included or purchased separately
    • โœ“ Consumable availability and cost verified

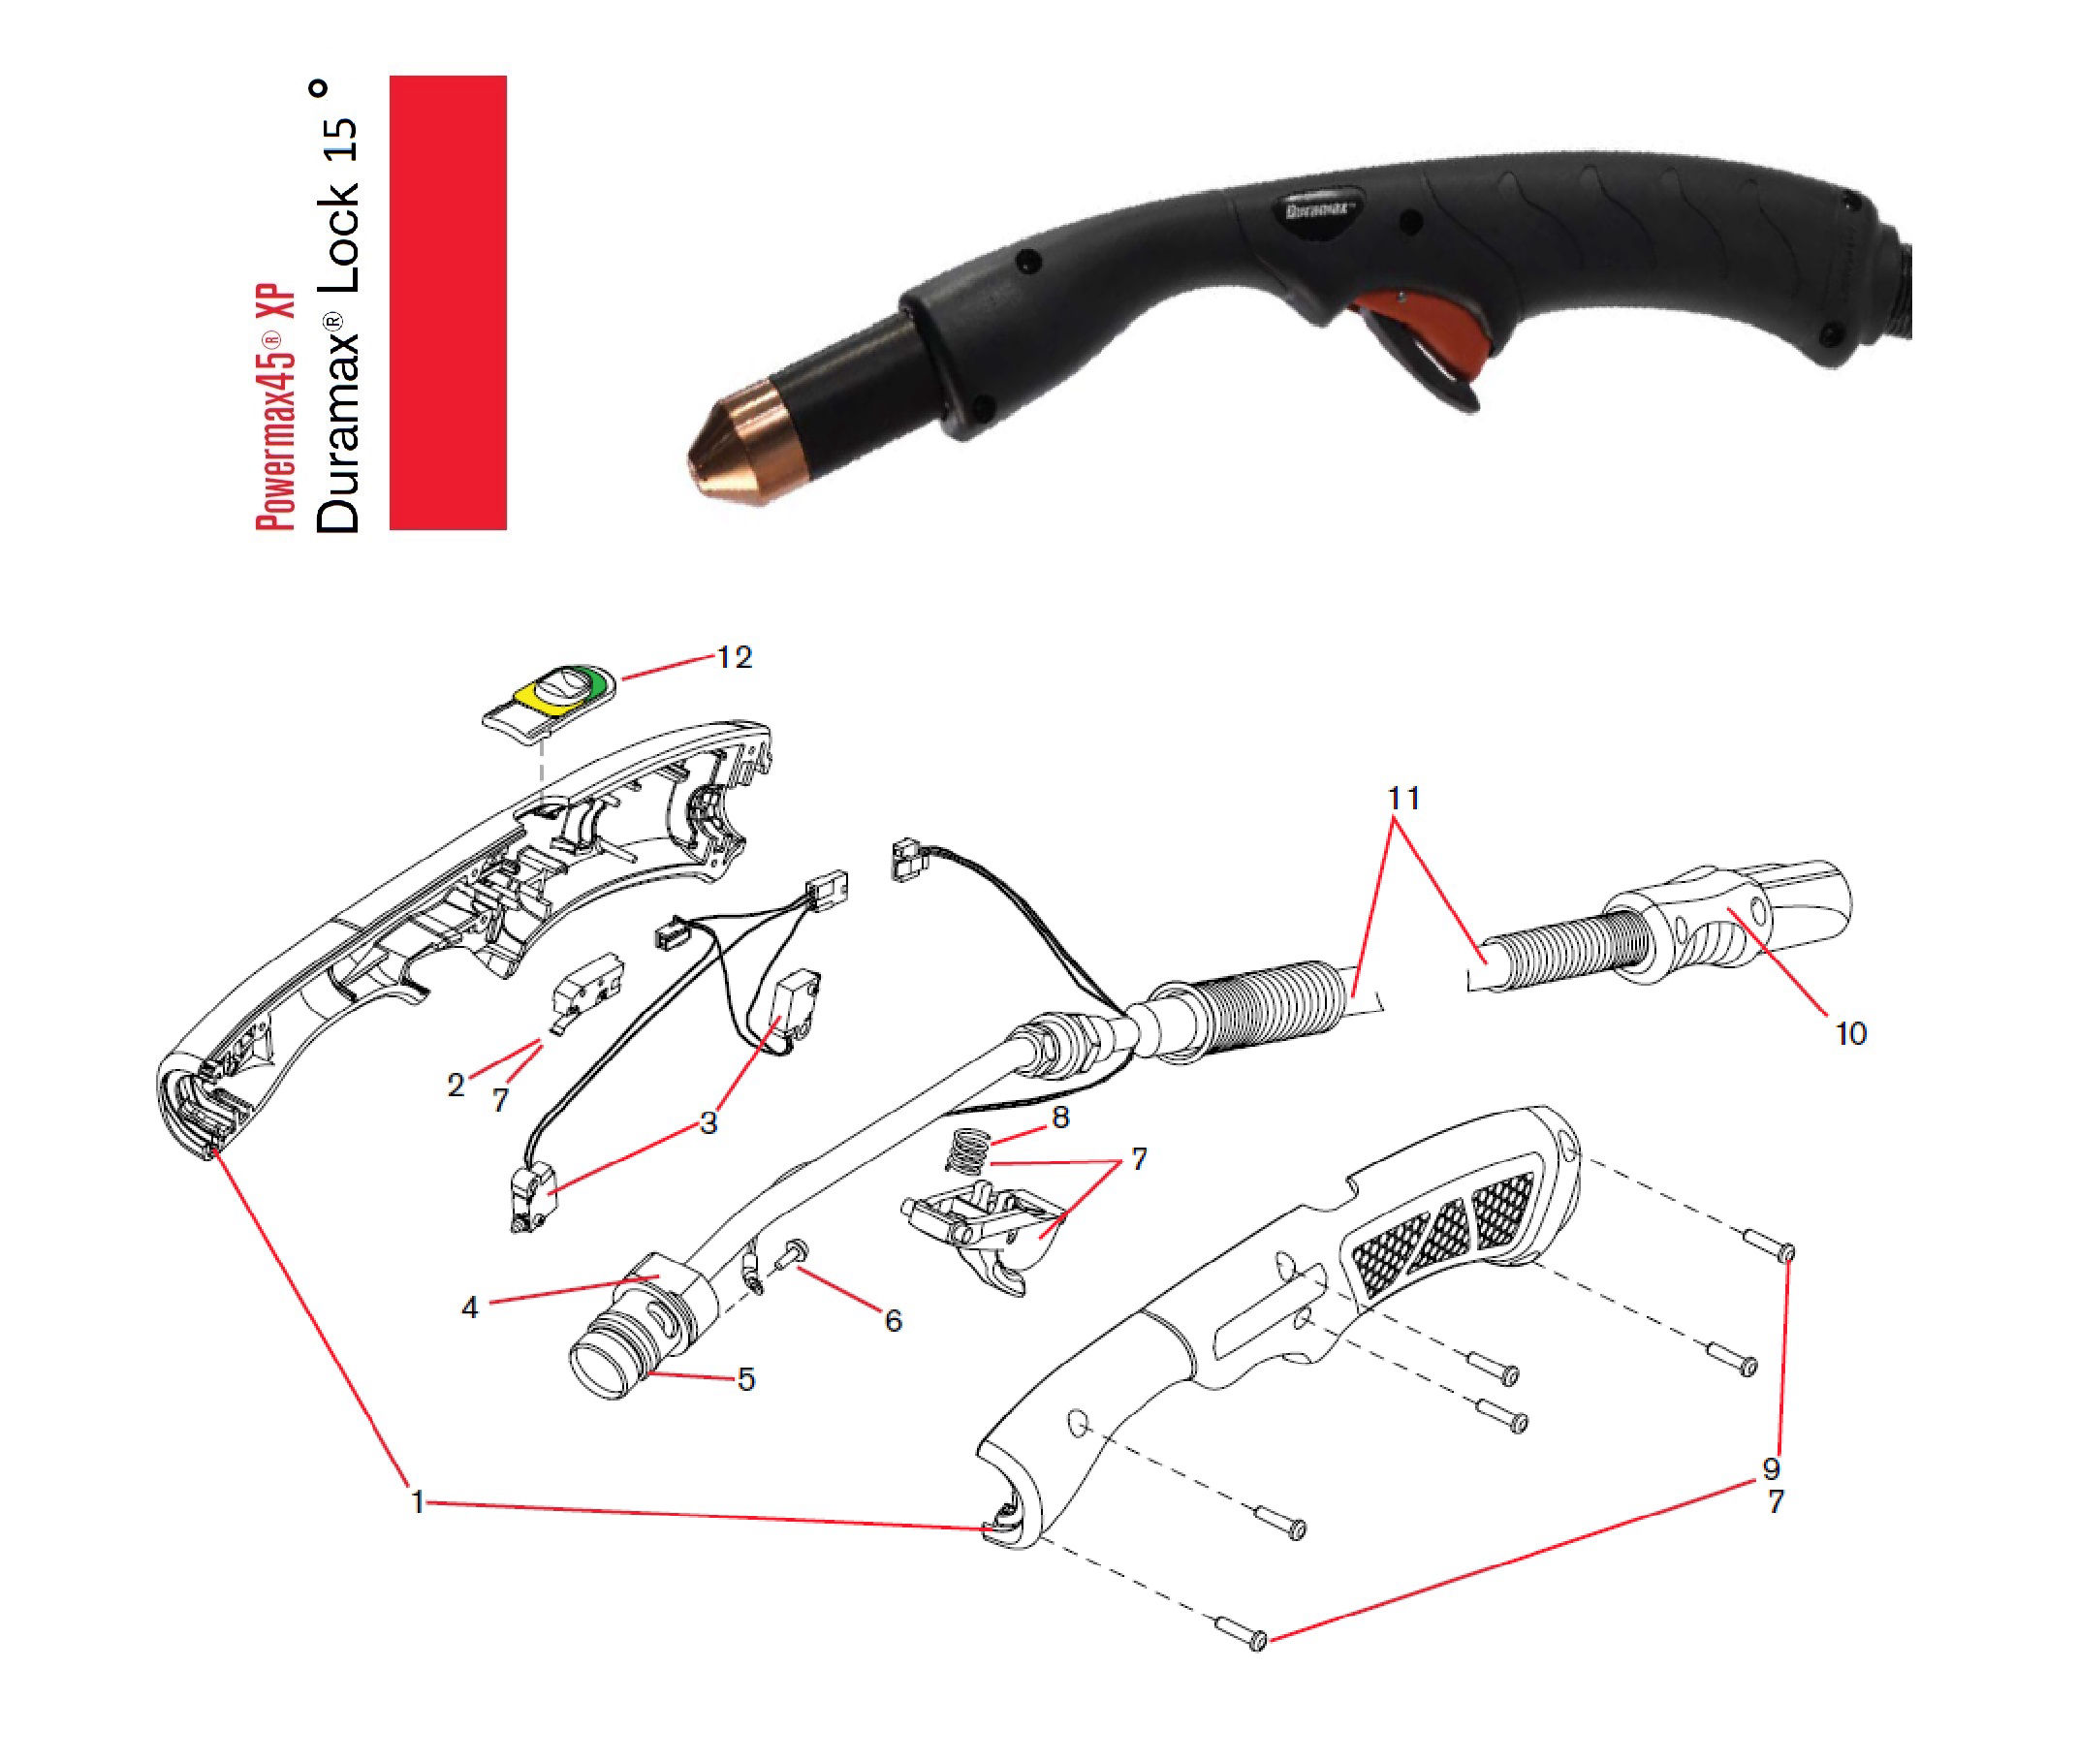
  • Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown

    If you are maintaining a Hypertherm Duramax Lock 15 Degree hand torch, the main job is not guessing part numbers. It is identifying the wear path, matching the torch to the machine context, and confirming the replacement against the catalog before anything is ordered. This is a consumable replacement problem first, and a parts-compatibility problem second.

    Key Takeaways

    • Use the torchโ€™s breakdown page as the starting point, not the final approval step.
    • Confirm the torch style, angle, and lock style before comparing parts.
    • Inspect the nozzle, electrode, shield, swirl ring, and retaining hardware for heat damage, arc misalignment, and physical wear.
    • If fitment is uncertain, stop and verify against the WSP lookup page before ordering.
    • Do not assume a part from another Duramax family torch will fit. Verify each item by catalog reference.

    What This Torch Parts Breakdown Is For

    The Hypertherm Duramax Lock 15 Degree hand torch parts breakdown is useful when you need to replace worn consumables or identify a damaged torch component after poor cut quality, arc instability, or visible heat distortion. In practice, the breakdown helps you separate routine wear items from parts that may indicate a deeper torch issue.

    For this torch, the critical point is to match the exact torch configuration shown on the source page: Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown. That page is the verified lookup source for the torch context provided here.

    How to Work the Replacement Decision

    Start with a visual inspection. Then move to part-by-part verification. Do not replace parts only because cut quality changed; verify the torch condition and the machine setup first.

    Check

    • Check the torch head for heat discoloration, cracks, or arc tracking marks.
    • Check the consumable stack for uneven wear, melted edges, or carbon buildup.
    • Check the lead and handle area for cuts, crushed sections, or loose strain relief.
    • Check the retaining hardware for cross-threading, distortion, or seizure.

    Inspect

    • Inspect the electrode tip for deep crater wear or a collapsed center. If the wear pattern is abnormal, replace and verify arc transfer behavior.
    • Inspect the nozzle orifice for ovality, spatter blockage, or visible deformation.
    • Inspect the shield for heat damage, edge warping, or fit issues at the torch front end.
    • Inspect any swirl ring or internal alignment part for cracks, burns, or contamination.

    Verify

    • Verify the torch model and angle match the catalog listing before selecting a replacement.
    • Verify the part number from the lookup page or linked breakdown page, not from memory.
    • Verify the machine context if the torch is being used on a specific plasma system. If the machine is not clearly identified, treat compatibility as Unknown (Verify).
    • Verify that the replacement set matches the wear pattern you found. If only one part is damaged, do not automatically replace the full stack unless the inspection supports it.

    Common Failure Signs That Point to Consumable Replacement

    Most maintenance calls on plasma torches start with cut quality. That is useful, but not enough. Use the symptoms to guide inspection, then confirm with the part breakdown.

    • Rough edge or heavy dross: often points to nozzle wear, incorrect standoff, or an electrode nearing end of life.
    • Weak start or intermittent arc: may involve the torch front end, pilot arc behavior, or worn internal components. See the related troubleshooting guide for more on arc loss and no-start conditions: Pilot Arc Failure Troubleshooting.
    • Excessive spatter in the front end: check the nozzle and shield for contamination and fit.
    • Unexpected heat at the torch head: inspect for poor consumable seating or a damaged component stack.

    If the torch is producing unstable arc behavior across more than one set of consumables, do not assume the consumables are the only issue. Confirm machine settings, air quality, and lead condition. If the cause is unclear, mark the condition as Unknown (Verify) and cross-check with the machine manual and torch breakdown.

    WSP Lookup Section

    Use the verified WSP source page below to review the torch breakdown and item context before ordering:

    Open the Hypertherm Duramax Lock 15 Degree Hand Torch Parts Breakdown lookup

    This lookup page should be treated as the catalog-backed starting point for identifying the correct parts. If a replacement item is not clearly confirmed on the page, do not guess. Record it as Unknown (Verify) and confirm before purchase.

    Replacement Workflow for Maintenance Teams

    1. Identify the torch style and front-end layout.
    2. Remove the torch consumables and document the wear pattern.
    3. Compare the damaged parts against the breakdown page.
    4. Check whether wear is isolated to the consumables or extends into the torch head and lead.
    5. Verify the replacement part number against the WSP lookup page.
    6. Only then release the order.

    Safety Notes

    • Power down and isolate the plasma system before handling the torch head.
    • Allow the torch and consumables to cool before inspection.
    • Use eye protection when removing hot or stuck consumables.
    • Do not force threaded parts. If a component binds, inspect for damage instead of tightening harder.
    • Use compressed air and cleaning methods that do not introduce debris into the torch front end.

    FAQ

    How do I know if I need a full torch consumable set or only one part?
    Inspect the wear pattern first. If only the nozzle shows normal end-of-life wear and the electrode is still within acceptable condition, a partial replacement may be enough. If multiple parts show heat damage or arc instability, verify whether the full stack should be replaced.

    Can I use another Duramax torch part if it looks similar?
    No. Similar appearance does not confirm compatibility. Use the exact breakdown page and verify each item number before ordering. If the match is not clear, treat it as Unknown (Verify).

    What should I check before blaming the consumables for poor cut quality?
    Check air quality, torch seating, work lead condition, standoff, and machine settings. Consumables are a common cause, but not the only one. If the issue persists after replacement, inspect the torch and power source path.

    Where do I confirm the correct parts?
    Use the verified lookup page linked above. That is the reference source for this torch breakdown.

    Sources Checked

    When the torch condition is unclear, do not force a replacement decision. Inspect, verify, then order. That is the safe path for plasma support work.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Hypertherm Air T30 Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Air T30 Torch Parts Breakdown: Replacement Decision Guide

    Hypertherm Air T30 Torch Parts Breakdown

    The Hypertherm Air T30 torch is a serviceable plasma cutting consumable path, but replacement decisions should start with inspection, not guesswork. A wrong nozzle, electrode, swirl ring, shield, or retaining component can create arc instability, poor cut quality, and repeated part failure. For maintenance buyers and shop support teams, the goal is simple: identify what is worn, confirm what is actually compatible, and replace only the parts that match the torch setup in service.

    Key Takeaways

    • Inspect the torch stack before ordering replacements.
    • Match parts to the exact torch and system path in use; do not assume cross-compatibility.
    • Most plasma consumable issues show up as arc start trouble, unstable cutting, excess dross, or accelerated wear.
    • Use the WSP lookup page as the starting point for the Air T30 service path.
    • When technical details are not confirmed, treat them as Unknown (Verify).

    What to Check First on an Air T30 Torch

    Before replacing anything, isolate the torch from power, shut down the cutter, and allow the system to cool. Then inspect the consumable stack in sequence. Start with the nozzle or tip, electrode, shield, swirl ring, and retaining components. Look for pitting, deformation, heat tint beyond normal service wear, cracked insulating surfaces, or a loose fit at assembly.

    Check the air path as well. Restricted or contaminated air can mimic worn consumables. Verify the air filter, regulator settings, hose condition, and any evidence of oil or water in the line. If air quality is poor, new parts may fail early even when the torch hardware is correct.

    Replacement Decision Guide

    Inspect: Remove the front-end parts and compare them to the torch configuration currently installed. Missing pieces, mixed wear patterns, or uneven burn marks often indicate the torch has been run with mismatched or overdue consumables.

    Verify: Confirm the torch model path against the WSP page for the Hypertherm Air T30. Do not rely on visual similarity alone. Two parts that look close can still differ in dimensions, thread form, or gas flow design. If a part detail is not stated clearly, mark it as Unknown (Verify) rather than assuming a fit.

    Replace: Replace components as a matched set when wear is uneven or when repeated arc transfer issues point to more than one damaged part. A single worn electrode can damage the nozzle, and a damaged nozzle can shorten the life of the next electrode.

    Recheck: After installation, verify that the stack is seated correctly, all retaining parts are secure, and the torch tip is clean. Run a controlled test cut on known material before returning the machine to production.

    Common Symptoms and What They Usually Mean

    Hard start or no start: Check electrode wear, nozzle condition, air pressure, and torch connections. If the pilot arc does not transfer consistently, inspect for contamination, loose assembly, or internal damage.

    Weak or wandering arc: Inspect the nozzle orifice, swirl ring, and air quality. A damaged air path can distort the arc even when the torch appears mechanically sound.

    Excess dross or bevel angle changes: Verify cut speed, torch height, and consumable condition. If the parts are worn unevenly, replace the full front-end stack rather than only the most visible part.

    Repeated consumable failure: Check for overloaded duty conditions, piercing technique problems, poor air quality, or incorrect part pairing. If the failure pattern repeats after replacement, the root cause is usually upstream of the torch tip.

    WSP Lookup Page: Start Here

    Use the WSP lookup page for the Hypertherm Air T30 torch as the first reference point for service part identification and standard consumables in this support path:

    Hypertherm Air T30 Torch Parts Breakdown

    This page should be used as a parts identification starting point, not as a substitute for verifying the actual torch in hand. If a part detail is not fully specified on the page, treat it as Unknown (Verify) and confirm against the torch body, existing consumables, or the machine documentation.

    Practical Inspection Steps Before Ordering

    • Clean the torch front end and remove spatter or dust before inspection.
    • Check the electrode and nozzle for crater wear, chipping, or ovalized openings.
    • Verify that the swirl ring or insulator has no cracks, burns, or distortion.
    • Inspect the retaining cup or shield for heat damage and thread condition.
    • Compare the old part to the replacement by form, seat, and visible geometry, not by part name alone.
    • Confirm the air supply is dry, clean, and within the system requirement; if the requirement is not confirmed, mark it Unknown (Verify).
    • After assembly, check for smooth fit and no cross-threading before energizing the cutter.

    Safety Notes

    Plasma torch parts can remain hot long after shutdown. Wear gloves and eye protection when removing used consumables. Do not handle damaged electrodes or nozzles barehanded if they are still warm. Disconnect power before service. If you see cracked insulation, exposed conductors, or signs of internal torch damage, remove the torch from service until it is inspected by qualified personnel.

    Do not test-fire a torch with uncertain part compatibility. If the part stack is not verified, the machine can arc unpredictably and damage the torch, workpiece, or operator PPE.

    Related Troubleshooting References

    For deeper diagnosis, these related guides can help separate consumable wear from machine-side faults:

    FAQ

    How do I know whether to replace one part or the whole consumable set?
    If wear is isolated and the rest of the stack checks clean, a single part may be enough. If the electrode, nozzle, and shield all show heat damage or uneven wear, replace the set and verify the air supply.

    Can I match parts by appearance only?
    No. Visual similarity is not enough. Verify the torch path, seat geometry, and any stated part details. If a detail is not confirmed, mark it Unknown (Verify) before ordering.

    What if the torch still cuts poorly after new parts are installed?
    Check air quality, work lead condition, cut speed, torch height, and machine output. Consumables are often the symptom, not the root cause.

    Is the WSP page enough to approve a replacement order?
    It is a starting point for identification, but final approval should still be based on the torch in hand, the machine setup, and any confirmed part details.

    Sources Checked

    • WSP lookup page: https://www.weldsupportparts.com/hypertherm-air-t30-torch.html
    • Internal link: Plasma Consumable Compatibility: How to Verify Torch Parts Before Ordering
    • Internal link: Plasma Cutter Pilot Arc Failure Troubleshooting: No Start, Weak Spark, Arc Dropout, and Torch Consumable Checks
    • Internal link: Plasma Torch Nozzle Damage Causes: Orifice Wear, Double Arcing, Piercing, and Air Problems

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

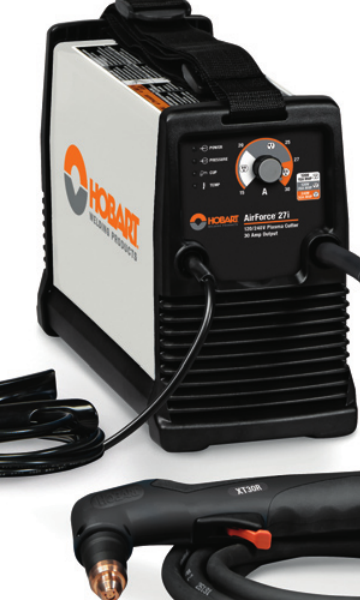
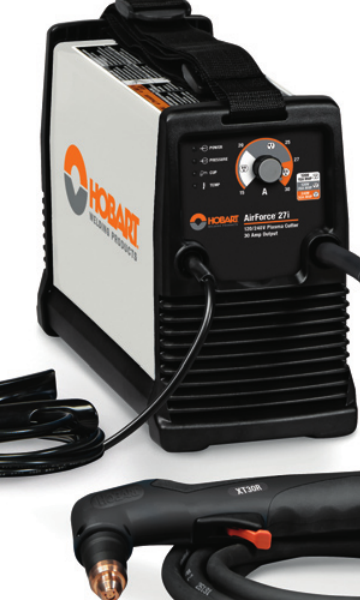
  • Hobart AirForce 27i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 27i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 27i Plasma Cutter Support

    If you maintain a Hobart AirForce 27i, the fastest way to avoid wrong-parts orders is to verify the machine identifier, torch family, power input, and air-side support items before you buy. The AirForce 27i support page from Weld Support Parts is set up as a lookup starting point for those checks. It lists the unit support page, the stock reference 500575, 120/240 V information, an XT30R replacement torch reference, consumables, MVP adapters, an air filter kit, cutting guides, and plasma support links.

    Key Takeaways

    • Use the support page to confirm the AirForce 27i parts path before ordering.
    • Verify torch model, consumable style, and power input at the machine nameplate and on the existing torch.
    • Air quality matters. Inspect the air filter path before troubleshooting arc problems.
    • Do not assume adapter or torch compatibility from appearance alone.
    • When details are unclear, mark them as Unknown (Verify) and confirm against the machine and torch labels.

    What the Support Page Is Useful For

    The Weld Support Parts AirForce 27i page is a parts lookup and support reference, not a substitute for the machine manual. It is useful when you need to match the cutter to support items such as the replacement torch, consumables, and air-side accessories. For this model, the page references stock 500575 and indicates 120/240 V support information. Treat those details as lookup cues and verify them on the machine before purchasing or installing parts.

    Open the Hobart AirForce 27i support page

    Buying Checks Before You Order Parts

    Before a maintenance buyer releases an order, do these checks in order:

    1. Check the machine data plate. Verify the exact model is Hobart AirForce 27i and confirm input power requirements. If the plate is unclear, record Unknown (Verify).
    2. Inspect the torch neck and handle label. Confirm whether the installed torch matches the XT30R family reference shown on the support page. Do not assume the torch is original.
    3. Pull the consumable set and compare wear patterns. Look at the nozzle, electrode, swirl ring, shield, and retaining parts. Replace only with the correct style for the torch in use.
    4. Check the air delivery path. Inspect filters, fittings, hoses, and water or oil contamination. A plasma cutter with poor air quality will often show unstable arc behavior.
    5. Confirm adapter needs. If the shop uses an alternate power plug or input arrangement, check whether the MVP adapter reference is relevant to your setup. Compatibility details not shown on the support page should stay Unknown (Verify).

    Troubleshooting and Support Checks

    Use these checks when the cutter starts to misbehave or when you are deciding which support part to buy.

    1) Torch and Consumable Check

    • Inspect: Look for heat damage, cracked cups, eroded electrodes, and loose retaining parts.
    • Verify: Match the torch consumables to the actual torch family on the machine. If the torch label is unreadable, mark the torch type Unknown (Verify) until confirmed.
    • Replace: Only the parts that are visibly worn or listed for the identified torch family.

    2) Air Supply Check

    • Inspect: Air filter kit condition, bowl contamination, hose leaks, and regulator settings.
    • Verify: The shop air is dry and clean enough for plasma use. If you see oil, water, or heavy debris, correct that before blaming the torch.
    • Check: Flow remains stable during trigger pull. A pressure drop can mimic a bad torch or bad consumable.

    3) Power and Input Check

    • Inspect: Input cord, plugs, adapters, and receptacle condition.
    • Verify: The machine is connected to the correct input class shown for the AirForce 27i support reference. If the exact electrical setup is not confirmed, note it Unknown (Verify).
    • Check: Any adapter or extension is rated and approved for the actual jobsite setup. Do not use an adapter just because the plug shape fits.

    4) Cut Quality Check

    • Inspect: Edge squareness, dross, and arc consistency.
    • Verify: The torch is held at a consistent standoff and travel speed.
    • Check: The cut guide or drag shield is appropriate for the work method you are using.

    WSP Lookup Page Notes

    The AirForce 27i support page is the correct first stop when you need a parts and support overview for this machine. It identifies the machine support page, stock 500575, the XT30R replacement torch reference, consumables, MVP adapters, air filter kit, cutting guides, and other plasma support links. Use those references to narrow the search, then confirm exact fitment against the machine and torch markings.

    Important: This page is a selection aid, not a blanket approval for every installed torch or accessory. If the part family is not confirmed from labels or existing component markings, the correct status is Unknown (Verify).

    Go to the Hobart AirForce 27i support page

    Practical Inspection Routine for Shops

    For routine maintenance, use a short inspection routine before each parts order or service ticket:

    • Record the machine model and serial tag information.
    • Compare torch markings to the support page reference.
    • Pull the last installed consumables and note wear pattern.
    • Inspect air filters and moisture traps.
    • Check the power plug, adapters, and cord strain relief.
    • Confirm any cutting guides or accessories are intended for the actual torch setup.

    Safety Notes

    • De-energize the machine before inspecting internal or electrical components.
    • Bleed pressure from the air system before opening filters or fittings.
    • Do not touch hot consumables immediately after cutting.
    • Use eye, hand, and body protection suitable for plasma cutting and grinding cleanup.
    • Do not bypass safety devices or use unverified adapters in an attempt to make a part fit.

    FAQ

    Is the XT30R replacement torch definitely the correct torch for every AirForce 27i?

    No. The support page references XT30R as a replacement torch reference, but you should still verify the torch family on the machine and existing torch. If the installed torch is not confirmed, mark it Unknown (Verify).

    Can I order consumables just by machine model?

    Not safely. Consumables must match the actual torch family and installed setup. Start with the AirForce 27i support page, then verify the torch label and worn parts before ordering.

    What should I check first if the cutter will not make a stable arc?

    Start with the consumables and the air supply. Inspect electrode and nozzle wear, then verify that air is clean, dry, and steady. If those checks are inconclusive, move to power input and torch condition.

    Are the MVP adapters universal?

    Do not assume that. The support page lists MVP adapters as a support reference, but any actual compatibility must be confirmed against the machine and power setup. If it is not confirmed, use Unknown (Verify).

    Sources Checked

    For maintenance teams, the key is simple: verify the machine, verify the torch, verify the air, then buy the parts that match what is actually installed. That is the cleanest way to support a Hobart AirForce 27i without creating avoidable returns or downtime.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

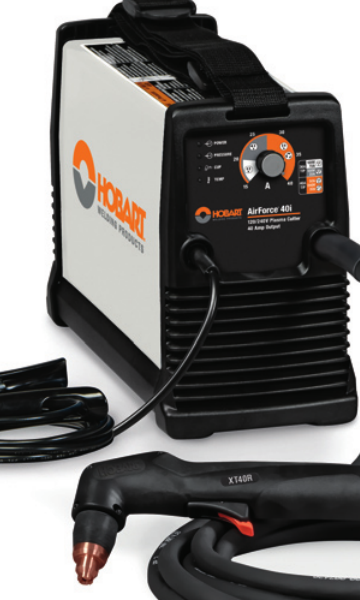
  • Hobart AirForce 40i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 40i Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 40i Plasma Cutter Support

    The Hobart AirForce 40i is a compact plasma cutter support topic that usually comes down to four checks: input power, torch condition, consumable wear, and air quality. If the machine is cutting poorly or not starting, the fastest path is to verify the torch setup and the air supply before replacing parts. This guide is built for parts lookup and buying checks, not a repair manual. Use it to confirm what to inspect, what to match, and what to verify before ordering.

    Key Takeaways

    • Confirm the machine identification and stock reference before ordering any support part.
    • The listed support page for this unit references a replacement XT40R torch, consumables, MVP adapters, an air filter kit, and cutting guide support.
    • Do not assume a torch, adapter, or consumable is correct from appearance alone. Verify by model reference and connector style.
    • For cutting problems, check air pressure/flow, torch consumables, lead condition, and work lead attachment before replacing the power source.
    • Use the WSP lookup page as the primary reference for the support page and linked parts path.

    What to verify first on a Hobart AirForce 40i

    Start with the machine nameplate and the support reference. The provided WSP lookup page identifies the Hobart AirForce 40i support page with stock 500576 and 120/240 V specifications. Verify the exact unit label on your machine, because buying decisions depend on the input version and the torch package, not just the model name. If the machine has been moved between shops, it may be wired differently than expected. Unknown (Verify) whether your specific installation is set up for 120 V or 240 V service until you check the nameplate and receptacle.

    Check: machine name, serial or stock reference, input voltage, torch type, and connector style.

    Inspect: power cord, plug, torch lead, trigger cable, and air line for damage or heat discoloration.

    Verify: the torch package against the support page before ordering consumables or adapters.

    Troubleshooting and support checks

    1) No start or weak arc

    If the torch does not initiate, or the arc starts weakly and drops out, isolate the basics first.

    • Check that the machine is powered correctly and the breaker is not marginal under load.
    • Inspect the torch tip, electrode, and swirl ring for wear, erosion, or contamination.
    • Verify the air supply is dry and clean. Moisture or oil can shorten consumable life and cause arc instability.
    • Check the work clamp connection and the cut table contact path.

    If the torch parts are visibly worn, replace the full consumable set rather than mixing old and new parts. Mixed wear states can make troubleshooting harder.

    2) Poor cut quality

    When the machine starts but cut quality is inconsistent, focus on air and consumables before assuming a power source fault.

    • Inspect the nozzle for oval wear or spatter damage.
    • Check whether the torch stand-off or hand motion is too fast or too slow for the material being cut.
    • Verify the air filter kit condition if water or debris is present in the line.
    • Inspect the torch lead for cuts, tight bends, or repeated abrasion at the work area.

    Do not buy replacement parts until you confirm which failure mode is present. A bad nozzle, dirty air, and low input power can produce similar symptoms.

    3) Torch and adapter fit checks

    The support page references an XT40R replacement torch and MVP adapters. Those items should be treated as model-specific support parts. Before ordering, match the torch family, connector interface, and any adapter callout shown on the support page. Unknown (Verify) whether any adapter is required for your existing setup until you confirm the current torch package and machine configuration.

    • Check the printed torch model reference.
    • Inspect the connector ends for wear, bent pins, or damaged locking features.
    • Verify the replacement torch is the exact support path listed for this machine.

    WSP lookup page: use it as the starting point

    The provided WSP lookup page is the main source for this support topic:

    Hobart AirForce 40i Plasma Cutter Support

    Use that page to confirm the machine support path, the stock 500576 reference, and the listed support categories. The page references consumables, XT40R replacement torch support, MVP adapters, an air filter kit, cutting guides, and related plasma support links. That makes it a parts lookup starting point, not a blanket approval for every accessory you may see elsewhere.

    Buying check: match the item to the machine and torch package before adding it to a quote or cart.

    Verify: whether the part is a direct replacement, a service accessory, or a support accessory that only applies to a specific configuration.

    Practical part selection checks

    • Consumables: replace as a set when wear is visible or cut quality changes.
    • Torch assembly: confirm the torch model before ordering. Do not assume a different torch in the same family will fit without verification.
    • Air filter kit: choose this when the air line shows moisture, particulate, or oil contamination.
    • MVP adapters: verify the machine-side and torch-side connection points before buying.
    • Cutting guides: confirm the guide style works with your hand technique and work envelope.

    Safety notes

    Plasma cutters involve high voltage, hot metal, compressed air, and intense arc radiation. Disconnect input power before opening access panels or handling internal connections. Bleed stored air pressure before servicing the air system. Replace damaged torch leads or worn consumables before operation. Use approved eye, face, hand, and body protection for plasma cutting. Keep the work area dry and free of flammables.

    FAQ

    What is the first part I should inspect on an AirForce 40i with arc issues?

    Inspect the consumables first, then verify air quality and work lead connection. Those are the most common support checks before replacing the torch or power source.

    Can I order a replacement torch from appearance alone?

    No. Verify the torch model reference and connector style first. The support page references an XT40R replacement torch, but you should confirm the exact machine and torch package before buying.

    Do the listed accessories mean every item is required?

    No. The support page is a parts lookup starting point. Some items, such as an air filter kit or MVP adapter, may only be needed if your current setup has a matching need. Verify against your machine configuration.

    How do I know if the input power is correct?

    Check the machine nameplate and the site wiring. The provided support page references 120/240 V specifications, but your installed service must still be verified at the machine and receptacle.

    Sources Checked

    Use the support page as the primary reference, then verify the machine condition and part match before ordering. That reduces avoidable returns and prevents mismatched torch or consumable purchases.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

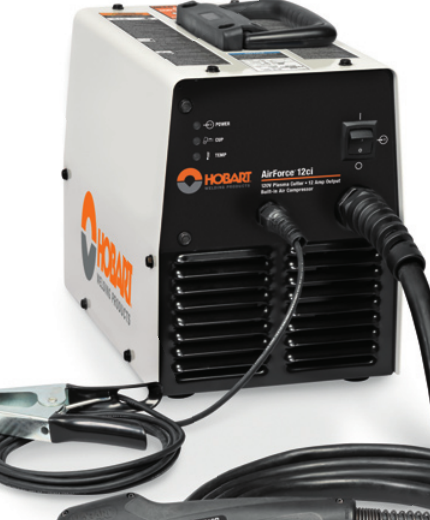
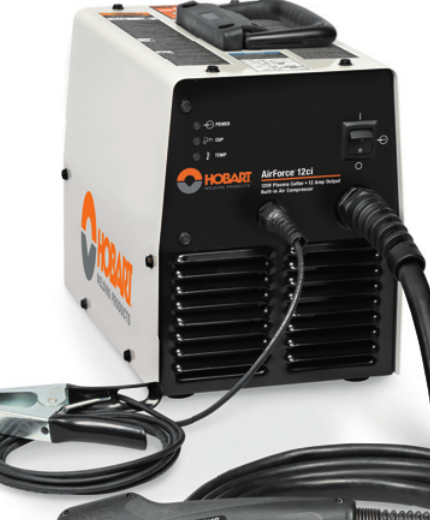
  • Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 12ci Plasma Cutter Support: Parts Lookup and Buying Checks

    Hobart AirForce 12ci Plasma Cutter Support

    The Hobart AirForce 12ci is a compact plasma cutter support case where the buying risk is usually not the cutter itself, but the parts that keep it running: torch fitment, consumables, protective gear, and whether the replacement item matches the machineโ€™s input and torch family. This guide is built to help welders, fabricators, and maintenance buyers verify the basics before ordering.

    Key Takeaways

    • Use the Hobart AirForce 12ci support page as the first parts reference before you buy.
    • Verify torch model, consumable type, and input power before ordering any replacement item.
    • Do not assume a plasma torch, consumable kit, or cover fits because it looks similar.
    • Check wear items first: nozzle, electrode, shield, swirl ring, retaining parts, air supply, and cable condition.
    • Safety glasses and a protective cover are support items, not optional extras.

    Start with the WSP lookup page

    The primary support page for this unit is here: Hobart AirForce 12ci Plasma Cutter Support. The page indicates stock 500564 and lists 120 V specs, XT12R replacement torch, consumable kits, safety glasses, and a protective cover. Treat those listings as the starting point for verification, not as a substitute for checking your exact machine and torch tag.

    Check before you order

    • Inspect the machine label: confirm the model is Hobart AirForce 12ci, not a similar unit.
    • Verify input power: the support page shows 120 V specs. Confirm your unit nameplate and outlet setup match.
    • Inspect the torch tag: confirm whether the unit uses the XT12R replacement torch listed on the support page.
    • Check consumable wear: look for recessed electrode, enlarged nozzle orifice, heat damage, cracks, or unstable arc start.
    • Verify cable and lead condition: cuts, melted sections, or loose strain reliefs can mimic consumable failure.

    Troubleshooting and support checks

    If the cutter is not performing well, the fastest path is a basic inspection sequence. Start simple and document what you find.

    1) No start or weak start

    • Check: power source status, plug condition, and supply voltage at the receptacle.
    • Inspect: trigger switch, torch lead, and any visible torch damage.
    • Verify: the consumables are installed correctly and are not worn beyond serviceable condition.

    2) Arc starts but cut quality is poor

    • Check: air pressure and air quality at the cutter.
    • Inspect: nozzle, electrode, shield, and retaining parts for spatter buildup or heat distortion.
    • Verify: the work clamp is clean and attached to bare metal.

    3) Arc drops out during cutting

    • Check: thermal condition of the machine and duty cycle usage pattern.
    • Inspect: torch lead for intermittent breaks or damaged insulation.
    • Verify: the air supply is steady and dry. Moisture can cause unstable operation and consumable damage.

    4) Consumables wear too quickly

    • Check: cutting technique, standoff distance, and travel speed.
    • Inspect: whether the nozzle is being run beyond normal wear indicators.
    • Verify: you are using the correct consumable kit for the torch family. If uncertain, use Unknown (Verify) until the exact kit is matched.

    Parts lookup buying checks for this model

    For the Hobart AirForce 12ci, the most useful parts categories are torch replacement, consumable kits, and protective items. The support page points to an XT12R replacement torch, but buyers should verify the torch family, connector style, and lead length against the existing machine before ordering. Unknown (Verify) should be used for any detail that is not confirmed by the machine label or the support page.

    Replacement torch check

    • Inspect: the old torch for model markings, connector type, and damage location.
    • Verify: the new torch is listed for the same support page and matches the original torch family.
    • Confirm: no modification is required for fitment unless the manufacturer states otherwise.

    Consumable kit check

    • Inspect: all wear components removed from the torch.
    • Compare: thread shape, size, and seating surfaces.
    • Verify: the kit is intended for the same torch model, not just a similar plasma system.

    Protective gear and cover

    • Check: whether the shop already stocks plasma-rated eye protection.
    • Inspect: the machineโ€™s storage location for dust, slag, and moisture exposure.
    • Verify: a protective cover will not trap heat when the machine is warm after use.

    Use the internal guides as support references

    If the cutter is giving you symptoms beyond basic wear, these related articles can help narrow the fault before you order parts:

    Safety notes

    • Disconnect power before inspecting torch leads, consumables, or internal connections.
    • Use eye protection and hand protection when checking the torch or removing worn parts.
    • Do not use damaged leads, cracked torch bodies, or loose consumable assemblies.
    • Verify ventilation and keep flammables clear of the cutting area.
    • If a part fitment is uncertain, mark it Unknown (Verify) and confirm through the machine label, torch tag, or support listing before use.

    FAQ

    What should I verify first for Hobart AirForce 12ci parts?

    Verify the machine model, input power, and torch family first. Then check consumables, cable condition, and air supply quality.

    Is the XT12R replacement torch listed on the support page the correct part for every unit?

    Unknown (Verify). The support page lists XT12R, but you should confirm the torch tag and connector style on your specific machine before ordering.

    How do I know if the problem is consumables or the torch?

    Inspect the nozzle, electrode, and shield first. If wear is visible or the arc is unstable, consumables are often the first suspect. If the lead, trigger, or torch body is damaged, the torch may need replacement.

    Can I buy based on similar-looking plasma parts?

    No. Similar appearance does not confirm fitment. Match the part to the support page and the machine tag, then verify before purchasing.

    Sources Checked

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Thermal Dynamics 8-4025, Plasma Lubricant, Pack of (1): Replacement Part Breakdown

    No products found.

    Thermal Dynamics 8-4025, Plasma Lubricant, Pack of (1) is a support item used in plasma cutting maintenance workflows. For buyers and maintenance teams, the main question is not just what the item is, but where it fits in the service routine, what it can and cannot solve, and what should be checked before it is put into service. For this product, the verified Amazon identifier is B0044FK0XY. Any deeper technical detail beyond the product listing should be treated as Unknown (Verify) unless confirmed by the equipment manual or supplier documentation.

    Key Takeaways

    • This is a plasma cutting support item, not a cutting torch, consumable kit, or machine assembly.
    • Use it as part of a maintenance plan, not as a fix for worn internal parts, damaged leads, or airflow faults.
    • Compatibility with any specific plasma system is Unknown (Verify) unless confirmed by the manufacturer or the machine manual.
    • Before use, check the equipment manual, service procedure, and worksite handling requirements.
    • For sourcing, the verified product reference is Thermal Dynamics 8-4025, Plasma Lubricant, Pack of (1) B0044FK0XY.

    What This Part Is Used For

    Lubricants in plasma support applications are generally used to reduce friction, support maintenance activities, or assist with service-related handling. The exact application for this item is Unknown (Verify) from the product reference alone. Do not assume it is intended for torch internals, O-rings, seals, cutting tips, or automated system components unless the equipment documentation says so.

    If you support production equipment, treat this as a controlled maintenance item. Verify where it belongs in the process, how it is applied, and whether any residue is acceptable on the specific machine or work area.

    Replacement Part Breakdown

    This listing is for a pack of one. Beyond that, the product page identifier does not confirm formulation, container size, application method, or temperature rating. Those details are Unknown (Verify).

    • Product name: Thermal Dynamics 8-4025, Plasma Lubricant, Pack of (1)
    • Amazon ASIN: B0044FK0XY
    • Package count: 1
    • Exact chemistry: Unknown (Verify)
    • Exact equipment compatibility: Unknown (Verify)
    • Certifications: Unknown (Verify)

    For maintenance buyers, that means the purchase decision should be driven by confirmed machine need, not assumption. Cross-check the part number against the service manual, service bulletin, or approved supplier list.

    Check, Inspect, Verify Before Ordering

    • Check: The machine model, torch family, and service procedure that calls for this lubricant.
    • Inspect: The current maintenance issue. If the problem is arc instability, torch damage, or airflow restriction, a lubricant alone will not correct it.
    • Verify: The exact part number 8-4025 in the manual or parts list.
    • Verify: Whether the application point is external service hardware, torch-related service points, or another assembly.
    • Check: Whether the work area requires any contamination control before applying a lubricant.
    • Inspect: Any warning notes about seals, plastics, elastomers, or post-application cleanup.

    Troubleshooting and Support

    If you are using a lubricant in a plasma cutting support role, start with the failure mode. Do not default to part replacement before the underlying issue is checked.

    • If motion feels stiff: Check for dirt, heat damage, worn bearings, or misalignment before applying lubricant.
    • If torch performance is poor: Inspect consumables, gas flow, power settings, and ground path. Do not assume lubricant is relevant.
    • If residue is present where it should not be: Verify whether the lubricant is approved for that location. Remove contamination per the machine procedure.
    • If the part number does not match: Stop and verify the revision or alternate part number in the equipment documentation.
    • If the application instruction is unclear: Use the manufacturer manual or support channel. Unknown (Verify) is the correct status until you confirm it.

    For recurring support issues, create a simple job record: machine ID, torch type, date of service, part number used, and the observed result after application. This helps distinguish a true maintenance improvement from a temporary symptom change.

    Product and Parts Notes

    This product should be treated as a maintenance consumable or support item, not a high-value replacement assembly. Because the public listing does not confirm material data or compatibility scope, buyers should not rely on general assumptions from other lubricants in the plasma category. Use the exact part number only where the equipment documentation supports it.

    If you are building a spare-parts shelf, label it clearly: manufacturer name, part number, intended equipment family, and storage controls if any are required. If those controls are not stated in the documentation, they remain Unknown (Verify).

    Safety Notes

    • Follow the equipment manual before applying any lubricant to plasma cutting equipment.
    • Keep lubricant away from cutting paths, electrical contact points, and surfaces where contamination could affect performance.
    • Use normal shop controls for chemical handling, including gloves, ventilation, and cleanup procedures where required by the product label.
    • Do not assume the product is suitable for every seal, hose, plastic, or coated surface.
    • If the labeling or SDS is unavailable, stop and verify before use.

    Buyer Guidance

    For maintenance buyers, the key question is whether this exact part number is listed in your approved spares plan. If it is, buy to the documented need. If it is not, verify the substitution path before ordering. A plasma support lubricant can be useful, but only when it matches the service requirement. Do not purchase based on brand recognition alone.

    If you need to compare the exact listing, the verified Amazon product reference is available through the product shortcode:

    No products found.

    .

    FAQ

    Is Thermal Dynamics 8-4025 a consumable for cutting performance?
    Not directly. It is a plasma support lubricant listing. Any performance benefit depends on the intended maintenance application, which is Unknown (Verify) without the manual.

    Can I use this on any plasma cutter?
    No assumption should be made. Compatibility is Unknown (Verify) unless the manufacturer documentation lists the exact part number for your machine or torch family.

    What should I check before installing or using it?
    Check the equipment model, inspect the service point, and verify the part number against the official parts list. Also confirm any contamination or cleanup requirements.

    Does the product listing confirm specifications or certifications?
    No. Specifications, certification status, and detailed formulation are Unknown (Verify) from the provided product reference alone.

    Sources Checked

    • Provided Amazon ASIN registry entry: B0044FK0XY
    • Provided product name: Thermal Dynamics 8-4025, Plasma Lubricant, Pack of (1)
    • Provided task metadata and buyer-guide instructions

    Where technical details were not confirmed by the provided sources, they are marked Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • Plasma Cutter Not Piercing Cleanly

    Hypertherm 220674 Plasma Cutting Shield - T45v Hand Cutting Shield, 1 Pack
    “>Hypertherm 220674 Plasma Cutting Shield - T45v Hand Cutting Shield, 1 Pack

    If a plasma cutter is not piercing cleanly, the usual cause is a setup problem rather than a major machine fault. Start with air quality, consumable condition, ground connection, torch angle, and pierce technique. Small errors in any of these areas can leave a ragged start, excessive dross, or a failed pierce.

    Key Takeaways

    Troubleshooting Steps

    1. Check air pressure and air quality

    Plasma cutting depends on clean, dry, correctly regulated air. Low pressure can produce a weak, unstable arc. Water, oil, or heavy contamination can cause sputtering and poor pierce quality.

    2. Inspect consumables

    Worn or damaged consumables are a common reason a plasma cutter is not piercing cleanly. The electrode and nozzle must be in good condition for a focused arc.

    3. Verify ground clamp placement

    Poor work return can make the arc start erratically and cause a messy pierce. The clamp must make solid metal-to-metal contact on clean material.

    4. Check pierce height and torch angle

    If the torch is too close, molten metal can blow back into the shield and nozzle. If it is too high, the arc can spread and fail to pierce cleanly.

    5. Reduce pierce demand on thicker or coated material

    Thick plate, rusty plate, painted plate, and galvanized material can make piercing harder. Start with a clean spot if possible. If the plate is thick, give the arc enough time to fully transfer before moving.

    6. Check torch and machine condition

    If air, consumables, and grounding are correct but the pierce still fails, inspect the torch body, leads, and machine output for damage. Intermittent cable faults, heat damage, or loose connectors can reduce performance.

    Product / Parts Support

    When consumables or shielding parts are worn, replace them with the correct torch parts. For hand cutting shield support, see:

    Hypertherm 220674 Plasma Cutting Shield - T45v Hand Cutting Shield, 1 Pack

    Hypertherm 220674 Plasma Cutting Shield – T45v Hand Cutting Shield, 1 Pack

    Introducing the Hypertherm 220674 Hand Cutting Shield, your essential companion for plasma cutting tasks. This high-quality plasma cutting shield is designed to protect both your workspace and yourself. Made by Hypertherm, a trusted name in plasma cutting technology, this product ensures superior performance and durability. The Hypertherm Hand Cutting Shield is perfect for both professionals and DIY enthusiasts. I…

    View at Arc Weld Store

    Hypertherm 220674 Plasma Cutting Shield – T45v Hand Cutting Shield, 1 Pack

    Use only if it matches the torch model and application. Compatibility for your machine is Unknown (Verify) unless confirmed by the torch manual or parts list.

    Safety Notes

    FAQ

    Why does my plasma cutter start but not pierce cleanly?

    Most often it is low air pressure, contaminated air, worn consumables, or poor ground contact.

    Can a bad shield cause poor piercing?

    Yes. A damaged or incorrect shield can affect arc focus and increase spatter. Verify the correct shield for the torch model.

    Should I drag the torch during the pierce?

    Only if the torch and process are designed for drag operation. Otherwise, maintain the correct standoff distance and start upright. Unknown (Verify).

    What is the fastest test for a bad pierce issue?

    Check air pressure, replace visibly worn consumables, and clean the ground point. Those three checks solve many start-up problems.

    Sources Checked

    Related Weld Support Guides

  • Lincoln Electric FlexCut 45 Plasma Cutter Troubleshooting, Consumables, and Air Supply Setup

    If your Lincoln Electric FlexCut 45 plasma cutter is producing excessive dross, struggling to maintain arc stability, refusing to transfer the pilot arc, or rapidly consuming tips and electrodes, the problem is often related to air quality, consumable wear, grounding issues, or incorrect setup. Operators commonly mistake these symptoms for a failed torch or power supply when the root cause is frequently restricted airflow, incorrect consumable installation, poor work clamp connection, or moisture contamination in the air system.

    The FlexCut 45 is designed for handheld plasma cutting applications where consistent air delivery, proper consumable fitment, and clean electrical connections are critical. Before replacing expensive components, verify the torch consumables, inspect swirl rings and retaining caps, confirm compressor output, and check for contamination inside the torch head. Many intermittent arc faults and poor cut quality complaints are resolved during basic inspection and setup verification.

    Common FlexCut 45 Symptoms

    • Pilot arc starts but will not transfer to the workpiece
    • Heavy bottom-edge dross during mild steel cutting
    • Uneven kerf width or wandering cut path
    • Torch consumables burning up quickly
    • Intermittent torch shutdowns during extended cutting
    • Arc sputtering or unstable plasma stream
    • Difficulty piercing thicker material
    • Poor cut edge quality on clean steel
    • Excessive moisture inside torch consumables
    • Torch overheating during continuous operation

    Most Likely Causes

    • Low inlet air pressure or restricted airflow
    • Moisture contamination from the compressor system
    • Incorrect tip and electrode installation
    • Worn electrode hafnium insert
    • Damaged retaining cap or swirl ring
    • Poor work clamp grounding
    • Torch lead damage or excessive bending
    • Incorrect amperage selection for material thickness
    • Improper torch stand-off distance
    • Using damaged or mixed consumable sets

    Quick Diagnostic Checks

    Inspection AreaWhat To CheckTypical Problem
    Air SupplyDry, stable compressed airMoisture causing unstable arc
    ElectrodeInspect hafnium pit depthHard starts and weak arc
    Tip OrificeRound, undamaged openingWandering or angled cuts
    Ground ClampClean metal contactPilot arc will not transfer
    Torch CableKinks, cuts, heat damageIntermittent cutting
    Cooling AirflowVentilation openings clearThermal shutdown

    Consumable Wear Indicators

    One of the most common FlexCut 45 service mistakes is replacing only the electrode or only the tip after severe wear. Plasma consumables function as a matched system. If the electrode is deeply worn, the tip orifice may already be distorted from unstable arc behavior. Running mixed-wear consumables often creates poor cut quality and shortens the life of new parts.

    • Electrode pit becoming excessively deep
    • Tip opening becoming oval-shaped
    • Visible torch spatter buildup inside retaining cap
    • Burn marks on swirl ring surfaces
    • Difficulty maintaining consistent stand-off
    • Double arcing inside the torch

    Air System Problems and Moisture Contamination

    Compressed air quality directly affects plasma cutter performance. Oil contamination, excessive moisture, and fluctuating compressor output will dramatically reduce consumable life. Operators frequently assume the plasma cutter itself has failed when the actual issue originates upstream in the air system.

    Install a properly sized filter and dryer system whenever possible. Drain compressor tanks regularly and inspect inline separators for saturation. If the torch begins cutting inconsistently after long run times, moisture buildup may be accumulating in the airline.

    Cut Quality Problems

    Excessive dross and bevel angle are usually setup-related rather than machine failure. Travel speed, torch height, consumable condition, and amperage selection all affect cut quality. Dragging the torch incorrectly or holding excessive stand-off distance can quickly produce rough edges and slag accumulation.

    • Slow travel speed often creates heavy bottom dross
    • Excessive stand-off can widen the kerf and reduce penetration
    • Worn tips produce angled or uneven cuts
    • Poor grounding causes unstable transfer arc behavior
    • Dirty steel surfaces may reduce arc consistency

    Field Fix vs Proper Repair

    Some operators temporarily restore cutting performance by cleaning consumables or increasing air pressure, but these fixes usually provide limited improvement if the consumables are already damaged. Severely worn electrodes and distorted tips should be replaced rather than reused.

    Likewise, wrapping leaking air fittings with thread tape may reduce leakage temporarily, but recurring pressure instability should be corrected with proper regulator, hose, or fitting replacement.

    Related Failure Paths

    • Dirty air systems accelerate torch wear
    • Damaged consumables increase nozzle overheating
    • Poor grounding stresses pilot arc components
    • Overheating from blocked ventilation may shorten internal component life
    • Incorrect extension cord sizing can create voltage instability

    Compatibility and Setup Notes

    • Machine Model: Lincoln Electric FlexCut 45
    • Process Type: Air plasma cutting
    • Input Requirements: Verify OEM specifications before installation
    • Compressed Air Requirement: Clean and dry compressed air required
    • Torch Compatibility: OEM consumables recommended
    • Extension Cord Compatibility: Verify conductor size and amperage rating
    • Generator Compatibility: Unknown (Verify)

    Safety Notes

    Plasma cutting systems generate intense ultraviolet radiation, molten metal spray, noise, and electrically energized components. Operators should use approved welding PPE including shaded eye protection, gloves, flame-resistant clothing, and respiratory protection where required. Keep combustible materials away from cutting areas and ensure adequate ventilation for fumes and airborne particulates.

    Never service torch consumables with power connected to the machine. Allow components to cool before inspection and replacement.

    Frequently Asked Questions

    Why does the pilot arc start but not transfer?

    The most common causes are poor grounding, contaminated material surfaces, worn consumables, or insufficient air pressure.

    Why are my consumables wearing out so fast?

    Moisture contamination, incorrect torch distance, excessive pierce height, or damaged airflow components are common causes of premature wear.

    Can dirty compressed air damage the torch?

    Yes. Moisture and oil contamination can destabilize the plasma stream and rapidly damage electrodes and tips.

    Sources Checked

    • Lincoln Electric FlexCut 45 OEM product information
    • Lincoln Electric equipment catalogues
    • Lincoln Electric expendable parts guide
    • General welding safety guidance and PPE documentation
  • More posts

    Stream with Amazon Music