Search results for: “mig wire guide”

  • MIG Birdnesting Troubleshooting Guide: Causes, Fixes & Wire Feed System Compatibility

    MIG wire birdnesting is one of the most common wire feed failures in both hobby and production welding environments. The problem usually appears as tangled welding wire packed behind the drive rolls or inside the feeder area after the wire stops feeding correctly.

    Birdnesting is trending heavily across welding forums, repair searches, and support communities because modern inverter MIG welders, long gun cables, soft aluminum wire, worn liners, and incorrect drive roll tension continue creating feed reliability problems.

    This guide explains the most common causes of MIG birdnesting, how to diagnose the failure correctly, compatibility issues between consumables and feeder systems, and what to inspect before replacing parts.

    Key Takeaways

    • Most birdnesting starts because wire feed resistance exceeds drive roll control.
    • Incorrect drive roll tension is one of the most common causes.
    • Worn liners frequently create intermittent feed drag.
    • Soft aluminum wire increases birdnesting risk dramatically.
    • Long MIG gun cables increase feed resistance.
    • Oversized or damaged contact tips commonly trigger burnback and birdnesting.
    • Poor wire spool tension can overload the drive system.
    • Knurled rolls used on solid wire can deform wire and worsen feeding.

    What MIG Birdnesting Looks Like

    Birdnesting occurs when welding wire stops moving through the gun normally while the drive rolls continue feeding wire. The wire then collapses and tangles near the feeder assembly, creating a compact โ€œbird nestโ€ of wire.

    This usually happens:

    • Behind the drive rolls
    • At the inlet guide
    • Inside the feeder housing
    • Near the gun connection block

    Common Symptoms

    SymptomLikely CauseSeverityCommon Related Part
    Wire bunches at feederExcessive feed resistanceHighLiner
    Burnback into tipFeed interruptionHighContact tip
    Intermittent feedingDirty or worn linerMediumMIG liner
    Wire shavingIncorrect drive rollsMediumDrive rolls
    Feed motor slippingImproper tension settingsMediumDrive assembly
    Aluminum wire collapsingPush distance too longHighMIG gun

    Most Common Causes of MIG Birdnesting

    1. Incorrect Drive Roll Tension

    Excessive drive roll pressure crushes welding wire and increases drag inside the liner. Insufficient pressure allows slipping.

    Proper tension normally allows the wire to stop against resistance without severe wire deformation.

    2. Worn or Dirty MIG Liner

    Liners collect metal dust, rust particles, wire shavings, and contamination over time. Increased liner resistance is one of the leading causes of feed instability.

    Steel liners eventually wear grooves internally, especially with high wire volume production welding.

    3. Wrong Drive Roll Type

    Drive roll selection must match wire type.

    Wire TypeRecommended Roll TypeNotes
    Solid steel wireV-grooveMost common MIG setup
    Flux-core wireKnurledImproves traction
    Aluminum wireU-groovePrevents wire deformation
    Soft alloy wireU-grooveReduces crushing

    4. Contact Tip Restrictions

    Undersized, worn, or partially blocked contact tips create wire drag and feed stoppage.

    Burnback often starts after wire movement slows at the contact tip.

    5. Long MIG Gun Cable Length

    Long gun assemblies increase wire friction. This becomes significantly worse with aluminum wire and small-diameter solid wire.

    Many birdnesting issues appear after upgrading from a 10 ft gun to a 15โ€“25 ft assembly without adjusting feeder settings.

    6. Aluminum Wire Feeding

    Soft aluminum wire is highly prone to collapsing under drive roll pressure. Push-only feeding systems commonly struggle with aluminum over long cable distances.

    Spool guns and push-pull systems are often used specifically to reduce aluminum birdnesting problems.

    Compatibility Notes

    Before replacing MIG feed components, verify:

    • Wire diameter
    • Drive roll style
    • Liner diameter
    • MIG gun length
    • Wire type
    • Contact tip size
    • Feeder compatibility
    • Gun amperage rating
    • Spool gun compatibility
    • Drive roll groove sizing

    Unknown (Verify) for imported MIG gun consumable interchangeability unless OEM documentation confirms compatibility.

    Inspection & Troubleshooting Steps

    1. Disconnect welding power.
    2. Remove the contact tip.
    3. Feed wire manually through the gun.
    4. Check for drag or resistance.
    5. Inspect drive roll wear.
    6. Verify drive roll type matches wire.
    7. Reduce excessive tension pressure.
    8. Inspect liner contamination.
    9. Check inlet guide alignment.
    10. Inspect spool brake tension.
    11. Replace damaged contact tips.
    12. Test feed speed under load.

    Parts Most Commonly Responsible

    PartFailure ModeCommon Wear SignsVerify Before Ordering
    MIG linerFeed dragErratic wire movementWire diameter & gun length
    Drive rollsWire slippingPolished groovesGroove style & wire size
    Contact tipBurnbackOval openingWire diameter
    Gun neckFeed restrictionExcessive heatGun series
    Inlet guideWire shavingSharp edgesFeeder compatibility
    Spool hub brakeExcess dragJerky spool movementMachine model

    What Usually Wears Out First

    • Contact tips
    • MIG liners
    • Drive roll grooves
    • Inlet guides
    • Gun neck strain points
    • Feeder tension springs

    Field Fix vs Proper Fix

    ProblemTemporary FixProper Repair
    Minor liner dragBlow out linerReplace liner
    BurnbackTrim wire and replace tipCorrect feed restriction
    Wire slippingIncrease tension slightlyReplace worn drive rolls
    Aluminum birdnestingShorten gun cableUse spool gun or push-pull system

    Common Wrong-Part Mistakes

    • Using knurled rolls with solid wire
    • Installing oversized liners
    • Using incorrect contact tip size
    • Running aluminum wire through worn steel liners
    • Using excessively long MIG guns for soft wire
    • Installing generic consumables without verifying fitment

    Related Failure Paths

    • Burnback failures
    • Porosity from unstable arc
    • Drive motor overload
    • Excess spatter
    • Wire shaving contamination
    • Contact tip overheating
    • Gun neck overheating

    Safety Notes

    • Disconnect machine power before feeder inspection.
    • Sharp wire ends can puncture gloves and skin.
    • Do not adjust drive rolls while feeding wire.
    • Overheated contact tips remain hot after welding stops.
    • Damaged liners can create erratic arc behavior.

    FAQ

    Why does aluminum wire birdnest more easily?
    Aluminum wire is softer and collapses more easily under feed pressure.

    Can a dirty liner cause birdnesting?
    Yes. Increased drag inside the liner is one of the most common causes.

    Should I increase drive roll tension to stop slipping?
    Excessive tension often worsens birdnesting by deforming the wire.

    Do spool guns help prevent birdnesting?
    Yes. Spool guns reduce wire push distance and improve aluminum feed reliability.

    Can incorrect contact tips cause feed issues?
    Yes. Undersized or damaged tips frequently create wire drag and burnback.

    Next Step

    Most MIG birdnesting problems can be solved by correcting liner condition, drive roll setup, wire path resistance, and consumable compatibility before replacing the entire gun assembly.

    Sources Checked

    • WeldingWeb symptom discussions
    • Reddit MIG wire feed troubleshooting discussions
    • Manufacturer MIG gun documentation
    • Drive roll compatibility references
    • Field troubleshooting reports
    • MIG feeder setup documentation
  • Erratic MIG Wire Feeding: Troubleshooting Guide

    Erratic MIG wire feeding usually starts in the wire path, not the voltage knob. Before changing weld settings, check the contact tip, liner, drive rolls, spool brake, gun lead position, and wire size match-up.

    Key Takeaways

    • Start at the gun end: nozzle, contact tip, diffuser area, and liner.
    • Drive roll tension should be just tight enough to feed without crushing the wire.
    • Wire size, contact tip size, liner size, and drive roll groove must match.
    • If feed improves when the gun cable is straight, suspect liner drag, cable damage, or a kinked liner.
    • Do not use voltage or wire-speed changes to hide a mechanical feed problem.

    Problem / Context

    Erratic feeding shows up as surging arc length, wire stubbing into the puddle, drive rolls chirping, birdnesting at the feeder, burnback into the contact tip, or inconsistent wire speed at the arc. The common causes are restriction, slipping, crushed wire, incorrect consumable sizing, spool drag, or a worn feed component.

    Main Support Section: Fast Diagnosis Path

    SymptomLikely CauseCheckFixNotes
    Wire surges or stuttersWorn contact tip, dirty liner, tight gun cable bendRemove contact tip and feed wire with cable straightReplace tip; inspect or replace linerIf feed improves without the tip, the restriction is near the gun end.
    Drive rolls spin but wire does not moveLow tension, wrong groove, worn rolls, liner restrictionInspect wire after rolls for shaving or flatteningReset roll tension and verify groove size/typeDo not simply crank tension higher.
    Birdnest at feederDownstream restriction or excess spool overrunCheck tip, liner, cable bends, spool brakeReplace restricted consumables; adjust hub tensionBirdnesting often means the feeder is pushing against a blocked path.
    Burnback into contact tipWire feeding slows, tip wrong size, worn tip, liner dragCompare tip size to wire diameterInstall correct fresh tip and verify linerBurnback is often a feed problem before it is a settings problem.
    Copper dust near drive rollsExcess roll pressure, wrong groove, wire shavingOpen feeder and inspect rolls/guidesClean feeder; reduce pressure; verify rollsDust can migrate into the liner and create repeat failures.

    Compatibility / Verification Notes

    Verify torch series, machine model, connector type, amperage rating, wire size, gas type, cable length, consumable family, lens size, OEM part number, and connector configuration.

    For MIG feed problems, the most important fitment checks are wire diameter, contact tip size, liner size/range, drive roll groove size, drive roll groove type, gun connection, and feeder style. Lincoln Electric documentation notes that the contact tip, liner, and drive rolls should match the wire size. Miller gun and feeder manuals also list damaged contact tips, incorrect drive roll groove, hub tension, dirty liners, and worn drive rolls as wire-feed troubleshooting points.

    Inspection or Troubleshooting Steps

    1. Turn the welder off before opening the feeder or handling drive rolls.
    2. Clip the wire cleanly and inspect it after the drive rolls. Flattened wire means too much pressure or the wrong groove.
    3. Straighten the gun cable and test feed. If feeding improves, suspect liner drag or cable damage.
    4. Remove the nozzle and contact tip. Feed wire again. If it feeds smoothly, replace the contact tip and inspect the diffuser/nozzle area.
    5. Confirm contact tip size matches the wire diameter.
    6. Confirm liner size/range matches the wire diameter and gun length.
    7. Confirm drive roll groove size and groove type match the wire. Solid wire commonly uses V-groove rolls; flux-cored wire often requires knurled rolls. Unknown (Verify) for the specific feeder and wire.
    8. Clean drive rolls and inlet/outlet guides. Remove copper dust, wire shavings, and debris.
    9. Set drive roll tension using the minimum pressure that feeds reliably without slipping.
    10. Adjust spool hub tension so the spool does not overrun when the trigger is released but does not drag heavily during feeding.
    11. Run a test bead only after the mechanical feed path is smooth.

    Parts / Consumables Table

    PartFunctionWear SignsVerify Before OrderingNotes
    Contact tipTransfers welding current to the wire and guides wire exitBurnback, oval hole, spatter blockage, blueing, inconsistent arcWire size, thread style, gun series, OEM part numberFastest low-cost test for erratic feeding.
    Gun linerGuides wire through the MIG gun cableDrag, dust, kink, wire feeds better when cable is straightWire size/range, gun model, length, trim procedureA dirty or kinked liner can make good drive rolls look bad.
    Drive rollsPush wire from spool into gun linerSlipping, worn groove, wire shaving, poor tractionWire size, groove type, feeder model, roll diameterWrong groove size can crush or under-drive the wire.
    Wire guide tubesKeep wire aligned through feederGrooving, burrs, poor alignment, wire shavingFeeder model and wire diameterOften missed during repeated birdnest problems.
    Spool hub / brakeControls spool drag and overrunCoasting spool, birdnesting, heavy dragMachine feeder designToo loose causes overrun; too tight causes feed resistance.
    MIG wireElectrode and filler metalRust, kink, cast issue, contamination, inconsistent unwindingWire diameter, alloy/classification, process, shielding gasRusty or damaged wire can contaminate the liner.

    Common Wrong-Part Mistakes

    • Installing a .035 contact tip with .030 wire, or the reverse.
    • Changing the contact tip but leaving a dirty liner in place.
    • Using a smooth V-groove roll on wire that needs a different groove style. Unknown (Verify).
    • Ordering a liner by wire size but not confirming gun length or torch series.
    • Assuming all โ€œLincoln-styleโ€ or โ€œTweco-styleโ€ consumables fit every gun.
    • Replacing the drive motor before checking restriction in the gun cable.

    Related Failure Paths

    Erratic wire feeding can lead to burnback, birdnesting, poor starts, inconsistent penetration, excessive spatter, poor bead shape, porosity from unstable arc behavior, and premature contact tip wear.

    Related internal support pages: MIG wire feed slipping fix, wire feeding support topics, contact tip burnback support, drive roll support topics, and MIG wire feed support.

    Field Fix vs Proper Fix

    SituationField FixProper FixRisk If Ignored
    Tip is partially blockedReplace contact tipReplace tip and inspect diffuser/nozzle for spatter buildupBurnback and unstable arc return quickly
    Liner is dirtyBlow out only if allowed by shop procedureReplace liner with correct size and trim correctlyRepeated slipping and birdnesting
    Roll tension is too highBack off pressure and retestClean rolls, inspect wire, reset tension correctlyCrushed wire and liner contamination
    Spool brake is too looseTighten slightly to stop overrunSet hub tension per machine manualBirdnesting when trigger is released

    Safety Notes

    • Turn off input power before opening the feeder, changing rolls, or servicing the gun.
    • Keep fingers clear of drive rolls and moving wire.
    • Wear safety glasses under the welding helmet when clipping wire or clearing birdnests.
    • Use proper welding PPE for arc radiation, sparks, spatter, and hot metal.
    • Follow the machine manual before changing feeder parts or working near energized equipment.
    • Do not test-feed wire toward your hand, body, gas hose, or another person.

    FAQ

    Why does my MIG wire feed fine in the air but stutter while welding?

    The contact tip may be worn, overheated, spatter-blocked, or the wrong size. Liner drag can also increase when the gun cable bends during welding.

    Should I tighten the drive rolls when wire feeding is erratic?

    Only after checking for restriction. Too much drive roll pressure can flatten the wire, create copper dust, and plug the liner.

    Can a bad liner cause burnback?

    Yes. A dirty, kinked, or wrong-size liner can slow wire feeding enough for the wire to burn back into the contact tip.

    How do I know if the contact tip is the problem?

    Remove the contact tip and feed wire with the gun cable straight. If feeding becomes smooth, the tip or front-end consumables are likely restricting the wire.

    What should match the wire size?

    At minimum, verify the contact tip, liner size/range, drive roll groove, and feeder guide setup against the machine or gun manual.

    Next Step

    If the wire feed is erratic, replace the contact tip first, straighten the gun cable, test feed with the tip removed, inspect the wire after the drive rolls, and verify the liner and drive rolls match the wire. If the issue remains, inspect the liner and wire guides before suspecting the drive motor.

    Sources Checked

    • Miller owner manuals: wire feed troubleshooting references for contact tip, drive roll pressure, drive roll groove, hub tension, dirty liner, and worn rolls.
    • Lincoln Electric operator/service manuals: matching contact tip, liner, and drive rolls to wire size; overload causes from improper tip, liner, drive rolls, guide tubes, obstructions, and cable bends.
    • Lincoln Electric MIG problems and remedies resource.
    • OSHA 1910 Subpart Q welding, cutting, and brazing standards.
    • OSHA eye protection guidance for welding and cutting.
    • Weld Support Parts internal MIG wire feed, burnback, wire feeding, and drive roll support pages.
  • Washington Alloy THF-700HT-173 Hard Face Flux-Cored MIG Wire Fitment Guide

    Washington Alloy THF-700HT-173 is a .045 in. hard face flux-cored MIG wire supplied on a 33 lb spool for rebuilding worn steel parts exposed to metal-to-metal abrasion. This article is built to help maintenance shops, repair departments, and industrial buyers verify whether this hardfacing wire matches the job before ordering.

    For current availability, order verification, and shipping details, Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

    “>view this product at Arc Weld Store.

    Key Takeaways

    • Product: Washington Alloy THF-700HT-173 hard face flux-cored MIG wire.
    • Size: .045 in. wire on a 33 lb spool.
    • Primary use: high metal-to-metal abrasion applications.
    • Deposit structure: martensitic; designed to work harden in service.
    • Common applications include rollers, conveyor screws, crusher rolls, and mill hammers.
    • Verify machine capacity, drive rolls, liner size, polarity, shielding gas, and base metal condition before ordering.

    Product Overview

    Washington Alloy 700HT is a hardfacing flux-cored wire intended for wear-facing work where abrasion resistance is more important than general fabrication weld strength. The Arc Weld Store listing describes this product as primarily used for high metal-to-metal abrasion. The manufacturer technical data states that 700HT produces martensitic weld deposits that work harden in service and bond well with fatigued or older hard-faced deposits.

    This is not a general-purpose ER70S-6 replacement. It should be selected when the repair objective is wear resistance on appropriate steel components, not when the job requires a mild steel structural filler wire.

    Upper-middle CTA: Need the .045 in. 33 lb spool? Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

    “>check current stock at Arc Weld Store before scheduling the repair.

    Best For

    • Industrial maintenance hardfacing.
    • Metal recovery on worn steel components.
    • High abrasion areas where parts see metal-to-metal wear.
    • Crusher rolls, mill hammers, conveyor screws, rollers, and similar wear parts.
    • Repair departments that need a full 33 lb spool for recurring hardface work.

    Key Specs

    FieldVerified Detail
    BrandWashington Alloy
    ProductTHF-700HT-173 Hard Face Flux-Cored MIG Wire
    SKUTHF-700HT-173 – 1 SPOOL
    Wire diameter.045 in.
    Spool weight33 lb
    Wire typeHardfacing flux-cored wire
    Polarity from manufacturer procedureDCEP
    Typical .045 in. procedure rangeWire speed 195โ€“475 ipm; amps 125โ€“245; volts 25โ€“29; electrical stickout 1/2โ€“1 in.; CO2 35โ€“45 cfh
    Mixed gas noteManufacturer TDS notes 1โ€“2 volts lower used with mixed gas
    Typical hardnessRockwell C 58โ€“61 per manufacturer TDS
    Typical weld metal chemistryCarbon, chromium, manganese, silicon, molybdenum, tungsten, nickel, vanadium, phosphorus, sulfur listed by manufacturer TDS
    AWS classificationUnknown (Verify)
    CertificationsUnknown (Verify)

    Compatibility / Fitment Notes

    Fitment for this product is less about torch model and more about whether your MIG or FCAW system can correctly feed and run .045 in. hardfacing flux-cored wire. Before ordering, verify that your feeder accepts 33 lb spools, your drive rolls match .045 in. flux-cored wire, your gun liner is sized correctly, and your power source can run the required amperage and voltage range.

    Compatibility with a specific welding machine, feeder, gun, liner, drive roll, contact tip, shielding gas blend, or base metal is Unknown (Verify) unless confirmed against your equipment documentation and the manufacturer procedure data.

    Before You Order

    • Machine model: Confirm your welder can run .045 in. FCAW hardfacing wire in the required output range.
    • Wire feeder: Verify 33 lb spool capacity and hub compatibility.
    • Drive rolls: Confirm the correct .045 in. flux-cored drive roll style. Compatibility: Unknown (Verify).
    • Gun liner: Confirm the liner supports .045 in. wire and is clean enough for consistent feed.
    • Contact tips: Use contact tips sized for .045 in. wire. Brand and series compatibility: Unknown (Verify).
    • Polarity: Manufacturer procedure data lists DCEP.
    • Shielding gas: Manufacturer procedure data lists CO2 ranges and notes lower voltage with mixed gas. Verify your exact procedure.
    • Base metal: Confirm the part is suitable for hardfacing and that previous deposits, cracking, or contamination are addressed.
    • Preheat/interpass: Manufacturer TDS notes that 300โ€“500ยฐF preheat/interpass may yield superior properties.
    • Application: Confirm the job is abrasion-focused rather than a structural joining weld.
    • Safety documentation: Review the SDS before use and confirm shop ventilation, PPE, and fume controls.

    Accessories / Compatible Products

    Because consumable fit depends on your exact MIG gun, feeder, and wire path, do not order tips, liners, nozzles, or drive rolls by wire diameter alone. Match the consumable series to your gun and confirm the .045 in. size before purchase.

    Weld Support Parts Breakdown Reference

    No torch-specific parts breakdown is required to identify this wire because the product is a welding consumable, not a gun or torch assembly. For safety documentation, review the confirmed hardfacing flux-cored SDS before use.

    If you are replacing contact tips, liners, nozzles, diffusers, or drive rolls at the same time, use the parts breakdown for your specific MIG gun or feeder before ordering those items.

    Common Applications

    • Crusher roll repair.
    • Mill hammer hardfacing.
    • Conveyor screw rebuilding.
    • Roller wear-facing.
    • Industrial equipment repair where metal-to-metal abrasion is the primary failure mode.
    • Maintenance welding on older hard-faced deposits when procedure and base metal condition are verified.

    Shipping / Returns Notes

    The Arc Weld Store product page lists free ground shipping to the lower 48 on qualifying orders, shipment from Corydon, Indiana, typical 1โ€“2 business day shipping unless noted, and returns accepted on unused items in original packaging. Confirm current shipping, pickup, and return details on the product page before purchasing.

    FAQ

    Is Washington Alloy THF-700HT-173 a general MIG wire?

    No. It is a hardfacing flux-cored MIG wire intended for abrasion-resistant deposits. Use a general-purpose filler only when the application calls for it.

    What wire size is this spool?

    The Arc Weld Store listing identifies this product as .045 in. wire on a 33 lb spool.

    What polarity does the manufacturer procedure list?

    The Washington Alloy technical data sheet lists DCEP for the typical FCAW welding procedures.

    Can I use my existing MIG gun consumables?

    Compatibility is Unknown (Verify). Confirm your gun series, liner size, contact tip size, drive roll style, and feeder capacity before ordering replacement consumables.

    Does this wire require shielding gas?

    The manufacturer procedure table lists CO2 flow ranges and notes voltage adjustment when using mixed gas. Verify the exact gas recommendation for your procedure, position, machine, and base metal.

    Where should I buy Washington Alloy THF-700HT-173?

    For this product, use Arc Weld Store as the primary ordering source: Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

“>view Washington Alloy THF-700HT-173 at Arc Weld Store.

Safety Notes

Hardfacing flux-cored welding produces fumes, gases, arc radiation, sparks, heat, and electrical hazards. Review the SDS, follow your employerโ€™s welding safety practices, use appropriate welding helmet, gloves, protective clothing, respiratory protection when required, and maintain adequate ventilation. The SDS references ANSI Z49.1 and OSHA Hazard Communication requirements. Always follow the manufacturer instructions and the safety program for your site.

Sources Checked

End CTA: Ready to order the verified .045 in. 33 lb spool? Washington Alloy THF-700HT-173  Hard Face Flux-Cored Mig Wire .045 x 33 Lb. Spool

“>view this product at Arc Weld Store and confirm current stock, shipping, and fitment before checkout.

  • Why does my MIG wire feed keep slipping? (Fast Fix Guide)

    If your MIG wire feed keeps slippingโ€”especially mid-beadโ€”youโ€™ll see an unstable arc, hear the drive rolls โ€œchirp,โ€ and end up with inconsistent penetration. This guide walks you through a fast diagnosis and a clean, one-variable-at-a-time fix so you stop chasing settings.

    Where to Buy (Quick Fix Parts)

    Most โ€œwire slippingโ€ complaints come down to these components:

    • Drive rolls (wrong groove / worn groove):ย rolls spin but canโ€™t grip the wire consistently.
    • Spool hub tension (too tight):ย the feeder canโ€™t pull wire off the spool smoothly, so it surges/slips.
    • Gun liner (dirty, kinked, wrong length):ย too much drag; the rolls slip before the wire moves.

    Top Pick (Primary Fix)

    Unknown (Verify ASIN) โ€” liner choices are highly gun-specific (length + wire size + brand compatibility). To avoid recommending the wrong part, no AAWP box is included.

    Backup / Consumable Option

    Unknown (Verify ASIN) โ€” drive rolls are feeder/model-specific. No AAWP box included.


    Key Takeaways

    • Wire โ€œslippingโ€ is usuallyย dragย (liner/tip) orย mismatchย (drive roll groove/wire size), not voltage/WFS settings.
    • Fix it fastest by checkingย spool brake tensionย andย drive roll grooveย first.
    • If itโ€™s not fixed inย 2โ€“3 minutes, stop adjusting andย replace the liner or contact tipย (most common wear items).
    • Keep one rule:ย one change at a timeย so you donโ€™t create a second problem.

    Symptoms (Fast Diagnosis)

    • Drive rolls spin but wire speedย surgesย orย stalls
    • Arc sounds like itโ€™sย cutting in/out
    • Wire feed feelsย jerkyย when you pull the trigger
    • You hearย clicking/chirpingย from the feeder
    • You get randomย burnbackย or the wire โ€œsticksโ€ at the tip
    • You seeย wire shavingsย near the drive rolls (wire being crushed)

    Root Causes (Mapped to Symptoms)

    • Surging wire speedย โ†’ spool brake too tight, liner drag, or contact tip partially blocked
    • Clicking/chirping at feederย โ†’ drive roll tension wrong, wrong groove for wire size/type, worn rolls
    • Wire shavings/dustย โ†’ too much drive roll pressure, wrong knurl/V-groove selection, misaligned inlet guide
    • Feeds fine with tip removedย โ†’ contact tip worn/blocked, diffuser/nozzle contamination, or tip size mismatch
    • Feeds worse when gun is bentย โ†’ liner kinked, liner too short/too long, cable damage, tight bends in lead

    Quick Fix (Do This First)

    • Stop adjusting voltage/WFS.ย Slipping is mechanical 90% of the time.
    • Set the gun lead straightย (no tight loops) and test again.
    • Back off spool brake tensionย until the spoolย justย stops free-spinning when you release the trigger.
    • Confirm drive roll groove matches the wireย (size and type).
    • Remove the contact tipย and test feed for 2 seconds:
      • If it feeds smoothly now โ†’ tip/diffuser/nozzle area is the restriction.
      • If it still slips โ†’ liner/drive rolls/spool tension is the restriction.

    (AAWP omitted โ€” no verified ASIN.)


    Step-by-Step Fix

    1. Confirm wire size and type
      • Verify the spool label (example: .030 in / 0.8 mm solid ER70S-6, or flux-core).
      • Make sure your drive rolls are correct for that wire (V-groove for solid, knurled for flux-coreโ€”model dependent).
    2. Check drive roll groove selection
      • Many rolls are double-sided. Make sure youโ€™re on the correct groove for your wire diameter.
      • If the groove is polished/worn, it may slip even with correct tension.
    3. Reset drive roll tension (donโ€™t crush the wire)
      • Start low. Increase only until the wire feeds without slipping.
      • Too much tension creates wire shavings and makes liner drag worse.
    4. Set spool hub/brake tension
      • Too tight = feeder struggles to pull wire, causing surging/slip.
      • Too loose = overrun/birdnesting risk when you stop feeding.
    5. Isolate the gun end
      • Remove nozzle and contact tip. Feed wire briefly.
      • If itโ€™s smooth now, replace theย contact tipย first (cheap, fast).
    6. If still slipping: service/replace the liner
      • Blow out the liner (dry air only) and inspect for kinks or rust/dirt.
      • If the liner is worn, kinked, or contaminated, replacement is usually faster than trying to โ€œsave it.โ€
    7. Re-test with the lead in a normal working bend
      • If it only fails under bend, the liner/cable is the culprit.

    Parts That Actually Fix This

    Liner
    Replace when: feed gets worse with bends, you see dust/rust, or it wonโ€™t feed smoothly even with correct roll setup.
    Adjust when: liner is clean and straight, and the issue disappears with the tip removed.

    Contact tips
    Replace when: wire sticks, arc is unstable, tip is ovaled, or feeding improves when the tip is removed.
    Adjust when: tip size is correct and the problem is clearly upstream (rolls/spool/liner).

    Drive rolls
    Replace when: groove is worn/polished, wire slips even at correct tension, or wire is being deformed.
    Adjust when: wrong groove/side is selected or tension is mis-set.

    Diffuser / nozzle (if relevant)
    Replace/clean when: spatter buildup constricts the wire path or the tip seat is damaged.
    Adjust when: itโ€™s simply dirtyโ€”cleaning restores normal feed.


    Replace vs Adjust (Fast Decision Table)

    ProblemAdjust FirstReplace
    Wire slips only at higher WFSSpool brake tension + correct roll grooveDrive rolls (worn groove)
    Feeds smooth with tip removedTip size/condition checkContact tip
    Worse when gun lead is bentStraighten lead + check routingLiner
    Wire shavings at feederReduce roll tension + correct roll typeLiner (if packed with debris)

    Copy table

    Rule: If not fixed in 2โ€“3 minutes โ†’ replace the consumable causing drag (tip or liner).


    Prevention Tips

    • Keep the gun lead as straight as practical; avoid tight coils on the floor.
    • Store wire dry; rust/dirt increases liner drag fast.
    • Donโ€™t overtighten drive rollsโ€”set tension to feed reliably without crushing wire.
    • Replace contact tips proactively when arc stability drops (interval: Unknown; depends on amperage/time-on-arc).
    • Use proper ventilation and fume control; keep spatter under control so the nozzle/tip area doesnโ€™t clog.

    Safety note: Wear ANSI Z87.1-rated eye protection under your hood, welding gloves, and ensure adequate ventilation when welding and when blowing out liners (avoid breathing dust/particulate).


    FAQ

    Why does my MIG wire feed slip only when Iโ€™m welding (not when I free-feed)?
    Heat and load increase drag at the tip/nozzle area. A marginal contact tip or spatter buildup can show up only under arc conditions.

    Should I crank drive roll tension until it stops slipping?
    No. Too much tension deforms wire, creates shavings, and makes liner drag worse. Fix the restriction first.

    How do I know if itโ€™s the liner or the contact tip?
    Remove the contact tip and test feed. If it becomes smooth, the tip/nozzle area is the restriction. If it still slips, look upstream (liner/rolls/spool tension).

    Can the wrong drive roll groove cause slipping?
    Yes. A mismatch between groove and wire size/type is a common cause of inconsistent feed and wire deformation.

  • MIG Wire Feed Bird Nesting: Causes, Fixes & Roller Replacement Guide

    Cluster: MIG Troubleshooting & Wire Feed Systems

    Quick Diagnosis

    You’re feeding wire, but it bunches up inside the gun or linerโ€”a tangled mess that stops the arc cold. This is bird nesting, and it kills productivity fast.

    Most likely causes (in order):

    1. Feed roller tension too tight โ€” squeezes wire, causes backpressure
    1. Dirty or worn feed roller โ€” grooves clogged with spatter, wire slips
    1. Kinked or damaged liner โ€” restricts wire path
    1. Wrong wire size for roller โ€” .023″ wire in a .030″/.035″ groove
    1. Spool cast โ€” wire coiled too tight, won’t feed straight

    Safety Notes

    • Disconnect the gun from the feeder before adjusting rollers or removing wire.
    • Relieve tension on the feed knob before servicingโ€”don’t let it snap back.
    • Always inspect the liner for cracks; damaged liners can cause wire drag and poor contact.

    Step-by-Step Troubleshooting Checklist

    Step 1: Check Feed Roller Tension

    1. Locate the feed knob (usually a thumbscrew or lever on the side of the feeder).
    1. Loosen it slightly โ€” you should be able to stop the wire by pinching it between your fingers without it feeding.
    1. Test: Spin the roller by hand; wire should slip smoothly, not bind.
    1. If still nesting: Move to Step 2.

    Step 2: Clean the Feed Roller

    1. Remove the spool of wire.
    1. Inspect the knurled grooves โ€” look for spatter buildup, rust, or debris.
    1. Clean with a wire brush or cloth; wipe dry.
    1. Check for flat spots or wear โ€” if grooves are smooth/shiny, the roller is worn and needs replacement.
    1. Reinstall and test.

    Step 3: Inspect the Liner

    1. Disconnect the gun from the feeder.
    1. Look inside the liner with a flashlight โ€” check for kinks, cracks, or blockages.
    1. Try to feed wire by hand through the liner without the gun attached; it should slide freely.
    1. If resistance: The liner is damaged and must be replaced.

    Step 4: Verify Wire Size Matches Roller Groove

    1. Check your wire diameter โ€” .023″, .030″, .035″, or .045″.
    1. Check the roller groove โ€” it’s usually marked on the feeder or roller itself (e.g., “K .030/.035”).
    1. If they don’t match: You’re using the wrong roller. Replace it.

    Step 5: Check Spool Cast

    1. Cut 2โ€“3 feet of wire from the spool.
    1. Lay it flat on a table โ€” it should lie nearly flat.
    1. If it coils tightly: The spool has excessive cast. Try a different spool or wire brand.

    Fix Options (Ranked by Cost & Effort)

    Free / Adjustment (Try First)

    • Loosen feed tension โ€” 80% of bird nesting stops here.
    • Clean the roller โ€” removes spatter that causes slipping.
    • Straighten the liner โ€” gently unbend kinked sections.

    Low Cost (~$10โ€“$20)

    • Replace the liner โ€” if kinked or cracked, a new liner solves drag issues.
    • Clean nozzle dip โ€” apply anti-spatter gel to reduce buildup inside the gun.

    Medium Cost (~$15โ€“$30)

    • Replace the feed roller โ€” if worn smooth or grooves are damaged, a new roller restores grip and eliminates slipping.

    Product Recommendation: Drive Roll K.023 K.030 K.035 K.045 Knurled V U Groove Wire Feed for MIG Welders

    Why it helps:

    • Multiple groove options โ€” choose K (knurled), V, or U groove to match your wire size and feeder type.
    • Bearing steel construction โ€” durable, resists spatter buildup better than soft rollers.
    • 15 size variants โ€” covers .023″ through .045″ wire, fits Clarke, SIP, and most hobby/pro MIG welders.
    • Direct replacement โ€” no special tools needed; swap in 2 minutes.
    • Affordable โ€” costs less than a service call.

    What to compare before you buy:

    • Your feeder model โ€” check the manual or feeder nameplate (Clarke, SIP, Lincoln, Hobart, etc.).
    • Wire size you run โ€” .023″, .030″, .035″, or .045″.
    • Groove type โ€” K (knurled for steel), V (V-groove for aluminum), or U (universal).
    • Roller diameter โ€” 1″ or 1.2″ OD (outer diameter); check your feeder.
    • Condition of your current roller โ€” if it’s smooth/shiny, replacement is overdue.

    No products found.

    Common Mistakes

    • Tightening tension to stop nesting โ€” this makes it worse. Loosen instead.
    • Ignoring a kinked liner โ€” you’ll keep having feed problems until you replace it.
    • Using the wrong wire size for your roller โ€” .023″ wire will slip in a .030″ groove every time.
    • Not cleaning the roller โ€” spatter buildup is invisible but deadly for feed consistency.
    • Replacing the roller without checking tension โ€” you’ll bird nest again in a week.

    FAQ

    Q: How do I know if my roller is worn? A: If the grooves look shiny/smooth instead of knurled (bumpy), it’s worn. Worn rollers slip and cause bird nesting even with correct tension.

    Q: Can I use a .030″ roller with .023″ wire? A: No. The wire will slip in the larger groove. Always match wire size to groove size.

    Q: How often should I replace my liner? A: Every 50โ€“100 spools of wire, or sooner if you notice drag or bird nesting. Liners wear out faster than rollers.

    Q: What’s the difference between K, V, and U grooves? A: K (knurled) grips steel wire best; V is for aluminum (softer); U is universal. Check your feeder manual.

    Q: Can I clean a worn roller instead of replacing it? A: Cleaning helps, but if grooves are smooth, replacement is the only fix. Worn rollers can’t grip wire properly.

    Next Steps

    1. Loosen your feed tension and test โ€” this solves most bird nesting.
    1. Clean your roller with a wire brush if it’s clogged with spatter.
    1. If nesting persists: Check your liner for kinks and verify wire size matches your roller groove.
    1. If your roller is worn smooth: Replace it with a bearing-steel roller that matches your wire size and feeder type.
    1. Check our MIG troubleshooting guides for arc length, spatter, and contact tip issues โ€” common companions to feed problems.

  • MIG Welding Wire Selection Guide 2025 | ER70S-6 vs ER70S-3 Specs

    MIG Welding Wire Selection Guide 2025 | ER70S-6 vs ER70S-3 Specs

    MIG wire selection affects weld quality, spatter levels, and penetration depth. Choosing the right wire depends on base metal composition, surface condition, and shielding gasโ€”not just diameter and tensile strength.

    Common MIG Wire Classifications

    ER70S-6 (Most Common)

    • Deoxidizers: Manganese, silicon
    • Tensile strength: 70,000 PSI minimum
    • Best for: Dirty or rusty steel, single-pass welds, general fabrication
    • Shielding gas: 75/25 Ar/COโ‚‚ or 100% COโ‚‚
    • Spatter level: Moderate

    ER70S-3

    • Deoxidizers: Lower manganese and silicon than ER70S-6
    • Tensile strength: 70,000 PSI minimum
    • Best for: Clean steel, multi-pass welds, automotive sheet metal
    • Shielding gas: 75/25 Ar/COโ‚‚ (100% COโ‚‚ not recommended)
    • Spatter level: Low

    ER308L (Stainless Steel)

    • Composition: 19-21% chromium, 9-11% nickel
    • Best for: 304/304L stainless steel
    • Shielding gas: 90/10 Ar/COโ‚‚ or tri-mix (He/Ar/COโ‚‚)
    • Corrosion resistance: Excellent

    ER316L (Stainless Steel)

    • Composition: 18-20% chromium, 11-14% nickel, 2-3% molybdenum
    • Best for: 316/316L stainless, marine environments, chemical processing
    • Shielding gas: 90/10 Ar/COโ‚‚ or tri-mix
    • Corrosion resistance: Superior (molybdenum addition)

    Wire Diameter Selection

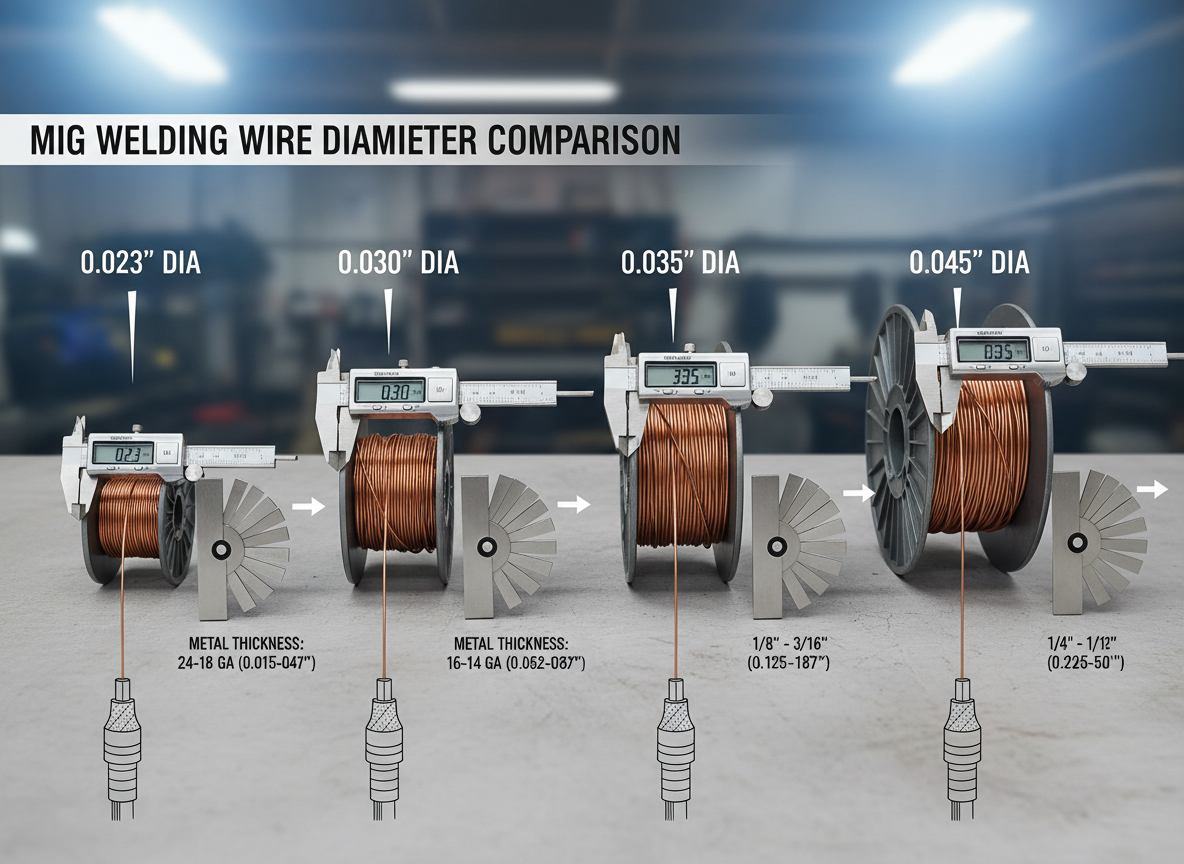
    DiameterAmperage RangeMaterial ThicknessTypical Use
    0.023โ€30-130A24-18 gaugeAutomotive sheet metal, thin tubing
    0.030โ€40-145A18-14 gaugeGeneral fabrication, light structural
    0.035โ€50-180A14 gauge-1/4โ€Most common all-purpose size
    0.045โ€75-250A1/4โ€-1/2โ€Heavy structural, thick plate
    0.052โ€100-300A1/2โ€+Industrial fabrication, heavy equipment

    Rule of thumb: Thinner wire = better control on thin material. Thicker wire = faster deposition on heavy plate.

    Shielding Gas Impact on Wire Performance

    75/25 Argon/COโ‚‚ (C25)

    • Pros: Low spatter, smooth arc, good bead appearance
    • Cons: Higher cost than 100% COโ‚‚
    • Best for: ER70S-3, ER70S-6, stainless steel

    100% COโ‚‚

    • Pros: Deep penetration, low cost
    • Cons: Higher spatter, rougher arc
    • Best for: ER70S-6 on thick steel (not recommended for ER70S-3)

    90/10 Argon/COโ‚‚

    • Pros: Minimal spatter, excellent for stainless
    • Cons: Shallow penetration on carbon steel
    • Best for: ER308L, ER316L stainless wire

    Surface Condition Requirements

    Wire TypeMill ScaleLight RustHeavy RustClean Steel
    ER70S-6โœ“โœ“โœ“โœ“
    ER70S-3โœ—โœ—โœ—โœ“
    ER308Lโœ—โœ—โœ—โœ“
    ER316Lโœ—โœ—โœ—โœ“

    ER70S-6 advantage: Higher deoxidizers clean impurities during welding. ER70S-3 requires clean base metal to avoid porosity.

    AWS Filler Metal Specifications

    AWS A5.18 (Carbon Steel MIG Wire) – Covers ER70S-3, ER70S-6, and other carbon steel wires – Defines chemical composition, tensile strength, and elongation requirements

    AWS A5.9 (Stainless Steel MIG Wire) – Covers ER308L, ER316L, and other stainless wires – Specifies corrosion resistance and ferrite content

    Wire Storage & Handling

    Moisture Contamination – Causes: Porosity, hydrogen cracking – Prevention: Store in sealed containers with desiccant packs – Shelf life: 12 months (carbon steel), 6 months (stainless)

    Wire Feed Issues – Kinked wire = erratic arc and bird-nesting – Solution: Use proper spool tension and liner size

    Liner Compatibility

    Wire DiameterLiner Inside Diameter
    0.023โ€-0.030โ€0.030โ€-0.035โ€
    0.035โ€0.035โ€-0.045โ€
    0.045โ€0.045โ€-0.052โ€
    0.052โ€0.052โ€-0.062โ€

    Oversized liner = wire wander. Undersized liner = excessive friction and burnback.

    Common Mistakes

    Using ER70S-3 on rusty steel
    Low deoxidizers canโ€™t compensate for surface contamination. Result: porosity and weak welds. Use ER70S-6 or clean the base metal.

    Wrong liner size for wire diameter
    0.035โ€ wire in 0.045โ€ liner causes erratic feeding. Match liner to wire diameter within 0.005โ€-0.010โ€.

    Storing stainless wire without moisture protection
    Stainless wire absorbs moisture faster than carbon steel. Always use sealed containers with desiccant.

    Buying Checklist

    • โœ“ Wire classification matches base metal (ER70S-6 for dirty steel, ER70S-3 for clean)
    • โœ“ Diameter suits material thickness and amperage range
    • โœ“ Shielding gas compatible with wire type
    • โœ“ AWS A5.18 or A5.9 certification marked on spool
    • โœ“ Liner size matches wire diameter
    • โœ“ Storage container includes moisture protection
    • โœ“ Spool size fits your machine (2 lb, 10 lb, 33 lb, 44 lb)

  • E70S-6 MIG Welding Wire: A Complete Technical Guide for Welders

    E70S-6 MIG Welding Wire: A Complete Technical Guide for Welders

    Purchase 70S-6 Mig WIre

    When it comes to MIG welding mild steel, E70S-6 welding wire is a go-to filler metal used across industriesโ€”from structural steelwork to automotive fabrication. Itโ€™s known for its excellent arc stability, high deposition rate, and strong mechanical properties.

    Whether you’re a welder, fabricator, or welding engineer, understanding E70S-6 is critical for making informed decisions about joint strength, weld quality, and process efficiency. In this guide, we break down everything you need to know about this essential wire type.


    Types, Classifications, and Variants

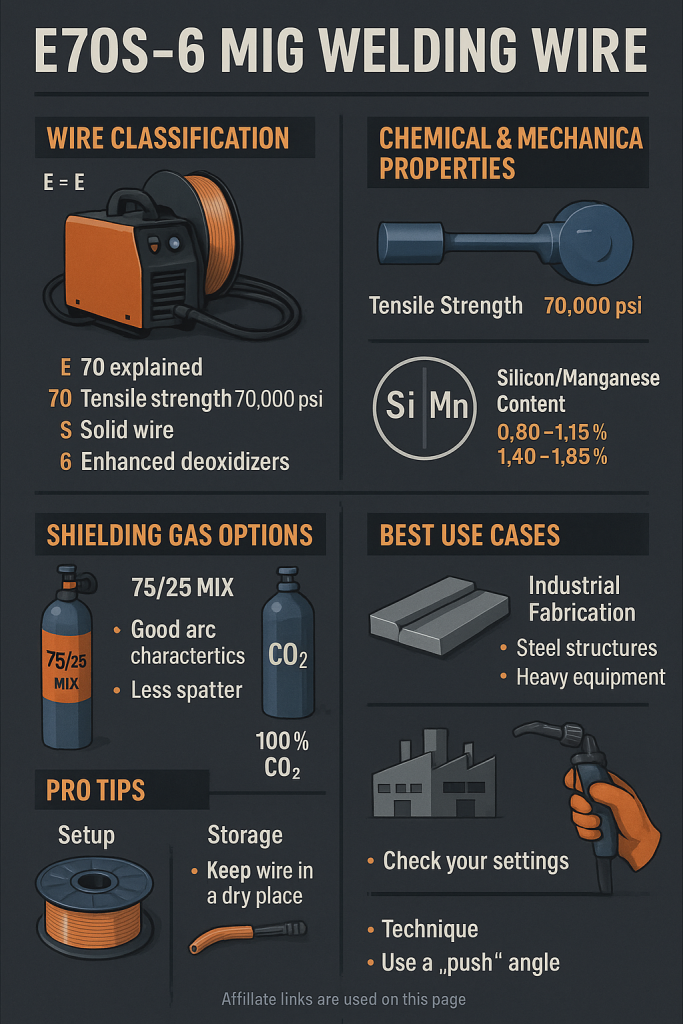
    E70S-6 is part of the AWS A5.18 classification system for solid carbon steel electrodes and rods used in gas metal arc welding (GMAW). Here’s what the designation means:

    • E โ€“ Electrode
    • 70 โ€“ Minimum tensile strength of 70,000 psi
    • S โ€“ Solid wire
    • 6 โ€“ Indicates the wireโ€™s chemical composition and performance characteristics

    Comparison with Other Carbon Steel MIG Wires:

    • E70S-3
      • Lower deoxidizer content
      • Less tolerant of mill scale or rust
      • Cleaner base metals are required
    • E70S-6
      • Higher levels of silicon and manganese
      • Designed for welding over mill scale, light rust, or surface contamination
      • More fluid weld puddle for flatter beads
    • E70C-6M (metal-cored)
      • Similar chemical composition to E70S-6
      • Offers higher deposition rates
      • Requires more expensive equipment and optimized parameters

    Key Characteristics & Properties

    E70S-6 wire stands out for its versatility and weld quality on less-than-perfect base metals. Letโ€™s take a closer look at its technical properties:

    • Tensile Strength: 70,000 psi (minimum)
    • Yield Strength: ~58,000 psi
    • Elongation: ~22% in 2 inches
    • Recommended Shielding Gas:
      • 75/25 Argon/COโ‚‚ for cleaner, more controlled arcs
      • 100% COโ‚‚ for deeper penetration and cost-effectiveness
    • Silicon Content: 0.80โ€“1.15%
    • Manganese Content: 1.40โ€“1.85%
    • Diameter Availability: .023″, .030″, .035″, .045″, and larger for industrial applications

    Real-World Example:
    If you’re welding mild steel tubing for handrails or machinery guards with surface mill scale, E70S-6 will give you a smooth, low-spatter weld bead that requires minimal cleanup.


    Process Considerations

    Compatibility with Welding Processes

    • โœ… GMAW (MIG Welding) โ€“ Primary application
    • โŒ Not suitable for FCAW, GTAW, or SMAW

    Equipment Notes:

    • Compatible with both transformer and inverter-based MIG machines
    • Works well in spray, short-circuit, and globular transfer modes
    • Ideal for semi-automatic or robotic applications

    Pros:

    • High feedability in wire feeders
    • Excellent bead appearance
    • Tolerant to minor surface contaminants

    Cons:

    • Not designed for high-alloy or exotic metals
    • Less effective on dirty or heavily rusted steel than flux-core options
    • Needs shielding gasโ€”canโ€™t be used outdoors without wind protection

    Application Use Cases

    E70S-6 is a workhorse wire used in general fabrication and manufacturing:

    Common Industries:

    • Structural steel erection
    • Heavy equipment repair
    • Shipbuilding
    • Automotive and trailer frame welding
    • Agricultural implement manufacturing

    Compatible Metals:

    • A36 mild steel
    • Hot-rolled steel
    • Low-carbon structural plates and tubing

    Ideal Conditions:

    • When high productivity, flat bead profiles, and minimal post-weld cleanup are important
    • When working with slightly rusty or mill-scaled materials

    Best Practices & Pro Tips

    Hereโ€™s what experienced welders need to keep in mind:

    • Use the Right Gas Mix:
      75/25 Argon/COโ‚‚ delivers cleaner welds; 100% COโ‚‚ increases penetration but increases spatter.
    • Clean Just Enough:
      Though E70S-6 handles light contamination, donโ€™t push itโ€”heavy rust or paint can still cause porosity.
    • Dial in the Voltage and Wire Speed:
      Start with manufacturer specs and fine-tune based on sound and bead shape. A smooth “buzz” sound = optimal settings.
    • Avoid Excess Heat Input:
      Especially when welding thinner material. Use pulsed MIG or short-circuit transfer to avoid burn-through.
    • Watch for Silicon Islands:
      After welding, shiny silicon deposits may form in the weld toe area. These should be ground off before painting or coating.
    • Store Wire Properly:
      E70S-6 is prone to rust if stored in humid conditions. Keep it in sealed containers or use wire feeders with covers.

    Conclusion

    E70S-6 MIG welding wire is the top choice for fabricators and welders dealing with carbon steels that aren’t in pristine condition. Its chemical makeup allows for smooth arcs, flat welds, and strong joints even when base metals have minor mill scale or rust.

    If youโ€™re looking to balance performance, affordability, and ease of use, this wire is probably the right fit for most carbon steel welding jobs.

    Purchase E70S-6 Mig Wire


    Note: Some links on this page may be affiliate links. If you click and purchase, we may earn a commission at no extra cost to you. We only recommend products we use and trust.

  • TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1): Application and Buying Checks

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1): Application and Buying Checks

    “>TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1) is a solid MIG wire intended for gas metal arc welding on mild and low-alloy steel. For buyers and maintenance teams, the main question is not only whether the wire will weld, but whether it matches the joint condition, wire feeder setup, and procedure requirements in your shop. This guide focuses on application checks, fitment checks, and practical verification steps before you commit to a spool.

    Key Takeaways

    What this wire is for

    Based on the available product information, this is a .030 in (0.8 mm) solid MIG wire in the ER70S-2 family, supplied on a 33 lb spool. That makes it a common size for general fabrication, repair work, and light-to-medium production welding on carbon steel. The added deoxidizers associated with ER70S-2 chemistry can help in situations with light mill scale or minor surface contamination, but they do not replace cleaning, fit-up control, or procedure compliance. Best results still come from clean base metal.

    Use this wire as a candidate when you need a general-purpose carbon steel MIG wire and your equipment is configured for .030 in solid wire. If your job is governed by a written WPS, the WPS controls. If the wire is being selected for maintenance repair without a formal WPS, verify the joint type, shielding gas, deposition target, and feeder setup before purchase or installation. Unknown (Verify) for any application outside mild and low-alloy steel service.

    Buying checks before you order or load the spool

    Check wire diameter. Confirm the feeder, gun, and contact tip are set up for .030 in wire. A mismatch can cause erratic feeding, burnback, or inconsistent arc starting.

    Inspect spool compatibility. Confirm that your feeder accepts the spool format and weight. The product listing indicates a 33 lb spool, but always verify your machineโ€™s maximum spool size and hub capacity. Unknown (Verify) if your feeder has a narrow spool compartment or light-duty hub.

    Verify shielding gas. ER70S-2 solid wire normally runs with shielding gas, but the exact mix depends on your procedure and base metal. Do not assume a gas type from the wire class alone. Check the WPS or internal process sheet.

    Check drive-roll and liner setup. Solid wire generally feeds best with the correct groove profile, proper tension, and a clean liner. If the feeder was last used with flux-cored wire, inspect drive-roll selection and liner wear before loading this spool.

    Inspect contact tip wear. A worn tip can look like a wire problem. Replace tips that are ovaled, burned, or loose.

    Application and process checks

    Check base metal condition. ER70S-2 can be more forgiving than basic wire on slightly imperfect surfaces, but do not use that as a substitute for cleaning. Remove oil, rust, heavy mill scale, paint, moisture, and weld residue wherever practical.

    Verify joint access and polarity. Confirm the gun can maintain a stable arc length and that the machine polarity matches the process setup required by your WPS or equipment instructions. If you do not have that documentation, verify it before starting production.

    Inspect fit-up. Poor gap control can hide under a good-looking bead. Check root opening, alignment, and tack quality before blaming the wire.

    Confirm feed consistency. Test feed the wire through the gun cable with the machine cold. Look for drag, birdnesting, or intermittent push. If the wire does not feed smoothly on setup, fix the feeder first.

    Verify arc behavior on coupon. Run a short test on scrap from the same material family. Inspect bead shape, spatter level, wetting, and tie-in. If results are inconsistent, compare gas flow, tip condition, liner wear, and feed speed before changing wire class.

    Troubleshooting support: check, inspect, verify

    If the arc is unstable: check gas flow, inspect for leaks or loose fittings, and verify tip-to-work distance and stickout against your procedure.

    If feeding is rough: check drive-roll tension, inspect the liner for wear or contamination, and verify the correct tip size for .030 in wire.

    If spatter is excessive: check voltage and wire feed settings, inspect ground connection quality, and verify the shielding gas setup before changing product.

    If weld appearance is inconsistent: inspect base metal cleanliness, verify travel speed, and check joint fit-up. Do not assume the spool is at fault until the machine and preparation are reviewed.

    WSP lookup and filler metal finder

    For procedure-controlled work, use the Weld Support Parts lookup tools as starting points, then verify against the approved WPS or engineering release. These pages help with selection and comparison, but they are not a substitute for procedure approval.

    If your job requires documented filler approval, use those pages to narrow the candidate list, then confirm the final selection against your internal welding documentation. Treat the result as a starting point, not a guaranteed procedure match.

    Safety notes

    Handle wire spools carefully. Edges can be sharp, and loose wire ends can whip back during loading. Wear gloves when opening packaging, setting a spool, or trimming wire. Keep the feeder powered down during installation. Verify ventilation and fume control before welding. Follow your siteโ€™s hot-work controls, especially on painted or contaminated material.

    FAQ

    Is this wire only for mild steel?
    The provided product information supports use on mild and low-alloy steel. Unknown (Verify) for other base metals or special applications.

    Can I use it on lightly scaled material?
    ER70S-2 chemistry may help tolerate light mill scale or minor contamination, but that is not a license to skip cleaning. Inspect the surface and clean it as much as the job allows.

    Do I need a specific gas or procedure?
    Verify your shielding gas and procedure from the WPS or internal welding instructions. Do not select gas solely from the wire class.

    How do I know if the spool will fit my feeder?
    Check the feederโ€™s spool diameter, hub design, and maximum weight rating. If the machine documentation is unavailable, measure and verify before purchase or install.

    Sources Checked

    Final verification should always come from the active WPS, machine manual, and shop qualification records.

    Related Arc Weld Part

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 04 is an ER70S-2 solid MIG (GMAW) wire for welding mild and low-alloy steels where consistent feeding and sound weld quality matter; ER70S-2 chemistry includes added deoxidizers that can help tolerate light mill scale and minor surface contamination versus standard ER70S-6 (best results still come from clean base metal). This item is one (1) spool of .030 in (0.8 mm) wire, 33 lb (0.91 kg)…

    View at Arc Weld Store

    Related Weld Support Guides

  • TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1) is an ER70S-2 solid GMAW wire for mild and low-alloy steel work where stable feeding and weld soundness matter. For buyers and support teams, the main value is straightforward: this is a general-purpose solid wire with deoxidizers, supplied as one 11 lb spool in .035 in (0.9 mm). Use it only after you verify the job requirements, base metal condition, shielding gas, and equipment setup.

    Key Takeaways

    What this wire is for

    This product is intended for GMAW on steels where a dependable general-purpose wire is needed. ER70S-2 is commonly selected for shop fabrication, maintenance repair, and production work on carbon steel or low-alloy steel. The exact application still depends on joint design, shielding gas, base metal condition, and the procedure being used. If your job calls for aluminum, stainless, flux-cored, or hardfacing wire, this is not the correct filler metal.

    Product and parts review

    The available product information identifies this item as one spool of Washington Alloy TC 70S-2 08 in .035 in diameter, 11 lb, pack of one. Beyond that, confirm the following before it is placed into service:

    If you are stocking wire for a maintenance crib, record the spool size, wire diameter, and machine compatibility on the shelf label. Do not assume every .035 solid wire fits every feeder without changes to drive rolls, liners, and contact tips.

    Setup checks: inspect before feeding

    Troubleshooting and support

    When a MIG wire does not run correctly, start with the feeder and the work setup before blaming the wire itself.

    If the wire bird-nests or feeds inconsistently

    If the arc is unstable or spatter is high

    If porosity appears in the weld

    How to use filler metal pages as a starting point

    When you are selecting wire for a job, use approved filler metal references as a starting point, not as automatic procedure approval. The available internal reference pages on the Weld Support Parts blog can help you compare product categories and related wire types. If a job is outside your normal range, confirm the final selection against the WPS, the machine manual, or a qualified welding authority. Do not rely on product pages alone for code or critical work.

    Related internal reference articles:

    Buyer guidance for maintenance teams

    For maintenance and fabrication buyers, the main checks are not marketing claims. They are feedability, repeatability, and fit with the shop process. Before ordering, verify the following:

    If a team routinely changes between wire sizes or wire classes, label the cabinet and gun setup clearly. That reduces downtime and avoids wrong-wire installation.

    Safety notes

    FAQ

    Is TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1) the same as ER70S-2?

    The product description identifies it as ER70S-2 solid MIG wire. Verify the label on the spool and the supplier listing before use.

    Can this wire be used on dirty or rusty steel?

    ER70S-2 includes deoxidizers, but that does not replace cleaning. Best practice is still to remove rust, oil, paint, and scale as required by the job.

    What shielding gas should be used?

    Unknown (Verify). Gas choice depends on the approved procedure, base metal, transfer mode, and weld requirements. Check the WPS or machine documentation.

    Will .035 in wire work in every MIG machine?

    No. Machine feedability depends on the feeder, liner, drive rolls, gun, and tip size. Verify compatibility before loading the spool.

    Sources Checked

    Related Arc Weld Part

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 08 Washington Alloy is an ER70S-2 solid MIG (GMAW) wire for welding mild and low-alloy steels where consistent feeding and sound weld quality matter; ER70S-2 chemistry includes added deoxidizers and is commonly selected for general fabrication and repair work (best results come from properly prepared base metal). This item is one (1) spool of .035 in (0.9 mm) wire, 11 lb, packaged as a pack of (1). Set up…

    View at Arc Weld Store

    Related Weld Support Guides

  • TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 093 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 33 lb (15 kg) spool. For buyers and support teams, the main question is not whether the wire can weld mild steelโ€”it canโ€”but whether it matches the jobโ€™s fit-up, base-metal condition, and feeder setup. This article breaks down where this wire fits, what to verify before use, and how to troubleshoot common feeding and weld-quality issues without guessing at specifications that are not documented here.

    Key Takeaways

    What This Wire Is For

    As listed, TC 70S-2 093 is aimed at mild-steel work in fabrication, maintenance, and repair. That makes it relevant for shops that need a practical solid wire for general production work and field repair where clean surface prep is not always perfect. The ER70S-2 classification is commonly used when a shop wants a wire that tolerates light oxidation better than a basic clean-steel setup.

    Do not assume this wire is the right answer for every joint. A MIG wire selection still depends on base metal chemistry, joint design, shielding gas, transfer mode, and the required mechanical properties of the finished weld. If any of those points are unclear, treat this product as a candidate, not a final approval.

    Inspect Before You Load the Spool

    Before installing the spool, do a basic receiving check.

    If the shop has recurring feed issues, the wire is not the first thing to blame. Check the feeder path, tension, liner condition, and tip wear before changing consumables again.

    Troubleshooting Support: What to Check First

    Problem: Erratic feeding or birdnesting

    Problem: Excess spatter or unstable arc

    Problem: Porosity in the weld bead

    Selection Support: Where to Confirm the Filler Metal

    If your team needs a starting point for filler selection or cross-checking wire classifications, use the WSP resources as reference tools rather than automatic approvals. When available, the filler metal finder should be treated as a selection starting point, not a guarantee that a procedure is approved for your job, code, or base metal combination.

    Use those pages to narrow down options, then verify the actual WPS, shielding gas, and wire classification before production use.

    Product and Parts Notes

    This listing is for one spool of Washington Alloy TC 70S-2 093. The documented size is .035 in and the documented spool weight is 33 lb. Beyond that, do not assume details such as drive-roll type, recommended gas mix, or exact machine compatibility unless your internal procedure sheet or manufacturer documentation confirms them. For uncertain technical details, mark them as Unknown (Verify).

    For buyers, the important points are simple: confirm the classification, confirm the diameter, confirm the spool weight, and confirm that the feeder setup matches the wire path requirements of your machine. If the wire is being purchased for a repair bay, make sure the operators know whether the work is light fabrication, maintenance welding, or a qualified procedure with tighter limits.

    Practical Use Notes

    Triple-deoxidized ER70S-2 wires are often chosen when the surface is not ideal, but that does not eliminate prep. Remove loose scale, paint, oil, moisture, and heavy corrosion whenever possible. The more contaminated the joint, the less likely any MIG wire will produce reliable results. The right response is better cleaning, not overreliance on filler metal chemistry.

    For shop support teams, the right workflow is: identify the base metal, confirm the required process, match the filler classification, and verify the feeder hardware. This wire may be a good general-purpose option, but the procedure still controls the final weld.

    Safety Notes

    FAQ

    Is TC 70S-2 093 suitable for mild steel?
    Yes, the listed application is mild-steel fabrication, maintenance, and repair. Final suitability still depends on the WPS and job requirements.

    Can I use this wire on material with light mill scale?
    The product description says the triple-deoxidized ER70S-2 chemistry is suited for light mill scale or minor surface contamination. That is helpful, but it is not a substitute for proper cleaning.

    Does .035 in wire work in every MIG machine?
    No. Wire diameter compatibility depends on the feeder, drive rolls, liner, contact tip, and procedure. Verify the setup before loading the spool.

    Is the shielding gas confirmed in the product listing?
    Unknown (Verify). The available product information does not document a specific gas requirement.

    Sources Checked

    This draft uses only the provided product information and internal links. Any details not explicitly documented should be treated as Unknown (Verify).

    Related Arc Weld Part

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 093 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 33 lb (15 kg) spool for mild-steel fabrication, maintenance, and repair, delivering stable arc characteristics and consistent feeding; its triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) is well-suited for producing clean welds when the base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1)…

    View at Arc Weld Store

    Related Weld Support Guides

  • More posts

    Try Amazon Prime Free