Search results for: “arc instability”

  • TIG Tungsten Splitting Causes: Cracked Electrodes, Spitting, Balling, and Arc Instability

    If TIG tungsten is splitting, cracking lengthwise, spitting small particles into the weld, balling excessively, or breaking down after only a few starts, stop and check heat load, shielding, polarity, tungsten type, and grind direction before blaming the torch. A split tungsten usually means the electrode is being overheated, contaminated, oxidized while hot, ground incorrectly, used on the wrong polarity, or run outside the amperage range for its diameter.

    The fast fix is to cut or break off the damaged end, regrind lengthwise on a clean dedicated wheel, verify 100% argon flow, check post-flow, confirm DCEN for steel/stainless, confirm AC settings for aluminum, and make sure the tungsten diameter and type match the amperage. Do not keep welding with a split electrode. Split tungsten can cause arc wander, hard starts, black specks, tungsten inclusions, porosity, and repeated rework. For related TIG issues, see unstable TIG arc from poor tungsten prep, TIG tungsten turning black, and TIG shielding gas coverage troubleshooting.

    Common Symptoms

    • Tungsten splits lengthwise after arc starts.
    • Tip cracks, flakes, or sheds particles into the puddle.
    • Arc wanders or splits into multiple weak arc points.
    • Tungsten balls excessively on AC aluminum.
    • Tungsten turns black, blue, gray, or chalky after welding.
    • Tip breaks down quickly at amperage that used to work.
    • Black specks appear in the TIG weld puddle.
    • Starts become hard, inconsistent, or noisy.
    • Electrode cracks after touching filler rod or the weld puddle.

    Likely Causes

    CauseWhat It DoesQuick Check
    Amperage too high for diameterOverheats the tungsten and causes cracking, balling, or erosionCompare amps to tungsten diameter range
    Wrong polarityOverloads the electrode, especially on DCEPUse DCEN for most steel/stainless TIG
    Too much AC cleaning/EPPuts extra heat into the tungstenReduce EP/cleaning action if tungsten overheats
    Wrong tungsten typeElectrode may split or erode in the applicationVerify tungsten type for AC or DC process
    Grinding across the electrodeCreates stress risers and arc wanderGrind lengthwise only
    Contaminated grind wheelEmbeds steel, aluminum, or abrasive contaminationUse dedicated tungsten grinder/wheel
    Poor shielding or short post-flowOxidizes hot tungsten and weakens the tipCheck argon, cup, gas lens, leaks, drafts, and post-flow
    Dipping tungstenContaminates and shocks the electrodeRegrind after any puddle or filler contact

    Fast Diagnosis Sequence

    1. Stop welding as soon as the tungsten splits or starts spitting.
    2. Cut back to clean tungsten. Do not just sharpen over a crack.
    3. Confirm the machine is set to DCEN for carbon steel and stainless steel TIG.
    4. For aluminum, confirm AC mode and reduce excessive EP cleaning if the tungsten overheats.
    5. Verify tungsten diameter against actual amperage, not just material thickness.
    6. Confirm tungsten type: lanthanated, ceriated, pure, zirconated, thoriated, or rare earth.
    7. Check argon flow at the torch and inspect for leaks, drafts, cracked cups, and plugged gas lens screens.
    8. Increase post-flow if the tungsten turns dark after the arc stops.
    9. Regrind lengthwise on a clean dedicated wheel or tungsten grinder.
    10. Run a short test bead and inspect the tungsten before continuing production.

    Inspection Steps

    • Tungsten end: Look for lengthwise cracks, side cracks, melted balling, black oxide, gray frosting, or missing chunks.
    • Grind marks: Marks should run lengthwise toward the tip, not around the circumference.
    • Diameter: A small electrode used at high amperage will overheat and split faster.
    • Collet and collet body: Loose, overheated, or worn parts can cause poor electrical contact and heat concentration.
    • Cup or gas lens: Check for cracks, plugged screens, wrong cup size, excessive stickout, or gas turbulence.
    • Shielding gas: Verify 100% argon for normal TIG work unless the procedure calls for another approved mix.
    • Post-flow: Tungsten must stay shielded while it cools after the arc stops.
    • Work lead: Poor work connection can make starts unstable and encourage repeated tungsten contamination.

    Test Procedures

    • Amperage reduction test: Drop amperage or move to a larger tungsten. If splitting stops, the original electrode was overloaded.
    • Polarity test: Confirm DCEN on steel or stainless. DCEP puts heavy heat into the tungsten and can destroy the tip quickly.
    • Post-flow test: Hold the torch still after arc stop. If tungsten no longer turns black or cracks, hot oxidation was part of the failure.
    • Gas coverage test: Block drafts, reduce excessive stickout, inspect the cup/gas lens, and retest. Poor shielding can oxidize and embrittle the tip.
    • Grind direction test: Regrind lengthwise on a clean wheel. If arc stability improves and splitting drops, prep was contributing.
    • Contamination test: Replace tungsten after a dip. If the next electrode holds up, the previous one was contaminated rather than defective.

    Root Cause Analysis

    Tungsten splitting is usually a heat-and-stress failure. The electrode carries current, holds a point, and sits in a hot arc zone while surrounded by shielding gas. If the tungsten is too small, the polarity puts too much heat into the electrode, the AC balance is too aggressive, or gas coverage fails while the tungsten is still hot, the tip can oxidize, weaken, crack, or shed particles into the weld.

    Grinding can also start the failure. Circumferential grinding marks act like grooves around the electrode. The arc can wander around those marks, and heat can concentrate along weak lines. A contaminated wheel can embed foreign metal into the tungsten. Once that contaminated area is heated by the arc, the tip can split, spit, or melt unevenly.

    Compatibility Notes

    Do not choose TIG tungsten by color alone. Verify the AWS/ISO classification, diameter, current type, polarity, machine waveform, base metal, amperage, torch size, cup size, and shielding gas. Many shops use 1.5% or 2% lanthanated tungsten for broad AC/DC work, but the correct choice still depends on the procedure and machine. Pure tungsten is older AC aluminum practice. Zirconated tungsten is commonly used where AC resistance to contamination is desired. Thoriated tungsten is common on DC steel/stainless but requires dust control and safety handling during grinding.

    For high-amperage DC work, using a larger tungsten can reduce overheating and contamination risk. For AC aluminum, too much cleaning action or the wrong tungsten can cause balling and splitting. For micro-TIG or low-amperage starts, a smaller tungsten may be needed, but it must not be pushed into a higher amperage range.

    What To Verify Before Ordering

    • Tungsten diameter and length.
    • Tungsten classification, not just color code.
    • Base metal: steel, stainless, aluminum, magnesium, nickel, titanium, or other.
    • Current type: AC, DCEN, or special waveform.
    • Amperage range and duty cycle.
    • Torch size, collet size, collet body, gas lens, cup size, and back cap.
    • Shielding gas type and flow range.
    • Grinding method and dust extraction requirements.
    • Whether the procedure restricts thoriated tungsten or radioactive materials.

    Common Wrong-Part Mistakes

    • Using too small of a tungsten because it starts easily at low amperage.
    • Using thoriated tungsten on high-heat AC aluminum without checking the machine and tungsten manufacturer guidance.
    • Buying by color code only when color markings vary by standard or supplier.
    • Using a collet that does not match tungsten diameter.
    • Using a cracked cup or plugged gas lens and blaming the electrode.
    • Grinding tungsten on the same wheel used for steel or aluminum.
    • Reusing dipped tungsten without cutting back past contamination.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Tungsten split after one startCut back and regrindVerify polarity, amperage, shielding, and tungsten type
    Tip balls too much on ACReduce heat input and regrindAdjust AC balance, use correct tungsten, and confirm diameter
    Tungsten turns blackIncrease post-flow and hold torch stillFix gas leaks, drafts, cup/gas lens problems, and post-flow settings
    Black specks in weldStop and replace/regrind tungstenPrevent dipping, spitting, and cracked tungsten contamination
    Arc wanders after grindingRegrind lengthwiseUse dedicated grinder, correct angle, and clean tungsten storage

    Related Failure Paths

    • Unstable TIG arc: Split or contaminated tungsten gives the arc multiple attachment points.
    • Black tungsten: Usually tied to shielding loss, short post-flow, drafts, or moving the torch out of gas coverage while hot.
    • Tungsten inclusions: Cracked or dipped tungsten can break off into the weld puddle.
    • Porosity: Poor shielding that oxidizes tungsten can also contaminate the weld pool.
    • Hard starts: Wrong grind, contamination, poor work clamp, or wrong tungsten size can make starts inconsistent.

    Safety Notes

    • Wear eye protection when grinding or snapping tungsten.
    • Use dust extraction or a controlled tungsten grinder, especially with thoriated tungsten.
    • Do not breathe grinding dust from tungsten or contaminated electrodes.
    • Keep thoriated tungsten grinding dust away from shared bench grinders and general shop surfaces.
    • Turn off output before changing tungsten, collets, cups, or torch parts.
    • Handle hot tungsten and cups with pliers or gloves.
    • Follow the electrode SDS and shop respiratory protection requirements.

    Sources Checked

    Sources checked include tungsten electrode current range references, TIG torch accessory catalog data, shielding gas troubleshooting references, and related Weld Support Parts TIG troubleshooting articles. Final tungsten selection must be verified by exact welding process, material, polarity, amperage, torch consumables, shielding gas, machine waveform, and safety requirements.
  • MIG Nozzle Spatter Buildup Troubleshooting: Poor Gas Coverage, Porosity, Burnback, and Arc Instability

    MIG nozzle spatter buildup is not just a cleaning issue. When spatter packs inside the nozzle, bridges toward the contact tip, or blocks the diffuser ports, shielding gas flow becomes restricted or turbulent. The weld can then show porosity, black soot, erratic arc starts, excess spatter, contact tip overheating, and repeated burnback even when the gas cylinder and regulator look normal.

    The fast fix is to shut the machine off, let the gun cool, remove the nozzle, clean or replace the nozzle, inspect the diffuser holes, and replace the contact tip if it is worn, arc-marked, or spatter-packed. Do not compensate for a blocked nozzle by raising gas flow first. High gas flow can also create turbulence. Clean the front end, verify nozzle bore and tip recess, then test weld on clean material. For related front-end failures, see MIG diffuser clogging symptoms, MIG porosity troubleshooting, and MIG wire burnback into the contact tip.

    Common Symptoms

    • Pinholes, wormholes, or scattered porosity appear after several welds.
    • Nozzle bore is packed with BB-like spatter or slag-colored deposits.
    • Gas sounds normal at the regulator, but the weld acts unshielded.
    • Arc starts rough, pops, or wanders before stabilizing.
    • Spatter increases even though settings have not changed.
    • Contact tip turns blue, burns back, or fuses wire more often.
    • Nozzle sticks to the work or fills faster in corners and short stickout work.
    • Weld bead has black soot or an oxidized surface around the toes.

    Likely Causes

    CauseWhat It DoesQuick Check
    Spatter-packed nozzleRestricts or redirects shielding gasRemove nozzle and inspect bore with light
    Blocked diffuser portsCreates uneven gas flow around the tipLook for plugged side holes behind the nozzle
    Nozzle too small for applicationFills quickly and limits gas envelopeCompare bore size to wire size, amperage, and joint access
    Tip recess or stickout wrongChanges gas coverage and arc behaviorVerify contact tip position for the gun/nozzle style
    Voltage/WFS imbalanceCreates excessive spatter at the arcAdjust one variable at a time after cleaning front end
    Too short stickoutRuns nozzle too close and overheats the front endHold a consistent contact-tip-to-work distance
    Too much anti-spatter or nozzle dipCan contaminate gas path or collect debrisUse a light coating only on approved areas
    Damaged nozzle insulationCan cause arcing to the nozzleReplace nozzles with cracked or burned insulation

    Inspection Steps

    1. Turn off the welder and let the gun front end cool.
    2. Remove the nozzle. Do not twist against a hot, seized nozzle with bare hands.
    3. Look inside the nozzle bore. Replace it if spatter is fused, the bore is distorted, or the insulation is damaged.
    4. Inspect the contact tip. Replace it if the bore is oval, rough, arc-marked, or partially plugged.
    5. Inspect the diffuser. Gas holes must be open and threads must hold the tip square.
    6. Check whether spatter is bridging between the nozzle, tip, and diffuser.
    7. Confirm the nozzle bore and contact tip recess match the gun setup and weld access needs.
    8. Reassemble with clean parts, then test on clean scrap before changing machine settings.

    A nozzle that repeatedly packs with spatter may be a symptom of another problem. After the nozzle is clean, check work clamp contact, wire feed consistency, polarity, stickout, travel angle, voltage, wire-feed speed, shielding gas type, and base-metal cleanliness. If the wire feed is slipping or surging, use MIG wire feed slipping troubleshooting before blaming the nozzle alone.

    Test Procedures

    • Clean-front-end test: Clean or replace the nozzle, tip, and diffuser, then run the same weld settings. If porosity and spatter drop immediately, the nozzle/diffuser area was the active failure.
    • Gas-flow path test: With the nozzle removed, inspect for blocked diffuser holes. Gas must flow evenly around the contact tip, not from one restricted side.
    • Nozzle comparison test: Install a clean correct-size nozzle. If the problem disappears, the previous nozzle was either blocked, damaged, undersized, or wrong for the job.
    • Stickout test: Run a short bead while keeping a consistent contact-tip-to-work distance. If buildup returns quickly when the nozzle is too close, operator distance is contributing.
    • Settings test: After front-end parts are clean, adjust voltage and wire-feed speed one variable at a time. Excessive spatter from poor settings will refill the nozzle fast.

    Visual Wear Indicators

    • Spatter ring inside the nozzle bore.
    • Spatter bridge touching the contact tip or diffuser.
    • One side of the nozzle packed more heavily than the other.
    • Burned, cracked, loose, or missing nozzle insulation.
    • Nozzle bore out-of-round from pliers, impact, or overheating.
    • Contact tip blue, mushroomed, ovaled, or loose in the diffuser.
    • Diffuser ports plugged with spatter or wire shavings.

    Root Cause Analysis

    The nozzle’s job is to direct shielding gas around the wire and weld pool. When spatter narrows the bore, the gas stream can lose coverage or become turbulent. That exposes the molten weld pool to air and can create porosity even when the flowmeter still shows gas. A dirty nozzle can also trap heat around the contact tip, which increases burnback and can make the wire stick inside the tip.

    Spatter buildup also feeds itself. A rough arc creates spatter, the spatter blocks gas, poor gas coverage makes the arc and weld puddle less stable, and the unstable arc throws more spatter into the nozzle. Break that loop by cleaning the front end first, then correcting the cause of excessive spatter.

    Compatibility Notes

    Do not order MIG nozzles by bore size alone. Verify gun brand, gun series, nozzle connection style, slip-on or threaded design, contact tip position, diffuser style, amperage range, wire size, shielding gas, and joint access. A bottleneck nozzle may help reach a tight joint, but a smaller bore can pack faster and may reduce gas coverage if used outside its intended range.

    Also verify whether the job needs flush, recessed, or protruding contact tip position. Wrong tip recess can change stickout, arc stability, gas coverage, and spatter collection. If the nozzle, diffuser, and contact tip are from mixed consumable systems, replace them as a matched front-end set for the installed gun.

    What To Verify Before Ordering

    • MIG gun manufacturer and exact gun series.
    • Nozzle style: slip-on, threaded, heavy-duty, tapered, bottleneck, or flush style.
    • Nozzle bore diameter and required joint access.
    • Contact tip position: flush, recessed, or extended.
    • Diffuser or retaining head style used by the gun.
    • Wire diameter, wire type, amperage range, and duty cycle.
    • Shielding gas and expected gas flow range.
    • Whether the nozzle insulation is separate or built into the nozzle.
    • Paint, galvanizing, or coating requirements if anti-spatter is used on workpieces.

    Common Wrong-Part Mistakes

    • Using a small bottleneck nozzle for high-spatter welding because it improves visibility.
    • Replacing only the nozzle while leaving a plugged diffuser in place.
    • Mixing nozzles, tips, and diffusers from different consumable systems.
    • Using too much nozzle dip and contaminating the gas path.
    • Spraying anti-spatter into the contact tip bore or threaded electrical contact area.
    • Ignoring nozzle insulation damage that allows arcing between the nozzle and work.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Light spatter in nozzleClean with MIG pliersAdd routine cleaning interval and correct settings
    Spatter fused inside boreInstall spare nozzleReplace nozzle and inspect diffuser/tip for heat damage
    Porosity after several weldsClean nozzle and check gasVerify gas path, diffuser, nozzle size, drafts, and base-metal prep
    Repeated burnbackReplace contact tipCorrect feed drag, stickout, diffuser blockage, and tip size
    Nozzle packs fast in cornersClean more oftenReview joint access, gun angle, nozzle bore, and anti-spatter method

    Anti-Spatter Use

    Anti-spatter spray or nozzle gel can slow buildup, but it should not be used to hide bad settings, poor wire feed, or a blocked diffuser. Apply only a light amount and follow the product directions. Keep product out of the contact tip bore, electrical thread contact areas, and gas passages unless the manufacturer specifically allows that use. For paint-sensitive work, verify silicone-free or paint-compatible chemistry before spraying workpieces.

    Ignored-Failure Consequences

    • Porosity and rejected welds from poor shielding gas coverage.
    • Burnback and downtime from overheated contact tips.
    • More spatter from unstable arc starts and poor gas flow.
    • Damaged diffuser threads or seized front-end consumables.
    • Premature gun neck heating and shorter consumable life.
    • False troubleshooting of regulators, gas cylinders, or machine output when the nozzle is the real restriction.

    Safety Notes

    • Turn off the welder before removing nozzles, tips, or diffusers.
    • Hot nozzles can burn gloves and skin; allow cooling time before service.
    • Wear eye protection when chipping, brushing, or clipping wire.
    • Do not use flammable cleaners near the arc or on hot parts.
    • Use ventilation or local exhaust during welding and testing.
    • Read anti-spatter and cleaner safety data sheets before use.

    Sources Checked

    Sources checked include OEM MIG troubleshooting guidance, welding safety references, uploaded anti-spatter and accessory catalogs, and related Weld Support Parts troubleshooting articles. Nozzle replacement must still be verified by gun series, nozzle connection, diffuser style, contact tip position, wire size, amperage, shielding gas, and application access.

  • 7018 Rod Moisture Contamination Troubleshooting: Porosity, Rod Sticking, Arc Instability, and Hydrogen Cracking Risk

    7018 rod moisture contamination is a low-hydrogen failure, not just a storage inconvenience. Damp E7018 electrodes can cause porosity, rough arc starts, excessive spatter, slag trouble, underbead cracking risk, and welds that fail inspection even when the bead looks acceptable. If 7018 rods have been left open in humidity, stored in a toolbox, rained on, or mixed with high-moisture rods, treat them as suspect before welding structural, code, pressure, lifting, or restrained joints.

    The fast field decision is simple: use fresh rods from a sealed container for critical work, keep opened low-hydrogen rods in a rod oven, and do not assume a warm shop shelf or sealed plastic tube restores low-hydrogen condition. If rods are wet, oily, rusty, chipped, or unknown, discard them for critical work. Reconditioning must follow electrode manufacturer and code requirements, not a torch, microwave, job box, truck dash, or improvised heater.

    Related stick welding checks include 7018 rod sticking causes, 6010 vs 7018 storage differences, rod oven storage support, and 7018 electrode support.

    Common Symptoms

    SymptomLikely Moisture LinkFirst Check
    Porosity or pinholesHydrogen/moisture in coating or contaminated jointUse fresh oven-held rods and clean base metal
    Rod sticks on startsDamp coating, low amperage, poor restart prepTry known-dry rod at correct amperage
    Rough unstable arcMoisture-altered coatingCompare sealed rods against suspect rods
    Excess spatterDamp coating or wrong arc length/amperageCheck rod storage and machine settings
    Slag acts glassy or irregularFlux coating condition problemInspect coating for chips, cracks, dampness
    Delayed crackingHydrogen in restrained/high-strength weldStop using exposed rods for critical work

    Why Moisture Matters on 7018

    E7018 is designed as a low-hydrogen electrode. Its coating must stay dry so the weld deposit stays low in diffusible hydrogen. When the coating absorbs moisture, hydrogen can enter the weld metal and heat-affected zone. That matters most on thicker steel, high-strength steel, cold material, restrained joints, hardenable base metal, repair welds, and code work where hydrogen cracking risk must be controlled.

    Quick Checks

    • Package condition: Use rods from intact hermetically sealed or manufacturer-approved packaging for critical work.
    • Exposure history: If the rod exposure time is unknown, treat it as Unknown (Verify), not acceptable.
    • Surface condition: Reject rods with cracked, chipped, swollen, oily, rusty, or soft coatings.
    • Storage oven: Opened 7018 should be stored in a holding oven at the manufacturer/code-required temperature.
    • Comparison test: Strike a fresh dry rod and a suspect rod on clean scrap. Rough arc, spatter, sticking, or porosity points to rod condition.
    • Job requirement: If the weld is structural or code-controlled, follow WPS, AWS code, and electrode manufacturer instructions.

    Inspection Steps

    1. Identify the electrode. Confirm E7018, E7018-1, E7018 H4R, E7018M, or other exact classification and brand.
    2. Check the container. Confirm whether the package was sealed, vacuum packed, damaged, or previously opened.
    3. Verify exposure time. Record how long rods were outside the oven and the shop humidity/rain exposure.
    4. Inspect the coating. Look for cracks, chips, powdering, swelling, discoloration, oil, rust, or soft flux.
    5. Separate suspect rods. Do not mix them back into the dry low-hydrogen oven inventory.
    6. Check the rod oven. Verify temperature with a reliable thermometer, not just the dial setting.
    7. Confirm rebake rules. Use the electrode manufacturer and job code. Do not invent a rebake schedule.
    8. Run a controlled test only for noncritical screening. Test beads cannot prove low-hydrogen compliance.
    9. Document disposition. Mark rods as fresh, oven-held, rebaked per procedure, downgraded to noncritical use, or discarded.

    Storage and Reconditioning Notes

    Low-hydrogen electrodes commonly require storage in a holding oven after opening. Manufacturer guidance often places low-hydrogen holding ovens in the 225–300°F range, but the exact temperature and exposure limits depend on electrode class, moisture-resistant suffix, manufacturer, and code. Some exposed rods may be rebaked one time under controlled conditions. Rods that became wet, oil-contaminated, cracked, or physically damaged should not be trusted for critical welds.

    Field Fix vs Proper Fix

    ConditionField FixProper Fix
    Opened rods sat out overnightUse fresh sealed rods for critical workFollow manufacturer/code rebake or discard rule
    Rods exposed to rainRemove from low-hydrogen stockDiscard for code/critical work unless procedure permits otherwise
    Rod sticks and spattersCheck amperage and try fresh rodCorrect storage, oven temp, and rod handling
    No rod oven availableUse sealed rods only as openedAdd approved holding oven and exposure log
    Mixed 6010 and 7018 in one warm boxSeparate immediatelyStore low-hydrogen rods separately at required temperature

    Common Wrong-Part and Wrong-Process Mistakes

    • Using damp 7018 on restrained structural joints because the bead still looks smooth.
    • Storing 6010/6011 cellulosic rods in the same oven as 7018 low-hydrogen rods.
    • Believing sealed plastic tubes equal a code-compliant rod oven.
    • Rebaking rods without confirming the electrode classification and manufacturer rule.
    • Using exposed 7018 for pressure, lifting, structural, or code welds without WPS approval.
    • Blaming amperage for sticking when the rod coating is damp or damaged.

    What To Verify Before Welding

    • Electrode classification and brand.
    • Whether the package was factory sealed or already opened.
    • Rod oven temperature and calibration status.
    • Maximum allowed exposure time from the WPS/code/manufacturer.
    • Whether rebake is allowed and exact rebake schedule.
    • Base metal strength, thickness, restraint, preheat, and hydrogen-cracking risk.
    • Whether the job permits reconditioned rods or requires fresh sealed/oven-held electrodes.

    Related Failure Paths

    • Porosity from hydrogen/moisture contamination.
    • Rod sticking from damp coating and unstable starts.
    • Delayed hydrogen cracking in restrained or high-strength welds.
    • Slag irregularity from damaged coating.
    • Arc instability from wrong current, poor ground, or wet rods.
    • Failed inspection from undocumented electrode exposure control.

    Safety Notes

    • Do not use wet or unknown 7018 rods for critical welds.
    • Do not heat rods with open flame, torches, microwaves, or uncontrolled shop heaters.
    • Use rod ovens according to manufacturer instructions and electrical safety requirements.
    • Use ventilation and keep your head out of welding fumes.
    • Follow the WPS, AWS code, engineer, or inspector requirement when low-hydrogen control is specified.

    Sources Checked

    • Lincoln Electric low-hydrogen electrode storage and redrying guidance.
    • ESAB low-hydrogen electrode storage and redrying guidance.
    • Weld Support Parts 7018 sticking, 6010 vs 7018, rod oven, and 7018 electrode pages.
    • Hobart 7018 electrode performance guidance.
  • 000-068P Miller Style M-Series Contact Tip .035 – Arc Weld by Masterweld Pack of (10): Replacement Part Breakdown

    The 000-068P Miller Style M-Series Contact Tip .035 – Arc Weld by Masterweld Pack of (10) is a replacement consumable for MIG welding setups that use a Miller-style M-series contact tip format in .035 in wire size. For maintenance buyers and welders, the main job is simple: keep wire feed stable, keep the electrical transfer consistent, and replace the tip before it becomes a source of arc instability.

    This product listing is a parts-level reference, not a full torch or gun assembly. That matters because the contact tip must match the gun, diffuser, and wire diameter used in the application. Do not assume fit based on the word “Miller style” alone. Check the exact gun model, part family, and wire size before ordering or installing.

    Key Takeaways

    • This is a .035 in contact tip pack.
    • It is described as Miller style M-series replacement hardware.
    • It should be treated as a wear item, not a permanent part.
    • Fit and function depend on the exact gun setup, not just the brand name.
    • If you cannot verify compatibility, stop and confirm before install.

    What the Part Does

    The contact tip is the final current-transfer point between the wire feeder and the arc. When the tip bore wears, the wire can wobble, drag, or chatter. That can show up as erratic feeding, inconsistent arc starts, spatter increase, or a burnback condition. A properly matched tip supports steady wire delivery and helps keep the arc stable.

    For a .035 in wire setup, the bore size must be appropriate for the wire being used. If the wire and tip are mismatched, feeding problems can appear even when the gun liner, drive rolls, and torch are otherwise in good condition.

    Inspection and Verification Steps

    Check: Confirm the wire diameter in use. This product is listed as .035 in. If your process uses another diameter, do not install it without verifying the application.

    Inspect: Remove the current tip and look for a bell-mouthed bore, metal pickup, discoloration, or signs of overheating. Any of these can indicate end-of-life wear.

    Verify: Match the gun and diffuser family. “Miller style M-series” is a description, not a blanket compatibility statement. If the exact machine or gun model is unknown, mark compatibility as Unknown (Verify).

    Check: Confirm the tip seats correctly in the diffuser or tip holder. Cross-threading or a loose seat will create heat and unstable current transfer.

    Inspect: Look at the wire feed path upstream. If the tip is repeatedly failing early, the issue may be liner wear, drive roll pressure, poor wire quality, or contamination.

    Troubleshooting Support

    If the arc feels unstable after tip replacement, isolate the cause step by step.

    • Check the tip bore: A tip that is too tight can cause drag. A tip that is too loose can allow wire wander and poor arc control.
    • Inspect wire condition: Rust, debris, birdnesting, or inconsistent coil tension can mimic a bad tip.
    • Verify contact face condition: Heavy spatter buildup can block smooth transfer and restrict wire exit.
    • Check gun neck heat: Excessive heat can accelerate tip wear. If tips are failing fast, review duty cycle and technique.
    • Verify drive settings: Excess drive-roll pressure can flatten wire and increase friction at the tip.

    If you cannot identify the root cause, treat the issue as a system problem rather than a single consumable failure. Replace the tip only after confirming the surrounding feed components are in serviceable condition.

    Product / Parts Notes

    The product identified here is the Amazon ASIN-linked pack of 10. Use the product reference below as the purchase and parts lookup point, but verify the actual gun compatibility on your side before use.

    No products found.

    Because no manufacturer cross-reference page or WSP lookup page was provided for this item, compatibility details remain Unknown (Verify). Do not assume equivalency to other Miller-style tips without checking the torch series, thread style, and seating design.

    How to Use This Part Safely

    • Power down the welding machine before changing consumables.
    • Let the gun cool before handling a tip that may be heat-soaked.
    • Use the correct tool pressure when installing to avoid thread damage.
    • Replace damaged or rounded tips; do not reuse a tip with a poor seat.
    • Confirm shielding gas and wire feed settings after any consumable change.

    When to Replace

    Replace the contact tip when wire feed becomes inconsistent, the orifice shows wear, or the tip has accumulated enough spatter that cleaning no longer restores performance. For maintenance planning, tips are consumable stock items. Keep spares on hand, but verify the exact style and size used in each cell or truck.

    FAQ

    Is this tip automatically compatible with all Miller guns?
    No. It is described as Miller style M-series in .035 in size, but exact compatibility is Unknown (Verify) until you confirm the gun, diffuser, and thread/interface details.

    Can I use this with a different wire diameter?
    Not without verification. A contact tip should match the wire size being run. If the wire size differs, fit and feeding can be affected.

    What causes a contact tip to fail early?
    Common causes include incorrect wire size, excess drive-roll pressure, contamination, poor liner condition, overheating, and spatter buildup. Check the full wire feed path, not only the tip.

    Is a pack of 10 enough for maintenance stock?
    That depends on production rate, changeout frequency, and job conditions. Stock planning is site-specific. Verify usage history before setting par levels.

    Safety Notes

    Always de-energize the system before service. Hot tips can burn skin and can also hide heat damage in adjacent parts. Do not force-thread consumables. If a part does not install cleanly, stop and verify the part family and fitment. Use PPE appropriate to the task and follow site lockout and hot-work procedures.

    Sources Checked

    • Provided Amazon ASIN registry reference: B07Y42LZC2
    • Provided product name: 000-068P Miller Style M-Series Contact Tip .035 – Arc Weld by Masterweld Pack of (10)
    • Provided internal links: none applicable beyond the allowed product reference

    Where technical specifics were not provided in the source package, details are marked Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

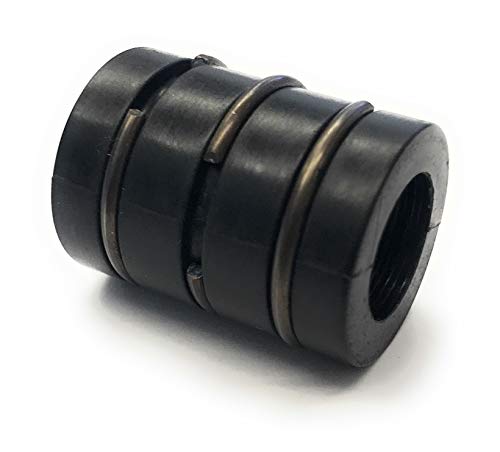
  • S19394-2 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2): Product Breakdown

    S19394-2 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2): Product Breakdown

    Product not found.
    “>S19394-2 Lincoln Style Nozzle Insulator - Arc Weld by Masterweld Pack of (2)

    The S19394-2 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2) is a replacement support part for MIG gun consumable assemblies. The product note provided by the source is specific: use with S18697-47 gas diffuser and Slip Style Nozzles, and it does not work with PRO series. That is the main fitment point to verify before you order or install.

    For buyers, maintenance teams, and welding support staff, the practical question is not just what the part is called, but where it sits in the torch assembly and what it will physically mate with. An insulator in this location supports nozzle placement and helps maintain separation between the nozzle and internal consumable parts. If the fit is wrong, the torch may run poorly, parts may not seat correctly, or the assembly may fail during routine use.

    Key Takeaways

    • This is a Lincoln style nozzle insulator sold as a pack of 2.
    • The source states it is for use with S18697-47 gas diffuser and Slip Style Nozzles.
    • The source states it does not work with PRO series.
    • Compatibility beyond that note is Unknown (Verify).
    • Confirm gun model, diffuser, and nozzle style before installing.

    What to check before you buy

    Do not rely on the product name alone. Lincoln-style parts can look similar across multiple torch families, but the interface details matter. Before ordering, review the current consumable stack on the gun and verify the part path from diffuser to nozzle.

    1. Check the diffuser part number. Compare your installed gas diffuser to S18697-47. If your diffuser number is different, compatibility is Unknown (Verify).
    2. Inspect nozzle style. Confirm that the gun uses Slip Style Nozzles. If the nozzle is a different design, do not assume this insulator will fit.
    3. Verify series family. The source says it does not work with PRO series. If the gun or consumable set is PRO series, stop and verify an alternate part.
    4. Check wear history. If you are replacing insulators often, inspect the nozzle, diffuser, and contact tip for heat damage, spatter buildup, or thread damage. The insulator may be a symptom, not the root cause.

    How to inspect the part on arrival

    When the package arrives, inspect both pieces before bringing them into service. This is basic receiving control and helps avoid assembly problems later.

    • Verify quantity. The product is sold as a pack of 2. Confirm both parts are present.
    • Inspect molding or machining quality. Look for cracks, deformation, or damaged interfaces. Any defect at the insulating surfaces can affect fit.
    • Check the seating surfaces. Confirm the part seats cleanly on the intended diffuser and accepts the intended slip nozzle without forcing.
    • Compare to the removed part. If you replaced an old insulator, place the old and new parts side by side and compare profile, depth, and engagement points.

    Installation check steps

    Use a controlled install process. Do not force a consumable stack together if the parts resist seating.

    1. Power down the welding system. Lock out or de-energize the machine according to site procedure.
    2. Remove the nozzle and diffuser assembly. Clean any spatter or buildup before attempting reassembly.
    3. Install the insulator on the correct diffuser. Confirm the diffuser is S18697-47 or otherwise verified as compatible.
    4. Fit the slip style nozzle. Seat the nozzle fully without excessive force.
    5. Verify alignment. Confirm the nozzle is centered and stable, with no visible tilt or cross-seating.
    6. Test run at low duty. Run a brief weld or gas-only check per shop practice and inspect for abnormal heat, looseness, or arc instability.

    Troubleshooting and support checks

    If the assembly does not fit or the torch behaves poorly after replacement, work through the problem methodically.

    Problem: The insulator does not seat correctly

    • Check: Is the diffuser actually S18697-47?
    • Inspect: Look for spatter, burn marks, or distortion on the diffuser and nozzle.
    • Verify: The gun is not PRO series. The source says this part does not work with PRO series.

    Problem: Nozzle feels loose after installation

    • Check: Is the nozzle style truly Slip Style?
    • Inspect: The nozzle and diffuser engagement surfaces for wear.
    • Verify: There is no missing support part in the consumable stack.

    Problem: Frequent burnback or heat damage

    • Check: Contact tip condition, gun stickout, and spatter control practices.
    • Inspect: Whether the nozzle and insulator are being overheated by poor fit or buildup.
    • Verify: The torch is configured correctly for the application; the insulator alone will not correct a setup issue.

    Product and parts notes

    This article is limited to the supplied ArcWeld product information. The confirmed product note is:

    • Product: S19394-2 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2)
    • Use note: Use with S18697-47 gas diffuser and Slip Style Nozzles
    • Restriction note: Does not work with PRO series

    Any additional fitment data is Unknown (Verify). If you are supporting multiple gun models in the shop, keep the current removed part and the gun model reference available before you place a replacement order.

    Safety notes

    • De-energize equipment before touching consumable assemblies.
    • Allow hot components to cool before handling.
    • Do not force mismatched parts together.
    • Use eye protection when removing spatter or cleaning the nozzle stack.
    • If any part shows cracking, severe heat damage, or deformation, replace it rather than returning it to service.

    FAQ

    Is this insulator compatible with PRO series guns?

    No. The source note says it does not work with PRO series. If your setup is PRO series, compatibility is Unknown (Verify) until you confirm a different part.

    What diffuser should I check first?

    Check for S18697-47 gas diffuser, since that is the only diffuser called out in the source note. If your diffuser is different, verify fit before use.

    What nozzle style is specified?

    The source calls for Slip Style Nozzles. If you use another nozzle style, do not assume this insulator will fit correctly.

    How many parts are included?

    The product title states a pack of (2). Verify the received quantity during inspection.

    Sources Checked

    “>S19394-2 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2)
  • Internal link provided for contextual welding content: Aluminum ER 5554 3/64″ X 5lb. MIG Welding Wire Spool By Washington Alloy – Weld Support Parts Blog

Note: No WSP lookup page or filler metal finder page was provided for this task. Compatibility beyond the source note remains Unknown (Verify).

Related Arc Weld Part

S19394-2 Lincoln Style Nozzle Insulator - Arc Weld by Masterweld Pack of (2)

S19394-2 Lincoln Style Nozzle Insulator – Arc Weld by Masterweld Pack of (2)

Lincoln Style Nozzle Insulator – Use with S18697-47 gas diffuser and Slip Style Nozzles – Does not work with PRO series

View at Arc Weld Store

Related Weld Support Guides

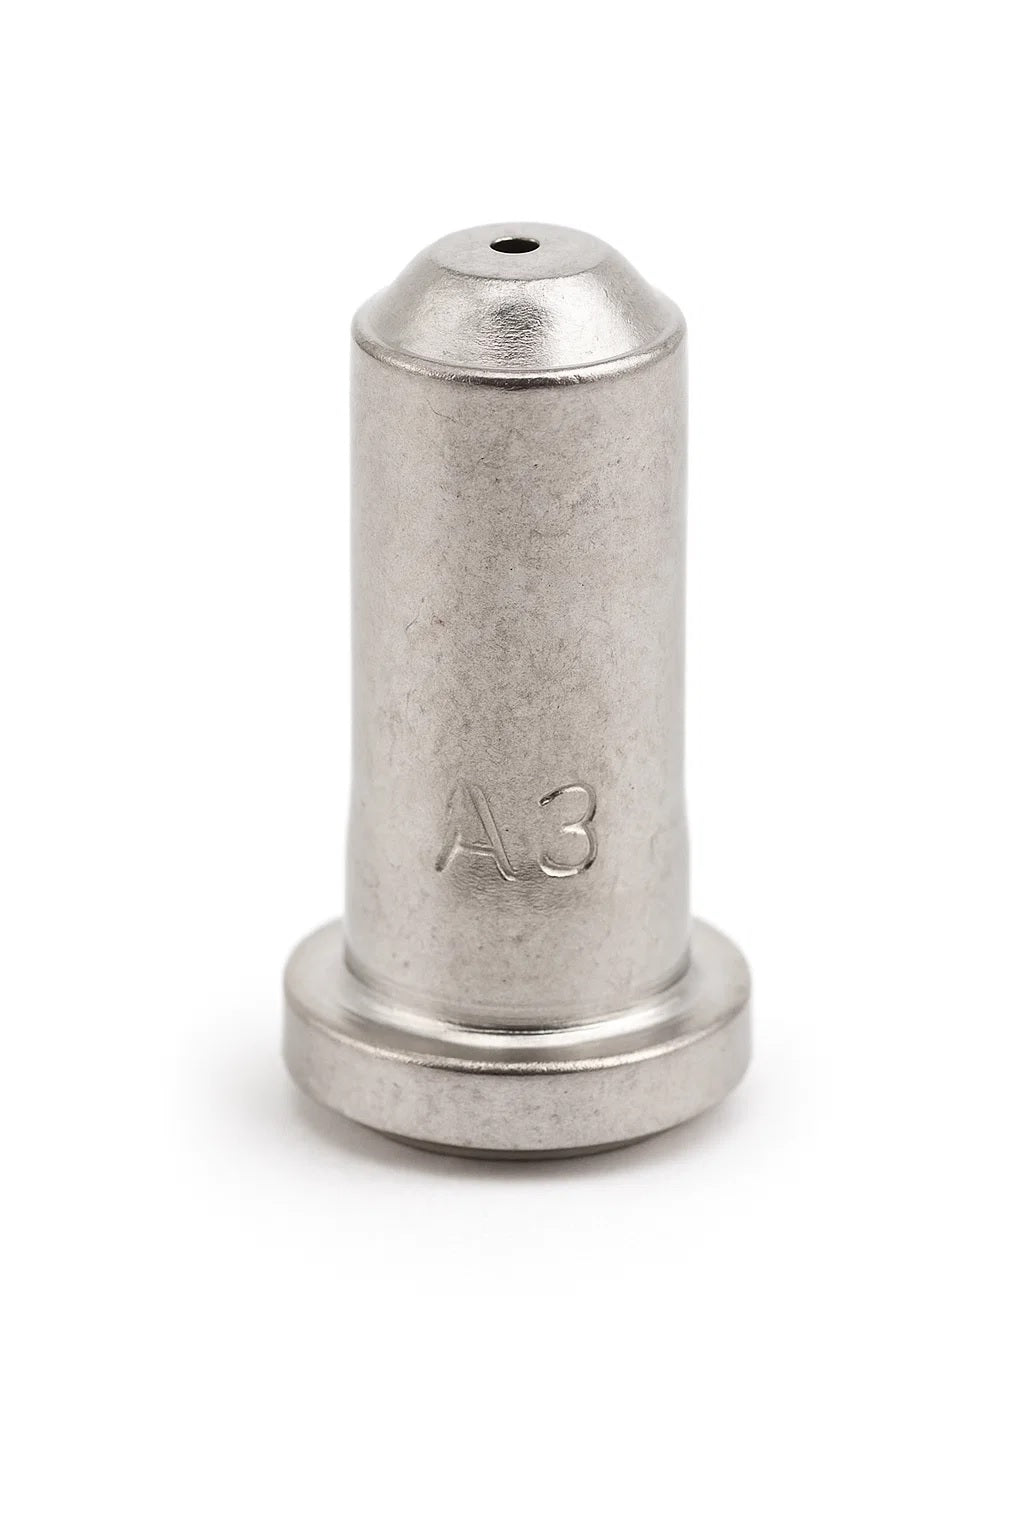
  • ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5): Product Breakdown

    ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5): Product Breakdown

    Product not found.
    “>ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5)

    The ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5) is a consumable part used in plasma cutting. For buyers, maintenance teams, and welding support staff, the main question is not whether it is a replacement part, but whether it matches the torch family, amperage range, and cut duty you actually run on the shop floor. This draft stays focused on that practical check.

    The product page indicates this is a 30 amp nozzle intended for PT-23 and PT-27 Plasmarc plasma torches. Beyond that, the important technical details that affect fit and performance should be verified against the machine manual and the torch consumable chart before purchase or installation. If a detail is not confirmed in the source material, treat it as Unknown (Verify).

    Key Takeaways

    What This Part Does

    A plasma nozzle constricts and directs the plasma arc. In practical terms, it affects kerf shape, arc concentration, and edge quality. A worn nozzle can show up as wider kerf, rougher edge, harder starts, arc instability, or accelerated wear in related consumables. If your cut quality has changed, do not assume the nozzle is the only cause. Air contamination, electrode wear, damaged swirl components, incorrect stand-off, and double arcing can produce similar symptoms.

    For broader root-cause checks, see the support article on plasma torch nozzle damage causes. For torch-family and consumable matching logic, the plasma drag shield compatibility guide is a useful reference point, even though this part is a nozzle and not a drag shield.

    Buyer Checklist Before Ordering

    Use this as a field check before you place the order or pull stock for a job:

    Support and Troubleshooting Notes

    When a nozzle is replaced too early, the real problem usually stays in the system. Use a simple inspect sequence:

    1) Inspect the nozzle. Remove it and examine the orifice under good light. Check for wash-out, eccentric wear, cracks, or heavy spatter. If the opening no longer looks uniform, replacement is justified.

    2) Inspect the electrode. A damaged electrode can create arc instability that looks like nozzle failure. Replace related consumables as a set when wear is obvious or when the torch manual recommends it.

    3) Inspect air quality. Moisture, oil, and dirt in the air supply shorten consumable life. Verify dryer function, filter condition, and regulator behavior. If air quality has not been measured recently, it is Unknown (Verify).

    4) Verify torch assembly condition. Check for damaged threads, loose fit, worn retaining parts, and signs of double arcing. If the consumable stack does not seat correctly, the nozzle will not run as expected.

    5) Verify cut setup. Wrong travel speed or stand-off can destroy a new nozzle quickly. If the cut profile is poor immediately after installation, the issue may be setup rather than part quality.

    Product / Parts Section

    The source product information identifies the part as ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5). The product summary also states use with PT-23 and PT-27 Plasmarc torches. No additional verified specs were provided in the source material, so any further material, dimensions, or certifications are Unknown (Verify).

    For sourcing support, the product can be reviewed through the provided ArcWeld listing: Product not found.

    “>ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5). Use the listing as the product reference, then verify torch compatibility and amperage in the machine documentation before deployment.

    How to Verify Fit in the Shop

    Before issuing the part, run these checks:

    Safety Notes

    FAQ

    Is this nozzle only for the PT-27?
    The source product information also states PT-23 compatibility. Verify the actual torch model and consumable chart before ordering.

    Can I use this nozzle at amperage other than 30 amp?
    The listing identifies it as a 30 amp nozzle. Other amperage use is Unknown (Verify) unless confirmed by the torch and power source documentation.

    What causes a new nozzle to fail quickly?
    Common causes include poor air quality, incorrect stand-off, damaged electrode parts, double arcing, and cutting too fast or too slow. Check the full system, not just the nozzle.

    Should I replace only the nozzle?
    Not always. If the electrode or other consumables are also worn, replace the worn set as a group according to the torch manual.

    Sources Checked

    Final note: treat this part as a consumable matched to a specific torch system. Verify torch model, amperage, and assembly details before purchase and before installation. If any technical detail is not confirmed by source material or machine documentation, mark it Unknown (Verify).

    Related Arc Weld Part

    ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5)

    ESAB Model 33368 30 Amp Nozzle for Plasmarc PT-27 Plasma Torch, Pack of (5)

    ESAB 33368 – 30 Amp Plasma Nozzle for Plasmarc PT-27 Torch (5-Pack) The ESAB 33368 is a 30 amp nozzle designed for use with PT-23 and PT-27 Plasmarc plasma torches. Engineered for clean, efficient cuts in light to medium-gauge metal, this nozzle delivers consistent arc stability and cut quality. Each pack contains five OEM-grade nozzles, ensuring reliable performance and compatibility with ESAB plasma systems. Spe…

    View at Arc Weld Store

    Related Weld Support Guides

  • Choosing Carbon Arc Gouging Rod Size

    Choosing Carbon Arc Gouging Rod Size

    Carbon Arc / Slice Torch Support

    Choosing the right carbon arc gouging rod size is not just a consumable choice. It affects arc stability, metal removal rate, groove width, operator control, and the load you place on the power source. Buyers often start with rod diameter alone, but the better approach is to match rod size to machine capacity, joint access, and the amount of metal that must be removed.

    If the rod is too small for the job, gouging can be slow and unstable. If it is too large, the arc may be hard to control, the machine may be overloaded, and the groove can become wider than needed. The correct carbon arc gouging rod size depends on the equipment and the job, not on a single rule.

    Key Takeaways

    • Match carbon arc gouging rod size to the power source output and the required metal removal rate.
    • Use the smallest rod that will complete the job efficiently when access and groove size allow it.
    • Verify torch, holder, and air system setup before starting.
    • Inspect the groove shape and adjust rod size if penetration, control, or removal rate is not meeting the job requirement.
    • When technical details are not confirmed by the equipment maker, mark them as Unknown (Verify).

    How Rod Size Affects the Cut

    Carbon arc gouging rod size changes how much current the process can use and how much material the arc removes. Larger rods generally support heavier gouging work, while smaller rods are better for lighter removal, tighter access, and more controlled groove work. The specific current range for any rod is Unknown (Verify) unless the rod manufacturer or equipment documentation confirms it.

    For maintenance buyers and welding support teams, the practical question is simple: does the rod size let the operator remove the required metal without fighting the arc or overloading the machine? If the answer is no, the size is wrong for the job.

    Check the Job Before Selecting a Rod

    Check: the amount of metal to be removed, the width of the groove needed, and the available access around the workpiece.

    Inspect: whether the work is surface cleanup, weld removal, backgouging, crack removal, or defect repair. Each job type can justify a different rod size.

    Verify: the power source capacity, polarity requirements, air supply setup, and holder compatibility in the equipment manual. If the manual is not available, those details are Unknown (Verify).

    A common buying mistake is to choose rod size only by habit. A team may stock one size because it is used often, but that does not mean it is the best choice for every repair. The right size should be chosen against the work scope and the machine available on site.

    Machine Capacity: The First Filter

    Before looking at groove dimensions, confirm the machine can support the planned gouging setup. Carbon arc gouging places a load on the power source, and the rod diameter influences that load. If a larger rod is selected without checking machine capability, the operator may see poor arc control, excessive heat, or repeated setup problems.

    Check: the machine nameplate and gouging guidance in the owner’s manual.

    Inspect: cable condition, connection tightness, and holder wear before starting.

    Verify: the machine can deliver the required output for the selected rod size. If not stated clearly by the manufacturer, keep the rating as Unknown (Verify).

    Job Type and Rod Size Selection

    For light repair work, smaller rod sizes are often easier to control. They can help when the goal is to remove defects without taking too much base metal. For heavy removal or deep backgouging, a larger rod may be needed to maintain progress and keep the work efficient.

    Use this practical approach:

    • Light cleanup or localized defect removal: start with a smaller rod size.
    • General gouging on medium sections: choose a mid-range rod size that balances control and removal rate.
    • Heavy removal or deep groove work: consider a larger rod size if the machine and holder setup support it.

    These are job-planning guidelines, not published size charts. Final selection should be based on the consumable maker’s instructions and the power source manual. If those details are not verified, they remain Unknown (Verify).

    Troubleshooting Rod Size Problems

    If gouging performance is poor, do not assume the rod is bad. Check the full setup first.

    Check: whether the rod is too small for the groove width or metal removal requirement.

    Inspect: the arc for instability, excessive spatter, or uneven groove formation.

    Verify: that the rod is clamped correctly, the air stream is aligned, and the machine output matches the job.

    If the groove is too wide or the operator is losing control, the rod may be too large for the application. If removal is too slow or the arc is difficult to maintain, the rod may be too small or the machine may be under capacity. Either way, work back through the setup before changing more variables.

    WSP Lookup Section

    For support resources and related carbon arc information, see the Weld Support Parts carbon arc support page: Carbon Arc / Slice Torch Support.

    This page can help buyers and support teams confirm the support category before selecting consumables or accessories. Product-specific details on that page should still be verified against the manufacturer documentation when available.

    Safety Notes

    • Wear proper eye, face, hand, and body protection for carbon arc gouging.
    • Keep flammables away from the work area.
    • Use ventilation suitable for smoke and fumes.
    • Confirm cables, holders, and air connections are in safe condition before energizing the circuit.
    • Do not guess on equipment ratings. If a value is not confirmed, treat it as Unknown (Verify).

    FAQ

    How do I choose the right carbon arc gouging rod size?
    Start with the job requirement, then confirm the machine can support the rod size. Use a smaller rod for tighter control and lighter removal, and a larger rod for heavier removal if the equipment supports it.

    Can I use one rod size for every gouging job?
    Not reliably. One size may cover several common tasks, but different groove widths, removal depths, and access conditions often call for different rod sizes.

    What if I do not know the machine’s gouging capacity?
    Stop and verify the machine manual, nameplate, or manufacturer guidance. If the capacity is not confirmed, it is Unknown (Verify).

    What should I check if the gouge is uneven?
    Check rod size, air alignment, cable condition, holder contact, and operator travel speed. Uneven gouges are often caused by setup issues, not rod size alone.

    Sources Checked

    Related Weld Support Guides

  • When to Replace Carbon Arc Electrodes

    Profax AEC-403, Carbon Arc Torch Insulator Assembly, Pack of (2)
    “>Profax AEC-403, Carbon Arc Torch Insulator Assembly, Pack of (2)

    Carbon arc electrodes do not last indefinitely. Replace them when wear, contamination, damage, or fit issues start to affect arc stability, gouging quality, or torch performance. Waiting too long can increase heat input, reduce control, and create avoidable torch or workpiece problems.

    Key Takeaways

    When to Replace a Carbon Arc Electrode

    Use the electrode until it no longer supports a stable, controllable arc. Replace it if you see any of the following:

    Signs the Electrode Is No Longer Serviceable

    Some signs are obvious. Others show up as process problems.

    Troubleshooting Before Replacement

    Do a basic check before discarding the electrode. Some problems come from the setup, not the carbon itself.

    If the problem remains after inspection and cleaning, replace the electrode. If instability continues, inspect the torch components and power delivery path. Unknown (Verify) for model-specific fault isolation.

    Replacement Timing for Maintenance Teams

    For shop and field support, track replacement by condition instead of waiting for a hard failure. Replace electrodes when inspection shows:

    Keep spare electrodes in clean, dry storage and protect them from impact. Carbon parts can be damaged in ways that are not obvious until the torch is in service.

    Product and Parts Check

    When servicing compatible arc gouging torches, verify the correct replacement parts before ordering. The following product is available in the ArcWeld catalog:

    Product link: Profax AEC-403, Carbon Arc Torch Insulator Assembly, Pack of (2)

    Do not assume compatibility beyond the listed torch models. Verify the part number and torch model before installation.

    Safety Notes

    FAQ

    How do I know a carbon arc electrode is worn out?
    Look for heavy tip wear, cracking, chipping, contamination, or unstable arc performance.

    Can I keep using a damaged electrode?
    No. Damage can reduce control and increase the chance of poor gouging performance or torch issues.

    What causes premature electrode replacement?
    Common causes include wrong size, poor storage, contamination, improper setup, and handling damage.

    Should I replace the electrode or the torch part?
    Replace the electrode first if the wear is on the carbon itself. If the torch holder, clamp, or insulator is damaged, inspect and replace those parts as needed. Unknown (Verify) for model-specific repair limits.

    Sources Checked

    Related Arc Weld Part

    Profax AEC-403, Carbon Arc Torch Insulator Assembly, Pack of (2)

    Profax AEC-403, Carbon Arc Torch Insulator Assembly, Pack of (2)

    Profax Insulator Assembly For AEC-3500, AEC-3500-1, AEC-4000-1, AEC-4500-1, AEC-5500 And AEC-5500-1 Arc Gouging Torches. Package of (2)

    View at Arc Weld Store
  • Stick Welding Porosity Troubleshooting: Pinholes, Wormholes, Moisture, Arc Length, and Electrode Checks

    Stick welding porosity usually comes from gas trapped in the weld metal before the puddle freezes. With SMAW, start with the electrode, base metal, arc length, amperage, polarity, and technique before blaming the welder. Pinholes after slag removal, wormholes in the bead, rough starts, popping arc behavior, and scattered pits usually point to moisture, contamination, long arc length, wrong rod handling, or welding over paint, oil, rust, zinc, primer, or damp steel.

    The repair path is simple: stop welding, identify whether the porosity is surface-only or through the bead, clean the joint to bright metal, switch to known-good electrodes, shorten the arc, verify amperage and polarity, and run a controlled test bead on clean scrap. For low-hydrogen rods, especially 7018, porosity must be treated as a storage and hydrogen-control issue, not only a bead appearance problem. See the related WSP guide on 7018 rod moisture contamination when damp rods, sticking, or cracking risk are present.

    Common Symptoms

    SymptomLikely CauseFirst Check
    Small pinholes after chipping slagMoisture, contamination, or long arcTry dry rods on clean scrap
    Wormholes or tunnels in beadSevere contamination or trapped gasGrind out and clean joint
    Porosity starts after rod changeBad rod batch, damp coating, wrong rod storageCompare against sealed rods
    Porosity only at startsPoor restart, long arc, damp rod tipClip/restrike properly and shorten arc
    Porosity on rusty or painted steelSurface contamination burning into puddleRemove coating and re-test
    Porosity with 7018 plus stickingLow amperage, damp coating, bad arc lengthCheck storage and amperage

    Likely Causes

    Moisture in electrodes: Damp coating can release hydrogen and other gases into the weld pool. Low-hydrogen electrodes are especially sensitive. Opened 7018 should be stored according to the electrode manufacturer, code, and WPS requirements.

    Dirty base metal: Oil, grease, paint, primer, rust, mill scale, cutting fluid, galvanized coating, and moisture can create gas pockets when heated. Stick welding is more tolerant than TIG or MIG, but it is not immune to contamination.

    Long arc length: A long arc can reduce shielding from the electrode coating and pull air into the arc zone. This is common with new operators trying to see the puddle.

    Wrong rod manipulation: Excessive whipping with low-hydrogen rods can cause porosity. Some cellulose rods tolerate whip-and-pause technique, but 7018 should normally be run with a short, steady arc.

    Wrong amperage or polarity: Too-low amperage can leave a cold, sluggish puddle that traps gas. Wrong polarity can create instability, spatter, poor penetration, and porous starts. If the symptom includes sticking, review 7018 rod sticking causes and solutions.

    Quick Checks

    • Use fresh, known-good electrodes from sealed or properly stored packaging.
    • Clean the weld area to bright metal at least 1/2 in beyond the weld zone.
    • Remove oil, paint, primer, zinc, moisture, rust, and grinding dust before welding.
    • Shorten the arc until the puddle is controlled and the arc sounds steady.
    • Verify polarity: 6010 commonly requires DCEP, while many 7018 rods run on AC or DCEP depending on formulation.
    • Check amperage against the rod diameter, position, and manufacturer chart.
    • Run one test bead on clean scrap with one change at a time.

    Root Cause Analysis

    If porosity disappears on clean scrap with fresh rods, the welder is probably not the root cause. The problem is usually the workpiece surface, electrode condition, or joint environment. If porosity follows one rod container but not another, quarantine the suspect rods. If porosity appears only in vertical or overhead work, look at arc length, travel speed, rod angle, and slag control.

    For rod selection, the difference between cellulose and low-hydrogen electrodes matters. WSP’s 6010 vs 7018 guide explains that 6010 is used for digging penetration and root work, while 7018 is used for low-hydrogen structural welds. Do not store or run them the same way. Mixing 6010 and 7018 in the same oven or job box can create wrong-rod and wrong-storage problems.

    Inspection Steps

    1. Chip and wire-brush the weld. Confirm whether holes are isolated surface pits or continuous porosity.
    2. Grind one defect open. If holes continue below the surface, remove the weld until sound metal is reached.
    3. Inspect rod coating. Reject rods with cracked, swollen, oily, soft, rusty, chipped, or wet coating.
    4. Check base metal. Look for paint, oil, water, galvanizing, primer, heavy rust, cutting fluid, and laminations.
    5. Check machine setup. Confirm amperage, polarity, lead connections, work clamp contact, and cable condition.
    6. Check technique. Look for long arc, excessive weave, whipping with low-hydrogen rods, or travel speed too fast for gas escape.
    7. Make a comparison weld using clean scrap and fresh rods. If the test is sound, return to the workpiece and correct cleaning or joint conditions.

    Test Procedures

    Use a clean scrap coupon of the same material when possible. Run three beads: one with the suspect rod, one with a fresh rod from sealed storage, and one after changing arc length and amperage. Keep polarity, rod diameter, and base metal consistent. If only the suspect rod creates porosity, remove that rod batch from critical work. If all beads are porous, inspect work clamp contact, machine output, arc length, and surface preparation.

    For 7018, test beads are not proof of low-hydrogen compliance. A rod can make an acceptable-looking bead and still be unacceptable for code, pressure, structural, lifting, or restrained work if exposure history is unknown. Follow the WPS, inspector, electrode manufacturer, or engineer requirement.

    Visual Wear Indicators

    • Electrode coating cracks: moisture cycling, impact damage, or old stock.
    • Soft or powdery coating: moisture damage; do not use for critical welds.
    • Rust on exposed core wire: storage failure or aged rods.
    • Oily rod surface: contamination that can create porosity and fumes.
    • Blackened start pits: poor restart, contamination, or arc instability.
    • Glassy irregular slag on 7018: possible damp coating or incorrect settings.

    Compatibility Notes

    Verify electrode classification, rod diameter, polarity, amperage range, base metal, position, and storage requirement before ordering or welding. E6010, E6011, E7014, E7018, E7018-1, E7018AC, stainless electrodes, nickel cast-iron rods, and hardfacing electrodes do not share the same storage, polarity, or technique rules. When the rod is unknown, label it Unknown (Verify) and do not use it on critical welds.

    What To Verify Before Ordering

    • Exact electrode class and brand required by the WPS or repair procedure.
    • Rod diameter that matches material thickness, position, and available amperage.
    • Machine output and polarity compatibility.
    • Whether 7018AC is required for an AC-only transformer machine.
    • Whether low-hydrogen storage, sealed cans, rod oven, or quiver control is required.
    • Base metal condition: clean mild steel, rusty repair work, galvanized, coated, cast iron, hardfacing, or unknown alloy.

    Common Wrong-Part Mistakes

    • Using old open 7018 from a toolbox on a structural repair.
    • Buying standard 7018 for a machine that only runs AC poorly.
    • Using 6010 because it burns through contamination instead of cleaning the joint.
    • Running a specialty electrode like nickel or hardfacing without checking polarity and procedure.
    • Assuming porosity is always caused by amperage when the rod is damp or the base metal is contaminated.

    Field Fix vs Proper Fix

    ConditionField FixProper Fix
    Pinholes with 7018Try fresh dry rods on clean scrapCorrect rod storage and follow WPS exposure limits
    Porosity over paint or rustGrind test area cleanRemove coating from full weld zone before welding
    Long arc porosityShorten arc and reduce travel speedRetrain technique and verify settings
    Damp rods in the fieldUse sealed fresh rods for noncritical testingUse approved oven/quiver procedure or discard
    Wormholes in finished weldStop and mark defectGrind out to sound metal and reweld under corrected conditions

    Related Failure Paths

    Porosity often travels with rod sticking, slag inclusions, lack of fusion, undercut, arc blow, cracking, and failed visual inspection. A bad ground or unstable arc can make the operator hold a longer arc, which then creates porosity. Damp 7018 can create porosity and increase hydrogen-cracking risk. Poor fume control is also common when welding dirty, coated, or contaminated steel; review welding fume extractor troubleshooting when smoke is not being captured at the arc.

    Safety Notes

    Do not weld over unknown coatings, paint, solvent residue, oil, galvanized coating, plating, or contaminated steel without identifying the hazard. Use ventilation, fume extraction, correct helmet shade, dry gloves, fire watch, and electrical safety practices. Keep your head out of the plume. Do not use wet rods, improvised rod heating, torch-baked electrodes, microwave drying, or truck-dash drying for low-hydrogen work.

    Sources Checked

    • Washington Alloy electrode catalog sections on 6010, 7018, low-hydrogen welding tips, and porosity warnings related to whipping low-hydrogen electrodes.
    • Lincoln Electric consumables storage and handling guidance for covered electrodes and moisture-resistant packaging.
    • Weld Support Parts stick welding support articles on 7018 moisture contamination, 7018 sticking, 6010 vs 7018 selection, and fume extraction troubleshooting.
  • MIG Ground Clamp Connection Problems: Arc Sputter, Heat, Poor Starts, and Weak Current Return

    A bad MIG ground clamp connection causes arc instability, poor starts, extra spatter, weak penetration, burnback, and random sputtering even when voltage and wire speed look correct. The work clamp is not just an accessory; it completes the welding circuit. If the clamp is loose, corroded, undersized, attached over paint/rust, or connected through a weak table path, the machine cannot deliver steady current to the weld.

    Start with the simple test: move the work clamp directly to clean bare metal on the workpiece, as close to the weld as practical. If the arc immediately becomes smoother, the problem is in the work return path, not the MIG gun, wire, or machine settings. Do this before changing voltage, wire speed, drive-roll pressure, or gas flow.

    Related MIG checks include welding cable and connector sizing, MIG wire feed slipping troubleshooting, and MIG burnback at the contact tip.

    Common Symptoms

    SymptomLikely Ground Clamp CauseFirst Check
    Arc sputters or cuts in and outLoose clamp, dirty contact, weak cable lugClamp directly to clean bare metal
    Hard arc startsHigh resistance at work clamp or table connectionClean workpiece and clamp jaws
    Clamp gets hotUndersized clamp, loose cable connection, poor jaw contactInspect lug, spring pressure, and cable size
    Spatter increases suddenlyUnstable current return pathMove clamp closer to weld
    Settings seem inconsistentVoltage drop through bad work lead or connectionInspect full work cable path

    What This Part Does

    The MIG work clamp connects the workpiece to the machine’s work lead so welding current can return to the power source. A clean, tight, low-resistance path lets the arc stay consistent. A poor path forces current through rust, paint, bearings, table hinges, loose bolts, thin sheet edges, or damaged cable strands. That resistance turns into heat and unstable arc behavior.

    Inspection Steps

    1. Stop welding and let hot parts cool. A hot clamp or lug can burn gloves and damage insulation.
    2. Move the clamp to the workpiece. Do not rely on the welding table unless the table connection is clean and proven.
    3. Clean the clamp spot. Grind or brush to bare metal. Remove paint, rust, mill scale, primer, oil, and heavy oxidation.
    4. Check jaw bite. Weak spring tension or worn copper/brass contact surfaces reduce contact area.
    5. Inspect the cable-to-clamp lug. Look for loose bolts, dark heat marks, melted insulation, green corrosion, or broken strands.
    6. Check cable size and length. Long leads or undersized cable can overheat and drop voltage.
    7. Check the machine-end connector. Loose Dinse, Tweco-style, stud, or lug connections can create the same symptoms as a bad clamp.
    8. Run a test bead. Use the same settings before and after moving the clamp so the ground-path change is isolated.

    What Wears Out First

    • Clamp jaws: arcing, rust, and grinding dust reduce metal-to-metal contact.
    • Spring tension: weak springs allow vibration and poor bite on the workpiece.
    • Cable lug: heat cycling loosens bolts and oxidizes the connection.
    • Cable strands: repeated bending near the clamp breaks copper under the jacket.
    • Machine connector: loose or worn plugs create heat and voltage drop.

    Test Procedures

    Clamp relocation test: Attach the work clamp directly to bright metal on the part. If the arc stabilizes, clean the old clamp point or repair the table/work lead path.

    Heat test: After a short weld, carefully check whether the clamp, lug, or machine connector is hotter than expected. Heat at a connection usually means resistance.

    Cable flex test: With power off, flex the work lead near the clamp and connector. Crunching, soft spots, or intermittent stiffness can indicate broken copper strands or jacket damage.

    Field Fix vs Proper Fix

    ProblemField FixProper Fix
    Clamp on painted metalMove to bare metalAdd a cleaned clamp pad to the workflow
    Clamp jaws dirtyWire brush jawsReplace worn or burned clamp
    Loose lug boltTighten after coolingReplace damaged lug and verify crimp/bolt connection
    Clamp gets hotReduce duty cycle and inspectInstall properly rated clamp/cable assembly
    Table path unreliableClamp directly to partMaintain dedicated work lead connection point

    Common Wrong-Part Mistakes

    • Buying a clamp by jaw size only instead of current rating and cable size.
    • Installing a new clamp on a burned or undersized cable.
    • Reusing a loose lug that has already overheated.
    • Assuming a clean welding table guarantees a clean work return path.
    • Replacing the MIG gun or contact tip before testing the work clamp connection.

    Compatibility Notes

    Ground clamp replacement depends on machine output amperage, duty cycle, cable size, connector style, and lead length. Do not assume one clamp fits every MIG welder. If the machine uses a Dinse, Tweco-style, stud, or lug connection, verify connector size before ordering. Some Weld Support Parts accessory pages list lead sets and connector styles, but compatibility must be matched to the actual welder and cable assembly.

    For connector and cable planning, see the welding cable connector kit guide and verify any machine-specific connector before replacement.

    Related Failure Paths

    • Arc instability mistaken for wire-feed trouble.
    • Spatter increase blamed on voltage settings.
    • Contact tip burnback caused by unstable arc behavior.
    • Poor penetration caused by current loss through a bad return path.
    • Overheated work lead insulation from undersized cable or loose lugs.

    Safety Notes

    • Disconnect input power before servicing cable lugs, connectors, or internal machine terminals.
    • Do not touch hot clamps, lugs, or cable ends with bare hands.
    • Replace melted insulation, cracked clamps, or burned connectors instead of continuing to weld.
    • Never let welding current return through bearings, chains, lift tables, hinges, or vehicle electronics.
    • Use welding PPE and adequate ventilation during test welds.

    Sources Checked

    • Weld Support Parts welding cable connector kit guide.
    • Weld Support Parts MIG support pages mentioning work clamp checks.
    • Lincoln Electric MIG troubleshooting resources.
    • American Torch Tip MIG cable conductivity troubleshooting.
    • Weld Support Parts machine accessory pages showing cable/connector examples.
  • More posts

    Stream with Amazon Music