Search results for: “TIG welding parts”

  • ERTi-2 TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERTi-2 TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERTi-2 TIG / GTAW Filler Metal

    ERTi-2 TIG / GTAW filler metal is used as a starting point for commercially pure titanium welding where the procedure, base metal grade, and service conditions support that choice. It is not a substitute for WPS review or manufacturer data. Before you load a rod, confirm what the base material actually is, what the code allows, and whether the service environment calls for a different titanium filler.

    This draft is focused on selection and compatibility checks. The practical issue is not just whether the rod is labeled ERTi-2, but whether it matches the job after you verify the base metal, joint condition, shielding plan, and cleanliness standard.

    Key Takeaways

    • Use ERTi-2 only after confirming the base metal grade and WPS.
    • Commercially pure titanium applications need tight control of contamination, shielding, and heat input.
    • Do not assume a filler grade is acceptable for every CP titanium repair or fabrication job.
    • Manufacturer data sheet review is still required before order release or weld start.
    • If a detail is not confirmed, mark it as Unknown (Verify) and stop until it is checked.

    What the ERTi-2 designation means for the shop

    The provided filler metal record identifies this item as ERTi-2 for TIG / GTAW use, with an AWS A5.16 reference and a base material description of commercially pure titanium Grade 2. That gives you a useful starting point, but not final approval for any job.

    For titanium work, the filler selection normally depends on the exact base metal, the joint design, the service environment, and the governing procedure. If any of those inputs are missing, treat compatibility as Unknown (Verify) until the WPS, code requirements, or manufacturer literature confirms the match.

    Selection checks before you order rod

    Use the following checks before releasing ERTi-2 to the floor:

    1. Check the base metal identification. Verify the heat number, mill cert, or purchase record. If the base metal is only described as CP titanium, stop and confirm the grade. If the grade is not established, compatibility remains Unknown (Verify).
    2. Inspect the WPS. Confirm the procedure calls for ERTi-2 or equivalent filler for the exact joint and service condition.
    3. Verify code or customer requirements. Some jobs control filler selection by specification, qualification record, or purchaser note. Do not rely on generic material family matching.
    4. Inspect the joint condition. Titanium requires clean, oxide-free, contamination-free surfaces. Oil, marker residue, abrasive dust, and moisture can become weld defects.
    5. Verify shielding strategy. Confirm primary shielding, trailing coverage if required, purge requirements if applicable, and gas quality before welding starts.

    Troubleshooting and support checks

    If the job is already in motion and the welds are not meeting expectations, work through the issue in a controlled order.

    1) If the arc starts poorly or the bead looks unstable

    • Inspect the tungsten condition, cup setup, and gas delivery.
    • Check for drafts, loose hoses, or inadequate coverage.
    • Verify that the filler rod is dry, clean, and not contaminated by shop handling.

    2) If the weld surface discolors excessively

    • Inspect the shield coverage at the weld pool and trailing edge.
    • Check travel speed and heat input against the WPS.
    • Verify that the purge and torch shielding remain in place until the joint cools enough for the procedure requirements.

    3) If the filler does not appear to match the job requirement

    • Inspect the material traceability documents.
    • Check whether the base metal is truly Grade 2 CP titanium or another titanium grade.
    • Verify with the manufacturer data sheet and the approved procedure before continuing.

    WSP lookup and filler metal finder

    Use the filler metal record as a starting point for selection review:

    ERTi-2 TIG / GTAW Filler Metal

    Use the finder page when you need to cross-check the filler family against other listed options and confirm whether the job should stay with ERTi-2 or move to another approved material:

    WSP Filler Metal Finder

    These pages support selection. They do not replace the WPS, code review, or manufacturer data sheet.

    Practical shop handling points

    Titanium filler handling is a contamination control task. Keep the rod package closed until needed. Store rods so they are not exposed to dirt, moisture, grinding debris, or mixed-metal contact. If a rod has dropped to an unclean floor or has visible contamination, treat it as Unknown (Verify) until it is cleaned or replaced according to shop practice and procedure requirements.

    During setup, confirm the following before striking an arc:

    • Base metal identity is confirmed.
    • Filler designation is confirmed.
    • Gas supply is verified and suitable for the procedure.
    • Joint surfaces are clean and ready.
    • Operator knows the cooling and shielding requirements.

    Safety notes

    Titanium welding is sensitive to contamination and shielding failure. Do not improvise filler choice on critical work. Do not assume CP titanium grades are interchangeable. Do not weld over questionable surface contamination. If the procedure, service condition, or material grade is unclear, stop and verify before welding.

    Use standard welding PPE, keep the work area clean, and maintain gas safety and cylinder handling practices. If a weld shows unusual discoloration, cracking, or surface contamination, quarantine the part for review rather than passing it to inspection without a documented decision.

    FAQ

    Is ERTi-2 always correct for commercially pure titanium?

    No. It is a starting point for CP titanium applications, but final selection depends on the WPS, the exact base metal grade, and service requirements. If any of those are unconfirmed, the compatibility is Unknown (Verify).

    Can I use ERTi-2 if the base metal is only labeled titanium?

    Not without more information. You need the actual grade, traceability, or approved procedure. “Titanium” alone is not enough to confirm filler compatibility.

    Do I need to check the manufacturer data sheet if the listing already says ERTi-2?

    Yes. The listing is a reference point, not final approval. Verify the data sheet, the WPS, and any customer or code requirements before welding or purchasing.

    What should I do if the weld color looks off?

    Stop and inspect shielding, purge, cleanliness, and heat input. Discoloration on titanium often points to coverage or contamination issues. Verify the procedure before continuing.

    Sources Checked

    • ERTi-2 TIG / GTAW Filler Metal: https://www.weldsupportparts.com/filler-metal-tig-erti-2.html
    • WSP Filler Metal Finder: https://www.weldsupportparts.com/filler-metal-finder.html
    • Provided filler metal summary for ERTi-2 TIG / GTAW filler metal

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • ERCuNi TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuNi TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuNi TIG / GTAW Filler Metal

    ERCuNi TIG / GTAW filler metal is used on copper-nickel work where the joint design, service environment, and procedure call for a copper-nickel filler rather than a general-purpose bronze or nickel alloy. For maintenance buyers and welders, the main risk is assuming the rod name alone is enough. It is not. Selection has to follow the WPS, the base metal grade, the service conditions, and the manufacturer data sheet.

    Use this page as a starting point for compatibility checks only. Before ordering or welding, verify the exact joint requirements and confirm the filler against the procedure and governing code. If any of those inputs are unclear, stop and resolve them first.

    Key Takeaways

    • ERCuNi is a filler selection starting point, not automatic approval for every copper-nickel job.
    • Confirm the base metal grade before matching filler to the joint.
    • Check the WPS, service environment, and corrosion requirements before release to weld.
    • Do not assume a rod labeled for copper-nickel will fit every 70/30 or 90/10 application without review.
    • When technical details are uncertain, use Unknown (Verify) rather than guessing.

    What ERCuNi is used for in practice

    The allowed filler metal page identifies ERCuNi as a TIG / GTAW filler for copper-nickel alloys and related applications. That makes it relevant where the work involves copper-nickel piping, tube, or fabrications that call for this classification. The page also points to common diameter references and brand names, but those details still need to be checked against the actual job package and supplier data sheet.

    For shop use, treat the filler metal page as a quick reference, not a procedure substitute. It helps narrow the field, but it does not confirm the WPS, the exact alloy compatibility, or whether the weld is intended for corrosion service, seawater service, or another duty. Those are job-specific decisions.

    Check the job before you select the rod

    Start with the base metal. Identify the copper-nickel grade from the drawing, MTR, or vessel/piping documentation. If the alloy is not clearly defined, mark it as Unknown (Verify). Do not rely on appearance alone. Copper-nickel alloys can be misidentified in maintenance work, especially after service exposure, coating, or repair prep.

    Next, check the WPS. Verify that the procedure actually permits ERCuNi for the joint. Confirm any limits on base material, thickness, welding position, backing, heat input, and shielding gas. If the WPS references a specific classification or alternate filler family, follow that document. The filler rod choice must match the procedure, not the other way around.

    Then verify service conditions. Copper-nickel joints can be sensitive to the intended environment, especially where corrosion resistance is a key requirement. If the weld will see marine exposure, process fluid contact, or elevated temperature service, make sure the filler selection is still acceptable for that duty. If the service requirement is not clearly documented, treat it as Unknown (Verify).

    Troubleshooting and support checks

    If the filler metal seems right but the job still does not line up, use this sequence:

    1. Check the base metal identification. Confirm the alloy grade from paperwork or positive identification. If you cannot verify it, stop and escalate.
    2. Inspect the WPS. Verify the exact filler classification, process, and essential variables. Make sure the procedure has not been superseded.
    3. Verify the service requirement. Confirm whether the weld is for general fabrication, corrosion service, or another controlled application.
    4. Inspect the rod condition. Look for contamination, moisture, damaged packaging, or mix-up with another alloy.
    5. Verify the shielding setup. GTAW shielding gas, cup selection, tungsten prep, and arc stability all affect the weld outcome. If the gas setup is uncertain, use Unknown (Verify) until confirmed.

    If weld quality problems show up after setup, do not assume the rod is the root cause. Check for contamination, poor joint cleaning, incorrect fit-up, and wrong procedure settings first. For general TIG support on arc stability and tungsten condition, see the related guide on TIG tungsten contamination troubleshooting. For gas shielding and stickout control on cup selection, see the Square Wave 205 TIG cup size selection guide.

    Use the filler metal page as a starting point

    The ERCuNi filler metal page at https://www.weldsupportparts.com/filler-metal-tig-ercuni.html is the right place to begin a selection review. It identifies the process as TIG / GTAW, the classification as ERCuNi, the AWS specification as AWS A5.7, and the intended base material family as copper-nickel alloys. It also lists common search terms that may help narrow down a stock match.

    Use the filler metal finder when you need to compare options across filler families or confirm the route to a better match. That page is also a starting point only. It does not replace the WPS, the code requirement, or the manufacturer data sheet.

    If the filler name on the job ticket does not match the procedure, do not substitute based on naming similarity. ERCuNi, ERNiCu-7, and other copper-based filler families are not interchangeable without verification. If the selection is unclear, tag it Unknown (Verify) and route it through the welding engineer or responsible supervisor.

    Practical shop checks before release

    • Check the base metal grade against the drawing or MTR.
    • Inspect the WPS for permitted filler classification and process.
    • Verify the service environment and corrosion requirement.
    • Confirm rod size from the job package or manufacturer data sheet.
    • Inspect packaging for damage, contamination, or shelf exposure.
    • Confirm shielding gas, cup, tungsten, and joint prep before arc start.

    Safety notes

    Do not weld from assumptions. Copper-nickel work can carry process and service requirements that are not visible at the joint. Follow the site hot-work controls, ventilation requirements, and PPE rules. Keep filler metals clean and dry. If the alloy, service condition, or procedure requirement is uncertain, stop and verify before use.

    Grinding, cleaning, and surface prep can also expose residue or contamination from prior service. Treat unknown residues as a hazard until identified. If the joint has been in corrosive or marine service, verify cleaning and handling requirements before fit-up.

    FAQ

    Is ERCuNi always correct for 70/30 copper-nickel?

    No. ERCuNi may be a common starting point, but the correct choice depends on the WPS, the base metal grade, and the service condition. Verify the procedure before welding.

    Can I use the filler metal page as approval to weld?

    No. The filler metal page is a selection starting point only. It does not replace the WPS, code requirements, or manufacturer data sheet.

    What if the base metal is not clearly identified?

    Mark it Unknown (Verify). Do not guess the alloy. Confirm the material from documentation or approved identification methods before selecting the filler.

    Are ERCuNi and ERNiCu-7 interchangeable?

    Not by default. They are different filler families and should only be used when the WPS and supporting technical documents allow it. Verify compatibility before release.

    Sources Checked

    Metadata note: if the exact rod size, brand approval, or compatibility detail is not confirmed in the job packet or manufacturer data sheet, use Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32″): Application and Buying Checks

    TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32″): Application and Buying Checks

    “>TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32")

    A TIG gas lens collet body is a small part, but it controls two things that matter: tungsten retention and shielding gas flow. When the collet body is the wrong size, worn, or clogged, the torch can still arc, but the setup becomes harder to control. For buyers and maintenance teams, the main job is not to guess. It is to verify torch series, tungsten size, and the condition of the existing consumables before ordering.

    The TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32″) is listed as a standard size gas lens collet body for TIG torch #17, #18, and #26. The critical buying point is the 3/32 in. tungsten size in the part title. If your torch, cup, collet, or back-end hardware does not match that setup, stop and verify before purchase.

    Key Takeaways

    • Confirm torch series first: #17, #18, or #26.
    • Confirm tungsten diameter: 3/32 in. on this part title.
    • Inspect the current collet body for burn marks, thread damage, gas passage blockage, and slip-related wear.
    • Do not assume all gas lens parts interchange across every TIG torch variant.
    • Use the torch manual and existing consumable stack as the final check, not memory.

    What This Part Does

    A gas lens collet body holds the collet and tungsten in the torch head and supports shielding gas distribution through the lens assembly. In normal service, the part should clamp the tungsten securely, support consistent gas coverage, and let the operator maintain a stable arc without tungsten movement. If the collet body is worn, the tungsten may slip, gas coverage may become uneven, or the torch may feel inconsistent from one setup to the next.

    For general troubleshooting on wear patterns, see TIG Torch Slipping Tungsten? Your Collet Body Is Worn (Here’s the Fix) and TIG Torch Consumable Wear Signs: Cup Cracks, Collet Slip, Gas Lens Clogs, and Dirty Tungsten.

    Application and Fitment Checks

    Before ordering, check the torch and the current hardware in the hand. Do not rely only on the torch body label if the torch has been rebuilt or mixed with aftermarket consumables.

    Check

    • Check the torch series marking or manual: #17, #18, or #26.
    • Check the tungsten size currently used: 3/32 in. or Unknown (Verify).
    • Check whether the torch is built around a gas lens stack or a standard collet setup.
    • Check the cup, collet, and back cap for matching wear patterns or mixed parts.

    Inspect

    • Inspect the existing collet body threads for galling, rounding, or heat distortion.
    • Inspect the gas lens screen or passage for clogging, soot, or spatter contamination.
    • Inspect the tungsten seating surface for slip marks or deformation.
    • Inspect the cup fit. If the cup feels loose or bottoms oddly, the stack may be mismatched.

    Verify

    • Verify the replacement part title matches the torch series and tungsten size you actually use.
    • Verify the collet body style matches the rest of the consumable stack already on the torch.
    • Verify gas flow path cleanliness before blaming the torch body for poor shielding.
    • Verify the machine settings and gas delivery are correct before replacing parts unnecessarily.

    Buying Checks for Maintenance Teams

    For stocked consumables, the safest approach is to compare the failed part with the replacement before issuing it to production. A part can look close and still be wrong in the details that matter. If the torch is a repair item coming in from the floor, tag it with the torch series, tungsten size, and any cup or back-cap part numbers that were on the assembly.

    When reviewing an order, confirm the following:

    • Torch family: #17, #18, or #26.
    • Tungsten size: 3/32 in. for this listed part.
    • Gas lens requirement: Only buy gas lens hardware when the torch setup is designed for it.
    • Current consumable stack: Unknown (Verify) if the torch has mixed components or no part markings.

    If your team keeps alternative consumable families on hand, label bins clearly. Do not mix standard collet bodies and gas lens collet bodies in the same tray unless they are separated by torch series and tungsten size.

    Support Note: Related Torch Buying Review

    If you are also replacing the torch or the lead assembly, review the torch kit article here: Rocker R-17FV-25R TIG Torch Kit Review & Buying Guide (180A, Flex-Head, Valve, 25′ Rubber). Use it as a support reference only. Do not assume the torch kit and this collet body share the same exact consumable stack without checking the actual hardware.

    Safety Notes

    • Shut down the welding power source before disassembly.
    • Let the torch cool before handling burned or discolored consumables.
    • Do not force a tungsten or collet into a damaged body.
    • Replace contaminated parts if they cannot be cleaned back to a reliable condition.
    • Use eye protection when disassembling hot or spattered torch components.

    FAQ

    Is this collet body only for #17, #18, and #26 torches?

    The part title lists #17, #18, and #26 torch compatibility. If your torch is a different series, verify the manual or the existing consumables before ordering. Unknown (Verify) for any other torch family.

    Does the 45V26-3/32″ title mean it is for 3/32 in. tungsten?

    Yes, the part title indicates 3/32 in. tungsten size. Still verify the complete consumable stack on your torch, especially if the machine has been rebuilt or mixed with non-original parts.

    How do I know if my old collet body is worn out?

    Look for tungsten slip, rough threads, heat damage, clogged gas passages, or inconsistent shielding behavior. If the torch runs better after replacing the collet body, the old part was likely the problem. For a deeper wear checklist, use the consumable wear signs article linked above.

    Can I use this part if my gas lens setup is not confirmed?

    Do not assume. Confirm whether your torch is built for a gas lens assembly. If that is unclear, inspect the current hardware and verify the part stack before purchase.

    Sources Checked

    Final check: match the torch series, confirm 3/32 in. tungsten sizing, and inspect the existing consumable stack before placing the order. If any of those details are unclear, mark them Unknown (Verify) and verify from the torch itself or the manual before buying.

    Related Arc Weld Part

    TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32")

    TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V26-3/32")

    Standard Size Gas Lens Collet Body for TIG torch #17, 18, 26

    View at Arc Weld Store

    Related Weld Support Guides

  • ERCuAl-A2 TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuAl-A2 TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuAl-A2 TIG / GTAW Filler Metal

    ERCuAl-A2 is a TIG/GTAW filler metal used in copper and bronze repair, overlay, and buildup work where aluminum bronze chemistry is the right fit. It is not a general-purpose rod. Before you order wire or strike an arc, confirm the base metal, the service condition, and the welding procedure requirements. The wrong match can create cracking, dilution problems, or a repair that will not hold up in service.

    This draft focuses on selection checks and compatibility verification for ERCuAl-A2 TIG / GTAW filler metal. Use it as a starting point only. Confirm the WPS, code requirements, base metal grade, and manufacturer data sheet before welding.

    Key Takeaways

    • ERCuAl-A2 is for aluminum bronze and related overlay work, not for every copper alloy job.
    • Verify the exact base metal grade before selecting the filler.
    • Check whether the repair is a deposit, a buildup, or a joining weld; the service duty changes the filler choice.
    • Do not assume compatibility from color, appearance, or old shop habits.
    • Use the WPS and the filler manufacturer data sheet as the final authority.

    Start With the Base Metal

    The first compatibility check is the parent metal. ERCuAl-A2 is associated with aluminum bronze and overlay work, but the exact fit depends on the alloy family and the service requirements. If the base metal is unknown, identify it before you weld. If the part has a casting number, mill cert, or in-house repair record, review that data first. If not, use positive material identification, shop records, or a qualified lab method as required by your procedure.

    Check: Is the base metal aluminum bronze, a copper alloy, or something else? If the alloy is unknown, mark it as Unknown (Verify) and do not assume ERCuAl-A2 is correct.

    Inspect: Look for previous repair welds, mixed-alloy sections, corrosion products, and wear patterns. These clues can change the deposit requirement.

    Verify: Confirm the alloy family against the WPS and the manufacturer’s filler data sheet. If the procedure does not list the base metal, stop and get approval.

    Match the Service Condition

    Aluminum bronze filler is often considered for wear and corrosion overlays, but service conditions drive the final decision. A filler that works for one environment may fail in another. Temperature, abrasion, seawater exposure, chemical contact, impact, and galvanic pairing all matter. If the part runs hot, sees sliding wear, or sits in a corrosive environment, review whether the deposit chemistry and hardness range are suitable. If those details are not listed in the available data, treat them as Unknown (Verify).

    Check: Is the job repair, buildup, surfacing, or joining? Different duties can require different filler metal selection.

    Inspect: Review wear direction, crack location, and corrosion pattern. These details tell you whether you need a ductile deposit, a harder overlay, or a different repair method.

    Verify: Confirm with the WPS or engineering note that ERCuAl-A2 is approved for the service environment.

    Review the Welding Procedure Before You Order Rod

    Do not buy filler metal first and hope it fits the procedure later. The WPS controls what you can use. Check the base metal range, joint type, preheat requirements, interpass limits, shielding gas, polarity, and any postweld requirements. If the WPS is missing, outdated, or written for a different alloy family, stop and get it corrected.

    Check: Does the WPS specifically allow ERCuAl-A2 or an equivalent filler classification?

    Inspect: Confirm whether the weld is governed by code, internal repair practice, or OEM instruction.

    Verify: Match the rod diameter, process, and technique to the procedure. If rod size is not stated, use Unknown (Verify) until the document is reviewed.

    Use the WSP Filler Metal Finder as a Starting Point

    The WSP filler metal finder can help narrow the selection, but it does not replace procedure approval. Use it to compare classification, process, and intended application, then cross-check the result with the WPS and the base metal data.

    Open the WSP filler metal finder and compare ERCuAl-A2 against the job requirements. Treat the finder as a selection aid, not a guarantee that the filler is approved for your part or code.

    Check: Does the finder entry align with your process, material family, and repair intent?

    Inspect: Look for any mismatch between the finder result and the procedure sheet.

    Verify: If the finder suggests alternatives, confirm those alternatives before changing wire.

    Review the ERCuAl-A2 Filler Page

    The ERCuAl-A2 filler page is another starting point for selection. It identifies the product family as TIG/GTAW filler metal for aluminum bronze and overlay work, with AWS A5.7 referenced on the page. That is useful, but it is not the same as weld approval. Final compatibility still depends on the WPS, the base metal grade, and the service conditions.

    Open the ERCuAl-A2 filler metal page and compare the page details with your repair requirement. Use it to confirm the classification and general application only. Do not treat it as automatic approval for a specific job.

    Check: Does the page description match aluminum bronze and overlay work?

    Inspect: Compare the page information with the filler data sheet from the manufacturer.

    Verify: If the exact rod diameter, package size, or manufacturer is needed, use Unknown (Verify) until the actual item and datasheet are confirmed.

    Practical Setup Checks Before Welding

    Compatibility is not only about chemistry. TIG/GTAW setup affects the result. Clean the joint, remove oxides, and control fit-up. Use a clean tungsten, correct gas coverage, and stable torch technique. If the part shows porosity, arc wandering, or contamination, stop and correct the setup rather than continuing to add filler.

    Check: Is the joint free of grease, oxide, paint, and embedded debris?

    Inspect: Confirm torch angle, shielding coverage, and work lead placement.

    Verify: If contamination appears, re-clean and re-check the tungsten before restarting. For related TIG setup issues, see TIG Tungsten Contamination Troubleshooting and Square Wave 205 TIG Arc Wandering Causes.

    Safety Notes

    • Review the SDS and manufacturer instructions before use.
    • Use fume control and local exhaust ventilation.
    • Wear eye, hand, and skin protection suitable for hot metal and arc exposure.
    • Do not weld on unknown alloys until the material and procedure are verified.
    • Follow hot-work, confined-space, and lockout rules where applicable.

    FAQ

    Is ERCuAl-A2 a universal bronze filler?
    No. It is a specific TIG/GTAW filler metal for aluminum bronze and overlay work. Confirm the base metal and procedure before using it.

    Can I choose ERCuAl-A2 based on the part color or previous repair history?
    No. Visual clues are not enough. Verify the alloy family and service condition first.

    Does the WSP filler metal finder approve the weld?
    No. It is a selection aid only. Final approval comes from the WPS, code requirements, and manufacturer data.

    What if the base metal grade is not known?
    Mark it as Unknown (Verify) and identify it before welding. Do not assume ERCuAl-A2 is correct.

    Sources Checked

    For ERCuAl-A2 TIG / GTAW filler metal selection, the order of work is simple: identify the base metal, confirm the service duty, verify the WPS, then cross-check the filler page and data sheet. If any step is unclear, stop and mark the detail as Unknown (Verify) until it is proven.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8″): Application and Buying Checks

    TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8″): Application and Buying Checks

    “>TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8")

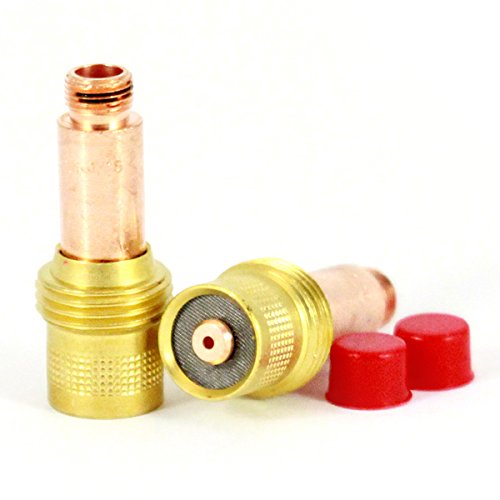
    Gas lens collet bodies are small parts, but they control a lot of TIG torch performance. If the fit is wrong, the tungsten may slip, shielding gas flow can be uneven, and the arc can become harder to manage. For buyers and maintenance teams, the main job is not just to order a replacement. It is to confirm the torch family, thread or consumable style, and the wear condition before parts are pulled from stock or installed.

    The TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8″) is listed as a standard size gas lens collet body for TIG torch #17, #18, and #26. Beyond that, any deeper fitment detail should be treated as Unknown (Verify) unless it is confirmed in the torch and consumable documentation you are using.

    Key Takeaways

    • Confirm the torch model before ordering. Do not assume all #17, #18, and #26 setups use the same consumables in every torch configuration.
    • Check the tungsten retention parts for wear if the tungsten slips, arcs wander, or the cup area looks damaged.
    • Verify the gas lens style, thread/series match, and cup compatibility before installation.
    • Use replacement as a controlled maintenance step, not just a cleanup task after arc problems appear.
    • If any compatibility point is uncertain, mark it Unknown (Verify) and confirm against the torch manual or the supplier listing.

    Where this part fits in the torch

    A gas lens collet body supports the tungsten and helps shape shielding gas flow through the front end of the torch. In practice, it is part of the consumable stack that includes the collet, cup or cup adapter, and tungsten. When the collet body is worn, dirty, or the wrong style, you may see inconsistent gas coverage, difficulty holding tungsten position, or an unstable arc.

    For this item, the title indicates use with torch sizes #17, #18, and #26. That is the first check. The second check is whether your torch uses the same consumable family as the part you are buying. If your shop keeps mixed torch brands or mixed front-end setups, do not rely on torch size alone. Verify the series from the torch body, the old consumable, or the parts sheet.

    Buying checks before you place the order

    Use the steps below before you approve purchase or pull from stock:

    1. Check the torch model. Read the torch tag, handle marking, or parts breakdown. Confirm it is a #17, #18, or #26 torch family.
    2. Inspect the current front end. Remove the cup and look at the collet body for heat discoloration, thread damage, cracks, or contamination.
    3. Verify the consumable series. Match the old part to the new part. If the old item is worn beyond legible markings, compare dimensions and thread style to the supplier description.
    4. Check tungsten size and setup. The tungsten diameter and collet size must match the torch setup. If that match is uncertain, mark it Unknown (Verify).
    5. Confirm gas lens versus standard collet body. This article is about a gas lens style. Do not substitute a standard collet body unless the torch setup is designed for it.
    6. Check stock handling. Keep consumables clean, dry, and separated by torch series so front-end parts are not mixed during issue.

    Troubleshooting: signs the collet body needs attention

    If TIG performance has changed, inspect the collet body before replacing other parts at random. Common clues include tungsten slip, poor gas coverage, black soot near the cup, or repeated arc wandering. Those symptoms can also come from contaminated tungsten, poor gas supply, a damaged cup, or loose assembly. Do not assume the collet body is the only fault.

    Check: Remove the consumables and look for carbon, spatter, or grinding dust in the gas path.

    Inspect: Examine the collet body threads and contact surfaces for deformation, wear, or cross-threading.

    Verify: Confirm that the collet, cup, and tungsten are assembled in the correct stack and tightened to normal shop practice. If the part style is unclear, stop and verify against the torch documentation.

    Installation and support checks

    When installing a new collet body, keep the work clean. Metal chips, lubricant, and abrasive dust can all affect front-end performance. Use a clean bench or a clean tray. Do not force threads. If the part does not start smoothly by hand, back out and verify the match rather than tightening through resistance.

    After installation:

    • Check that the tungsten seats straight and does not rotate or slip under normal handling.
    • Inspect the cup interface for gaps, damage, or misalignment.
    • Verify gas flow at the torch before welding on production work.

    Related support reading

    For more on front-end wear, see TIG Torch Slipping Tungsten? Your Collet Body Is Worn (Here’s the Fix) and TIG Torch Consumable Wear Signs: Cup Cracks, Collet Slip, Gas Lens Clogs, and Dirty Tungsten. If you are evaluating a complete torch setup, the Rocker R-17FV-25R guide may help with general torch support context: Rocker R-17FV-25R TIG Torch Kit Review & Buying Guide (180A, Flex-Head, Valve, 25′ Rubber).

    Safety notes

    • Depressurize and isolate the torch/gas system before removing front-end parts.
    • Let hot consumables cool before handling.
    • Do not use damaged threads or cracked consumables in service.
    • Keep tungsten and consumables clean; contamination can affect arc stability and weld quality.
    • If the torch setup is unfamiliar, verify the parts breakdown before energizing the system.

    FAQ

    Q: Is this collet body automatically correct for every #17, #18, and #26 torch?
    A: No. The title indicates those torch families, but you still need to verify the exact torch series and consumable stack used on your setup.

    Q: What are the main signs of a worn gas lens collet body?
    A: Tungsten slip, unstable arc behavior, poor shielding gas coverage, thread damage, and visible contamination in the front end are common signs. Other causes are possible, so inspect the full setup.

    Q: Can I swap in a standard collet body instead of a gas lens collet body?
    A: Not by assumption. Gas lens and standard front-end parts are not interchangeable in every setup. Verify the torch and cup configuration first.

    Q: What should I do if I cannot confirm compatibility?
    A: Treat the part as Unknown (Verify) until you match it against the torch parts breakdown, the removed consumable, or supplier documentation.

    Sources Checked

    • ArcWeld product page: TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8″)
    • Internal support articles on TIG consumable wear and collet body troubleshooting

    Related Arc Weld Part

    TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8")

    TIG Gas Lens Collet Body #17, 18, 26 Torch 2PK (45V27-1/8")

    Standard Size Gas Lens Collet Body for TIG torch #17, 18, 26

    View at Arc Weld Store

    Related Weld Support Guides

  • ERCuSn-A TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuSn-A TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuSn-A TIG / GTAW Filler Metal

    ERCuSn-A TIG / GTAW filler metal is a starting point for phosphor bronze and copper-alloy repair and fabrication work. It is not a stand-alone approval to weld. Before you order rod or strike an arc, verify the WPS, code requirements, base metal grade, service conditions, and the manufacturer data sheet. If any of those inputs are unclear, stop and confirm them first.

    This matters because bronze and copper-alloy jobs often look similar at the bench but behave differently in service. A filler that seems reasonable for one component can be wrong for another if the part sees wear, pressure, corrosive exposure, seawater, elevated temperature, or load-bearing service. Use the filler metal page as a selection starting point only.

    Key Takeaways

    • ERCuSn-A is a selection starting point, not a procedure approval.
    • Verify the base metal family before matching filler to joint.
    • Check service conditions before welding bronze or copper alloys.
    • Confirm the WPS, code requirement, and manufacturer data sheet before use.
    • If compatibility is uncertain, document it as Unknown (Verify) and escalate.

    What ERCuSn-A is used for

    ERCuSn-A is listed on the Weld Support Parts filler metal page as a TIG / GTAW option for phosphor bronze and copper-alloy applications. That description is useful for narrowing the search, but it does not tell you whether the rod is approved for your job. The final decision belongs to the governing procedure, drawing, code, or OEM repair instruction.

    For the source listing, review the filler metal page here: ERCuSn-A TIG / GTAW Filler Metal. Use the page as a reference point only. Confirm the base metal, diameter, and service requirement before ordering or welding.

    Check the job before you choose the rod

    Start with the part itself. Many compatibility errors happen because the base metal is assumed instead of verified.

    • Check the part drawing, BOM, or maintenance record for the base metal grade.
    • Inspect the failed part, if available, for color, wear pattern, and prior repair evidence.
    • Verify whether the component is phosphor bronze, copper alloy, or another bronze family. If the grade is not confirmed, record it as Unknown (Verify).
    • Check whether the joint is a repair, buildup, fillet, overlay, or fit-up weld. Different geometries create different dilution and heat-input concerns.
    • Verify whether the service includes corrosion exposure, seawater, electrical conductivity requirements, or sliding wear. Those conditions can change filler selection.

    Compatibility checks at the bench

    Before setup, compare the rod choice against the WPS and available documentation. Do not rely on memory or on a similar part that was welded in the past.

    • Check the WPS for the allowed filler classification.
    • Inspect the manufacturer data sheet for the filler metal family and any stated limitations.
    • Verify whether the code or job spec allows ERCuSn-A for the specific application.
    • Check whether alternate fillers are listed, such as ERCuSi-A, only if the procedure or spec names them. Do not substitute by assumption.
    • Verify rod diameter against joint access, heat input, and bead placement needs. Common sizes may exist, but any specific size for your job is Unknown (Verify) unless documented.

    Procedure support: what to inspect before welding

    Bronze and copper-alloy work is sensitive to contamination, fit-up, and heat control. A good filler cannot compensate for poor prep.

    • Inspect the joint for oil, oxide, paint, corrosion, and embedded dirt.
    • Check that the joint faces are bright and mechanically clean where required by the procedure.
    • Verify clamp stability and heat-sink needs before starting.
    • Check torch gas coverage and cup setup if your weld access is tight. For related setup guidance, review the Square Wave 205 TIG Cup Size Selection Guide.
    • Inspect tungsten condition and grind quality. Contamination problems can create arc instability that looks like a filler issue. See TIG Tungsten Contamination Troubleshooting.

    WSP lookup and cross-check workflow

    If your internal purchasing or support process includes a Weld Support Parts lookup step, use it to confirm the current listing and related guidance before release to the floor. For this topic, the allowed filler metal source page is the primary reference. When a WSP lookup page is available in your workflow, compare the lookup result against the filler listing and the job documentation. If there is a mismatch, stop and investigate. If no lookup page is provided, note that as Unknown (Verify) and proceed only after the responsible engineer or supervisor confirms the selection.

    Use the filler metal finder here as a starting point for narrowing the choice: WSP Filler Metal Finder. It helps direct the search, but it does not approve a procedure, a code case, or a repair plan.

    Field troubleshooting when ERCuSn-A is being considered

    If the part has already failed once, the wrong filler may not be the only issue. Work through the job in sequence.

    • Check whether the original failure was caused by overload, corrosion, wear, or poor fit-up.
    • Inspect the fracture surface and heat-affected area for signs of previous contamination or overheating.
    • Verify that the repair method matches the duty cycle. A cosmetic repair is not the same as a structural or wear repair.
    • Check whether preheat or interpass controls are specified. If not specified, do not assume values; mark them Unknown (Verify).
    • Verify final acceptance criteria before post-weld cleanup and return to service.

    Safety notes

    • Use normal TIG/GTAW PPE, including eye protection, gloves, and skin coverage.
    • Control fumes, especially in confined areas or on contaminated bronze/copper components.
    • Do not weld unknown materials until the base metal is identified.
    • Do not substitute filler based on color, habit, or availability alone.
    • If the job is safety-critical, stop and verify approval before welding.

    FAQ

    Q: Is ERCuSn-A automatically correct for any bronze repair?
    A: No. It is only a starting point. Confirm the base metal, the WPS, and the service condition before use.

    Q: Can I swap in a similar bronze filler if ERCuSn-A is unavailable?
    A: Not without procedure approval. If the filler is not named on the WPS or job spec, treat the substitute as Unknown (Verify) until it is approved.

    Q: What should I check first on a copper-alloy repair job?
    A: Check the base metal identification, then inspect the joint for contamination, then verify the WPS and service requirements.

    Q: Does the filler metal page guarantee code compliance?
    A: No. The filler page is a selection guide, not a code or procedure approval.

    Sources Checked

    Before release to production, verify the job against the current WPS and the manufacturer data sheet. If any input is missing, document it as Unknown (Verify) and hold the work until it is confirmed.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • ERCuSi-A TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuSi-A TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCuSi-A TIG / GTAW Filler Metal

    ERCuSi-A TIG / GTAW filler metal is a common starting point for silicon bronze braze-welding and certain copper-alloy applications. It is often selected when the job calls for lower base-metal dilution, improved cosmetic appearance, or joining sheet metal with controlled heat input. That said, the filler metal name alone does not make it a qualified choice. The weld support team still needs to verify the WPS, the base metal, the service environment, and the manufacturer data sheet before the first arc starts.

    This guide is for selection checks, not procedure approval. If the material, joint design, or service condition is uncertain, stop and verify before welding.

    Key Takeaways

    • ERCuSi-A is a starting point for silicon bronze TIG/GTAW work, not a blanket approval for every copper or sheet metal job.
    • Check the WPS first. If no WPS exists, verify whether the job requires one and whether ERCuSi-A is permitted.
    • Confirm base metal grade, thickness, and service conditions before selecting wire size or travel plan.
    • Use the filler metal finder and manufacturer data sheet to confirm the intended use, not just the classification name.
    • For uncertain compatibility, mark the detail as Unknown (Verify) and route it for review.

    Where ERCuSi-A Fits

    ERCuSi-A is typically associated with silicon bronze filler selection for TIG/GTAW. In support work, it is often evaluated for braze-welding, sheet metal repair, cosmetic build-up, and compatible copper-alloy work. The practical benefit is usually lower heat input than a fusion weld on thin or sensitive base metal. That does not mean it is suitable for every repair. Joint design, fit-up, corrosion exposure, fatigue loading, and post-weld requirements can change the decision.

    If the base metal is not clearly identified, treat it as Unknown (Verify). Do not assume a bronze filler is acceptable just because the material looks similar to copper or brass.

    Check the WPS Before You Select Wire

    Start with the welding procedure specification if one exists. The WPS should define whether the job allows braze-welding, which filler metal classifications are approved, and whether any preheat, shielding gas, or joint limits apply. If the WPS is missing, incomplete, or outdated, stop and verify before ordering wire or setting up the torch.

    Check:

    • WPS number, revision, and job scope
    • Approved filler metal classification
    • Base metal group and thickness range
    • Required shielding gas and process limits
    • Any code or customer restrictions

    Inspect: the joint area for contamination, paint, plating, oxide buildup, oil, and moisture. Silicon bronze work is sensitive to surface condition. Dirty edges can give poor wetting, unstable arc behavior, or weak cosmetic results.

    Verify: whether the repair is structural, cosmetic, or service-critical. If the repair carries load, pressure, or corrosion exposure, the filler choice may require formal approval. Unknown (Verify) is the correct status until that review is complete.

    Base Metal Compatibility Checks

    ERCuSi-A is not a universal match for all copper alloys or all mixed-metal joints. The support team should confirm the actual base metal grade before proceeding. That includes checking whether the part is copper, brass, bronze, or a coated steel assembly. If the part was previously repaired, identify the existing filler if possible. Mixed chemistry can change wetting behavior and service performance.

    Check:

    • Base metal identification from print, mill cert, tag, or site record
    • Thickness and heat sensitivity
    • Whether dissimilar metal joining is involved
    • Whether the application is decorative, low-load, or service-critical

    Inspect: edges and joint fit-up. Large gaps may push the repair outside the intended use of the filler. If fit-up is inconsistent, verify whether build-up or backing is needed, or whether the repair should be reworked before welding.

    Verify: the service temperature, corrosion exposure, and any downstream finishing steps. A filler that wets well during welding may still be the wrong choice if the assembly sees chemicals, high wear, or code-controlled service.

    Filler Metal Finder as a Selection Starting Point

    Use the WSP filler metal finder as a selection starting point only. It can help narrow the search by process, classification, or base-material family, but it does not replace the WPS or manufacturer data sheet. If the finder suggests ERCuSi-A for the job, treat that as a lead to review, not a final approval.

    When comparing options, confirm whether the application needs silicon bronze, a different copper-alloy filler, or another repair method entirely. If the part is aluminum, steel, stainless, cast iron, or an unknown alloy, do not assume ERCuSi-A is appropriate. Mark the fit as Unknown (Verify) until the compatibility question is resolved.

    Practical Setup and Handling Checks

    Before welding, check the wire condition and setup. Filler rod should be clean, dry, and free of heavy oxidation or contamination. Keep rods separated from steel grinding dust, oil, and shop debris. Use the size called out by the WPS or job plan. If the wire diameter is not specified, verify the required size before selecting from stock.

    Check: torch setup, cup size, tungsten condition, and shielding gas flow. For general TIG setup support, see the Square Wave 205 TIG Cup Size Selection Guide for cup size, gas lens, and stickout checks. Although that article is not specific to ERCuSi-A, the setup discipline is the same: stable shielding, clean arc starts, and correct torch geometry.

    Inspect: tungsten for contamination or improper grind. If the arc wanders, starts dirty, or black specks appear, review the tungsten and gas path before blaming the filler. See the TIG Tungsten Contamination Troubleshooting guide for re-grind and contamination checks.

    Verify: arc stability, wetting behavior, and bead shape on a test coupon when the application is new, thin-gauge, or service-critical.

    Troubleshooting Support Checks

    If the bead is rough, the wetting is poor, or the repair lifts at the edges, work through the basic checks in order:

    • Check joint cleanliness again.
    • Inspect shielding gas coverage and torch angle.
    • Verify travel speed and heat input.
    • Confirm that the base metal and filler are actually compatible.
    • Review whether the job should be braze-welded or repaired by another method.

    For arc wander or unstable starts, grounding and torch setup can also matter. The TIG arc wandering causes guide covers tungsten, gas, ground, and AC setup checks that apply broadly to GTAW troubleshooting.

    Safety Notes

    Follow standard welding safety practices. Use eye and face protection, gloves, and flame-resistant clothing. Provide ventilation appropriate for the work area. Clean coatings, oils, and plated surfaces before welding only if the site procedure allows it. If there is any chance of unknown coating chemistry, treat the job as a fume risk and verify controls before proceeding.

    Do not weld on pressure-containing, load-bearing, or regulated parts without confirming the required procedure and approval path. If the job classification is uncertain, stop and verify with the supervisor, engineer, or quality contact.

    FAQ

    Q: Is ERCuSi-A the right choice for every copper repair?
    A: No. It is a starting point for silicon bronze TIG/GTAW selection. Confirm the exact base metal, joint design, and service condition first.

    Q: Can I use ERCuSi-A just because the finder suggests it?
    A: No. The filler metal finder is a selection aid, not procedure approval. The WPS and manufacturer data sheet still control the final choice.

    Q: What should I do if the base metal is not clearly identified?
    A: Treat it as Unknown (Verify). Do not assume compatibility from appearance alone.

    Q: Does ERCuSi-A automatically fit structural or code work?
    A: Not automatically. Verify code requirements, WPS limits, and customer approval before using it on regulated work.

    Sources Checked

    Notes: AWS spec listed on the source page: AWS A5.7. Any additional technical detail not confirmed on the provided source pages should be treated as Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.
    Related Weld Support Guides

  • Lincoln Electric Welding Helmet Replacement Parts: What to Check Before Ordering

    Lincoln Electric Welding Helmet Replacement Parts: What to Check Before Ordering

    Lincoln PRO-Torch PTA-17 Support

    If you are searching for Lincoln Electric welding helmet replacement parts, the first step is not ordering. It is confirming what part you actually need, what helmet model you own, and whether the replacement is a direct fit or only a possible match. Helmet shells, lenses, headgear, inner covers, sweat bands, and gaskets can look similar across models, but small differences in mounting points, lens frames, or adjustment hardware can stop a part from working as expected.

    This article focuses on the checks that reduce returns, delays, and fitment mistakes. Use it as a pre-order checklist before you buy anything for a Lincoln helmet.

    Key Takeaways

    • Confirm the exact helmet model and part location before ordering.
    • Check the mounting style, dimensions, and wear pattern, not just the brand name.
    • Use the WSP lookup page as a support reference, not a substitute for model verification.
    • When details are unclear, mark them as Unknown (Verify) and inspect the helmet directly.
    • For welding procedure questions, use filler metal pages only as selection starting points, not automatic approval.

    Start with the helmet model, not the part name

    Many support calls begin with a description like “I need the inside cover for a Lincoln helmet.” That is not enough information. The same common part name can apply to multiple helmet families, but the attachment method may differ. Before ordering, inspect the label, model marking, or shell identification on the helmet itself.

    Check:

    • Helmet brand and model number
    • Any printed code on the shell, headgear, or lens frame
    • Whether the helmet is an auto-darkening model, passive lens model, or grinder-style support setup

    Inspect: The current part for distortion, cracked tabs, stretched elastic, stripped knobs, or heat damage.

    Verify: If the model marking is missing or unreadable, record it as Unknown (Verify) and compare the helmet against manufacturer documentation or a support reference before ordering.

    Check the failure point before replacing anything

    Not every worn helmet symptom means a full parts replacement. A loose headgear may only need an adjustment or strap replacement. A blurry view may point to scratched cover lenses instead of the filter cartridge. A helmet that feels unstable may have a worn pivot point, not a bad shell.

    Common checks:

    • Outer cover lens: Look for spatter pits, heat haze, scratches, and clouding.
    • Inner cover lens: Inspect for fingerprints, micro-scratches, and warp.
    • Headgear: Check strap elasticity, ratchet operation, pivot friction, and crown pad wear.
    • Gaskets and seals: Look for shrinkage, tearing, or sections that no longer sit flat.
    • Shade cartridge area: Check for loose retainers, broken clips, and housing damage.

    Verify: Replace only the failed wear item unless the helmet frame or carrier parts are also damaged.

    Measure before you order

    Part fit depends on more than the brand name. Measure the visible opening, lens frame size, pivot spacing, and any clip or tab locations if you can access them safely. Do not guess based on appearance alone.

    Check:

    • Lens width and height
    • Clip location and tab shape
    • Pivot hole spacing
    • Depth of the lens carrier or filter pocket

    Inspect: The old part for deformation. Heat-warped plastic can mislead measurements and make a replacement seem wrong when the original part is actually damaged.

    Verify: If the original part is bent or broken, measure the surrounding undamaged area and compare that with the replacement reference. If the required dimension is uncertain, treat it as Unknown (Verify).

    Troubleshooting support checks before ordering

    Use a short troubleshooting pass before you buy. This helps separate a true replacement need from an adjustment problem.

    • Helmet feels loose: Check the ratchet, crown adjustment, and side pivots.
    • Helmet slips down: Inspect headband tension and worn padding.
    • View is scratched or cloudy: Replace the outer or inner cover lens first if the filter itself is still functional.
    • Shades or visibility seem off: Inspect the cartridge mount, battery area, and lens carriers before assuming the helmet needs a shell-level part.

    Check / Inspect / Verify sequence:

    1. Check the symptom during normal use.
    2. Inspect the related wear item on the bench under good light.
    3. Verify whether the issue is the part itself, the adjustment, or a damaged mounting point.

    Use the WSP lookup page as a support reference

    For Lincoln support pages and related lookup guidance, use the Weld Support Parts reference page here:

    Lincoln PRO-Torch PTA-17 Support

    That page is a support reference and a starting point for checking compatible documentation, replacement-first guidance, and linked Lincoln lookup information. It is not a substitute for confirming the exact helmet model and part geometry.

    How to use it:

    • Open the support page while you have the helmet in hand.
    • Match the model and the part category before selecting anything.
    • Use the page as a cross-check if your current part is worn, broken, or missing markings.

    Ordering checks that prevent the wrong part

    Before finalizing an order, compare the replacement against the worn part and the helmet model record.

    Check:

    • Part name and function
    • Mounting style
    • Orientation and left/right placement
    • Any note about model-specific fit
    • Whether the part is a wear item or a structural component

    Inspect: The original part beside the product image or support reference, if available.

    Verify: If the ordering page does not clearly confirm fitment, do not assume compatibility. Record the fit as Unknown (Verify) and confirm with the seller or support documentation.

    Safety notes

    • Remove the helmet from service if the shell is cracked, the lens carrier is loose, or the headgear will not hold position.
    • Do not use a damaged lens assembly for arc welding.
    • Replace missing or failed protective components before returning the helmet to the shop.
    • If you are unsure whether a part affects eye or face protection, treat it as a safety-critical item until verified.

    FAQ

    How do I know which Lincoln helmet part I need?
    Start with the helmet model, then identify the failed component by location and function. Compare the worn part to the helmet before ordering.

    Can I order by appearance only?
    No. Similar-looking helmet parts may differ in tabs, spacing, or carrier style. Appearance alone is not enough.

    What if the model number is missing?
    Mark the model as Unknown (Verify) and inspect the shell, headgear, and lens frame for identifying marks before buying a replacement.

    Should I replace the whole helmet if one part is worn?
    Not always. Replace the failed wear item first unless the shell, carrier, or protective assembly is damaged.

    Sources Checked

    Related reading: If you are comparing helmet support approaches across brands, see Lincoln K3034-4 Viking Helmet: What to Expect and the 3M Speedglas G5-02 Welding Helmet Support Guide for additional fitment-check structure.

    Related Weld Support Guides

  • ERCu TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCu TIG / GTAW Filler Metal: Selection and Compatibility Checks

    ERCu TIG / GTAW Filler Metal

    ERCu TIG / GTAW filler metal is used for compatible deoxidized copper applications, but it should never be treated as an automatic match. For copper repair and joining work, the key questions are still the same: what is the base metal, what does the WPS allow, what is the service condition, and what does the filler manufacturer state on the data sheet. If those answers are not confirmed, the filler choice remains unverified.

    This article is a selection and compatibility check guide for welders, fabricators, maintenance buyers, and support teams. It is not a procedure approval. Use the filler page as a starting point, then verify the job requirements before ordering wire or striking an arc.

    Key Takeaways

    • ERCu is an AWS A5.7 copper filler classification. Treat the classification as a starting point, not a final approval.
    • Confirm the base metal grade before use. Deoxidized copper and copper repair are the stated application area, but specific alloy acceptance is Unknown (Verify).
    • Check the WPS, code requirements, and service conditions before selecting filler.
    • Verify rod diameter, joint access, gas coverage, and torch setup before production welding.
    • If any compatibility point is unclear, stop and verify with engineering, the WPS, or the filler data sheet.

    What ERCu TIG / GTAW filler is used for

    The WSP filler metal page identifies the filler as ERCu TIG / GTAW Filler Metal for copper TIG/GTAW work, with a stated use on deoxidized copper and copper repair. That is the starting point. It does not replace the WPS, job specification, or manufacturer data sheet.

    A practical selection check starts with the base metal. If the part is copper, verify whether it is deoxidized copper, oxygen-free copper, a copper alloy, or a repair build-up on an existing component. ERCu may be appropriate for some jobs and not acceptable for others. That decision is controlled by procedure and service requirement, not by filler classification alone.

    Check the job before you choose the rod

    Use this sequence before cutting wire or filling the machine feeder with rod stock:

    1. Check the WPS. Confirm whether ERCu is listed or whether another copper filler is required. If no WPS exists, the job needs review before weld start.
    2. Inspect the base metal identification. Look for stamping, material certs, heat tags, drawings, or repair history. If the grade is unknown, mark it Unknown (Verify).
    3. Verify service conditions. Copper repair in water service, thermal service, electrical service, or pressure-related service may have different filler requirements. Do not assume equivalence.
    4. Check joint design. Copper joints often need clean fit-up and good torch access. Confirm root opening, backing, and access for filler addition.
    5. Confirm rod diameter. The filler page keywords reference 1/16 in, 3/32 in, and 1/8 in. That indicates common sizes, but the correct size for your job is Unknown (Verify) unless the order or WPS specifies it.

    Compatibility checks that matter in the shop

    Compatibility for copper GTAW work is not just chemistry. It is also thermal control, contamination control, and joint cleanliness. Copper pulls heat quickly and can produce poor tie-in if setup is weak.

    1) Base metal compatibility

    Verify the exact copper grade. The allowed filler page says deoxidized copper and copper repair, but it does not confirm every copper alloy. If the workpiece is brass, bronze, copper-nickel, or a proprietary alloy, compatibility is Unknown (Verify) until the WPS or data sheet says otherwise.

    2) Joint cleanliness

    Inspect the joint for oil, oxide, paint, plating, and embedded contamination. Clean copper before welding. Use approved cleaning methods for the job, then verify the surface is bright enough for sound wetting. Dirty copper can produce unstable starts, poor fusion, and excessive cleanup.

    3) Heat input and torch control

    Copper requires disciplined heat management. Verify torch angle, arc length, and filler addition rhythm before production. If the arc is wandering, the issue may be tungsten condition, gas coverage, or grounding rather than the filler itself. For related TIG setup checks, see the internal guide on TIG arc wandering causes.

    4) Gas coverage and contamination control

    Inspect gas lenses, cups, flow path, and consumable condition. Poor shielding can make a good filler look wrong. If contamination is visible, verify cup size, stickout, and tungsten prep using the internal guide on TIG cup size selection and the troubleshooting note on tungsten contamination.

    How to use the filler metal finder

    The WSP filler metal finder is a selection tool, not a procedure approval. Use it to narrow the candidate list, then verify the final choice against the WPS and the filler data sheet. You can review the finder here: WSP Filler Metal Finder.

    Use the finder when you need to cross-check process, classification, or application fit. If the finder suggests ERCu for a copper repair case, that is still not enough to release the job. Confirm:

    • Base metal grade
    • Joint design
    • Service environment
    • WPS and code limits
    • Manufacturer instructions

    If any of those points are not documented, the compatibility status is Unknown (Verify).

    Troubleshooting support checks

    Problem: poor wetting or weak tie-in. Check surface contamination, joint fit-up, and heat input first. Verify copper cleanliness before changing filler.

    Problem: arc instability. Inspect tungsten condition, gas coverage, and ground connection. Do not assume the filler is the cause. Review the tungsten contamination and arc wandering guides for setup checks.

    Problem: wrong rod size at the bench. Verify the WPS and the job package. If size is not listed, hold the job and confirm with supervision or engineering.

    Problem: material identity is unclear. Stop and verify the base metal with certs, tags, or testing. Unknown material means Unknown (Verify) filler selection.

    Safety notes

    • Copper welding can produce intense reflected heat. Wear full hand, eye, and body protection suitable for the process.
    • Verify local ventilation requirements before welding. Fume and ozone control may be needed depending on the job setup.
    • Do not weld on unidentified material without review.
    • Follow site hot work and lockout requirements when repairing copper components in service.
    • When in doubt, stop the job and verify the WPS, material ID, and filler data sheet.

    FAQ

    Is ERCu always the right filler for copper?

    No. ERCu is a classification, not a universal approval. Verify the base metal, WPS, and service conditions before use.

    Can I use the filler metal page as proof of compatibility?

    No. The filler page is a selection starting point only. Final compatibility depends on the WPS, code requirements, material grade, and manufacturer data sheet.

    What if the copper alloy is not clearly identified?

    Mark it Unknown (Verify) and stop until the material is identified. Do not guess on copper compatibility.

    Do the listed rod sizes mean they are approved for every job?

    No. The keywords reference common sizes, but the correct size for a specific job is Unknown (Verify) unless the WPS or job documents confirm it.

    Sources Checked

    Use ERCu only after the WPS, base metal, and service conditions are verified. If the job file does not support the choice, the correct action is to stop and verify.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • Miller Spoolmatic 30A Parts Diagram: How to Identify Replacement Parts

    Miller Spoolmatic 30A Parts Diagram: How to Identify Replacement Parts

    Miller Spoolmatic Spool Guns Parts Breakdown

    If you are trying to match a Miller Spoolmatic 30A parts diagram to an actual replacement need, the main task is not just naming a part. It is confirming the exact wear item, the item number on the breakdown, and the condition that caused the failure. On spool guns, small parts can create feeding problems, intermittent arc stability, burnback, or wire damage when they are worn, loose, or installed incorrectly.

    This guide is for welders, maintenance buyers, and support teams who need a practical way to identify replacement parts without guessing. It complements the parts lookup on Weld Support Parts and helps you verify what you are seeing before you order anything.

    Key Takeaways

    • Use the parts diagram to match item numbers first, not just visual shape.
    • Check the gun body, cable ends, trigger, gun tube, drive path, liner path, and consumable end for wear.
    • Do not assume two parts are interchangeable because they look similar. Verify by the diagram and the lookup page.
    • For uncertain details, treat them as Unknown (Verify) until confirmed on the supported lookup page or by direct inspection.

    How to Read the Parts Diagram Correctly

    A parts diagram is a reference map. It shows how the gun is broken into assemblies and item numbers, but it does not replace physical verification. Start by locating the section that matches the problem area:

    • Front end: nozzle, tip, retaining parts, and any front insulator components.
    • Feed path: liner, drive roll-related components, wire guide parts, and inlet/outlet paths.
    • Handle and trigger area: trigger, switch, fasteners, strain relief, and housing pieces.
    • Cable and gun body: power cable, control leads, and connectors.

    Then check the item number on the diagram against the breakdown list. If the page uses a part description that is close but not exact, stop there and verify the actual item number, assembly position, and revision before replacing anything.

    Inspection Steps Before You Replace a Part

    Use these checks before you remove the gun from service:

    1. Inspect the feed path: remove wire and check for shavings, liner damage, tight bends, or contamination.
    2. Inspect the front end: verify the tip, nozzle, and any retaining parts are not burned, worn, or physically loose.
    3. Inspect the trigger action: confirm the trigger returns freely and does not stick.
    4. Inspect cable strain relief: look for cuts, flattening, heat damage, or broken support near the handle and power connection.
    5. Inspect connections: confirm all fittings are secure and there is no movement where there should be none.

    If the symptom is wire feeding failure, do not replace the gun body first. Verify the consumables, liner path, and spool drag condition before moving to larger components.

    Troubleshooting Support: Check, Inspect, Verify

    Check: wire feed speed consistency, trigger response, and whether the wire stops cleanly when the trigger is released.

    Inspect: the nozzle, tip, liner, cable routing, and any points where the wire may catch or birdnest.

    Verify: the exact item number on the parts diagram and match it to the WSP lookup page before ordering a replacement.

    If the gun feeds erratically, the problem may be in more than one place. For example, a worn tip can mimic a liner problem, and a liner problem can mimic spool drag. Replace only the part you have verified as worn, damaged, or out of position.

    WSP Lookup Section

    Use the Weld Support Parts breakdown page here: Miller Spoolmatic Spool Guns Parts Breakdown.

    This lookup page is the starting point for item-number matching, diagram review, and replacement notes. Use it to confirm the support task, not to assume fitment beyond what the page and your own inspection verify. If a detail is not clearly identified, mark it as Unknown (Verify).

    What Usually Matters on a Spool Gun Replacement Job

    Most replacement work on a spool gun comes down to a few practical questions:

    • Is the problem in the consumable end, the feed path, or the cable/trigger assembly?
    • Is the part physically damaged, worn, or simply dirty?
    • Does the diagram item number match the failed component exactly?
    • Do you need one part, or a small set of related parts to solve the issue?

    Do not use a general description alone. A front-end wear item, a liner-related item, and a housing fastener can all appear similar in a quick photo. Verify the location and function before ordering.

    Safety Notes

    • Disconnect welding power before opening the gun or removing parts.
    • Let hot parts cool before handling the nozzle, tip, or front-end hardware.
    • Use eye protection when cutting wire, removing a liner, or cleaning debris from the feed path.
    • Do not force fittings or connectors. If a part does not seat correctly, stop and verify the part number and orientation.
    • Keep the wire secured so it does not unspool unexpectedly during service.

    FAQ

    How do I know which part from the diagram I need?
    Start with the symptom, then inspect the matching section of the gun. Confirm the item number on the diagram and compare it to the WSP lookup page before you order.

    Can I use a similar-looking part if the original is unavailable?
    Do not assume interchangeability. If the page does not clearly confirm fitment, treat the match as Unknown (Verify).

    What should I replace first when wire feeding becomes inconsistent?
    Check the consumable end, liner path, wire condition, and spool drag before replacing larger assemblies. Many feed issues come from wear or contamination in one of those areas.

    Does the diagram tell me how to repair the gun?
    It tells you how the parts are identified and organized. Repair procedure still depends on the actual fault, safe disassembly, and confirmed part condition.

    Sources Checked

    Internal links checked for supporting troubleshooting context:

    Technical details not clearly confirmed on the provided lookup page should be treated as Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • More posts

    Listen with Audible