Search results for: “MIG welding parts”

  • Miller Spoolmatic 30A Parts Diagram: How to Identify Replacement Parts

    Miller Spoolmatic 30A Parts Diagram: How to Identify Replacement Parts

    Miller Spoolmatic Spool Guns Parts Breakdown

    If you are trying to match a Miller Spoolmatic 30A parts diagram to an actual replacement need, the main task is not just naming a part. It is confirming the exact wear item, the item number on the breakdown, and the condition that caused the failure. On spool guns, small parts can create feeding problems, intermittent arc stability, burnback, or wire damage when they are worn, loose, or installed incorrectly.

    This guide is for welders, maintenance buyers, and support teams who need a practical way to identify replacement parts without guessing. It complements the parts lookup on Weld Support Parts and helps you verify what you are seeing before you order anything.

    Key Takeaways

    • Use the parts diagram to match item numbers first, not just visual shape.
    • Check the gun body, cable ends, trigger, gun tube, drive path, liner path, and consumable end for wear.
    • Do not assume two parts are interchangeable because they look similar. Verify by the diagram and the lookup page.
    • For uncertain details, treat them as Unknown (Verify) until confirmed on the supported lookup page or by direct inspection.

    How to Read the Parts Diagram Correctly

    A parts diagram is a reference map. It shows how the gun is broken into assemblies and item numbers, but it does not replace physical verification. Start by locating the section that matches the problem area:

    • Front end: nozzle, tip, retaining parts, and any front insulator components.
    • Feed path: liner, drive roll-related components, wire guide parts, and inlet/outlet paths.
    • Handle and trigger area: trigger, switch, fasteners, strain relief, and housing pieces.
    • Cable and gun body: power cable, control leads, and connectors.

    Then check the item number on the diagram against the breakdown list. If the page uses a part description that is close but not exact, stop there and verify the actual item number, assembly position, and revision before replacing anything.

    Inspection Steps Before You Replace a Part

    Use these checks before you remove the gun from service:

    1. Inspect the feed path: remove wire and check for shavings, liner damage, tight bends, or contamination.
    2. Inspect the front end: verify the tip, nozzle, and any retaining parts are not burned, worn, or physically loose.
    3. Inspect the trigger action: confirm the trigger returns freely and does not stick.
    4. Inspect cable strain relief: look for cuts, flattening, heat damage, or broken support near the handle and power connection.
    5. Inspect connections: confirm all fittings are secure and there is no movement where there should be none.

    If the symptom is wire feeding failure, do not replace the gun body first. Verify the consumables, liner path, and spool drag condition before moving to larger components.

    Troubleshooting Support: Check, Inspect, Verify

    Check: wire feed speed consistency, trigger response, and whether the wire stops cleanly when the trigger is released.

    Inspect: the nozzle, tip, liner, cable routing, and any points where the wire may catch or birdnest.

    Verify: the exact item number on the parts diagram and match it to the WSP lookup page before ordering a replacement.

    If the gun feeds erratically, the problem may be in more than one place. For example, a worn tip can mimic a liner problem, and a liner problem can mimic spool drag. Replace only the part you have verified as worn, damaged, or out of position.

    WSP Lookup Section

    Use the Weld Support Parts breakdown page here: Miller Spoolmatic Spool Guns Parts Breakdown.

    This lookup page is the starting point for item-number matching, diagram review, and replacement notes. Use it to confirm the support task, not to assume fitment beyond what the page and your own inspection verify. If a detail is not clearly identified, mark it as Unknown (Verify).

    What Usually Matters on a Spool Gun Replacement Job

    Most replacement work on a spool gun comes down to a few practical questions:

    • Is the problem in the consumable end, the feed path, or the cable/trigger assembly?
    • Is the part physically damaged, worn, or simply dirty?
    • Does the diagram item number match the failed component exactly?
    • Do you need one part, or a small set of related parts to solve the issue?

    Do not use a general description alone. A front-end wear item, a liner-related item, and a housing fastener can all appear similar in a quick photo. Verify the location and function before ordering.

    Safety Notes

    • Disconnect welding power before opening the gun or removing parts.
    • Let hot parts cool before handling the nozzle, tip, or front-end hardware.
    • Use eye protection when cutting wire, removing a liner, or cleaning debris from the feed path.
    • Do not force fittings or connectors. If a part does not seat correctly, stop and verify the part number and orientation.
    • Keep the wire secured so it does not unspool unexpectedly during service.

    FAQ

    How do I know which part from the diagram I need?
    Start with the symptom, then inspect the matching section of the gun. Confirm the item number on the diagram and compare it to the WSP lookup page before you order.

    Can I use a similar-looking part if the original is unavailable?
    Do not assume interchangeability. If the page does not clearly confirm fitment, treat the match as Unknown (Verify).

    What should I replace first when wire feeding becomes inconsistent?
    Check the consumable end, liner path, wire condition, and spool drag before replacing larger assemblies. Many feed issues come from wear or contamination in one of those areas.

    Does the diagram tell me how to repair the gun?
    It tells you how the parts are identified and organized. Repair procedure still depends on the actual fault, safe disassembly, and confirmed part condition.

    Sources Checked

    Internal links checked for supporting troubleshooting context:

    Technical details not clearly confirmed on the provided lookup page should be treated as Unknown (Verify).

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1): Application and Buying Checks

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1): Application and Buying Checks

    “>TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1) is a solid MIG wire intended for gas metal arc welding on mild and low-alloy steel. For buyers and maintenance teams, the main question is not only whether the wire will weld, but whether it matches the joint condition, wire feeder setup, and procedure requirements in your shop. This guide focuses on application checks, fitment checks, and practical verification steps before you commit to a spool.

    Key Takeaways

    • ER70S-2 class solid wire is commonly selected for mild and low-alloy steels where stable feeding and weld quality matter.
    • Wire diameter, spool size, drive-roll setup, liner condition, and contact tip size all need verification before use.
    • Do not assume the wire will overcome poor prep; clean base metal still gives better results.
    • If procedure approval matters, verify the WPS and any filler metal listing before release to production.

    What this wire is for

    Based on the available product information, this is a .030 in (0.8 mm) solid MIG wire in the ER70S-2 family, supplied on a 33 lb spool. That makes it a common size for general fabrication, repair work, and light-to-medium production welding on carbon steel. The added deoxidizers associated with ER70S-2 chemistry can help in situations with light mill scale or minor surface contamination, but they do not replace cleaning, fit-up control, or procedure compliance. Best results still come from clean base metal.

    Use this wire as a candidate when you need a general-purpose carbon steel MIG wire and your equipment is configured for .030 in solid wire. If your job is governed by a written WPS, the WPS controls. If the wire is being selected for maintenance repair without a formal WPS, verify the joint type, shielding gas, deposition target, and feeder setup before purchase or installation. Unknown (Verify) for any application outside mild and low-alloy steel service.

    Buying checks before you order or load the spool

    Check wire diameter. Confirm the feeder, gun, and contact tip are set up for .030 in wire. A mismatch can cause erratic feeding, burnback, or inconsistent arc starting.

    Inspect spool compatibility. Confirm that your feeder accepts the spool format and weight. The product listing indicates a 33 lb spool, but always verify your machineโ€™s maximum spool size and hub capacity. Unknown (Verify) if your feeder has a narrow spool compartment or light-duty hub.

    Verify shielding gas. ER70S-2 solid wire normally runs with shielding gas, but the exact mix depends on your procedure and base metal. Do not assume a gas type from the wire class alone. Check the WPS or internal process sheet.

    Check drive-roll and liner setup. Solid wire generally feeds best with the correct groove profile, proper tension, and a clean liner. If the feeder was last used with flux-cored wire, inspect drive-roll selection and liner wear before loading this spool.

    Inspect contact tip wear. A worn tip can look like a wire problem. Replace tips that are ovaled, burned, or loose.

    Application and process checks

    Check base metal condition. ER70S-2 can be more forgiving than basic wire on slightly imperfect surfaces, but do not use that as a substitute for cleaning. Remove oil, rust, heavy mill scale, paint, moisture, and weld residue wherever practical.

    Verify joint access and polarity. Confirm the gun can maintain a stable arc length and that the machine polarity matches the process setup required by your WPS or equipment instructions. If you do not have that documentation, verify it before starting production.

    Inspect fit-up. Poor gap control can hide under a good-looking bead. Check root opening, alignment, and tack quality before blaming the wire.

    Confirm feed consistency. Test feed the wire through the gun cable with the machine cold. Look for drag, birdnesting, or intermittent push. If the wire does not feed smoothly on setup, fix the feeder first.

    Verify arc behavior on coupon. Run a short test on scrap from the same material family. Inspect bead shape, spatter level, wetting, and tie-in. If results are inconsistent, compare gas flow, tip condition, liner wear, and feed speed before changing wire class.

    Troubleshooting support: check, inspect, verify

    If the arc is unstable: check gas flow, inspect for leaks or loose fittings, and verify tip-to-work distance and stickout against your procedure.

    If feeding is rough: check drive-roll tension, inspect the liner for wear or contamination, and verify the correct tip size for .030 in wire.

    If spatter is excessive: check voltage and wire feed settings, inspect ground connection quality, and verify the shielding gas setup before changing product.

    If weld appearance is inconsistent: inspect base metal cleanliness, verify travel speed, and check joint fit-up. Do not assume the spool is at fault until the machine and preparation are reviewed.

    WSP lookup and filler metal finder

    For procedure-controlled work, use the Weld Support Parts lookup tools as starting points, then verify against the approved WPS or engineering release. These pages help with selection and comparison, but they are not a substitute for procedure approval.

    If your job requires documented filler approval, use those pages to narrow the candidate list, then confirm the final selection against your internal welding documentation. Treat the result as a starting point, not a guaranteed procedure match.

    Safety notes

    Handle wire spools carefully. Edges can be sharp, and loose wire ends can whip back during loading. Wear gloves when opening packaging, setting a spool, or trimming wire. Keep the feeder powered down during installation. Verify ventilation and fume control before welding. Follow your siteโ€™s hot-work controls, especially on painted or contaminated material.

    FAQ

    Is this wire only for mild steel?
    The provided product information supports use on mild and low-alloy steel. Unknown (Verify) for other base metals or special applications.

    Can I use it on lightly scaled material?
    ER70S-2 chemistry may help tolerate light mill scale or minor contamination, but that is not a license to skip cleaning. Inspect the surface and clean it as much as the job allows.

    Do I need a specific gas or procedure?
    Verify your shielding gas and procedure from the WPS or internal welding instructions. Do not select gas solely from the wire class.

    How do I know if the spool will fit my feeder?
    Check the feederโ€™s spool diameter, hub design, and maximum weight rating. If the machine documentation is unavailable, measure and verify before purchase or install.

    Sources Checked

    • Provided ArcWeld product reference for TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)
    • WSP lookup page
    • WSP filler metal finder
    • Allowed internal links provided in the task

    Final verification should always come from the active WPS, machine manual, and shop qualification records.

    Related Arc Weld Part

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 063 Washington Alloy .030, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 04 is an ER70S-2 solid MIG (GMAW) wire for welding mild and low-alloy steels where consistent feeding and sound weld quality matter; ER70S-2 chemistry includes added deoxidizers that can help tolerate light mill scale and minor surface contamination versus standard ER70S-6 (best results still come from clean base metal). This item is one (1) spool of .030 in (0.8 mm) wire, 33 lb (0.91 kg)…

    View at Arc Weld Store

    Related Weld Support Guides

  • TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1) is an ER70S-2 solid GMAW wire for mild and low-alloy steel work where stable feeding and weld soundness matter. For buyers and support teams, the main value is straightforward: this is a general-purpose solid wire with deoxidizers, supplied as one 11 lb spool in .035 in (0.9 mm). Use it only after you verify the job requirements, base metal condition, shielding gas, and equipment setup.

    Key Takeaways

    • ER70S-2 is a solid MIG wire used on mild and low-alloy steels.
    • Added deoxidizers help when base metal has light surface contamination, but they do not replace proper cleaning.
    • .035 in wire is a common size for general fabrication and repair, but the correct choice still depends on the machine, transfer mode, and joint details.
    • Pack size is one spool, 11 lb. Verify spool dimensions and machine fit before purchase.
    • Use a verified procedure from the machine, WPS, or qualified welding engineer when code work is involved.

    What this wire is for

    This product is intended for GMAW on steels where a dependable general-purpose wire is needed. ER70S-2 is commonly selected for shop fabrication, maintenance repair, and production work on carbon steel or low-alloy steel. The exact application still depends on joint design, shielding gas, base metal condition, and the procedure being used. If your job calls for aluminum, stainless, flux-cored, or hardfacing wire, this is not the correct filler metal.

    Product and parts review

    The available product information identifies this item as one spool of Washington Alloy TC 70S-2 08 in .035 in diameter, 11 lb, pack of one. Beyond that, confirm the following before it is placed into service:

    • Wire type: solid MIG/GMAW wire, ER70S-2.
    • Diameter: .035 in (0.9 mm).
    • Net weight: 11 lb.
    • Package quantity: one spool.
    • Machine fit: Unknown (Verify) spool hub, spool diameter, and drive-roll compatibility.
    • Shielding gas: Unknown (Verify) based on procedure and application.

    If you are stocking wire for a maintenance crib, record the spool size, wire diameter, and machine compatibility on the shelf label. Do not assume every .035 solid wire fits every feeder without changes to drive rolls, liners, and contact tips.

    Setup checks: inspect before feeding

    • Check the spool label. Verify diameter, classification, and lot identification if your quality system requires traceability.
    • Inspect wire condition. Look for rust, kinks, or contamination. If the wire is damaged, do not install it.
    • Verify feeder setup. Confirm the drive rolls are the correct groove type for solid wire and that liner condition is acceptable.
    • Check contact tip size. The tip should match the wire diameter. If not, verify the correct replacement before welding.
    • Inspect shielding gas flow. Make sure the gas hose, regulator, and connections are leak-free and set according to the approved procedure.
    • Verify polarity. Confirm the machine is set for the wire and transfer mode being used.

    Troubleshooting and support

    When a MIG wire does not run correctly, start with the feeder and the work setup before blaming the wire itself.

    If the wire bird-nests or feeds inconsistently

    • Check: Drive-roll tension. Too much tension can deform the wire; too little can slip.
    • Inspect: Liner, contact tip, and gun cable routing for blockage or sharp bends.
    • Verify: Spool brake setting and feeder alignment.

    If the arc is unstable or spatter is high

    • Check: Voltage, wire feed speed, and shielding gas flow.
    • Inspect: Work clamp placement and base metal surface condition.
    • Verify: That the wire classification, polarity, and gas blend match the approved procedure.

    If porosity appears in the weld

    • Check: Shielding gas coverage and leaks at the torch, hose, and fittings.
    • Inspect: Rust, oil, paint, mill scale, and moisture on the joint.
    • Verify: Whether the selected wire and gas are suitable for the job and whether the joint prep meets requirements.

    How to use filler metal pages as a starting point

    When you are selecting wire for a job, use approved filler metal references as a starting point, not as automatic procedure approval. The available internal reference pages on the Weld Support Parts blog can help you compare product categories and related wire types. If a job is outside your normal range, confirm the final selection against the WPS, the machine manual, or a qualified welding authority. Do not rely on product pages alone for code or critical work.

    Related internal reference articles:

    Buyer guidance for maintenance teams

    For maintenance and fabrication buyers, the main checks are not marketing claims. They are feedability, repeatability, and fit with the shop process. Before ordering, verify the following:

    • Diameter matches the feeder setup used on the machine.
    • Spool size fits the wire feeder or spool gun arrangement. Unknown (Verify).
    • Wire classification matches the material and procedure. Unknown (Verify) if the job is not plain carbon or low-alloy steel.
    • Shielding gas and transfer mode are approved for the weld being made.
    • Your inventory system can identify the spool as ER70S-2, .035 in, 11 lb.

    If a team routinely changes between wire sizes or wire classes, label the cabinet and gun setup clearly. That reduces downtime and avoids wrong-wire installation.

    Safety notes

    • Use approved PPE, including helmet, gloves, jacket, and safety footwear.
    • Keep the work area clear of flammables before striking an arc.
    • Do not weld on unknown coatings, sealed containers, or contaminated material without proper hazard review.
    • Handle the spool carefully. Cut wire ends can cause injury.
    • Follow the machine manual and shop procedure for setup, lockout, and maintenance.

    FAQ

    Is TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1) the same as ER70S-2?

    The product description identifies it as ER70S-2 solid MIG wire. Verify the label on the spool and the supplier listing before use.

    Can this wire be used on dirty or rusty steel?

    ER70S-2 includes deoxidizers, but that does not replace cleaning. Best practice is still to remove rust, oil, paint, and scale as required by the job.

    What shielding gas should be used?

    Unknown (Verify). Gas choice depends on the approved procedure, base metal, transfer mode, and weld requirements. Check the WPS or machine documentation.

    Will .035 in wire work in every MIG machine?

    No. Machine feedability depends on the feeder, liner, drive rolls, gun, and tip size. Verify compatibility before loading the spool.

    Sources Checked

    • ArcWeld product reference for TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)
    • Provided internal Weld Support Parts blog links
    • No WSP lookup page was provided for this task
    • No filler metal finder page was provided for this task

    Related Arc Weld Part

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 08 Washington Alloy .035, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 08 Washington Alloy is an ER70S-2 solid MIG (GMAW) wire for welding mild and low-alloy steels where consistent feeding and sound weld quality matter; ER70S-2 chemistry includes added deoxidizers and is commonly selected for general fabrication and repair work (best results come from properly prepared base metal). This item is one (1) spool of .035 in (0.9 mm) wire, 11 lb, packaged as a pack of (1). Set up…

    View at Arc Weld Store

    Related Weld Support Guides

  • TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 093 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 33 lb (15 kg) spool. For buyers and support teams, the main question is not whether the wire can weld mild steelโ€”it canโ€”but whether it matches the jobโ€™s fit-up, base-metal condition, and feeder setup. This article breaks down where this wire fits, what to verify before use, and how to troubleshoot common feeding and weld-quality issues without guessing at specifications that are not documented here.

    Key Takeaways

    What This Wire Is For

    As listed, TC 70S-2 093 is aimed at mild-steel work in fabrication, maintenance, and repair. That makes it relevant for shops that need a practical solid wire for general production work and field repair where clean surface prep is not always perfect. The ER70S-2 classification is commonly used when a shop wants a wire that tolerates light oxidation better than a basic clean-steel setup.

    Do not assume this wire is the right answer for every joint. A MIG wire selection still depends on base metal chemistry, joint design, shielding gas, transfer mode, and the required mechanical properties of the finished weld. If any of those points are unclear, treat this product as a candidate, not a final approval.

    Inspect Before You Load the Spool

    Before installing the spool, do a basic receiving check.

    If the shop has recurring feed issues, the wire is not the first thing to blame. Check the feeder path, tension, liner condition, and tip wear before changing consumables again.

    Troubleshooting Support: What to Check First

    Problem: Erratic feeding or birdnesting

    Problem: Excess spatter or unstable arc

    Problem: Porosity in the weld bead

    Selection Support: Where to Confirm the Filler Metal

    If your team needs a starting point for filler selection or cross-checking wire classifications, use the WSP resources as reference tools rather than automatic approvals. When available, the filler metal finder should be treated as a selection starting point, not a guarantee that a procedure is approved for your job, code, or base metal combination.

    Use those pages to narrow down options, then verify the actual WPS, shielding gas, and wire classification before production use.

    Product and Parts Notes

    This listing is for one spool of Washington Alloy TC 70S-2 093. The documented size is .035 in and the documented spool weight is 33 lb. Beyond that, do not assume details such as drive-roll type, recommended gas mix, or exact machine compatibility unless your internal procedure sheet or manufacturer documentation confirms them. For uncertain technical details, mark them as Unknown (Verify).

    For buyers, the important points are simple: confirm the classification, confirm the diameter, confirm the spool weight, and confirm that the feeder setup matches the wire path requirements of your machine. If the wire is being purchased for a repair bay, make sure the operators know whether the work is light fabrication, maintenance welding, or a qualified procedure with tighter limits.

    Practical Use Notes

    Triple-deoxidized ER70S-2 wires are often chosen when the surface is not ideal, but that does not eliminate prep. Remove loose scale, paint, oil, moisture, and heavy corrosion whenever possible. The more contaminated the joint, the less likely any MIG wire will produce reliable results. The right response is better cleaning, not overreliance on filler metal chemistry.

    For shop support teams, the right workflow is: identify the base metal, confirm the required process, match the filler classification, and verify the feeder hardware. This wire may be a good general-purpose option, but the procedure still controls the final weld.

    Safety Notes

    FAQ

    Is TC 70S-2 093 suitable for mild steel?
    Yes, the listed application is mild-steel fabrication, maintenance, and repair. Final suitability still depends on the WPS and job requirements.

    Can I use this wire on material with light mill scale?
    The product description says the triple-deoxidized ER70S-2 chemistry is suited for light mill scale or minor surface contamination. That is helpful, but it is not a substitute for proper cleaning.

    Does .035 in wire work in every MIG machine?
    No. Wire diameter compatibility depends on the feeder, drive rolls, liner, contact tip, and procedure. Verify the setup before loading the spool.

    Is the shielding gas confirmed in the product listing?
    Unknown (Verify). The available product information does not document a specific gas requirement.

    Sources Checked

    This draft uses only the provided product information and internal links. Any details not explicitly documented should be treated as Unknown (Verify).

    Related Arc Weld Part

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 093 Washington Alloy .035, 33 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 093 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 33 lb (15 kg) spool for mild-steel fabrication, maintenance, and repair, delivering stable arc characteristics and consistent feeding; its triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) is well-suited for producing clean welds when the base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1)…

    View at Arc Weld Store

    Related Weld Support Guides

  • TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1) is a solid MIG wire intended for mild-steel fabrication, maintenance, and repair. The key points for buyers are straightforward: it is .035 in (0.9 mm) diameter, it is an ER70S-2 class wire, and it is supplied on a 44 lb (20 kg) spool. For welders and maintenance teams, the practical question is not just what the label says, but whether the wire fits the feeder, matches the job, and gives stable performance in the actual work environment.

    This breakdown focuses on what to check before purchase and what to inspect after the spool arrives. It does not assume machine settings, procedure approval, or certification details that are not stated on the product page. Where a detail is not confirmed in the provided source, it is marked as Unknown (Verify).

    Key Takeaways

    What the Product Is Used For

    Based on the supplied product information, this wire is aimed at mild-steel fabrication, maintenance, and repair. That makes it relevant to production shops, farm and fleet repair, structural maintenance, and general fabrication work where a solid wire is preferred over flux-cored wire. The triple-deoxidized ER70S-2 chemistry is positioned for cleaner welds on steel that may have light mill scale or minor contamination. That does not remove the need for cleaning, but it may provide a wider practical window than a basic wire on less-than-perfect material.

    For buyer guidance, the first decision is whether your work is actually mild steel. If the job is stainless, aluminum, hardfacing, or a specialty alloy, this is not the right starting point. If the job is carbon steel and the feeder can handle .035 wire, it becomes a reasonable candidate for evaluation.

    Check Before You Buy

    Troubleshooting and Support: What to Inspect if Feeding or Arc Stability Is Poor

    If the wire arrives and the arc is unstable, do not immediately blame the filler metal. Run a basic inspection sequence.

    If porosity appears, inspect the work surface, shielding gas flow, leaks in the gas path, and joint prep before changing wire type. If lack of fusion appears, verify voltage, travel speed, and joint prep. If burnback or birdnesting shows up, inspect wire feed tension, tip size, and liner friction first.

    WSP Lookup and Filler Metal Finder

    Use the Weld Support Parts lookup tools as selection starting points, not guaranteed procedure approvals. They help narrow options, but they do not replace a qualified WPS, procedure test, or equipment verification.

    WSP lookup page

    WSP filler metal finder page

    If your team uses filler metal search tools, compare the wire class, diameter, and intended base metal against your actual job. Then verify the final choice against machine limits, spool size limits, and procedure requirements.

    Product / Parts Review

    The listing provided for this article identifies TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1). The confirmed details are limited to the wire class, diameter, spool weight, and pack quantity. Other technical details such as country of origin, AWS approval language beyond the ER70S-2 class designation, exact gas recommendation, and machine compatibility are Unknown (Verify).

    For maintenance buyers, the main value of a large spool is reduced changeover time. For production or repair work, that can help reduce interruptions. The tradeoff is storage and handling. A 44 lb spool needs a feeder and shop process that can manage the larger package without feed problems.

    If you are comparing this wire against another ER70S-2 option, evaluate the following: feeder fit, spool size fit, workpiece condition, and your normal gas and procedure setup. Do not compare only on price or spool weight. Those alone do not tell you whether the wire will run well in your machine.

    Safety Notes

    FAQ

    Is TC 70S-2 104 Washington Alloy .035 meant for stainless or aluminum?
    No. Based on the provided information, it is a solid MIG wire for mild steel and general carbon-steel repair work.

    Can I assume it will run on my MIG welder?
    No. Verify feeder capacity, spool hub fit, liner condition, drive-roll size, and your machine settings. Unknown (Verify) until checked against your equipment.

    Does ER70S-2 mean I can skip metal prep?
    No. The chemistry may help with light mill scale or minor contamination, but it does not replace cleaning, fit-up, or procedure control.

    Is the 44 lb spool better than a smaller spool?
    It can be better for high-use shops because it reduces changeovers. But only if your feeder and storage setup can handle it. Verify before buying.

    Sources Checked

    Final check before purchase: verify wire diameter, spool size, feeder fit, and procedure acceptance. If any of those are unknown, treat them as Unknown (Verify) until your team confirms them.

    Related Arc Weld Part

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 104 Washington Alloy .035, 44 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 104 is a .035 in (0.9 mm) ER70S-2 solid MIG wire on a 44 lb (20 kg) spool for mild-steel fabrication, maintenance, and repair, providing consistent feeding and a stable arc; the triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) helps produce clean welds when base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1) spool (verify your machine/spool…

    View at Arc Weld Store

    Related Weld Support Guides

  • TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1): Product Breakdown

    Product not found.
    “>TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 16 is a solid MIG wire in .045 in. diameter on an 11 lb spool. The core value of this wire is straightforward: it is intended for mild-steel fabrication, maintenance, and repair where stable feeding and practical arc control matter more than marketing claims. The ER70S-2 classification is typically used for cleaner welds on steel with light mill scale or minor surface contamination, but it is not a substitute for proper joint prep. Always verify the base metal condition and welding procedure before use.

    Key Takeaways

    What This Wire Is For

    This product is positioned for general mild-steel MIG welding in fabrication and maintenance environments. The triple-deoxidized ER70S-2 chemistry is commonly used to tolerate light surface oxidation better than basic solid wires, but the practical result depends on current settings, gas coverage, and operator technique. Use it as a production filler wire when the weldment calls for solid wire MIG on steel and the setup is already aligned to .045 in wire.

    If you are comparing options for steel filler metal selection, a filler metal finder can help you narrow down the starting point. It does not replace the welding procedure or a code requirement. Use the WSP filler metal finder as a selection reference only, then verify the final match against the application requirements.

    Setup Checks Before You Load the Spool

    Check: Confirm the machine is configured for .045 in solid wire. Verify drive rolls, gun liner, and contact tip size are appropriate for the wire diameter. Unknown (Verify) if the existing setup was previously used for a different diameter.

    Inspect: Look at the spool wrap, wire surface, and feed path. Any kinks, corrosion, or contamination can cause feed irregularity and arc instability.

    Verify: Confirm shielding gas type and flow are correct for the procedure. The product details provided here do not state a gas requirement, so use Unknown (Verify) and follow the approved WPS or shop standard.

    Check: Make sure the polarity matches solid MIG wire requirements for your process. If polarity is not confirmed by procedure or machine label, treat it as Unknown (Verify).

    Inspect: Clean the work lead connection, gun neck, liner entrance, and drive rolls. Small restrictions in the feed path often show up as birdnesting or erratic burnback.

    Verify: Test feed on scrap before going to production. A short trial pass is faster than correcting a bad setup on the part.

    Troubleshooting and Support

    If the wire feeds poorly

    Check drive roll tension first. Too much pressure flattens the wire and increases drag; too little lets the rolls slip. Inspect the liner for wear, contamination, or incorrect size. Verify that the contact tip is not oversized or worn out. If the wire was stored in a humid area, inspect it for surface oxidation before loading.

    If the arc is unstable

    Inspect the contact tip, nozzle, and work clamp. Verify consistent stickout and travel speed. If the arc wanders after a spool change, confirm the wire is seated correctly in the feeder and that the gun cable is not sharply bent.

    If weld quality is inconsistent

    Check base-metal prep before changing machine settings. ER70S-2 can help with light contamination, but it cannot compensate for heavy rust, paint, oil, or poor joint alignment. Verify fit-up, cleaning method, and shielding coverage before assuming the wire is the problem.

    For surface prep support, the Weld Support Parts blog includes a wire-wheel and pen-brush article that can help with cleaning strategy: Rocaris 6 Pack Wire Wheel & Pen Brush Set: Carbon Steel for Weld Cleaning & Surface Prep. Use it as a cleaning reference, not a process approval.

    Product and Parts Notes

    The provided product is the only confirmed item for this article: TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1). The available listing information identifies it as an ER70S-2 solid MIG wire on an 11 lb spool. Any additional details about spool construction, manufacturing tolerance, or machine compatibility are Unknown (Verify) unless confirmed by the product page or your shop procedure.

    If you need to cross-check whether this wire belongs in a larger consumables strategy, use the WSP product resources and internal references already approved for your team. Do not assume that a similar-looking wire will share the same operating window.

    Safety Notes

    FAQ

    Is this wire only for mild steel?

    The confirmed product information identifies it as ER70S-2 solid MIG wire for mild-steel fabrication, maintenance, and repair. Use on other metals is Unknown (Verify) unless your procedure specifically approves it.

    Can I use this wire on rusty or dirty material?

    ER70S-2 is often selected when there is light mill scale or minor surface contamination, but heavy rust, oil, paint, or poor joint prep still need removal. Inspect the base metal and verify cleaning requirements first.

    What machine settings should I use?

    Unknown (Verify). Machine settings depend on the welding procedure, material thickness, transfer mode, shielding gas, and joint design. Start from the approved WPS or manufacturer guidance, then verify on scrap.

    Will an 11 lb spool fit my feeder?

    Unknown (Verify). Spool size and hub compatibility vary by machine and feeder design. Check the feeder documentation and compare it with the spool dimensions and adapter requirements before purchasing.

    Sources Checked

    Support note: If you are building a consumables list for steel MIG work, start with the approved procedure, then verify feeder setup, wire diameter, and base-metal condition. That sequence prevents most wire-related problems before they start.

    Related Arc Weld Part

    TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    TC 70S-2 16 Washington Alloy .045, 11 Lb. 70S-2 MIG Wire, Pack of (1)

    Washington Alloy TC 70S-2 16 is a .045 in (1.2 mm) ER70S-2 solid MIG wire on an 11 lb (5 kg) spool for mild-steel fabrication, maintenance, and repair, offering consistent feeding and a stable arc; the triple-deoxidized ER70S-2 chemistry (Al/Ti/Zr) supports clean welds when base metal has light mill scale or minor surface contamination, and this listing includes Pack of (1) spool (set drive rolls/liner for .045 in…

    View at Arc Weld Store

    Related Weld Support Guides

  • Lincoln ED035417, 0.045″ UltraCore 111K3M-H Plus Mig Wire, 33 Lbs. Spool: Product Breakdown

    Lincoln ED035417, 0.045″ UltraCore 111K3M-H Plus Mig Wire, 33 Lbs. Spool: Product Breakdown

    Product not found.
    “>Lincoln ED035417, 0.045" UltraCore 111K3M-H Plus Mig Wire, 33 Lbs. Spool

    Lincoln ED035417, 0.045" UltraCore 111K3M-H Plus Mig Wire, 33 Lbs. Spool is a gas-shielded flux-cored wire intended for welding programs that need controlled arc behavior and all-position capability. For welders, fabricators, and maintenance buyers, the main question is not just what the wire is, but whether it fits the procedure, the base metal group, the shielding gas setup, and the duty cycle of the job. Use this breakdown as a working guide, not as a substitute for WPS review or procedure approval.

    Key Takeaways

    What This Wire Is Used For

    Gas-shielded flux-cored wire is commonly selected when the operation needs a balance of deposition rate, arc stability, and mechanical property control. The product description indicates use in high-strength, low-alloy applications and all-position work. That makes it relevant for structural fabrication, repair work, and field maintenance where weld access can change from flat to vertical or overhead.

    Do not assume a product title alone proves procedure compliance. Check the WPS, material group, shielding gas, and required classification. If the job is governed by code or customer requirement, the wire must match the approved filler metal family and the documented process.

    Check, Inspect, Verify Before Use

    Troubleshooting and Support

    If the wire does not weld as expected, isolate the problem before changing settings repeatedly.

    If a problem continues after these checks, compare the job setup against a known-good feeder, gun, and gas delivery system. That helps separate wire issues from equipment issues. When the exact wire qualification is unclear, set the classification as Unknown (Verify) and obtain the supplier data sheet before release to production.

    Product and Parts Notes

    This item is sold as a Lincoln Electric wire on a 33 lb plastic spool. The plastic spool format is common for feeder use, but the feeder spindle and brake setup still need to be verified against your equipment. Do not assume every spool adapter, hub, or tension setting will be correct without inspection.

    Important: product details such as exact weld deposit chemistry, diffusible hydrogen level, recommended shielding gas blend, and qualification scope were not fully provided in the source data. Treat those items as Unknown (Verify) until confirmed from the product page, label, or supplier documentation.

    For the source product listing, use the ArcWeld product link provided with this item and confirm the current description before ordering. No compatibility beyond what is explicitly documented should be assumed.

    How to Use WSP Support Pages

    When a WSP lookup page is available, use it as a quick reference to confirm how the wire is categorized in the support catalog and to navigate related items. In this draft, no separate WSP lookup URL was provided, so there is no lookup link to include. If your internal workflow requires a lookup step, treat it as a selection aid only. It does not replace a WPS, PQR, or engineer approval.

    For filler metal comparison, use the WSP filler metal finder only as a starting point for narrowing options. It helps identify candidate wires, but it does not guarantee procedure approval or code acceptance for a specific job.

    Safety Notes

    FAQ

    Is Lincoln ED035417 the right wire for all structural jobs?

    Not automatically. The wire may be suitable for structural and heavy fabrication work, but the WPS and material requirements control final selection. Verify the classification, shielding gas, and qualification status before use.

    Can I use this wire without checking my feeder setup?

    No. Check drive rolls, liner, contact tip size, tension, and spool fit before loading. Wire feeding problems are often equipment-related, not wire-related.

    Does the product title confirm all mechanical properties?

    No. The title alone does not confirm all mechanical properties, diffusible hydrogen values, or code approvals. Those details must be verified from the product data sheet or other controlled documentation.

    Is the 33 lb spool better than smaller spools?

    It can reduce changeovers in higher-volume work, but โ€œbetterโ€ depends on the feeder, job duration, storage control, and electrode handling process. Verify fit and handling requirements first.

    Sources Checked

    Bottom line: Lincoln ED035417 is a production-oriented gas-shielded flux-cored wire, but the buying decision should be based on verified classification, WPS alignment, and machine setup. Treat any missing technical detail as Unknown (Verify) until confirmed from the controlled product data.

    Related Arc Weld Part

    Lincoln ED035417, 0.045" UltraCore 111K3M-H Plus Mig Wire, 33 Lbs. Spool

    Lincoln ED035417, 0.045" UltraCore 111K3M-H Plus Mig Wire, 33 Lbs. Spool

    Lincoln Electric ED035417 UltraCore 111K3M-H Plus is a 0.045 in (1.1 mm) gas-shielded flux-cored wire (FCAW-G) on a 33 lb (15 kg) plastic spool, designed for high-strength, low-alloy applications where you need consistent arc performance, strong mechanical properties, and dependable all-position capability. Itโ€™s commonly selected for structural and heavy fabrication work where procedure control and toughness matte…

    View at Arc Weld Store

    Related Weld Support Guides

  • Miller 263348 Welding Gloves, 3D, Wing, 11In, White/Blue, Pack of (1 Pair): Replacement Part Breakdown

    This draft is a practical buyer guide for the Miller 263348 Welding Gloves, 3D, Wing, 11In, White/Blue, Pack of (1 Pair). Use it as a support and purchasing reference when you are matching a glove set for welding work, maintenance tasks, or general hot-work handling. The product reference in the registry is the ASIN-linked item B00I4Z44RS. Any field not confirmed in the provided source should be treated as Unknown (Verify).

    Key Takeaways

    • Use the product listing as the primary reference before you order replacements or duplicates.
    • Verify fit, cuff style, seam condition, and heat exposure needs against your job task.
    • Do not assume the listing covers every welding process or every shop condition.
    • If a glove is being replaced after damage, inspect the cause of failure first so the same issue does not repeat.

    What This Product Reference Tells You

    The provided item name identifies a pair of welding gloves in a 3D wing style, 11 in. length, white and blue colorway. The registry does not confirm material makeup, reinforcement pattern, liner details, stitch type, or heat rating. Treat those fields as Unknown (Verify) until you confirm them from the product page or packaging.

    For buyers and support teams, that means the first step is not just to order a replacement. It is to compare the glove against the task, the current wear pattern, and the actual work environment. A glove can be the wrong choice even when it matches the basic size and shape on paper.

    Check, Inspect, Verify

    Use this sequence before you issue the glove to a welder or maintenance tech:

    1. Check the task: Determine whether the glove will be used for MIG, TIG, stick, grinding, torch handling, or general hot work. If the process is not confirmed, mark it Unknown (Verify).
    2. Inspect the fit area: Confirm hand size, finger reach, cuff clearance, and how the glove interfaces with jacket sleeves or gauntlets.
    3. Verify coverage needs: An 11 in. glove may be suitable for some hand and wrist protection needs, but do not assume it is enough for every spark, slag, or splash exposure.
    4. Inspect construction: Look for loose stitching, worn palms, seam separation, heat damage, hardening, and contamination from oil or grinding residue.
    5. Verify replacement timing: Replace gloves when insulation, dexterity, or seam integrity is degraded. Do not wait for a full failure.

    Troubleshooting and Support Notes

    If the glove is not performing as expected, isolate the failure mode.

    • Problem: Reduced dexterity. Check whether the glove is too large, too stiff, or contaminated. Verify that the task does not require a thinner glove style.
    • Problem: Premature seam failure. Inspect whether the glove is being used beyond its intended duty or exposed to repeated flexing, abrasion, or sharp edges.
    • Problem: Heat discomfort. Verify whether the work produces more heat, spatter, or contact exposure than the glove can manage. Do not use comfort alone as the selection rule.
    • Problem: Wet or oily handling issues. Inspect the work area for contamination. Cleaning the glove may not restore safe performance if the structure is already degraded.

    When support teams handle glove complaints, document the task, the failure location, and the wear timeline. That record helps determine whether the issue is product selection, process change, or operator misuse.

    Product and Parts Breakdown

    This item is listed as a pair of welding gloves. No replacement sub-parts are confirmed in the provided source. For this reason, any breakdown beyond the glove pair itself is Unknown (Verify).

    • Primary item: Welding glove pair
    • Style: 3D wing, as stated in the product name
    • Length: 11 in., as stated in the product name
    • Color: White/Blue, as stated in the product name
    • Material details: Unknown (Verify)
    • Stitching and reinforcement: Unknown (Verify)
    • Heat and cut performance claims: Unknown (Verify)

    If you are building a purchasing record, keep the glove name, ASIN reference, and observed wear condition together. That makes it easier to reorder the same item or to replace it with a better-matched option later.

    Buyer Support Checklist

    • Check the work process first.
    • Inspect the hand and wrist coverage needed for the actual task.
    • Verify whether the glove can be worn with sleeves, cuffs, or other PPE.
    • Confirm whether the wearer needs dexterity for small parts, torch adjustments, or clamp handling.
    • Review previous glove failures for burn-through, seam split, or abrasion.

    Safety Notes

    Welding gloves are PPE, not universal protection. Match them to the hazard. Inspect before use. Remove from service if they are burned through, stiffened, torn, or contaminated in a way that cannot be corrected. For hot work, make sure the rest of the PPE set is also appropriate, including jacket, sleeves, face protection, and footwear.

    Do not assume any glove description confirms suitability for a specific code requirement, procedure, or site rule. If you need a compliance answer, verify it against your site safety program and the manufacturer documentation.

    FAQ

    Is this glove pair confirmed for a specific welding process?

    No. The provided source does not confirm process-specific approval. Treat process compatibility as Unknown (Verify).

    Can I rely on the listed 11 in. length for full forearm protection?

    No. An 11 in. length does not automatically mean full forearm protection for every task. Verify the actual exposure, sleeve overlap, and job hazard before use.

    Are the material and heat-resistance details confirmed?

    No. The provided source does not confirm those technical details. Use Unknown (Verify) until you check the product page or packaging.

    What should I inspect before replacing a worn pair?

    Inspect seams, palm wear, burn marks, stiffness, contamination, and fit. If the same failure repeats, verify whether the task or glove selection needs to change.

    Sources Checked

    • Provided ASIN registry entry for Miller 263348 Welding Gloves, 3D, Wing, 11In, White/Blue, Pack of (1 Pair), ASIN B00I4Z44RS
    • Provided product name and task metadata in the request

    Any technical detail not confirmed in those sources remains Unknown (Verify).

    Matched Replacement Option

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

  • Washington Alloy 2 Lb. Spool Mig Welding Wire 308L Stainless Steel (.023 X 2lb.): Replacement Part Breakdown

    Washington Alloy 2 Lb. Spool Mig Welding Wire 308L Stainless Steel (.023 x 2 lb.) is a small-format stainless MIG wire option used in support and maintenance workflows where a compact spool makes sense. For buyers and welders, the important part is not the spool label alone. The wire has to match the base metal, shielding gas, feeder setup, and the actual welding procedure in use. If any one of those points is off, the result is usually birdnesting, unstable arc starts, excessive spatter, or a weld that does not meet job requirements.

    This breakdown focuses on what to verify before ordering or loading the spool, what to inspect during setup, and how to troubleshoot common issues without guessing at compatibility. Product-specific procedure approval is always governed by the job spec or WPS. If the procedure is not documented, treat the selection as a starting point and verify before use.

    Key Takeaways

    • ER308L stainless MIG wire is commonly evaluated as a starting point for austenitic stainless work, but procedure approval depends on the job.
    • .023 in wire is a small-diameter option; feeder condition and contact tip size matter more at this scale.
    • A 2 lb spool is useful for short runs, repair work, and limited feeder capacity, but verify your feeder can handle the spool format.
    • Do not assume stainless wire will run like carbon steel wire. Cleanliness, gas coverage, and liner condition are critical.
    • Unknown (Verify) on exact machine compatibility, shielding gas mix, and all procedure limits unless your WPS or equipment manual confirms them.

    What This Wire Breakdown Means for the Shop

    For maintenance buyers, replacement-part breakdown starts with function. This spool is a consumable, not a standalone solution. The wire only performs correctly when the feeder, drive rolls, gun liner, contact tip, shielding gas, and workpiece prep are in line with stainless requirements. If the shop uses multiple wire types, label storage and feeder changeover steps clearly to prevent cross-contamination.

    Check: confirm the wire designation, diameter, and spool size before it goes into the crib or on the machine. If the printout, bin tag, and package do not match, stop and verify. Inspect: the spool for shipping damage, loose wraps, and contamination. Verify: the feeder, tip size, and liner are suitable for a .023 in stainless wire installation.

    Setup and Troubleshooting Support

    Stainless wire problems usually show up fast. If the arc is unstable or the wire feed feels rough, work through the system in order rather than changing multiple variables at once.

    Check the feeder first

    • Check: drive roll type and tension. Over-tight drive pressure can deform smaller wire.
    • Inspect: the inlet and outlet guides for burrs, dust, or metal fines.
    • Verify: the wire path is clean from spool hub to contact tip.

    Check the gun consumables

    • Check: contact tip wear, heat damage, and tip size.
    • Inspect: liner condition if feed resistance is present.
    • Verify: the gun neck and torch routing do not create sharp bends that can cause feed instability.

    Check the weld environment

    • Check: shielding gas supply and flow at the machine and gun end.
    • Inspect: for drafts, fan turbulence, or poor nozzle coverage.
    • Verify: the base metal is clean and free of oil, rust, paint, and carbon steel transfer.

    If porosity appears, do not assume the wire is defective. First verify gas coverage, nozzle cleanliness, and surface prep. If the wire hesitates or birdnests, inspect the drive system, liner, and tip condition before changing feed speed or voltage. If burnback occurs, verify stickout, contact tip wear, and feed consistency. These are routine support checks, not guarantees of correction.

    Replacement Part Considerations

    As a replacement item, the spool should be matched against the feeder and the application, not just the product description. The most common support questions are about spool mounting, feed performance, and whether the wire is appropriate for a given stainless job. Without the machine model and WPS, those details remain Unknown (Verify).

    Check: the spool hub, drive roll groove, and gun liner diameter handling for .023 in wire. Inspect: whether the feeder has been used with carbon steel wire previously and clean any contamination. Verify: the internal job requirements before putting stainless wire into production use.

    For team reference on stainless filler selection, use the Weld Support Parts article Best MIG Wire for Stainless Steel (ER308L vs ER309L) as a selection starting point. It is not a procedure approval document.

    Related Support References

    If your prep process includes surface cleaning before stainless welding, the article Stainless Steel Wire Wheel Brush for Welding Surface Prep: 8mm Rotary Drill Attachment may help with prep planning. For alternate stainless wire direction, review Best Flux Core Wire for Stainless Steel Welding. For non-stainless comparison, see Aluminum ER 5554 3/64โ€ณ X 5lb. MIG Welding Wire Spool By Washington Alloy โ€“ Weld Support Parts Blog.

    Safety Notes

    • Use proper eye, hand, and body protection when loading wire and setting up the feeder.
    • Do not touch live electrical components or feed mechanisms without following lockout or machine shutdown procedures.
    • Stainless welding can generate fumes and metal particulates. Use local exhaust ventilation and follow site safety rules.
    • Keep wire and consumables clean. Do not store stainless wire where it can pick up carbon steel dust or grinding debris.

    FAQ

    Is this wire automatically approved for stainless steel repair work?
    No. It may be a candidate, but approval depends on the WPS, base metal, and service requirements. Verify before use.

    Can .023 in wire run in any MIG feeder?
    No. Feeder condition, drive roll setup, liner condition, and tip sizing all matter. Machine-specific fit is Unknown (Verify) unless confirmed by the equipment manual.

    What should I check first if the arc is erratic?
    Check the contact tip, liner, drive roll pressure, and shielding gas flow. Inspect the spool for feed damage and verify the wire path is clean.

    Is the 2 lb spool format better for production?
    Not necessarily. It is often more practical for short jobs, repairs, and limited feeder capacity. Production suitability depends on job volume and feeder setup.

    Sources Checked

    • Provided Amazon ASIN registry entry: B081XDF1LM
    • Provided product title and target keyword
    • Allowed internal Weld Support Parts links listed in the task

    Product link for reference:

    No products found.

    Disclosure: As an Amazon Associate, Weld Support Parts may earn from qualifying purchases.

    Related Weld Support Guides

  • You Never Look at a Handrail the Same Way Again: How Welding Changes the Way You See the Built World

    You Never Look at a Handrail the Same Way Again: How Welding Changes the Way You See the Built World

    Beyond the Booth

    Learn to weld and a handrail stops being just a handrail.

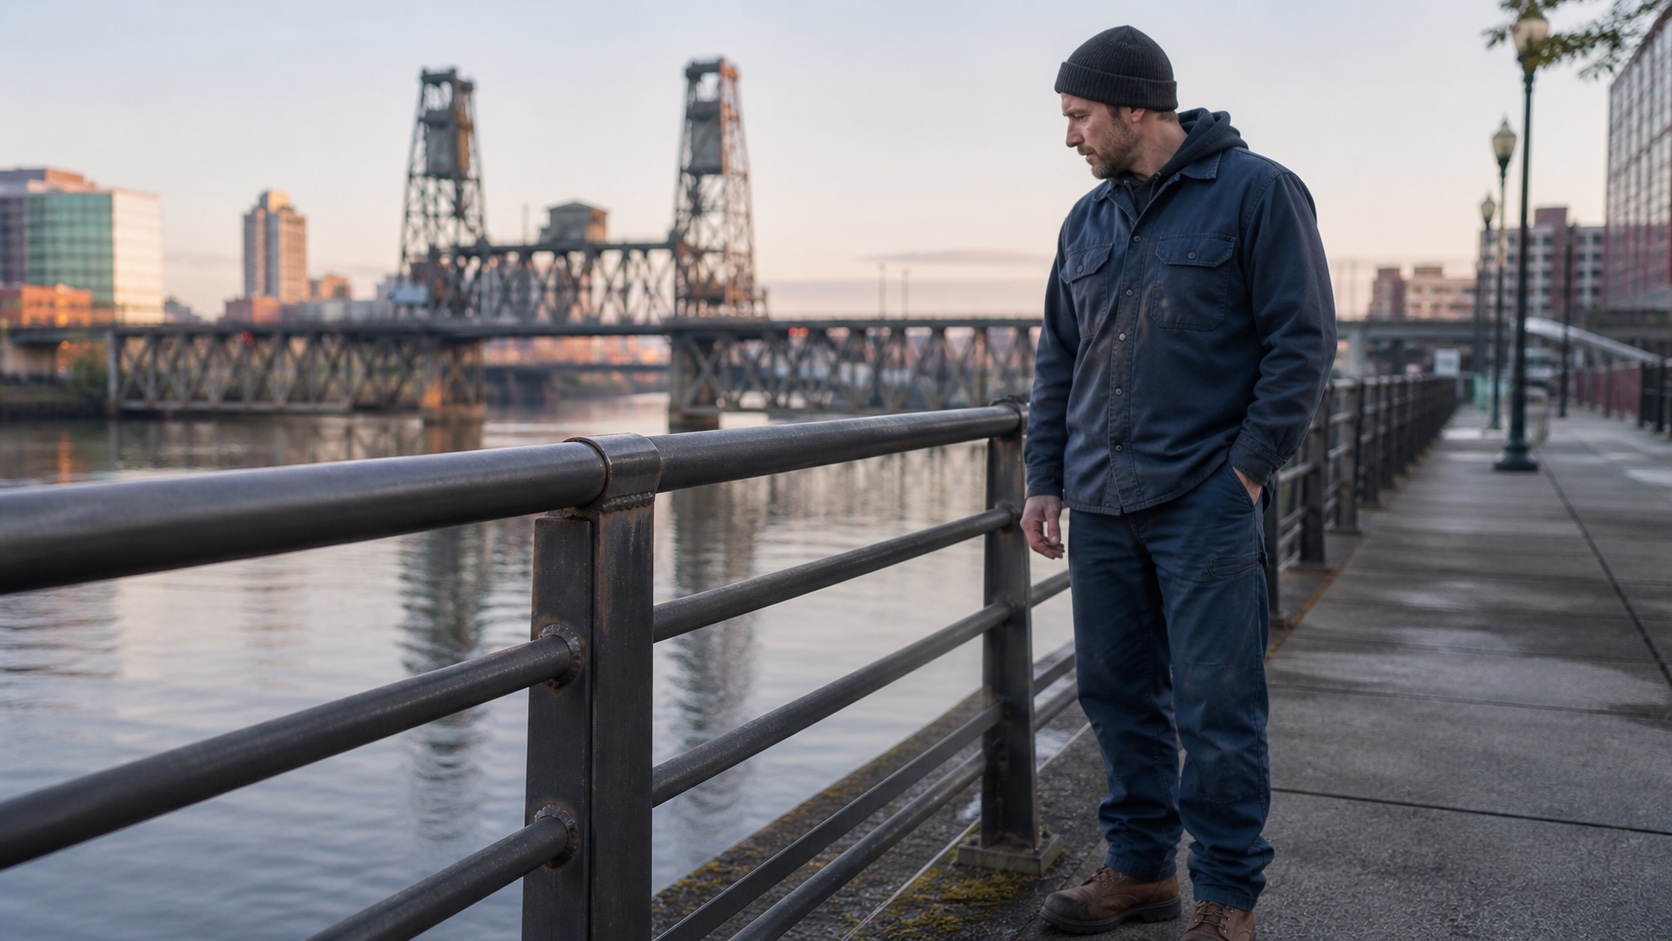
    You notice where the posts meet the top rail. You wonder how the fabricator reached the back side. You catch the places where the finish changes around a repair. A trailer passes on the highway and, for half a second, you are looking at the frame instead of the load. A gate closes and your eyes follow the joints before your brain remembers that you are supposed to be off the clock.

    That habit is one of the quiet changes the trade makes in a person. Welding teaches the hands, but it also trains attention. The built world starts leaving clues everywhere.

    The Trade Teaches a Second Way of Looking

    Most people see an object by what it does. A railing keeps people back. A cart carries material. A staircase gets someone to the next level. A welder can see the same purpose while also noticing the choices that made the object possible.

    Was it built in sections or assembled in place? Where could a torch, gun, or electrode actually reach? Which joints were designed to disappear under paint, and which ones were left visible? What had to be held square before anything permanent happened?

    This is not a superpower and it is not reserved for veterans. It starts early. Once an apprentice has fought a gap, chased distortion, cleaned mill scale, or tried to position a part that looked simple on paper, ordinary metalwork stops looking accidental. Even a plain bracket carries a sequence of decisions.

    Curiosity Is Not Condemnation

    There is an important line between noticing a weld and judging a structure from the sidewalk. Surface appearance can invite questions, but it does not reveal the entire joint, the design requirements, the procedure, the material, or what testing may have been performed.

    The Federal Highway Administration’s Bridge Welding Reference Manual treats welded construction as a system involving design, fabrication, constructability, quality control, quality assurance, and inspection. The agency’s guidance on ultrasonic testing also explains that sound-based examination can detect internal conditions such as cracks, porosity, and lack of fusion. In other words, a glance is not an inspection report.

    The better habit is curiosity without the instant verdict. Ask what the builder may have been solving. Notice the access, the joint, and the finish. Respect the fact that important work is rarely understood from one angle.

    Ordinary Objects Become Small Lessons

    A city block can turn into an open-air shop notebook. Handrails show repetition and alignment. Gates reveal how a frame carries its own weight after the clamps come off. Restaurant furniture puts fit and finish inches from the customer. Utility trailers show what happens when fabrication has to survive weather, movement, loading, and years of use.

    Public art can be even more interesting. The finished shape may look effortless, but a welder sees the problem hiding behind it: how to support an awkward form, how to join curved pieces, how to make the structure strong without letting the structure swallow the idea.

    The range is part of the appeal. The American Welding Society’s mobile education program points to welding across infrastructure, agriculture, heavy equipment, and manufacturing. Those are not abstract sectors when you know the trade. They are places full of joints, sequences, repairs, and people whose work is holding up somebody else’s day.

    You Start Reading the Choices

    The most interesting part is not sorting every weld into good or bad. It is learning to read the decisions around it.

    • Access: Could the builder get into position, or did the design make a simple joint difficult?
    • Sequence: Which pieces likely had to be joined first, and how might heat have moved the assembly?
    • Fit: Where did parts meet cleanly, and where did the fabricator have to solve a mismatch?
    • Finish: Was the weld meant to remain part of the visual language, or disappear beneath grinding, coating, or trim?
    • Service: Does the object live a quiet indoor life, or take vibration, weather, impact, and constant handling?

    Those questions make the world more interesting. They also make a person less casual about the labor inside familiar objects.

    The Habit Follows You Off the Clock

    Welders joke about checking beads in parking lots, underneath restaurant tables, or along the trailer at the gas pump. The joke lands because the habit is real. Once the eye has been trained to see how separate pieces become one useful thing, it does not shut down neatly at the time clock.

    That can be a good thing. The habit connects the trade to everyday life. It turns a walk across a bridge into a reminder that someone detailed it, someone fitted it, someone welded it, and someone inspected it. It replaces the idea of a faceless “built environment” with thousands of specific acts of skill.

    It can also build humility. The closer you look at work outside your own lane, the easier it is to see how much you do not know about the constraints behind it. Respect grows when attention is paired with questions instead of swagger.

    The World Is Full of Somebody’s Work

    There is a lot of invisible labor in plain sight. A clean rail in a public building does not announce the hours spent measuring, cutting, fitting, controlling heat, finishing corners, and making repeated sections agree with one another. It simply does its job.

    Knowing the trade makes that silence easier to hear. You may never know the fabricator’s name, but you can recognize that a person was there. That awareness is bigger than welding technique. It is a way of seeing craftsmanship, responsibility, and human effort in the things everybody else walks past.

    Arc Life is about that wider life around the arcโ€”the habits, observations, and shared language welders carry beyond the booth. Read more about the idea on About Arc Life, or see the current Arc Life collection.

    Community question: What everyday object do you inspect without meaning to?


    Sources Checked

  • More posts

    Watch with Prime Video